

Injection Molding
Tooling and molding for your repeat plastic parts.
From prototype to production, coordinated manufacturing solutions for your custom parts.
View All Services →
Precision parts for your tight tolerances and complex geometry.
Tooling and molding for your repeat plastic parts.

Metal casting options for your part and production volume.

Cutting, forming and welding for your fabricated parts.

Custom profiles for your section, length and finish requirements.

Finishes for your appearance, corrosion and wear requirements.

Sub-assemblies and final builds for your production program.

Production tooling built around your process and volume.

Prototype parts to check fit, function and design.
DFM, process planning and production support for your project.
Inspection, documentation, inventory and delivery planning for your program.
Choose air- or liquid-cooling components around your thermal and mechanical requirements.

Manufacturing support for your cold plates, manifolds and cooling assemblies.

Find components for your power electronics, energy, laser and telecom application.

Components for your electronic systems.
Start with your functional and quality requirements.
Build around your operating environment.
From prototype to production, review material performance, manufacturability and cost for your part.
Review grade, temper and finish for your metal parts.
 AluminumStrength, weight and machining›
 Stainless SteelCorrosion and finish requirements›
 Carbon & Alloy SteelDiscuss grade and heat treatment›
 Tool SteelDiscuss tooling and wear needs›
 TitaniumReview grade and part geometry›
 Copper & BrassDiscuss conductivity and machining›
Match your polymer to function, process and environment.
 ABSReview enclosure and molding needs›
 Polycarbonate (PC)Discuss clarity and impact needs›
 Nylon (PA)Review moisture and wear conditions›
 POM / AcetalReview fit and sliding features›
 PEEKDiscuss operating conditions›
 PTFEReview friction and chemical exposure›
 ULTEM / PEIDiscuss thermal and electrical needs›
Confirm grade availability and application requirements.
 Silicone / LSRDiscuss flexible component needs›
 TPU / TPEReview flexibility and processing›
 EPDMReview weathering and chemical exposure.›
 NBRReview oil and fuel exposure.›
 FKMReview temperature and chemical exposure.›
 G10 / FR4Review insulation and laminate needs›
 CompositesReview stiffness, weight and laminate.›Customer-Specified MaterialsConfirm your grade and requirements.›Other Specialty MaterialsDiscuss your application and grade.›
Practical guidance for your part geometry and material decisions.
Prepare your process, budget and sourcing questions.
Build your knowledge before production.
Learn who we are and how we operate.
Find our U.S. support team or start a conversation.
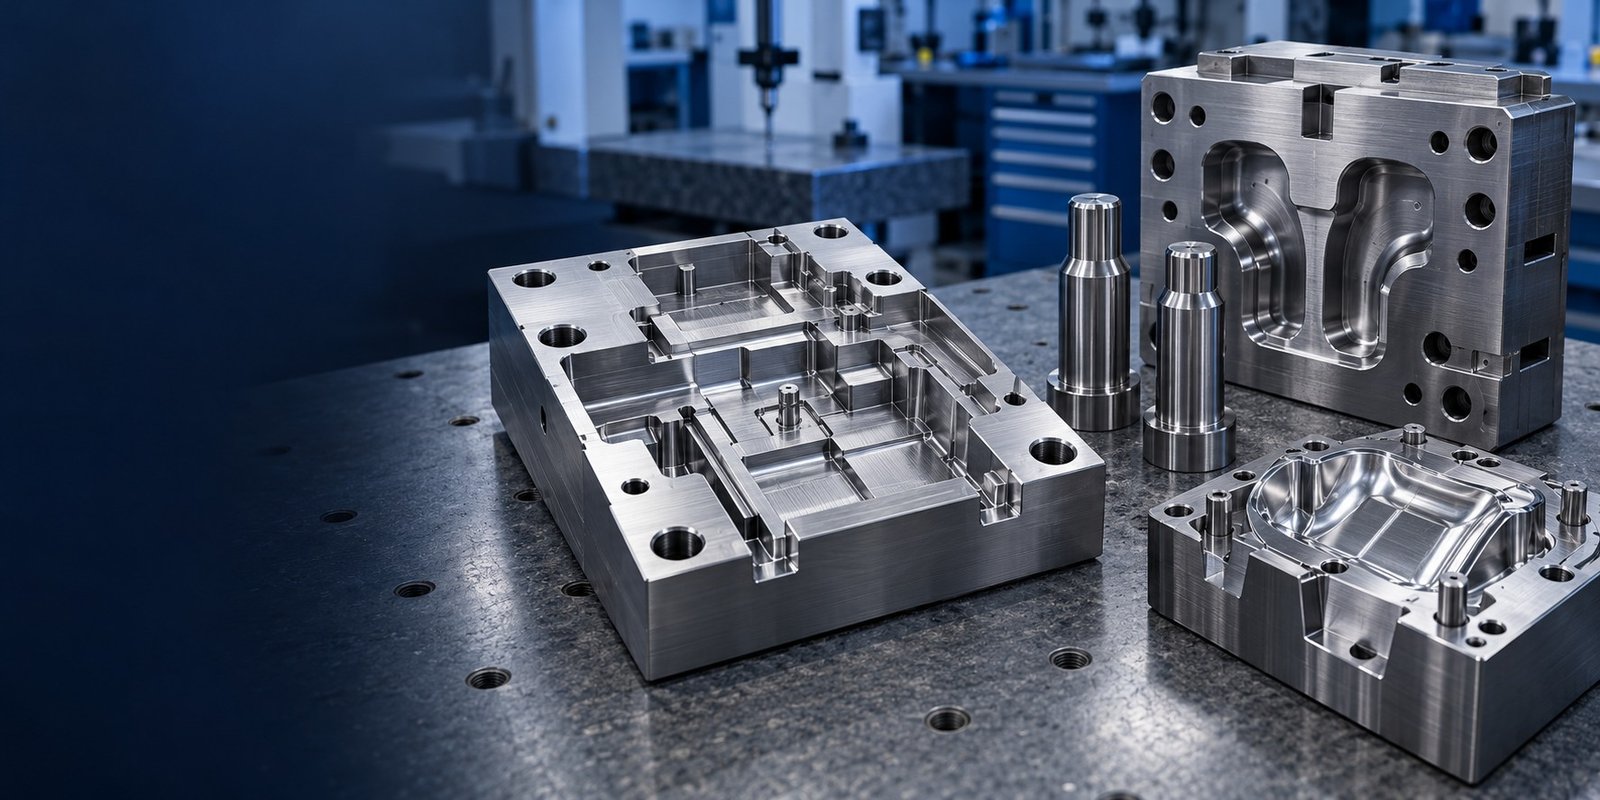
Match wear, impact and heat exposure to the grade you specify. Plan your stock condition, heat-treatment route and final-fit inspection before the first cut.
Tool steel is a family of materials. Choose against the failure mode of your die, punch, mold insert or wear component, then define the condition on your drawing.
Cold work · hot work · plastic molds · impact, high-speed and powder grades.
Supplied hardness and final working hardness are separate requirements. A grade name does not fix either value.
| Average wt.% | A2 / K305 | D2 / K110 | H13 / W302 |
|---|---|---|---|
| C | 1.00 | 1.55 | 0.39 |
| Cr | 5.20 | 11.30 | 5.20 |
| Mo | 1.10 | 0.75 | 1.40 |
| V | 0.25 | 0.75 | 0.95 |
Selected BÖHLER products, producer average composition, not standard limits or LK lot analysis. Listed product data refer to long products; confirm your actual form.
| Your decision | What to define |
|---|---|
| Annealed stock | Plan roughing, remaining stock and the required later treatment. |
| Prehardened stock | Confirm delivered condition, section and machining requirements. |
| Final working state | Define hardness test locations, critical fit and inspection after all operations. |
Producer average wt.% · common axis 0–12%
Composition comparison only. Chromium percentage is not a wear, toughness or corrosion rating.
BÖHLER K305 ↗ K110 ↗ W302 ISOBLOC ↗
| Grade | European comparison index | Your selection question |
|---|---|---|
| A2 | 1.2363 / X100CrMoV5 | Cold-work dies, punches and wear inserts; compare impact and abrasion. |
| D2 | 1.2379 / X153CrMoV12 | Abrasion-focused dies and wear tooling; review edge support and finishing. |
| O1 | 1.2510 / 100MnCrW4 | Gauges and general cold-work tooling; allow for the specified hardening route. |
| S7 | No single EN substitute assigned | Impact-loaded tooling; confirm the actual supplier grade and specification. |
| H13 | 1.2344 / X40CrMoV5-1 | Hot-work dies and inserts; specify thermal duty and melting route. |
| P20 | Common reference:1.2311 | Plastic molds and inserts; distinguish sulfur and nickel modifications. |
| M2 | Common reference:1.3343 / HS6-5-2C | High-speed steel tooling; confirm machining, finishing and acceptance scope. |
| DC53 | Daido brand;no direct generic EN equivalent | Brand-specific cold-work tooling; do not relabel D2 or SKD11 as DC53. |
Comparison names support your material review. Confirm product standard, chemistry, delivery state, section and your approval before substitution. Availability and manufacturing scope are confirmed for your drawing.
For your O2, D3, D6, H10, H11, 1.2367, S1, 1.2312, 1.2738, 1.2083, NAK80, 1.2316, M35, M42, T1, A11, Vanadis 4 Extra or ASP 2023 inquiry, send the complete material designation and producer document. Trade names and standard grades are reviewed separately.
European comparison examples: O2 / 1.2842; H10 / 1.2365; H11 / 1.2343; M35 / 1.3243; M42 / 1.3247. These are candidate references, not automatic replacements.
Other Tool Steel specification review →Compare carbon and alloy steel routes for your finished components. These grades are not automatic substitutes for tool steel; confirm the application and material approval for your drawing.
Low-carbon steel
For your 1018 steel machining review, identify datum faces, bore fits and any welded or plated features. Cold-drawn and hot-rolled conditions must be specified separately.
General machined blocks, collars and fixture parts.
Specify product form and supplied condition.
Confirm final geometry and required records.
No universal EN substitute: compare the actual low-carbon steel specification.
Review tool access, datums, threads, burr removal and finish before choosing your setup. General machined blocks, collars and fixture parts.
Identify the functional datum scheme.
Agree setups and access to critical features.
Inspect in the specified final condition.
No universal EN substitute: compare the actual low-carbon steel specification.
State whether material is supplied cold drawn or hot rolled; do not assume one strength from the grade name.
Specify stock form and supplied condition.
Agree the required condition and responsible party.
Inspect functional features after the full route.
No universal EN substitute: compare the actual low-carbon steel specification.
Protect functional bores and threads when specifying coating thickness.
Grade, product standard, lot and condition.
Datums, dimensions and inspection state.
Agree document type and scope at inquiry.
No universal EN substitute: compare the actual low-carbon steel specification.
Low-carbon steel
For your 1020 steel machining inquiry, define stock form, fit and joining requirements. Confirm permitted substitutes against the drawing.
Clevises, pins and general machined components.
Specify product form and supplied condition.
Confirm final geometry and required records.
No automatic EN equivalence; compare specified chemistry and product form.
Review tool access, datums, threads, burr removal and finish before choosing your setup. Clevises, pins and general machined components.
Identify the functional datum scheme.
Agree setups and access to critical features.
Inspect in the specified final condition.
No automatic EN equivalence; compare specified chemistry and product form.
Specify the incoming state and any required treatment; do not infer finished properties from carbon content.
Specify stock form and supplied condition.
Agree the required condition and responsible party.
Inspect functional features after the full route.
No automatic EN equivalence; compare specified chemistry and product form.
Identify surface protection, masked faces and dimensional acceptance after finishing.
Grade, product standard, lot and condition.
Datums, dimensions and inspection state.
Agree document type and scope at inquiry.
No automatic EN equivalence; compare specified chemistry and product form.
Medium-carbon steel
For your 1045 steel machining project, connect shaft journals, keyways and final hardness to the complete manufacturing sequence.
Shafts, rollers and pins with defined final requirements.
Specify product form and supplied condition.
Confirm final geometry and required records.
Compare C45 / C45E: EN 1.0503 / 1.1191 are similar-designation references, not blanket substitutes.
Review tool access, datums, threads, burr removal and finish before choosing your setup. Shafts, rollers and pins with defined final requirements.
Identify the functional datum scheme.
Agree setups and access to critical features.
Inspect in the specified final condition.
Compare C45 / C45E: EN 1.0503 / 1.1191 are similar-designation references, not blanket substitutes.
Identify hardening method, treatment locations, final hardness and machining allowance before release.
Specify stock form and supplied condition.
Agree the required condition and responsible party.
Inspect functional features after the full route.
Compare C45 / C45E: EN 1.0503 / 1.1191 are similar-designation references, not blanket substitutes.
Mark ground journals, surface texture and protected areas for your final fit.
Grade, product standard, lot and condition.
Datums, dimensions and inspection state.
Agree document type and scope at inquiry.
Compare C45 / C45E: EN 1.0503 / 1.1191 are similar-designation references, not blanket substitutes.
Carbon structural steel
For your A36 steel machining and fabrication review, connect the plate thickness, joint details and mounting faces to the final assembly.
Welded bases, gussets and support plates.
Specify product form and supplied condition.
Confirm final geometry and required records.
Review EN structural grades such as S235JR against the actual requirements; A36 is not automatically equivalent.
Review tool access, datums, threads, burr removal and finish before choosing your setup. Welded bases, gussets and support plates.
Identify the functional datum scheme.
Agree setups and access to critical features.
Inspect in the specified final condition.
Review EN structural grades such as S235JR against the actual requirements; A36 is not automatically equivalent.
A36 is a structural product specification. Any stress relief or other treatment requires project review.
Specify stock form and supplied condition.
Agree the required condition and responsible party.
Inspect functional features after the full route.
Review EN structural grades such as S235JR against the actual requirements; A36 is not automatically equivalent.
Agree mill-scale removal, coating, mounting-pad protection and flatness in the finished assembly.
Grade, product standard, lot and condition.
Datums, dimensions and inspection state.
Agree document type and scope at inquiry.
Review EN structural grades such as S235JR against the actual requirements; A36 is not automatically equivalent.
Free-machining carbon steel
For your 1215 steel machining inquiry, define turned diameters, thread engagement, burr access and finish. Review joining requirements before selecting a free-machining grade.
Turned spacers, threaded parts and bushings.
Specify product form and supplied condition.
Confirm final geometry and required records.
Compare free-cutting specifications individually; no universal EN substitute is stated.
Review tool access, datums, threads, burr removal and finish before choosing your setup. Turned spacers, threaded parts and bushings.
Identify the functional datum scheme.
Agree setups and access to critical features.
Inspect in the specified final condition.
Compare free-cutting specifications individually; no universal EN substitute is stated.
Do not select a heat-treatment route from machinability alone; agree the required final condition.
Specify stock form and supplied condition.
Agree the required condition and responsible party.
Inspect functional features after the full route.
Compare free-cutting specifications individually; no universal EN substitute is stated.
Specify deburring and coating requirements at intersecting holes and thread runouts.
Grade, product standard, lot and condition.
Datums, dimensions and inspection state.
Agree document type and scope at inquiry.
Compare free-cutting specifications individually; no universal EN substitute is stated.
Leaded free-machining steel
For your 12L14 steel machining project, confirm the lead-containing grade is permitted for your application and market before reviewing turned features.
Precision turned sleeves and standoffs when material approval permits.
Specify product form and supplied condition.
Confirm final geometry and required records.
Review 11SMnPb30 / EN 1.0718 only as a candidate requiring specification and compliance checks.
Review tool access, datums, threads, burr removal and finish before choosing your setup. Precision turned sleeves and standoffs when material approval permits.
Identify the functional datum scheme.
Agree setups and access to critical features.
Inspect in the specified final condition.
Review 11SMnPb30 / EN 1.0718 only as a candidate requiring specification and compliance checks.
Confirm the complete specification and final condition; substitution and joining need review.
Specify stock form and supplied condition.
Agree the required condition and responsible party.
Inspect functional features after the full route.
Review 11SMnPb30 / EN 1.0718 only as a candidate requiring specification and compliance checks.
Agree coating, cleaning and material declaration requirements before ordering.
Grade, product standard, lot and condition.
Datums, dimensions and inspection state.
Agree document type and scope at inquiry.
Review 11SMnPb30 / EN 1.0718 only as a candidate requiring specification and compliance checks.
Chromium-molybdenum alloy steel
For your 4130 steel machining review, identify tube or bar product form, wall thickness, joint geometry and the final condition.
Tubular components, fittings and machined yokes.
Specify product form and supplied condition.
Confirm final geometry and required records.
25CrMo4 / EN 1.7218 is a comparison candidate; verify chemistry, product standard and condition.
Review tool access, datums, threads, burr removal and finish before choosing your setup. Tubular components, fittings and machined yokes.
Identify the functional datum scheme.
Agree setups and access to critical features.
Inspect in the specified final condition.
25CrMo4 / EN 1.7218 is a comparison candidate; verify chemistry, product standard and condition.
Include the complete joining and thermal route in your dimensional acceptance plan.
Specify stock form and supplied condition.
Agree the required condition and responsible party.
Inspect functional features after the full route.
25CrMo4 / EN 1.7218 is a comparison candidate; verify chemistry, product standard and condition.
Review access for cleaning and surface protection around joints and internal passages.
Grade, product standard, lot and condition.
Datums, dimensions and inspection state.
Agree document type and scope at inquiry.
25CrMo4 / EN 1.7218 is a comparison candidate; verify chemistry, product standard and condition.
Chromium-molybdenum alloy steel
For your 4140 steel machining inquiry, separate annealed, prehardened and quenched-and-tempered stock. Mark critical shoulders, threads and bearing journals.
Drive shafts, coupling hubs and loaded mechanical components.
Specify product form and supplied condition.
Confirm final geometry and required records.
Compare 42CrMo4 / EN 1.7225. Only specified variants meet SAE 4140; a similar name does not approve substitution.
Review tool access, datums, threads, burr removal and finish before choosing your setup. Drive shafts, coupling hubs and loaded mechanical components.
Identify the functional datum scheme.
Agree setups and access to critical features.
Inspect in the specified final condition.
Compare 42CrMo4 / EN 1.7225. Only specified variants meet SAE 4140; a similar name does not approve substitution.
Plan your 4140 condition before cutting. Agree incoming material state, heat-treatment route and final inspection stage.
Specify stock form and supplied condition.
Agree the required condition and responsible party.
Inspect functional features after the full route.
Compare 42CrMo4 / EN 1.7225. Only specified variants meet SAE 4140; a similar name does not approve substitution.
Confirm final grinding or machining allowance, surface protection and inspection records.
Grade, product standard, lot and condition.
Datums, dimensions and inspection state.
Agree document type and scope at inquiry.
Compare 42CrMo4 / EN 1.7225. Only specified variants meet SAE 4140; a similar name does not approve substitution.
Nickel-chromium-molybdenum alloy steel
For your 4340 steel machining review, identify load-related features, generous shoulder transitions and the delivery and final conditions.
Axles, shafts and mechanical components with specified heat-treatment requirements.
Specify product form and supplied condition.
Confirm final geometry and required records.
34CrNiMo6 / EN 1.6582 is a comparison candidate, not a direct equivalent.
Review tool access, datums, threads, burr removal and finish before choosing your setup. Axles, shafts and mechanical components with specified heat-treatment requirements.
Identify the functional datum scheme.
Agree setups and access to critical features.
Inspect in the specified final condition.
34CrNiMo6 / EN 1.6582 is a comparison candidate, not a direct equivalent.
Keep the required condition, section size, hardness and acceptance method on the same release.
Specify stock form and supplied condition.
Agree the required condition and responsible party.
Inspect functional features after the full route.
34CrNiMo6 / EN 1.6582 is a comparison candidate, not a direct equivalent.
Agree grinding allowance, surface condition and final dimensional records for critical journals.
Grade, product standard, lot and condition.
Datums, dimensions and inspection state.
Agree document type and scope at inquiry.
34CrNiMo6 / EN 1.6582 is a comparison candidate, not a direct equivalent.
Case-hardening alloy steel
For your 8620 steel machining project, identify functional case-hardened surfaces and separate them from the core and noncritical geometry.
Gears, pins and components with specified case requirements.
Specify product form and supplied condition.
Confirm final geometry and required records.
Review European case-hardening grades individually; 16MnCr5 is not automatically interchangeable with 8620.
Review tool access, datums, threads, burr removal and finish before choosing your setup. Gears, pins and components with specified case requirements.
Identify the functional datum scheme.
Agree setups and access to critical features.
Inspect in the specified final condition.
Review European case-hardening grades individually; 16MnCr5 is not automatically interchangeable with 8620.
Specify case depth, hardness, test locations, masking and final finishing sequence when carburizing is required.
Specify stock form and supplied condition.
Agree the required condition and responsible party.
Inspect functional features after the full route.
Review European case-hardening grades individually; 16MnCr5 is not automatically interchangeable with 8620.
Agree stock allowance and final inspection after the complete treatment and finishing route.
Grade, product standard, lot and condition.
Datums, dimensions and inspection state.
Agree document type and scope at inquiry.
Review European case-hardening grades individually; 16MnCr5 is not automatically interchangeable with 8620.
Additional specified grades
For your unlisted carbon or alloy steel component, provide the complete material designation, product standard and supplied condition. Review the required route from the controlled drawing.
Components requiring a specifically approved carbon or alloy steel grade.
Specify product form and supplied condition.
Confirm final geometry and required records.
Provide any proposed European material number and producer record for comparison; do not approve substitution by name alone.
Review tool access, datums, threads, burr removal and finish before choosing your setup. Components requiring a specifically approved carbon or alloy steel grade.
Identify the functional datum scheme.
Agree setups and access to critical features.
Inspect in the specified final condition.
Provide any proposed European material number and producer record for comparison; do not approve substitution by name alone.
Define treatment and acceptance for the actual grade and geometry. No general treatment recipe applies to every unlisted steel.
Specify stock form and supplied condition.
Agree the required condition and responsible party.
Inspect functional features after the full route.
Provide any proposed European material number and producer record for comparison; do not approve substitution by name alone.
Agree the final surface, dimensional state and material documentation before ordering.
Grade, product standard, lot and condition.
Datums, dimensions and inspection state.
Agree document type and scope at inquiry.
Provide any proposed European material number and producer record for comparison; do not approve substitution by name alone.
Sequence depends on your grade, geometry and specification. No single hardness or tolerance applies to every part.
Select your tooling duty, then review the four decisions that shape your manufacturing route.
A2, D2, O1 and DC53 serve different cold-work requirements. For your punches, die inserts and wear surfaces, compare abrasion, impact, working-edge support and final geometry.
| Your decision | What to define |
|---|---|
| Your fit | Working surfaces, datums and mating features. |
| Your process | Supplied condition, sequence and finishing allowance. |
| Your approval | Final dimensions and required records. |
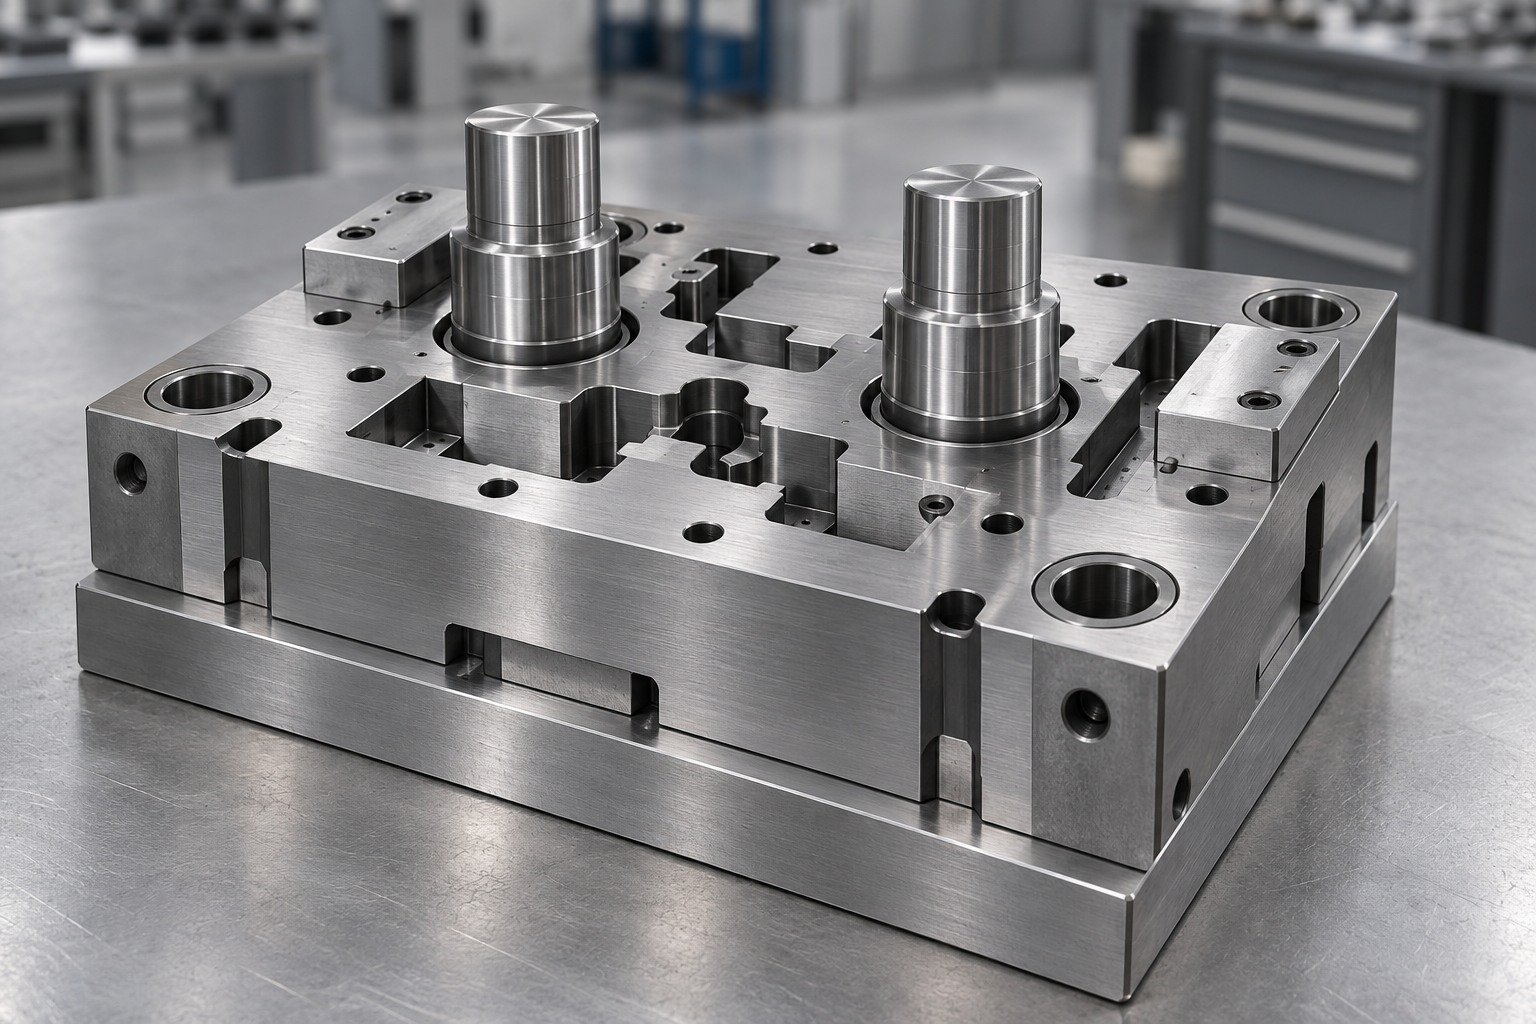
For your tool steel CNC machining review, identify pocket radii, dowel fits, working profiles and clamping surfaces. Reserve access for final machining or grinding where specified.
| Your decision | What to define |
|---|---|
| Your fit | Working surfaces, datums and mating features. |
| Your process | Supplied condition, sequence and finishing allowance. |
| Your approval | Final dimensions and required records. |

Agree the supplied condition, required hardening and tempering, section changes and remaining finish stock. Air hardening does not eliminate dimensional movement.
| Your decision | What to define |
|---|---|
| Your fit | Working surfaces, datums and mating features. |
| Your process | Supplied condition, sequence and finishing allowance. |
| Your approval | Final dimensions and required records. |
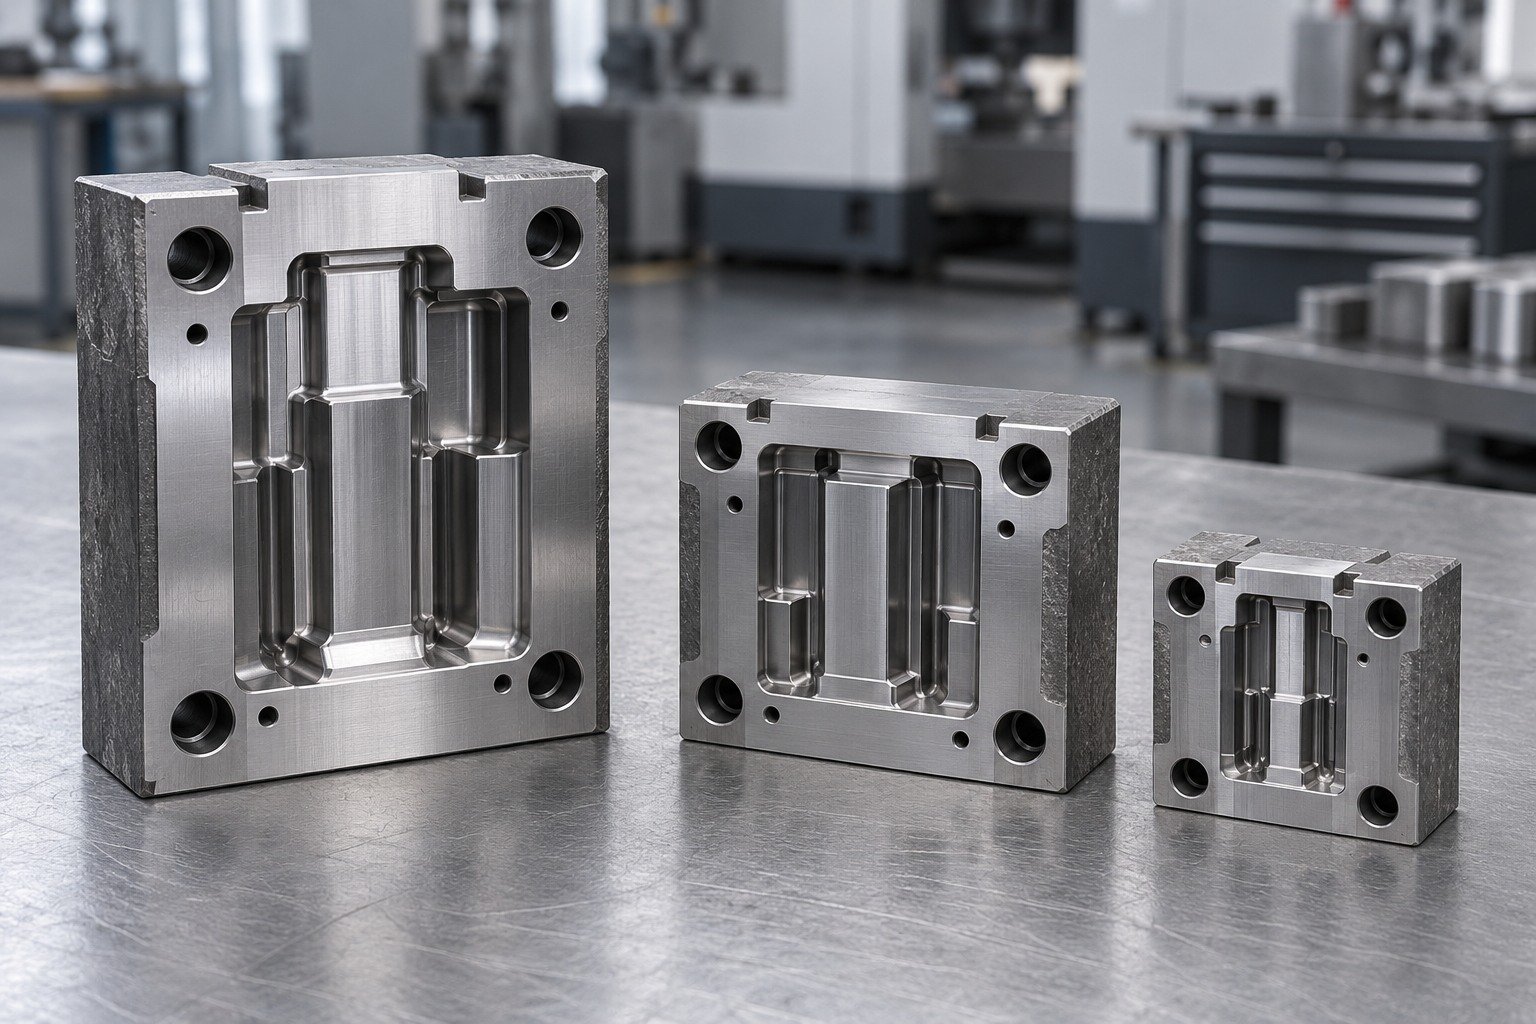
Specify the working profile, datum faces, dowel bores and final measurement state. Keep the material identity and approved drawing revision with the inspection record.
| Your decision | What to define |
|---|---|
| Your fit | Working surfaces, datums and mating features. |
| Your process | Supplied condition, sequence and finishing allowance. |
| Your approval | Final dimensions and required records. |
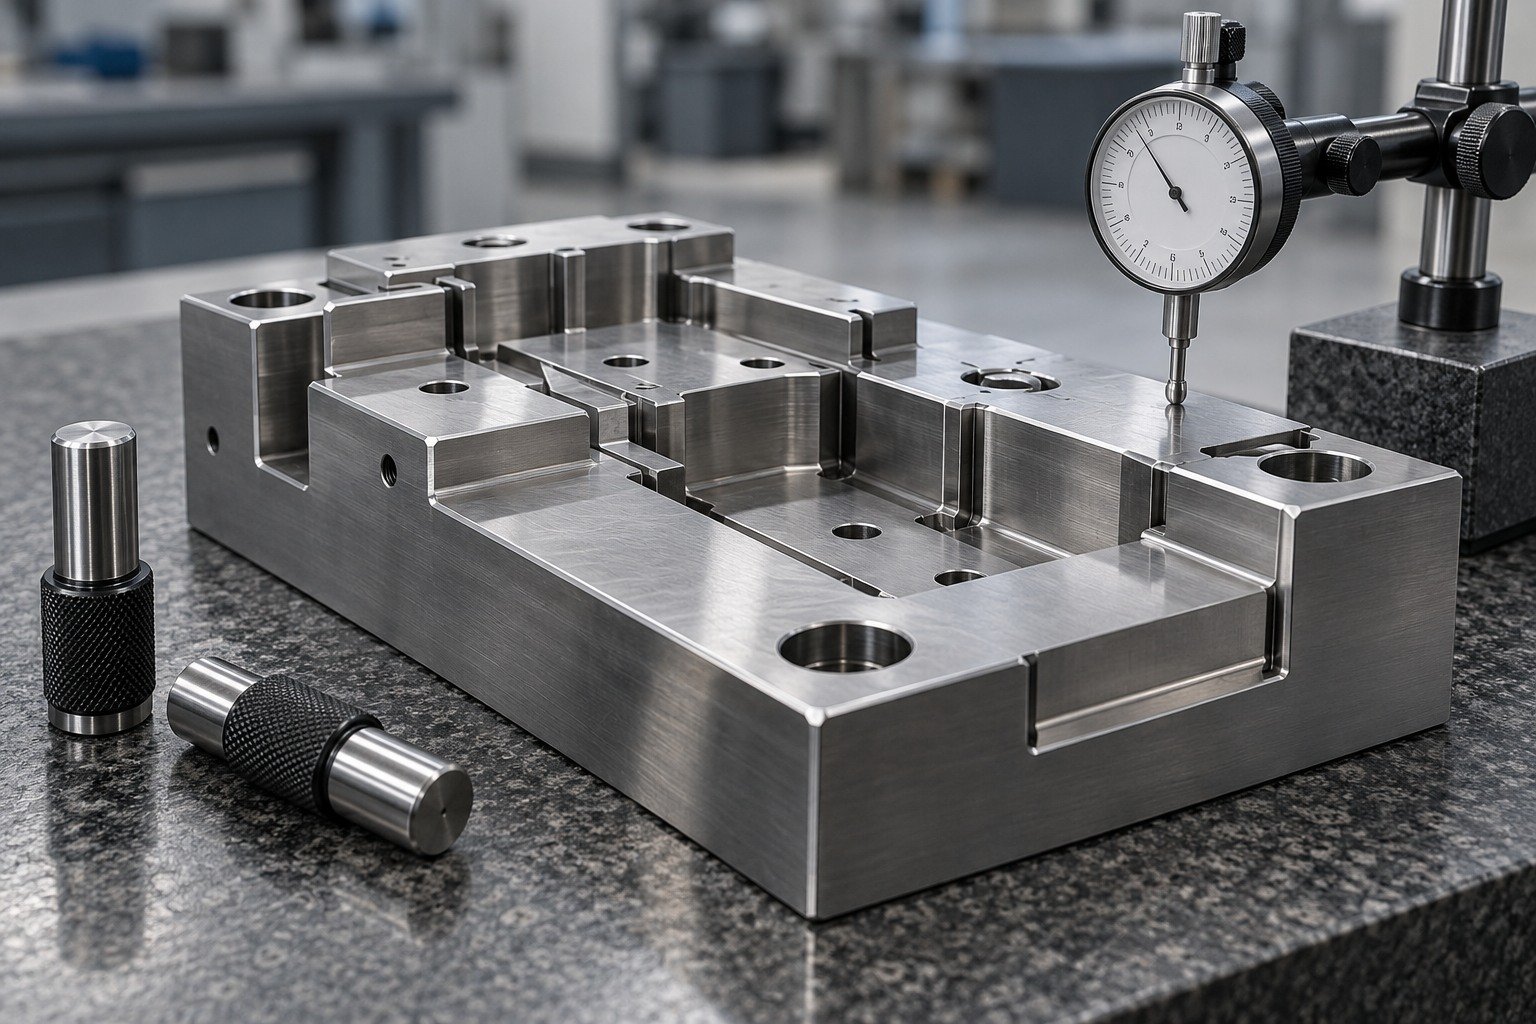
H13 is a starting point for hot-work dies and inserts. Define contact temperature, thermal cycling, loads, cooling geometry and the failure mode you need to address.
| Your decision | What to define |
|---|---|
| Your fit | Working surfaces, datums and mating features. |
| Your process | Supplied condition, sequence and finishing allowance. |
| Your approval | Final dimensions and required records. |
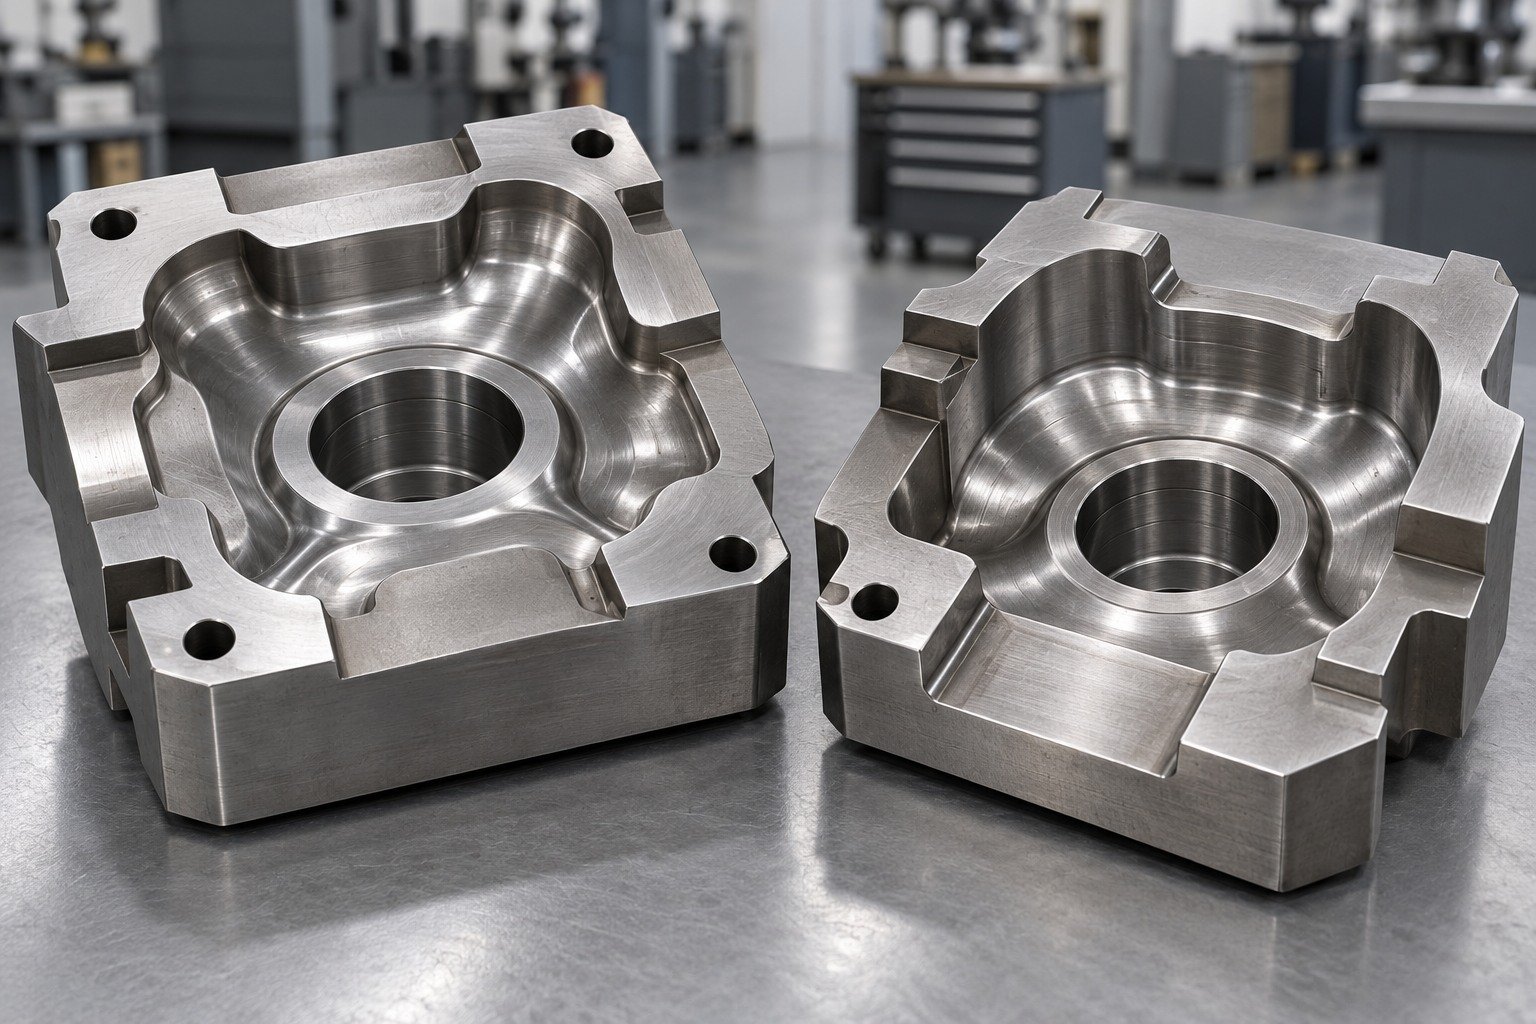
Review cavity access, thick-to-thin transitions, cooling passages and realistic corner radii before programming your insert.
| Your decision | What to define |
|---|---|
| Your fit | Working surfaces, datums and mating features. |
| Your process | Supplied condition, sequence and finishing allowance. |
| Your approval | Final dimensions and required records. |
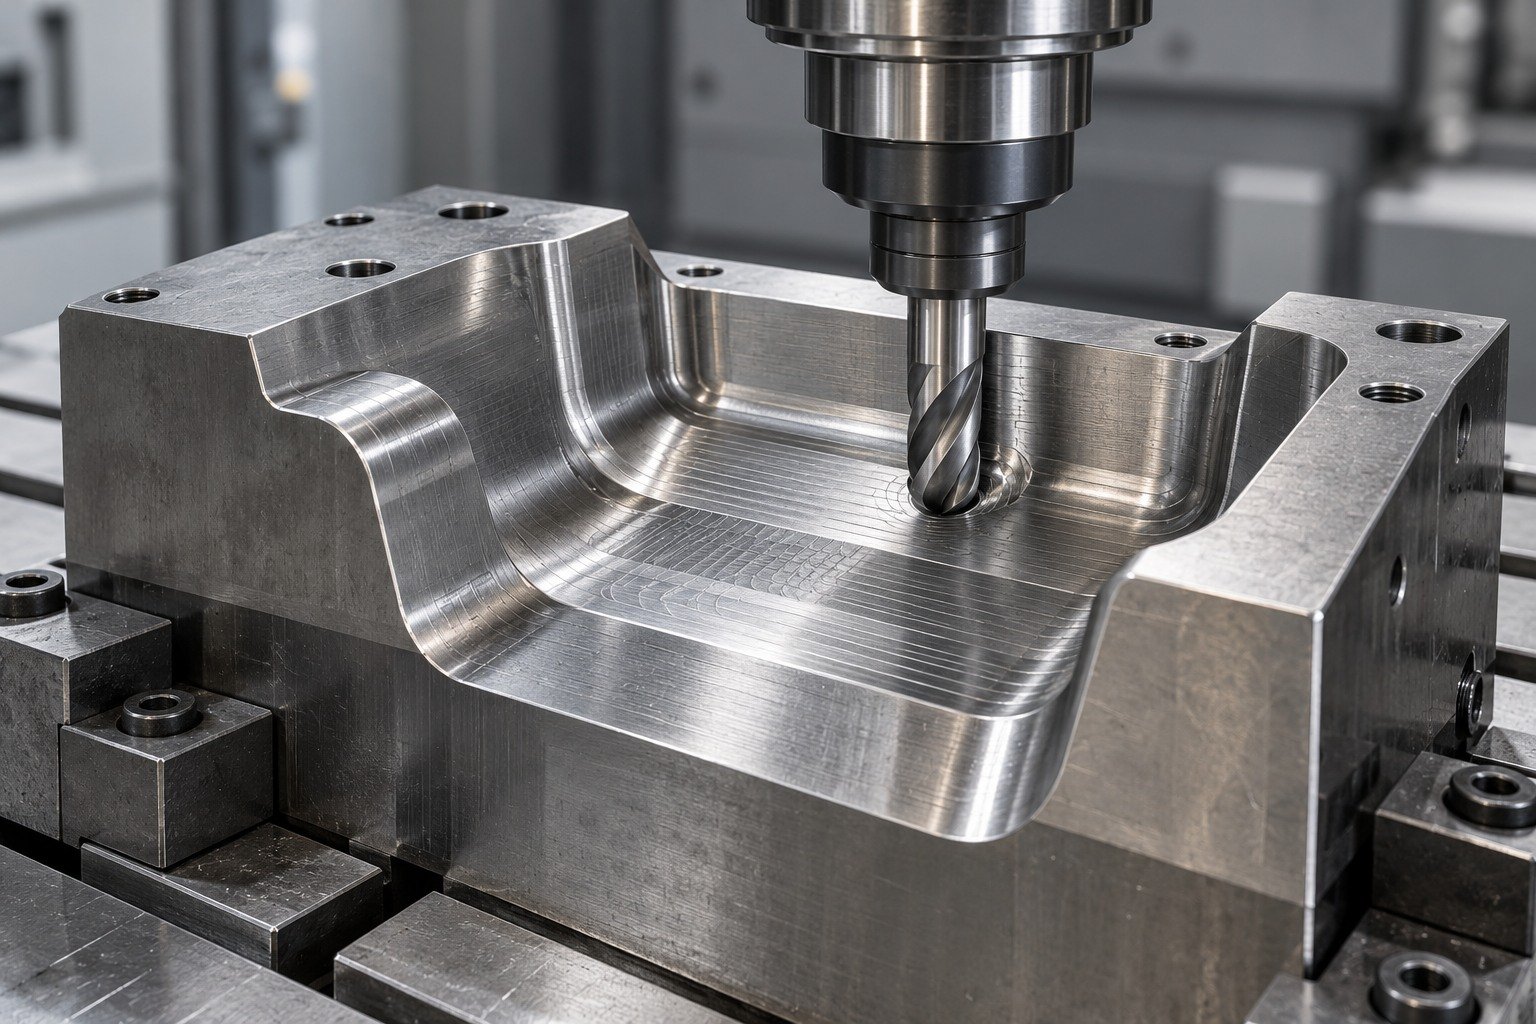
Specify the actual H13 product, melting route when required, target condition and verification. ESR describes a remelting route; it is not a separate universal grade.
| Your decision | What to define |
|---|---|
| Your fit | Working surfaces, datums and mating features. |
| Your process | Supplied condition, sequence and finishing allowance. |
| Your approval | Final dimensions and required records. |
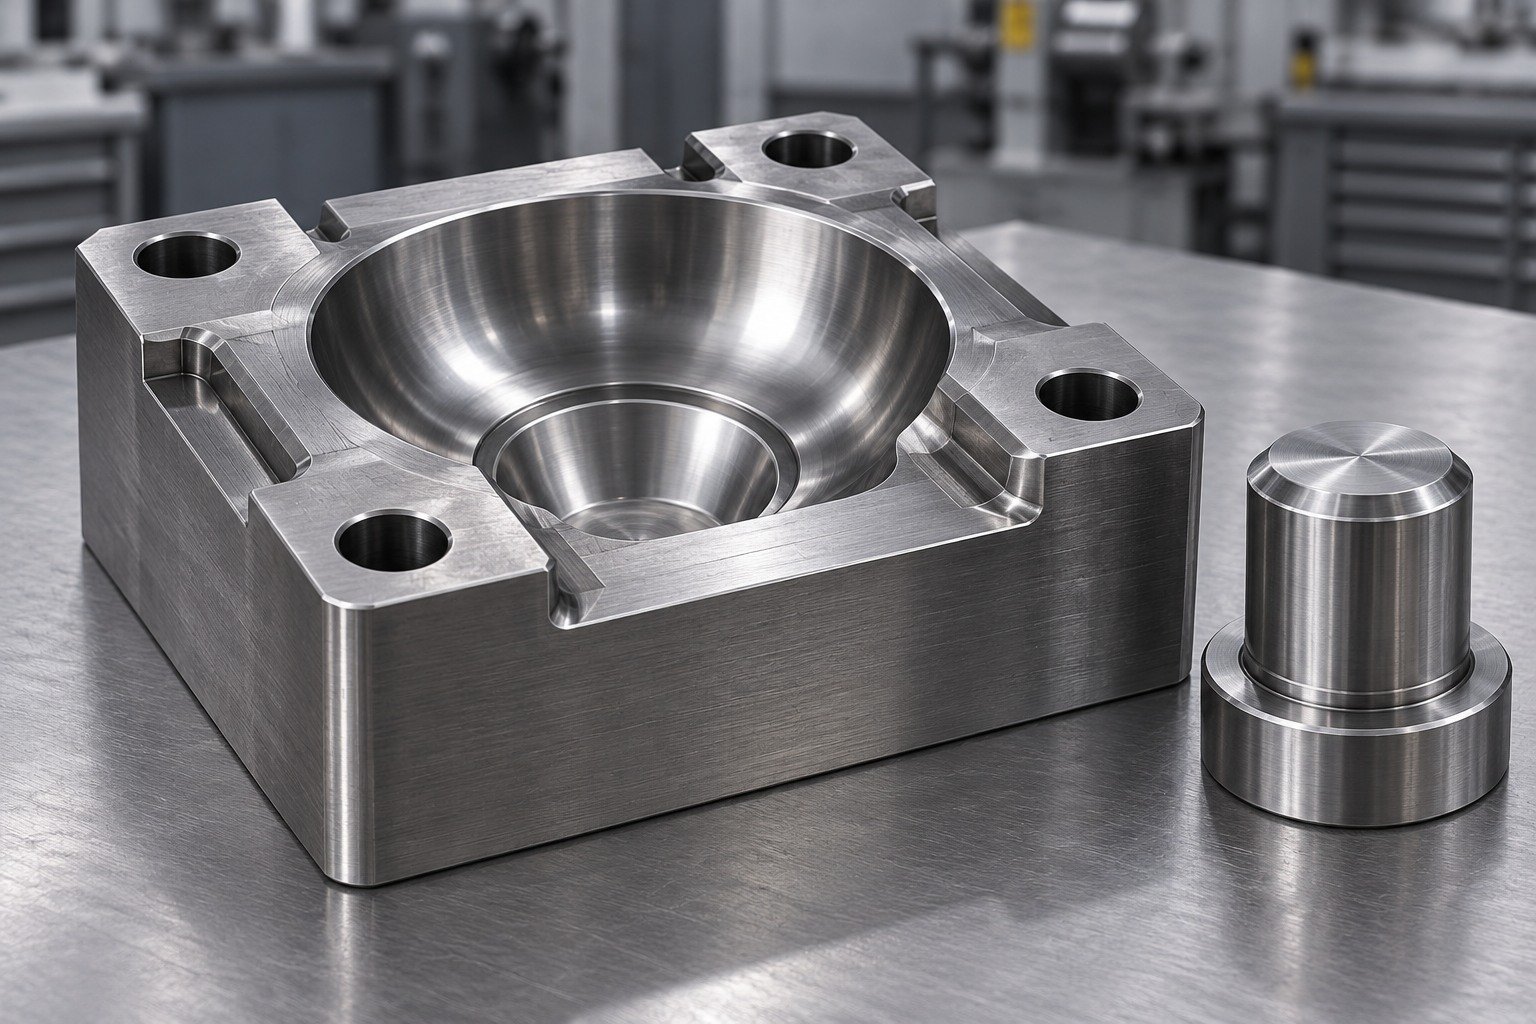
Connect cavity geometry and locating faces to the final working state. Agree any hardness or process records with your drawing review.
| Your decision | What to define |
|---|---|
| Your fit | Working surfaces, datums and mating features. |
| Your process | Supplied condition, sequence and finishing allowance. |
| Your approval | Final dimensions and required records. |
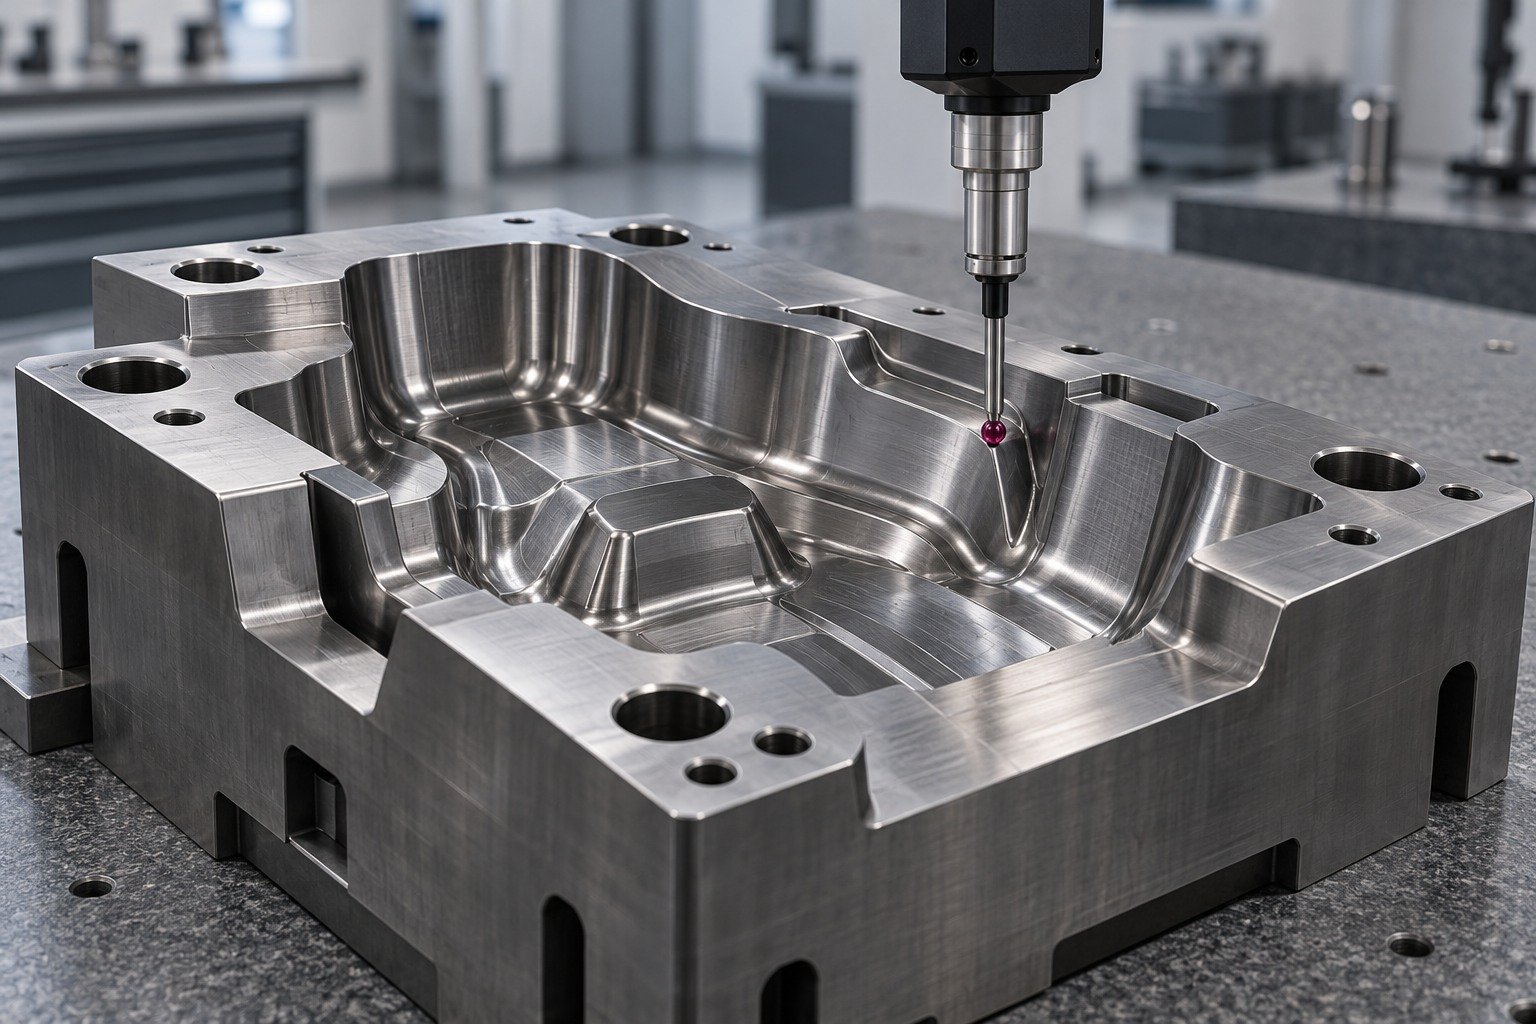
For your P20 mold steel machining inquiry, define the cavity, core, molding resin, polish or texture requirement and expected service exposure.
| Your decision | What to define |
|---|---|
| Your fit | Working surfaces, datums and mating features. |
| Your process | Supplied condition, sequence and finishing allowance. |
| Your approval | Final dimensions and required records. |
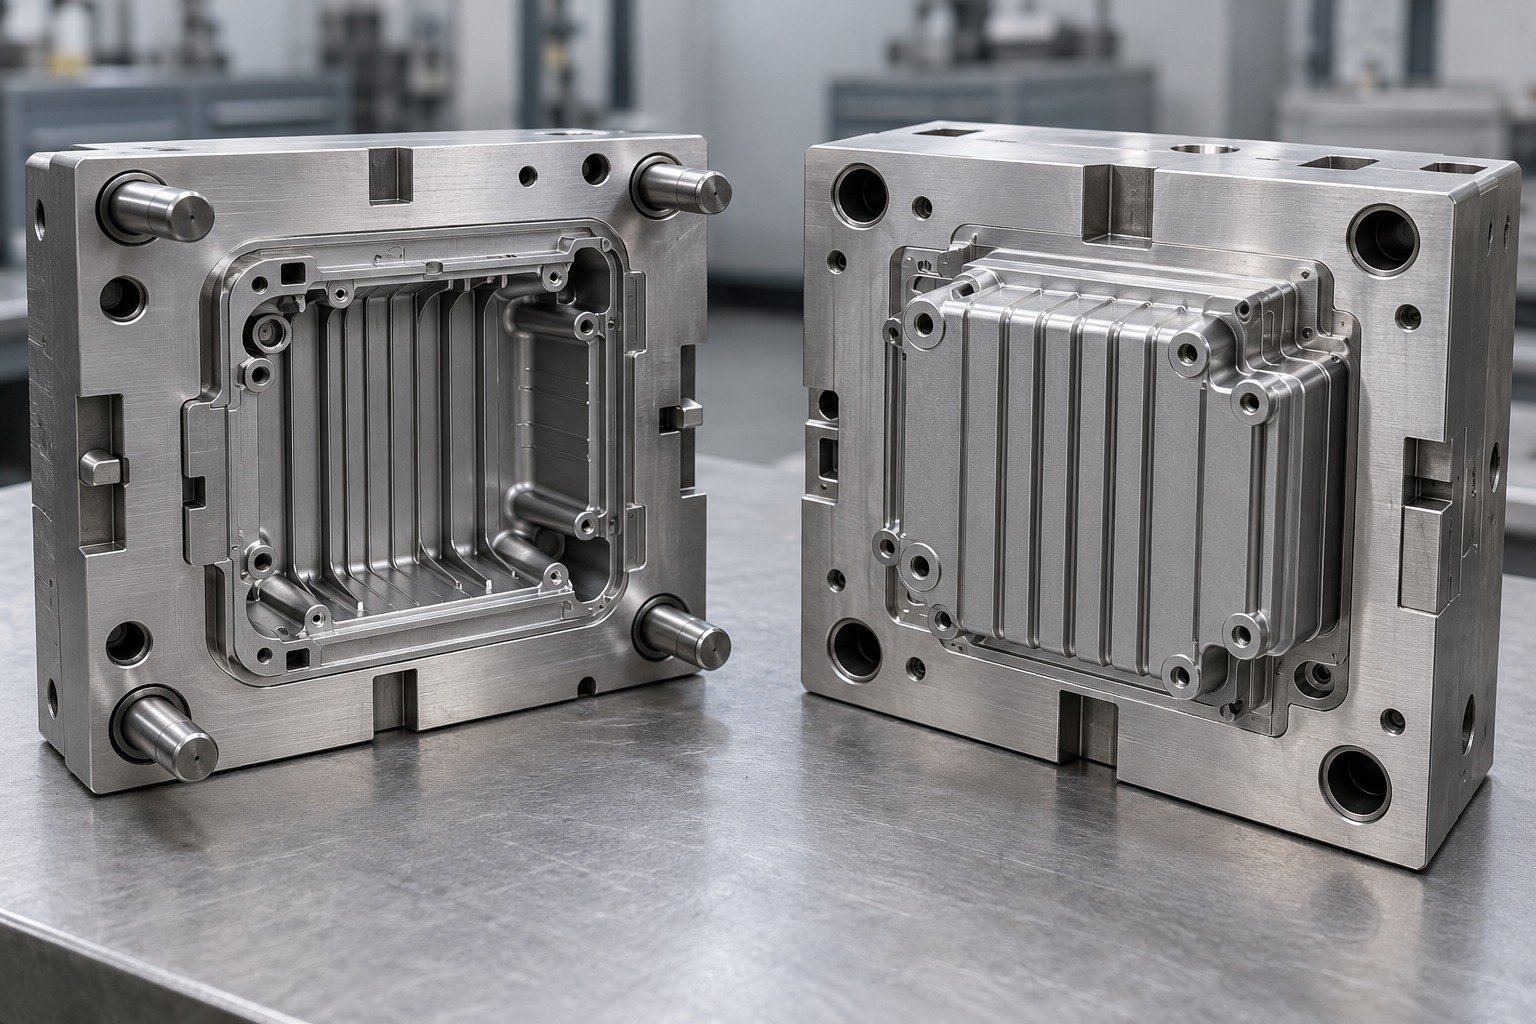
Identify ribs, cooling ports, parting faces and shutoff features. Confirm access and finishing direction on visible or sealing surfaces.
| Your decision | What to define |
|---|---|
| Your fit | Working surfaces, datums and mating features. |
| Your process | Supplied condition, sequence and finishing allowance. |
| Your approval | Final dimensions and required records. |
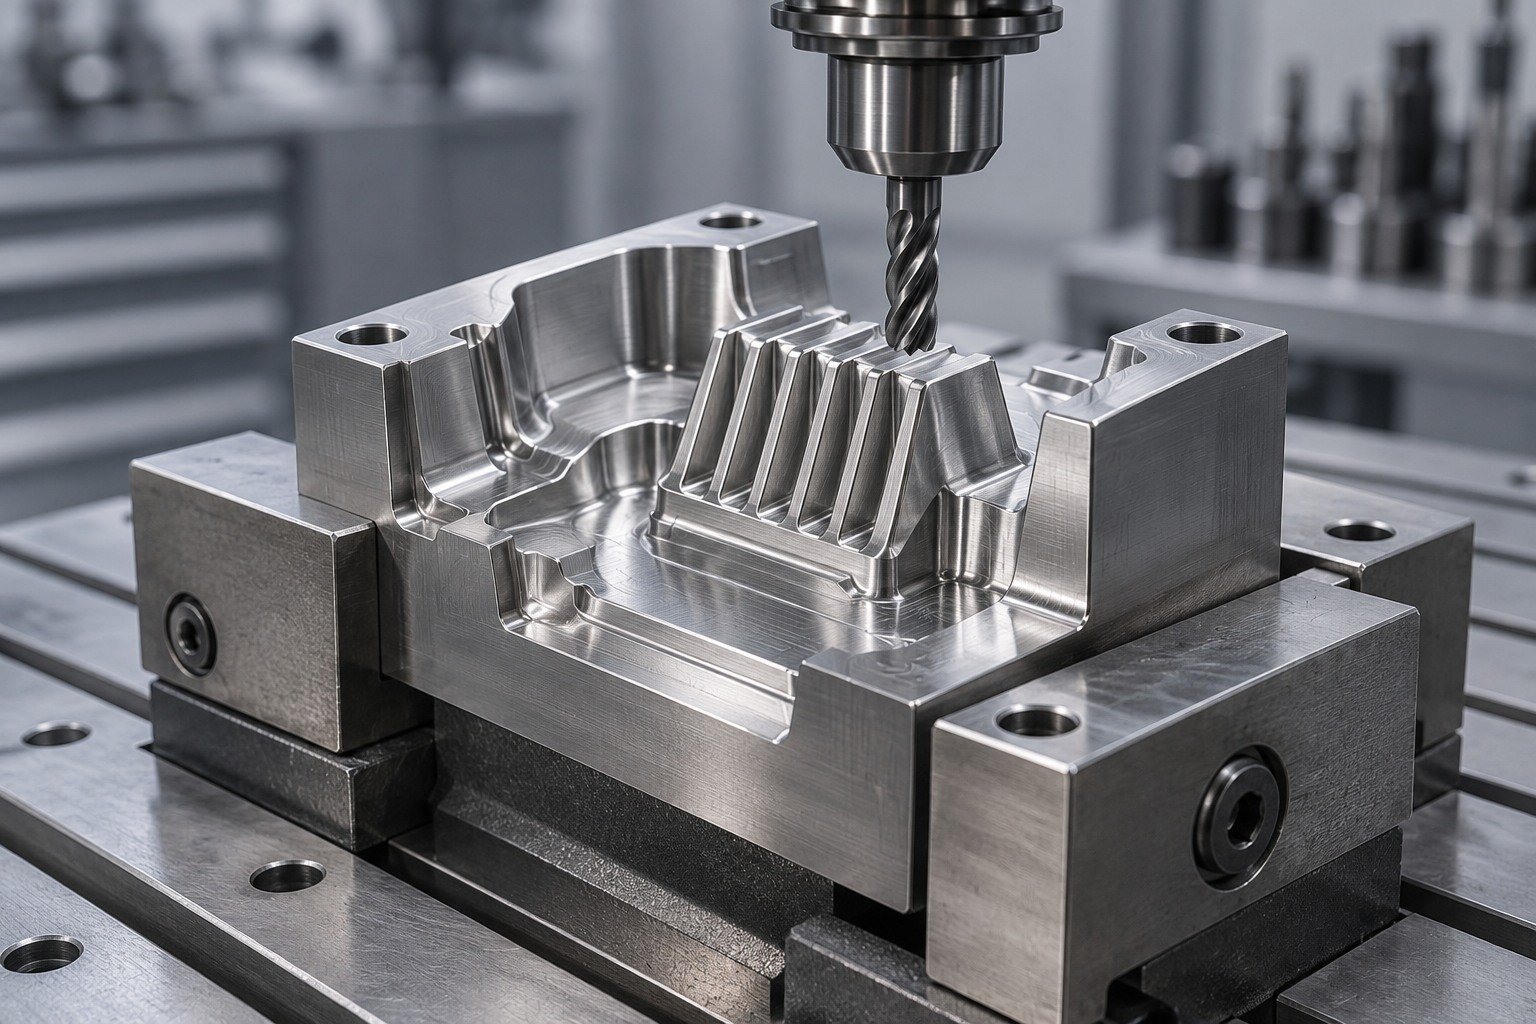
Confirm the prehardened delivery state. 1.2311, sulfur-modified 1.2312 and nickel-modified 1.2738 should not be purchased as one interchangeable material.
| Your decision | What to define |
|---|---|
| Your fit | Working surfaces, datums and mating features. |
| Your process | Supplied condition, sequence and finishing allowance. |
| Your approval | Final dimensions and required records. |
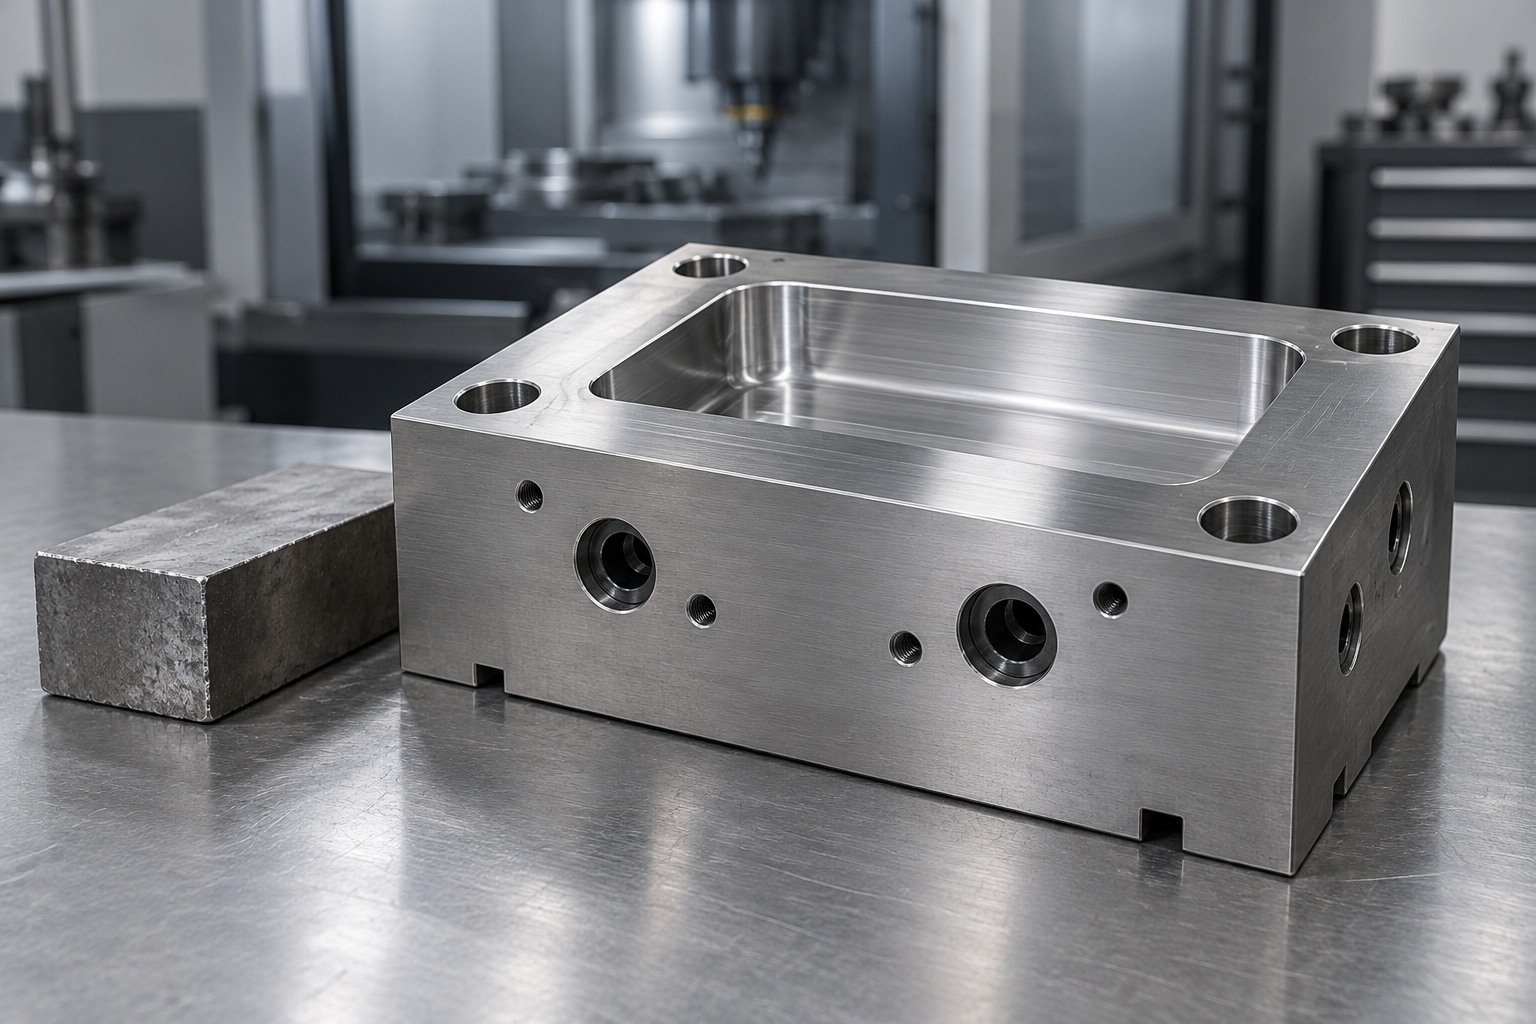
Inspect parting faces, critical shutoffs and locating features after finishing. Agree the finish sample and dimensional acceptance together.
| Your decision | What to define |
|---|---|
| Your fit | Working surfaces, datums and mating features. |
| Your process | Supplied condition, sequence and finishing allowance. |
| Your approval | Final dimensions and required records. |
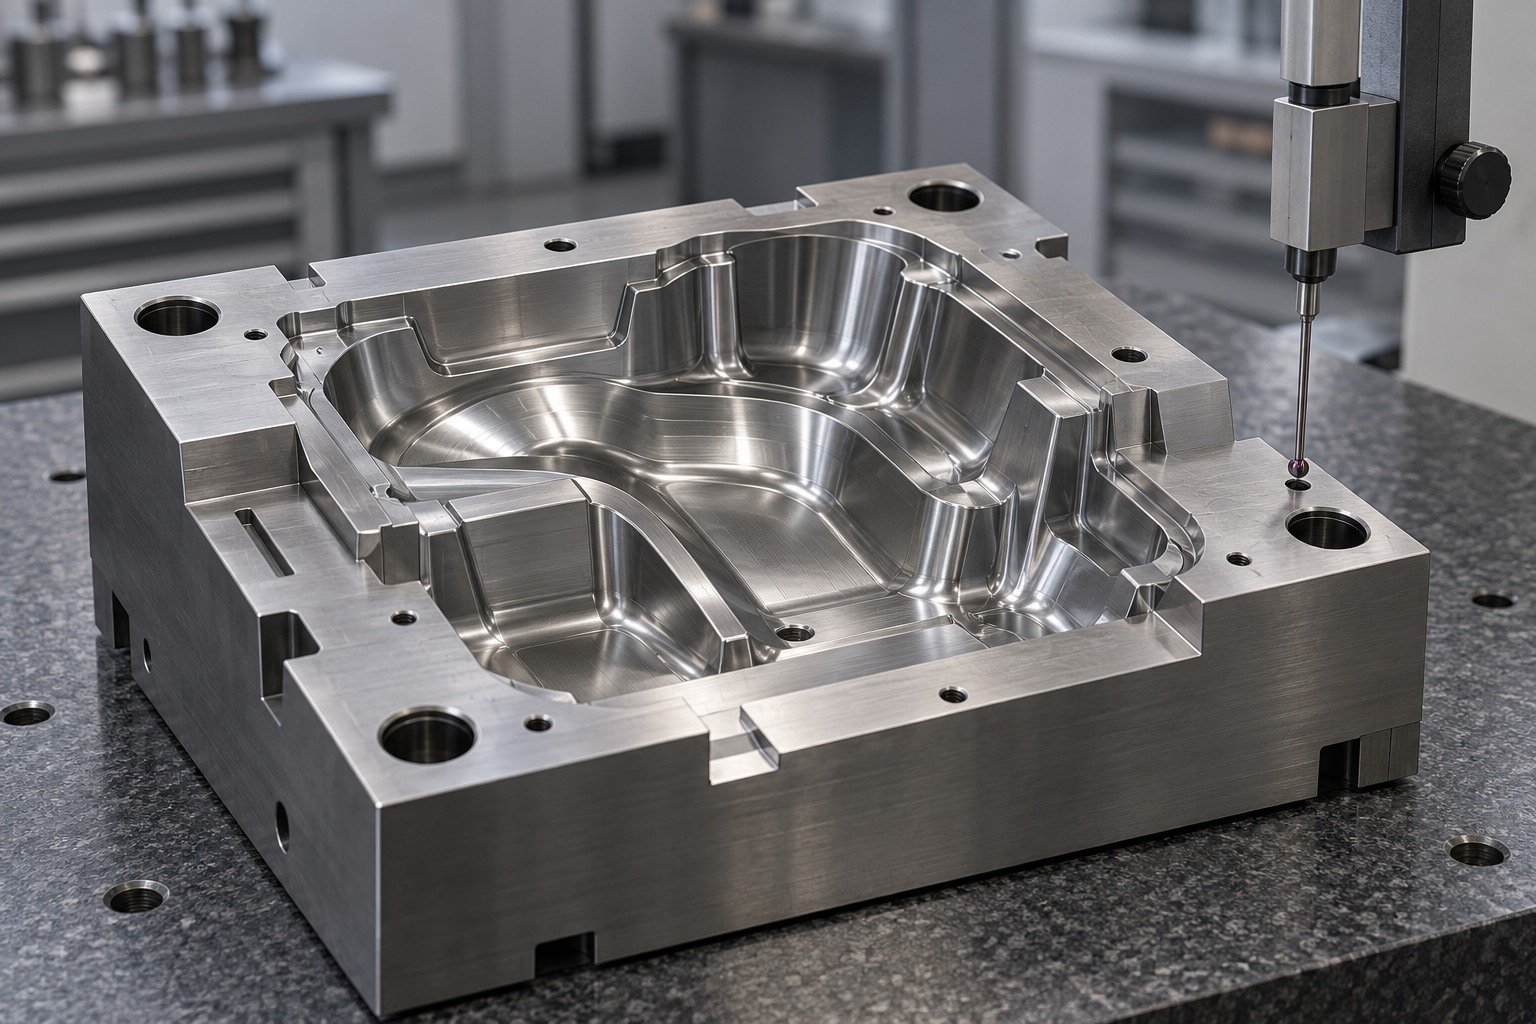
For impact-loaded tools, review S7 separately from abrasion-focused grades. M2 is high-speed steel; DC53 and powder products retain their producer identities.
| Your decision | What to define |
|---|---|
| Your fit | Working surfaces, datums and mating features. |
| Your process | Supplied condition, sequence and finishing allowance. |
| Your approval | Final dimensions and required records. |
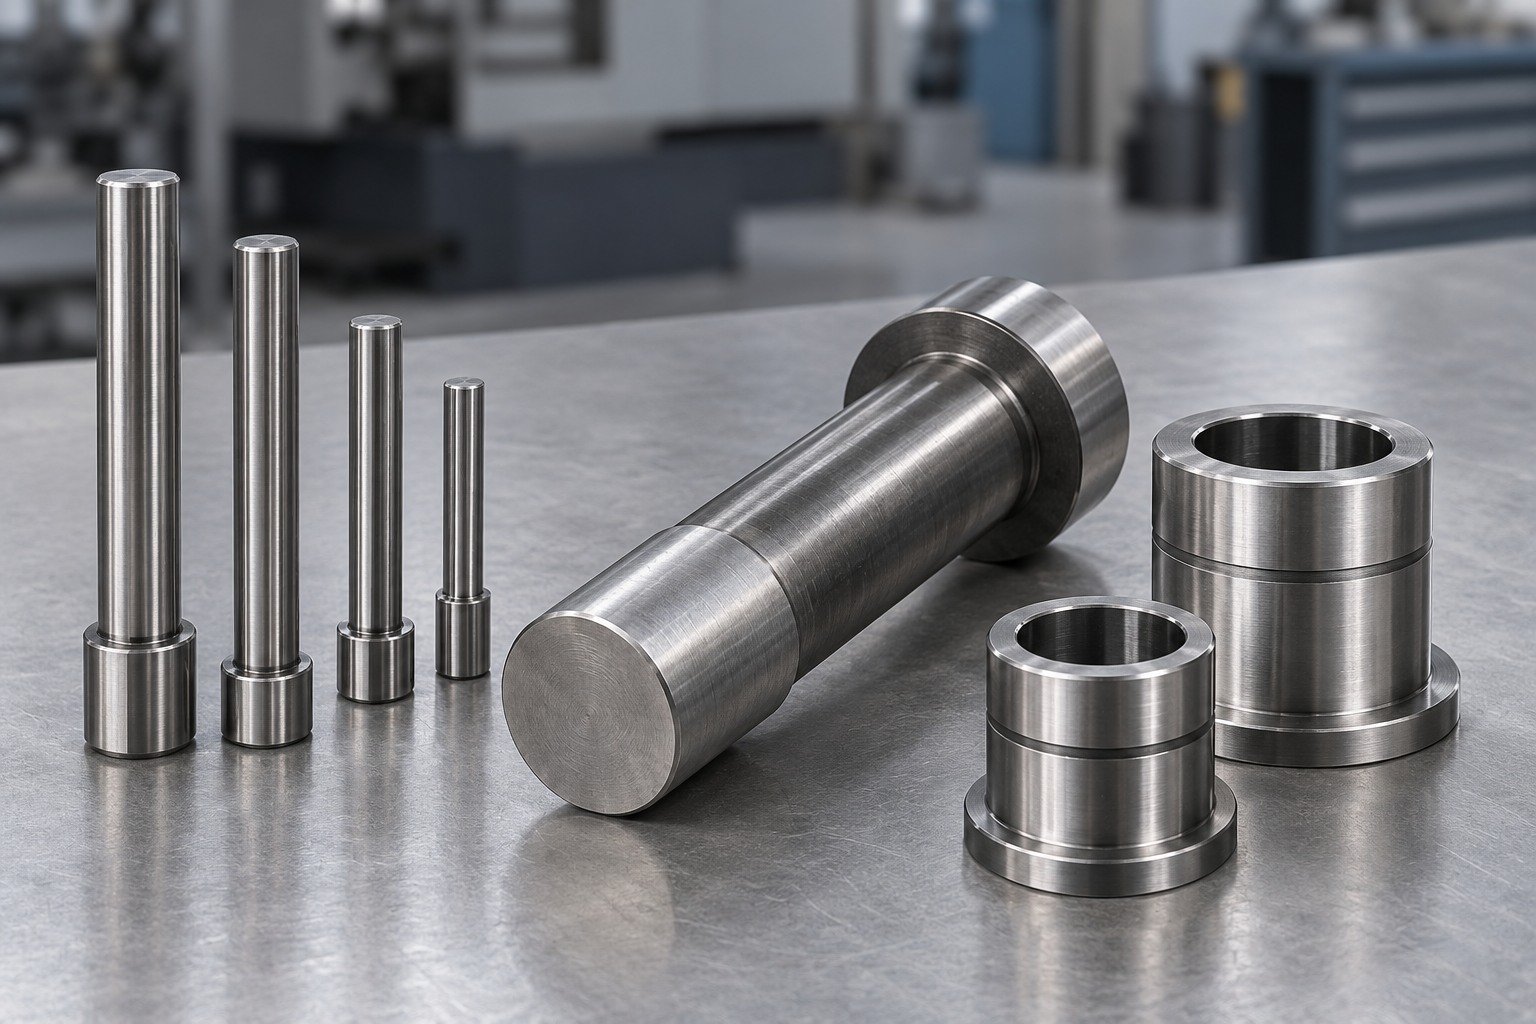
Show shoulder radii, supported length, bore fits and feature access for punches, pins and wear bushings. Specialized cutting-tool manufacture needs separate scope review.
| Your decision | What to define |
|---|---|
| Your fit | Working surfaces, datums and mating features. |
| Your process | Supplied condition, sequence and finishing allowance. |
| Your approval | Final dimensions and required records. |
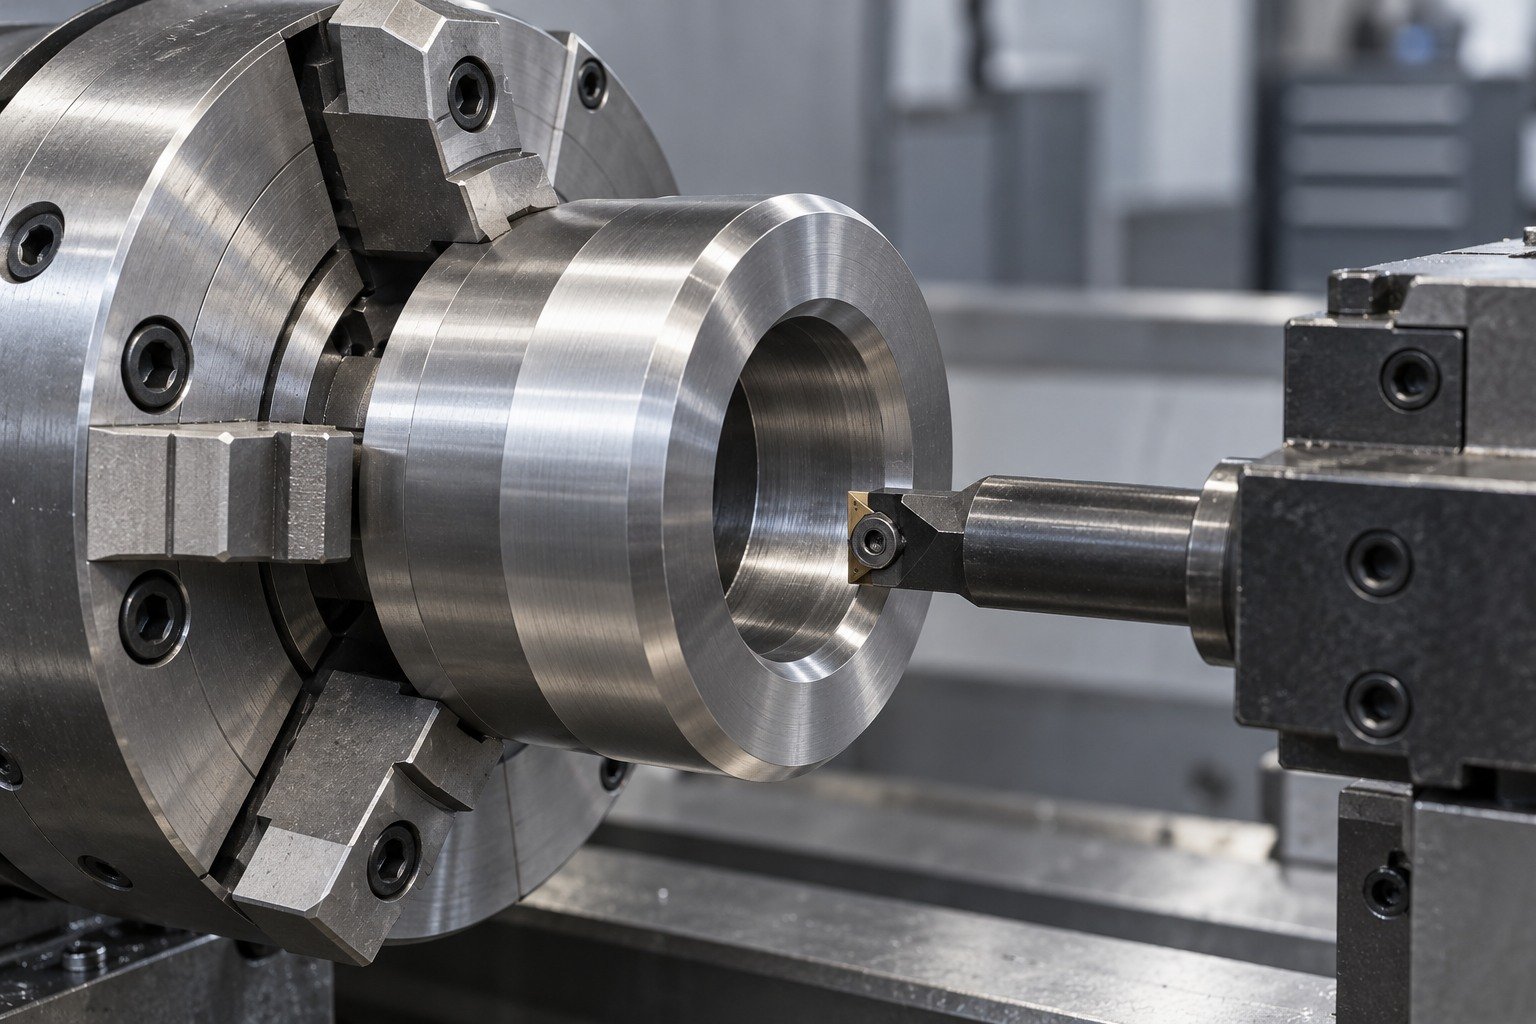
Provide the exact producer designation and specified thermal route. A hardness number alone does not describe toughness, carbide structure or suitability.
| Your decision | What to define |
|---|---|
| Your fit | Working surfaces, datums and mating features. |
| Your process | Supplied condition, sequence and finishing allowance. |
| Your approval | Final dimensions and required records. |
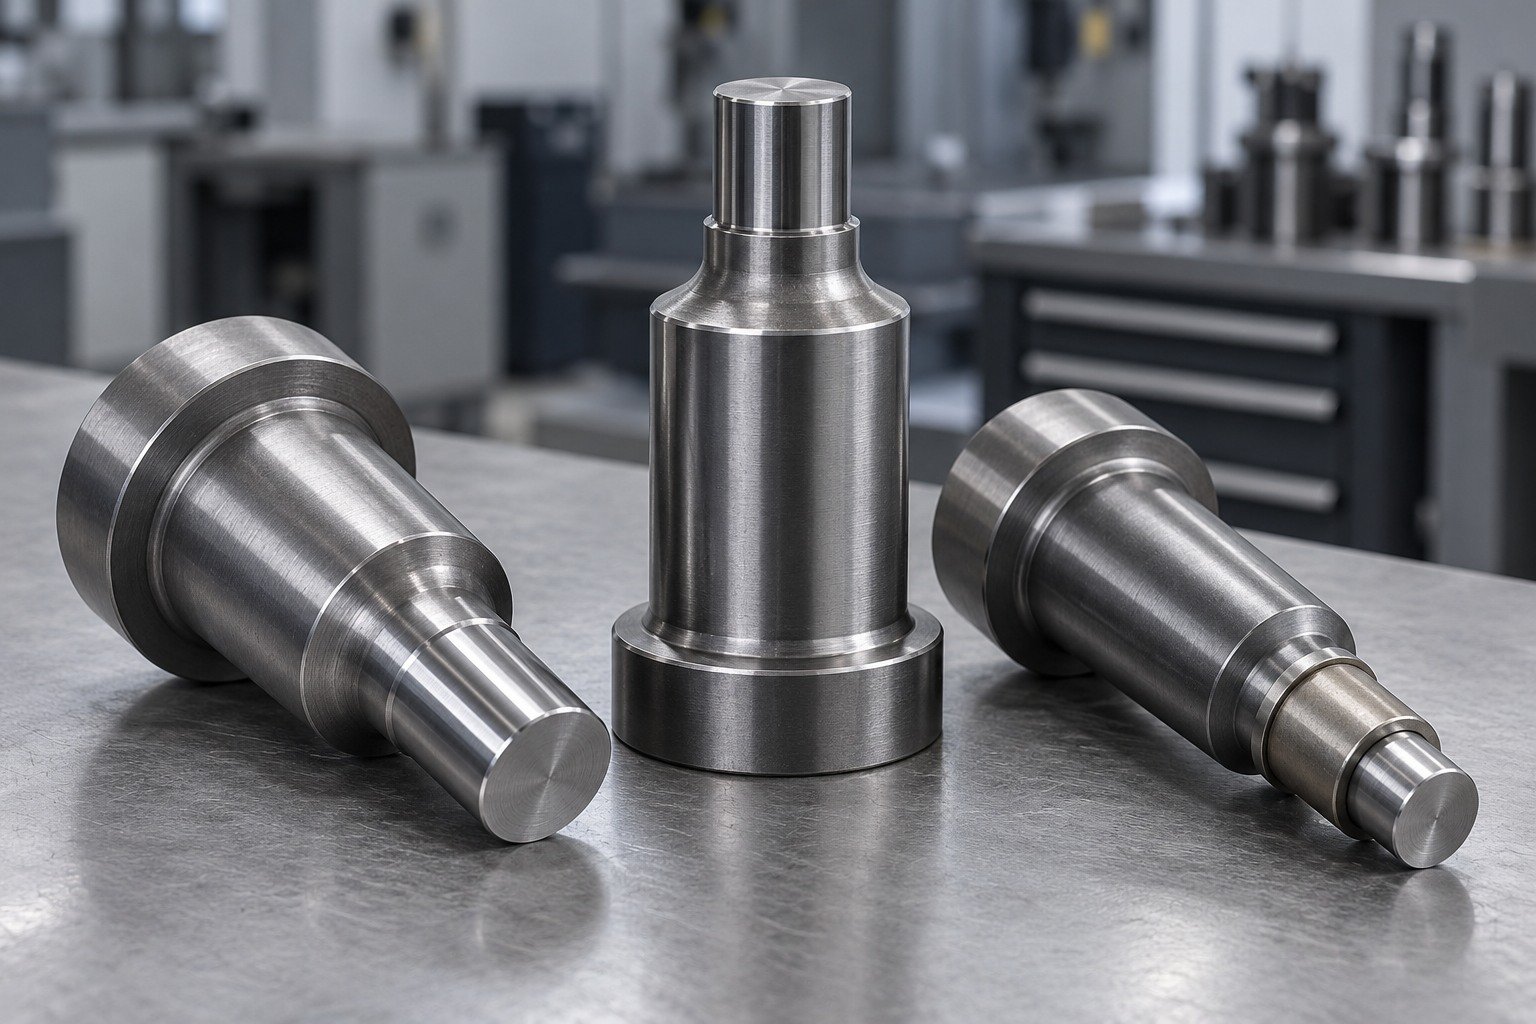
Agree diameter and shoulder checks, working-face acceptance, material traceability and any required test method before release.
| Your decision | What to define |
|---|---|
| Your fit | Working surfaces, datums and mating features. |
| Your process | Supplied condition, sequence and finishing allowance. |
| Your approval | Final dimensions and required records. |
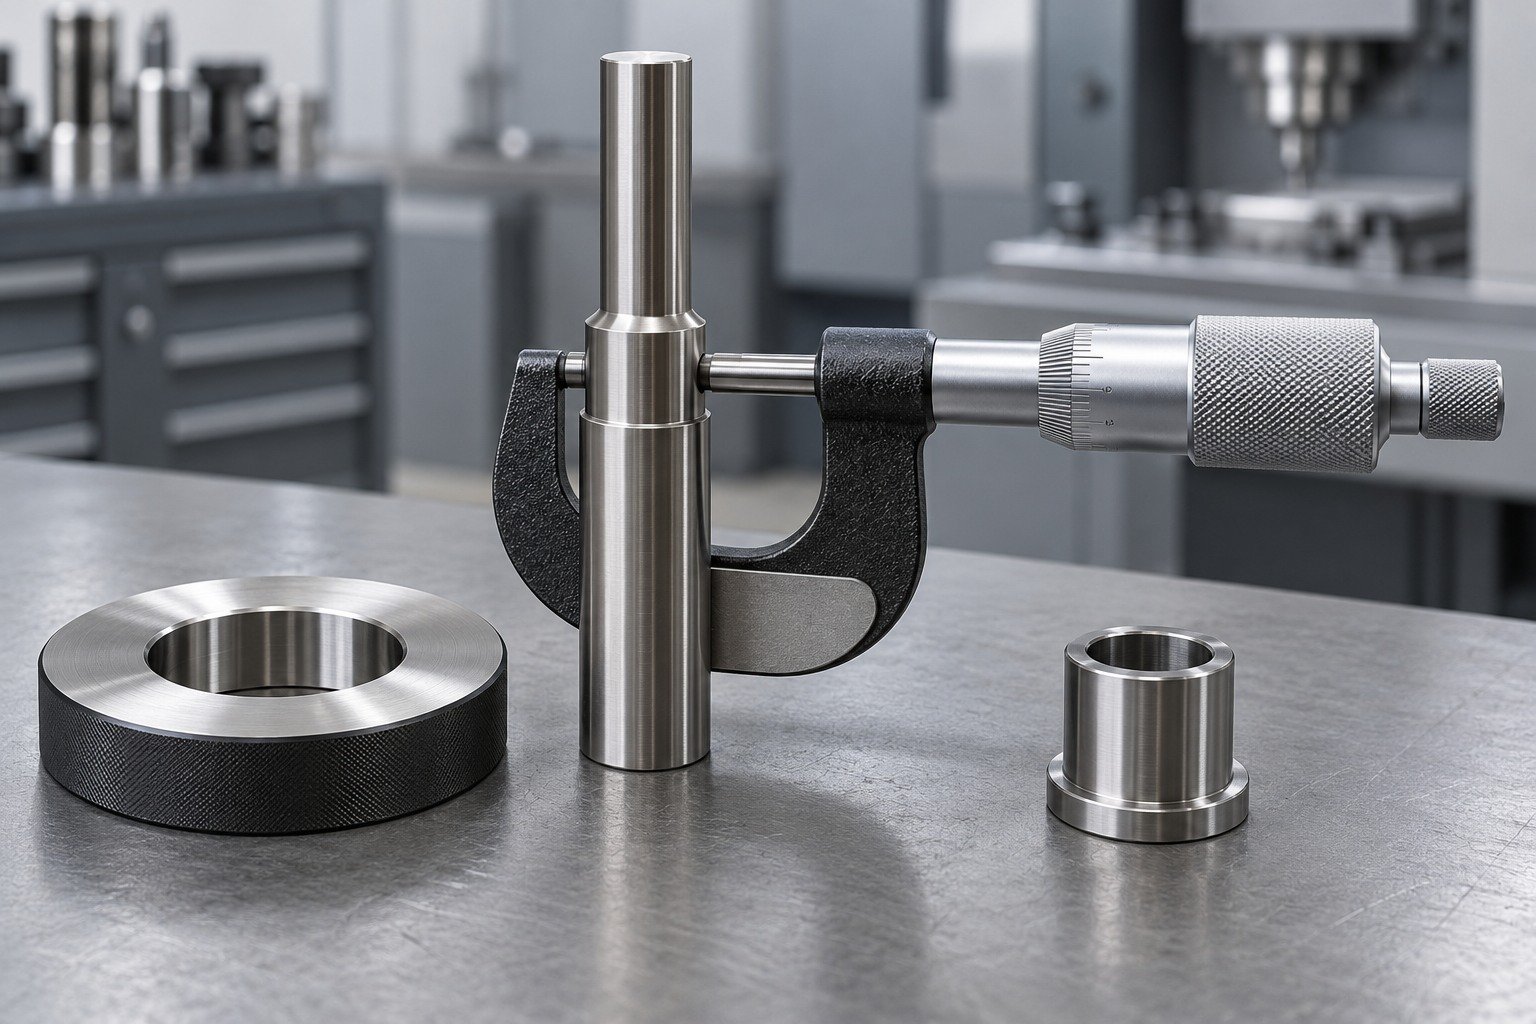
Agree the operations and acceptance sequence for your actual grade, condition and geometry.
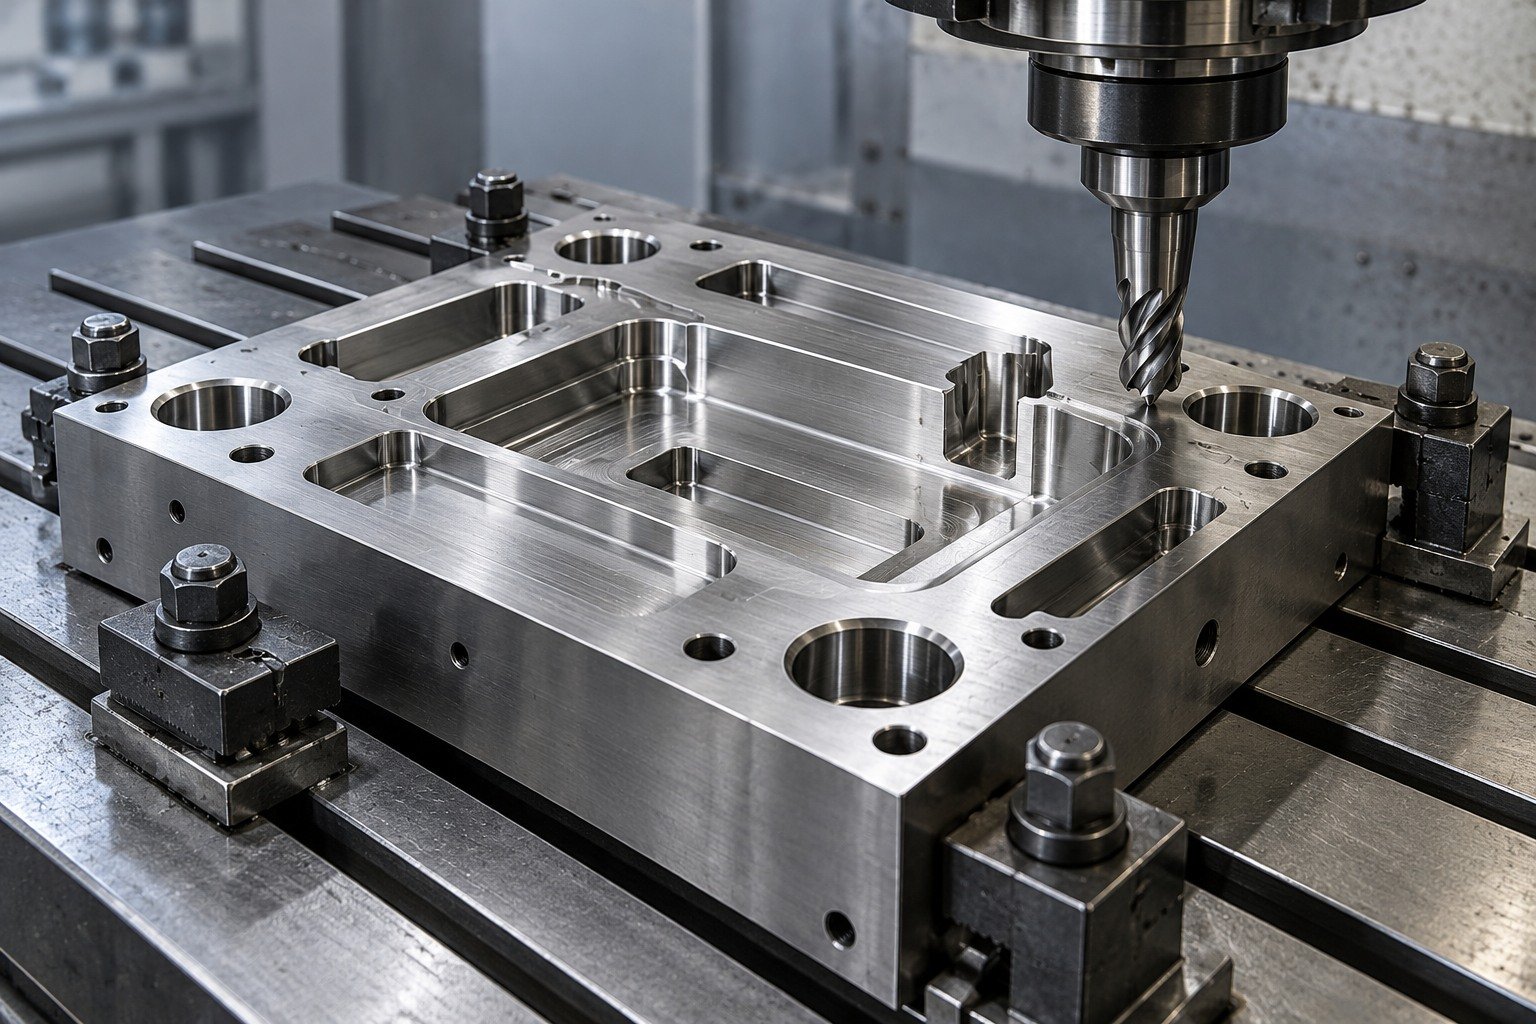
For die pockets, mold cavities, datums and dowel features.
Explore Milling & Drilling →

Your tooling cost and service outcome depend on more than the material name or hardness number.
Unknown scrap or a trade name without a producer record can leave your heat-treatment route undefined. Confirm stock identity, product form, condition and any supplied-material restrictions.
Define the controlled feature and final state.
Agree method, location and document scope.
Accept geometry after the full process.
Define entry direction, useful engagement, thread runout and burr-removal access. Identify dowel fits and the stage at which holes reach final size.
Define the controlled feature and final state.
Agree method, location and document scope.
Accept geometry after the full process.
Specify target condition, test method and locations, section and finishing allowance. Confirm the sequence after distortion; a rough-machined dimension is not final acceptance.
Define the controlled feature and final state.
Agree method, location and document scope.
Accept geometry after the full process.
Show permitted corner radii, backing sections and critical edge conditions. Compare chipping, impact and wear needs before choosing a harder grade.
Define the controlled feature and final state.
Agree method, location and document scope.
Accept geometry after the full process.

Specify the finish system, working temperature, masked surfaces and final bore or datum requirements. Review coating compatibility with the heat-treated substrate.
Define the controlled feature and final state.
Agree method, location and document scope.
Accept geometry after the full process.
Plan final geometry and hardness verification after machining, treatment and finishing. Agree separate evidence for dimensions, material identity and specified properties.
Define the controlled feature and final state.
Agree method, location and document scope.
Accept geometry after the full process.


Visual samples are concepts. Treatment suitability, color, surface texture, masking and manufacturing scope require your project review.
Surface Finishing →| Your comparison | What to confirm |
|---|---|
| A2 vs D2 | Wear, impact, edge support and final geometry. |
| H13 vs cold-work grades | Thermal cycling and hot-work duty. |
| P20 vs P20+S or P20+Ni | Producer chemistry, polish requirement and delivered state. |
| S7 or proprietary grades | Exact product identity, condition and approval. |
Higher chromium or a larger hardness number does not establish a better choice for your tool.
Grade, product form, supplied state and lot identity.
Required condition, distortion and remaining finish stock.
Working geometry, functional surfaces and records.
Review grade, producer, product standard, stock form, condition and required lot records before machining.
Sampling, methods and document scope are agreed with your quotation.
Quality Assurance →
Review the sample against critical faces and the planned treatment and finishing stages. Confirm remaining stock before final release.
Sampling, methods and document scope are agreed with your quotation.
Quality Assurance →
Agree the final working profile, datum scheme, locating fits and any specified hardness or surface tests.
Sampling, methods and document scope are agreed with your quotation.
Quality Assurance →
Define protected edges, identification, packaging and the documents your receiving team needs.
Sampling, methods and document scope are agreed with your quotation.
Quality Assurance →
Coordinate your drawing review, material specification, sample decisions and receiving requirements.
Start with the failure mode: abrasion, chipping, impact, thermal cycling or mold-surface requirements. Compare the exact product and condition with your tool geometry; no one grade is best for every application.
Agree the route for your drawing. Roughing may precede specified hardening, with critical features finished afterward. Prehardened material follows a different plan. Define stock condition, remaining allowance and final inspection.
Compare abrasive wear with impact and edge-support needs. A higher alloy content does not automatically reduce chipping or improve your finished tool. Include working material and service conditions in your inquiry.
Use the EN material number and symbolic designation as comparison aids. Check the complete product standard, chemistry, delivery state, section and approved processing before substitution. Trade names require producer identification.
Yes. Heat treatment and subsequent material removal can affect geometry. Agree final datums, machining or grinding allowance, sequence and measurement state before production.
Treat repair as a separate engineering review. Identify the steel, prior treatment, damage, section and required service condition. Confirm a qualified procedure and final acceptance rather than assuming a general welding route.
Send CAD and the controlled drawing, exact grade and stock state, quantities, target condition, finish, critical dimensions, inspection records and delivery needs. Compare quotations for the same drawing revision and final state.





