

Injection Molding
Tooling and molding for your repeat plastic parts.
From prototype to production, coordinated manufacturing solutions for your custom parts.
View All Services →
Precision parts for your tight tolerances and complex geometry.
Tooling and molding for your repeat plastic parts.

Metal casting options for your part and production volume.

Cutting, forming and welding for your fabricated parts.

Custom profiles for your section, length and finish requirements.

Finishes for your appearance, corrosion and wear requirements.

Sub-assemblies and final builds for your production program.

Production tooling built around your process and volume.

Prototype parts to check fit, function and design.
DFM, process planning and production support for your project.
Inspection, documentation, inventory and delivery planning for your program.
Choose air- or liquid-cooling components around your thermal and mechanical requirements.

Manufacturing support for your cold plates, manifolds and cooling assemblies.

Find components for your power electronics, energy, laser and telecom application.

Components for your electronic systems.
Start with your functional and quality requirements.
Build around your operating environment.
From prototype to production, review material performance, manufacturability and cost for your part.
Review grade, temper and finish for your metal parts.
 AluminumStrength, weight and machining›
 Stainless SteelCorrosion and finish requirements›
 Carbon & Alloy SteelDiscuss grade and heat treatment›
 Tool SteelDiscuss tooling and wear needs›
 TitaniumReview grade and part geometry›
 Copper & BrassDiscuss conductivity and machining›
Match your polymer to function, process and environment.
 ABSReview enclosure and molding needs›
 Polycarbonate (PC)Discuss clarity and impact needs›
 Nylon (PA)Review moisture and wear conditions›
 POM / AcetalReview fit and sliding features›
 PEEKDiscuss operating conditions›
 PTFEReview friction and chemical exposure›
 ULTEM / PEIDiscuss thermal and electrical needs›
Confirm grade availability and application requirements.
 Silicone / LSRDiscuss flexible component needs›
 TPU / TPEReview flexibility and processing›
 EPDMReview weathering and chemical exposure.›
 NBRReview oil and fuel exposure.›
 FKMReview temperature and chemical exposure.›
 G10 / FR4Review insulation and laminate needs›
 CompositesReview stiffness, weight and laminate.›Customer-Specified MaterialsConfirm your grade and requirements.›Other Specialty MaterialsDiscuss your application and grade.›
Practical guidance for your part geometry and material decisions.
Prepare your process, budget and sourcing questions.
Build your knowledge before production.
Learn who we are and how we operate.
Find our U.S. support team or start a conversation.

For your D2 tool steel machining services inquiry, connect abrasive wear and edge support to the actual stock condition. Define grinding, wire EDM and final inspection around your working profile before production.
D2 cold-work tool steel is used for wear tooling such as dies, punches and forming components. Review D2 tool steel properties against the actual product and condition; the grade name does not approve edge support or guarantee working life.
Cold-work tool steel. For European sourcing, review 1.2379 / X153CrMoV12 and the actual product specification.
Annealed D2 tool steel for initial machining and hardened D2 tool steel for the working condition require different planning.
A comparison name supports review; it does not approve a substitute.
| Element | K110 producer average wt.% |
|---|---|
| C | 1.55 |
| Si | 0.30 |
| Mn | 0.30 |
| Cr | 11.30 |
| Mo | 0.75 |
| V | 0.75 |
BÖHLER K110 average analysis. Producer data refer to long products. Confirm your supplied product form and material record; these are not acceptance ranges.
| Stage | Your required decision |
|---|---|
| Incoming stock | Product form, actual condition and grade identity. |
| Specified treatment | Target condition, responsible party and required evidence. |
| Finished tooling | Final datums, working features and inspection after finishing. |
The specified thermal route must suit your actual section and geometry.
Selected producer averages · wt.% · common axis 0–12%
Composition only. These bars are not a wear, toughness, machinability or corrosion score. They are not test results from your material lot.
D2 tool steel machinability depends on the actual condition, geometry and operation. Agree the route for your drawing; a generic cutting-speed table is not a production plan.
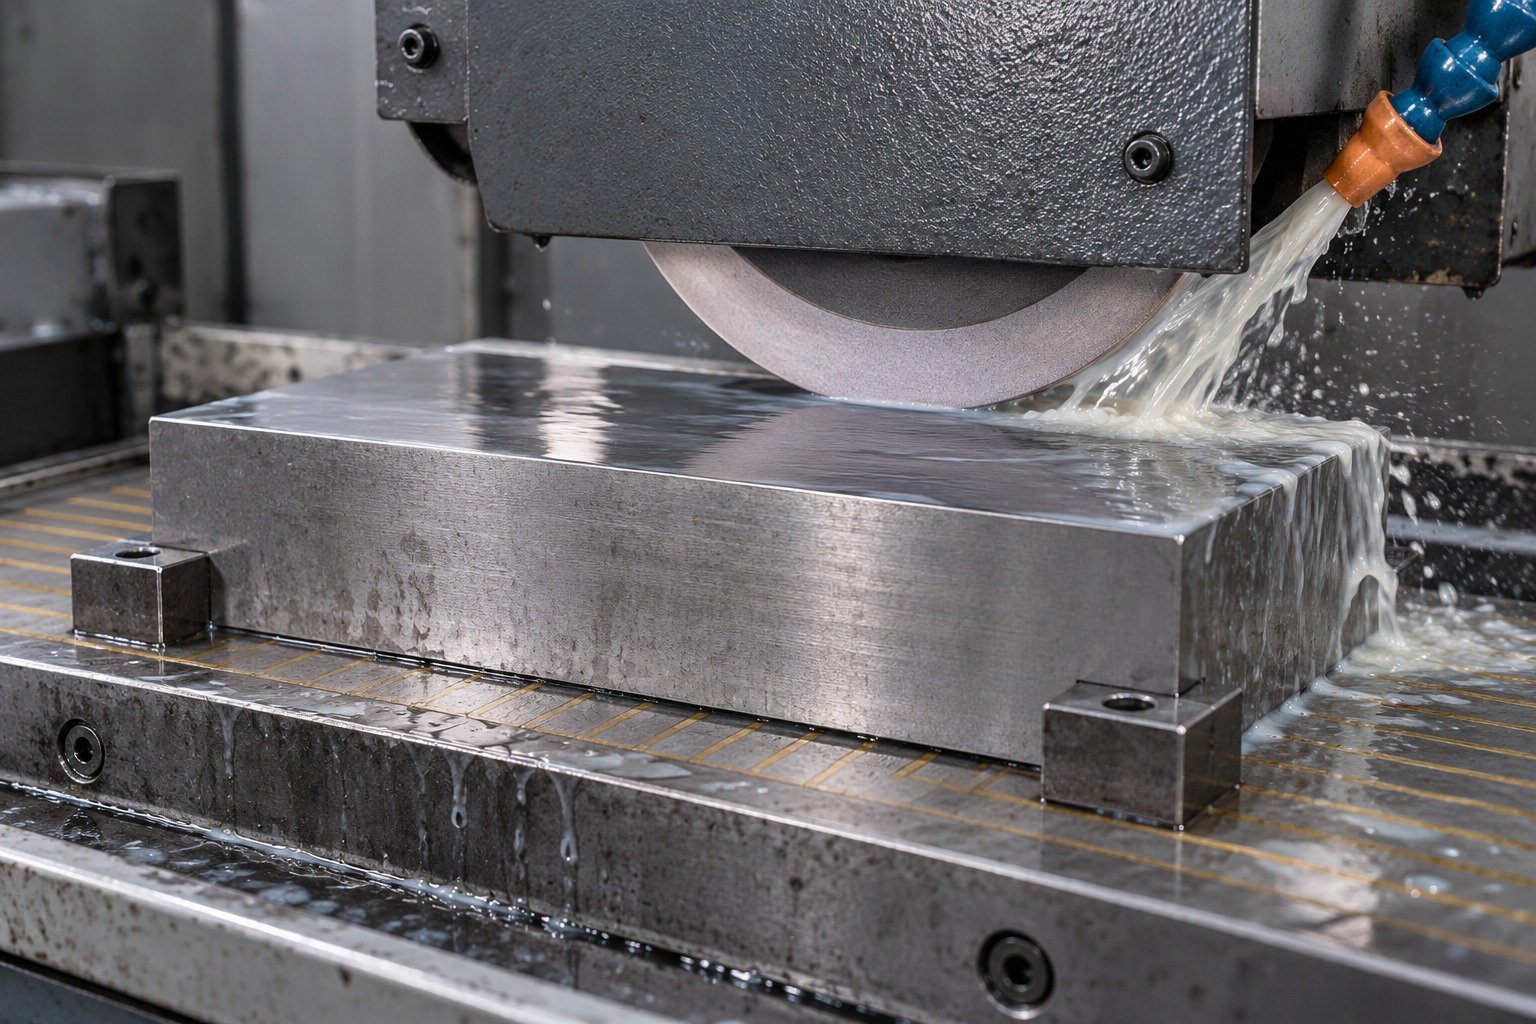
Define D2 tool steel grinding allowance and final measurement state.
Explore Precision Grinding →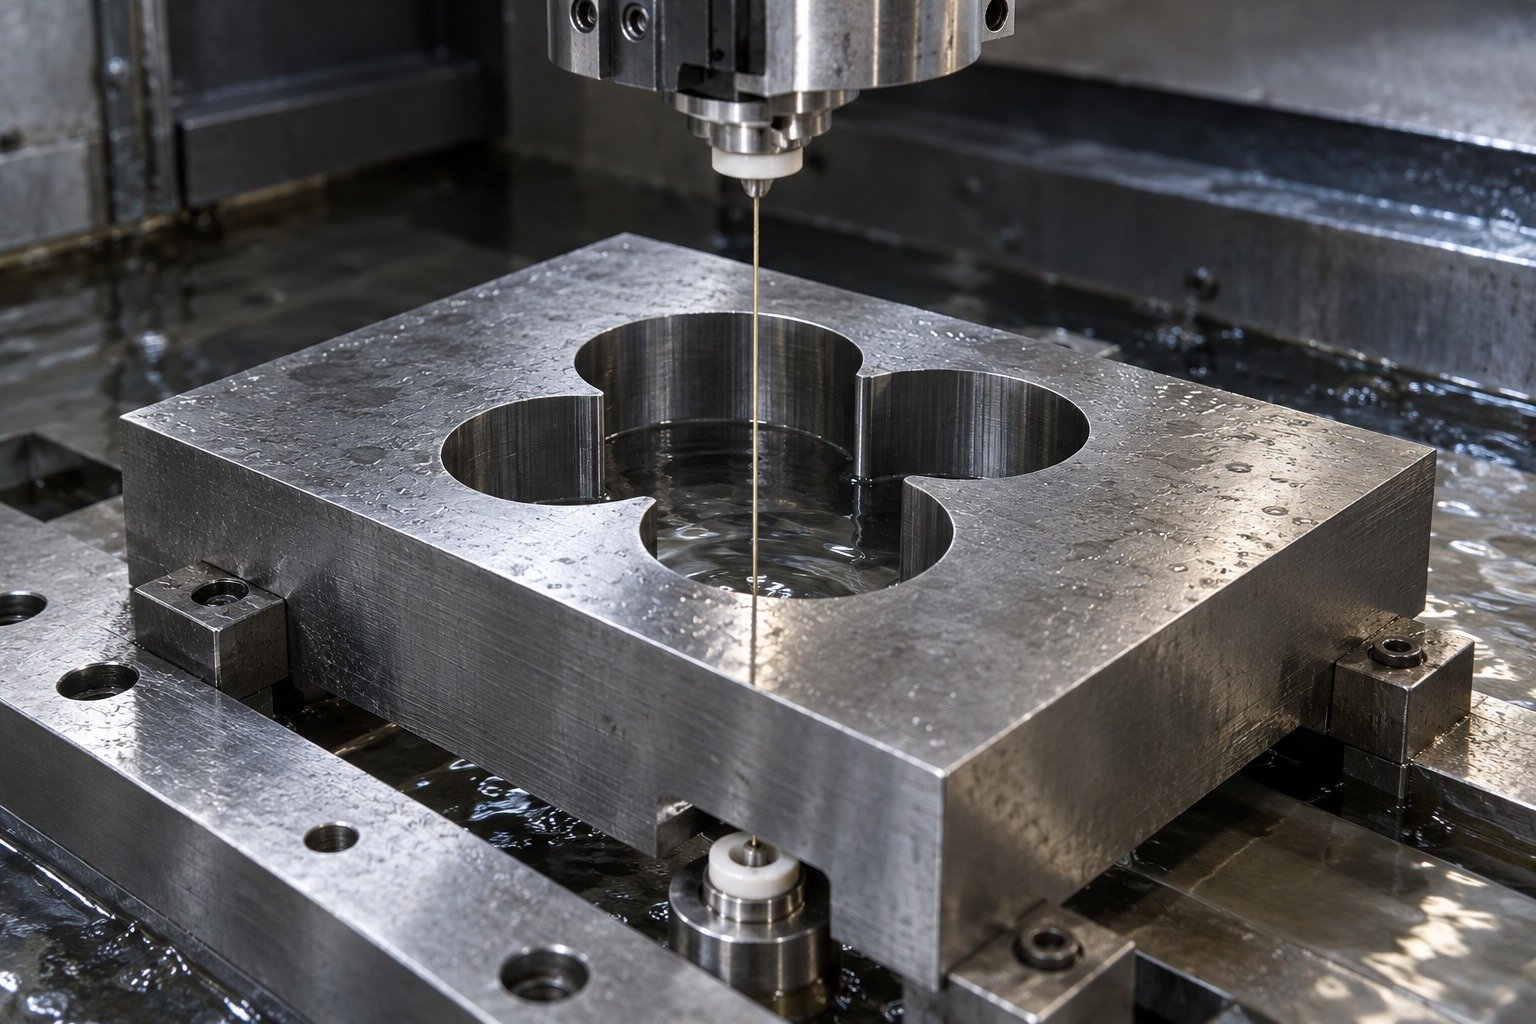
For D2 tool steel wire EDM review, identify through profiles and final surface requirements.
Explore Wire EDM →Select the part you need, then review machining, condition and final acceptance.
For your D2 tool steel dies, identify the stock being blanked, working clearance and edge support. Connect the final die profile to the mating punch and the backing arrangement.
| Your decision | What to define |
|---|---|
| Your fit | Working profile, clearance, backing and locating bores. |
| Your process | Initial machining, specified treatment and final finishing. |
| Your approval | Controlled drawing, final condition and receiving evidence. |
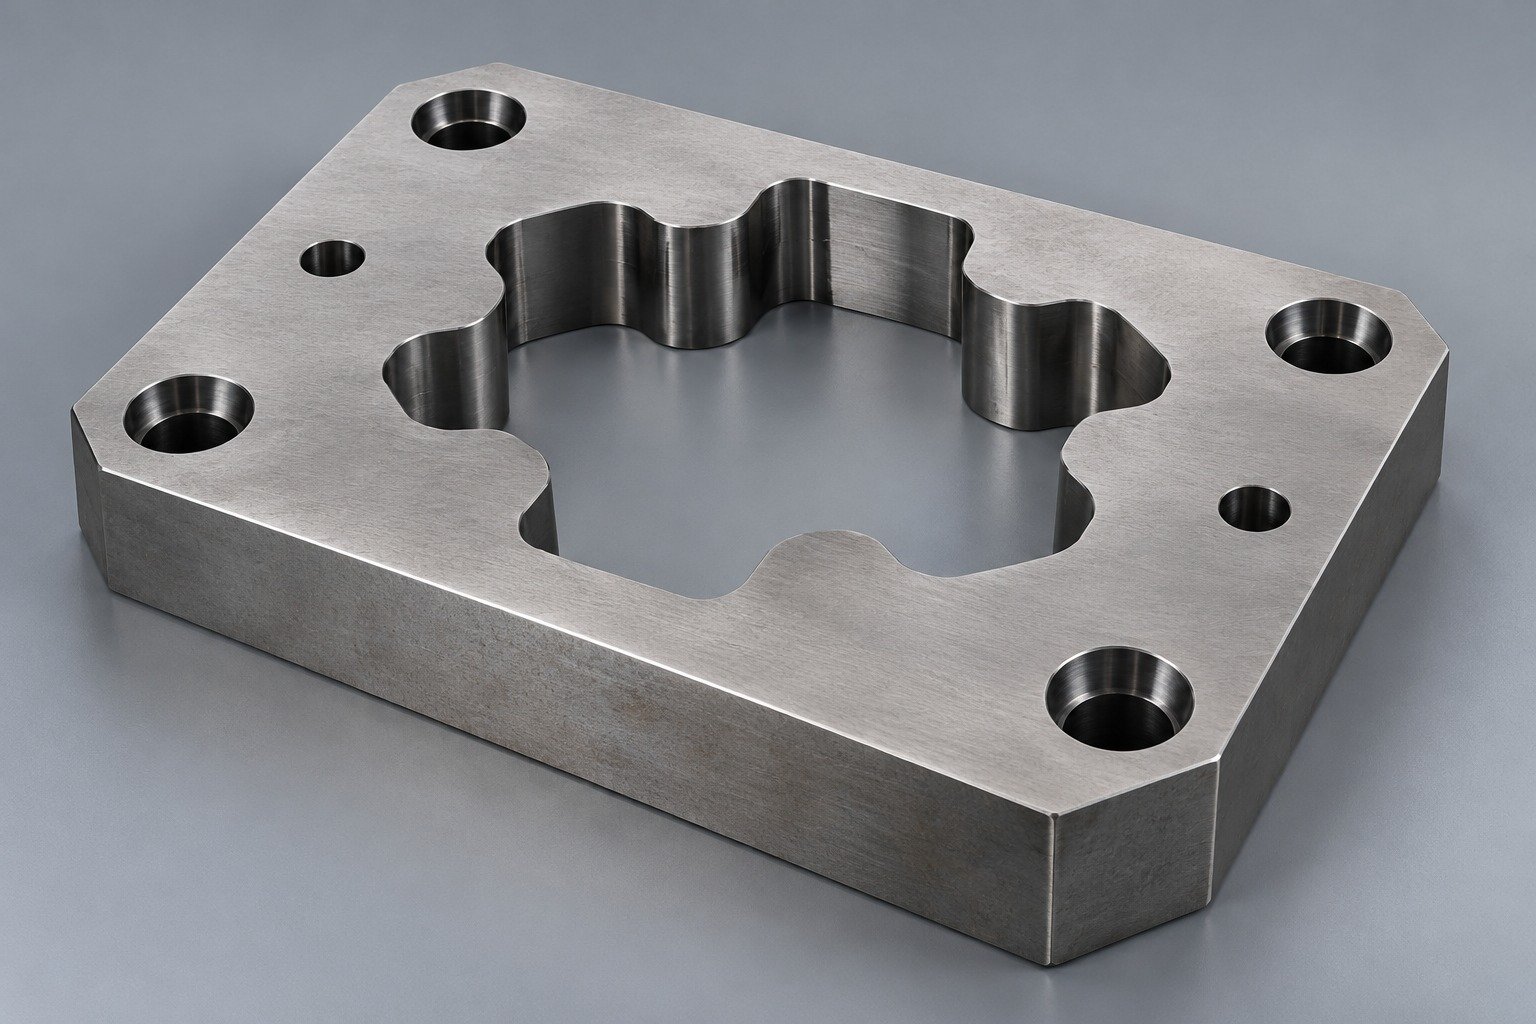
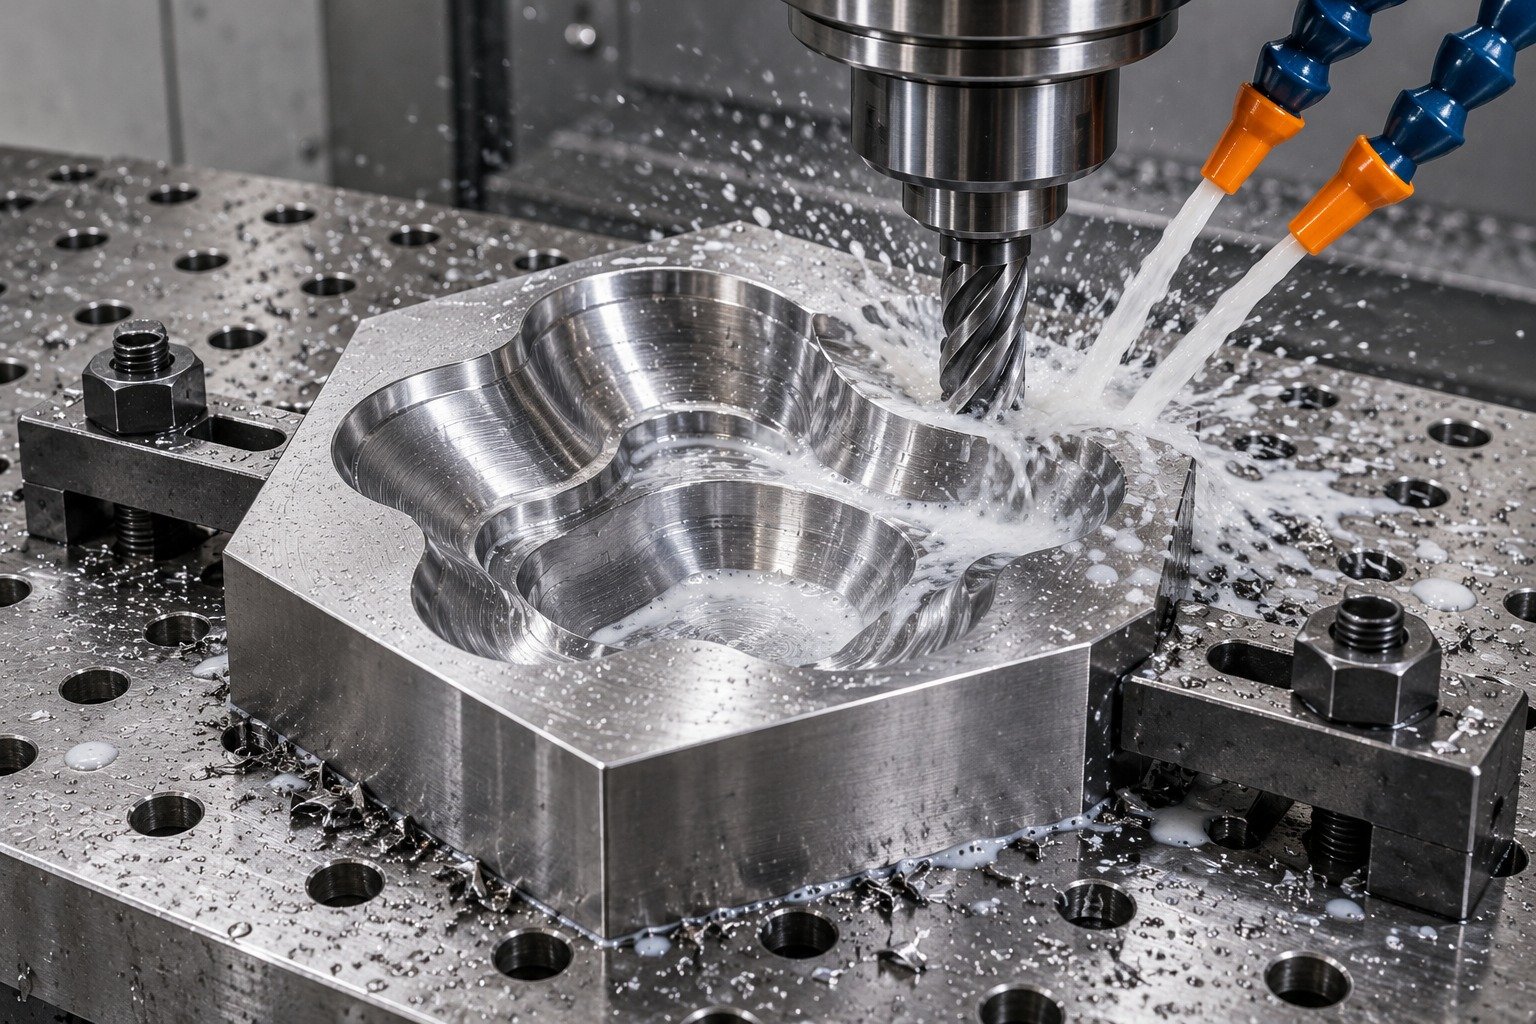
Plan D2 tool steel CNC machining around the relieved profile, accessible corner radii and recoverable datums. Specify which surfaces remain for grinding or EDM.
| Your decision | What to define |
|---|---|
| Your fit | Working profile, clearance, backing and locating bores. |
| Your process | Initial machining, specified treatment and final finishing. |
| Your approval | Controlled drawing, final condition and receiving evidence. |
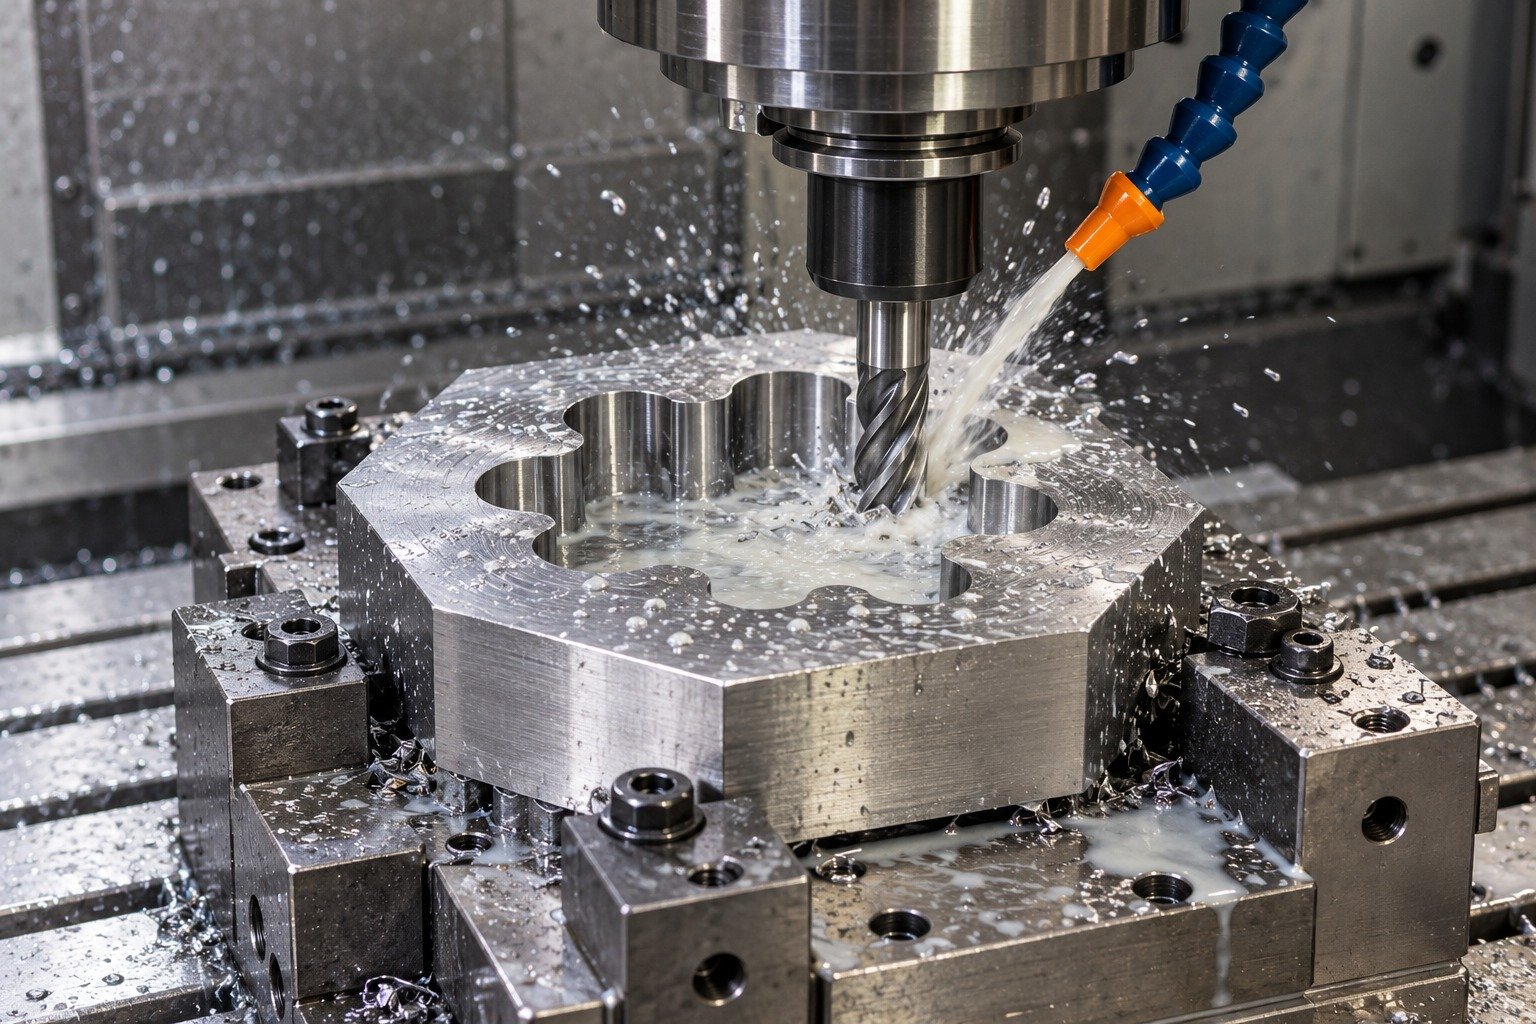
Connect the treatment provider, material condition and remaining stock before heat treatment. Reserve the functional profile for the agreed finishing stage.
| Your decision | What to define |
|---|---|
| Your fit | Working profile, clearance, backing and locating bores. |
| Your process | Initial machining, specified treatment and final finishing. |
| Your approval | Controlled drawing, final condition and receiving evidence. |

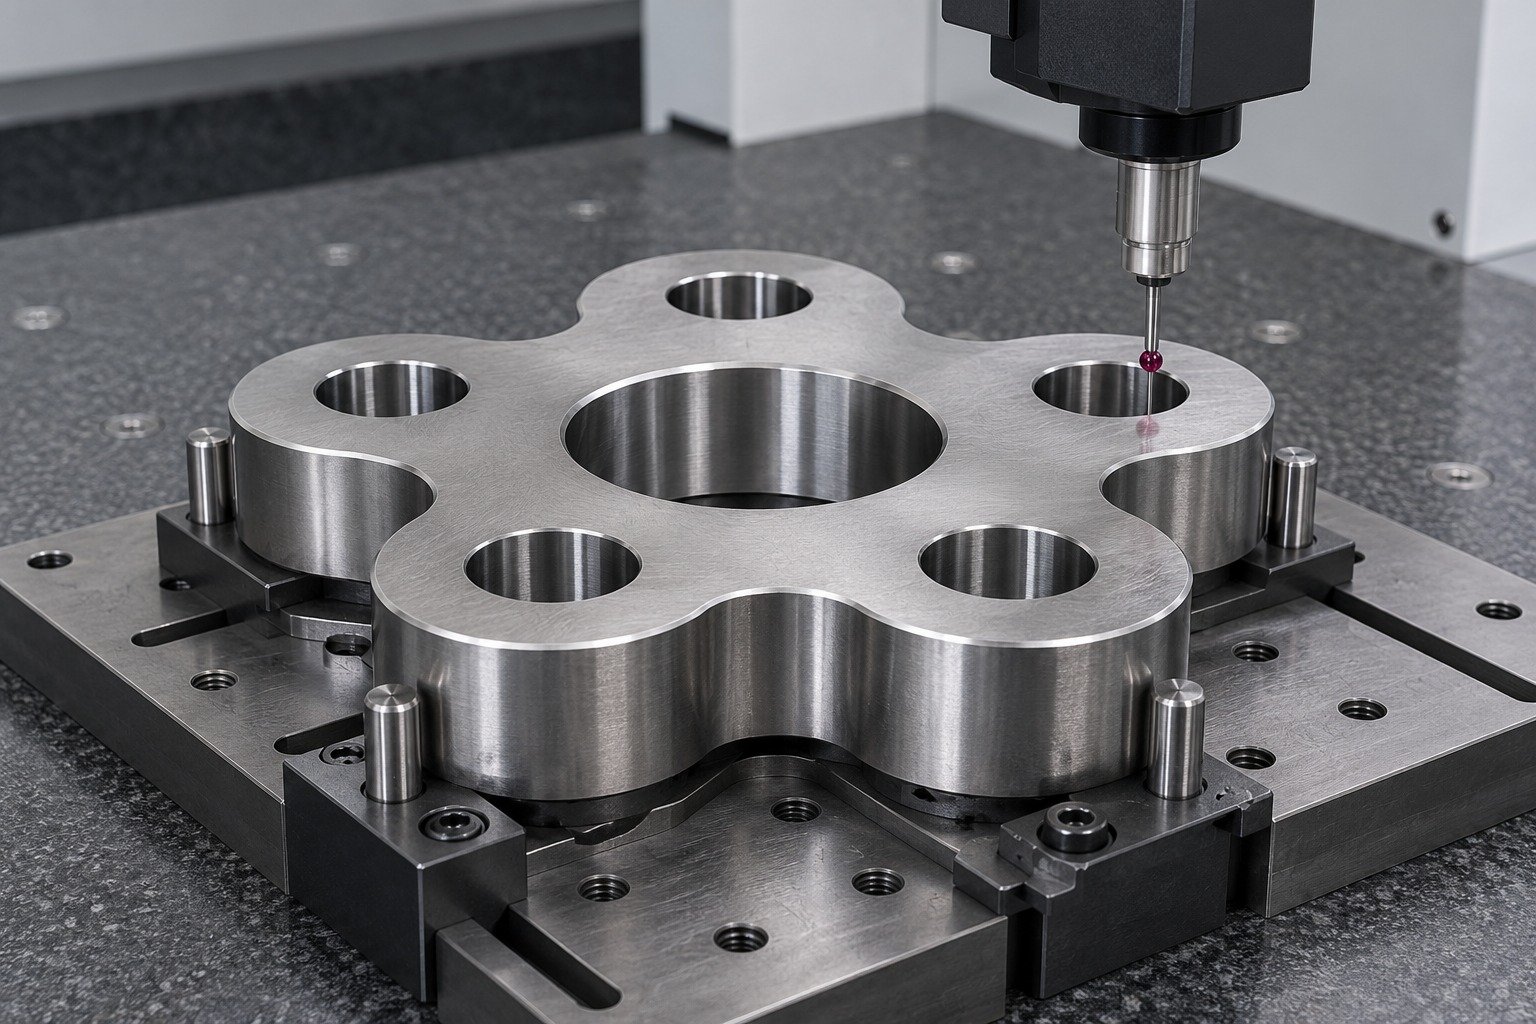
Verify the working profile and locating features after all specified operations. Define the edge acceptance and records with the drawing.
| Your decision | What to define |
|---|---|
| Your fit | Working profile, clearance, backing and locating bores. |
| Your process | Initial machining, specified treatment and final finishing. |
| Your approval | Controlled drawing, final condition and receiving evidence. |
For your D2 tool steel punches, show the working end, supported length and shoulder transitions. Review abrasive wear together with the risk of chipping at unsupported edges.
| Your decision | What to define |
|---|---|
| Your fit | Punch profile, supported shank, shoulder and mating die. |
| Your process | Initial machining, specified treatment and final finishing. |
| Your approval | Controlled drawing, final condition and receiving evidence. |
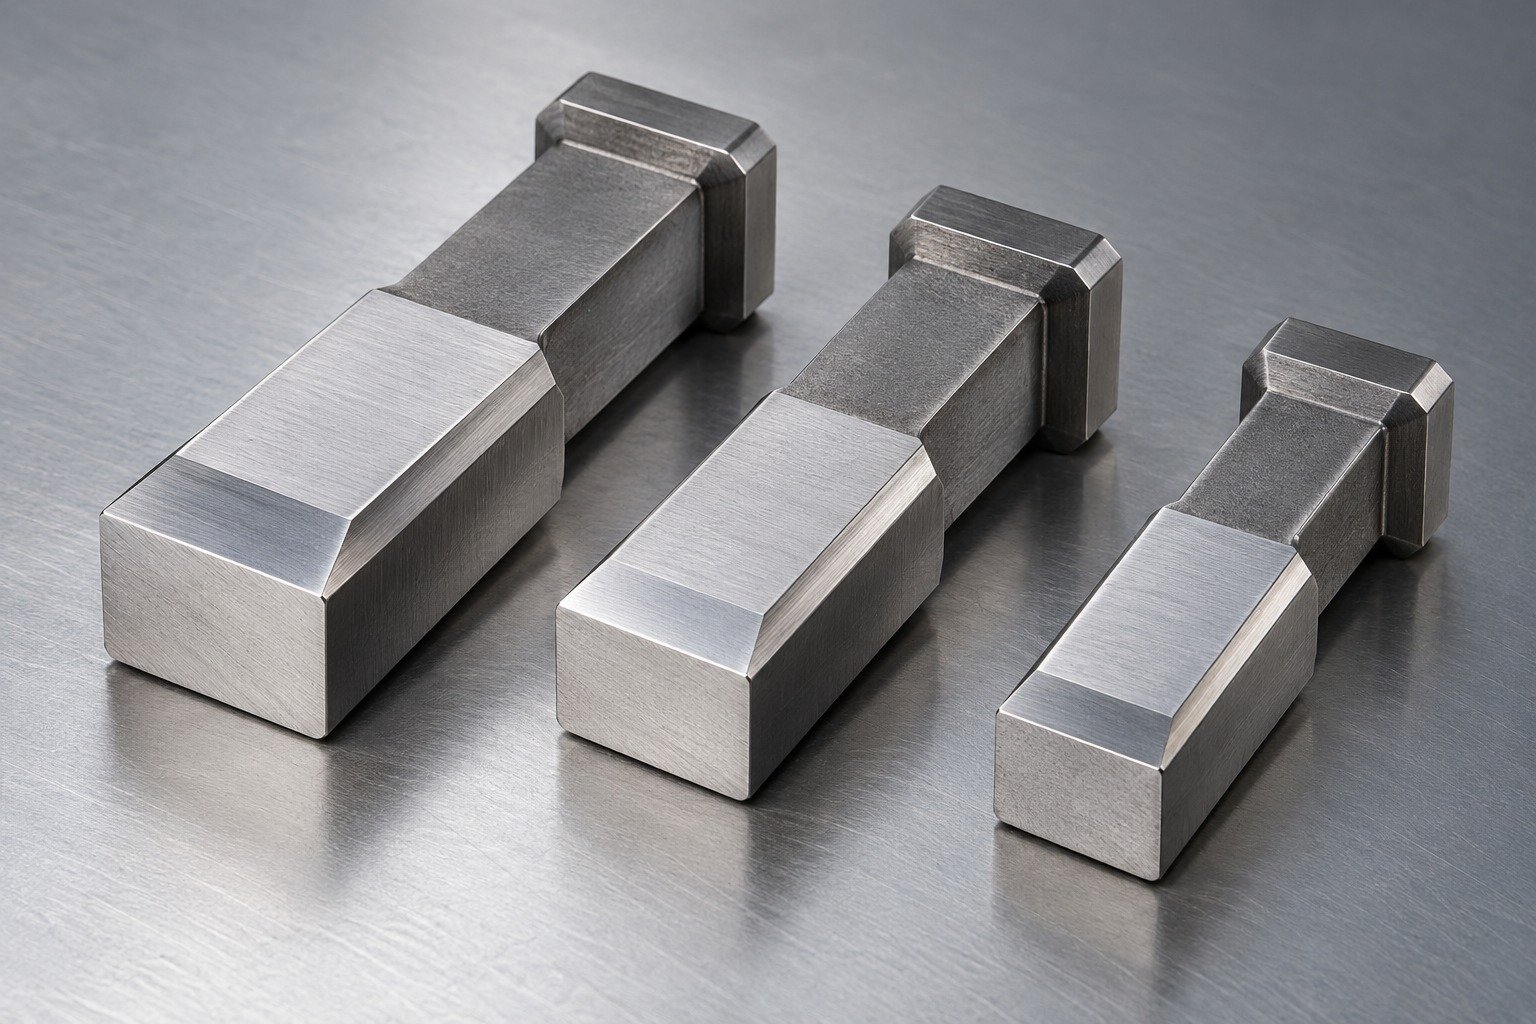
Machine the accessible reliefs and locating shank before final profile finishing. Separate rectangular punch geometry from features suited to D2 tool steel turning.
| Your decision | What to define |
|---|---|
| Your fit | Punch profile, supported shank, shoulder and mating die. |
| Your process | Initial machining, specified treatment and final finishing. |
| Your approval | Controlled drawing, final condition and receiving evidence. |

Specify the required working condition and test locations. Agree how shank alignment and the final working end are recovered after treatment.
| Your decision | What to define |
|---|---|
| Your fit | Punch profile, supported shank, shoulder and mating die. |
| Your process | Initial machining, specified treatment and final finishing. |
| Your approval | Controlled drawing, final condition and receiving evidence. |
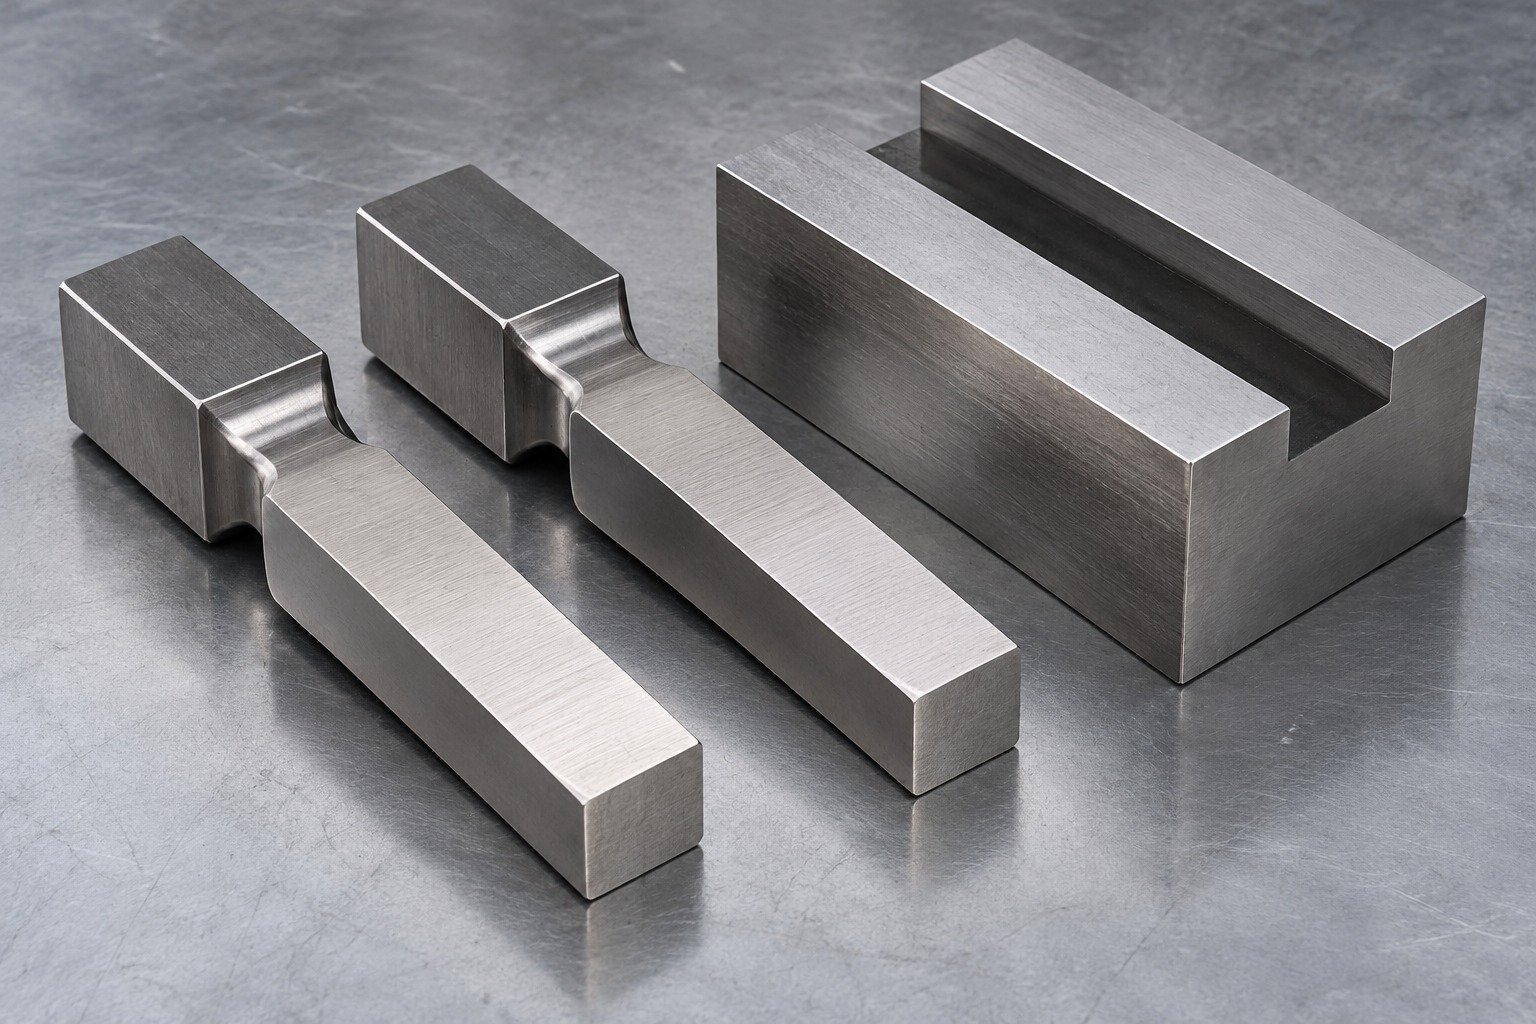
Measure the final working profile, shank relationship and supported shoulder. Define handling protection for the finished working end.
| Your decision | What to define |
|---|---|
| Your fit | Punch profile, supported shank, shoulder and mating die. |
| Your process | Initial machining, specified treatment and final finishing. |
| Your approval | Controlled drawing, final condition and receiving evidence. |
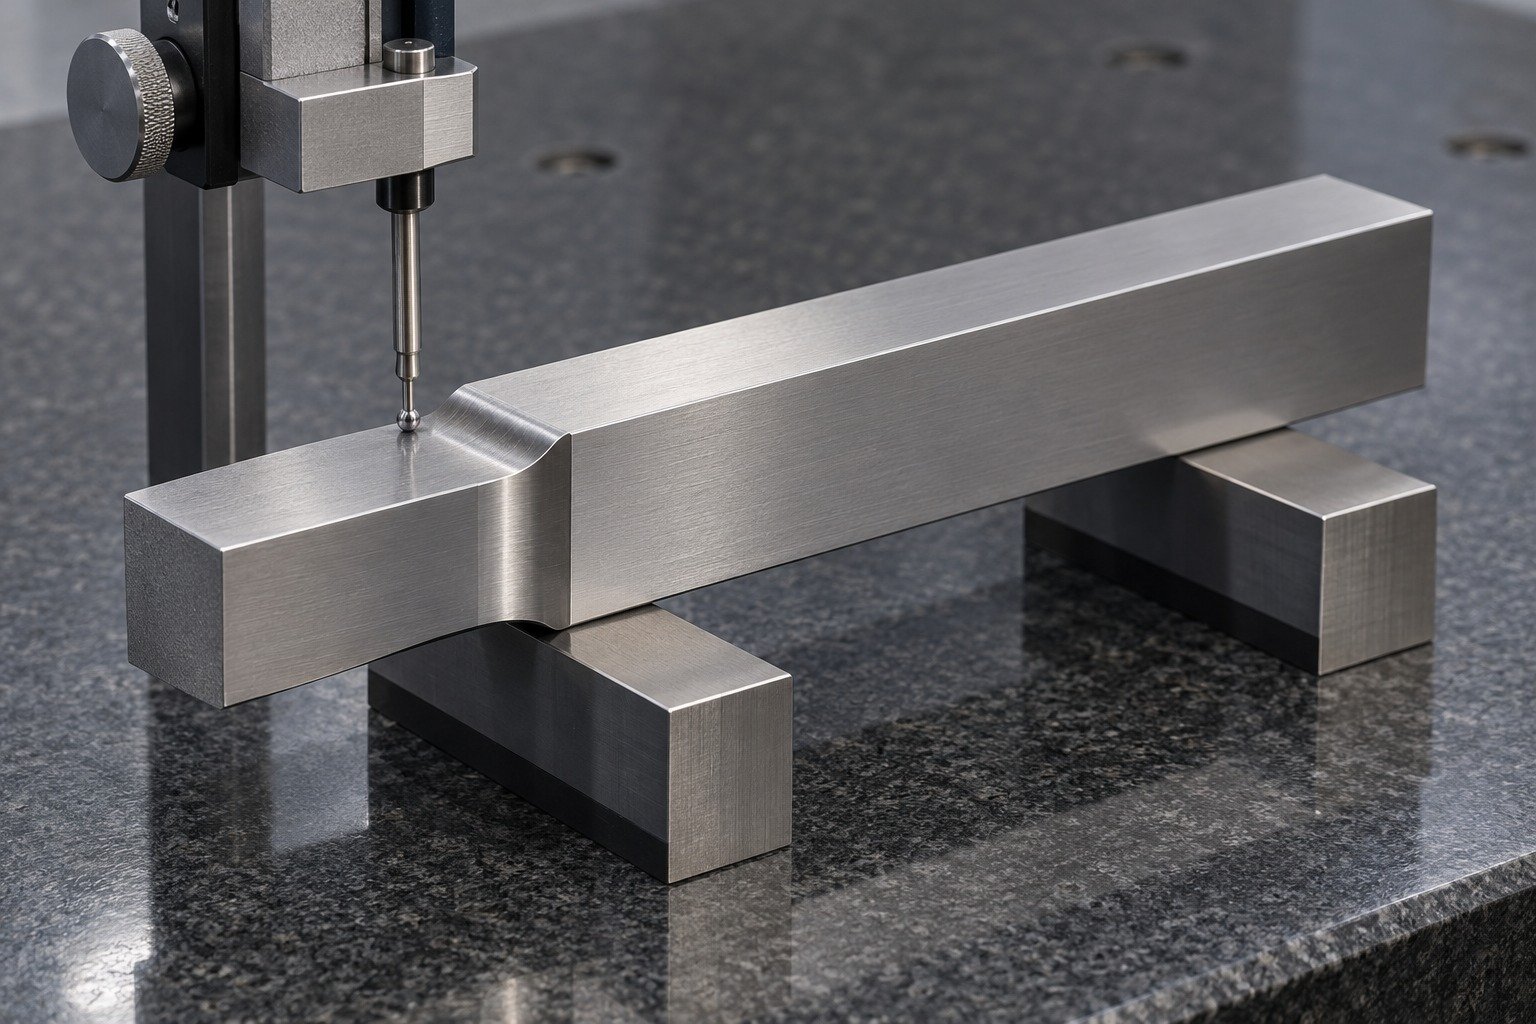
For your D2 tool steel wear parts, specify the contact pair, sliding path, support and contamination. A wear-resistant material choice still needs a defined finished surface.
| Your decision | What to define |
|---|---|
| Your fit | Sliding contact, mounting counterbores and supported section. |
| Your process | Initial machining, specified treatment and final finishing. |
| Your approval | Controlled drawing, final condition and receiving evidence. |

For D2 tool steel milling, define the clamping face, relief geometry and machining sequence. Keep thin sections and mounting faces accessible for the final operations.
| Your decision | What to define |
|---|---|
| Your fit | Sliding contact, mounting counterbores and supported section. |
| Your process | Initial machining, specified treatment and final finishing. |
| Your approval | Controlled drawing, final condition and receiving evidence. |
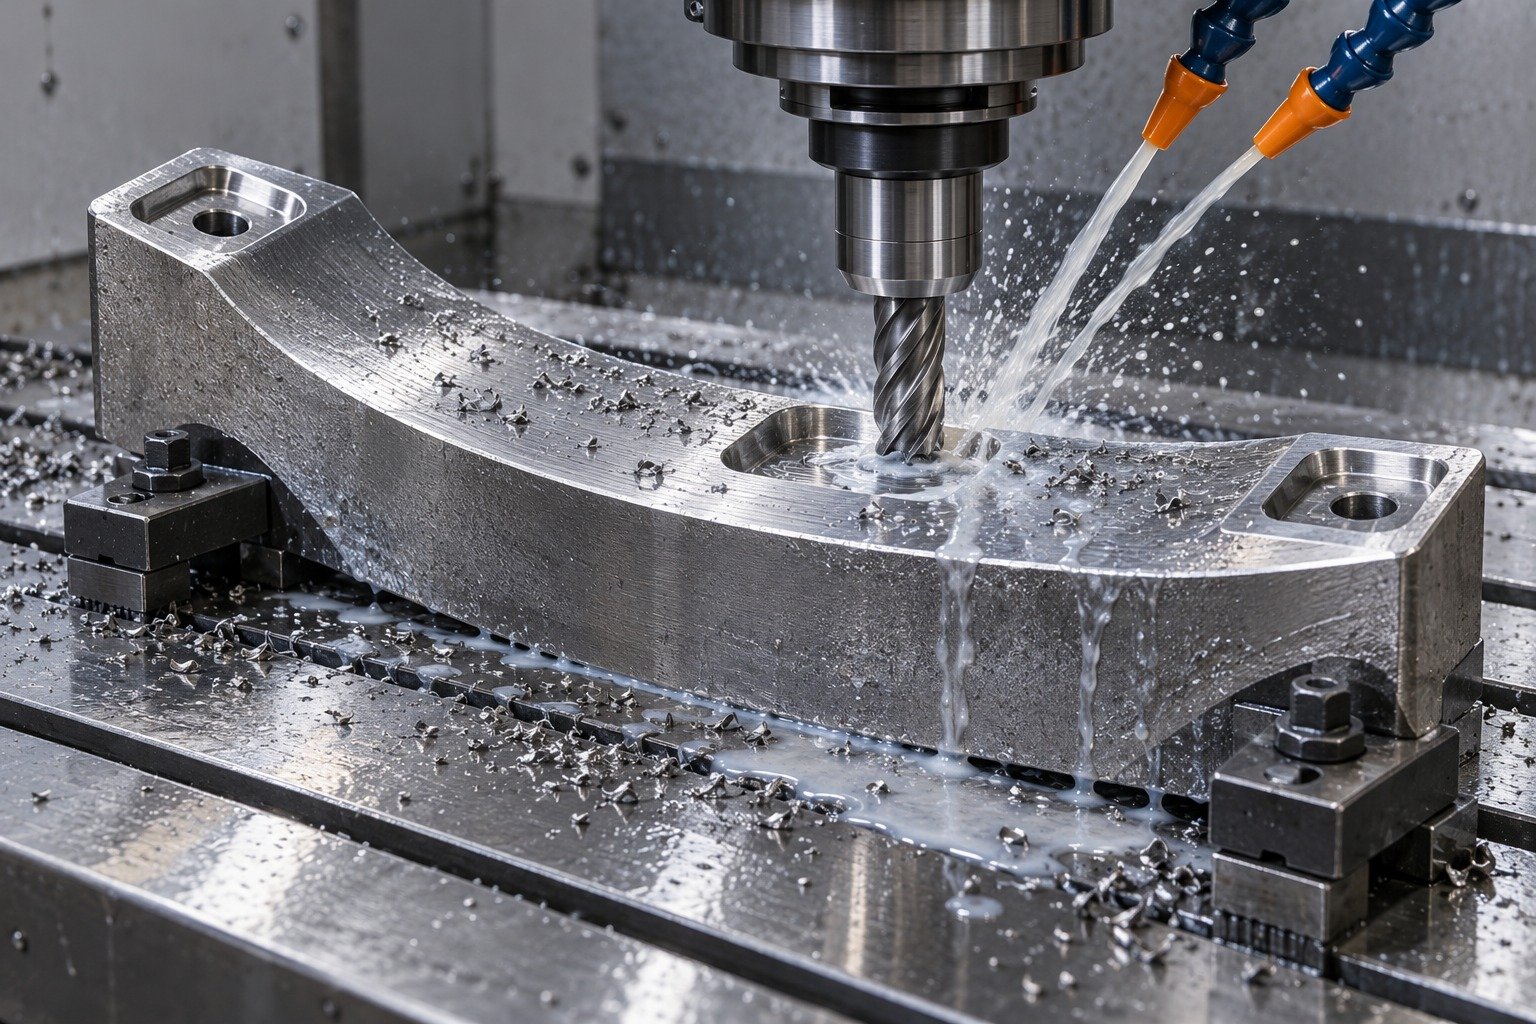
Review uneven material removal and the specified thermal route before final grinding. Define allowance by surface rather than borrowing a value from another part.
| Your decision | What to define |
|---|---|
| Your fit | Sliding contact, mounting counterbores and supported section. |
| Your process | Initial machining, specified treatment and final finishing. |
| Your approval | Controlled drawing, final condition and receiving evidence. |
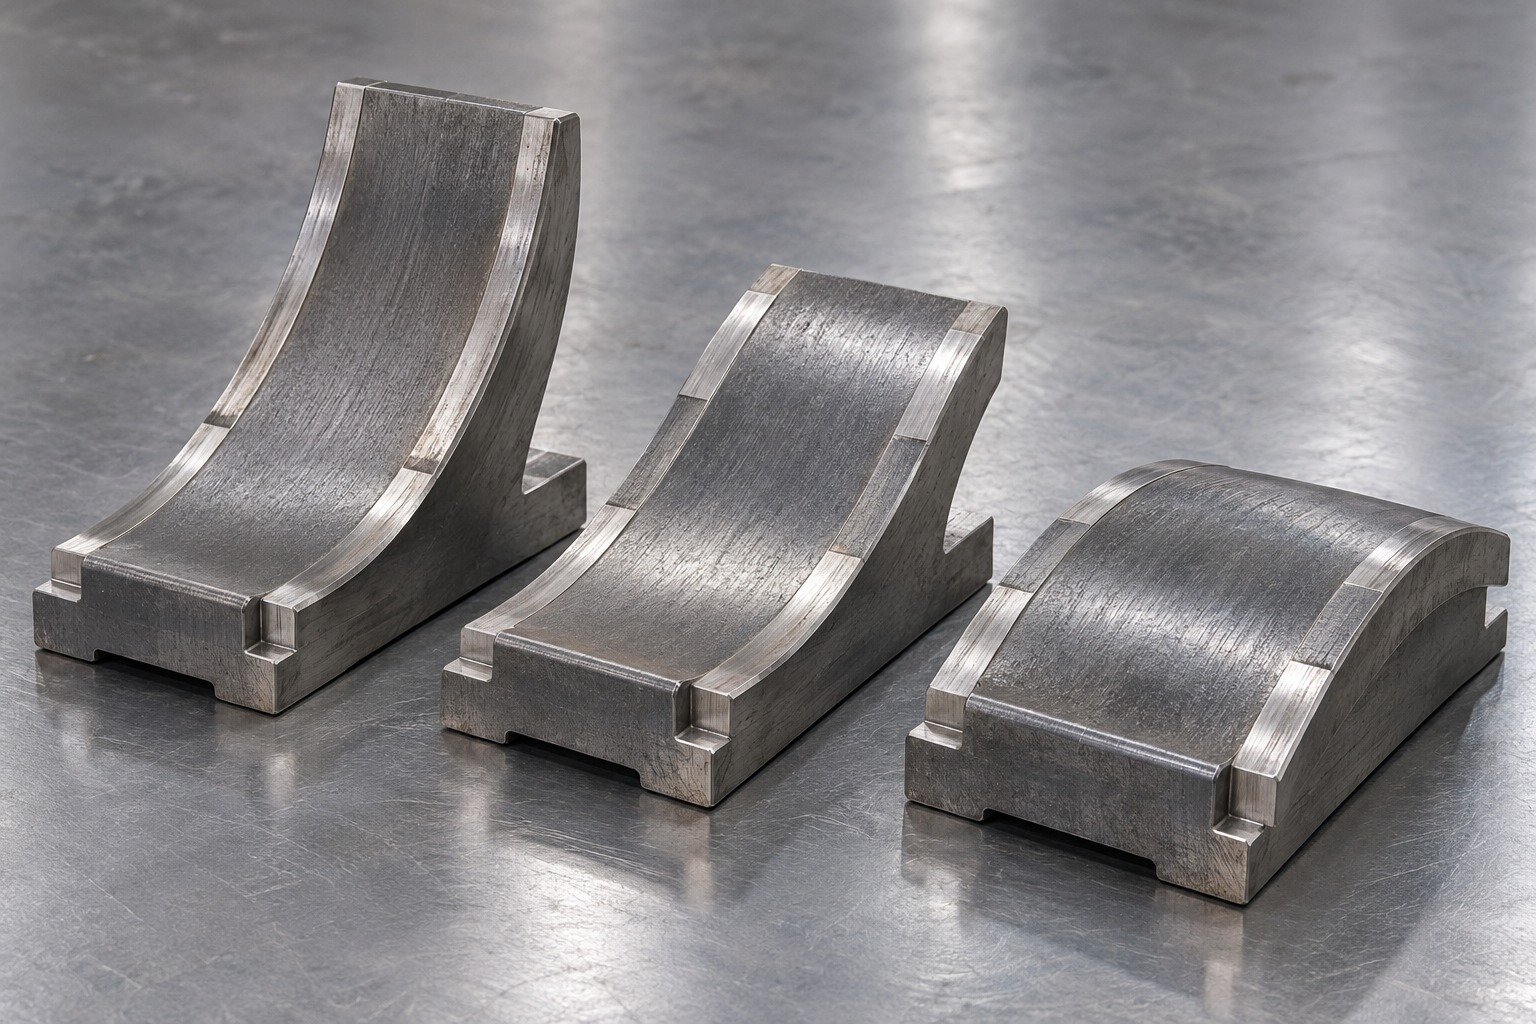
Verify thickness, mounting position and contact-face geometry. State the surface condition and protection your receiving team will accept.
| Your decision | What to define |
|---|---|
| Your fit | Sliding contact, mounting counterbores and supported section. |
| Your process | Initial machining, specified treatment and final finishing. |
| Your approval | Controlled drawing, final condition and receiving evidence. |

For a D2 forming roll or tooling sleeve, show the working contour, keyed bore and shaft relationship. Review the actual duty before approving a grade or working hardness.
| Your decision | What to define |
|---|---|
| Your fit | Working groove, bore fit, keyway and locating land. |
| Your process | Initial machining, specified treatment and final finishing. |
| Your approval | Controlled drawing, final condition and receiving evidence. |
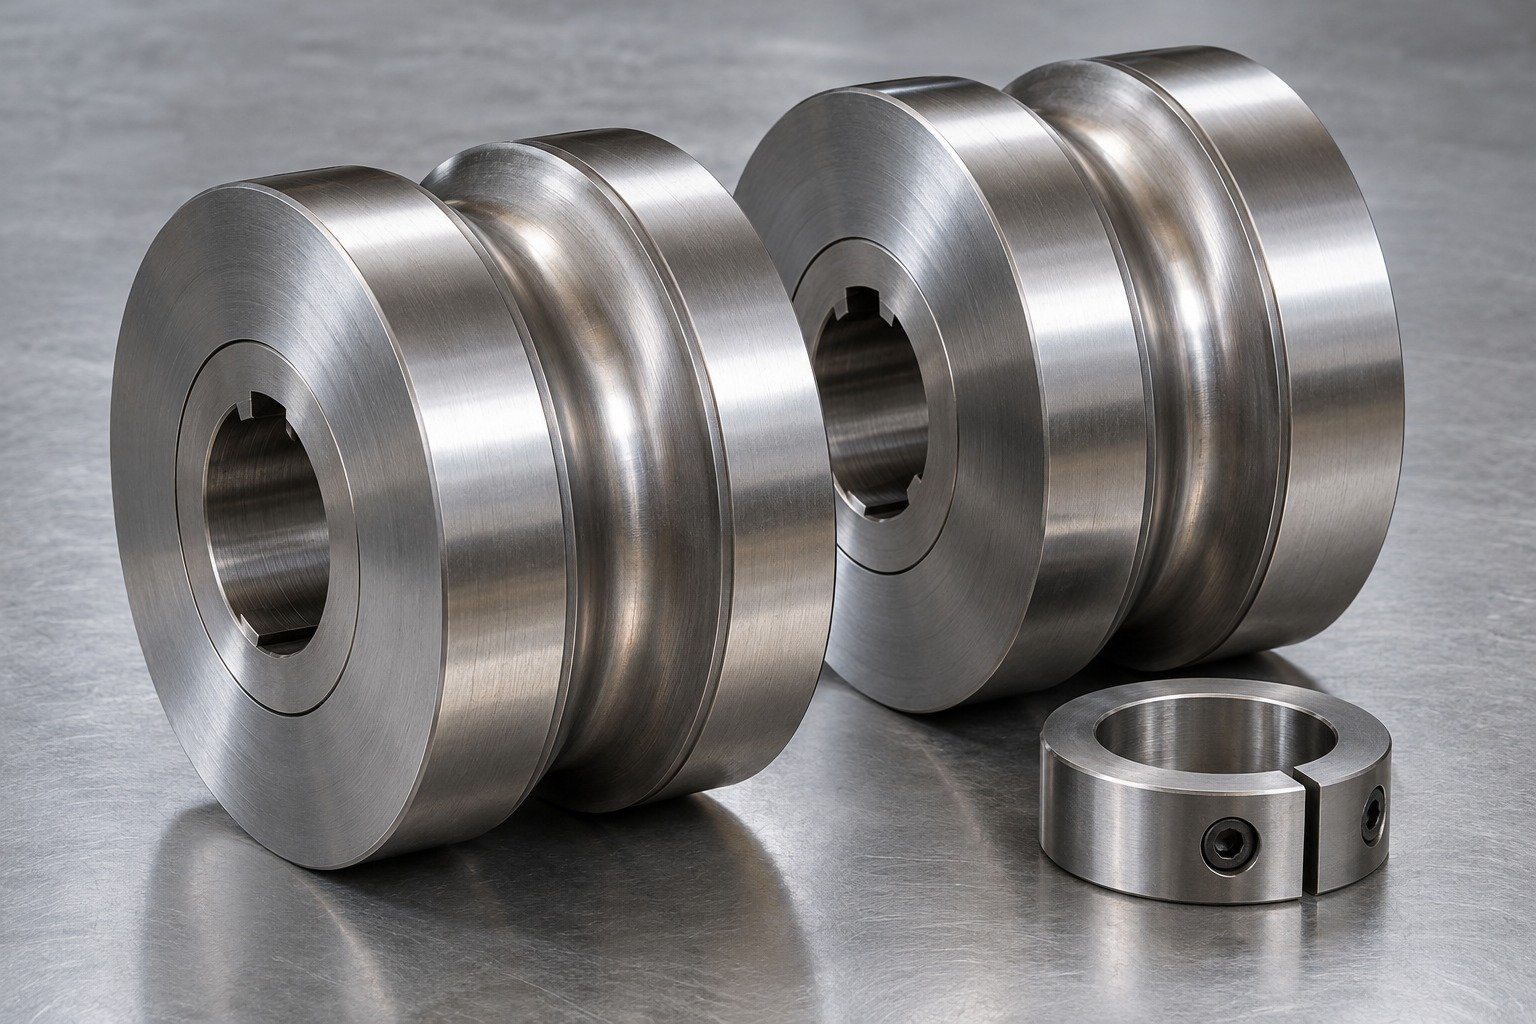
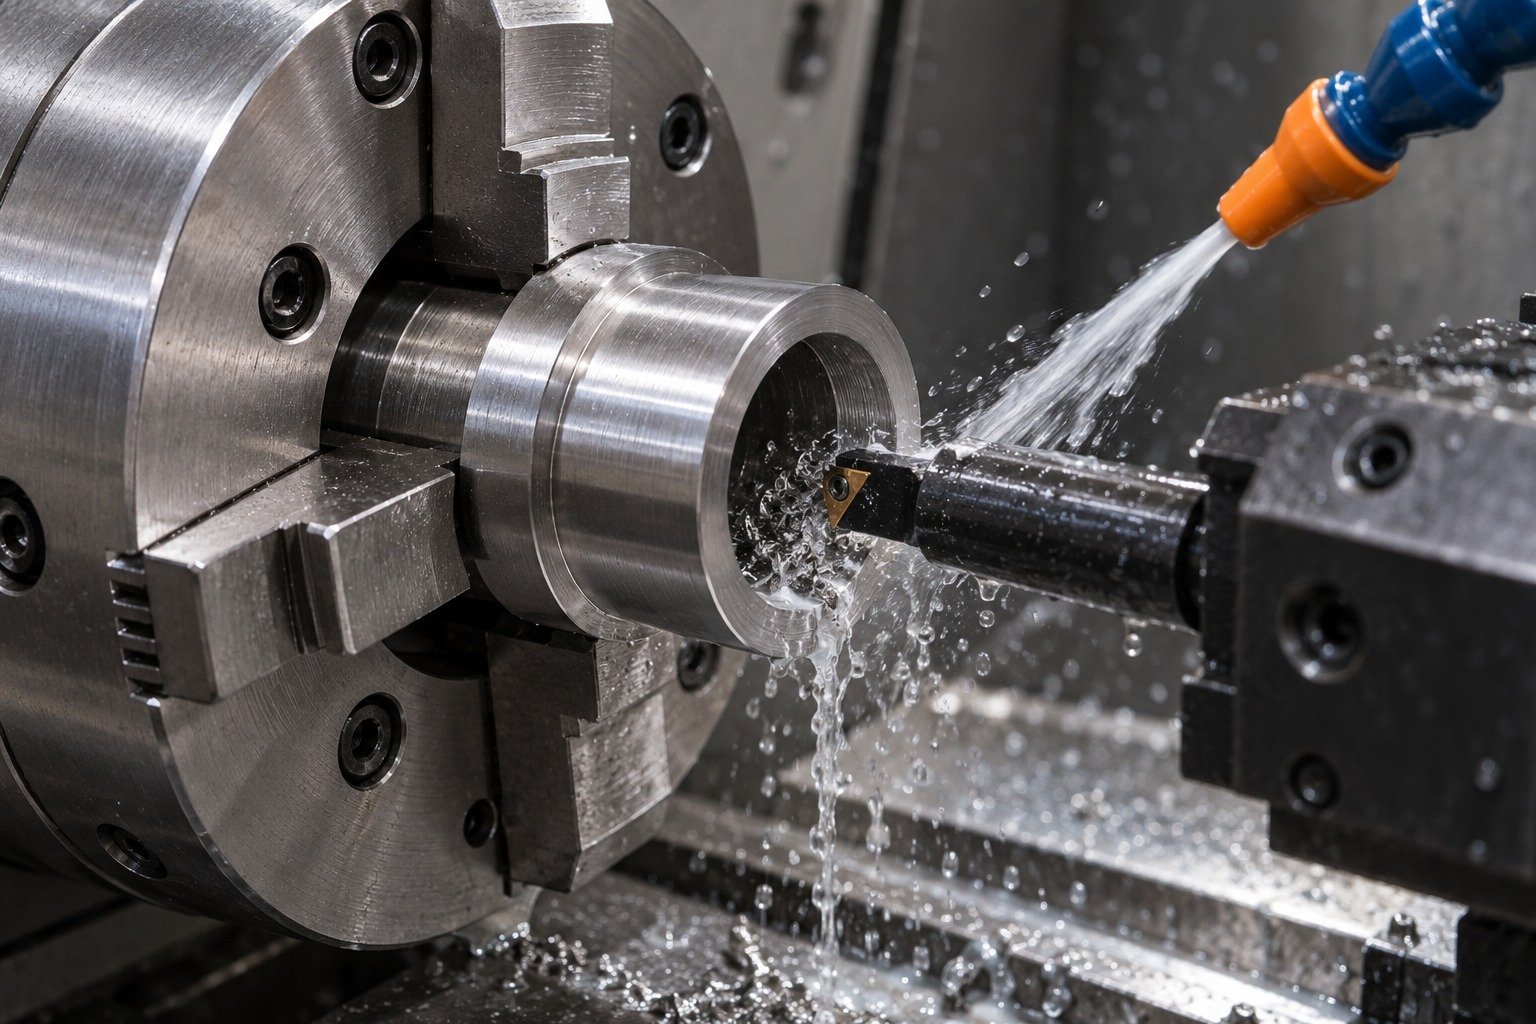
Plan the turning and bore sequence with suitable workholding. Identify which contour and locating surfaces need grinding after the specified treatment.
| Your decision | What to define |
|---|---|
| Your fit | Working groove, bore fit, keyway and locating land. |
| Your process | Initial machining, specified treatment and final finishing. |
| Your approval | Controlled drawing, final condition and receiving evidence. |

Connect the working contour and locating bore to the selected final condition. Plan the finishing route before closing the keyed fit.
| Your decision | What to define |
|---|---|
| Your fit | Working groove, bore fit, keyway and locating land. |
| Your process | Initial machining, specified treatment and final finishing. |
| Your approval | Controlled drawing, final condition and receiving evidence. |

Check runout, groove profile and bore relationships from the final datum scheme. Agree measurement and handling requirements for the finished roll.
| Your decision | What to define |
|---|---|
| Your fit | Working groove, bore fit, keyway and locating land. |
| Your process | Initial machining, specified treatment and final finishing. |
| Your approval | Controlled drawing, final condition and receiving evidence. |

Connect D2 tool steel heat treatment to finishing and inspection before approving the first production route.
Identify D2 product form, delivered condition and required material records. D2 tool steel machinability depends on the actual stock and operation, not only the grade label.
Show the controlled feature and final state.
Agree remaining stock for the actual route.
Verify the finished fit and specified condition.
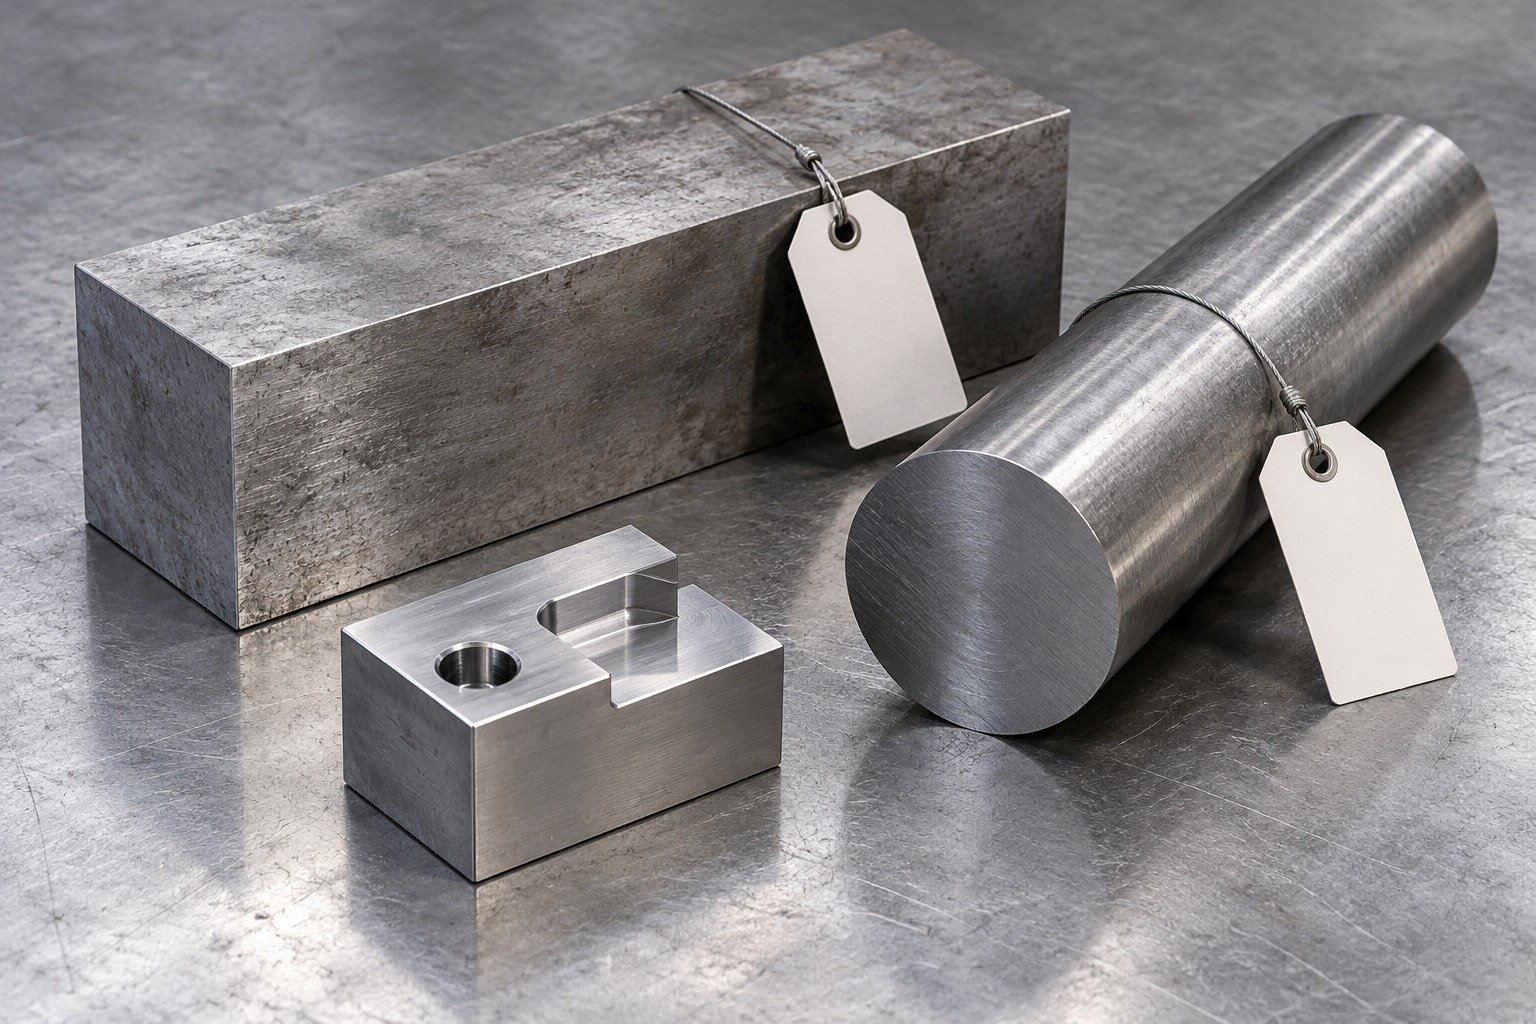
Separate mounting threads and datum bores from the working profile. Mark drilling access, thread runouts and features that need finishing after treatment.
Show the controlled feature and final state.
Agree remaining stock for the actual route.
Verify the finished fit and specified condition.
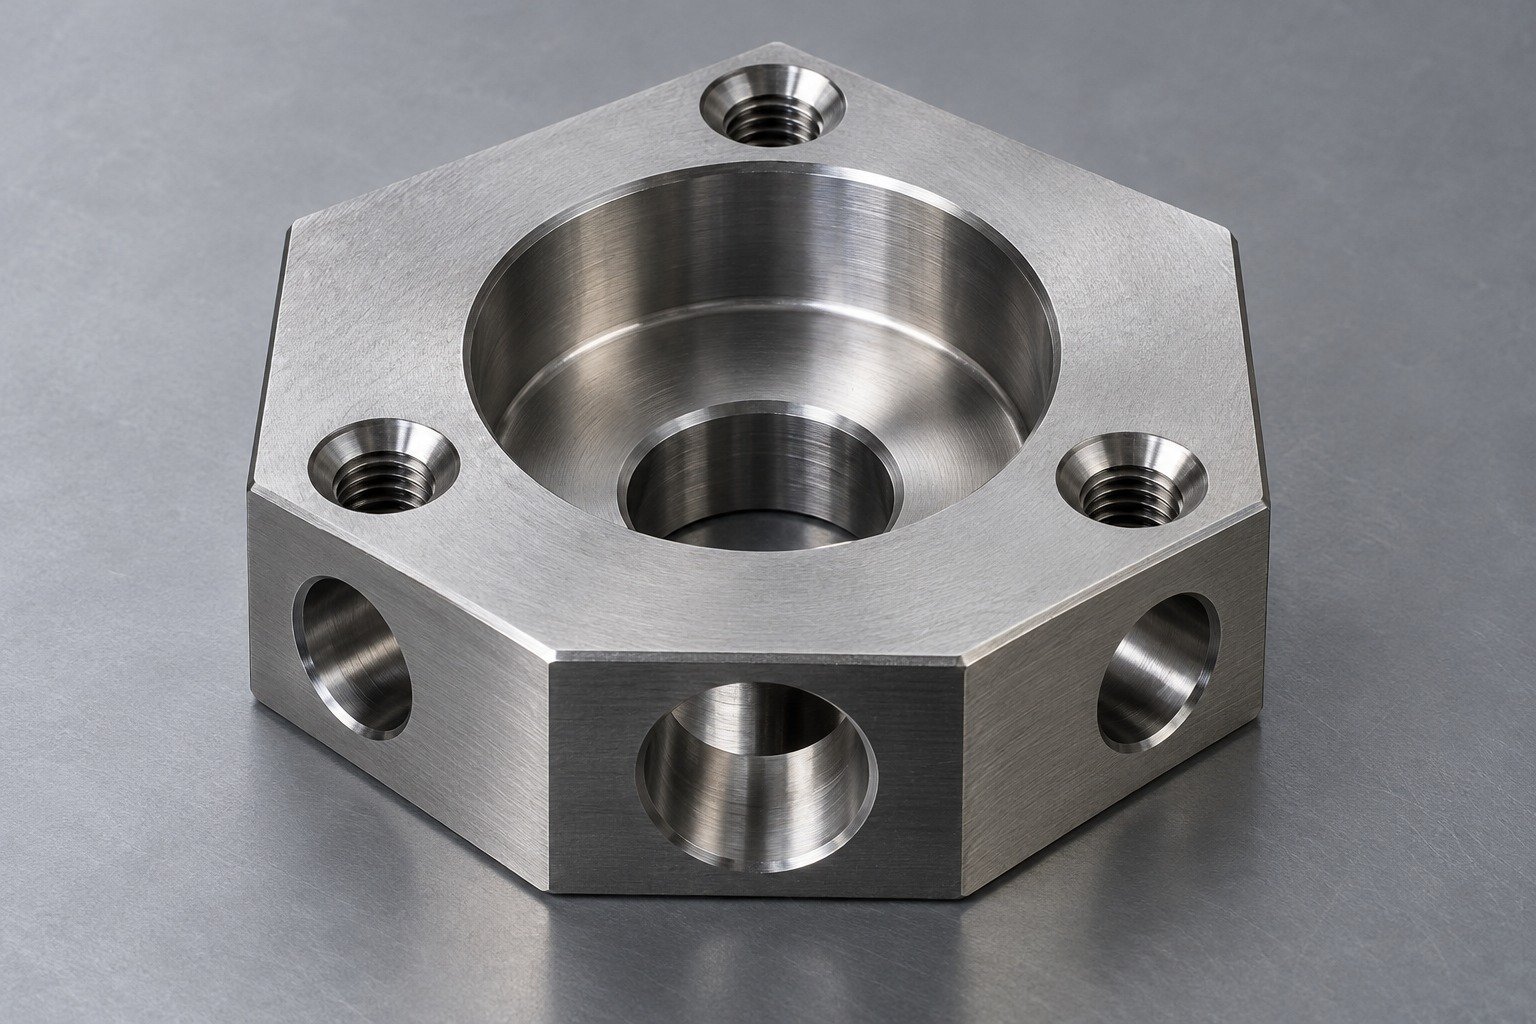
Define treatment responsibility, target condition and recoverable datums. Agree the remaining finishing stock for the actual section and final dimensional requirement.
Show the controlled feature and final state.
Agree remaining stock for the actual route.
Verify the finished fit and specified condition.
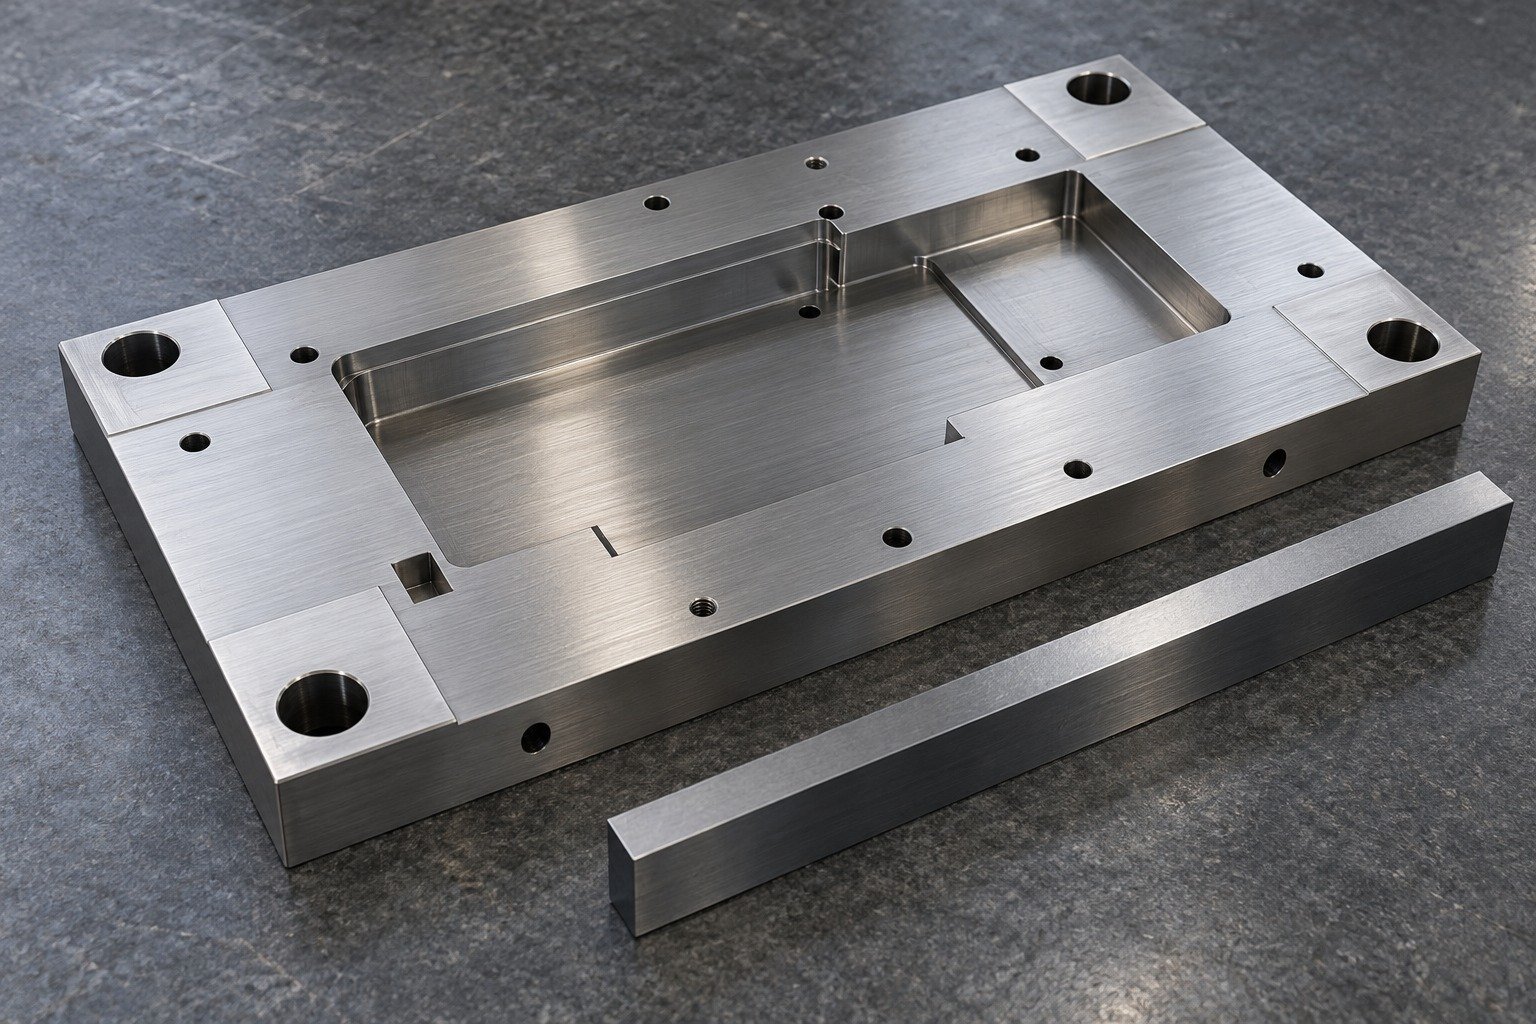
Show the edge land, corner radius and mating clearance. Compare wear needs with local impact and edge support before approving the tooling material.
Show the controlled feature and final state.
Agree remaining stock for the actual route.
Verify the finished fit and specified condition.
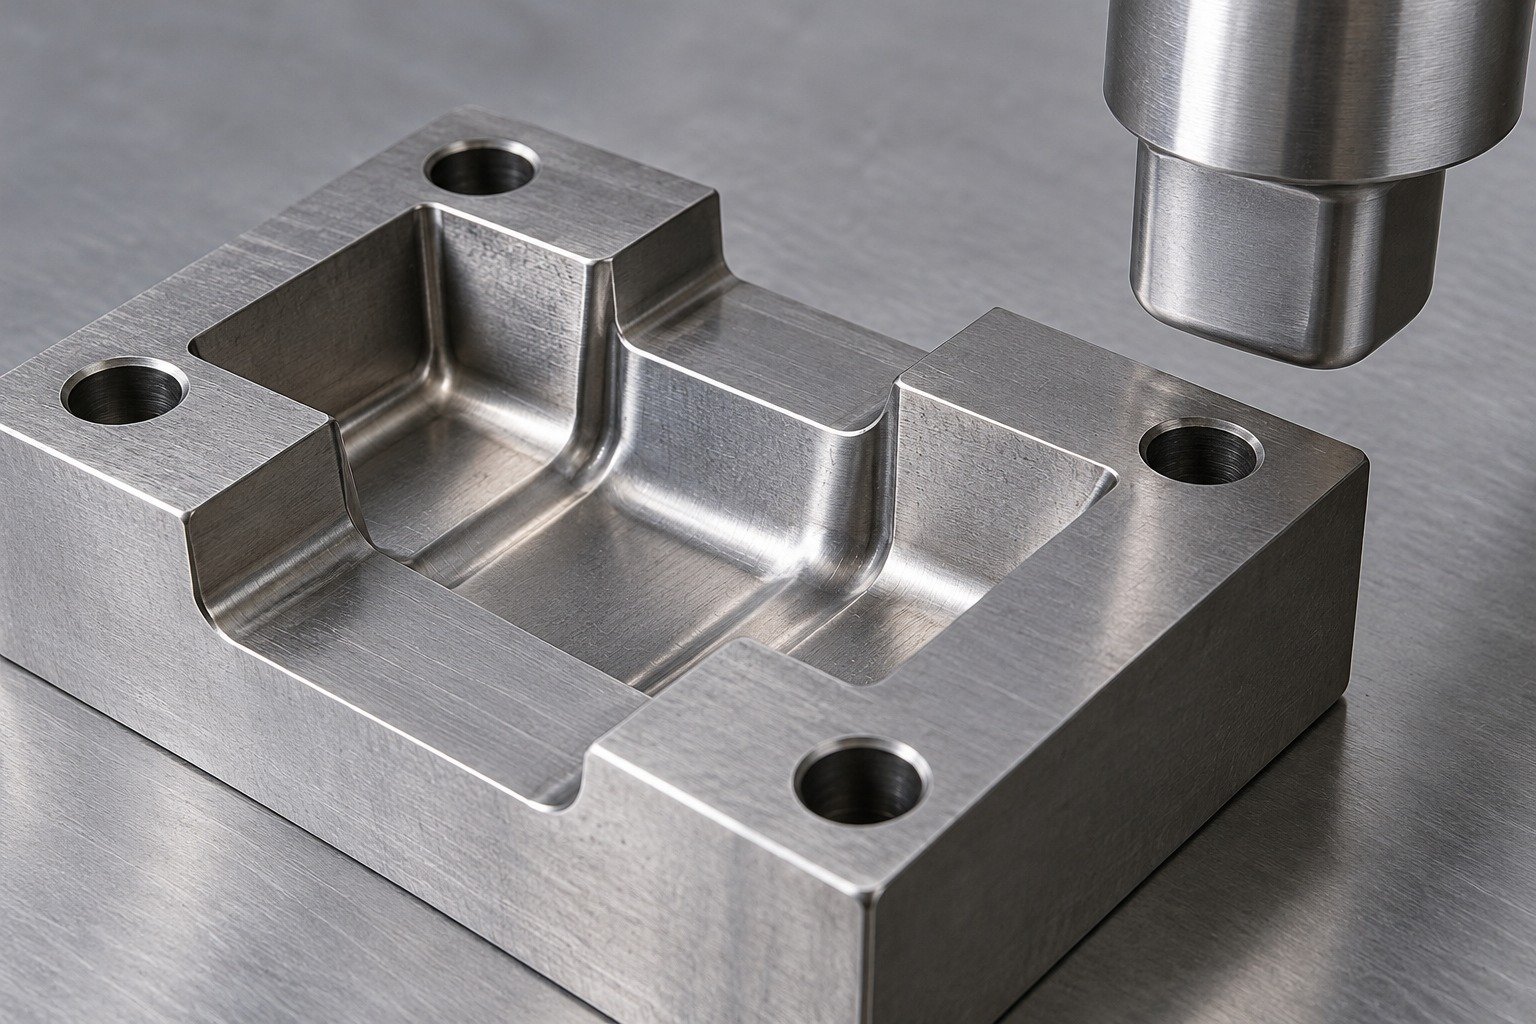
For D2 tool steel grinding after heat treatment, define surface condition, final allowance and the acceptance of critical faces. Include the required review for grinding burn or surface damage.
Show the controlled feature and final state.
Agree remaining stock for the actual route.
Verify the finished fit and specified condition.
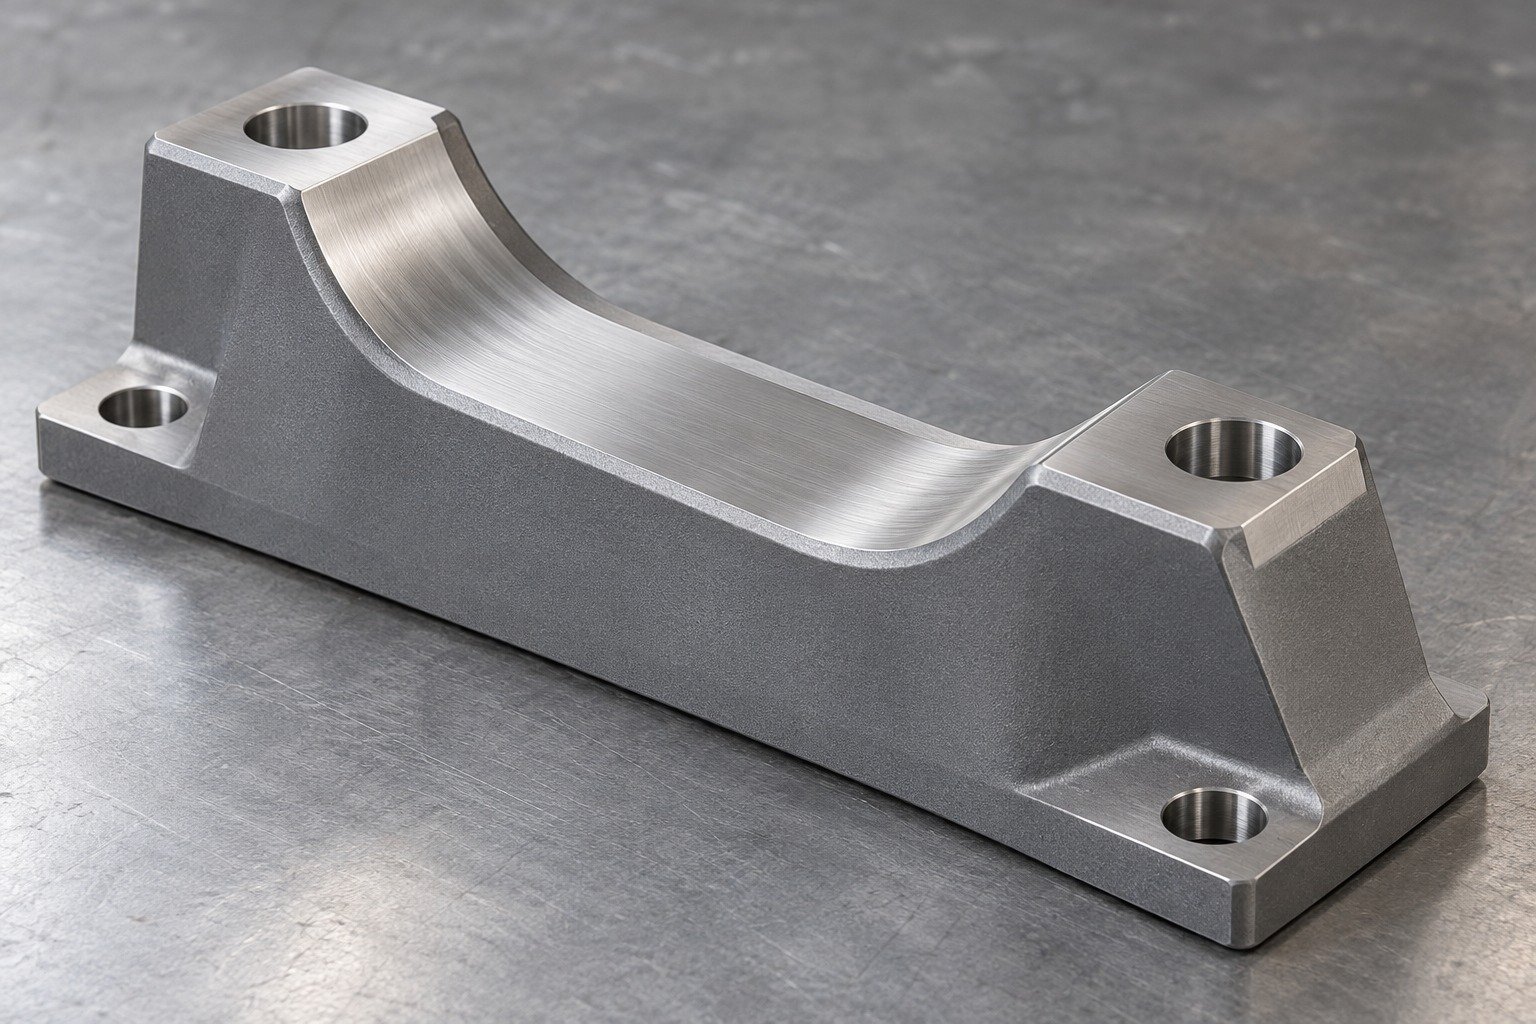
D2 tool steel machining tolerances belong to the controlled drawing and agreed manufacturing route. Define final measurement state, datums and required inspection evidence.
Show the controlled feature and final state.
Agree remaining stock for the actual route.
Verify the finished fit and specified condition.
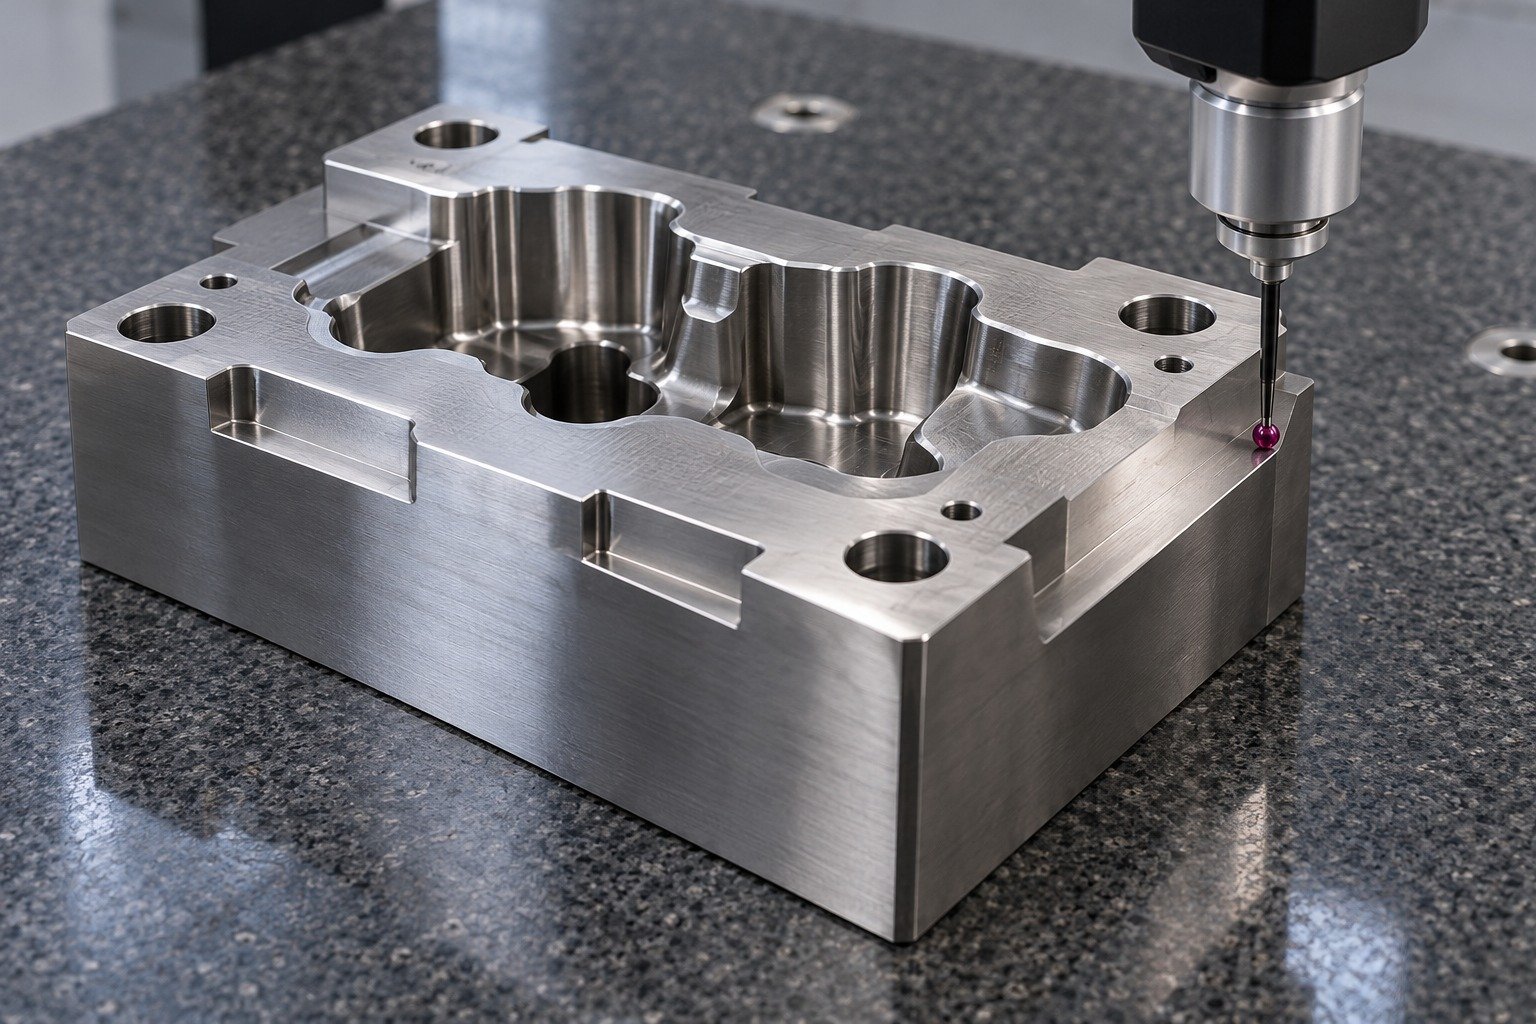
Identity, stock form and supplied condition.
Working condition and remaining finish stock.
Functional features, protection and records.
Verify D2 identity, product form, supplied condition and required lot evidence before releasing the machining route.
Sampling and document scope are agreed with your quotation.
Quality Assurance →
Review remaining stock, reference faces and the planned treatment and finishing responsibility before repeating the process.
Sampling and document scope are agreed with your quotation.
Quality Assurance →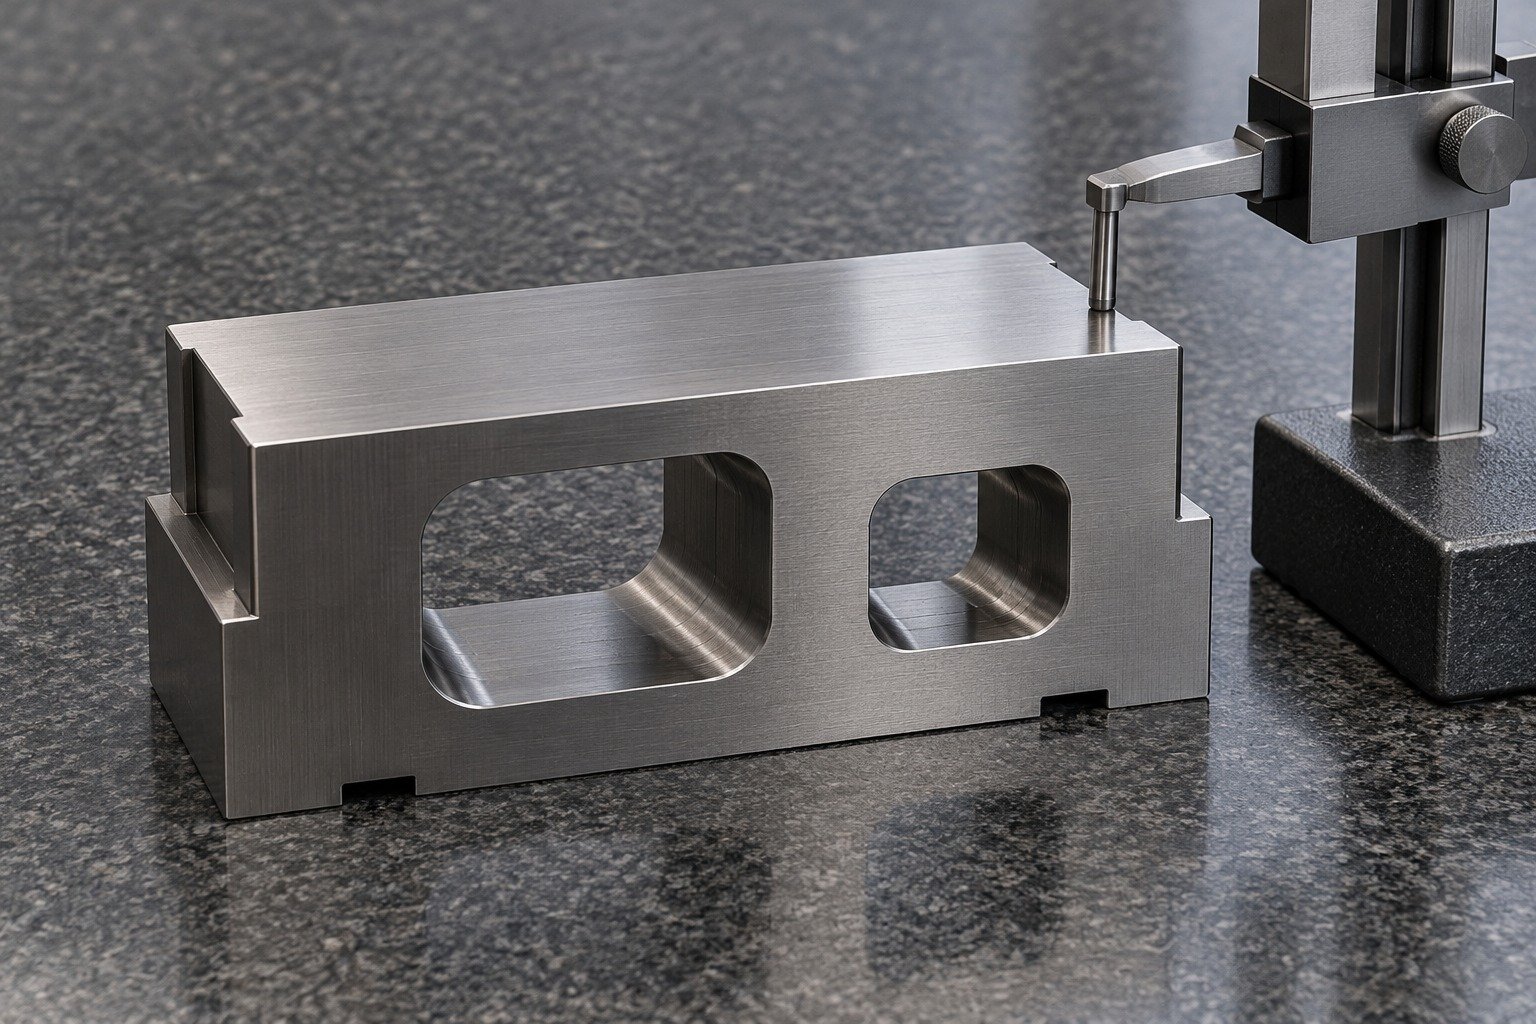
Check the agreed locating geometry and working profile after the complete route. Define the required review for grinding damage or EDM surface condition.
Sampling and document scope are agreed with your quotation.
Quality Assurance →
Agree edge protection, identification, packaging and the inspection records needed to release the tool at your receiving location.
Sampling and document scope are agreed with your quotation.
Quality Assurance →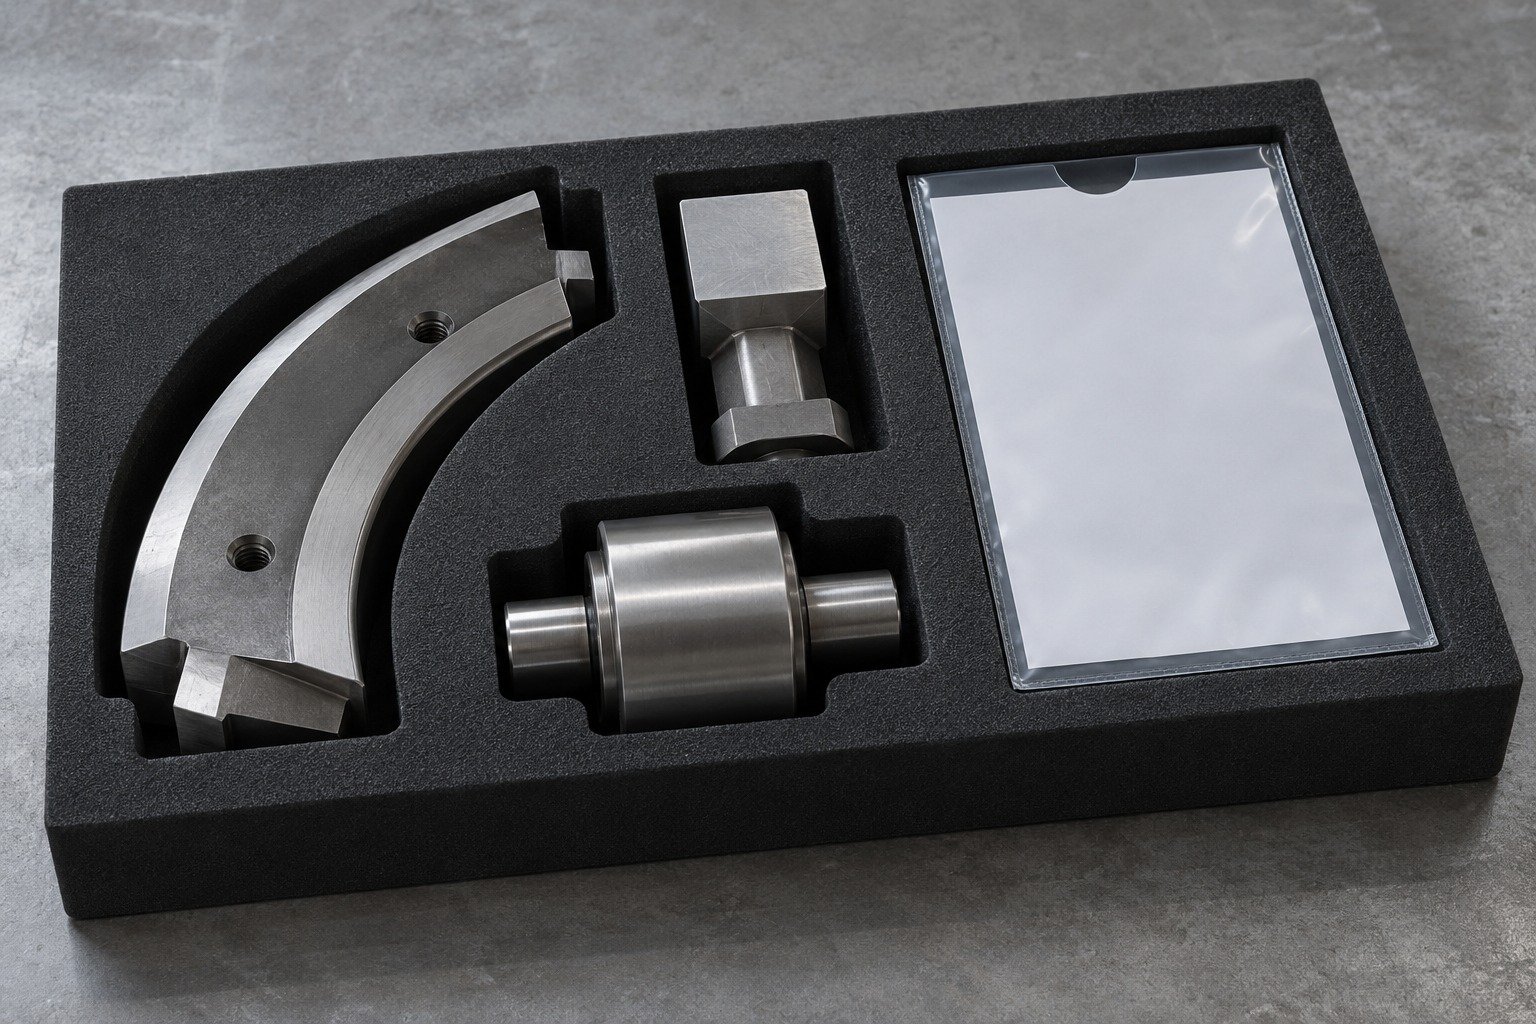
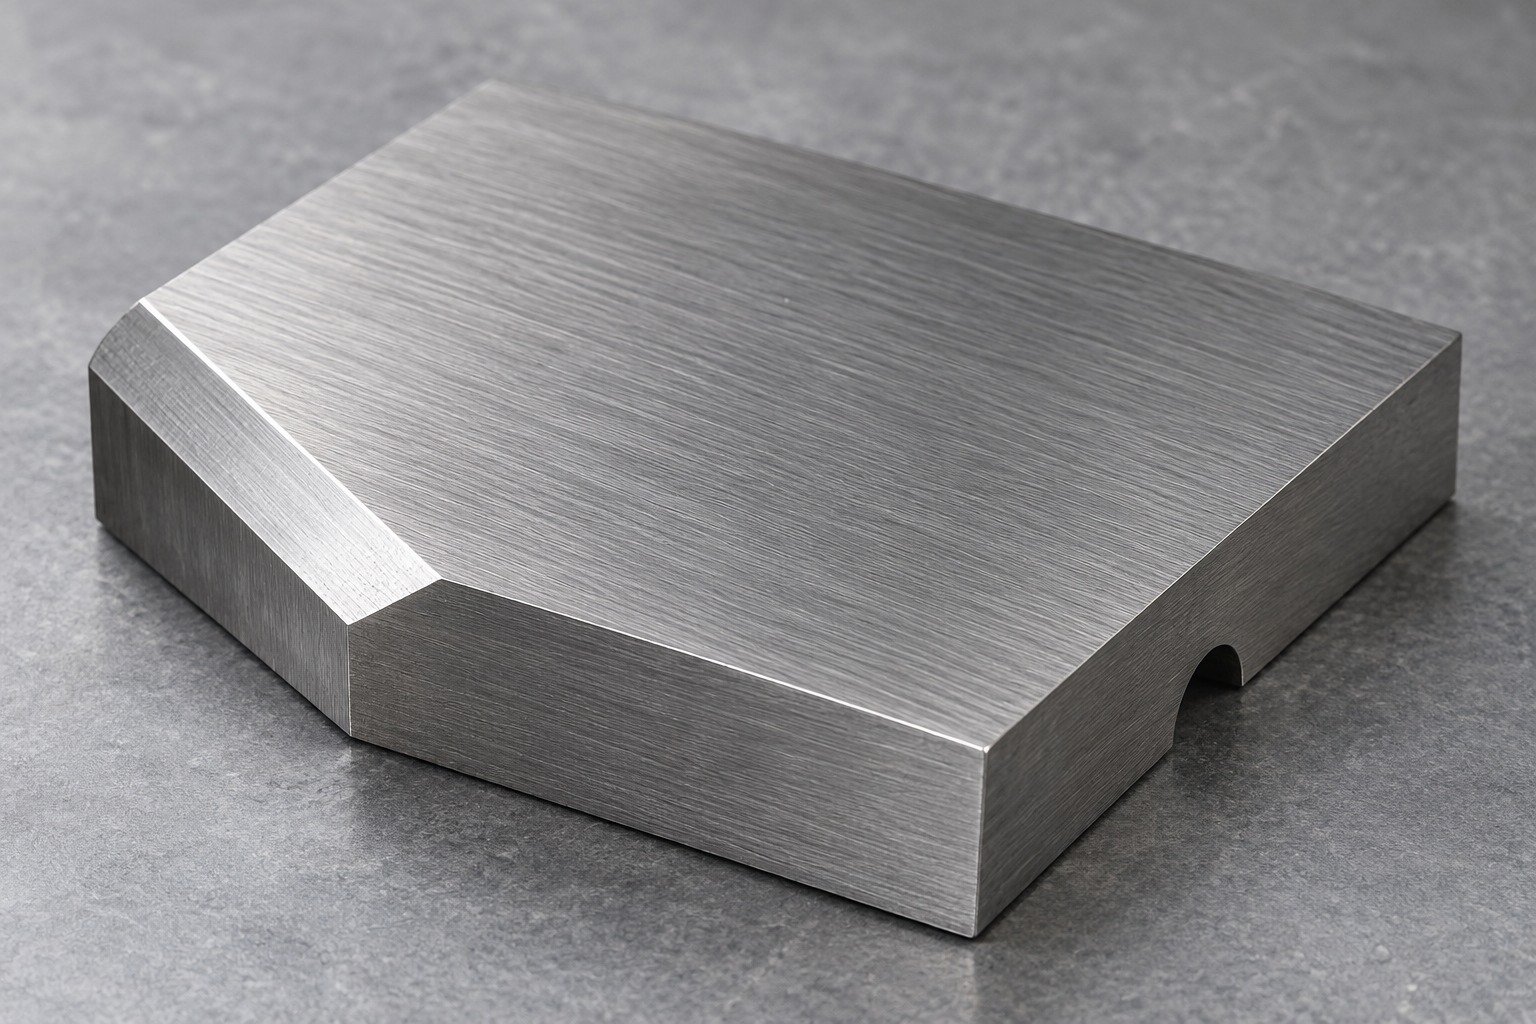
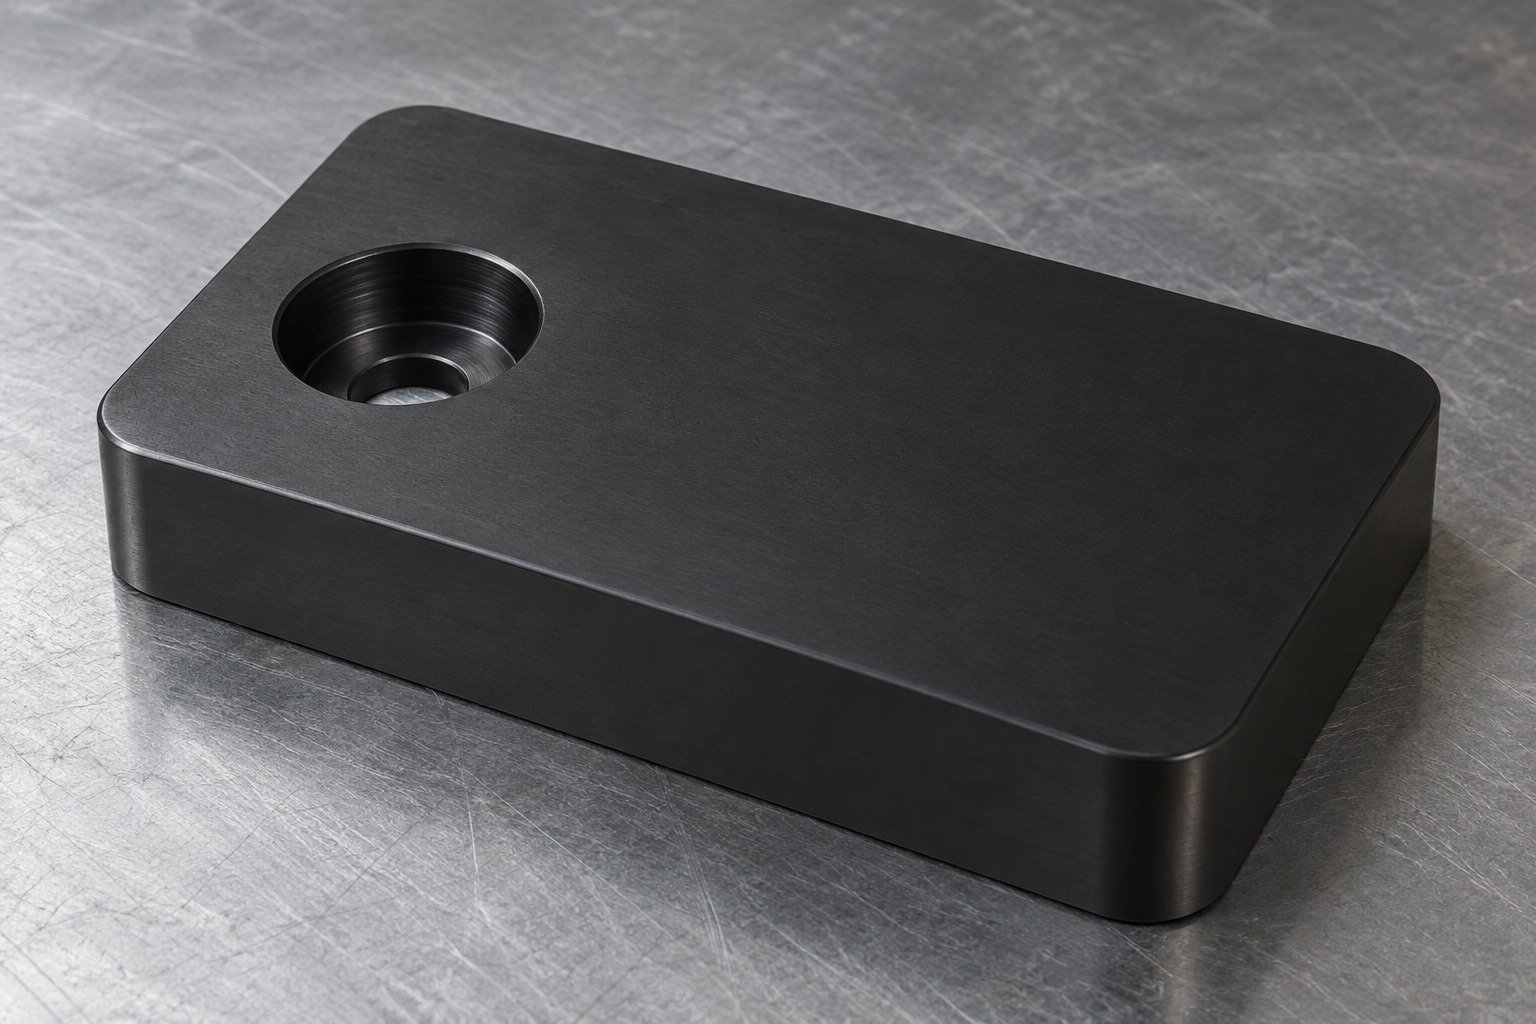
Illustrative appearance samples. Protection, treatment compatibility, masking and manufacturing scope require project review. A visual sample is not a process specification.
Surface Finishing →| Compare | What your drawing must resolve |
|---|---|
| D2 vs A2 tool steel | Abrasive wear, impact, working-edge support and the finishing route. |
| Working-edge support | Review chipping risk, local impact, section and the final profile before approving the grade. |
| European comparison | 1.2379 / X153CrMoV12 is a review reference; confirm the product standard and supplied state. |
Confirm an alternative before purchase. Do not assume that similar names or higher alloy content approve a replacement.
Connect China manufacturing with Dallas-area coordination for your drawing review, sample decisions and delivery requirements.
Define the final datums, surface requirement, remaining stock and accepted measurement state before treatment. Agree the grinding route for the actual part and supplied condition; a general allowance cannot guarantee your final fit.
Identify the critical faces and required surface-integrity acceptance. Agree the inspection method with the manufacturing and treatment providers. Surface appearance alone does not prove that the required condition has been preserved.
Distinguish the delivered stock condition from the final working requirement. State the accepted hardness, test method and test locations with the tool geometry and intended service; no single hardness suits every D2 component.
Review corrosion exposure and protective handling. Chromium content alone does not make D2 a stainless specification. Agree storage, cleaning and any protection without changing the working fit.
Treat joining or repair as an engineering review. Identify the exact steel, existing condition, section and required final properties. Agree a qualified procedure and final acceptance before committing the part to repair.
Define when EDM occurs relative to hardening and tempering, the final surface requirement and any subsequent operation. Producer guidance is condition-specific; confirm the route with the actual material and treatment provider.
For your D2 tool steel machining quote, send CAD, the controlled drawing, quantities, stock condition, treatment responsibility, final fit, finishing and required records. Compare quotations at the same revision and finished state.





