

Injection Molding
Tooling and molding for your repeat plastic parts.
From prototype to production, coordinated manufacturing solutions for your custom parts.
View All Services →
Precision parts for your tight tolerances and complex geometry.
Tooling and molding for your repeat plastic parts.

Metal casting options for your part and production volume.

Cutting, forming and welding for your fabricated parts.

Custom profiles for your section, length and finish requirements.

Finishes for your appearance, corrosion and wear requirements.

Sub-assemblies and final builds for your production program.

Production tooling built around your process and volume.

Prototype parts to check fit, function and design.
DFM, process planning and production support for your project.
Inspection, documentation, inventory and delivery planning for your program.
Choose air- or liquid-cooling components around your thermal and mechanical requirements.

Manufacturing support for your cold plates, manifolds and cooling assemblies.

Find components for your power electronics, energy, laser and telecom application.

Components for your electronic systems.
Start with your functional and quality requirements.
Build around your operating environment.
From prototype to production, review material performance, manufacturability and cost for your part.
Review grade, temper and finish for your metal parts.
 AluminumStrength, weight and machining›
 Stainless SteelCorrosion and finish requirements›
 Carbon & Alloy SteelDiscuss grade and heat treatment›
 Tool SteelDiscuss tooling and wear needs›
 TitaniumReview grade and part geometry›
 Copper & BrassDiscuss conductivity and machining›
Match your polymer to function, process and environment.
 ABSReview enclosure and molding needs›
 Polycarbonate (PC)Discuss clarity and impact needs›
 Nylon (PA)Review moisture and wear conditions›
 POM / AcetalReview fit and sliding features›
 PEEKDiscuss operating conditions›
 PTFEReview friction and chemical exposure›
 ULTEM / PEIDiscuss thermal and electrical needs›
Confirm grade availability and application requirements.
 Silicone / LSRDiscuss flexible component needs›
 TPU / TPEReview flexibility and processing›
 EPDMReview weathering and chemical exposure.›
 NBRReview oil and fuel exposure.›
 FKMReview temperature and chemical exposure.›
 G10 / FR4Review insulation and laminate needs›
 CompositesReview stiffness, weight and laminate.›Customer-Specified MaterialsConfirm your grade and requirements.›Other Specialty MaterialsDiscuss your application and grade.›
Practical guidance for your part geometry and material decisions.
Prepare your process, budget and sourcing questions.
Build your knowledge before production.
Learn who we are and how we operate.
Find our U.S. support team or start a conversation.
YOUR MODULE. YOUR INTERFACES. YOUR NEXT BUILD.
Bring your component BOM, mating interfaces and module acceptance into one review. Plan subassembly services around the condition your team needs at final assembly, with clear responsibility for parts, checks and delivery.
3 levels to define: component → subassembly → final assembly. The same module can be a finished delivery for your supplier and an intermediate unit for your production team.
What arrives assembled
How it enters your product
Who provides each item
What the checks demonstrate
Identity and protection
Resolve the handoff between component supply and your next assembly operation.
List installed parts, loose items and excluded next-level work.
Assign manufactured, purchased and customer-supplied BOM items.
Control datums, mounting features and accessible connections.
Separate module checks from complete-product validation.
Agree identification, protection, quantities and release records.
Start with the module you want to receive. Confirm operations, purchased items and checks around that boundary.
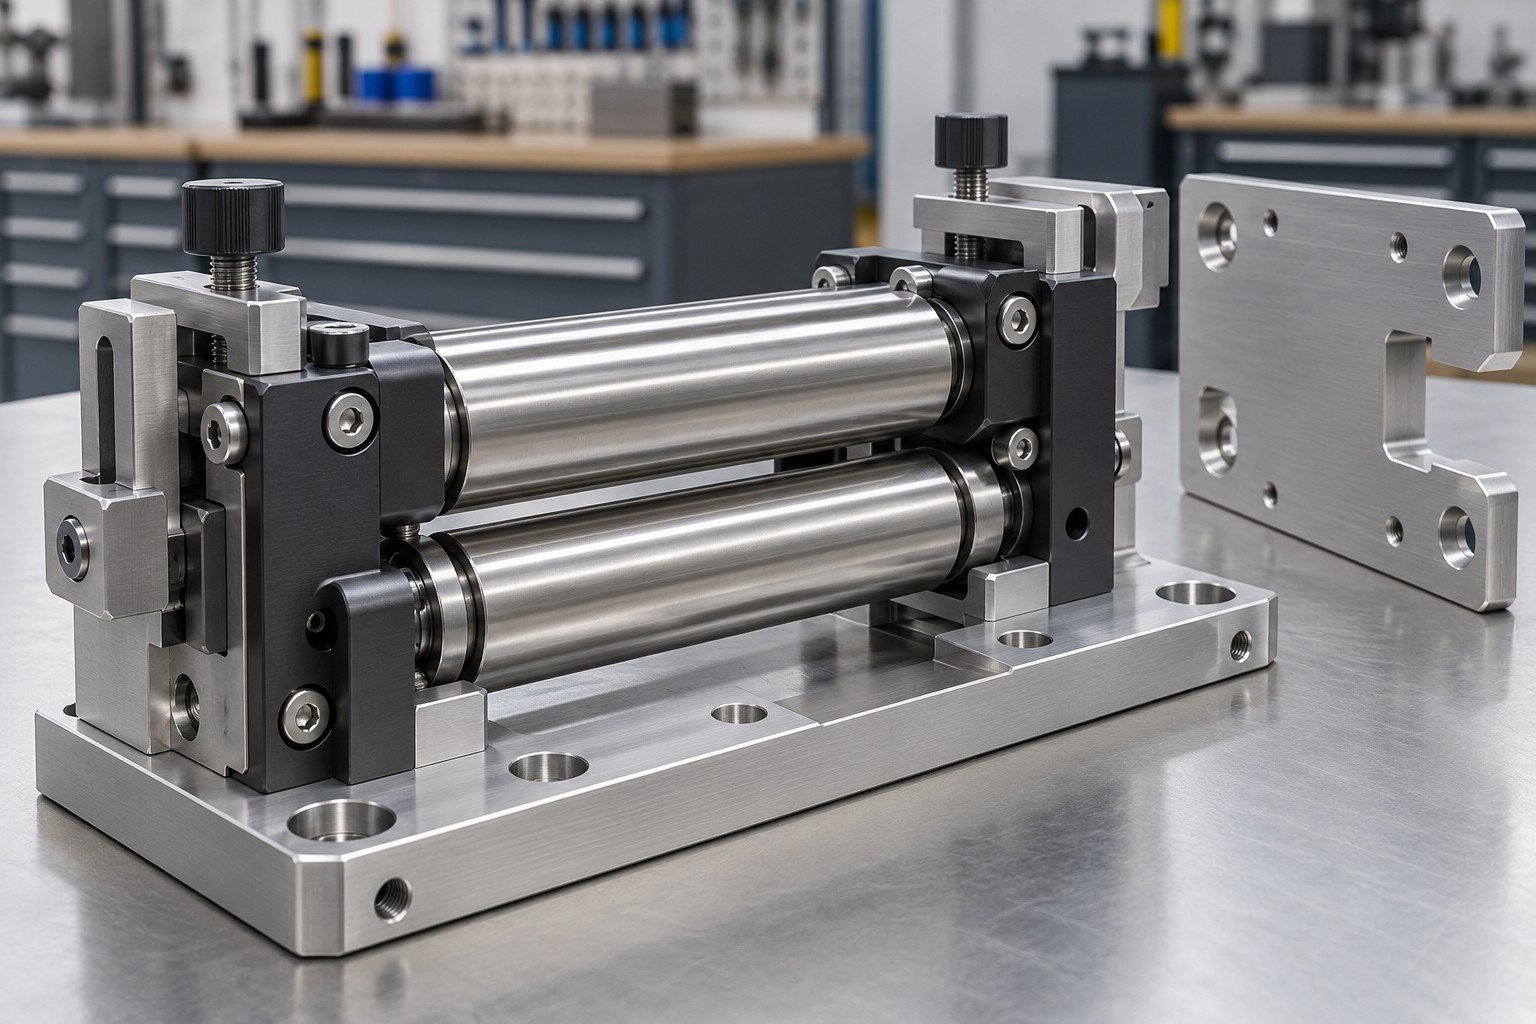
Machined subassemblies need more than accepted individual parts. Specify axial location, supported features and the interface your next build uses.
| Your input | Module drawing, shaft stack and receiving interface. |
|---|---|
| Your decision | Agree what is installed and what remains for your team. |
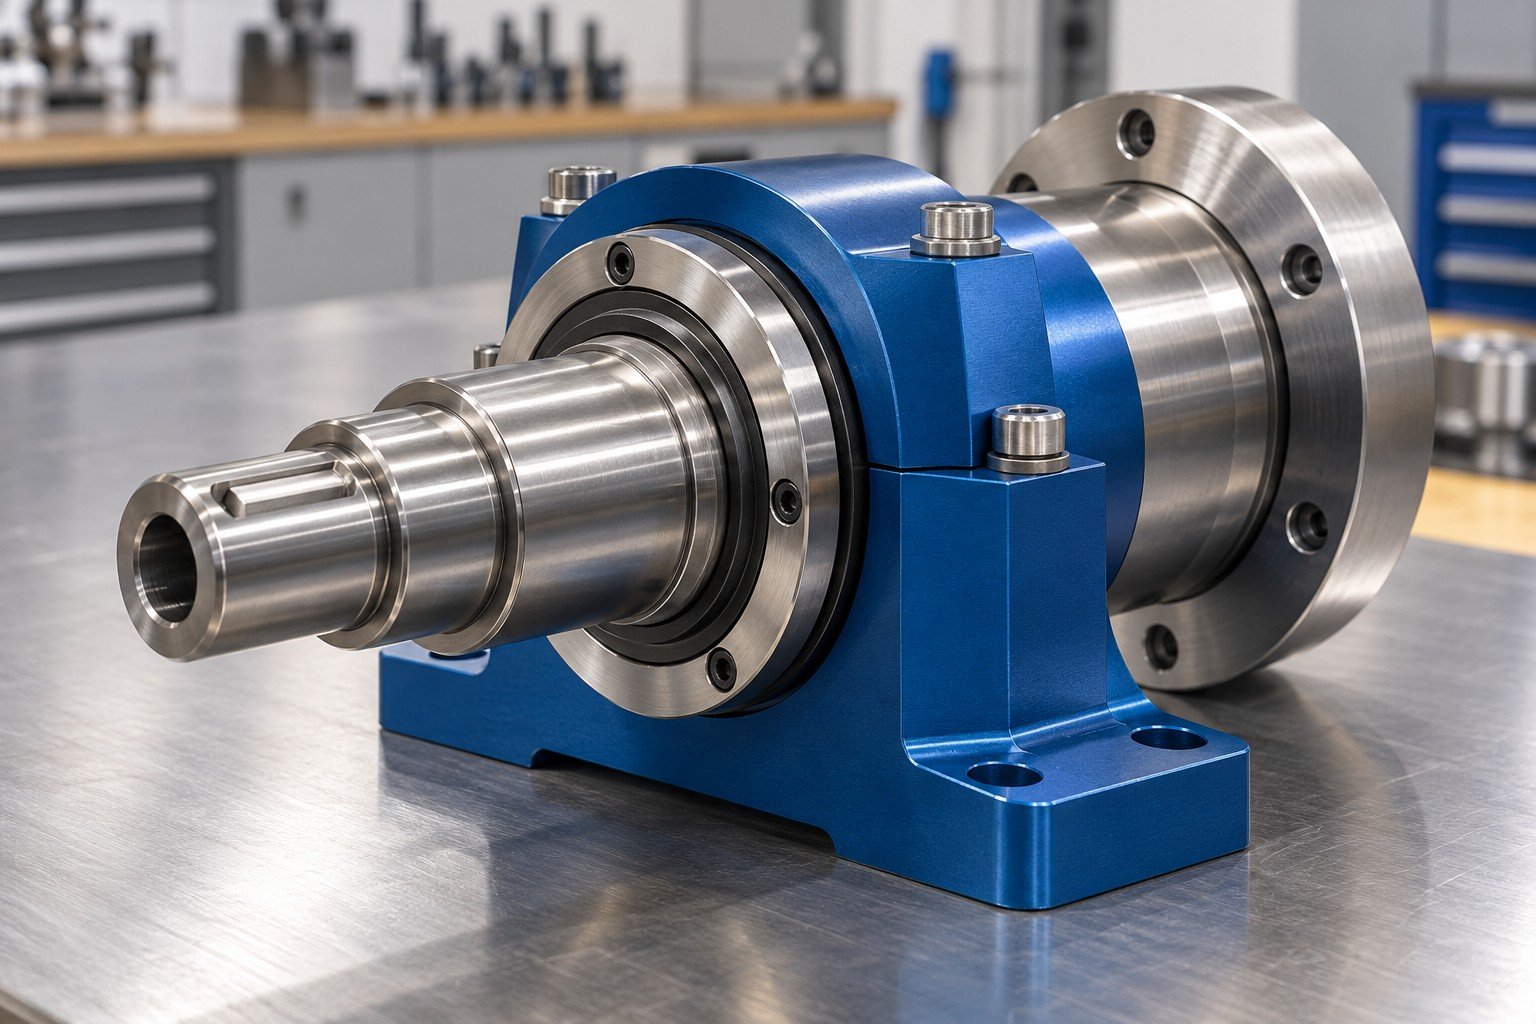
A subassembly bill of materials should identify approved bearings, spacers, seals and retaining hardware. Similar dimensions alone do not approve a substitute.
| Your input | Part numbers, grades and supplied-item responsibility. |
|---|---|
| Your decision | Authorize substitutions and shortages before the build. |
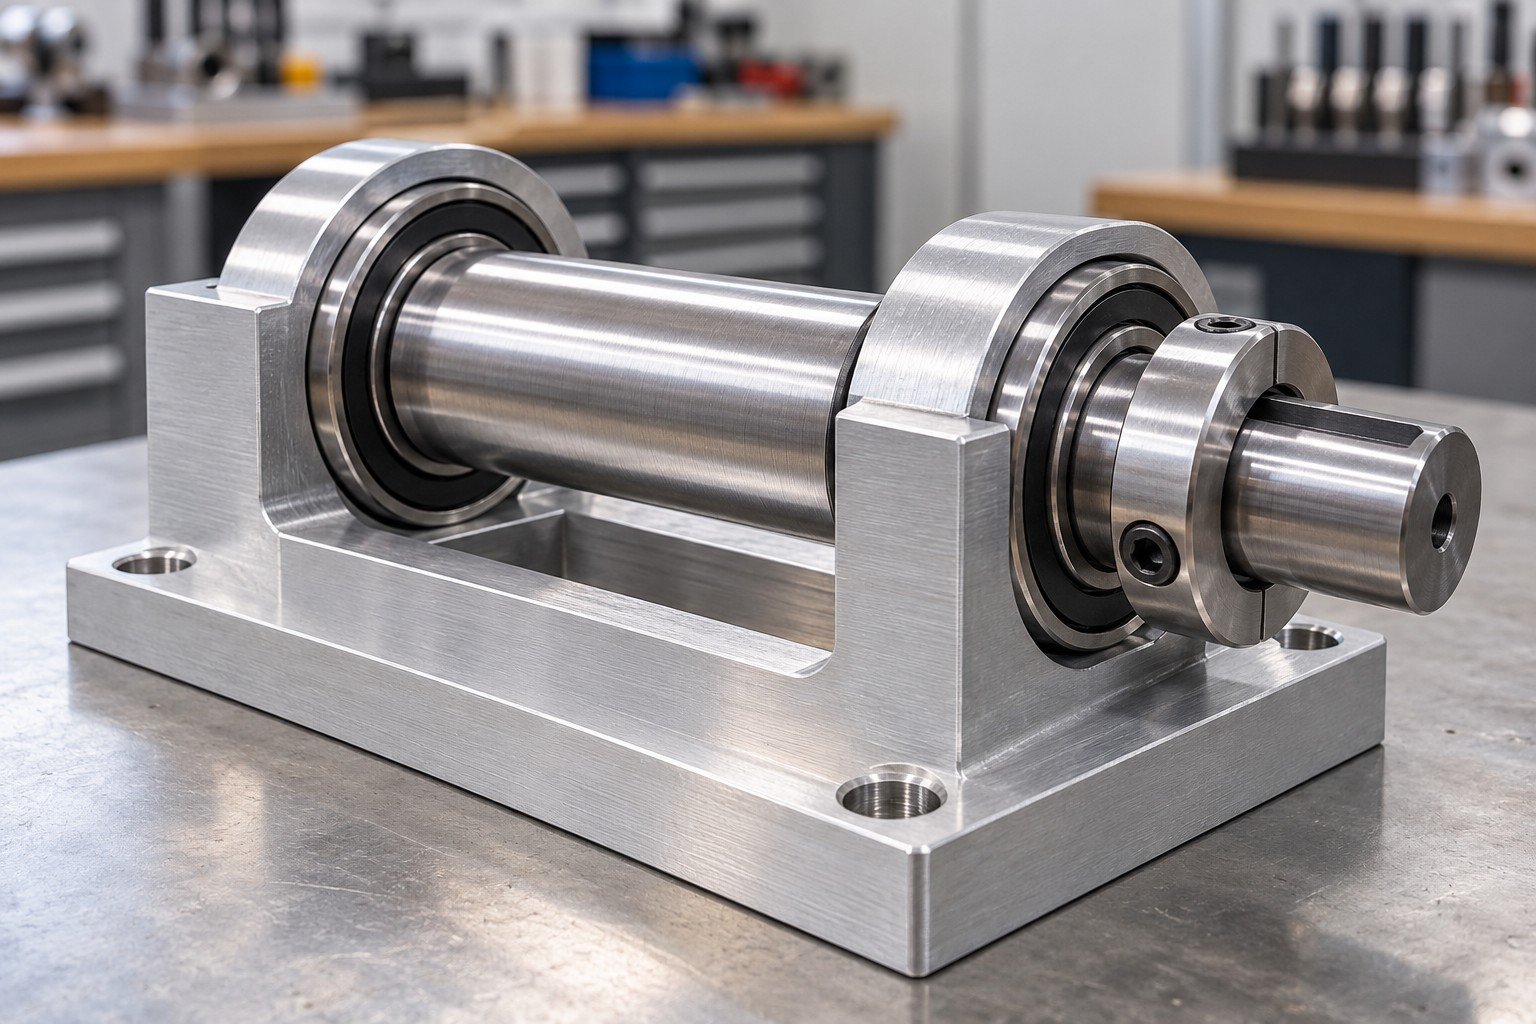
Subassembly tolerance analysis connects the shaft, bearing seats, spacers and mating structure. Define the relevant installed limits rather than promising a generic precision level.
| Your input | Datum scheme, fits, axial limits and mounting condition. |
|---|---|
| Your decision | Agree locating, installation and assembled measurement. |
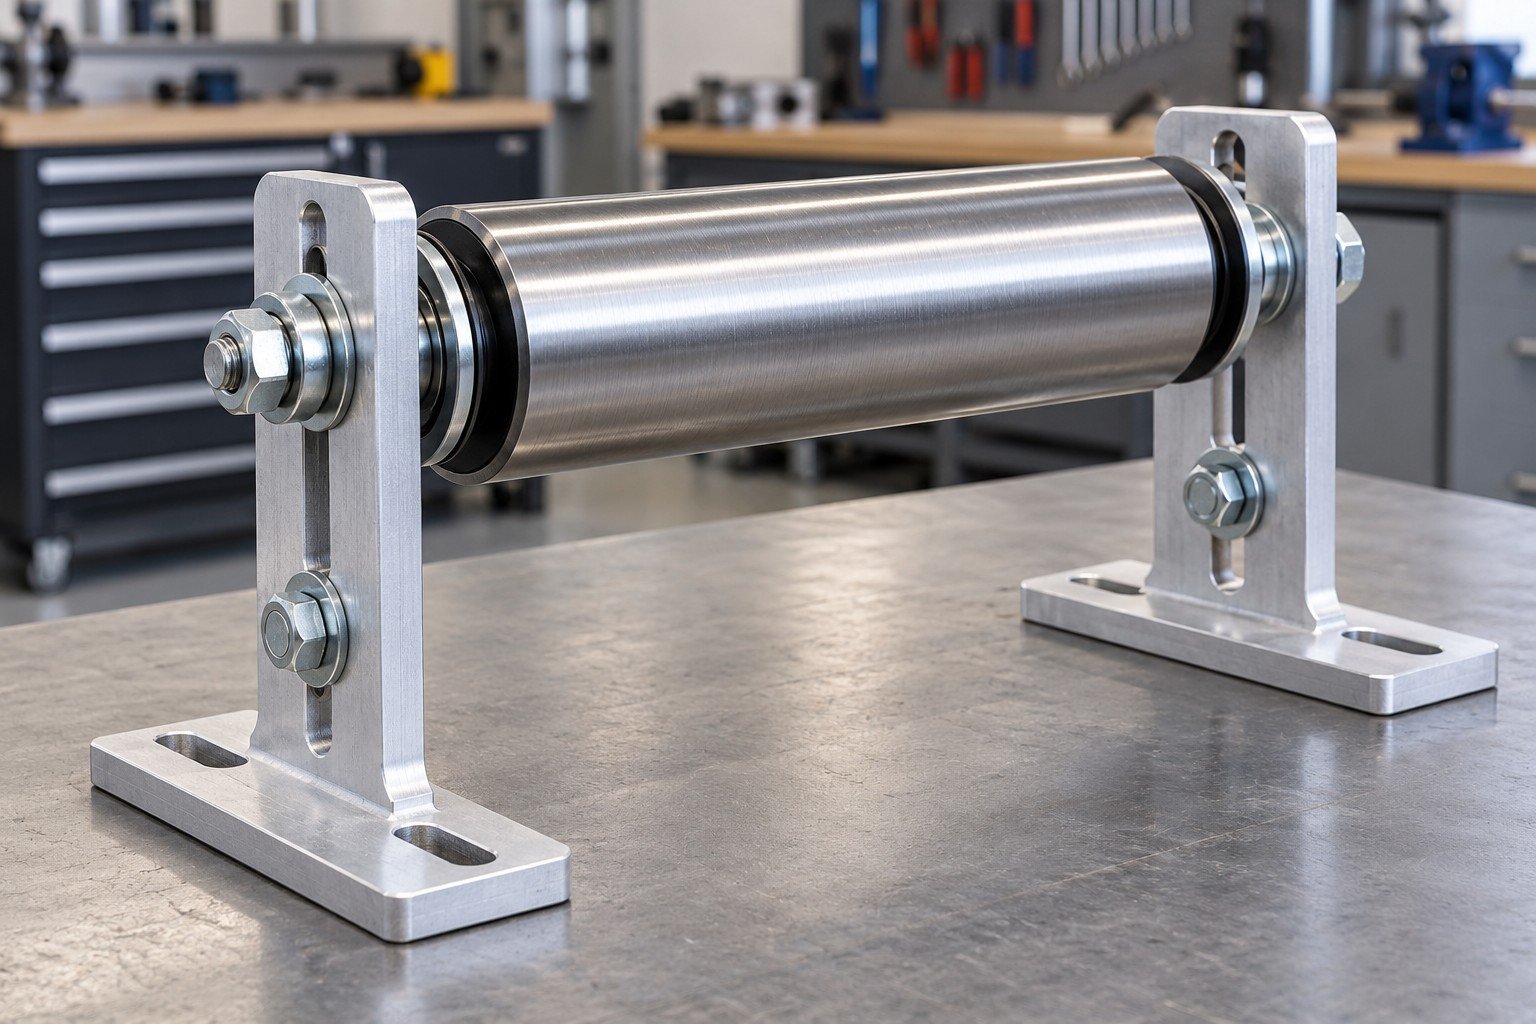
Define subassembly testing for the actual scope: position, rotation or another agreed check under stated conditions. A free-turning shaft does not establish load life.
| Your input | Check method, limits and required records. |
|---|---|
| Your decision | Separate module acceptance from product endurance validation. |
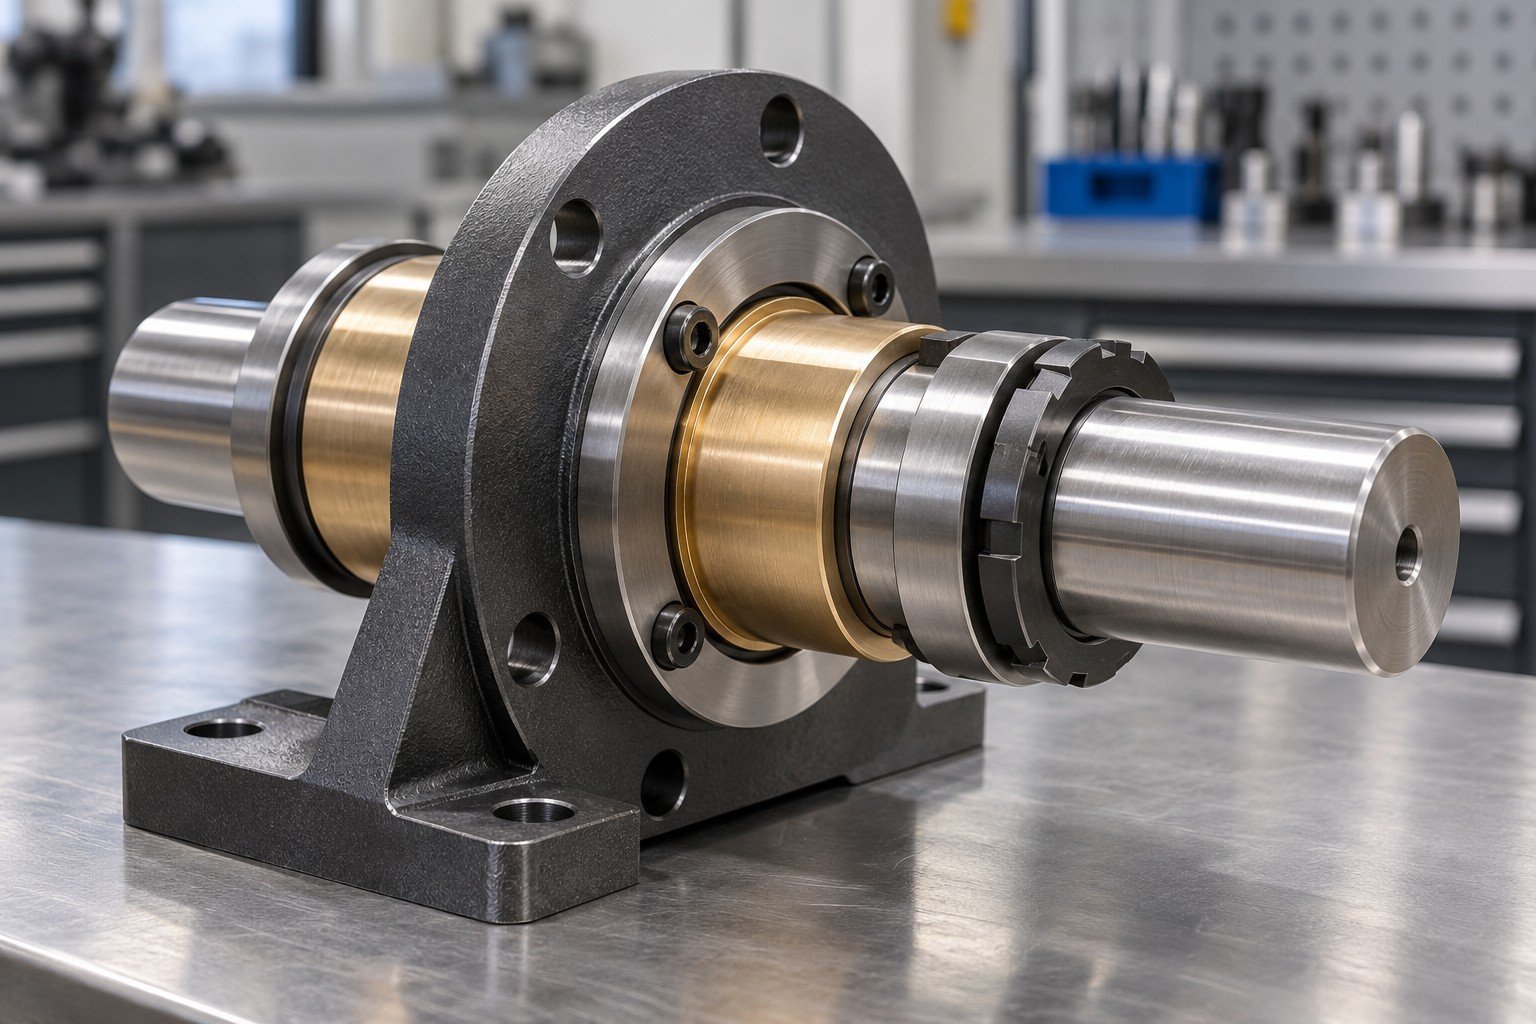
For precision subassembly, identify the locating faces and mounting points your production fixture will use. The word precision does not define a tolerance.
| Your input | Assembly and interface drawing with critical limits. |
|---|---|
| Your decision | Confirm the supplied cassette and receiving references. |
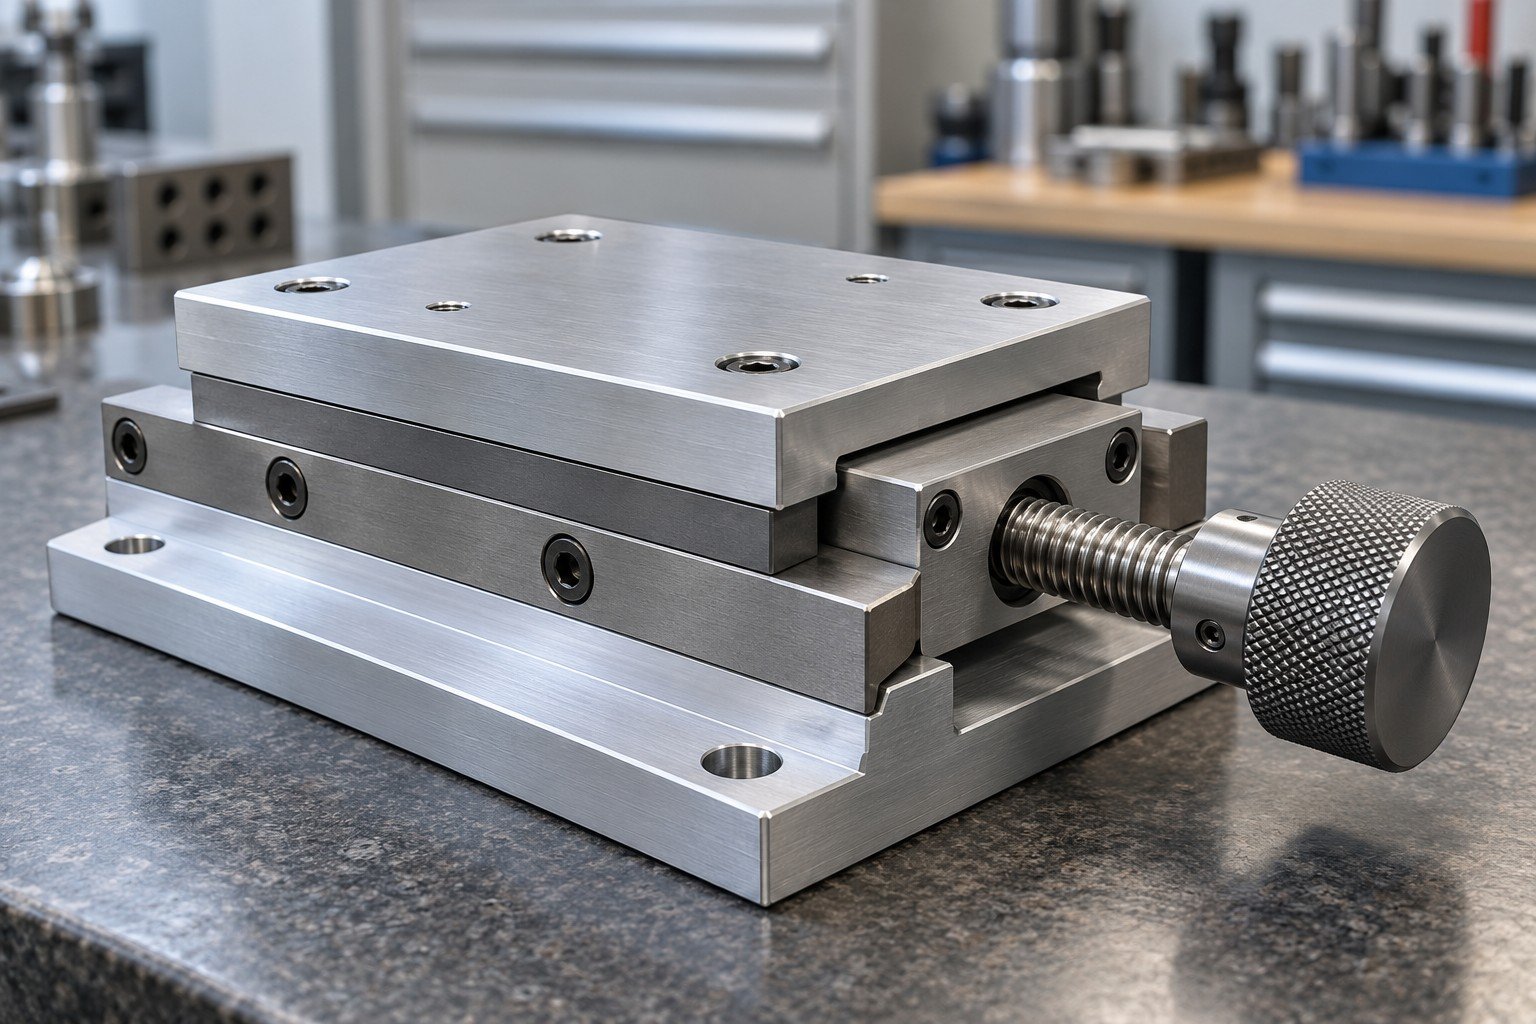
Identify approved purchased items and customer-supplied parts, including revision and incoming condition. Component responsibility should be visible in your quotation.
| Your input | BOM, component datasheets and approved sources. |
|---|---|
| Your decision | Define supply, incoming checks and substitution authority. |
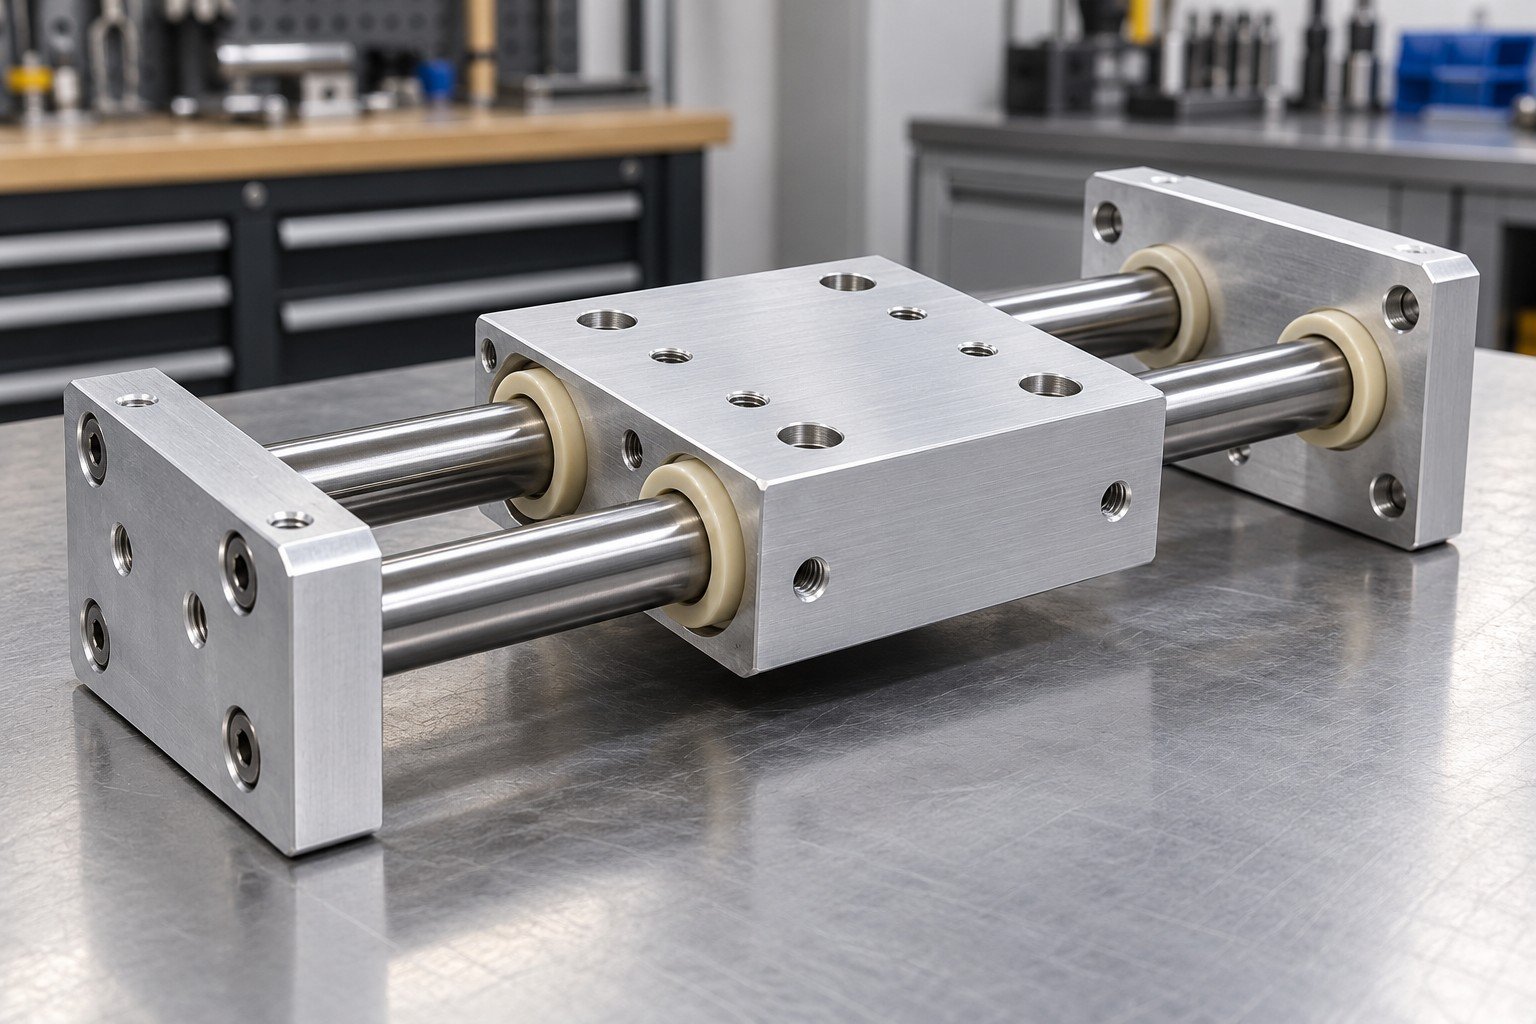
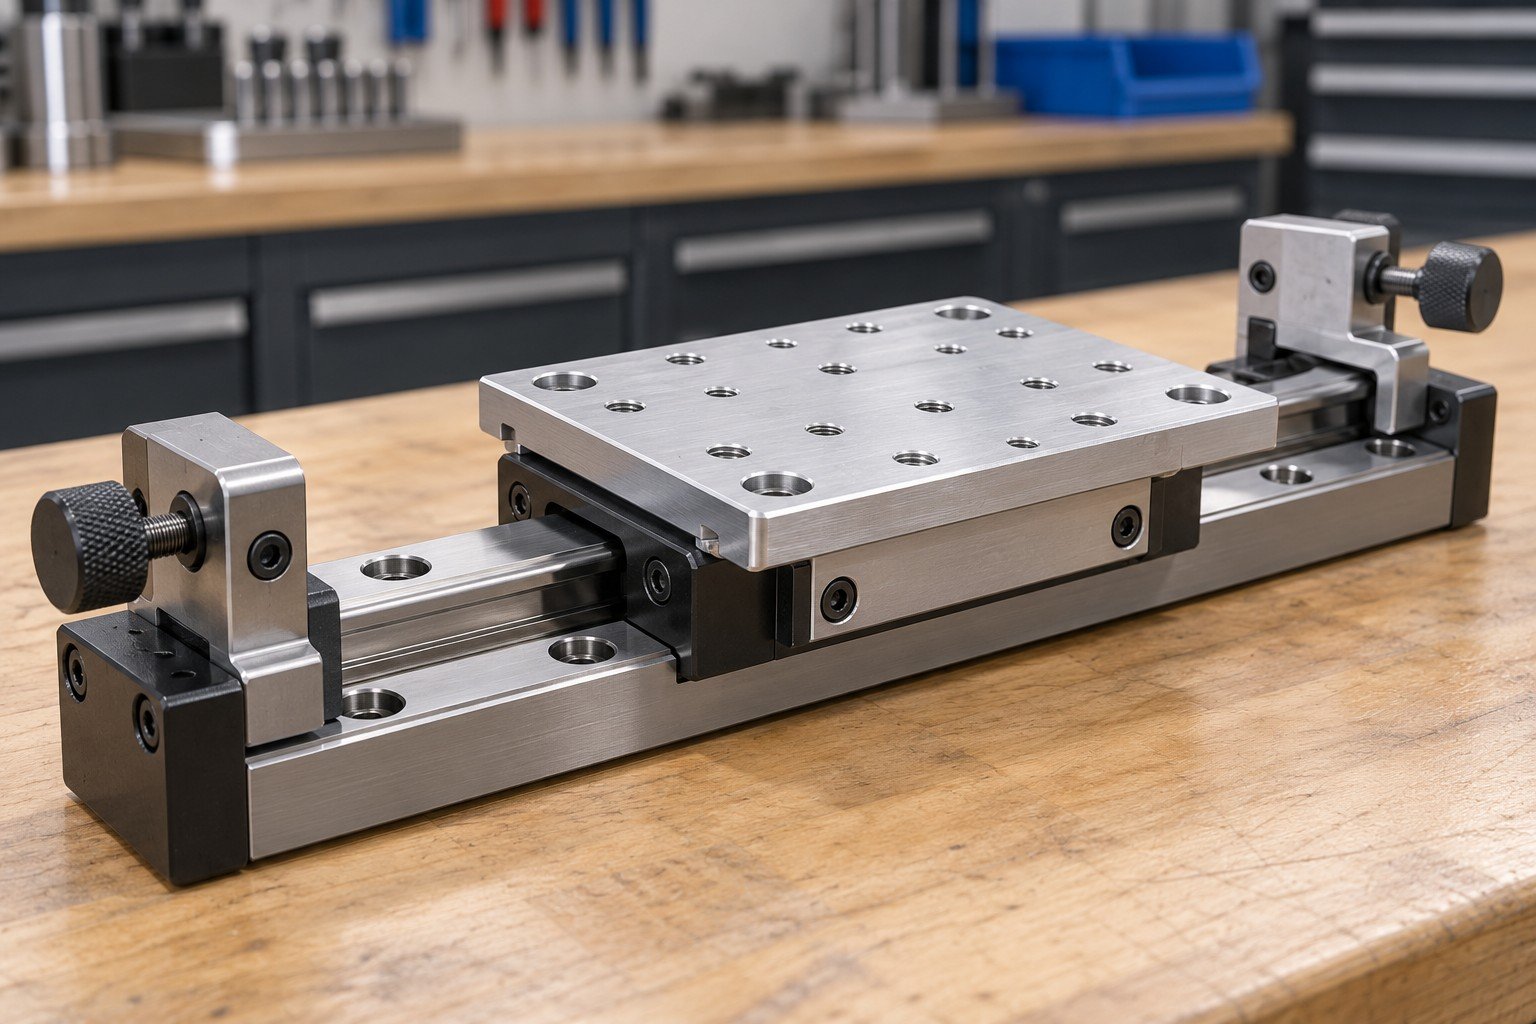
Review fastener, gib and stop access with the module installed in the host product. A bench-accessible adjuster may be hidden after integration.
| Your input | Host envelope, access zones and setup sequence. |
|---|---|
| Your decision | Agree fixture location and final adjustment ownership. |
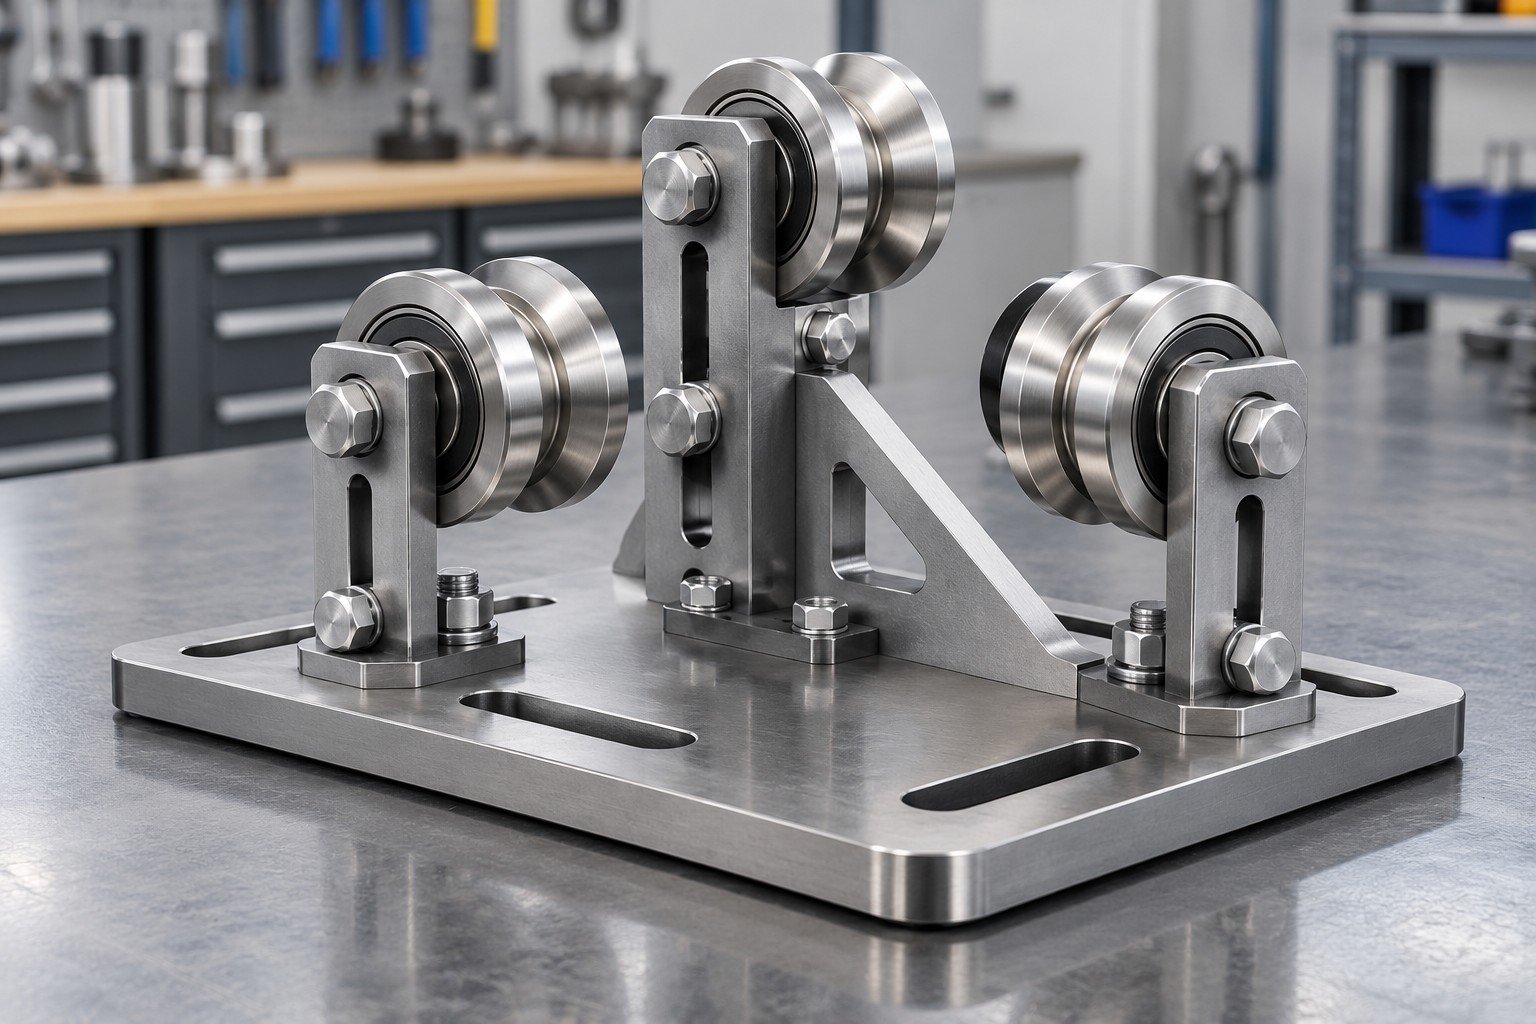
Check the specified mounting, travel or adjustment condition using an approved method. Confirm any required load or cycle validation separately.
| Your input | Travel requirements, interface gauge and acceptance plan. |
|---|---|
| Your decision | Record the accepted setup and unresolved deviations. |
A metal subassembly can include the housing, carrier, hinge, latch and installed hardware. State which electrical or final-product work is outside the module scope.
| Your input | Delivered drawing and installed-versus-loose item list. |
|---|---|
| Your decision | Set a clear closure and integration boundary. |
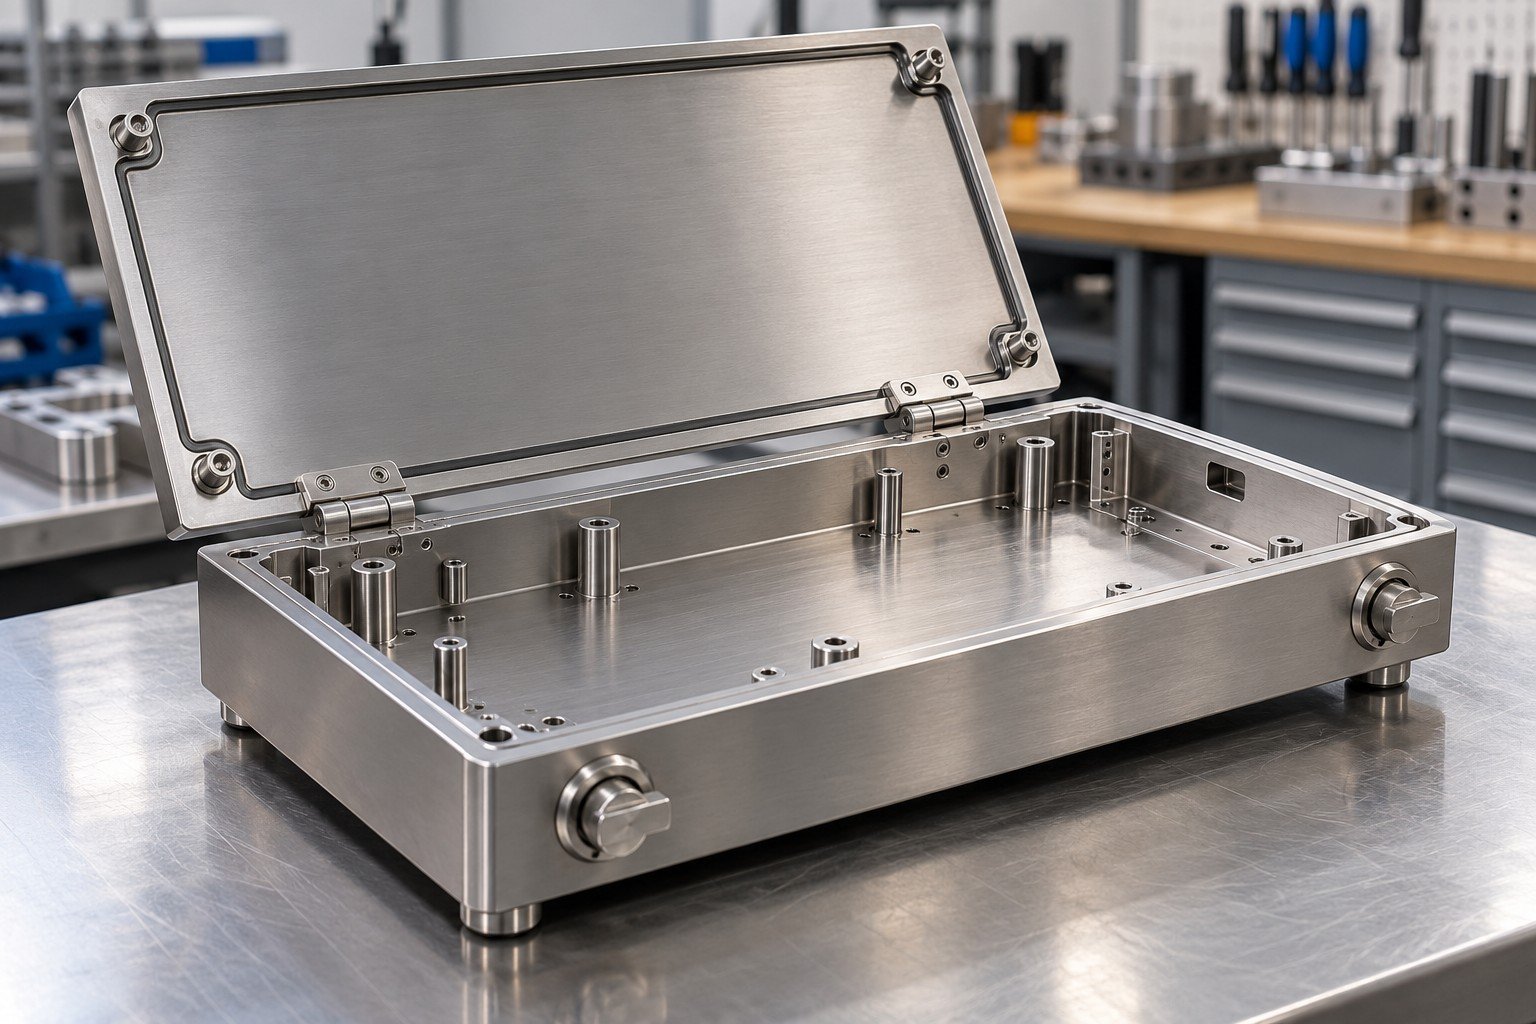
Match panels, hinges, fasteners and finish requirements to the controlled module BOM. A changed latch can alter cutouts or installation access.
| Your input | Component revisions, finish and approved hardware models. |
|---|---|
| Your decision | Review changes before sourcing or assembly. |
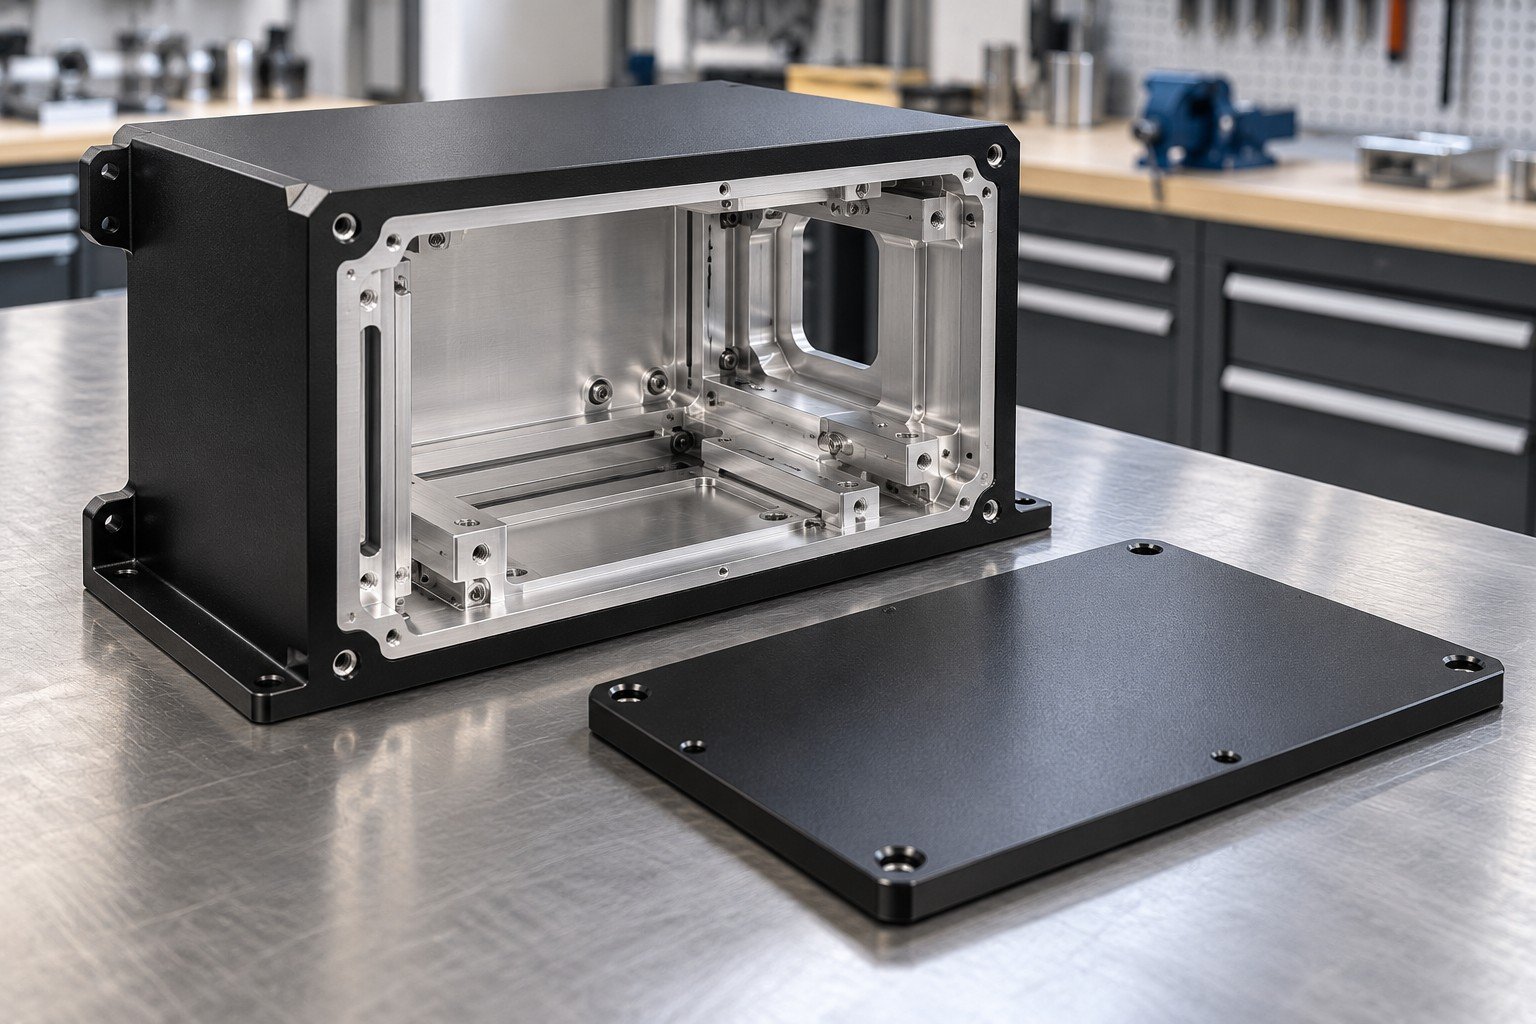
Review door swing, cover removal and mounting clearance against the next assembly. Include finish allowance at locating and mating features.
| Your input | Host CAD, opening envelope and protected interfaces. |
|---|---|
| Your decision | Confirm practical installation and service access. |
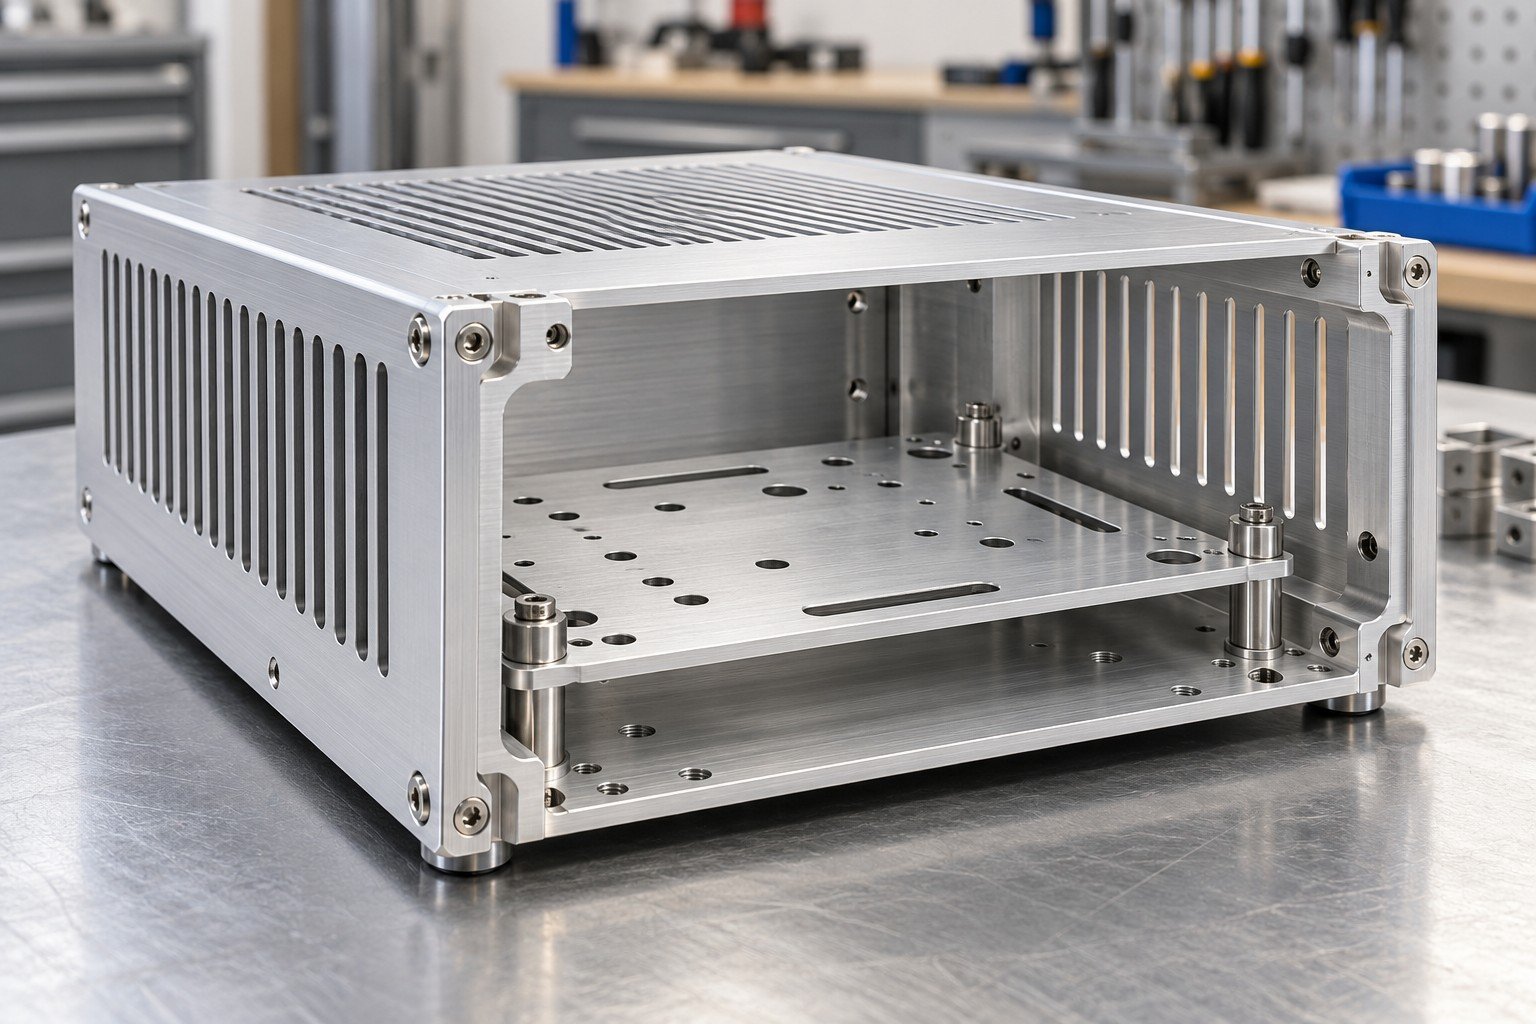
Subassembly inspection may cover fit, closure, gaps and visible condition. Specify sealing or electrical tests only when their method and resources are agreed.
| Your input | Appearance reference, closure criteria and check scope. |
|---|---|
| Your decision | Agree the evidence your receiving team will use. |
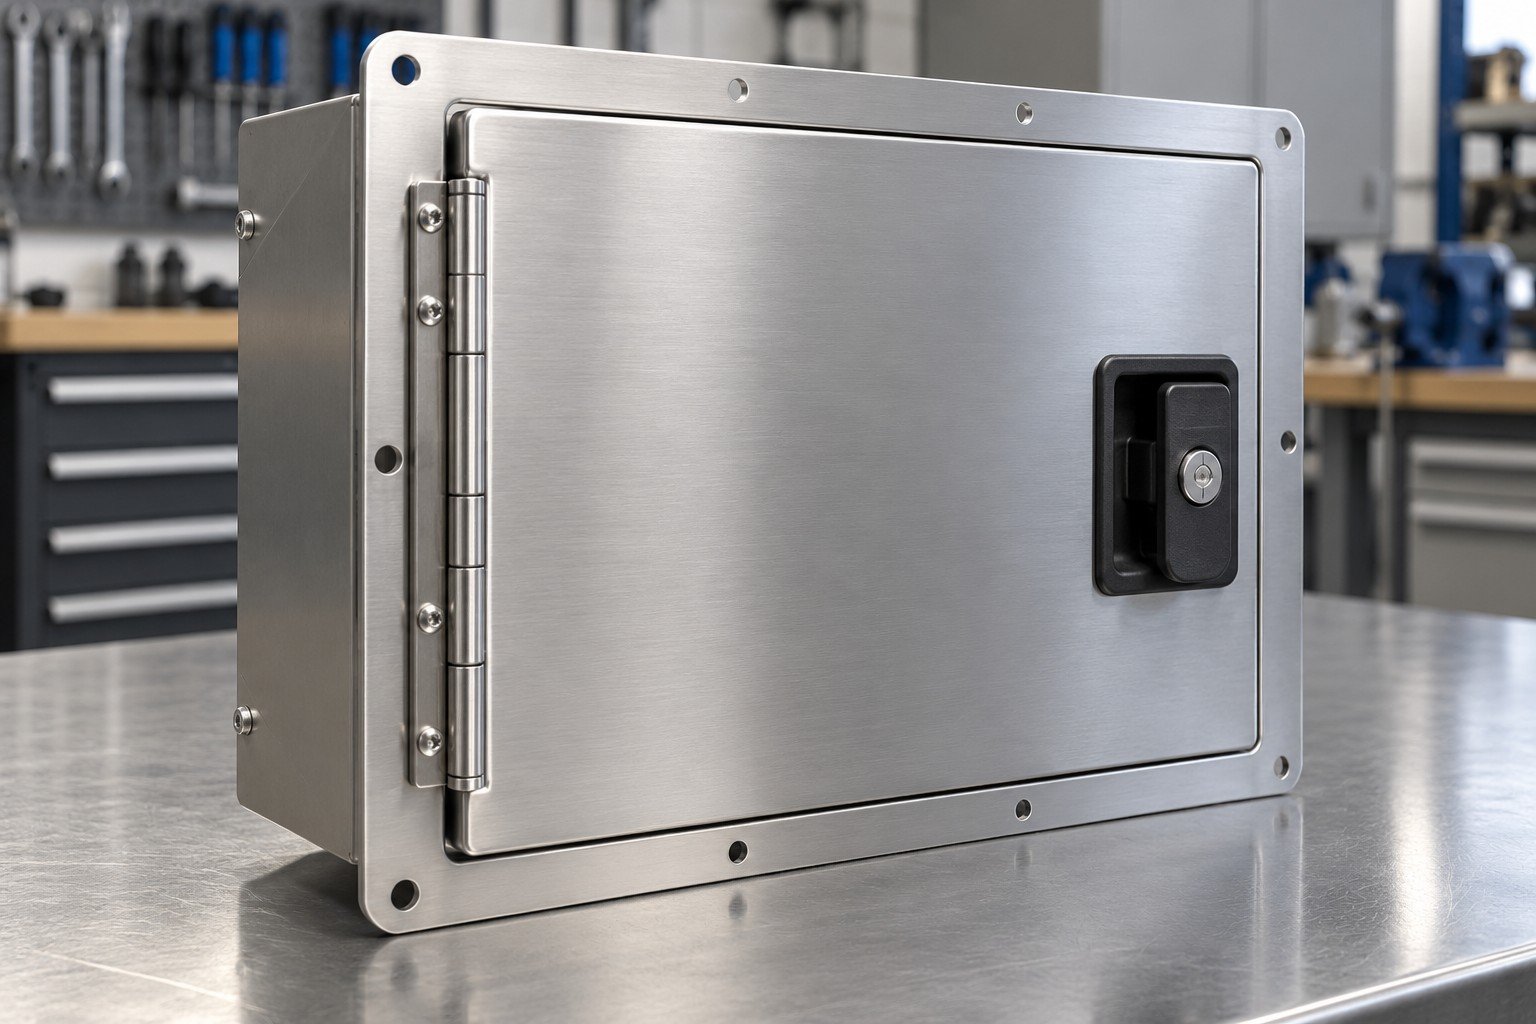
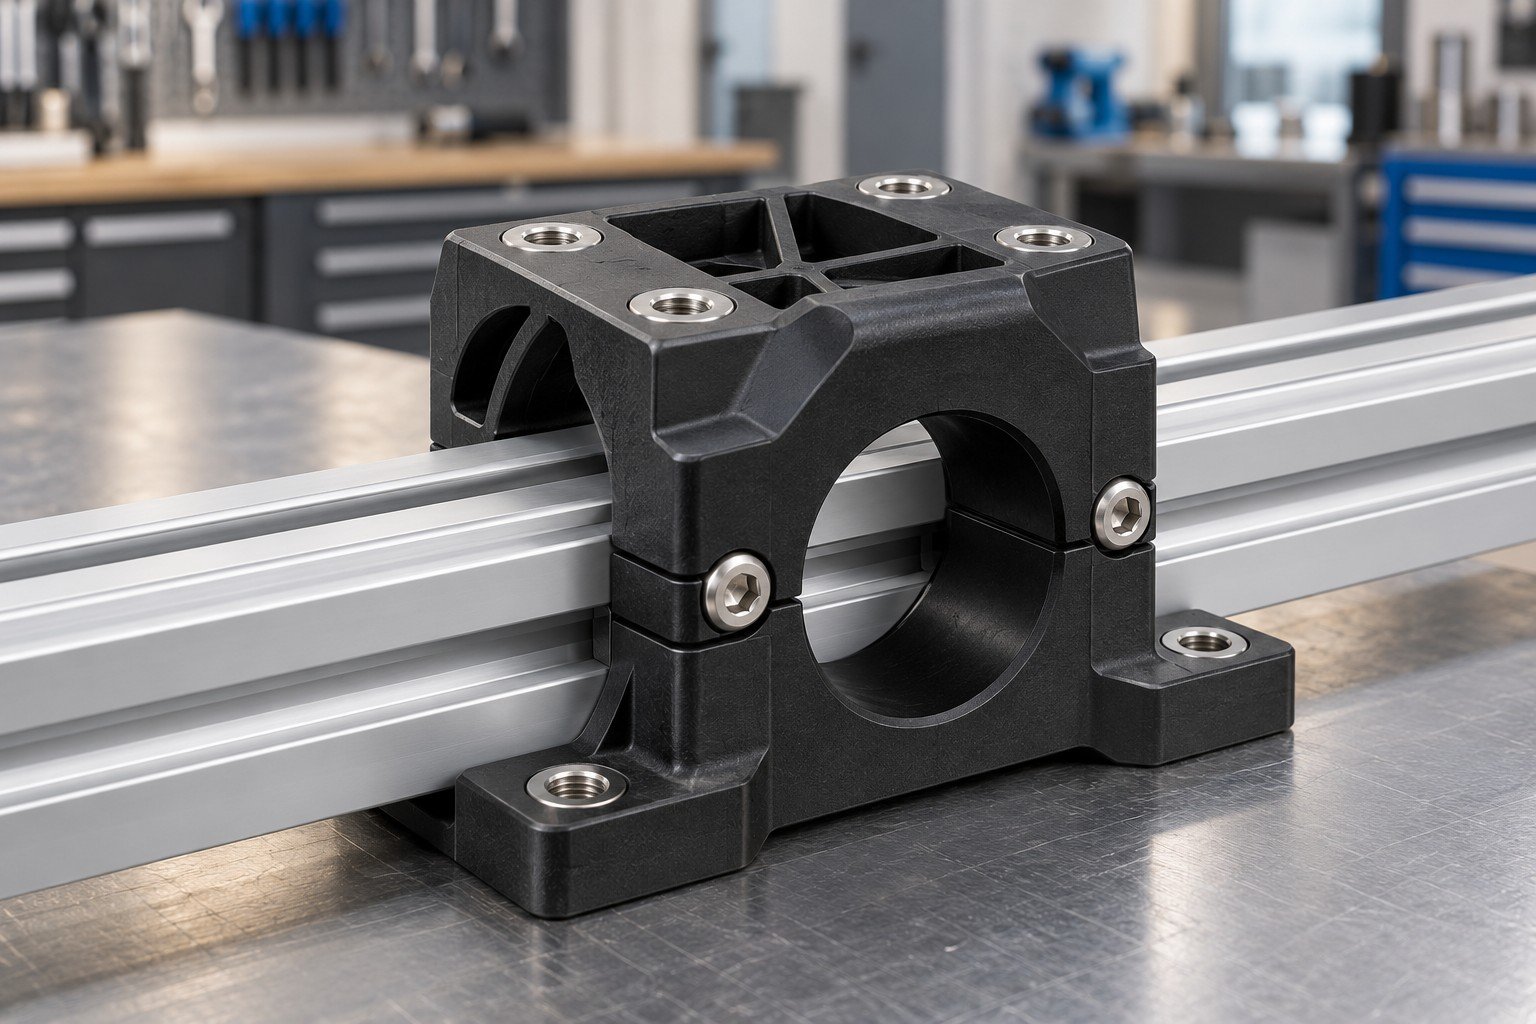
A plastic subassembly joined to metal needs a stated load, environment and mating condition. Material names alone do not establish joint suitability.
| Your input | Grades, environment and delivered geometry. |
|---|---|
| Your decision | Identify which interfaces need project-specific validation. |
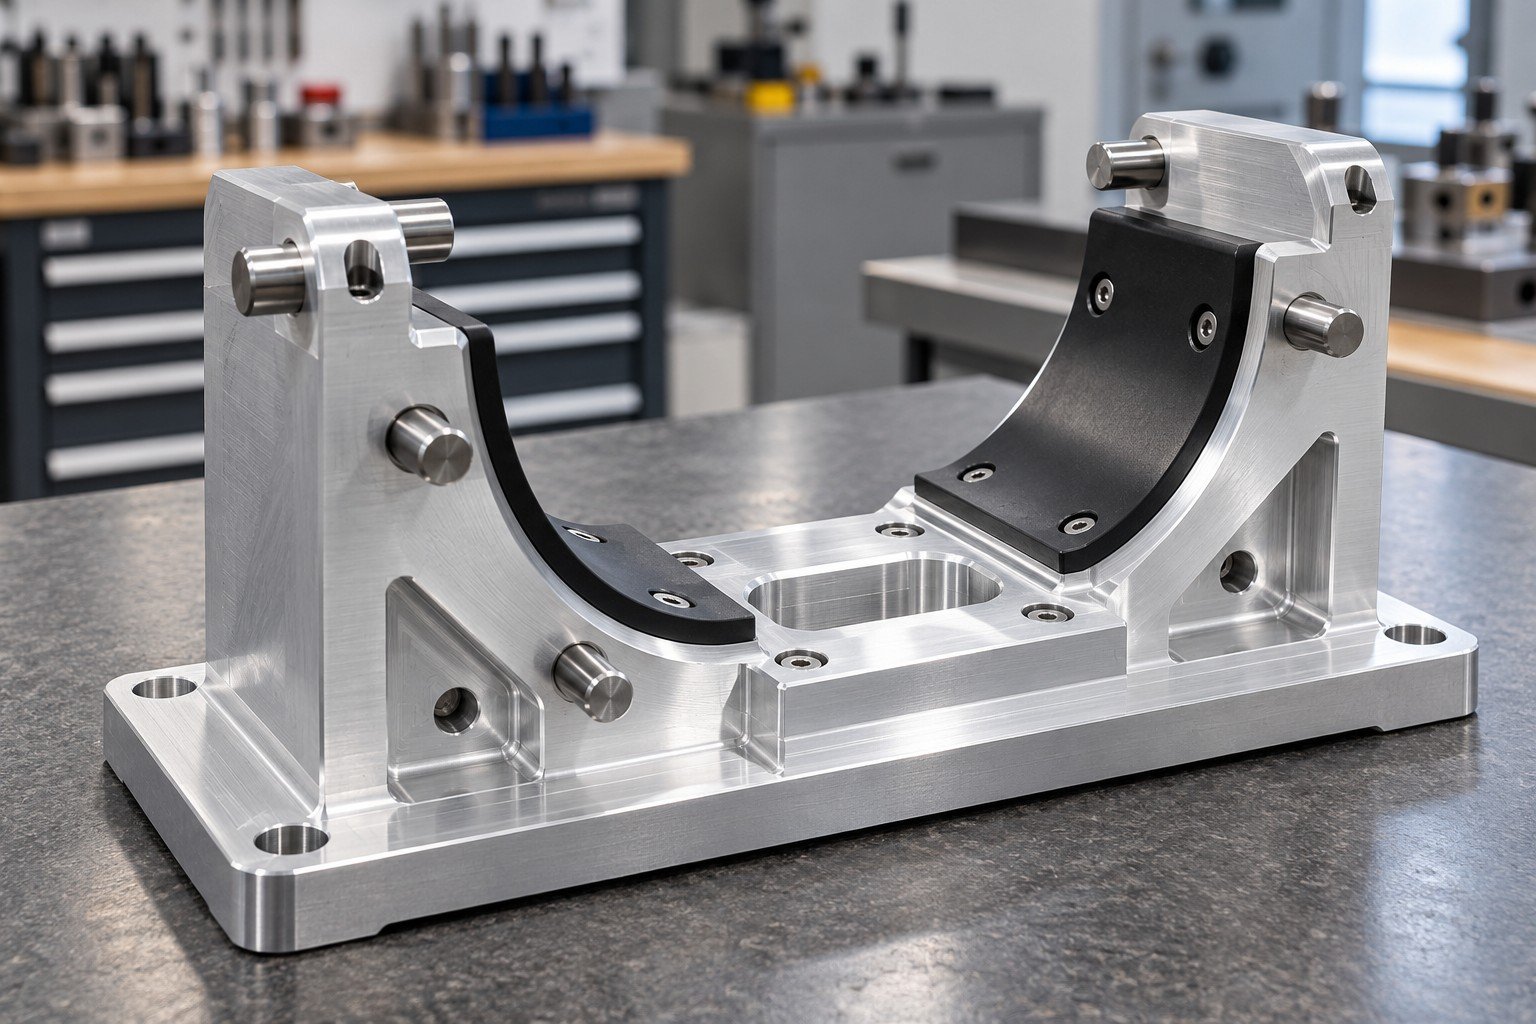
List approved polymer grades, inserts, pads and shoulder screws. Substituting a material can change fit, creep or friction behavior.
| Your input | BOM, material specifications and supplier instructions. |
|---|---|
| Your decision | Approve alternatives and incoming evidence. |
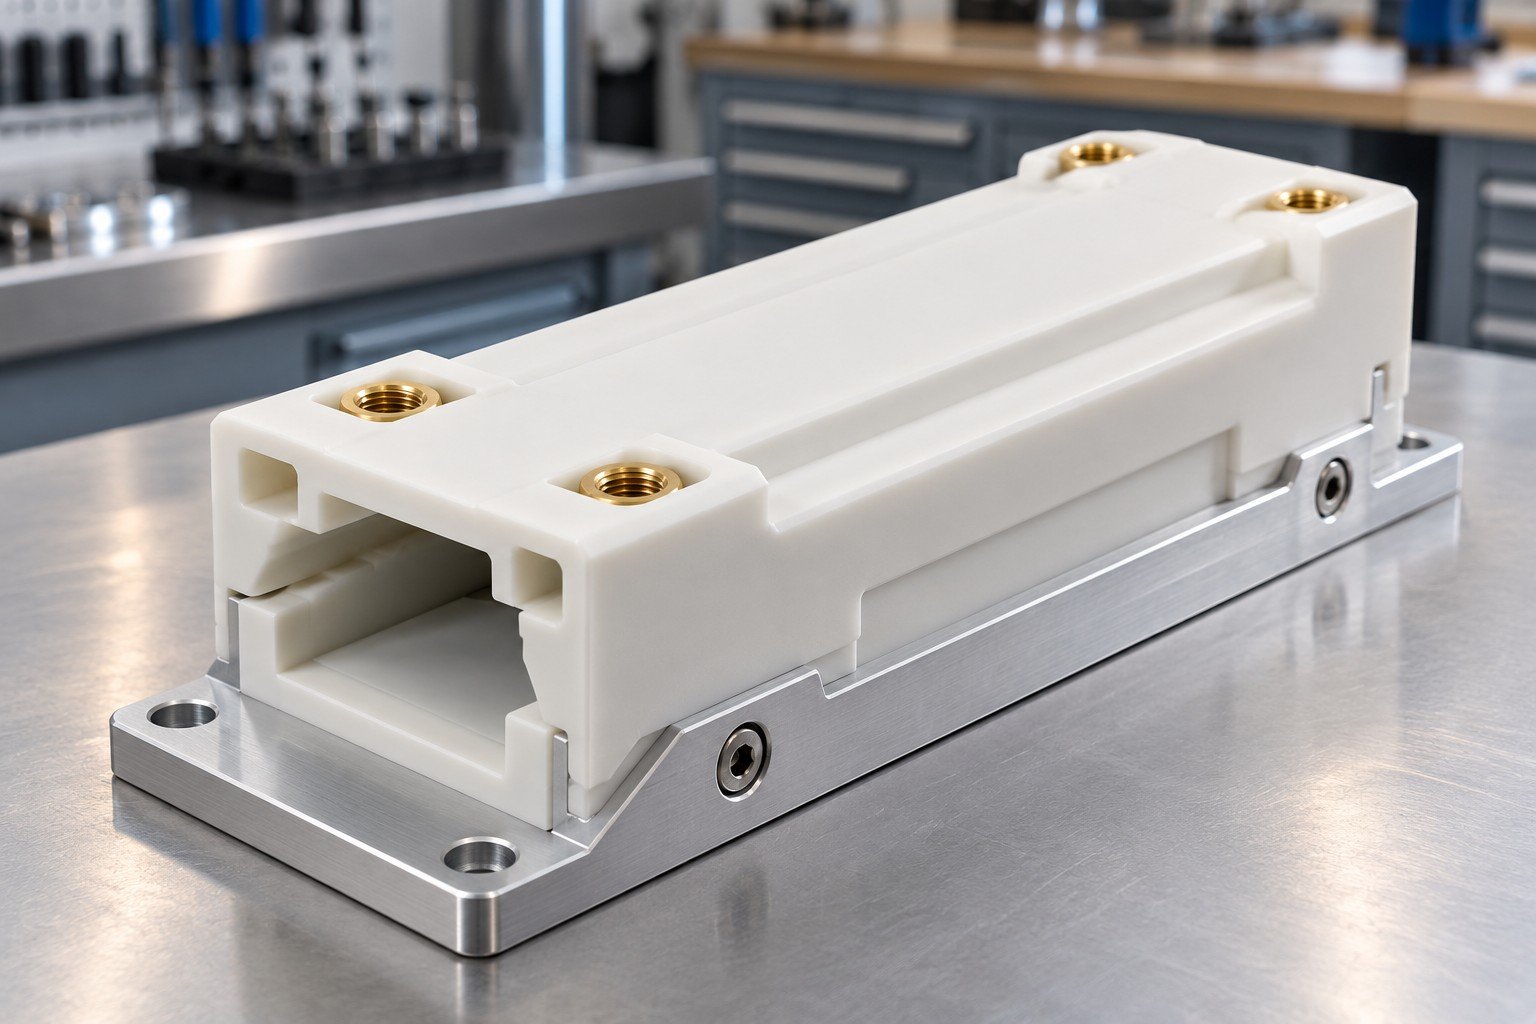
Plan support and joining so thin walls, inserts and wear pads are not distorted during installation. Define the intended fastening method.
| Your input | Joint detail, supports and installation requirements. |
|---|---|
| Your decision | Agree fixture support and relevant process checks. |
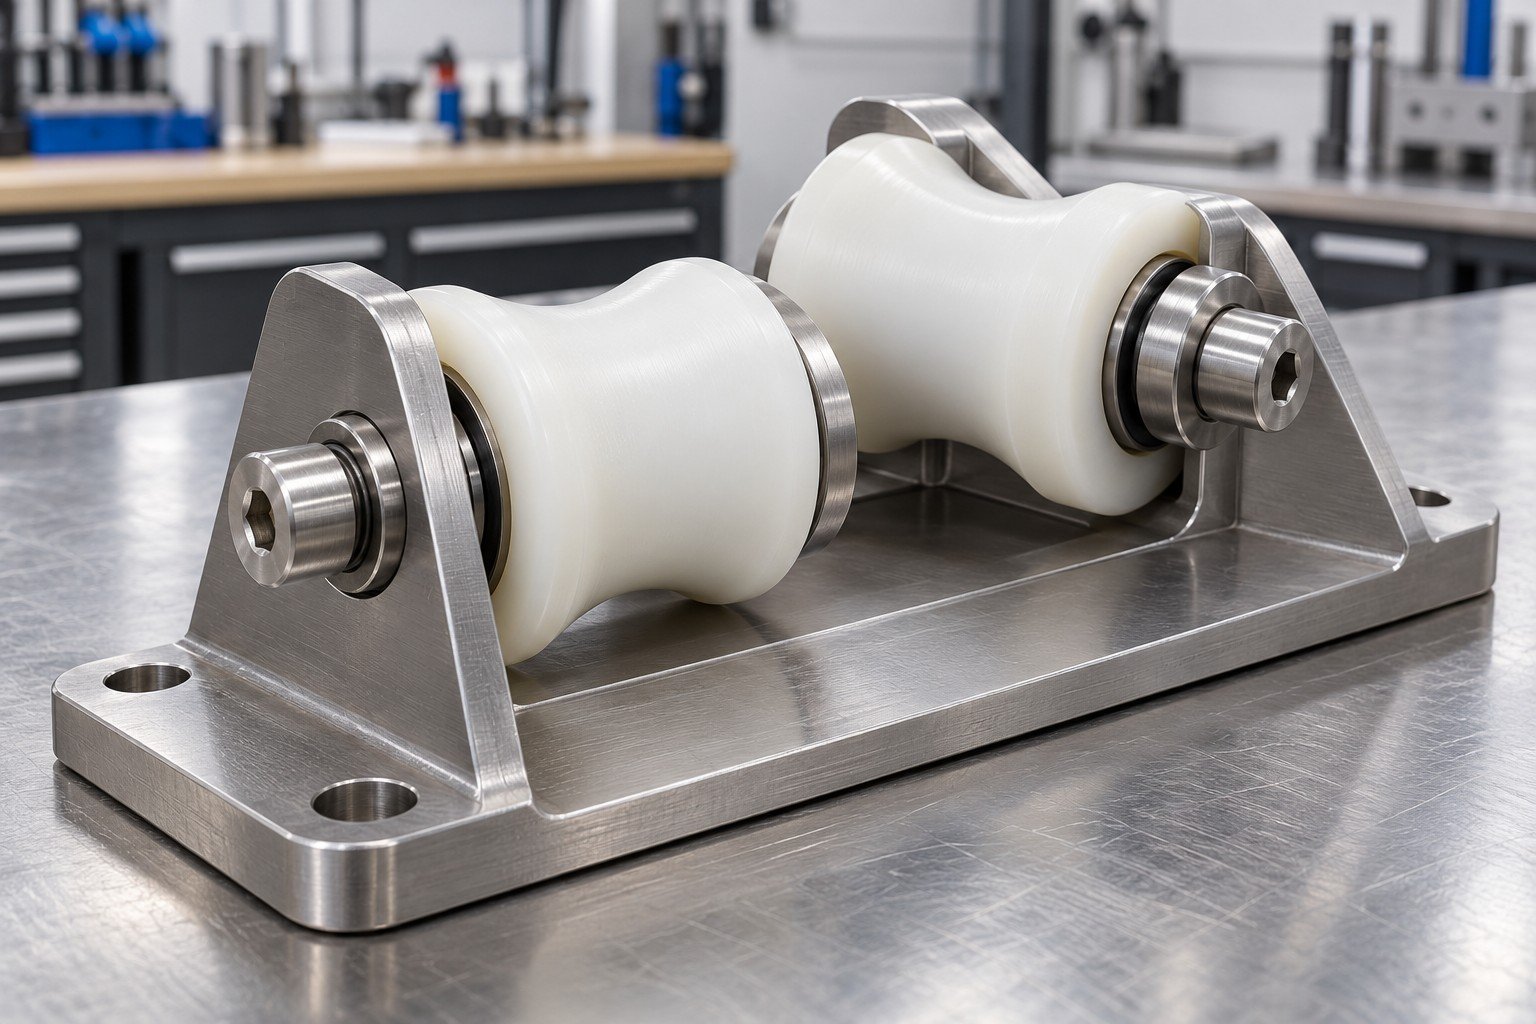
Verify the specified fit, retention and visible condition on the module, with operating validation defined separately where needed.
| Your input | Installed dimensions, workmanship and acceptance method. |
|---|---|
| Your decision | Approve the first complete module and changes. |
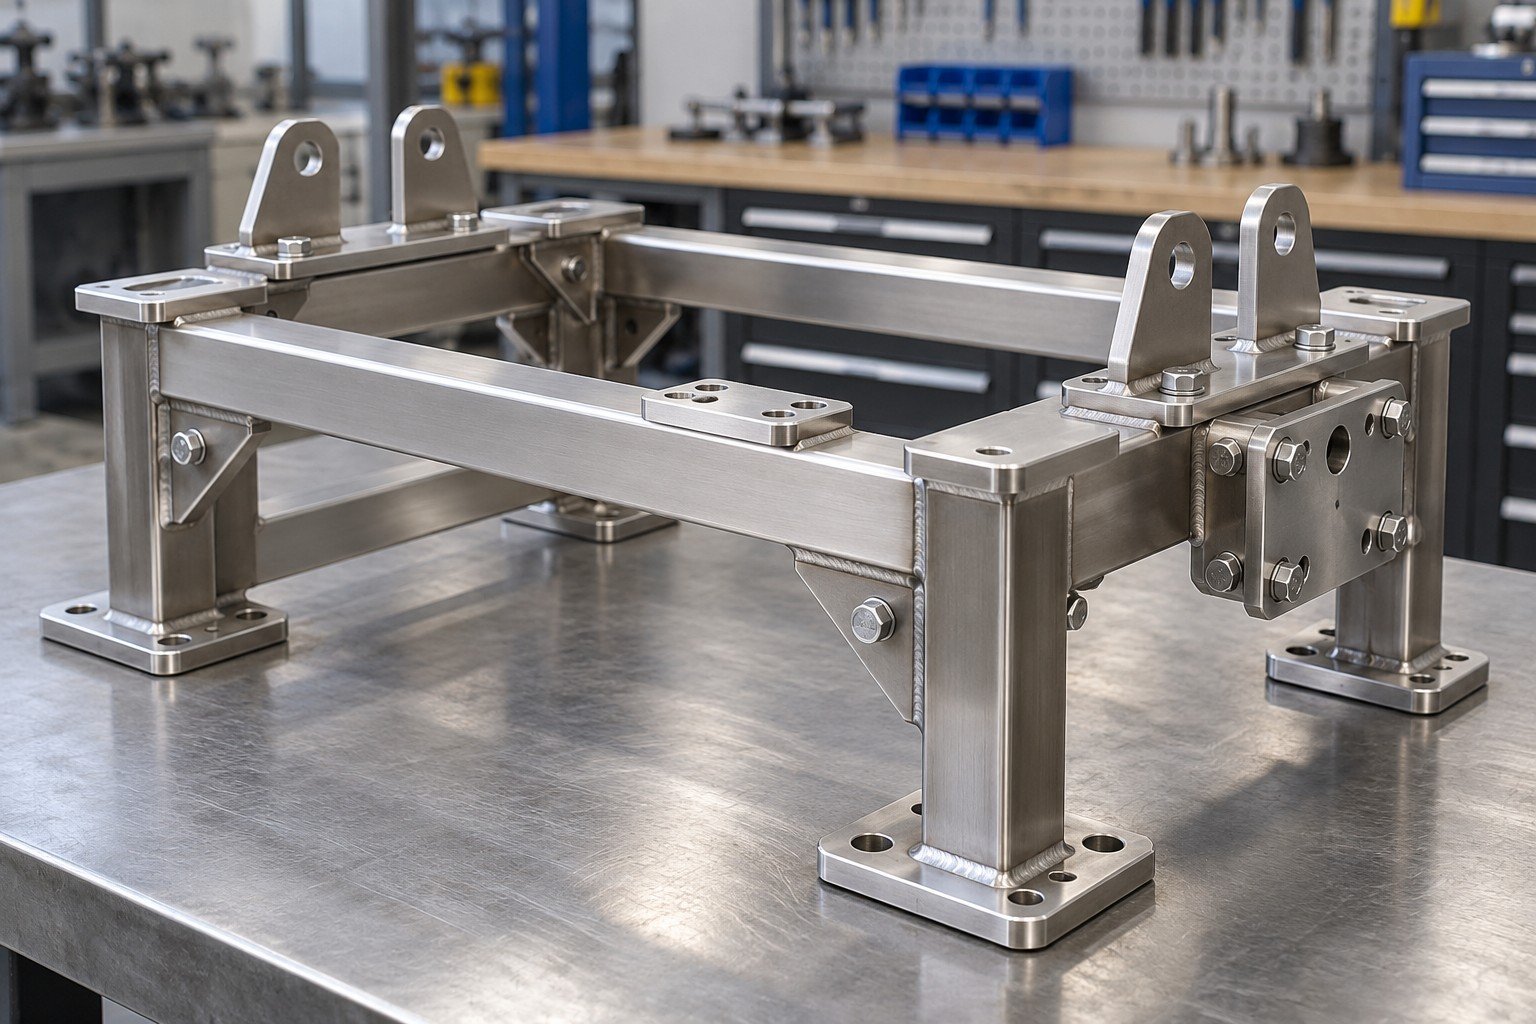
Industrial subassemblies need controlled references after joining, not only an accepted weld or individual bracket. Define the module mounting condition.
| Your input | Joined assembly and final interface drawings. |
|---|---|
| Your decision | Agree locating faces and downstream operation allowance. |
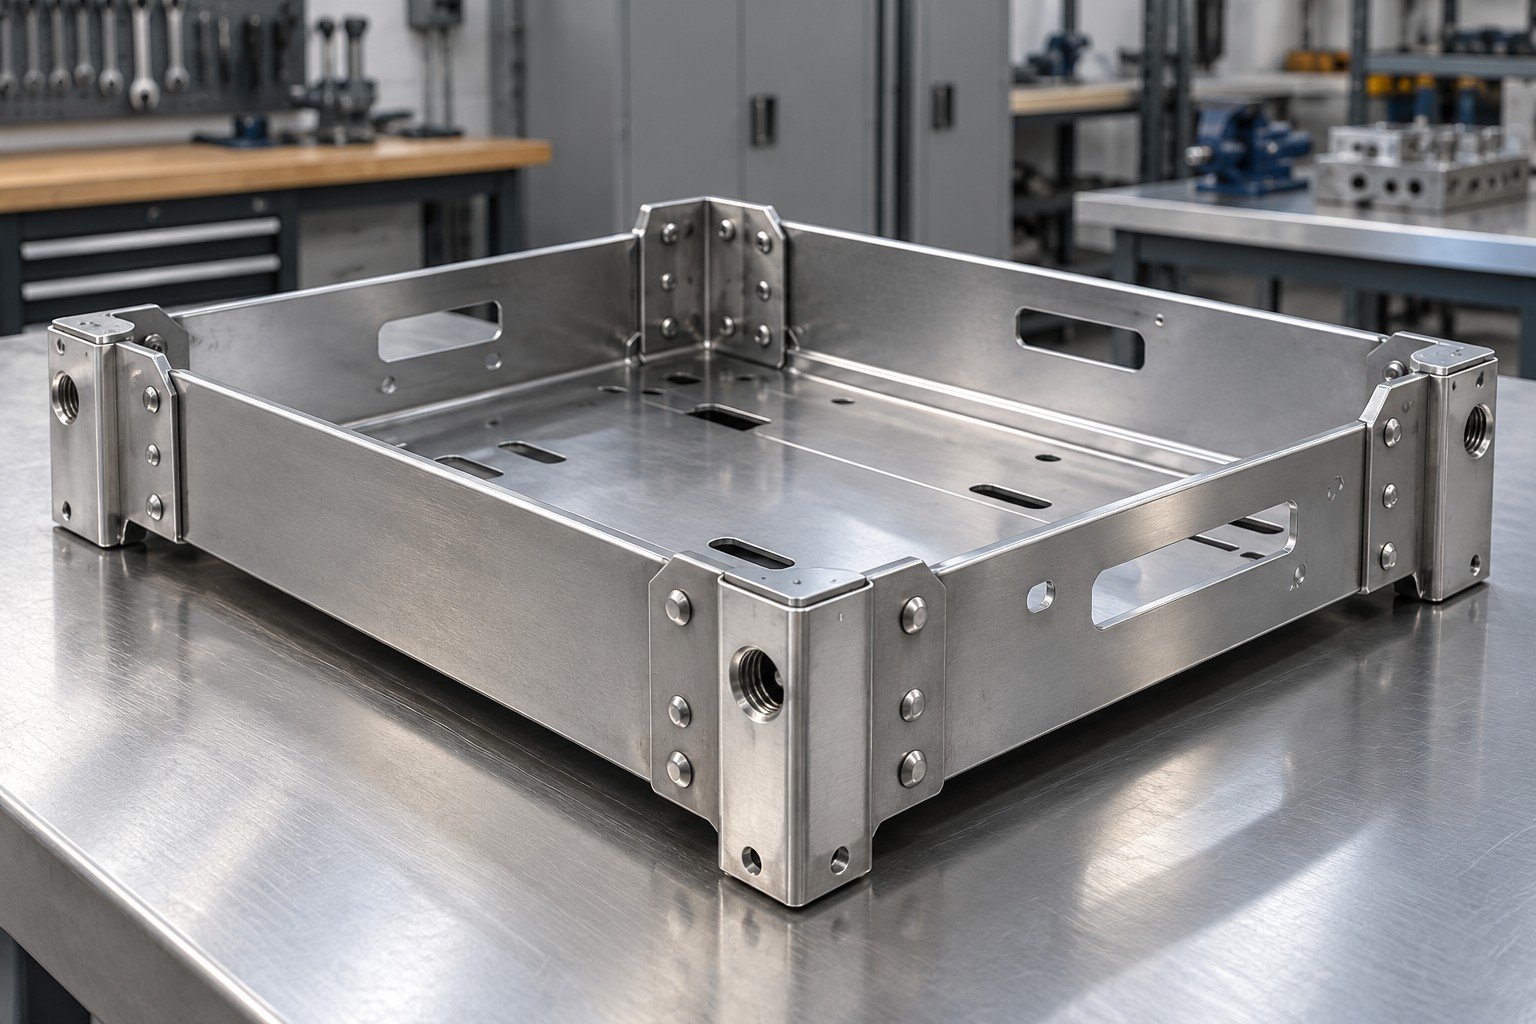
Identify grades, fasteners, joining specifications and supplied components. Confirm special workmanship or qualification requirements before quotation.
| Your input | Controlled BOM and applicable joining requirements. |
|---|---|
| Your decision | Assign materials, operations and acceptance responsibility. |
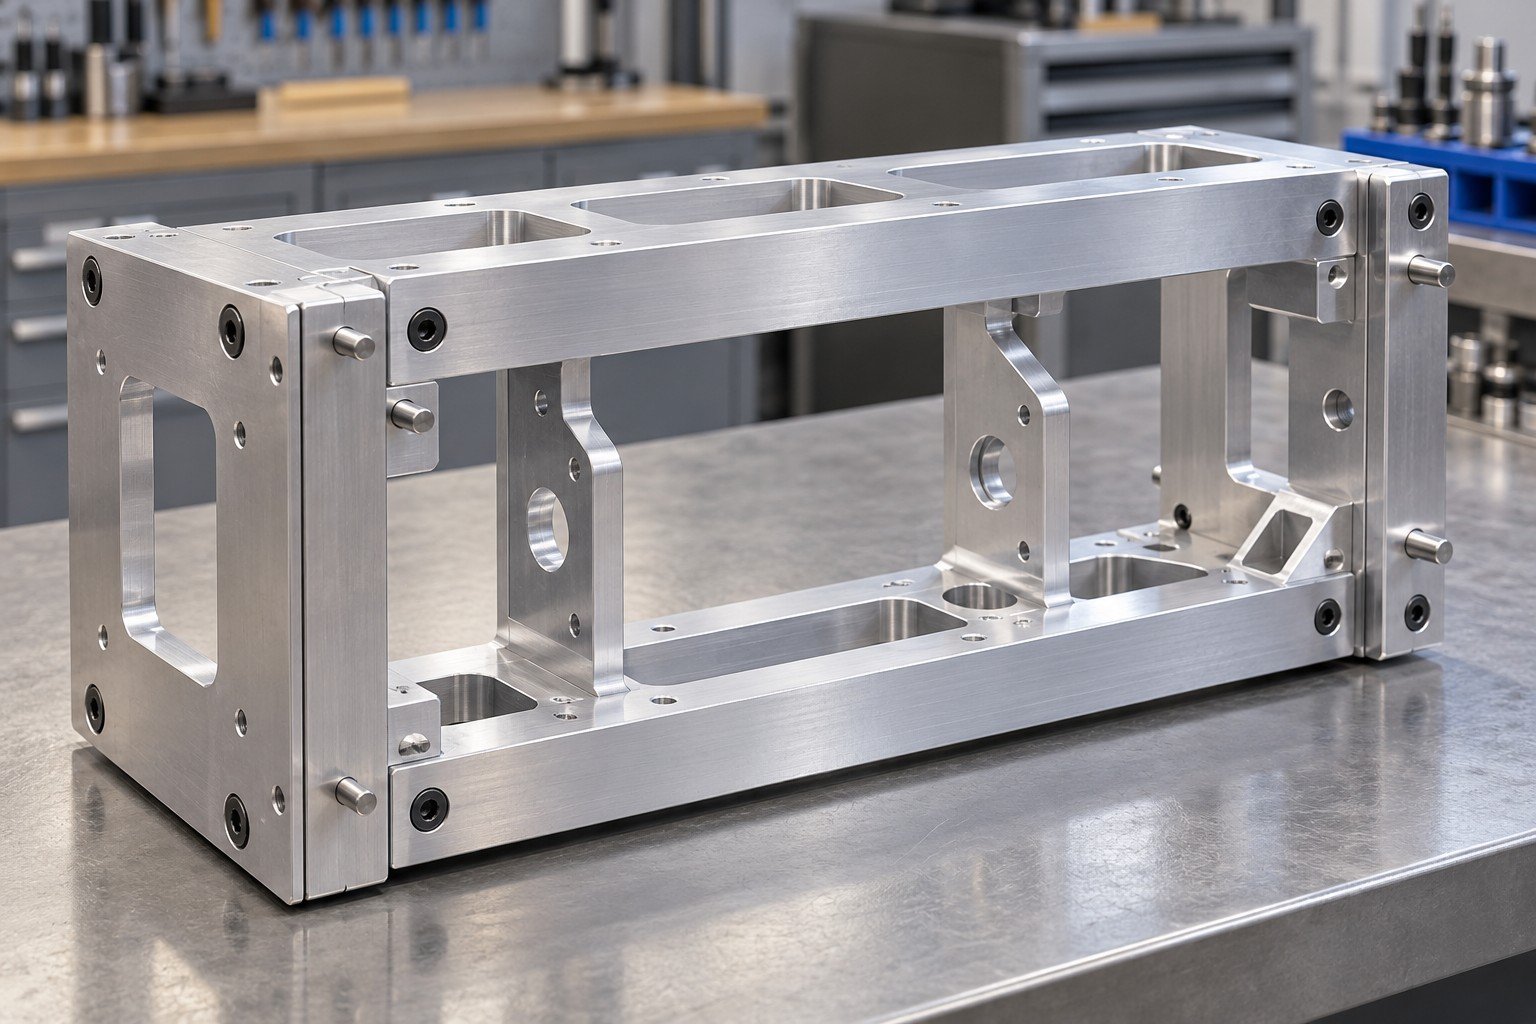
Review joining, machining, finishing and hardware order around distortion and access. Confirm protected threads and critical mounting faces.
| Your input | Process-sensitive features and finished interfaces. |
|---|---|
| Your decision | Agree the sequence, fixtures and protected areas. |
Check the final module against agreed dimensions and interface criteria. A joining inspection alone does not establish complete assembled fit.
| Your input | Final drawing, check points and required reports. |
|---|---|
| Your decision | Define deviation approval before repeat supply. |
A custom subassembly needs a defined receiving interface. Identify datums, mating parts, connectors and any loose items needed at installation.
| Your input | Host interface drawing and delivered-state definition. |
|---|---|
| Your decision | Agree which mating checks belong to the supplier. |
List approved dowels, gaskets, sensors or harnesses when included. Electrical installation and testing require their own confirmed scope.
| Your input | Approved part numbers, wiring details if applicable and supply list. |
|---|---|
| Your decision | Assign purchasing, installation and verification. |
Review insertion direction, screw access, connector engagement and seal protection in the intended receiving condition.
| Your input | Host geometry, access restrictions and assembly sequence. |
|---|---|
| Your decision | Agree fixtures, interface gauges and installation ownership. |
A successful interface-gauge fit demonstrates the agreed geometry, not every behavior of the finished product. Record exactly what was checked.
| Your input | Gauge definition, limits and functional responsibilities. |
|---|---|
| Your decision | Keep module and final-product acceptance distinct. |
Use prototype subassembly work to review fit, sequence or a specific check before repeat ordering. List open decisions and what evidence will close them.
| Your input | Trial quantity, design revision and review objectives. |
|---|---|
| Your decision | Agree first-build milestones and approval authority. |
Turnkey subassembly means an agreed procurement and build scope. It does not automatically include product design, every component manufacture or certification.
| Your input | BOM, approved sources and customer-supplied list. |
|---|---|
| Your decision | Define shortages, alternatives, excess stock and ownership. |
Low volume subassembly still requires controlled drawings, BOM and work instructions. Review revisions and component changes before the next release.
| Your input | Accepted module baseline and change procedure. |
|---|---|
| Your decision | Record changes and affected units or lots. |
Subassembly and kitting describe different delivery states. A kit groups items; an assembled module joins them and receives the agreed checks.
| Your input | Installed-item list, loose-item list and packing plan. |
|---|---|
| Your decision | Identify module acceptance separately from kit completeness. |
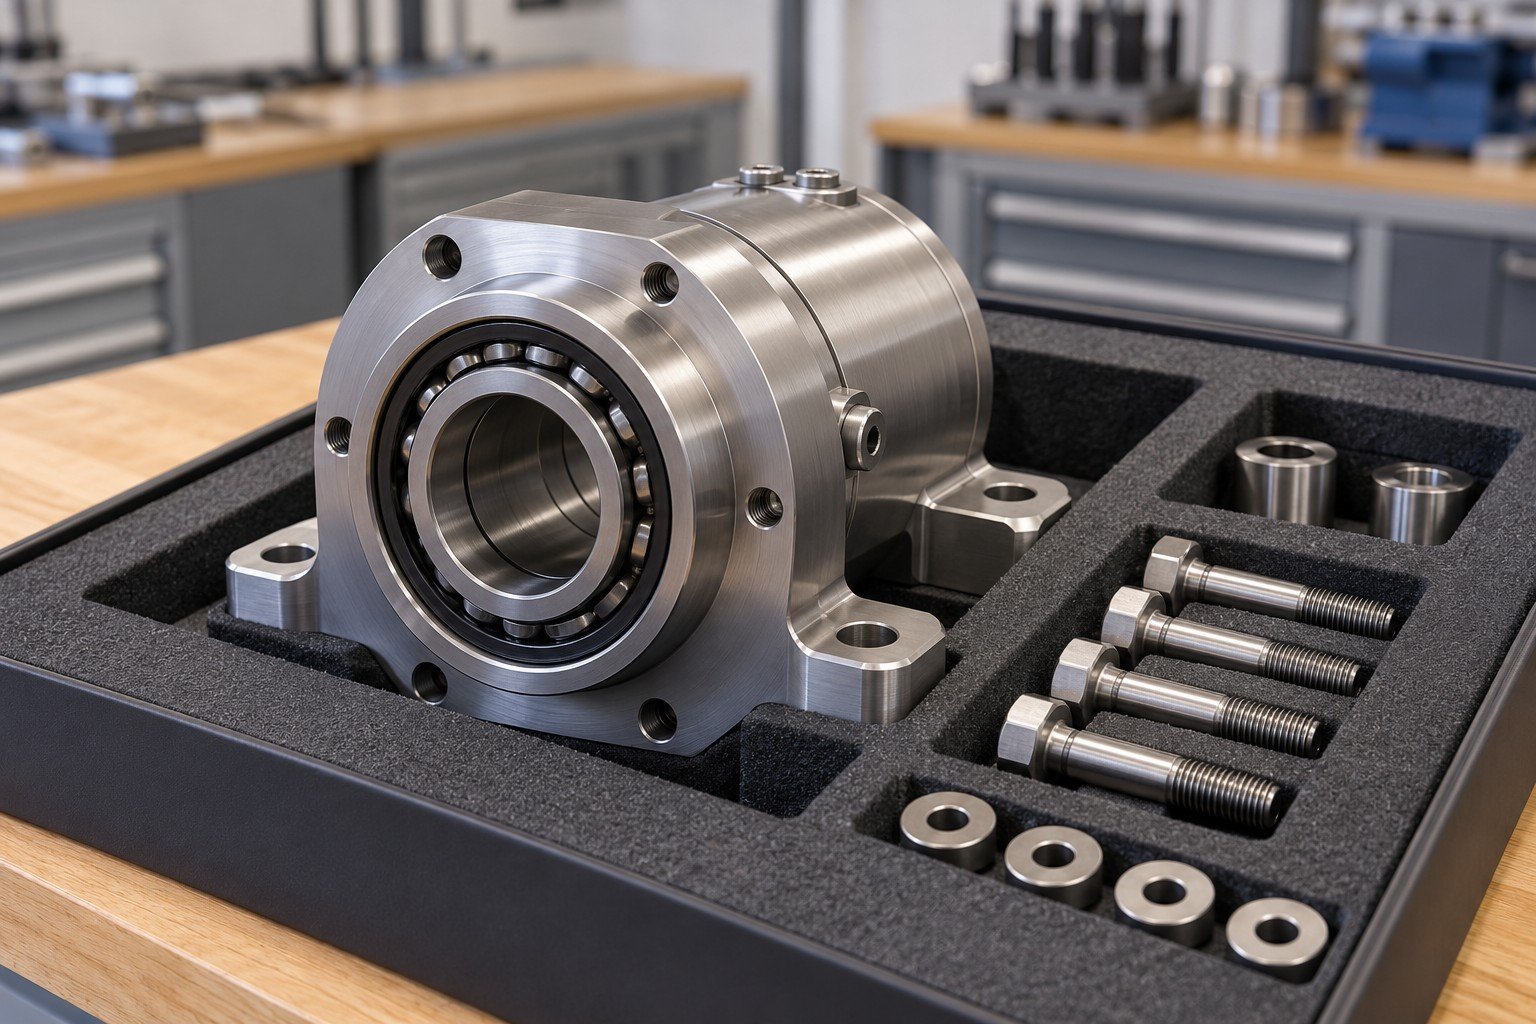
Material and component names are inputs, not a complete acceptance specification.
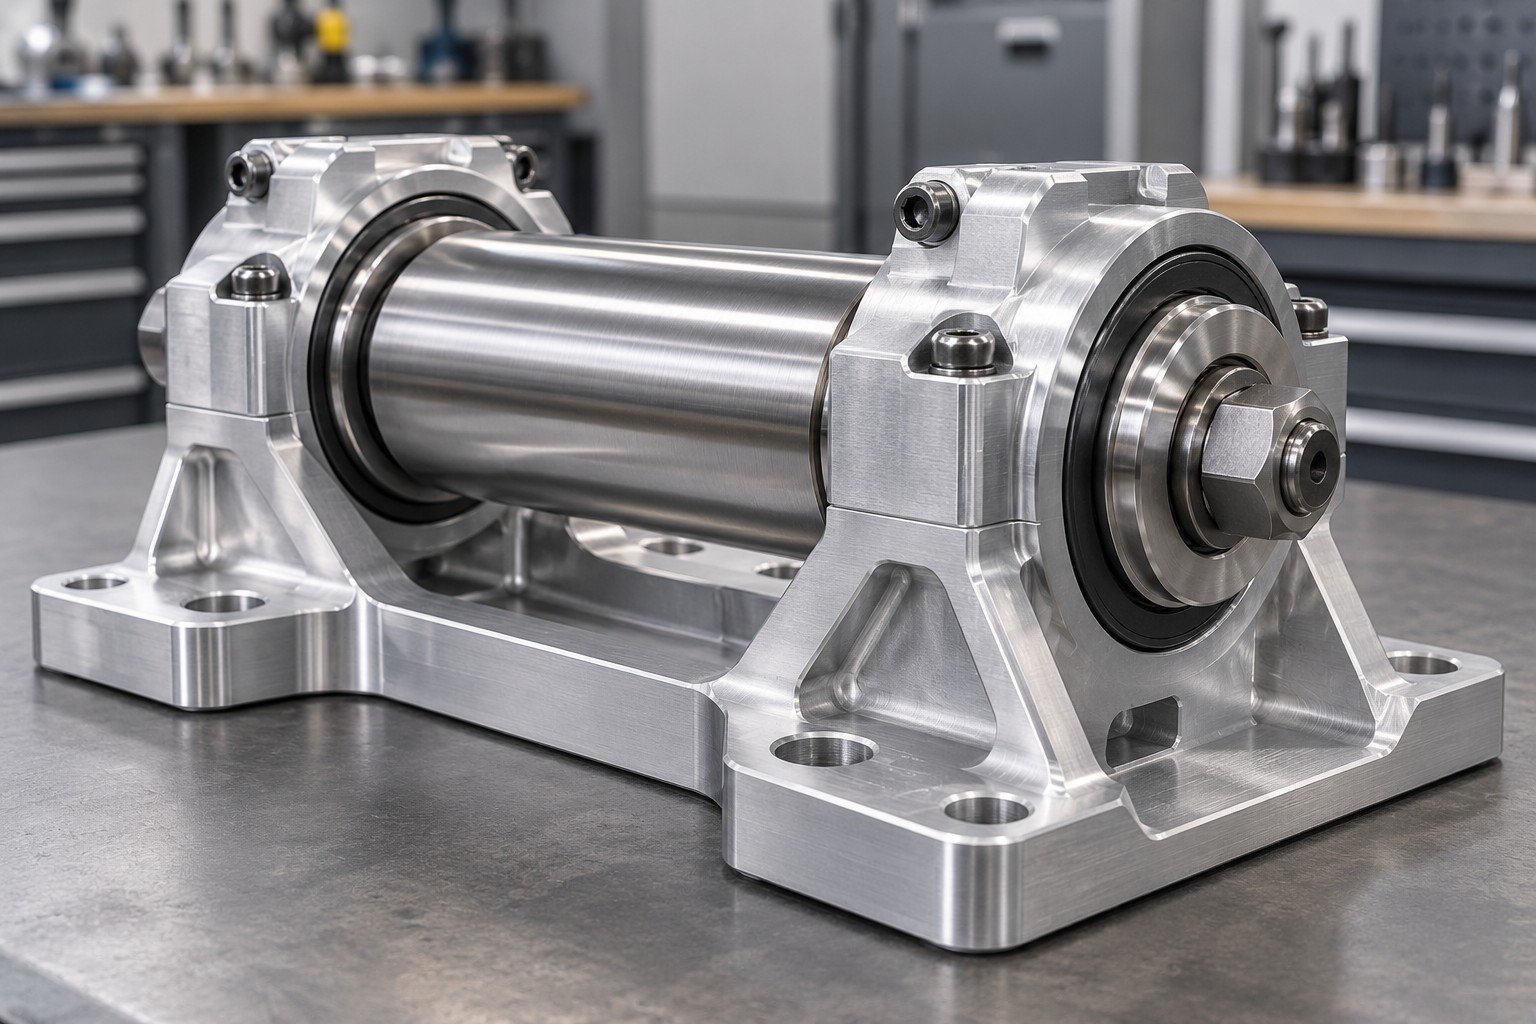
For metal subassembly work, control the mounting references, bores and finished condition.
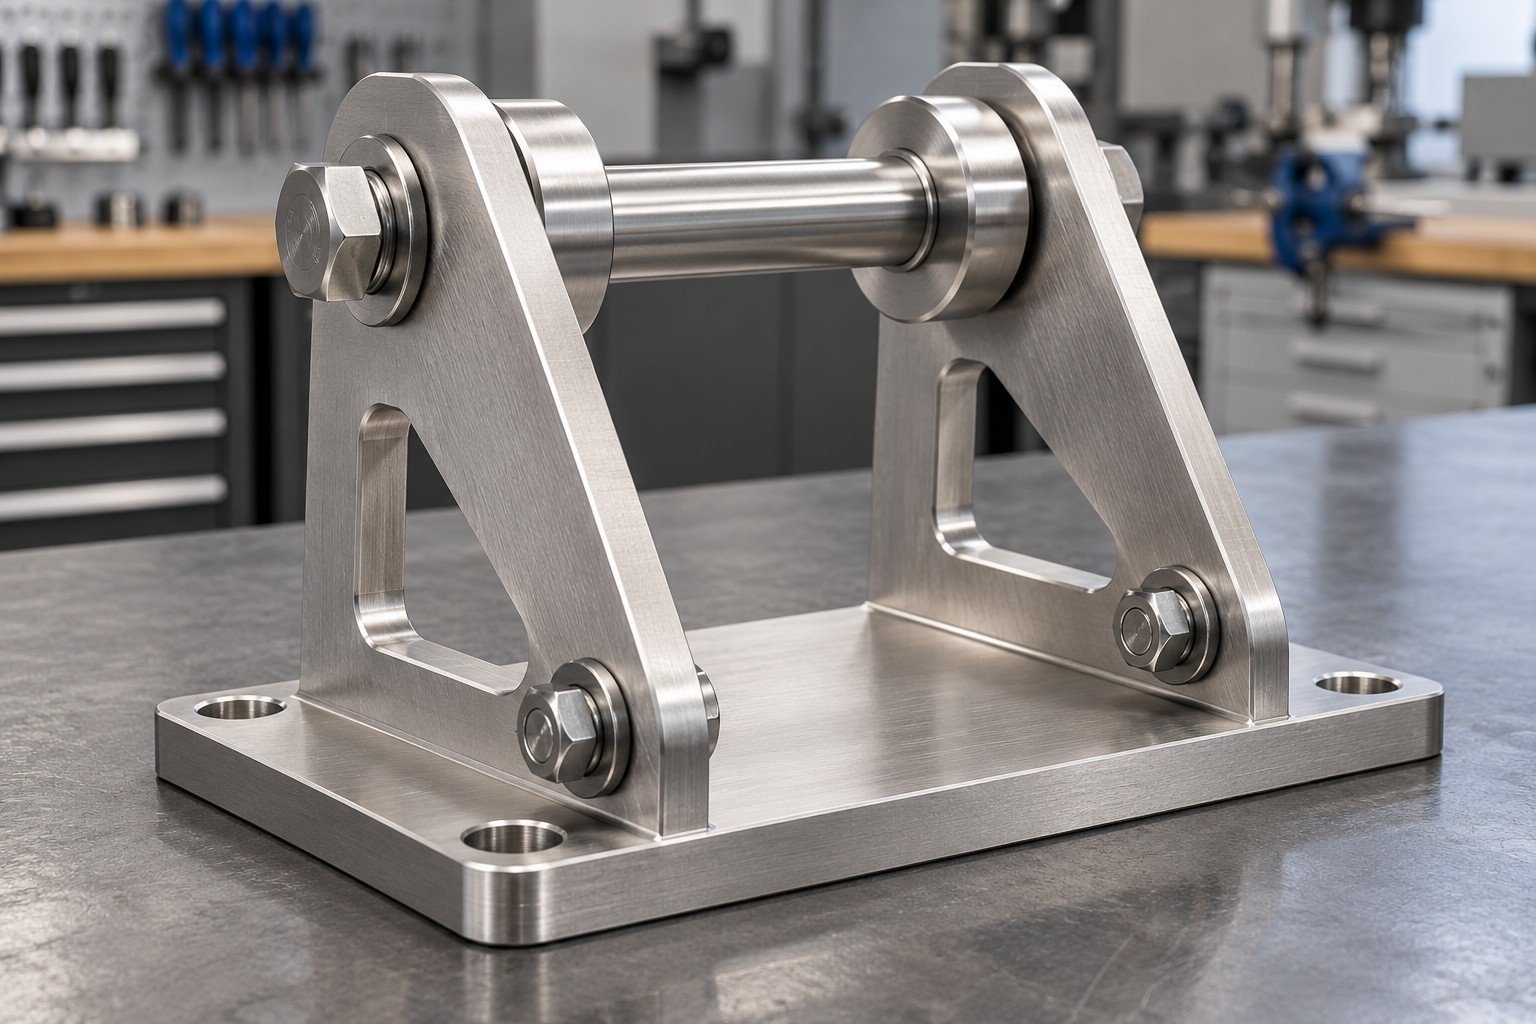
Specify grade, surface, joining requirements and acceptable visible condition.
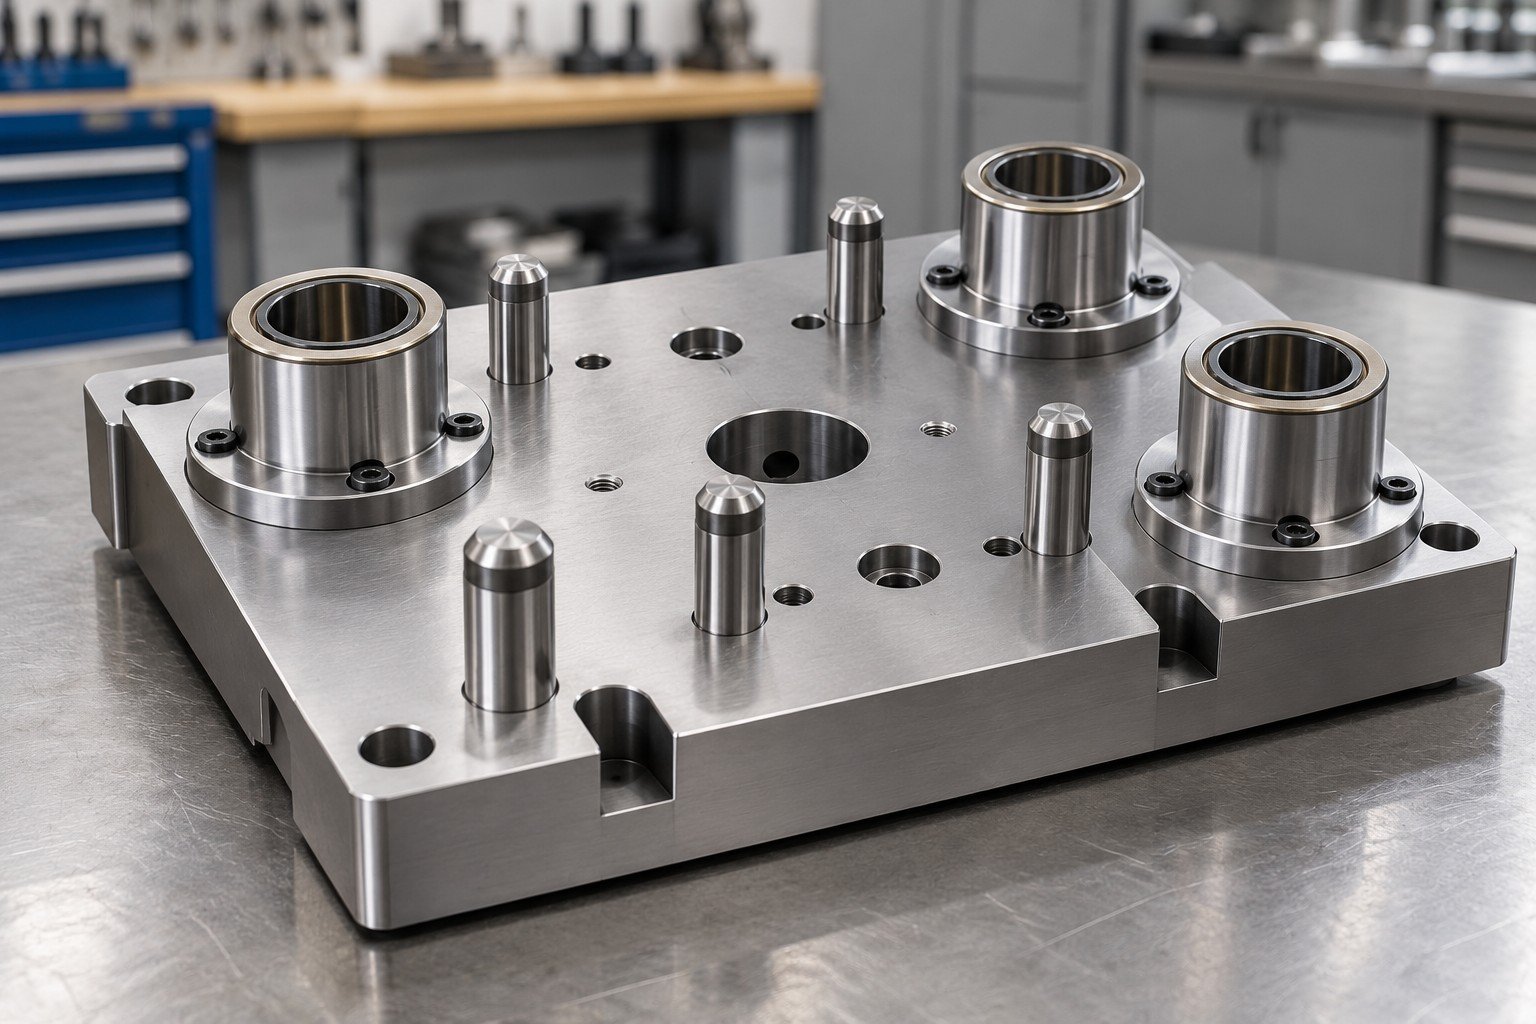
Define dowel, bushing and support interfaces with the intended installation method.
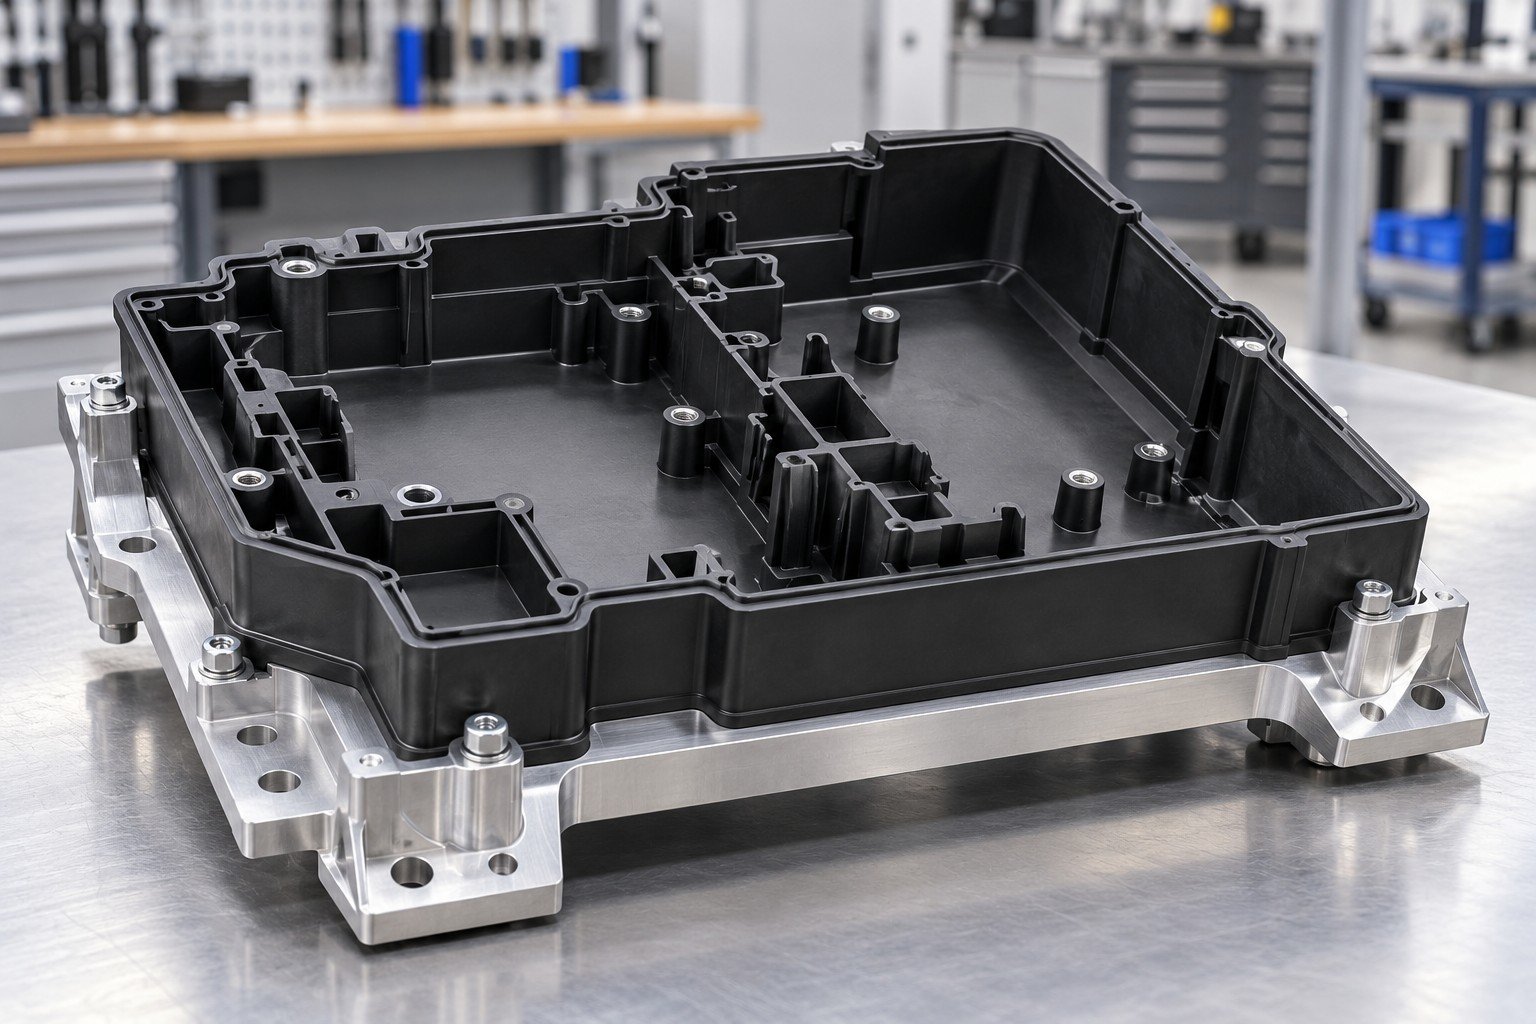
For plastic subassembly, confirm grade, inserts, loads and retention requirements.
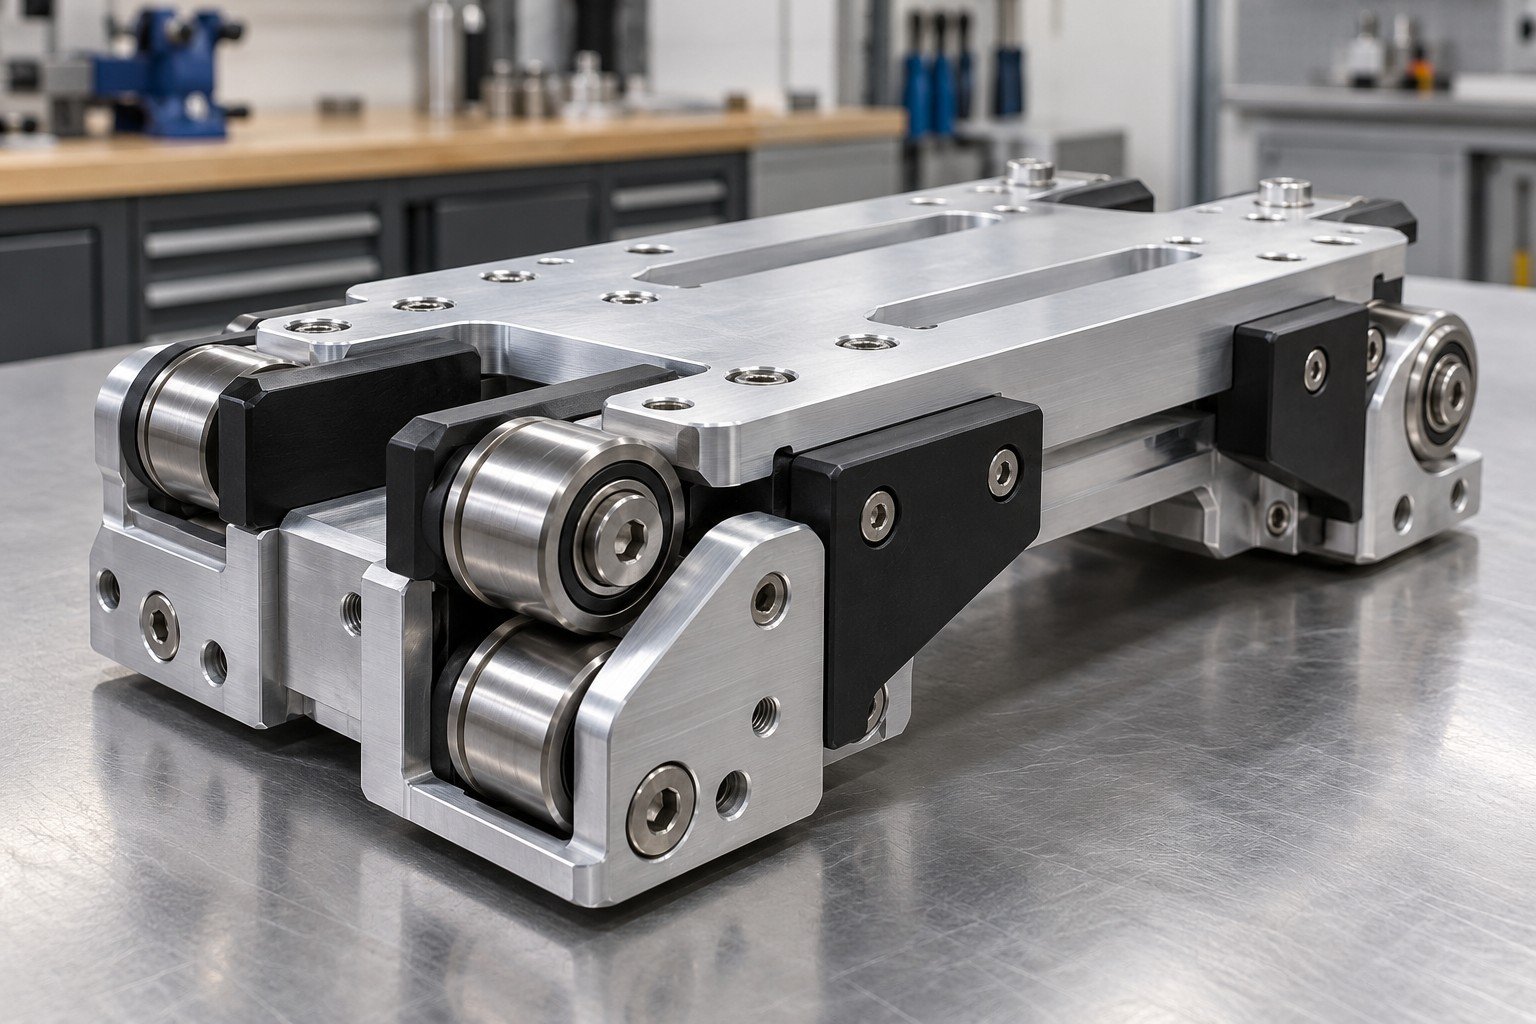
Identify approved grades and the contact, movement and replacement requirements.
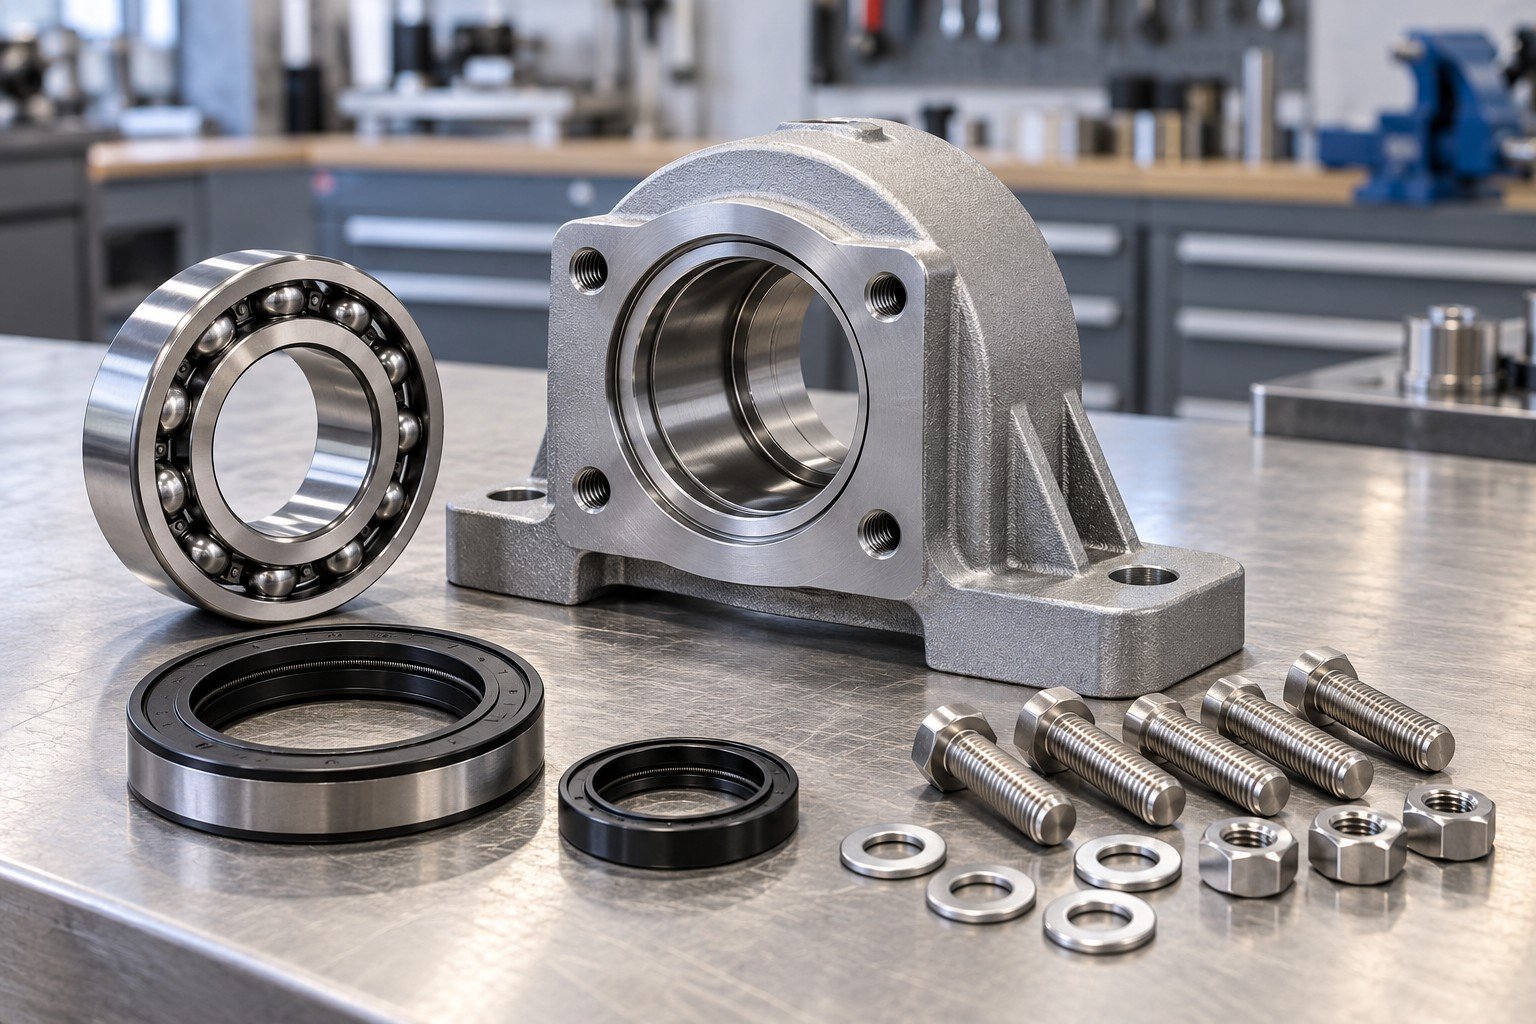
Use approved bearings, seals and fasteners; record sourcing and substitution authority.
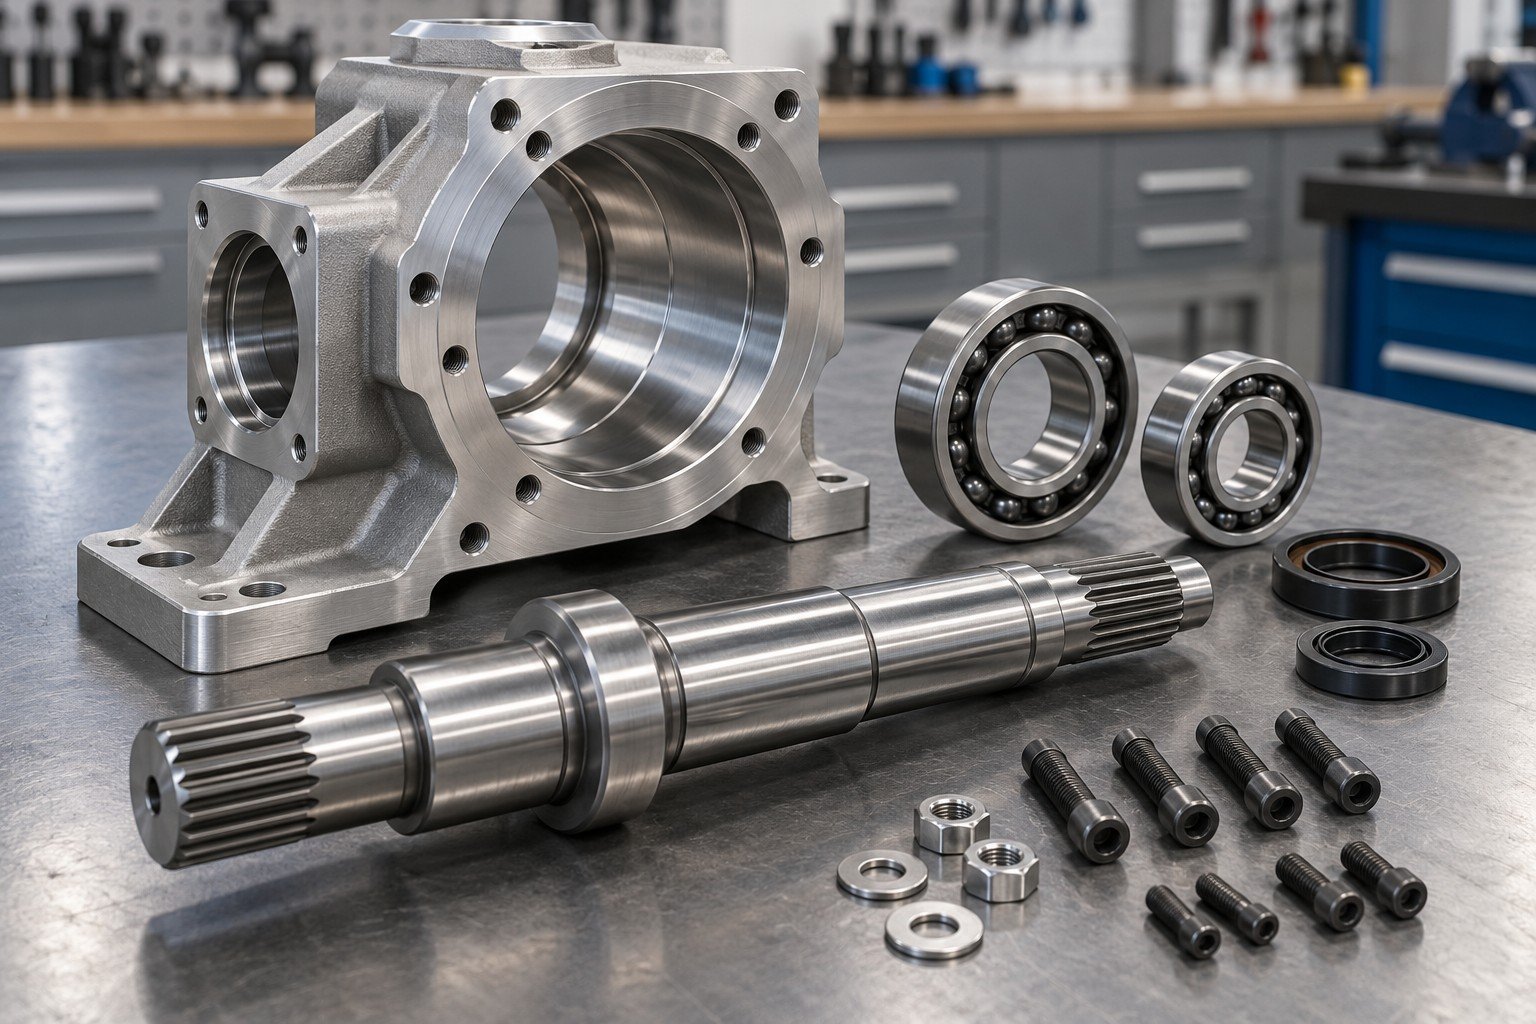
Record installed parts, loose items, excluded work and the mating product interface.
Approve the module and the interface your next build will use.
Separate manufactured, purchased and supplied components; approve alternatives before use.
Approve the module and the interface your next build will use.
Connect subassembly work instructions, locating fixtures and acceptance requirements.
Approve the module and the interface your next build will use.
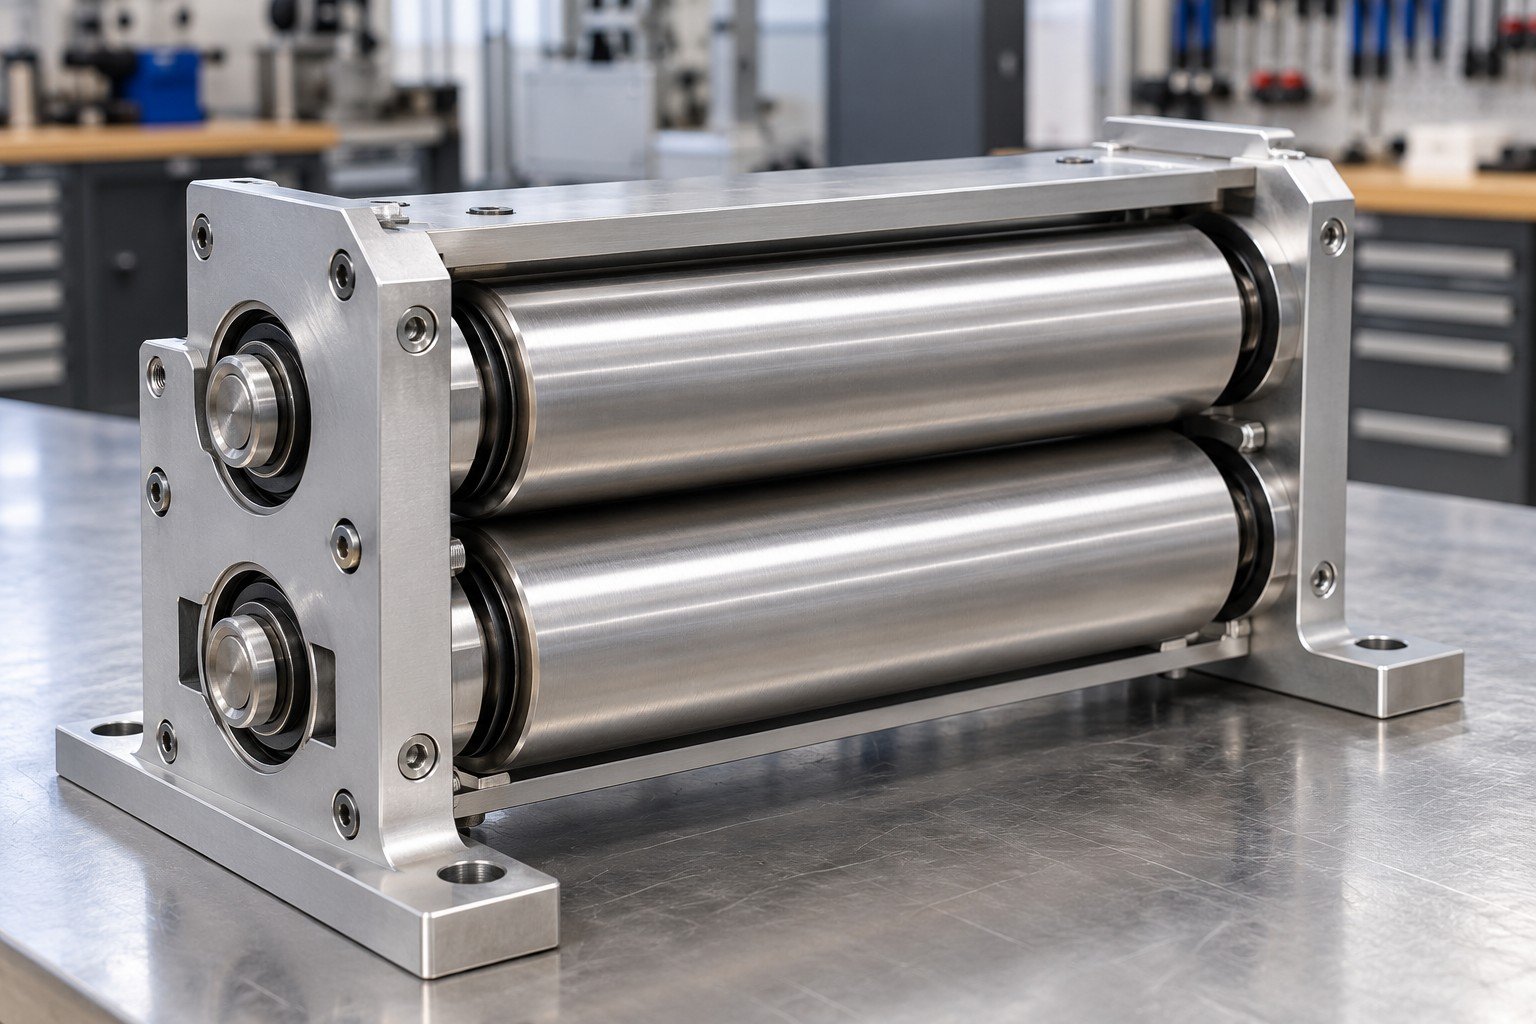
Use the first module to close fit, sequence, workmanship and interface questions.
Approve the module and the interface your next build will use.
Capture specified results and deviations; define final-product validation separately.
Approve the module and the interface your next build will use.
Link part number, revision, quantity, packing and agreed release records.
Approve the module and the interface your next build will use.
Review the features that can stop an accepted module from fitting into your next build.
Identify the datum features shared by the subassembly, fixture and receiving product. Unrelated reference schemes can hide an integration error.
| Your input | Module and host interface drawings. |
|---|---|
| Your decision | Agree locating, measurement and receiving ownership. |
Review contributing part dimensions, fits and finish allowances against the assembled requirement. Individually accepted parts can still produce an unacceptable stack.
| Your input | Critical fits, limits and operating condition. |
|---|---|
| Your decision | Use the agreed tolerance analysis and first-module checks. |
Check usable hole depth, fastener length, access and clean threads. Trapped debris or incorrect length can prevent the joint from seating.
| Your input | Thread size, depth and fastening specification. |
|---|---|
| Your decision | Define cleaning, engagement and seating checks. |
Joining, pressing and tightening can distort thin or flexible features. Review the fixture and load path before the build.
| Your input | Geometry, joining sequence and installation loads. |
|---|---|
| Your decision | Confirm supports and assembled-state inspection. |
Review finish build-up, masking and handling at bores, threads, seats and visible faces. Cleanliness needs a stated criterion.
| Your input | Finish specification and protected features. |
|---|---|
| Your decision | Agree sequence, cleaning and surface acceptance. |
Metal and polymer interfaces can respond differently to temperature, chemicals and load. Grade names alone do not establish suitability.
| Your input | Material grades and intended working conditions. |
|---|---|
| Your decision | Confirm retention, wear and applicable validation. |
Subassembly quality control includes the correct BOM, drawings and permitted alternatives. A component substitution can change the host interface.
| Your input | Accepted revisions and approved change process. |
|---|---|
| Your decision | Authorize changes and identify affected deliveries. |
Subassembly inspection and final-product testing answer different questions. Define coverage rather than assuming a module report proves complete system performance.
| Your input | Check methods, limits, sampling and records. |
|---|---|
| Your decision | Assign module versus final-product acceptance responsibility. |
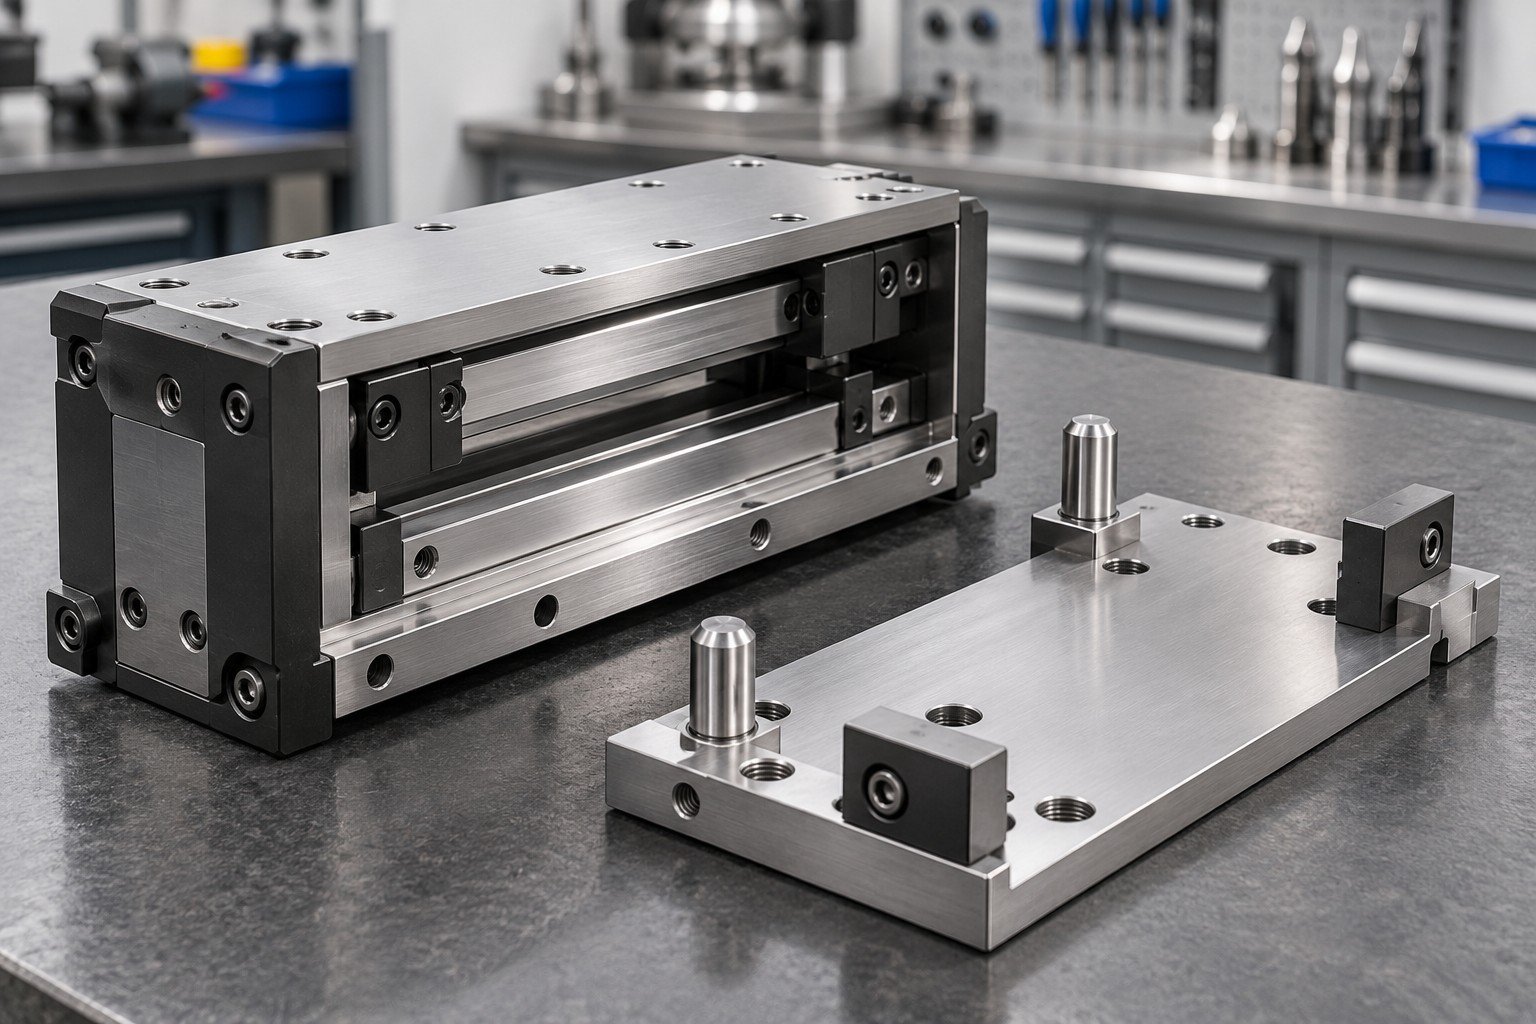
Keep the installed condition and the next receiving operation connected.
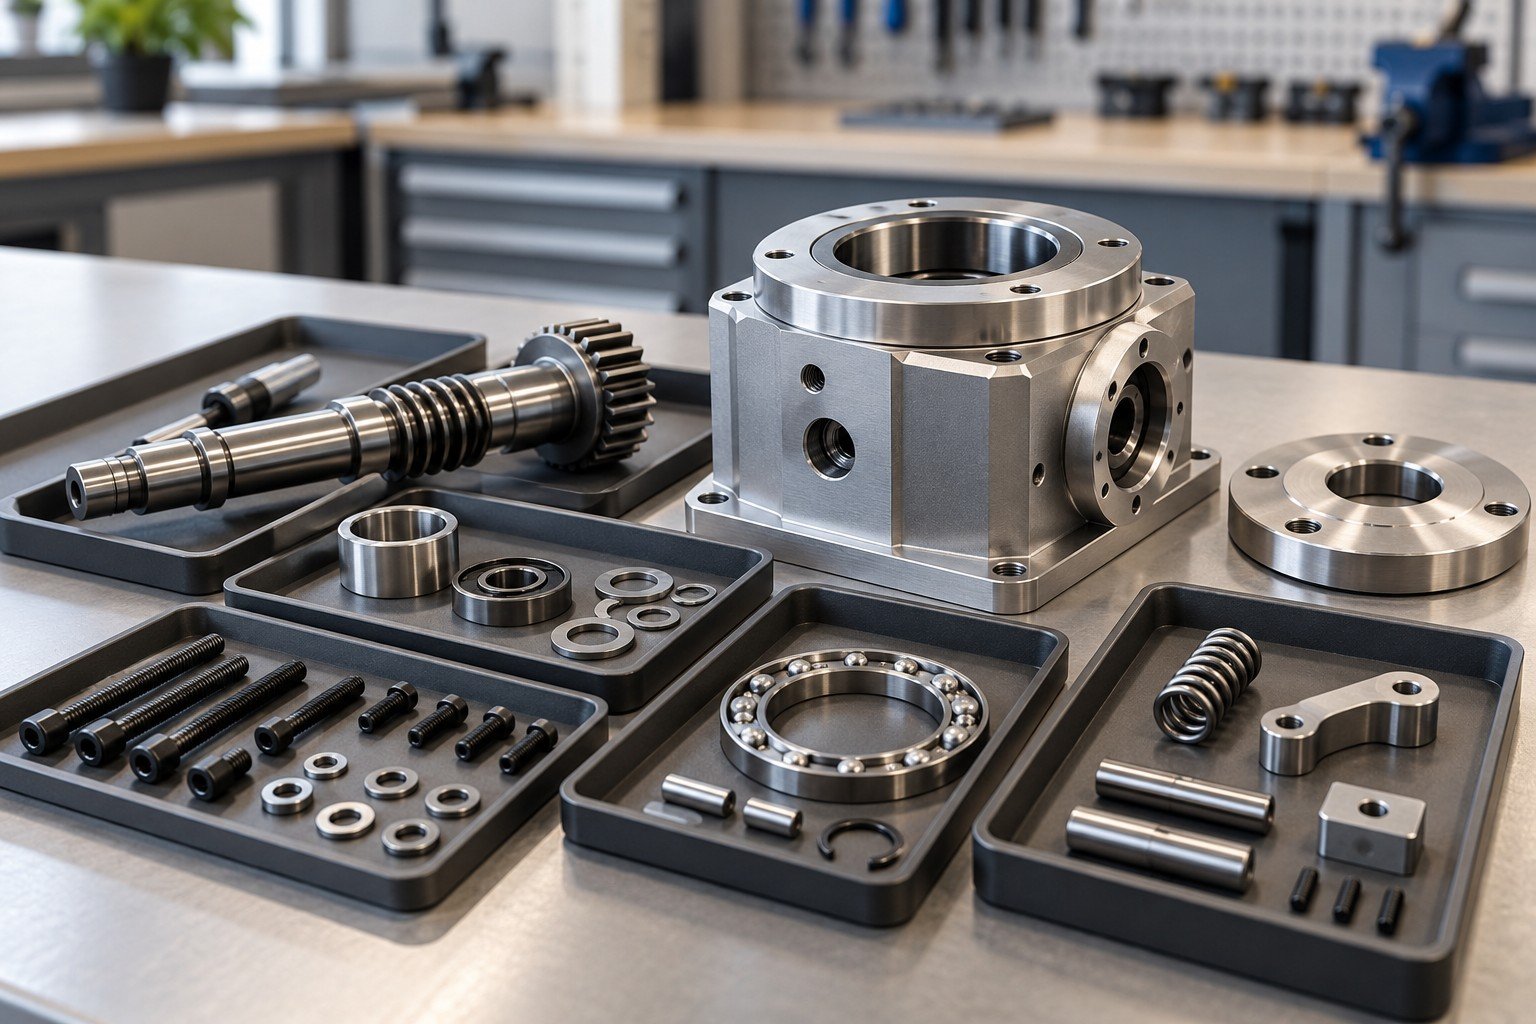
Reconcile quantities, revisions, supply ownership and incoming condition.
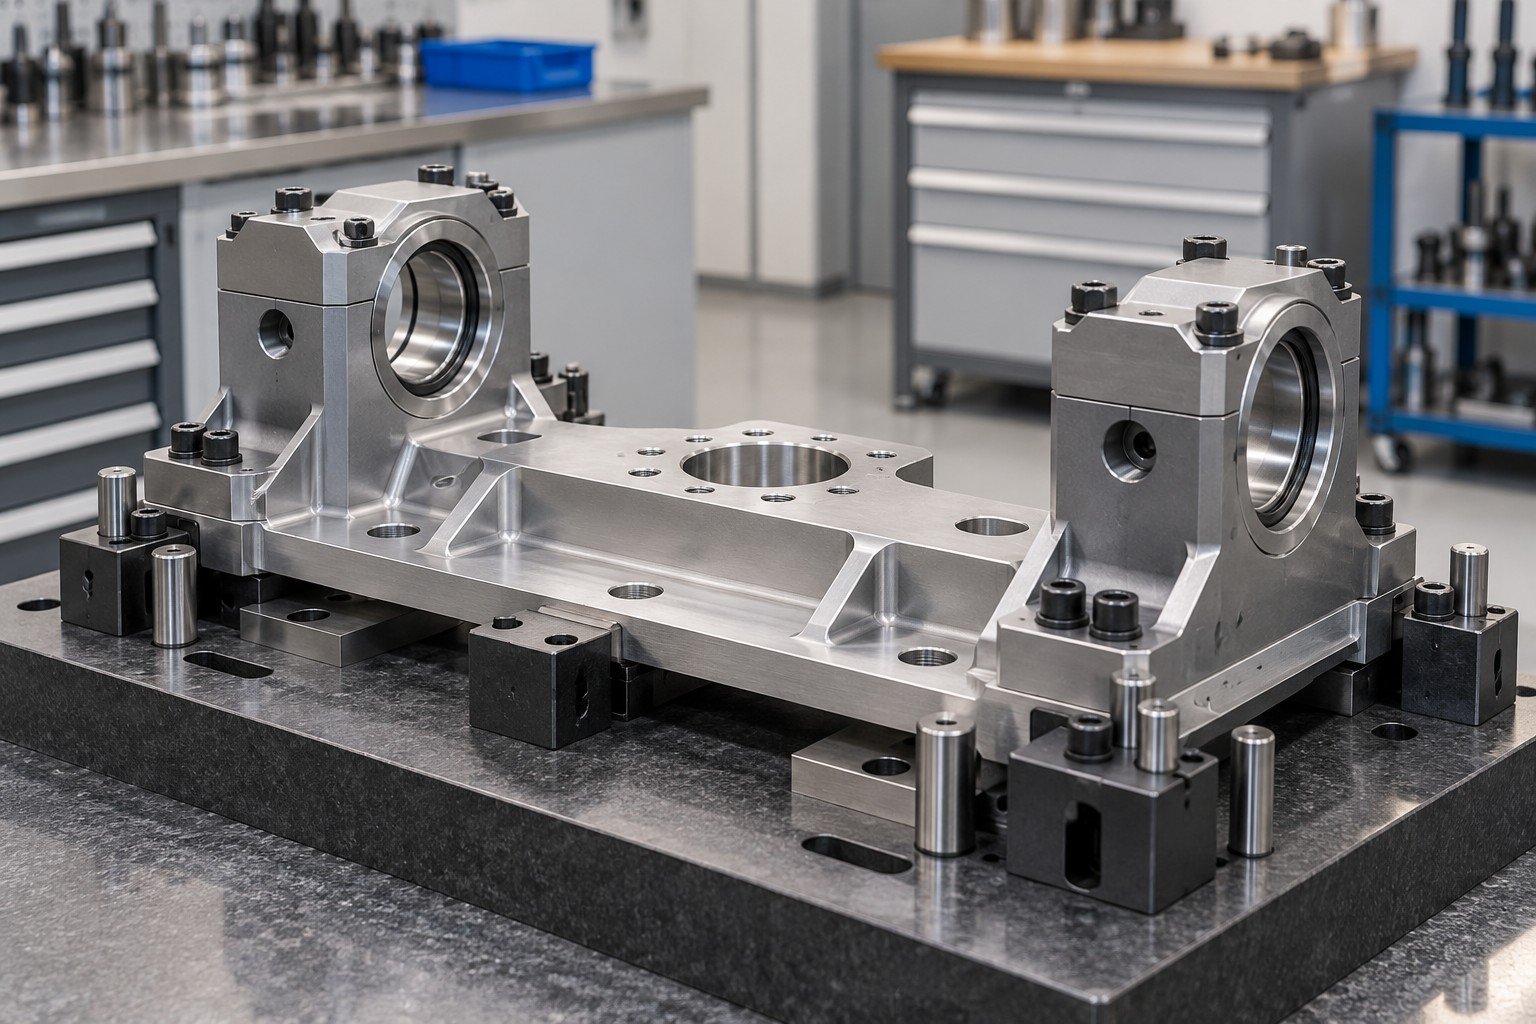
Follow the approved sequence, fixtures, joining and protected surfaces.
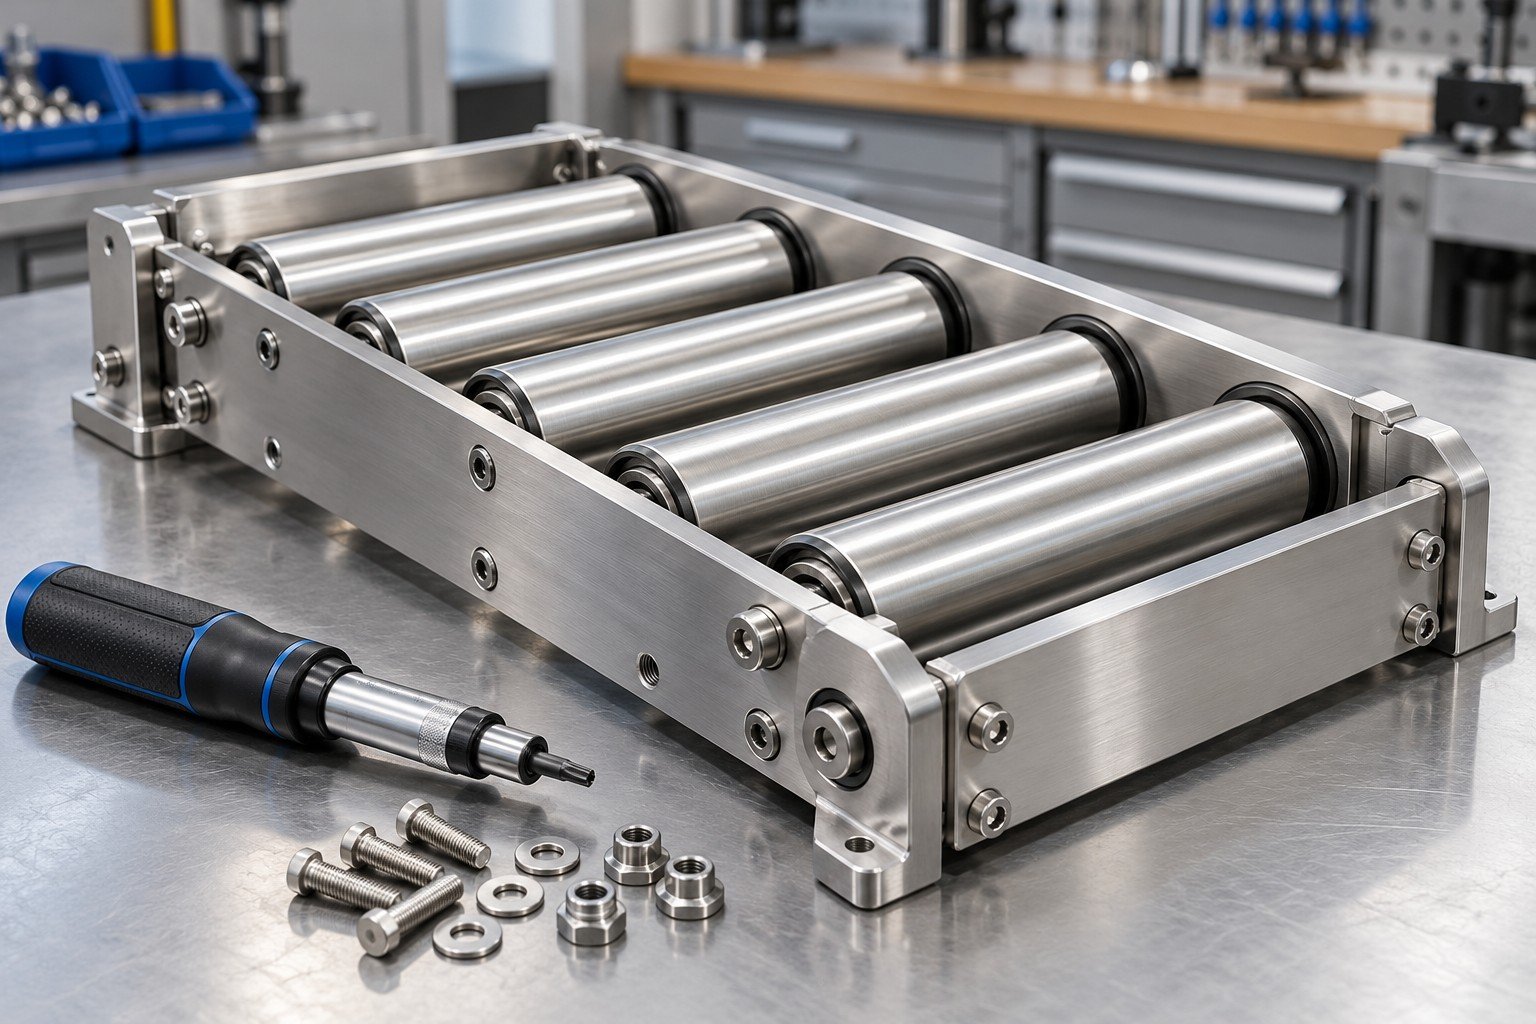
Record specified dimensions, interfaces and agreed function.
Subassembly packaging should protect the accepted revision, interfaces and defined loose items.
Specify what the module report covers, and what will be validated after integration.
| 01 · Identity | Module number, component BOM and drawing revisions. |
|---|---|
| 02 · Installed Parts | Approved items, quantities, orientation and workmanship. |
| 03 · Interfaces | Defined datums, mating features and receiving condition. |
| 04 · Agreed Function | Specified method, operating condition and limits. |
| 05 · Exceptions | Recorded deviations and authorized disposition. |
| 06 · Release | Unit or lot identity, packing list and accepted records. |
Subassembly testing needs an agreed method, resources and acceptance limits. Specialized load, sealing, electrical or life tests are confirmed separately.
| 01 · Identity | Module number, component BOM and drawing revisions. |
|---|---|
| 02 · Installed Parts | Approved items, quantities, orientation and workmanship. |
| 03 · Interfaces | Defined datums, mating features and receiving condition. |
| 04 · Agreed Function | Specified method, operating condition and limits. |
| 05 · Exceptions | Recorded deviations and authorized disposition. |
| 06 · Release | Unit or lot identity, packing list and accepted records. |
Subassembly testing needs an agreed method, resources and acceptance limits. Specialized load, sealing, electrical or life tests are confirmed separately.
| 01 · Identity | Module number, component BOM and drawing revisions. |
|---|---|
| 02 · Installed Parts | Approved items, quantities, orientation and workmanship. |
| 03 · Interfaces | Defined datums, mating features and receiving condition. |
| 04 · Agreed Function | Specified method, operating condition and limits. |
| 05 · Exceptions | Recorded deviations and authorized disposition. |
| 06 · Release | Unit or lot identity, packing list and accepted records. |
Subassembly testing needs an agreed method, resources and acceptance limits. Specialized load, sealing, electrical or life tests are confirmed separately.
| 01 · Identity | Module number, component BOM and drawing revisions. |
|---|---|
| 02 · Installed Parts | Approved items, quantities, orientation and workmanship. |
| 03 · Interfaces | Defined datums, mating features and receiving condition. |
| 04 · Agreed Function | Specified method, operating condition and limits. |
| 05 · Exceptions | Recorded deviations and authorized disposition. |
| 06 · Release | Unit or lot identity, packing list and accepted records. |
Subassembly testing needs an agreed method, resources and acceptance limits. Specialized load, sealing, electrical or life tests are confirmed separately.
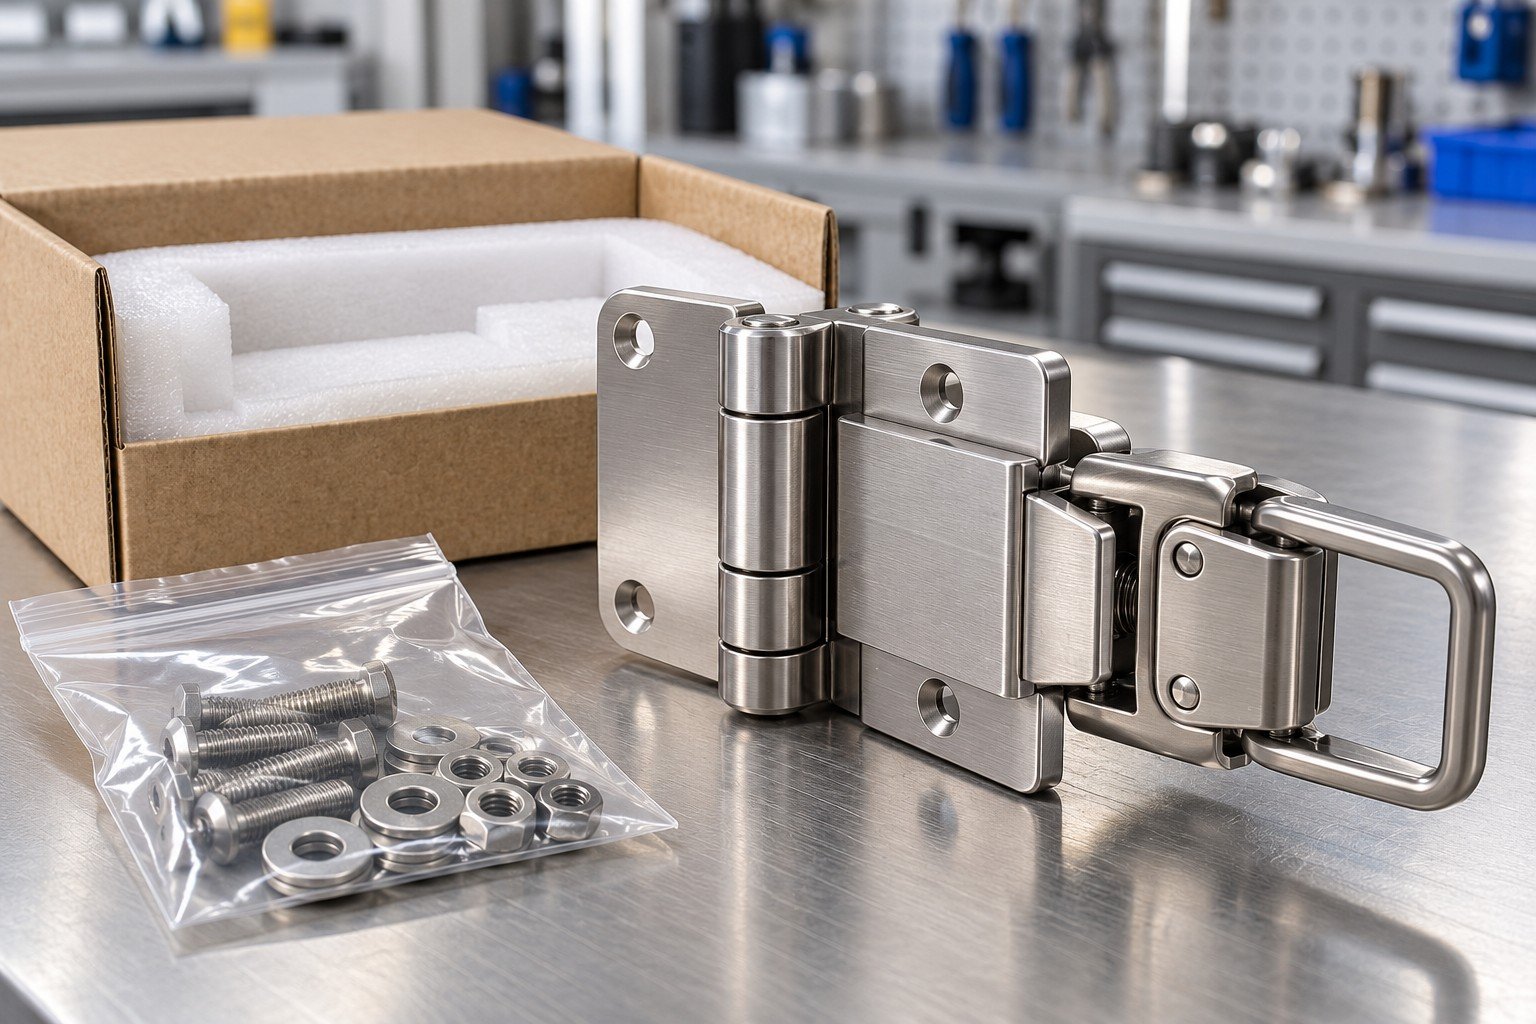
For subassembly contract manufacturing, compare the same installed items, interfaces and evidence.
Manufactured, purchased and customer-supplied items with approved sources.
Fixtures, setup, instructions and required check development.
Assembly, agreed inspection, identification and protected packing.
ILLUSTRATIVE BOM EXAMPLE — NOT A PRICE OR MINIMUM ORDER
Nominal BOM demand only. Samples, setup quantities, spares and permitted process losses are agreed separately. Subassembly inventory management and scheduled releases need a defined stock and delivery agreement.
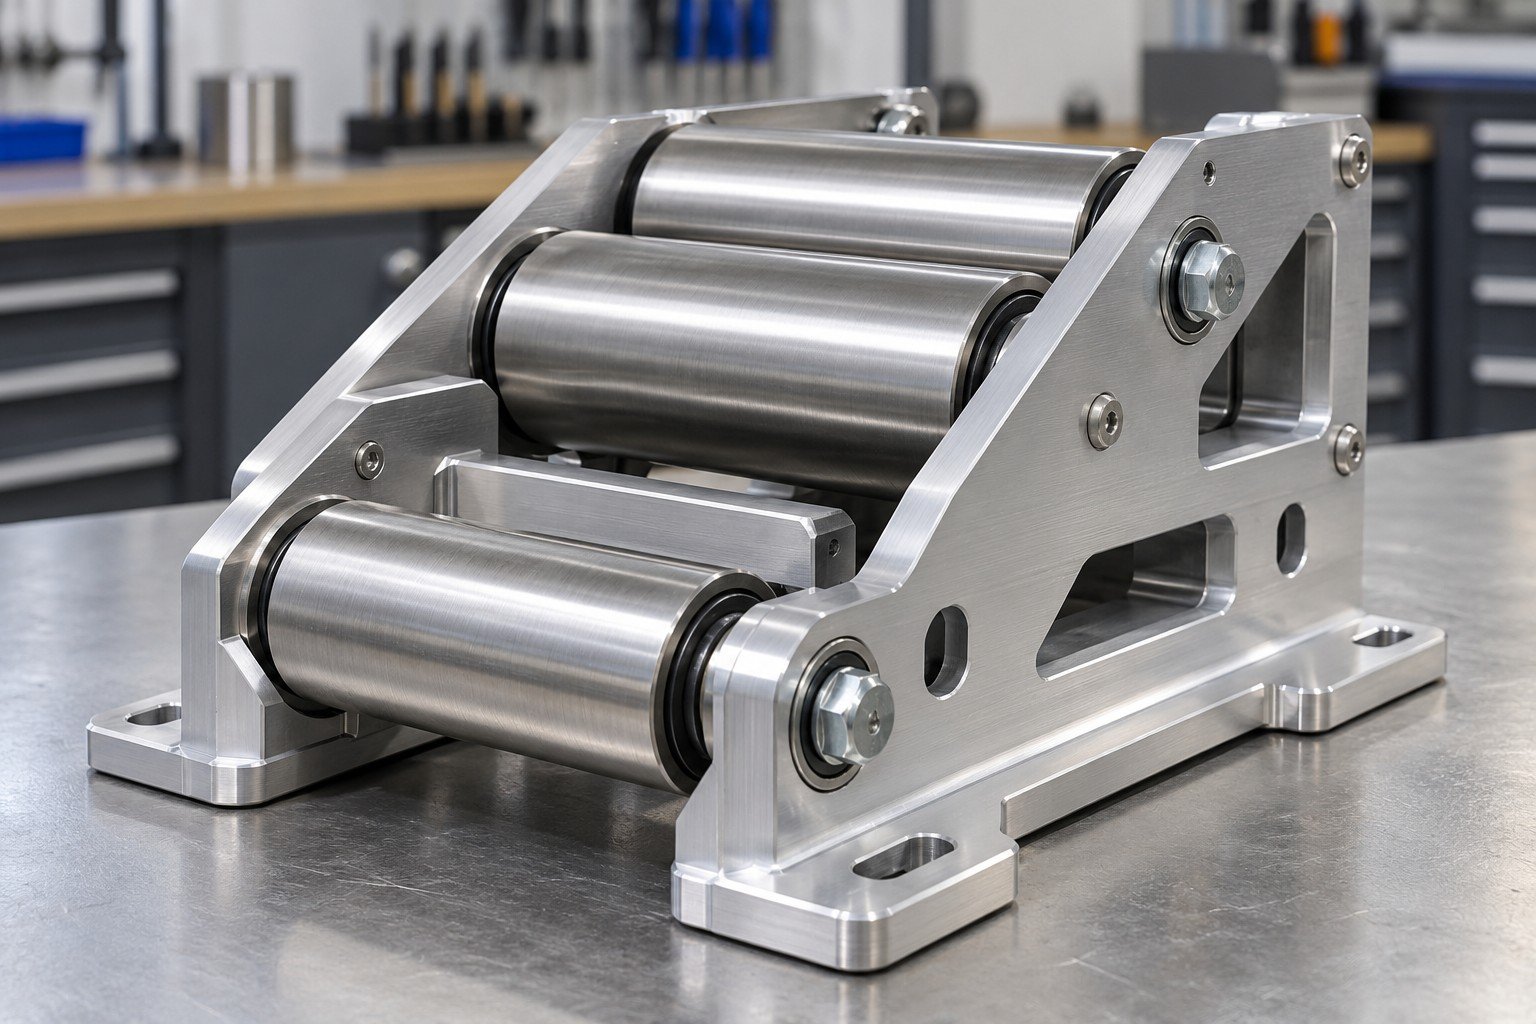
OEM subassemblies with defined mounting and receiving interfaces.
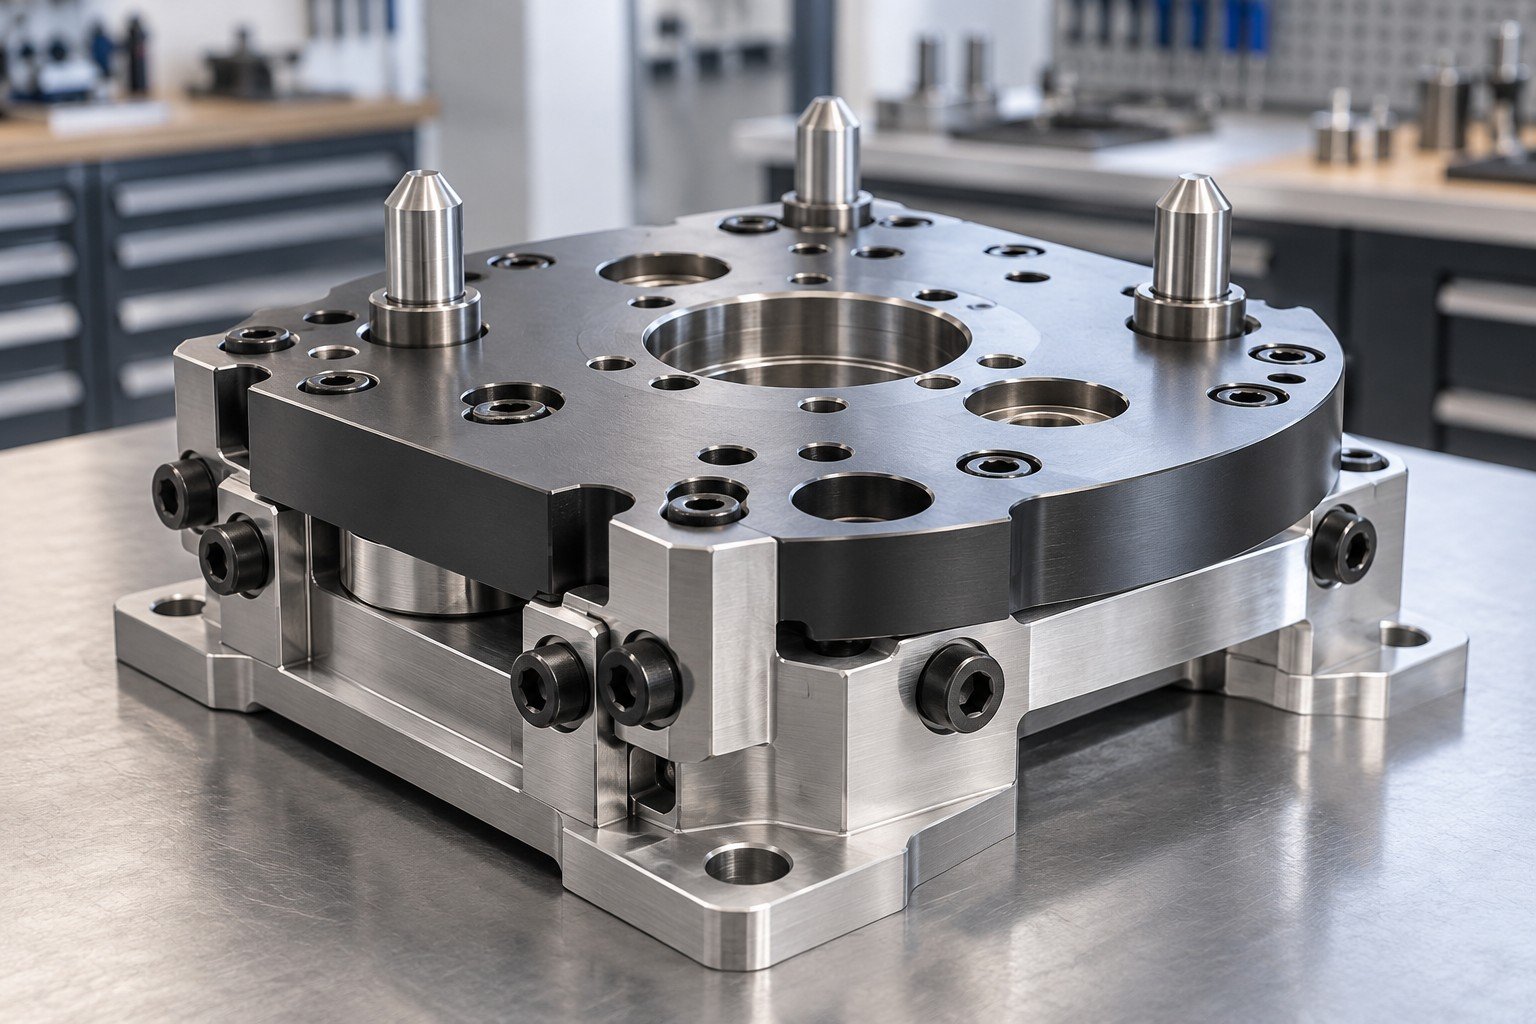
Mechanical locating and module handoffs for your next integration step.
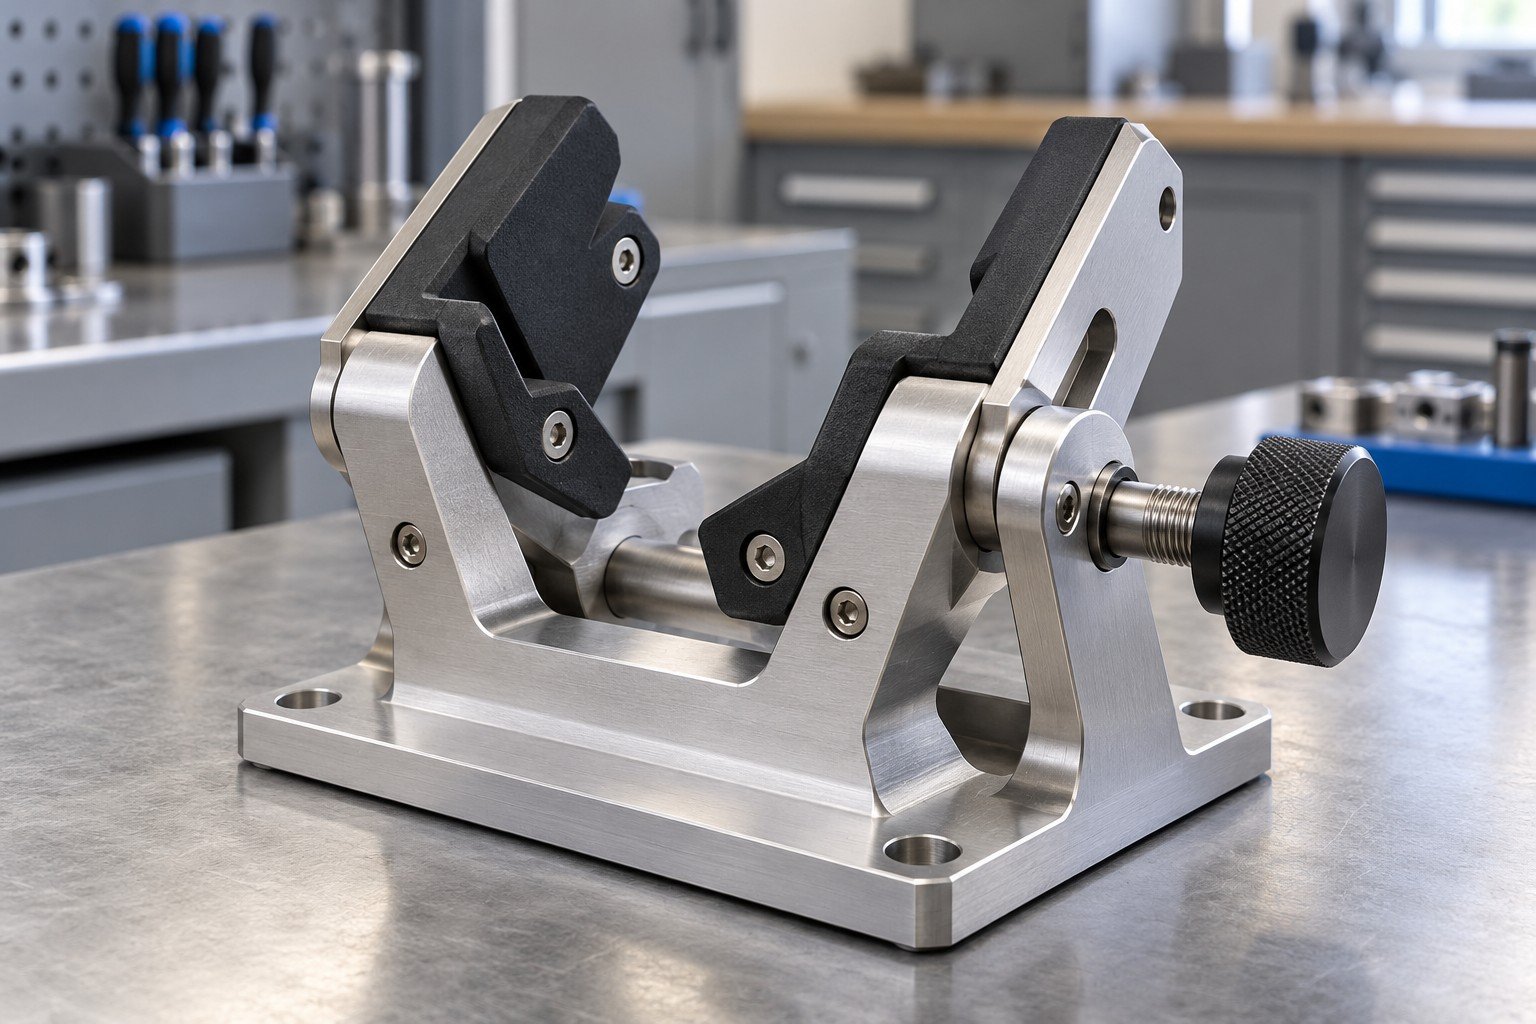
Adjustable mounts and guide modules with agreed fit and setup checks.
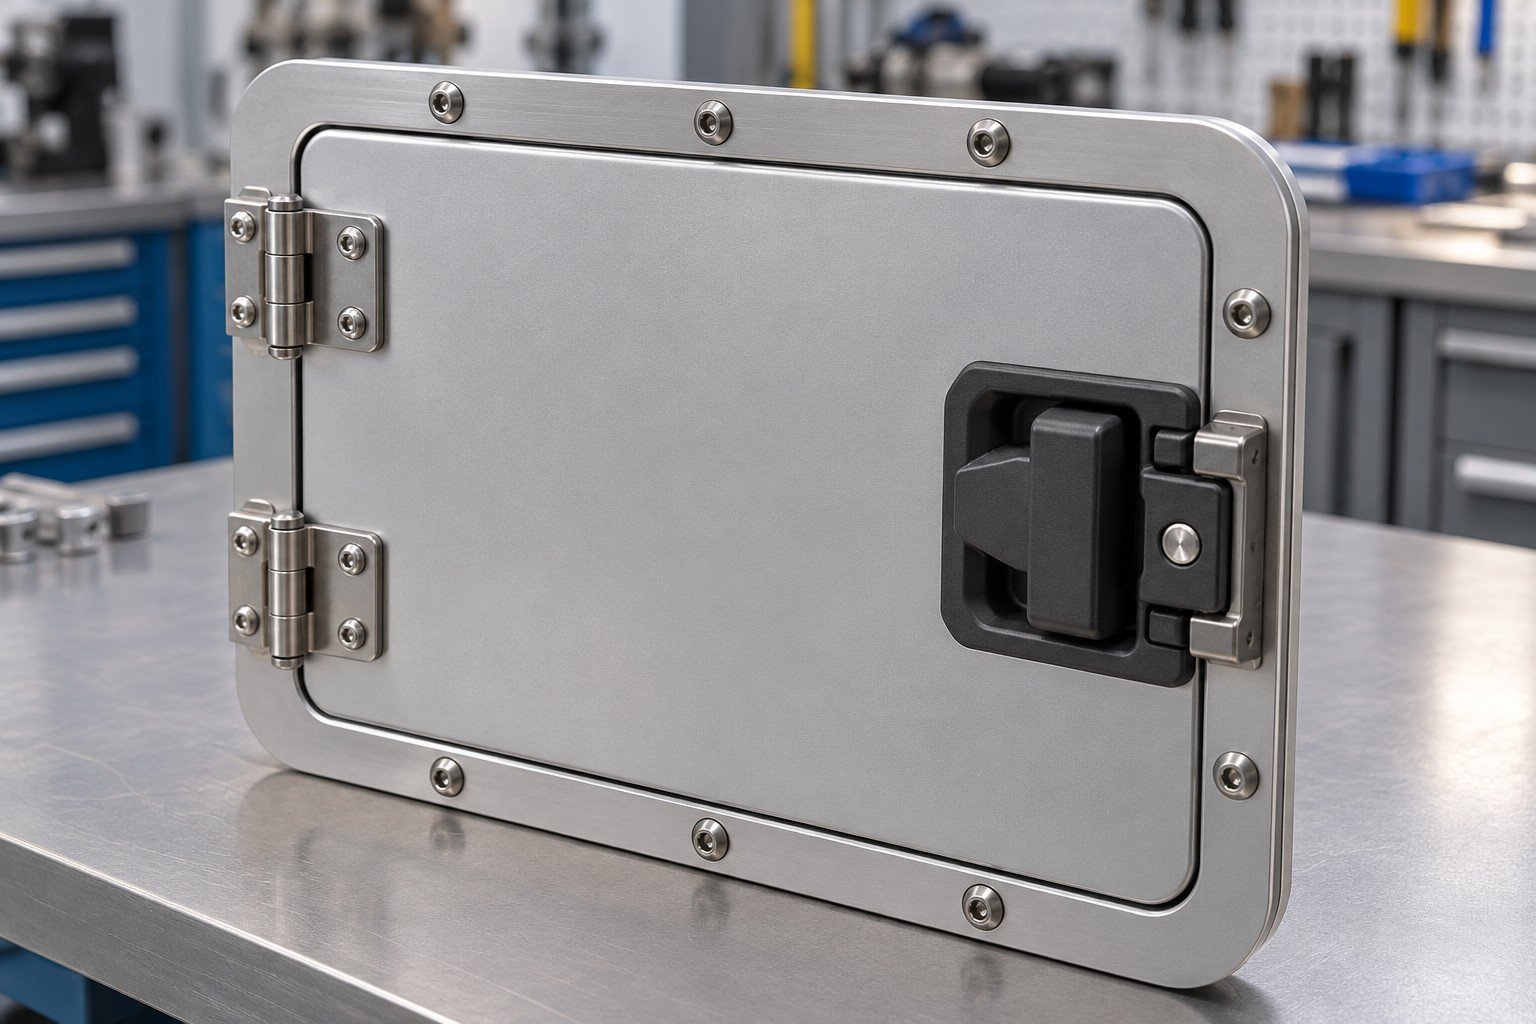
Housing, hinge, latch and loose-item scope stated before delivery.
Illustrative application concepts, not customer case studies. Suitability, manufacturing route and validation are confirmed for your project.
Keep your module boundary, supply decisions and receiving requirements connected to the responsible project team.
Resolve interface questions and record approved decisions.
Identify BOM responsibility, shortages and alternatives.
Agree module evidence and next-level validation ownership.
Confirm module identity, protection and receiving schedule.
Request an NDA before sharing confidential drawings. Identify missing inputs as scope-review items rather than leaving the module boundary undefined.
Aligned drawings, BOM, installed items and interfaces.
Fit, workmanship and specified module-check evidence.
Records, quantities, loose items, protection and delivery condition.
Subassembly traceability links the agreed unit or lot to its approved baseline and release evidence.
A subassembly joins several components into an intermediate module for a higher-level product. A bearing-supported roller cassette can be delivered as one module for installation in your machine. Define its interfaces and acceptance, not only its list of parts.
A component is an item within a product structure; a subassembly groups joined items at an intermediate level. These levels are relative to your BOM. Identify the module part number, included components and what your next assembly operation receives.
Module acceptance addresses the agreed subassembly condition. Final assembly integrates modules and other parts into the complete product, with its own acceptance and validation. Define who checks the mating interface and who validates complete-product performance.
An outsourced subassembly can consolidate component coordination and deliver a defined module to your production team. The benefit depends on supply ownership, stable interfaces, acceptance and logistics. Compare the total delivered scope; cost or lead-time savings are not automatic.
Cost depends on components, manufacturing, procurement, fixtures, setup, assembly, checks, records and packaging. Ask subassembly suppliers to quote the same controlled BOM and delivery boundary, separating nonrecurring work from repeat unit costs.
Provide the module and component drawings, controlled BOM, host interfaces, quantities and supply responsibility. Include module acceptance, required records, loose items, packaging and destination. Mark open design or test-development tasks explicitly.
Customer-supplied parts can enter a project review. Agree incoming checks, quantities, shortages, damaged items, permitted loss and return of unused stock. Receiving a shipment does not approve every item for assembly.
Ask each subassembly manufacturer for the same scope: installed items, sourcing, interface checks, records, change control and delivery condition. For contract subassembly, document acceptance and responsibility rather than relying on a general service label.
Subassembly minimum order and subassembly lead time depend on component availability, setup, fixtures, first-module approval, checks and scheduling. Send your trial and repeat demand plus required date for a project-specific quotation.
Yes, define both delivery states in the scope review. Sub assembly manufacturing joins the specified module components; a separate kit can contain loose mounting items for your next build. Custom subassembly acceptance and kit completeness need separate criteria.





