

Injection Molding
Tooling and molding for your repeat plastic parts.
From prototype to production, coordinated manufacturing solutions for your custom parts.
View All Services →
Precision parts for your tight tolerances and complex geometry.
Tooling and molding for your repeat plastic parts.

Metal casting options for your part and production volume.

Cutting, forming and welding for your fabricated parts.

Custom profiles for your section, length and finish requirements.

Finishes for your appearance, corrosion and wear requirements.

Sub-assemblies and final builds for your production program.

Production tooling built around your process and volume.

Prototype parts to check fit, function and design.
DFM, process planning and production support for your project.
Inspection, documentation, inventory and delivery planning for your program.
Choose air- or liquid-cooling components around your thermal and mechanical requirements.

Manufacturing support for your cold plates, manifolds and cooling assemblies.

Find components for your power electronics, energy, laser and telecom application.

Components for your electronic systems.
Start with your functional and quality requirements.
Build around your operating environment.
From prototype to production, review material performance, manufacturability and cost for your part.
Review grade, temper and finish for your metal parts.
 AluminumStrength, weight and machining›
 Stainless SteelCorrosion and finish requirements›
 Carbon & Alloy SteelDiscuss grade and heat treatment›
 Tool SteelDiscuss tooling and wear needs›
 TitaniumReview grade and part geometry›
 Copper & BrassDiscuss conductivity and machining›
Match your polymer to function, process and environment.
 ABSReview enclosure and molding needs›
 Polycarbonate (PC)Discuss clarity and impact needs›
 Nylon (PA)Review moisture and wear conditions›
 POM / AcetalReview fit and sliding features›
 PEEKDiscuss operating conditions›
 PTFEReview friction and chemical exposure›
 ULTEM / PEIDiscuss thermal and electrical needs›
Confirm grade availability and application requirements.
 Silicone / LSRDiscuss flexible component needs›
 TPU / TPEReview flexibility and processing›
 EPDMReview weathering and chemical exposure.›
 NBRReview oil and fuel exposure.›
 FKMReview temperature and chemical exposure.›
 G10 / FR4Review insulation and laminate needs›
 CompositesReview stiffness, weight and laminate.›Customer-Specified MaterialsConfirm your grade and requirements.›Other Specialty MaterialsDiscuss your application and grade.›
Practical guidance for your part geometry and material decisions.
Prepare your process, budget and sourcing questions.
Build your knowledge before production.
Learn who we are and how we operate.
Find our U.S. support team or start a conversation.
304 · UNS S30400 · EN 1.4301
Connect your material, manufacturing route and final surface requirements before you order.
For your 304 stainless steel machining project, identify the fits, formed features, welded joints and environment that control the finished component.
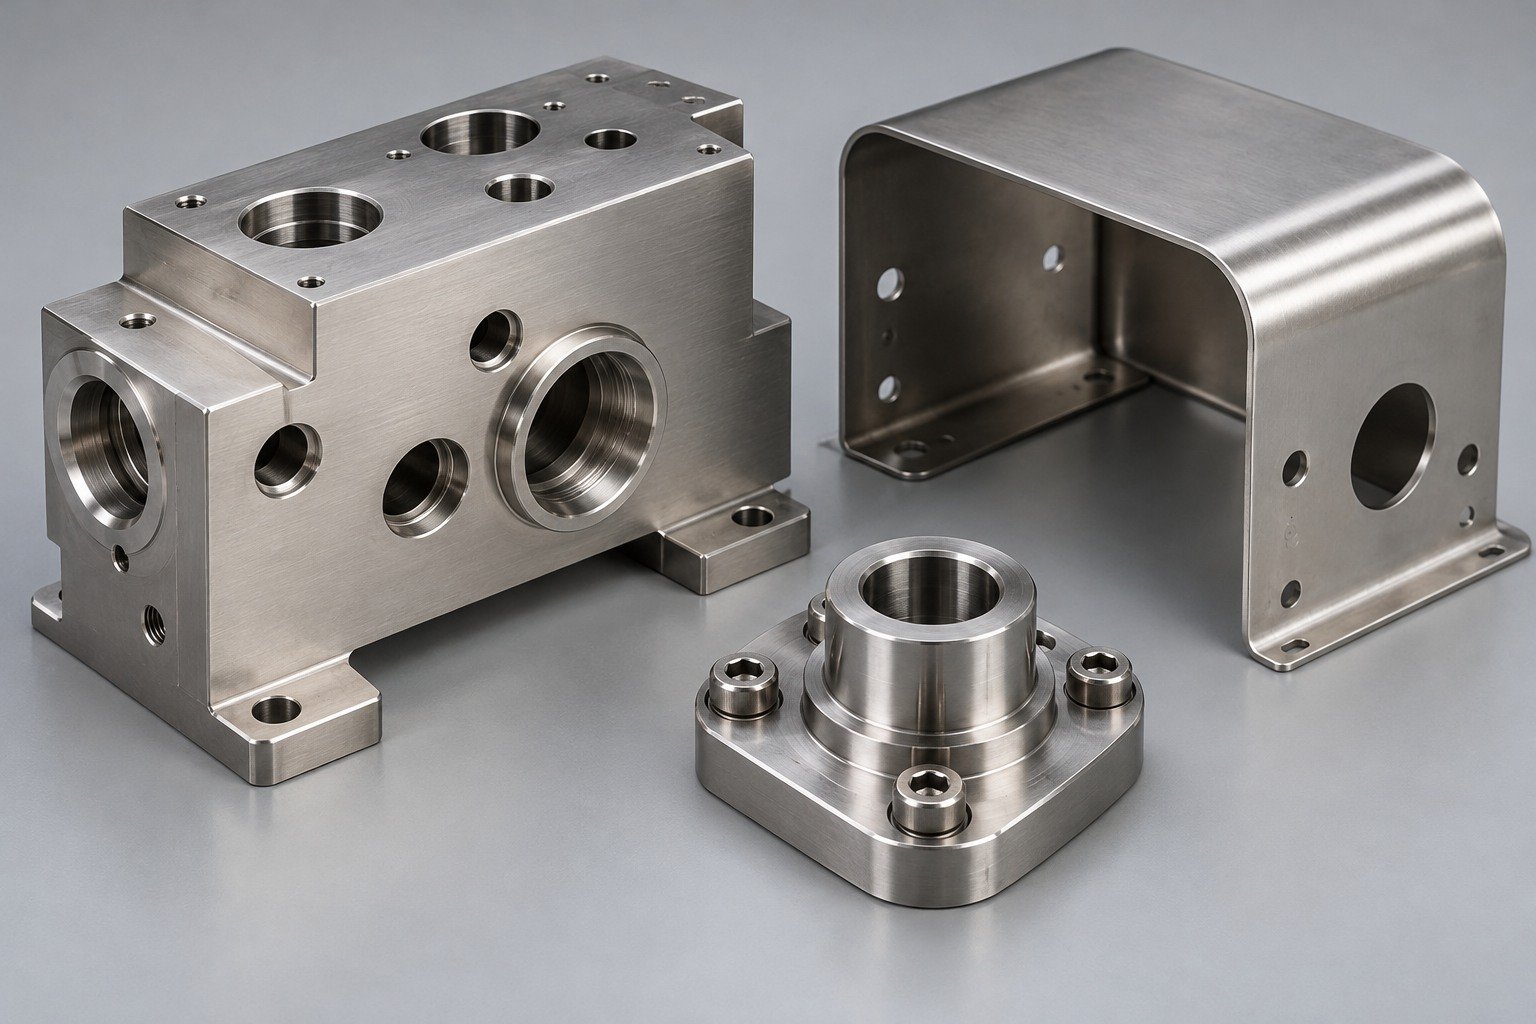
Keep 304 stainless, 304L and dual-certified stock distinct in your purchase requirement. Confirm the actual product standard.
Relate material removal, forming and joining to the same finished drawing. A stock description alone does not define a part.
State the inspection condition, appearance, cleanliness and any evidence your application requires.
Stainless steel 304 is an austenitic chromium-nickel material. Search names such as SS 304 help you find the family; your controlled drawing should retain the exact grade and specification.
| Designation | Your order check |
|---|---|
| 304 · UNS S30400 | EN 1.4301 / X5CrNi18-10 is a common European correspondence. |
| 304L · UNS S30403 | EN 1.4307 / X2CrNi18-9 identifies a low-carbon alternative; specify it when required. |
| 304 stainless steel ASTM A240 | Confirm the applicable flat-product specification, revision, thickness and condition; do not apply a sheet standard to every stock form. |
Names aid navigation; they are not blanket substitution approval. Stainless Steel Material Guide →
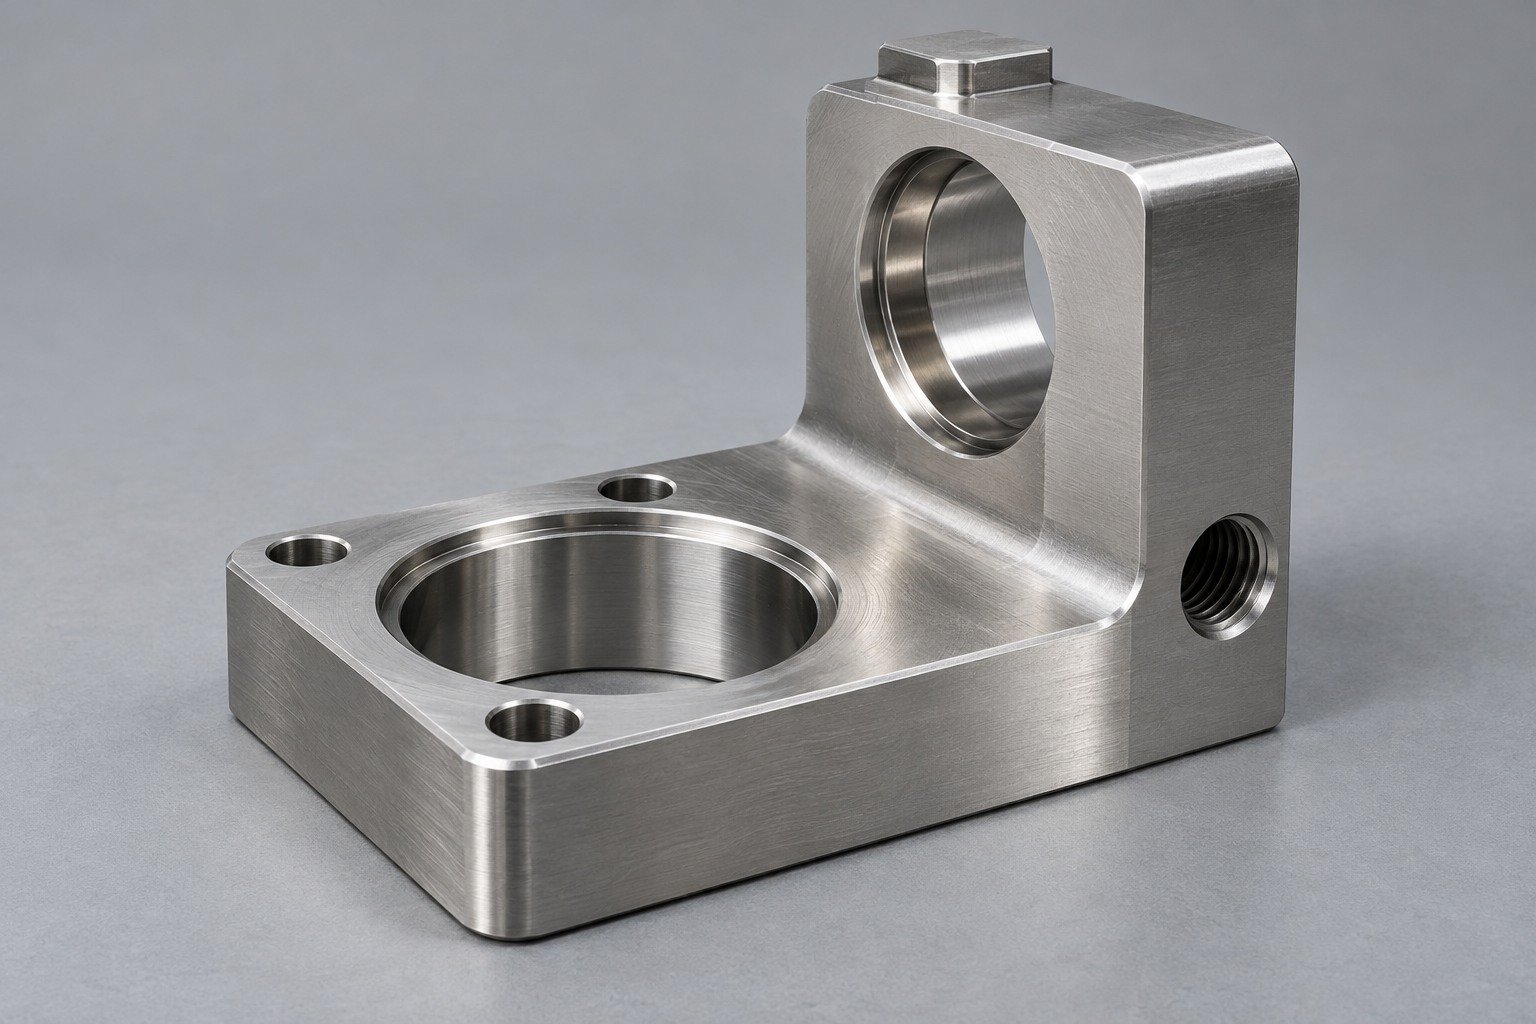
Read 304 stainless steel properties with the product form, standard and delivery condition. This selected 304 stainless steel composition comparison highlights the supplier's typical carbon difference.
Outokumpu Core reference · mass % · supplier typical values
Core 304 / 4301| Selected reference | C · mass % | Cr · mass % | Ni · mass % |
|---|---|---|---|
| Core 304 / 4301 | 0.04 | 18.1 | 8.1 |
| Core 304L / 4307 | 0.02 | 18.1 | 8.1 |
The cited values are selected typical chemistry from Outokumpu, not a complete specification or LK test report. Elements omitted from this comparison must still meet your controlled material requirement.
For your part, lower carbon is a selection input where welding-related material behavior matters. It does not remove the need to review the joint, environment and final condition.
For 304 stainless steel sheet metal fabrication, define thickness, bend direction, holes near bends and the faces that remain visible. Keep protective film and grain direction in the fabrication plan.
For custom 304 stainless steel sheet metal parts, connect 304 stainless steel laser cutting and 304 stainless steel bending to the finished assembly dimensions.
For 304 stainless steel brackets and 304 stainless steel enclosures, identify mounting interfaces, hardware and cosmetic acceptance before the flat pattern is released.
Sheet Metal Fabrication →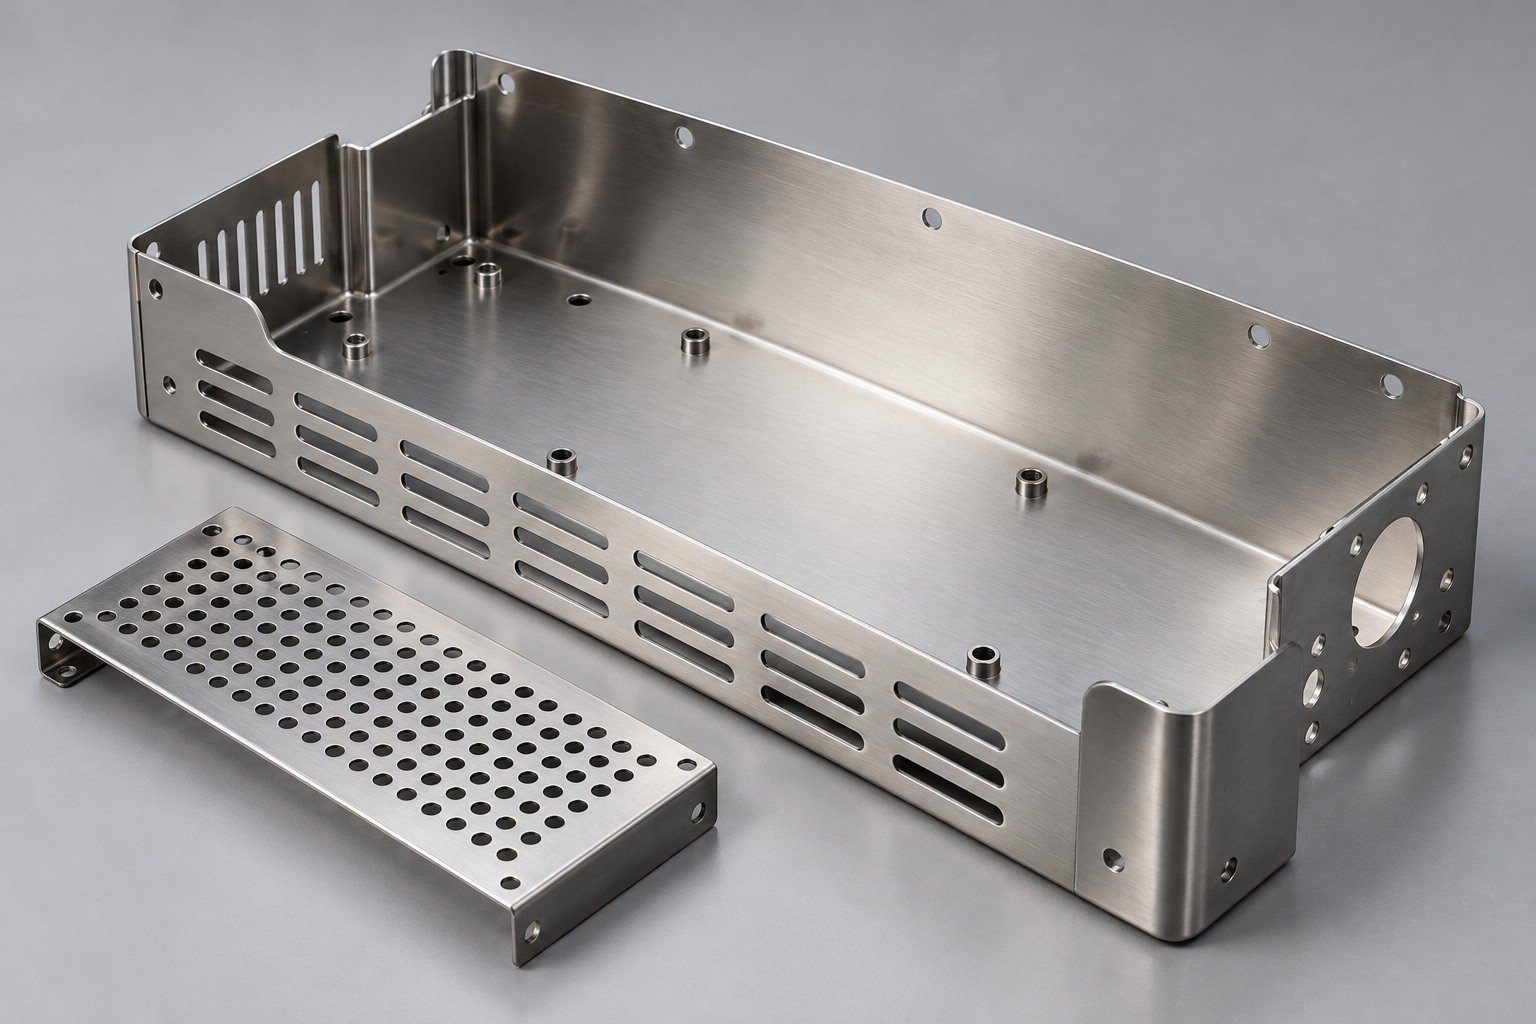
304 stainless steel machinability depends on condition, tooling, workholding and the actual cut. Describe the feature that must work rather than relying on one machinability score.
For 304 stainless steel milling, identify pocket depth, thin sections and datum access. For 304 stainless steel turning, connect bearing lands, shoulder lengths and bore relationships to inspection.
304 stainless steel turning services for 304 stainless steel spacers need a clear length, mating diameter and burr requirement.
CNC Milling → · CNC Turning →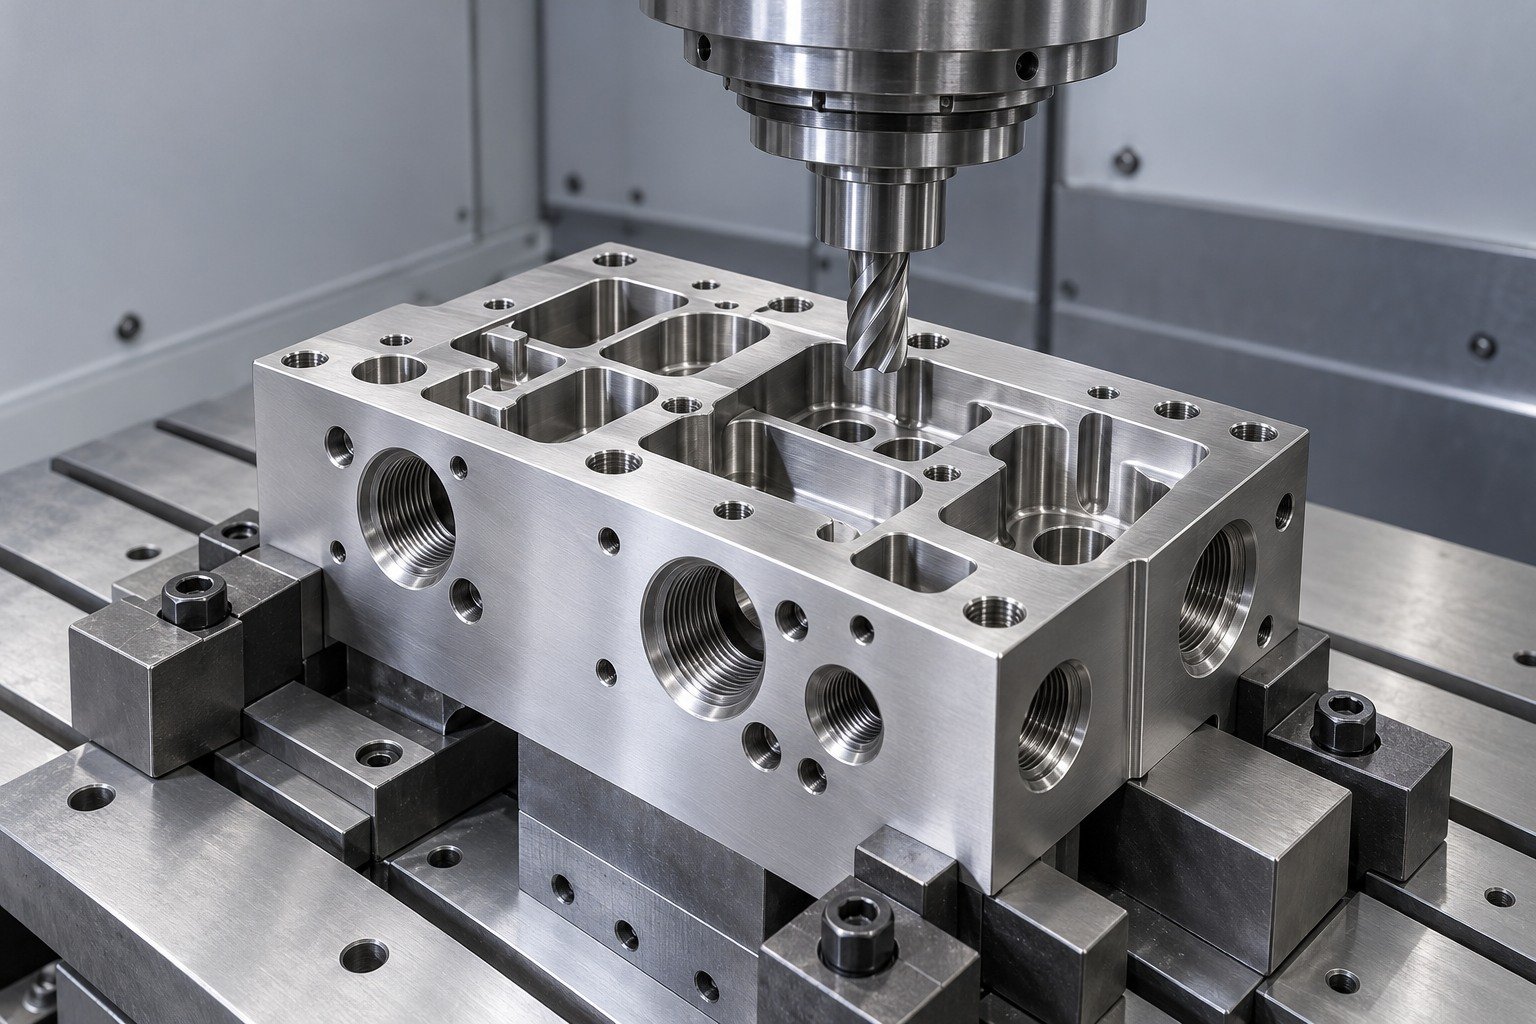
For 304 stainless steel welding, identify the joint, weld access, distortion-sensitive relationships and required final cleaning. Discuss whether the drawing should specify 304L.
For 304 stainless steel fabricated parts, agree the joining and machining sequence before setting final dimensional acceptance. State any procedure qualification or inspection requirement explicitly.
Welding & Fabrication →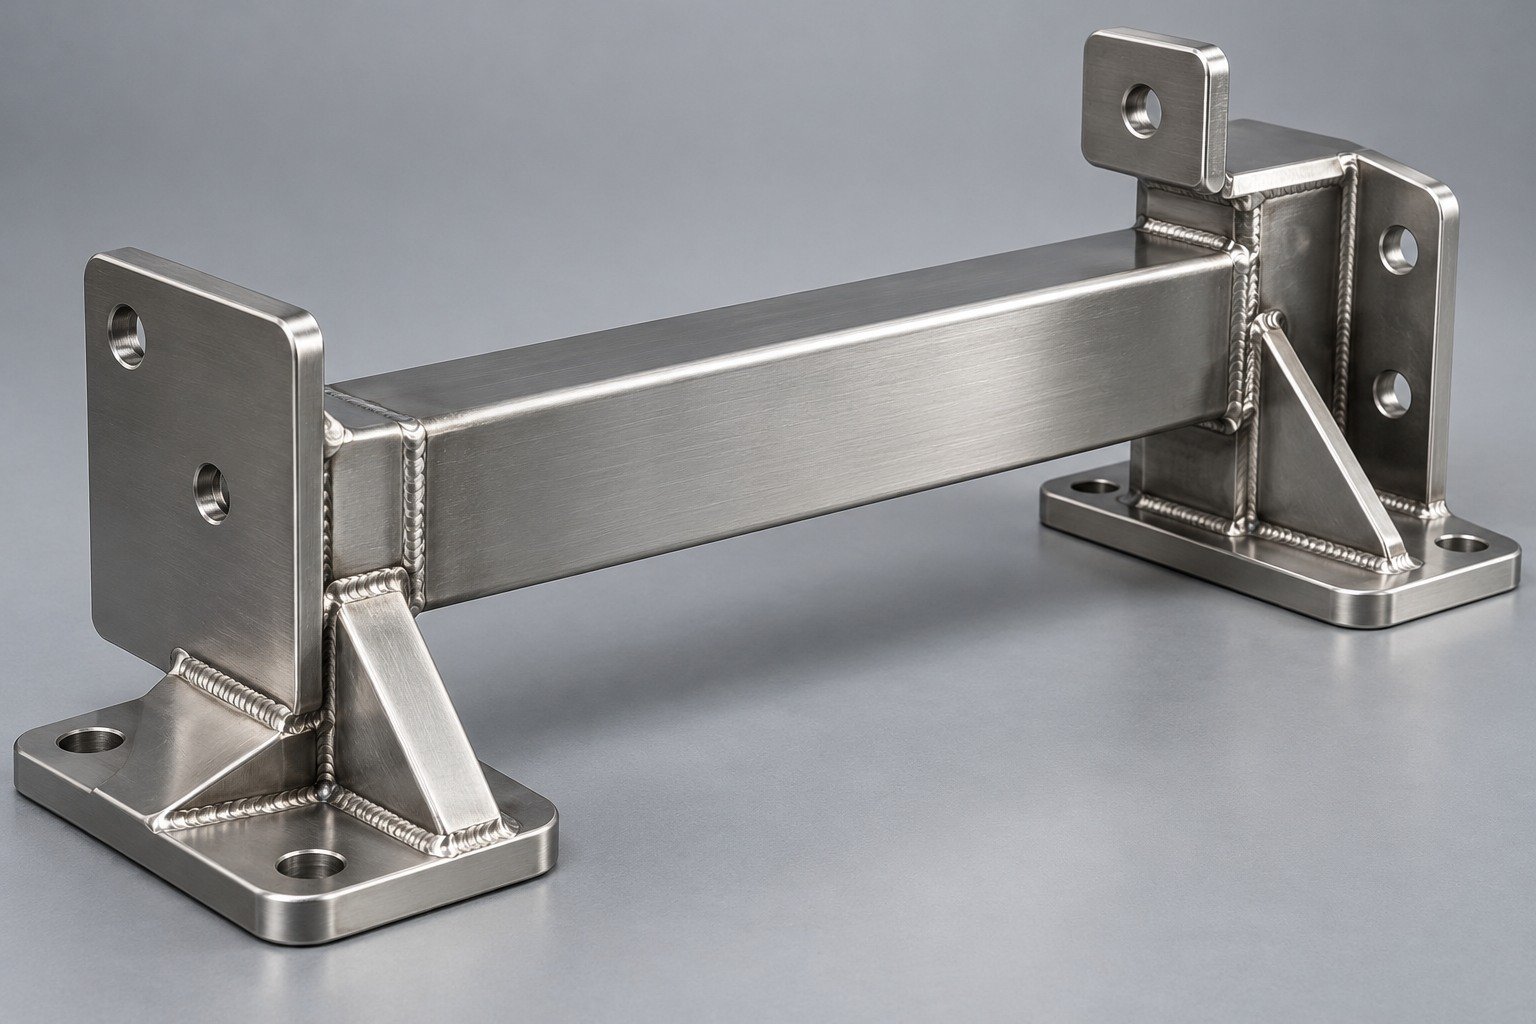
For 304 stainless steel polishing, define the faces, grain direction, reference sample and surfaces that must remain protected.
For 304 stainless steel passivation, agree cleaning, treatment compatibility and the verification scope for the actual component. A bright surface alone does not establish corrosion suitability.
For 304 stainless steel laser marking, identify the marking position, content, readability and any restrictions on functional or visible surfaces.
Brushing & Polishing → · Laser Marking Review →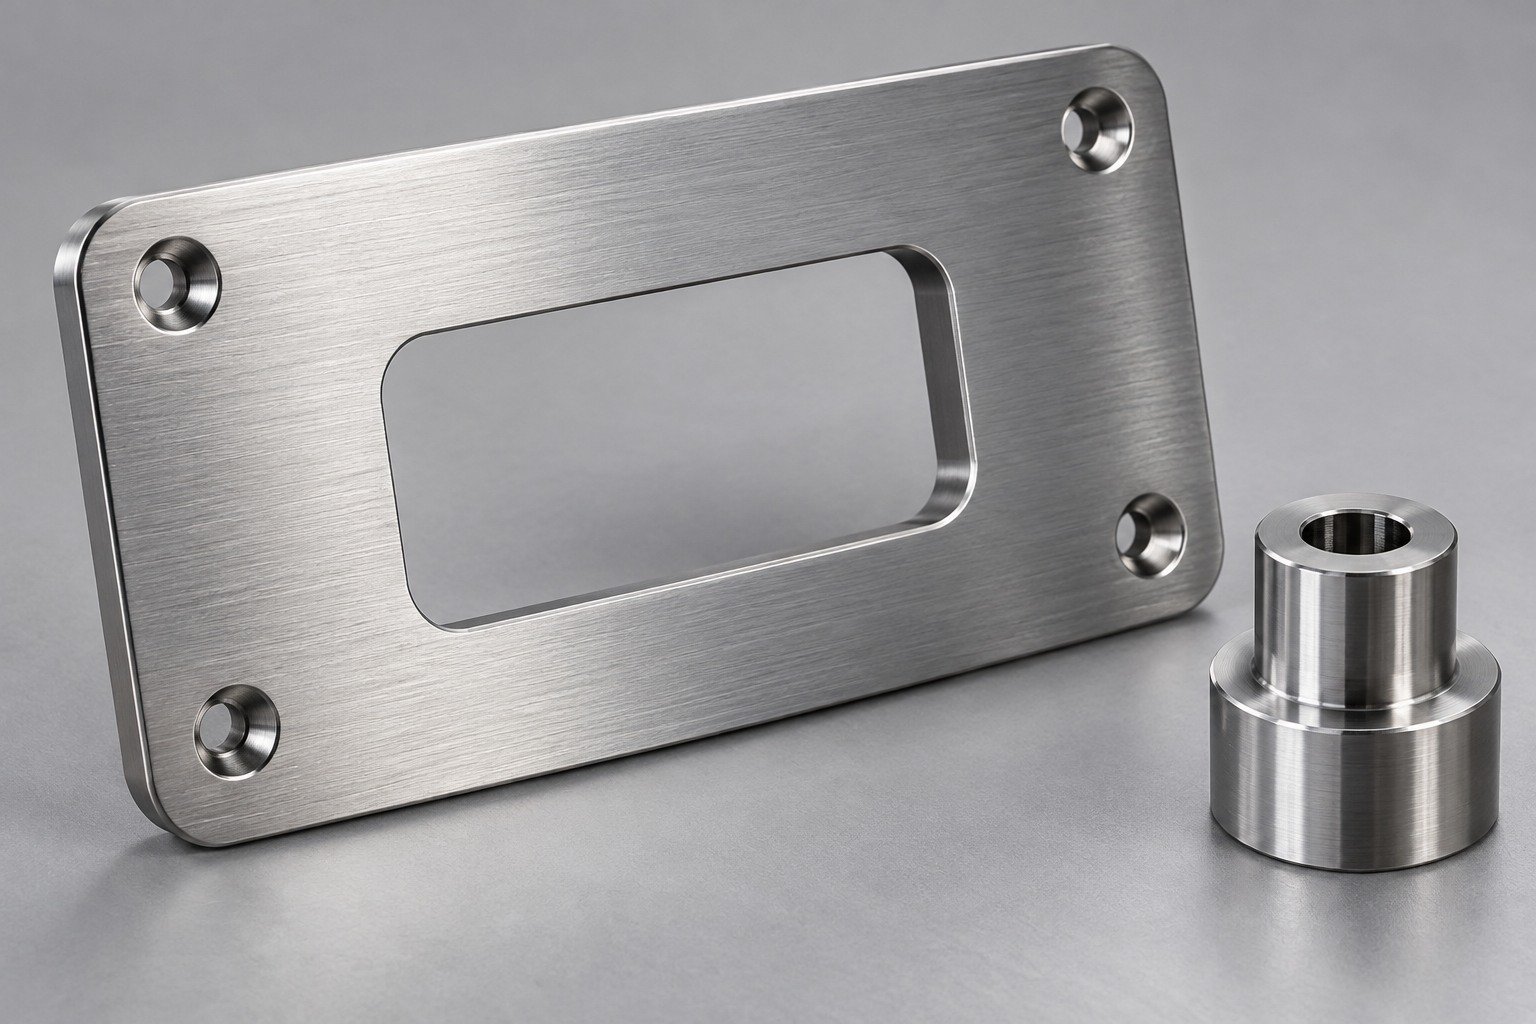
| Your decision | 304 / 304L | Alternative to review |
|---|---|---|
| Machined small features | Confirm chip control, condition and joining needs. | 303: review machining focus and exposure before any change. |
| Formed visible sheet | Confirm bends, grain and final environment. | 430: compare family, forming, finish and service suitability. |
| Fluid or chloride exposure | Specify the actual medium, temperature and cleaning. | 316 / 316L: review the exact application; no universal corrosion guarantee. |
| Welded assembly | Review low-carbon requirement and complete weld route. | 304L is not automatic approval for an unspecified welding procedure. |
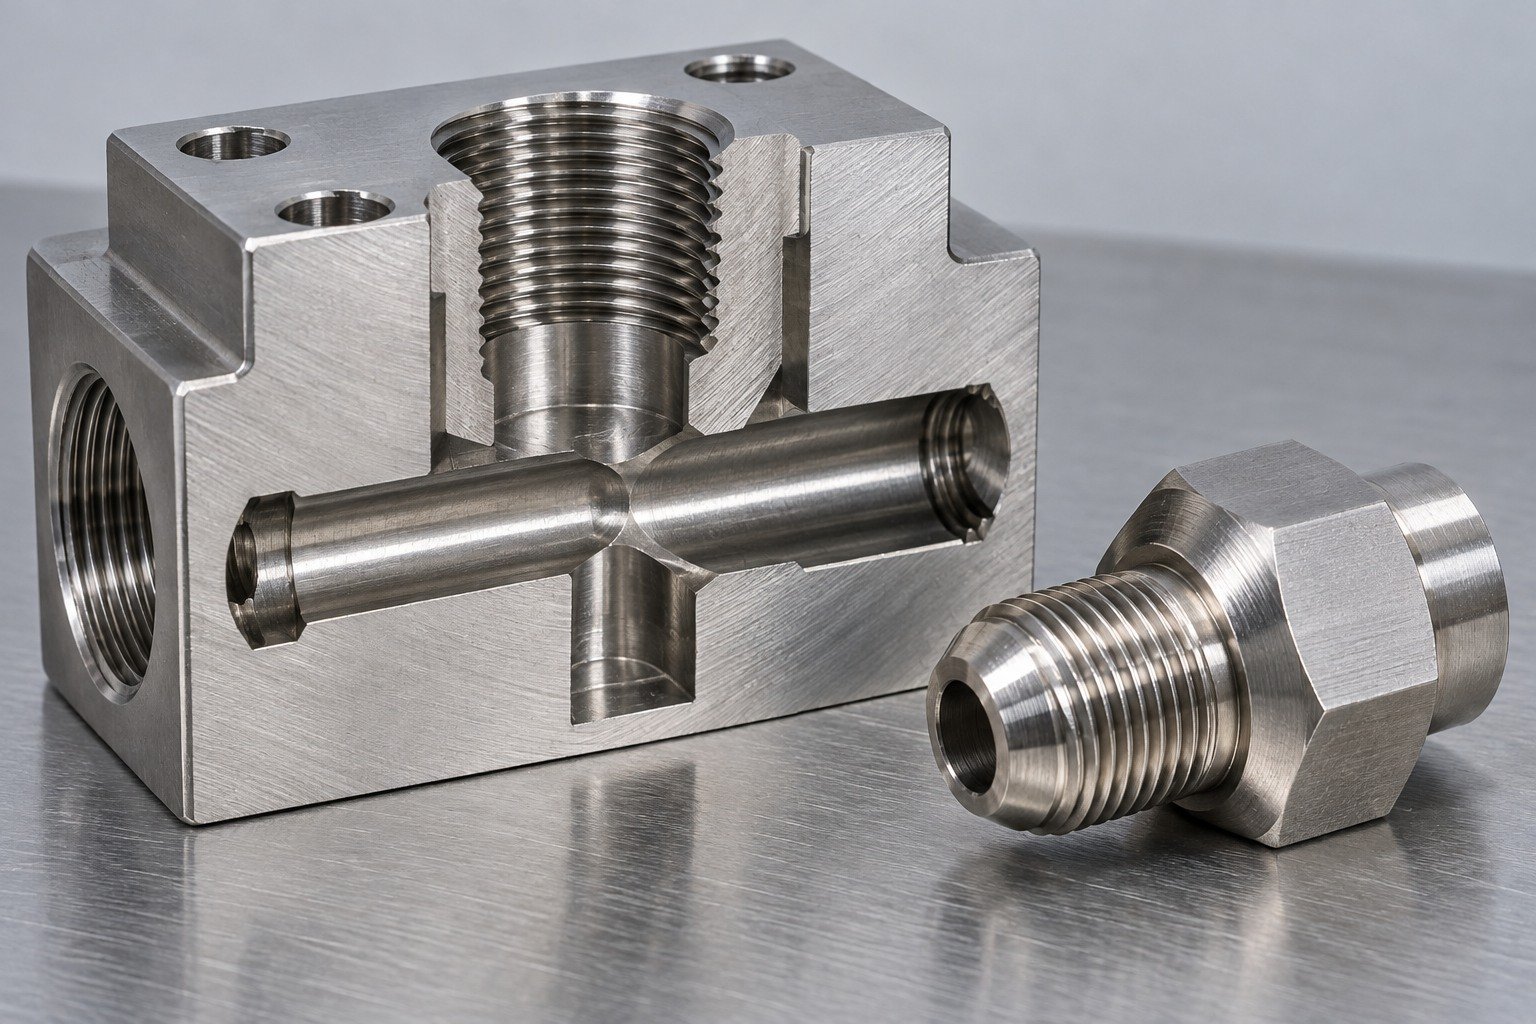
01 · Hole & thread access
Give the entry, intersection and useful depth for 304 stainless steel drilling and 304 stainless steel tapping. For 304 stainless steel threaded parts, specify the final functional fit.
Mark the thread standard, useful engagement, tool entry and internal burr-access route. Keep the supplied condition and inspection method with the drawing.
Outokumpu Core 304/4301 physical reference; this is a material stiffness value, not a thread-strength or tolerance guarantee.
Read the source and conditions →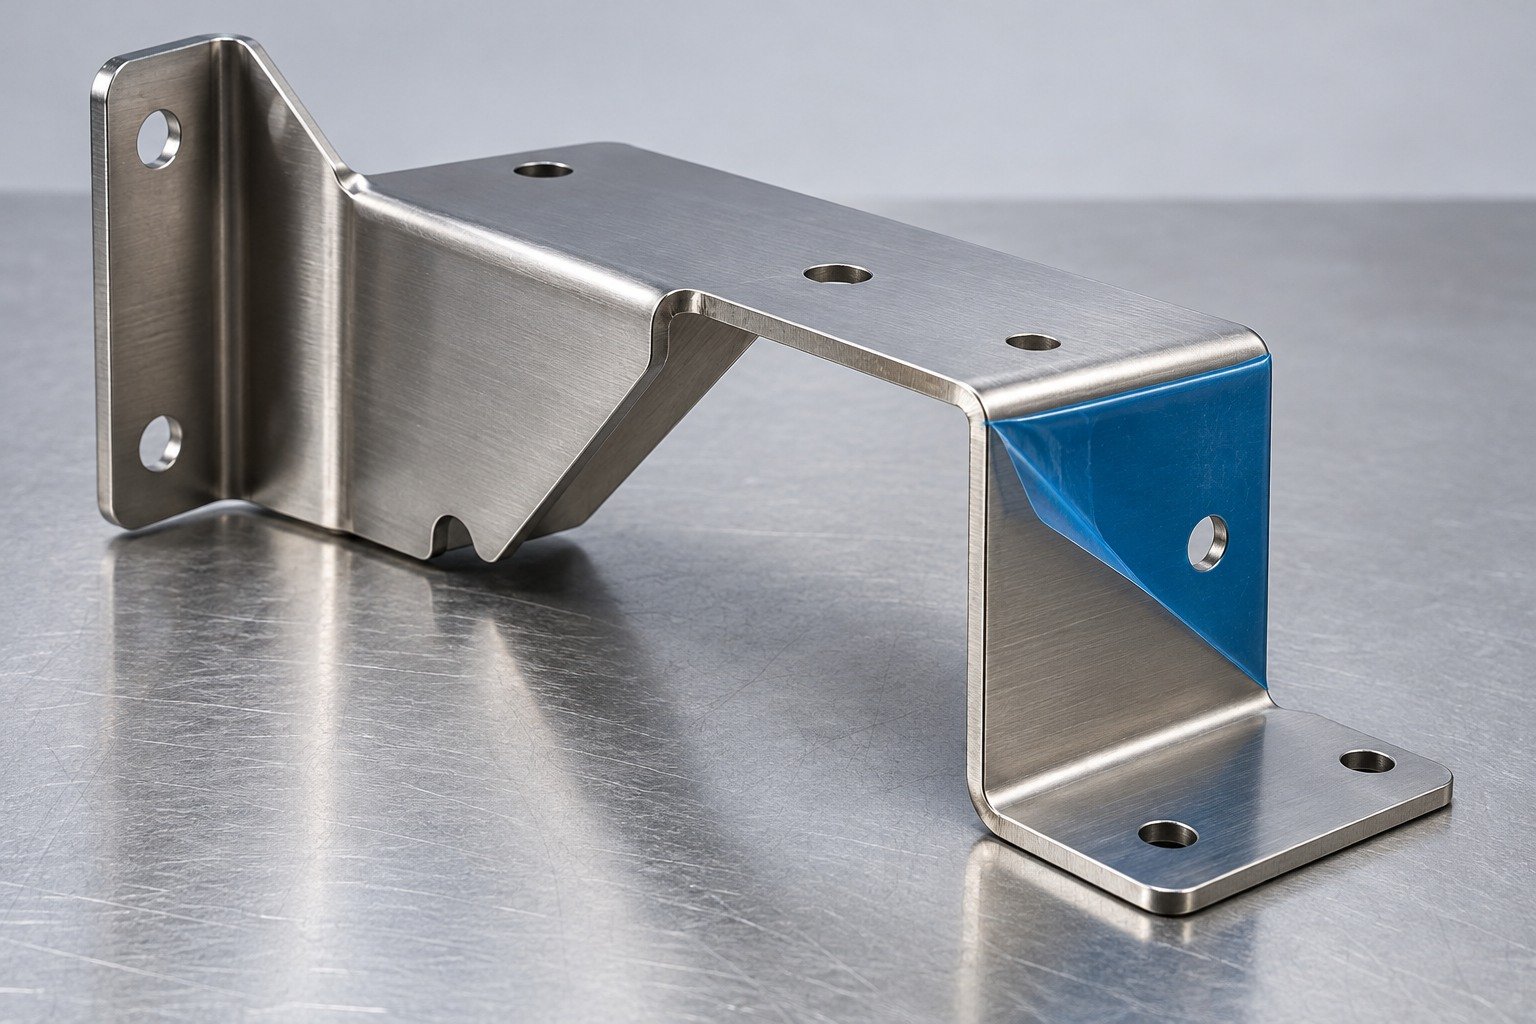
02 · Bend relationships
Connect the bend, hole pattern and visible face to the finished mounting condition. Discuss springback and tooling with the chosen material form.
Show sheet thickness, rolling direction and hole-to-bend relationships. Agree springback and the final formed inspection state for your geometry.
Core 304/4301, ASTM A240 strip t ≤ 5 mm in the cited Table 1. Tensile elongation does not prescribe a minimum bend radius.
Read the source and conditions →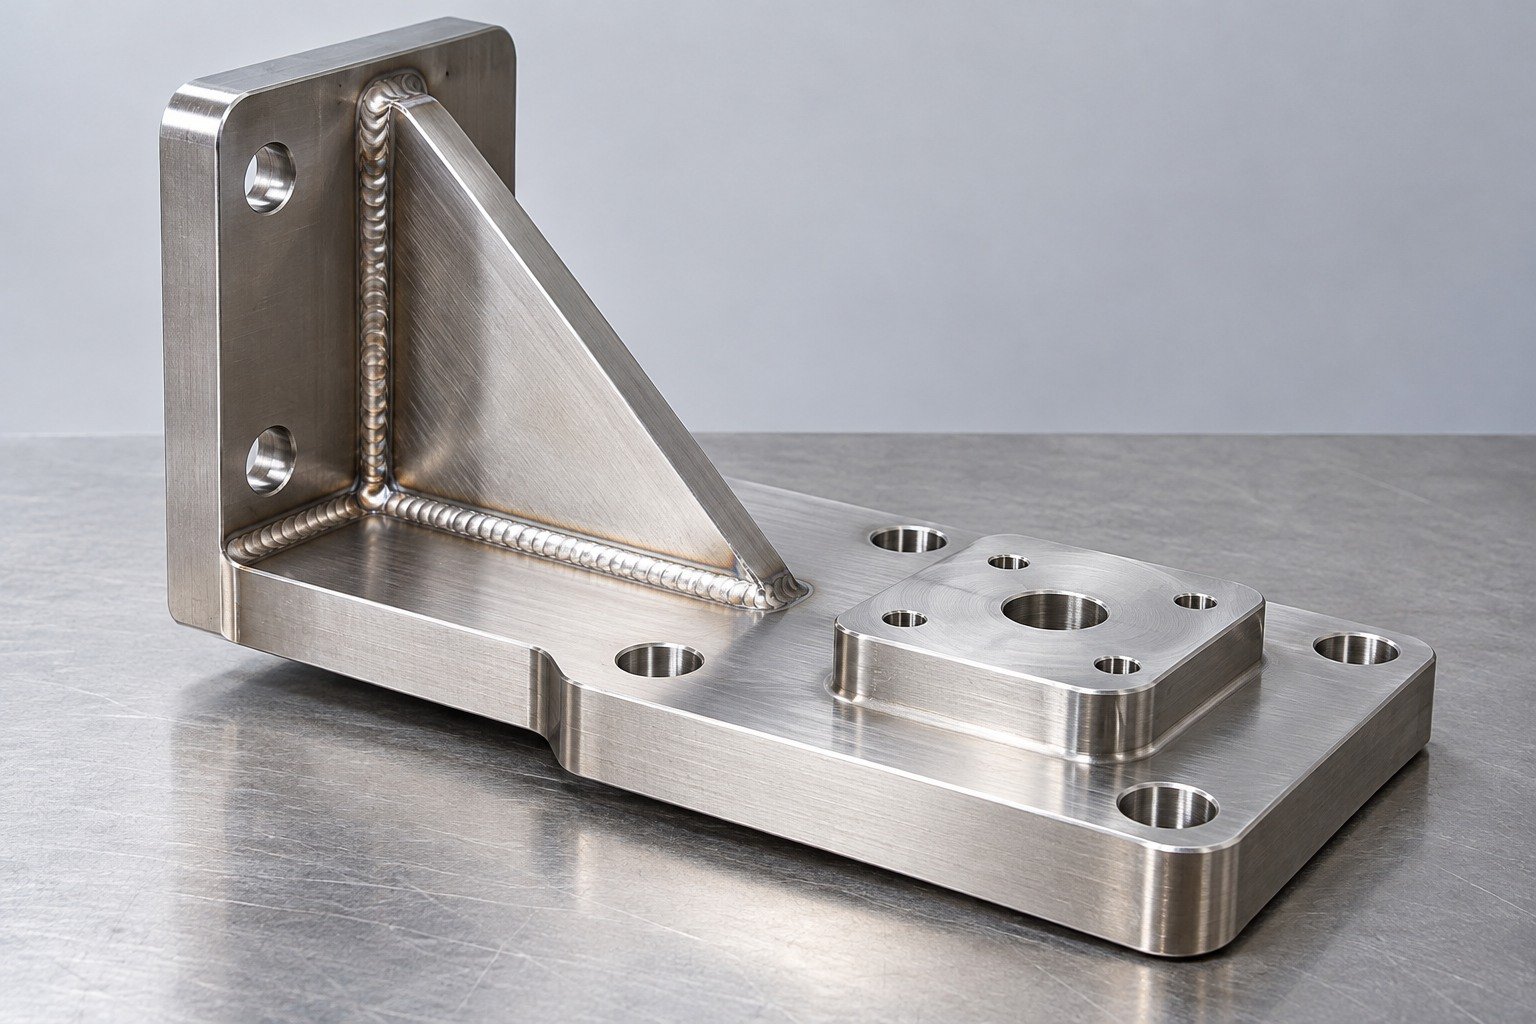
03 · Weld sequence
Define joint access, cleaning and inspection state before final machining. Identify the dimension that must hold after assembly.
Identify weld access, sequence, final machining and required cleaning. Discuss whether the drawing requires 304L before substituting material.
Supplier typical chemistry, not specification limits or a test of your lot. The low-carbon choice does not replace welding-procedure review.
Read the source and conditions →
04 · Appearance & handling
Mark cosmetic faces and grain direction. Keep accepted samples, protection and packaging tied to your release.
Identify grain direction, accepted sample, protected faces and packing. Keep the desired appearance separate from corrosion-suitability evidence.
Finish categories in the cited supplier discussion. They do not establish one roughness value; specify your required surface and acceptance.
Read the source and conditions →Exact grade, product standard and specified condition.
Datums, fits, threads and final inspection state.
Agreed appearance, cleaning and treatment records.
Revision, lot identification, exceptions and packing.
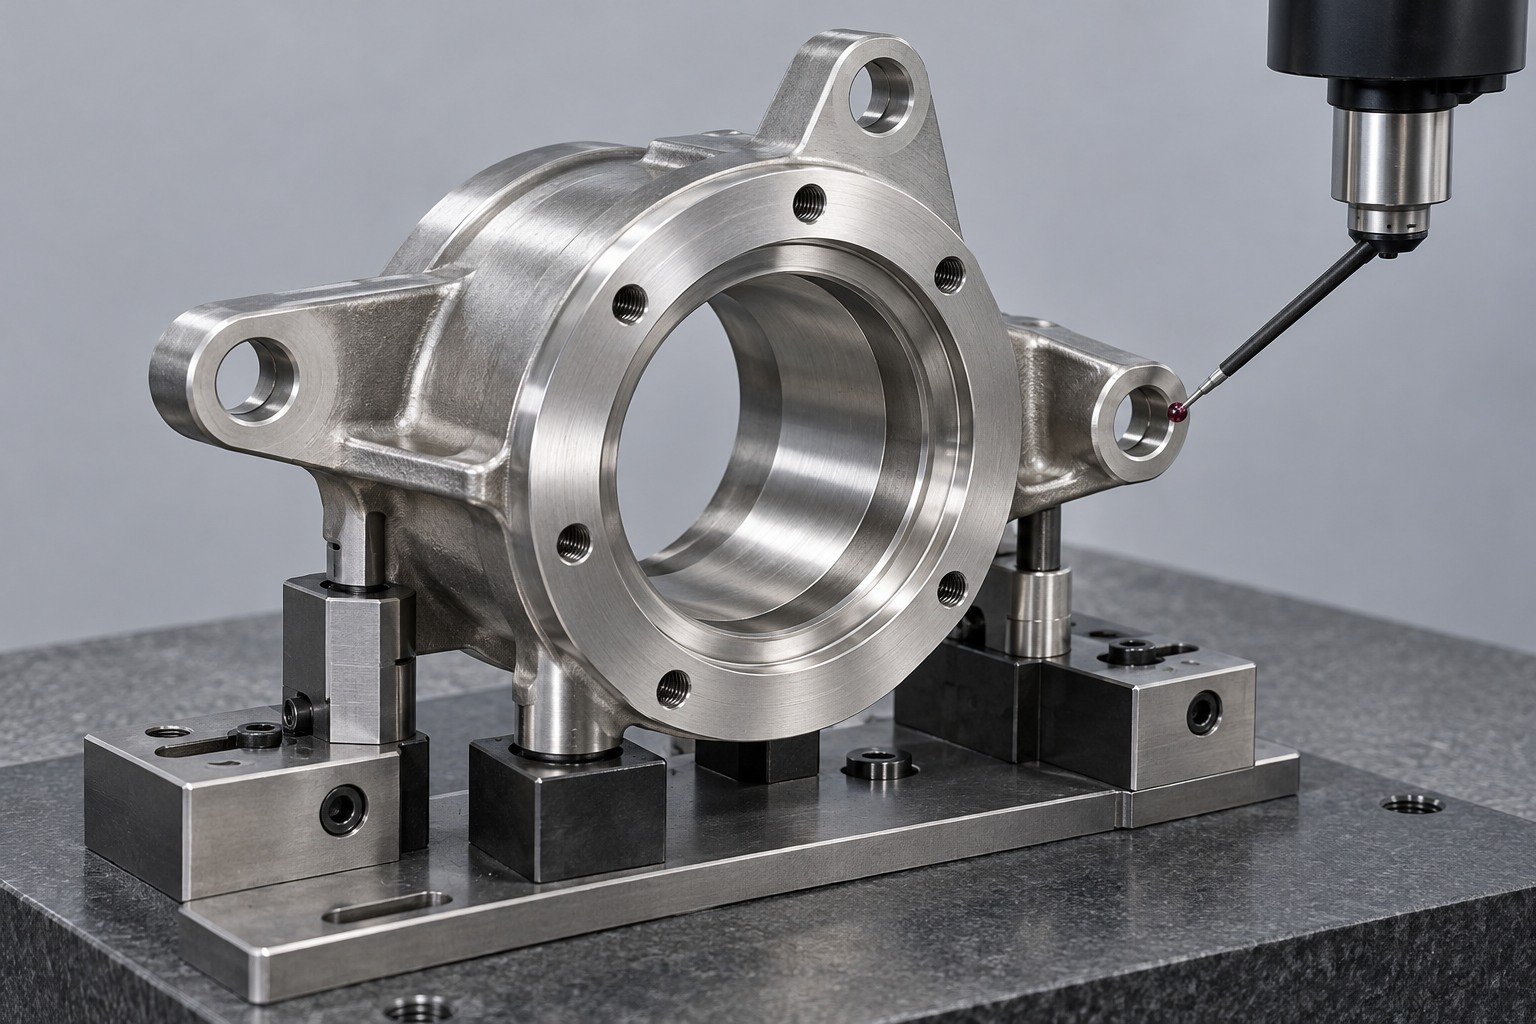
For your 304 stainless steel machining quote, compare the same finished scope. When reviewing a 304 stainless steel CNC parts manufacturer, connect the route and records to your drawing.
Grade, stock form, thickness and delivery condition.
Pockets, holes, threads and setup relationships.
Bends, joining, hardware and assembly sequence.
Grain, polishing, cleaning and marking.
Quantities, inspection records and packing.
For 304 stainless steel prototype machining, define what the sample must prove and how the intended production stock and condition will be represented.
Drawing revision, material, finish and acceptance.
Fit, appearance, assembly and inspection evidence.
Approved revision, change control and repeat inspection plan.
Specify the required grade and product standard. The low-carbon alternative matters to some welding-related selection decisions; confirm the full route and service requirement before changing material.
Review family, forming, joining, surface appearance and actual environment. Cost or a similar surface appearance alone does not establish interchangeability.
Do not use a magnet alone to accept the grade. Product condition and processing can affect the response; use the agreed material identity records.
It can corrode under unsuitable exposure or surface contamination. State the fluid, temperature, cleaning and retained moisture conditions for selection review.
Review the joint and qualified procedure requirements, distortion, cleaning and final acceptance. Confirm whether 304L is required for your application.
Specify the cleaning and passivation requirement, compatibility and evidence scope for your actual component before ordering.
Consider equipment brackets, enclosures, spacers and machined or fabricated components where the specified grade and environment suit the design. A material name is not an application certification.
Share the drawing, material form, quantity, fabrication, finish and evidence requirements. Compare the same finished-part scope rather than stock price alone.
For 304 stainless steel machining services, define the 304 stainless steel machined parts and any associated forming or joining as one controlled scope.
Revision and CAD when available.
Grade, standard, form and condition.
Fits, threads, bends and joints.
Prototype, repeat and release pattern.
Grain, finish, cleaning and marks.
Material identity, inspection and packing.





