

Injection Molding
Tooling and molding for your repeat plastic parts.
From prototype to production, coordinated manufacturing solutions for your custom parts.
View All Services →
Precision parts for your tight tolerances and complex geometry.
Tooling and molding for your repeat plastic parts.

Metal casting options for your part and production volume.

Cutting, forming and welding for your fabricated parts.

Custom profiles for your section, length and finish requirements.

Finishes for your appearance, corrosion and wear requirements.

Sub-assemblies and final builds for your production program.

Production tooling built around your process and volume.

Prototype parts to check fit, function and design.
DFM, process planning and production support for your project.
Inspection, documentation, inventory and delivery planning for your program.
Choose air- or liquid-cooling components around your thermal and mechanical requirements.

Manufacturing support for your cold plates, manifolds and cooling assemblies.

Find components for your power electronics, energy, laser and telecom application.

Components for your electronic systems.
Start with your functional and quality requirements.
Build around your operating environment.
From prototype to production, review material performance, manufacturability and cost for your part.
Review grade, temper and finish for your metal parts.
 AluminumStrength, weight and machining›
 Stainless SteelCorrosion and finish requirements›
 Carbon & Alloy SteelDiscuss grade and heat treatment›
 Tool SteelDiscuss tooling and wear needs›
 TitaniumReview grade and part geometry›
 Copper & Brass & BronzeDiscuss conductivity and machining›
Match your polymer to function, process and environment.
 ABSReview enclosure and molding needs›
 Polycarbonate (PC)Discuss clarity and impact needs›
 Nylon (PA)Review moisture and wear conditions›
 POM / AcetalReview fit and sliding features›
 PEEKDiscuss operating conditions›
 PTFEReview friction and chemical exposure›
 ULTEM / PEIDiscuss thermal and electrical needs›
Confirm grade availability and application requirements.
 Silicone / LSRDiscuss flexible component needs›
 TPU / TPEReview flexibility and processing›
 EPDMReview weathering and chemical exposure.›
 NBRReview oil and fuel exposure.›
 FKMReview temperature and chemical exposure.›
 G10 / FR4Review insulation and laminate needs›
 CompositesReview stiffness, weight and laminate.›Customer-Specified MaterialsConfirm your grade and requirements.›Other Specialty MaterialsDiscuss your application and grade.›
Practical guidance for your part geometry and material decisions.
Prepare your process, budget and sourcing questions.
Build your knowledge before production.
Learn who we are and how we operate.
Find our U.S. support team or start a conversation.
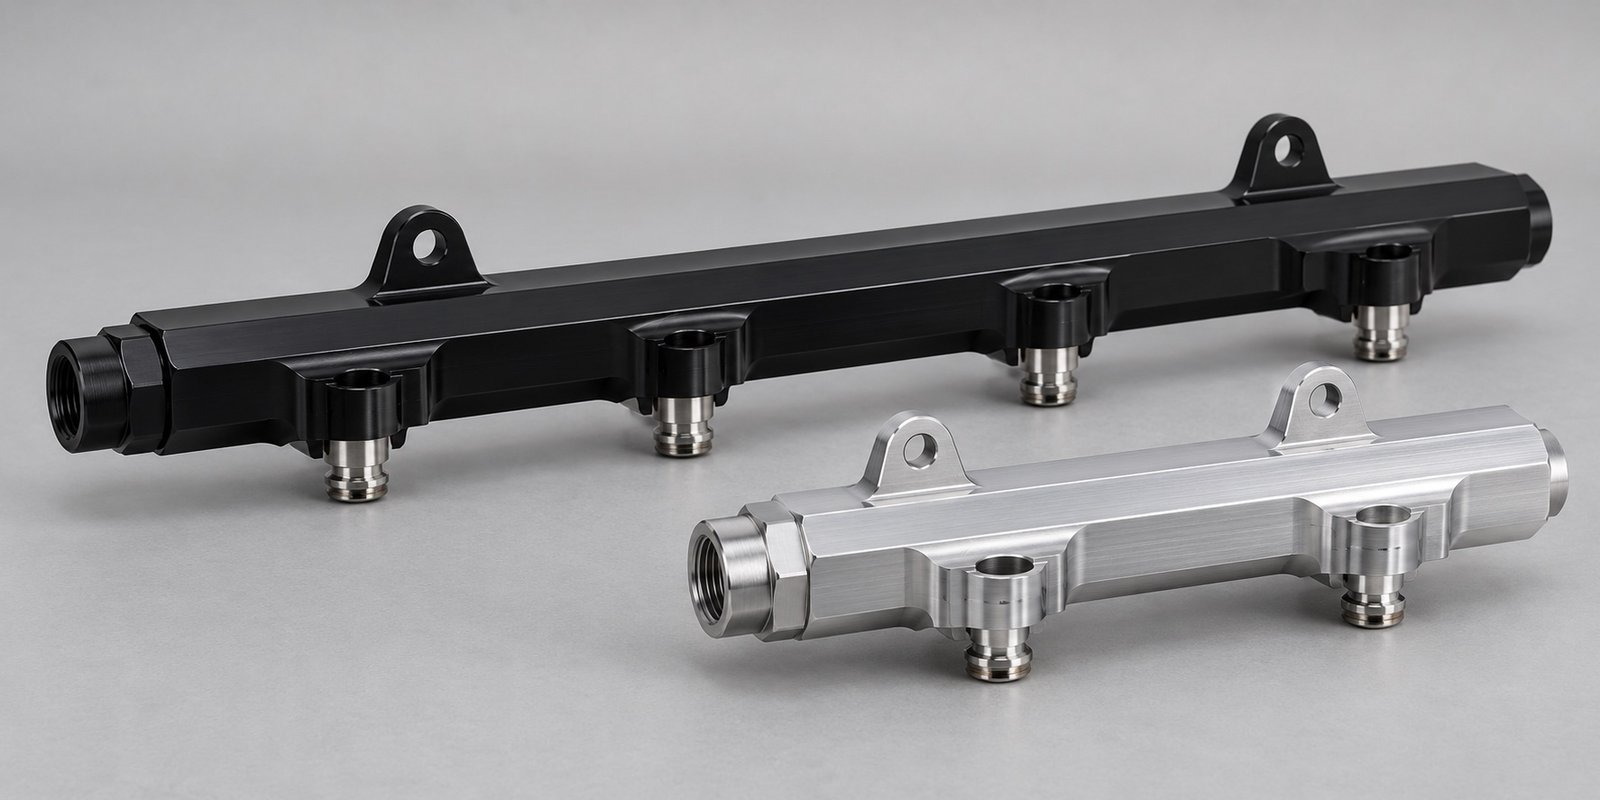
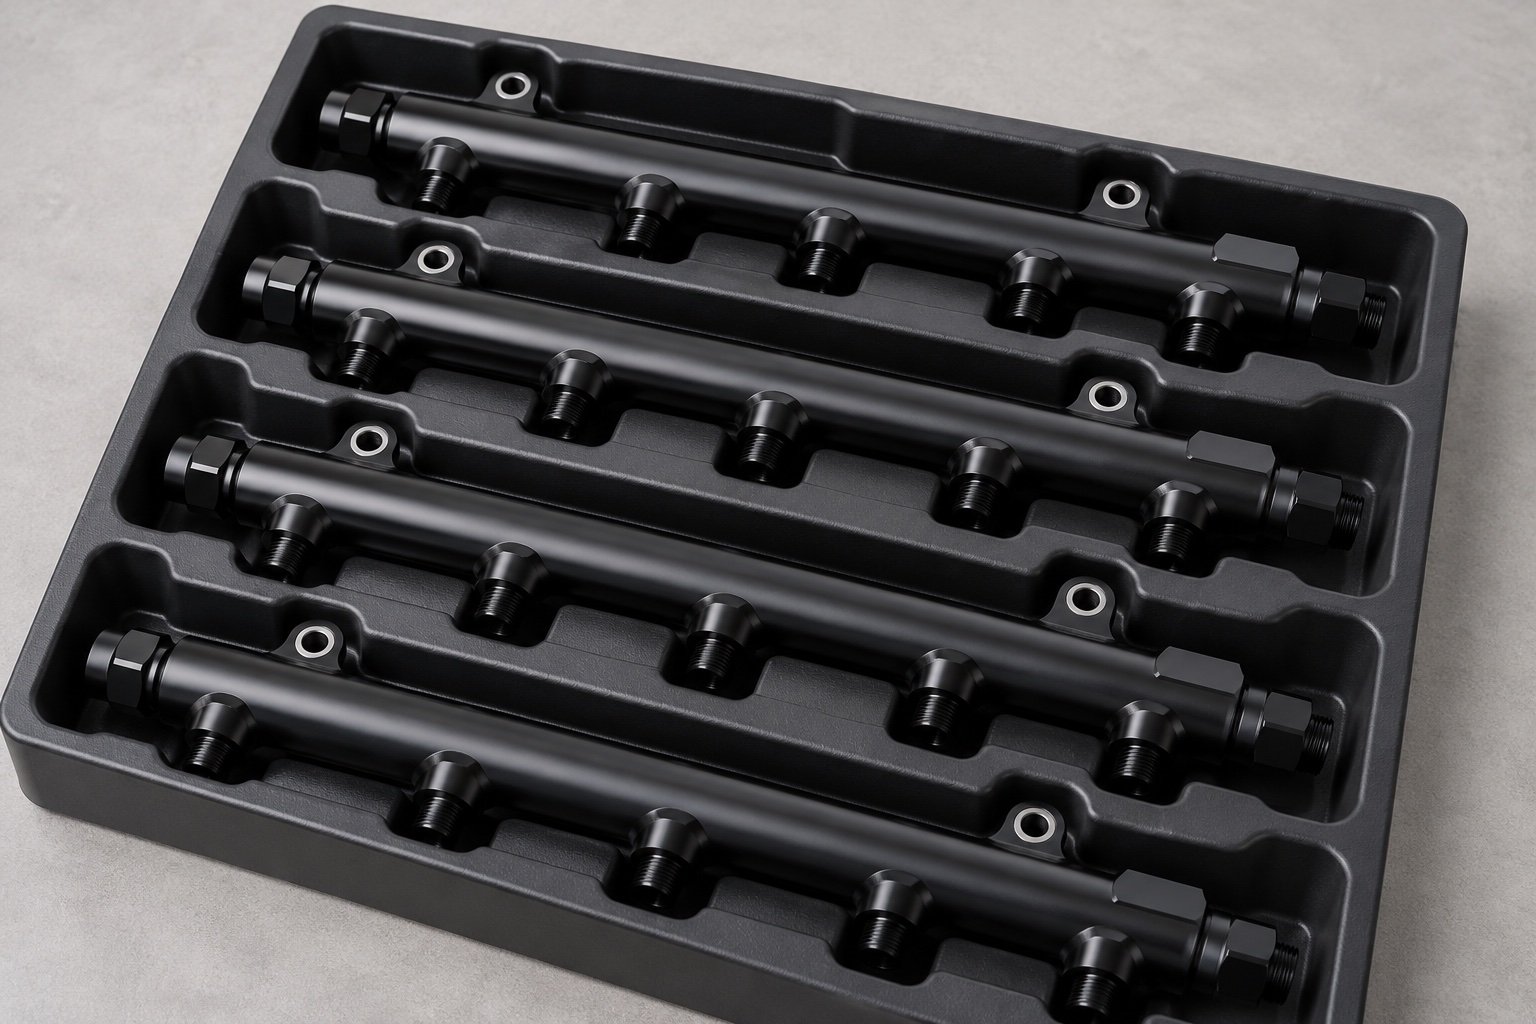
For your performance parts brand or engine development program, define injector spacing, sealing geometry and mounting height before your custom CNC fuel rails enter production. Send the drawing, injector reference and quantity plan so your quote addresses the interfaces that must fit together.
Bore, seal and spacing
Ports and mounting height
Specified alloy and masks
Agreed checks and records
Made to your approved drawing · Illustrative component concepts
Your injector and manifold references determine the layout; a vehicle name alone does not.
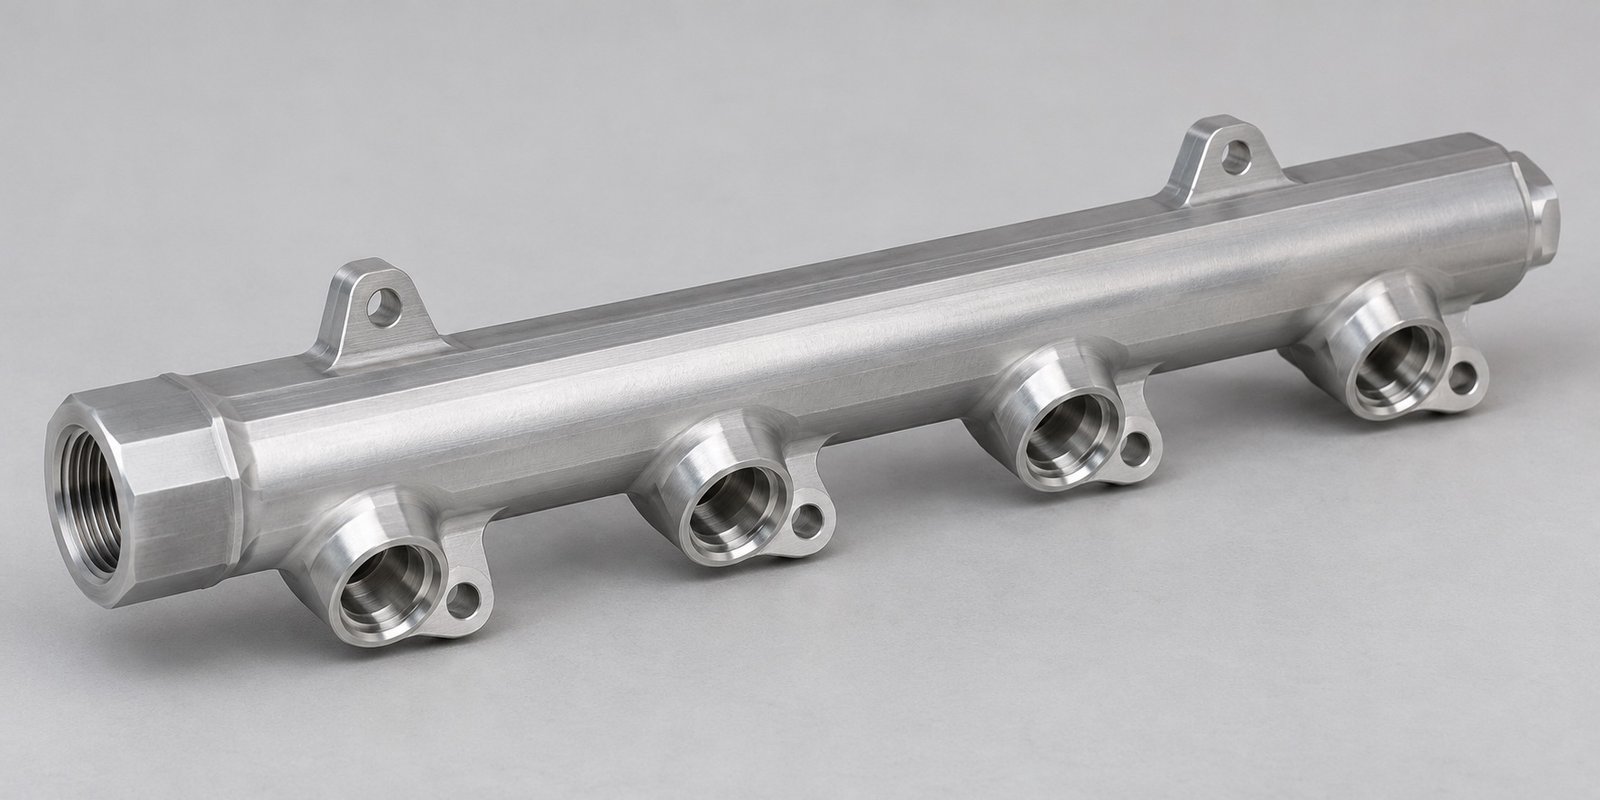
Define each injector center from a controlled datum and identify the longitudinal gallery.
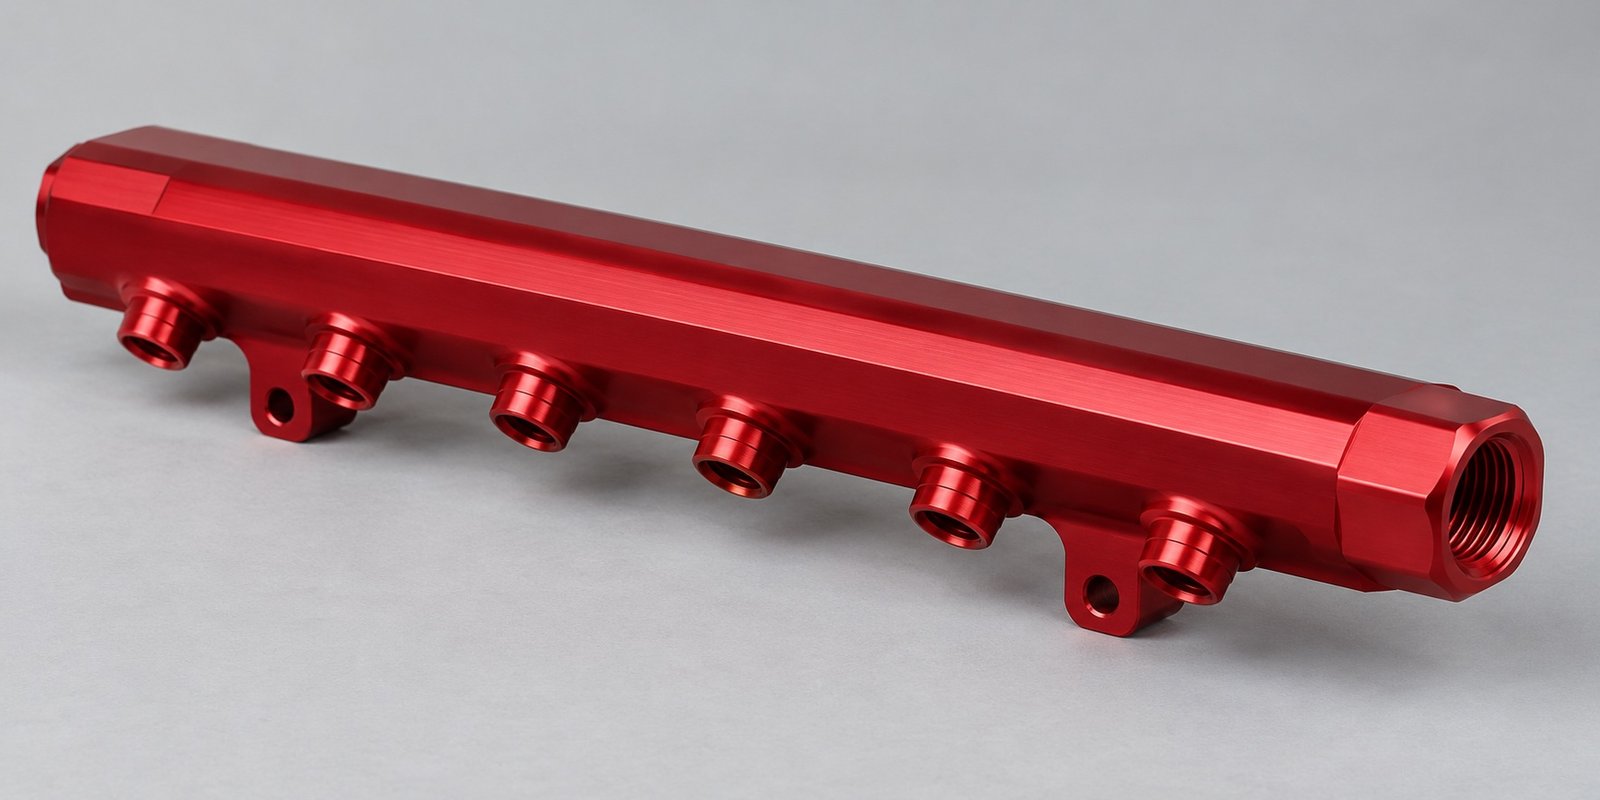
Identify feed, return and sensor connections with the complete thread and sealing specification.
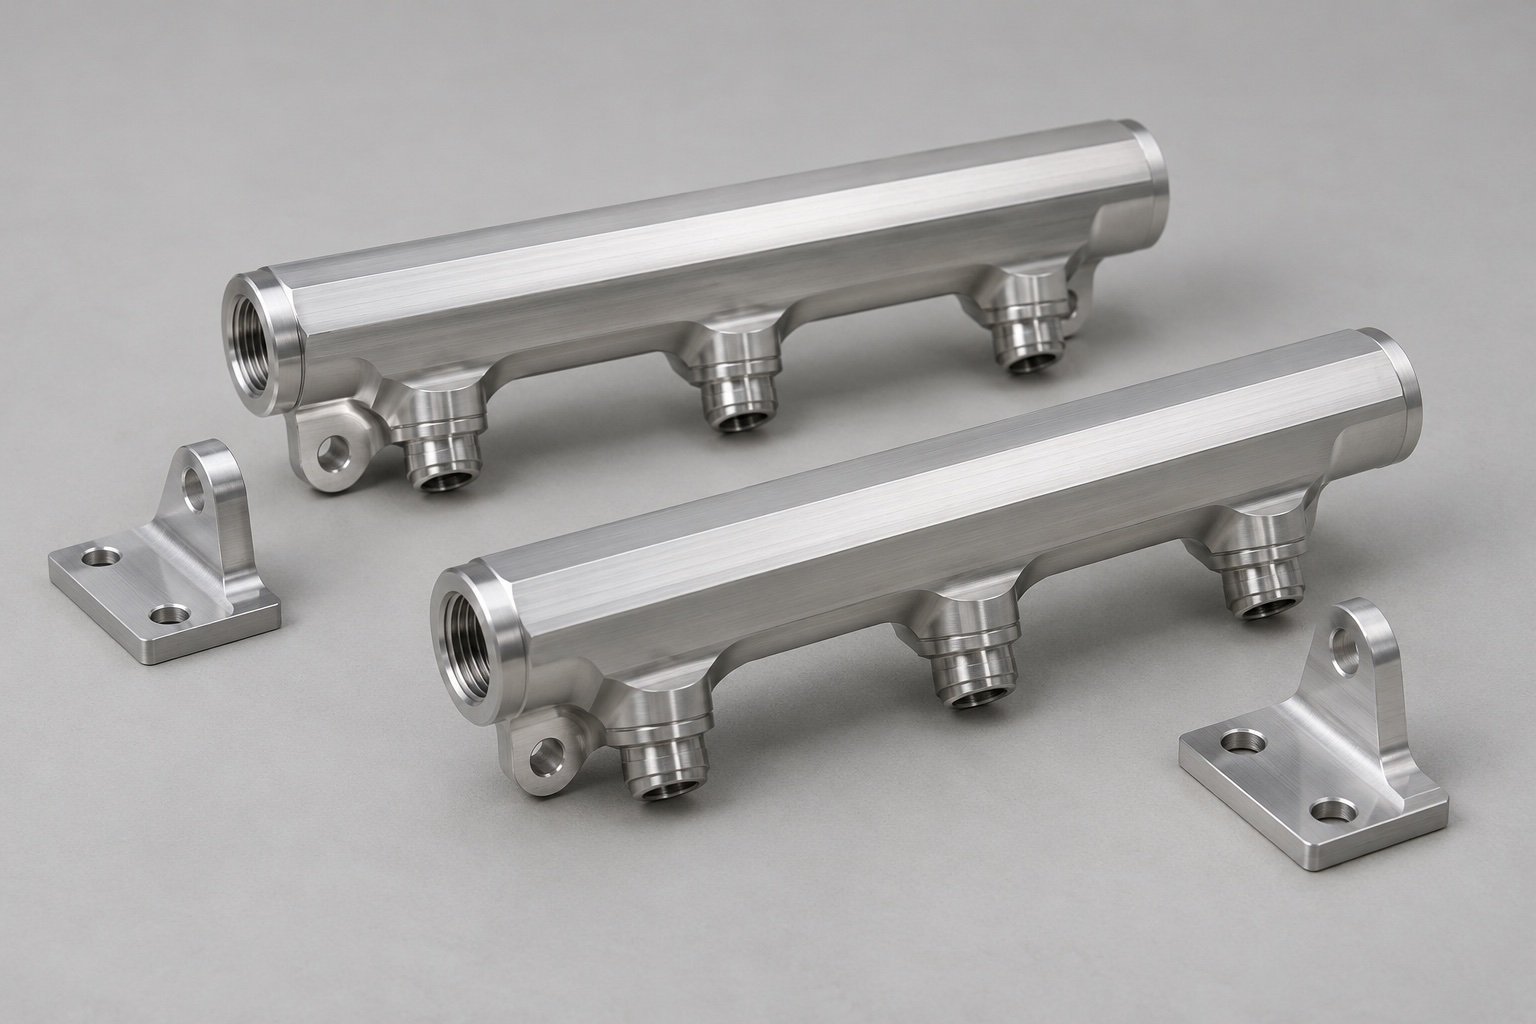
Review bank-to-bank mounting, injector height and retained bracket interfaces.
Resolve sealing and mounting questions before a sample is cut.
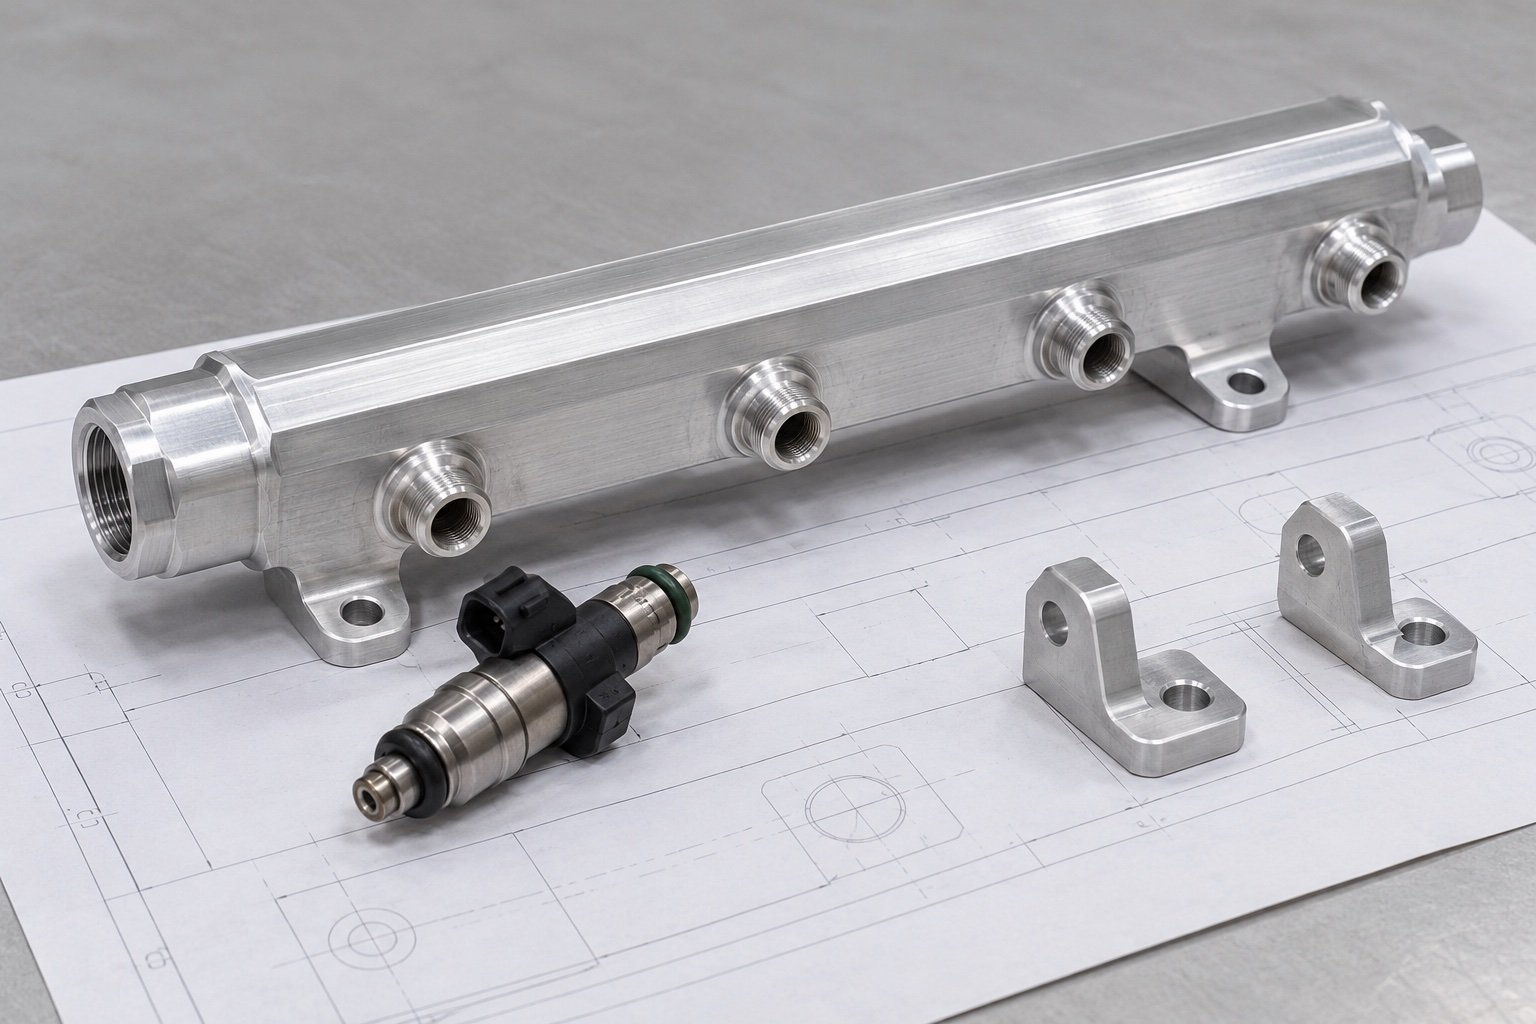
Provide CAD and a drawing revision with injector centers, end datums and mounting dimensions.
Identify the exact injector, seal dimensions and installed height; include approved mating references.
Define thread system, sealing seat, port orientation and any plugs or fittings in scope.
State material, finish, quantities, required records and sample or validation objective.
Keep the gallery, injector seats and bracket datums connected in the drawing.
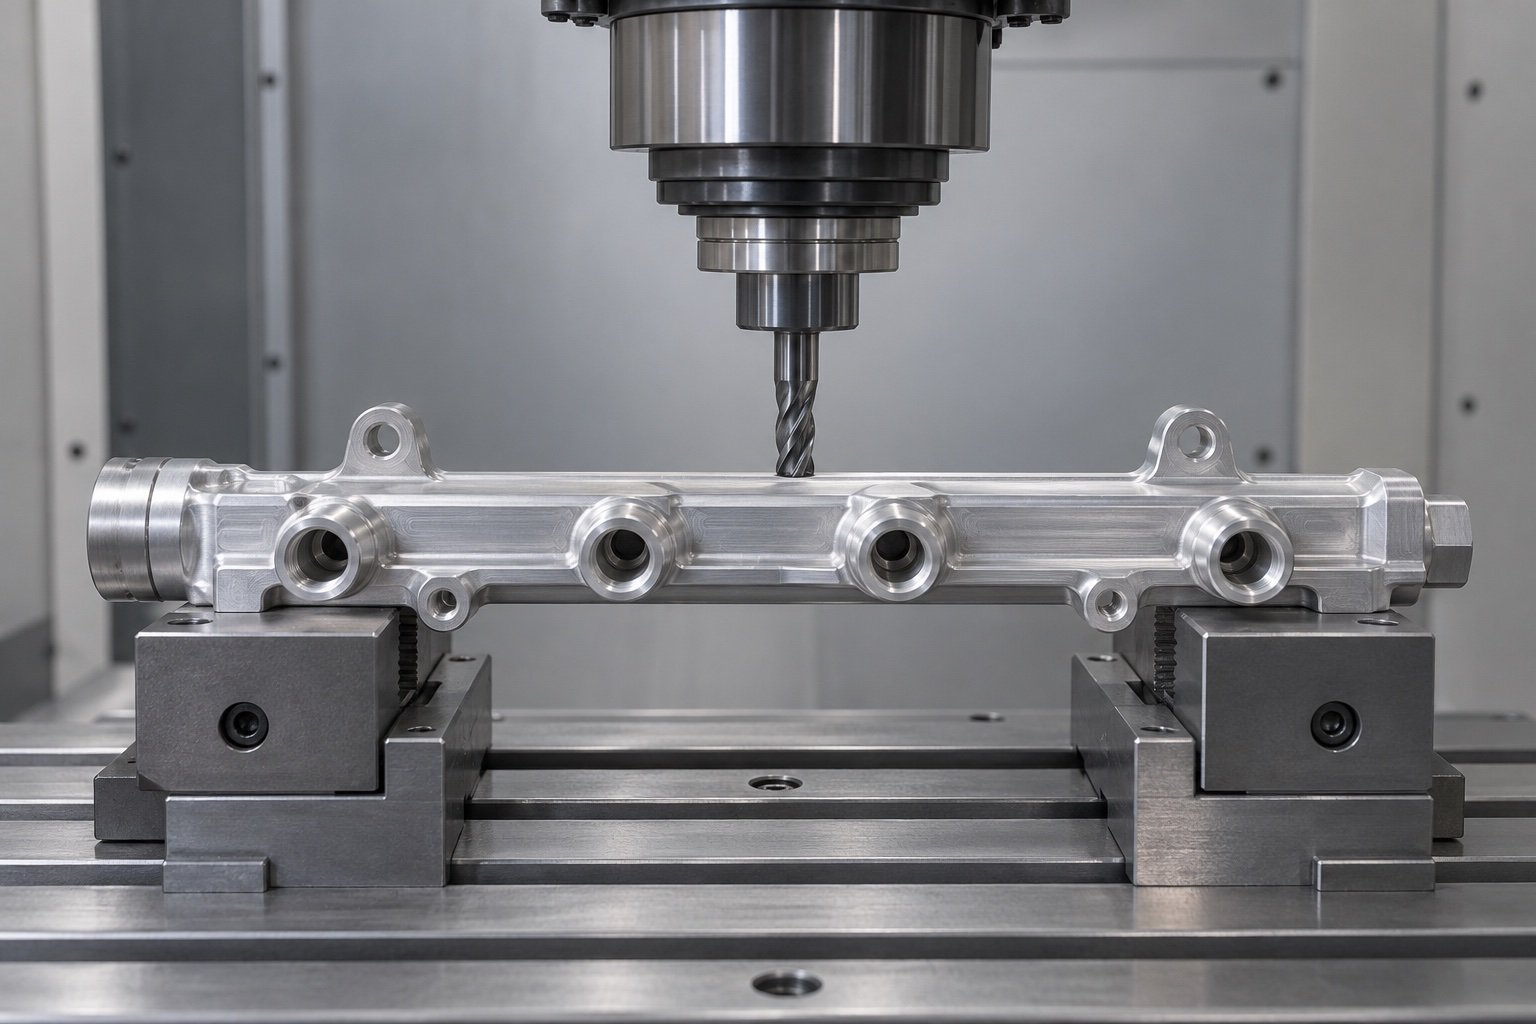
For your custom fuel rail manufacturing project, compare the specified stock form and required internal passage.
Identify sealing surfaces, bore geometry, thread callouts and the dimensions requiring reporting.
Agree deburring, cleanliness, protected interfaces and finish masks before release.
A silver or anodized appearance cannot identify the alloy or establish fuel compatibility.
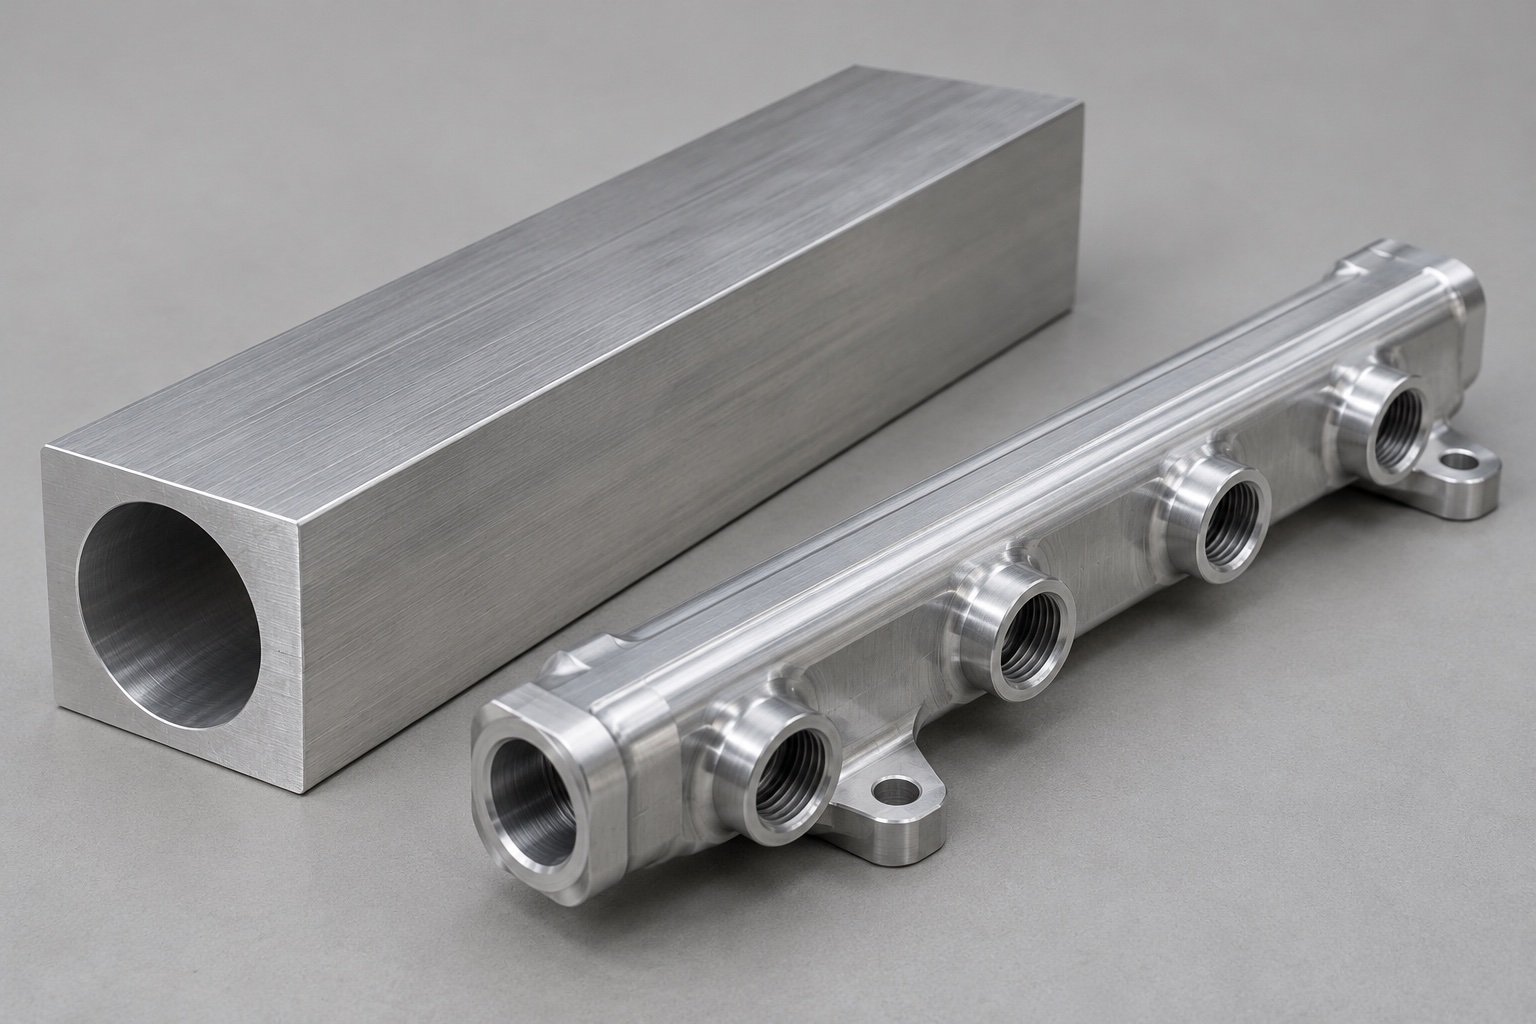
Specify alloy, temper and product form. EN AW-6061 is a designation reference for 6061, not approval to substitute another alloy.
Identify the intended fuel and operating conditions. Define required compatibility evidence for the metal, finish and seals.
Mark injector seats, sealing faces and threads requiring masks or final dimensional checks after finishing.
Agree dimensional inspection and any pressure or leak test as separate, explicit requirements.
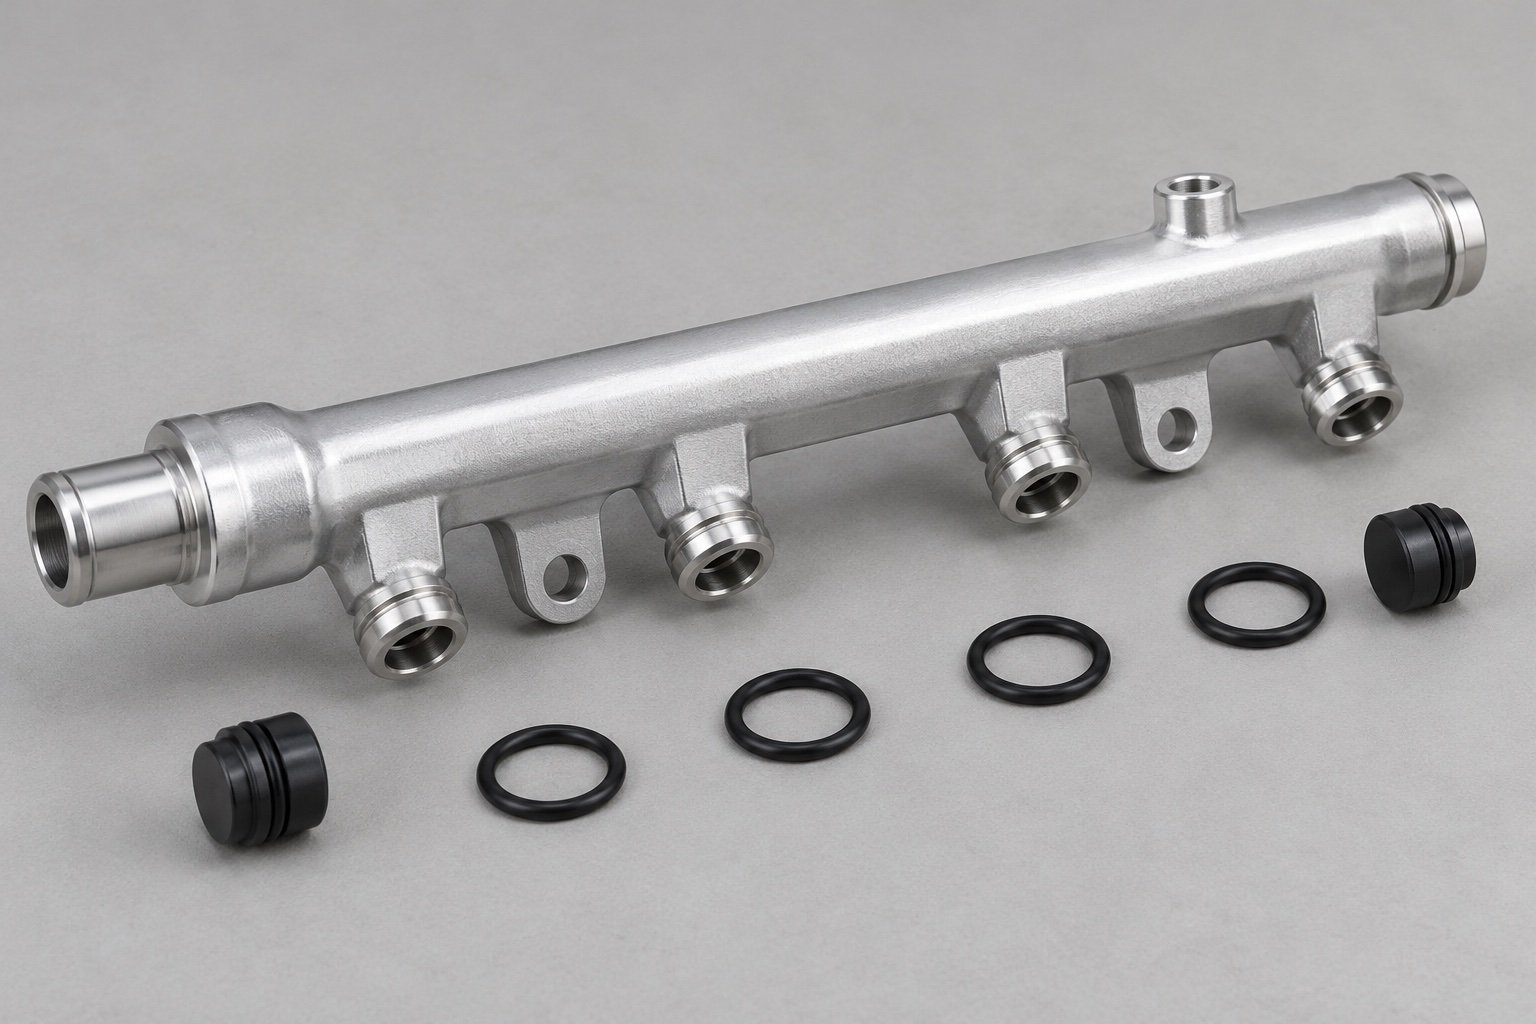
Check center locations and mounting references against the released drawing.
Identify bore dimensions, surface requirements and the actual mating seal reference.
Define thread verification, deburring and cleanliness acceptance requirements.
Specify test medium, pressure, method, acceptance criteria and required records if testing is needed.
Retain the approved injector interface and finish condition with your reorder baseline.
Send CAD, controlled drawing, injector reference and quantities.
Agree process, material, finish, sample objective and inspection or test scope.
Review fit and records; complete the application validation your design requires.
Retain revision, material records, finish sample and protective packing instructions.
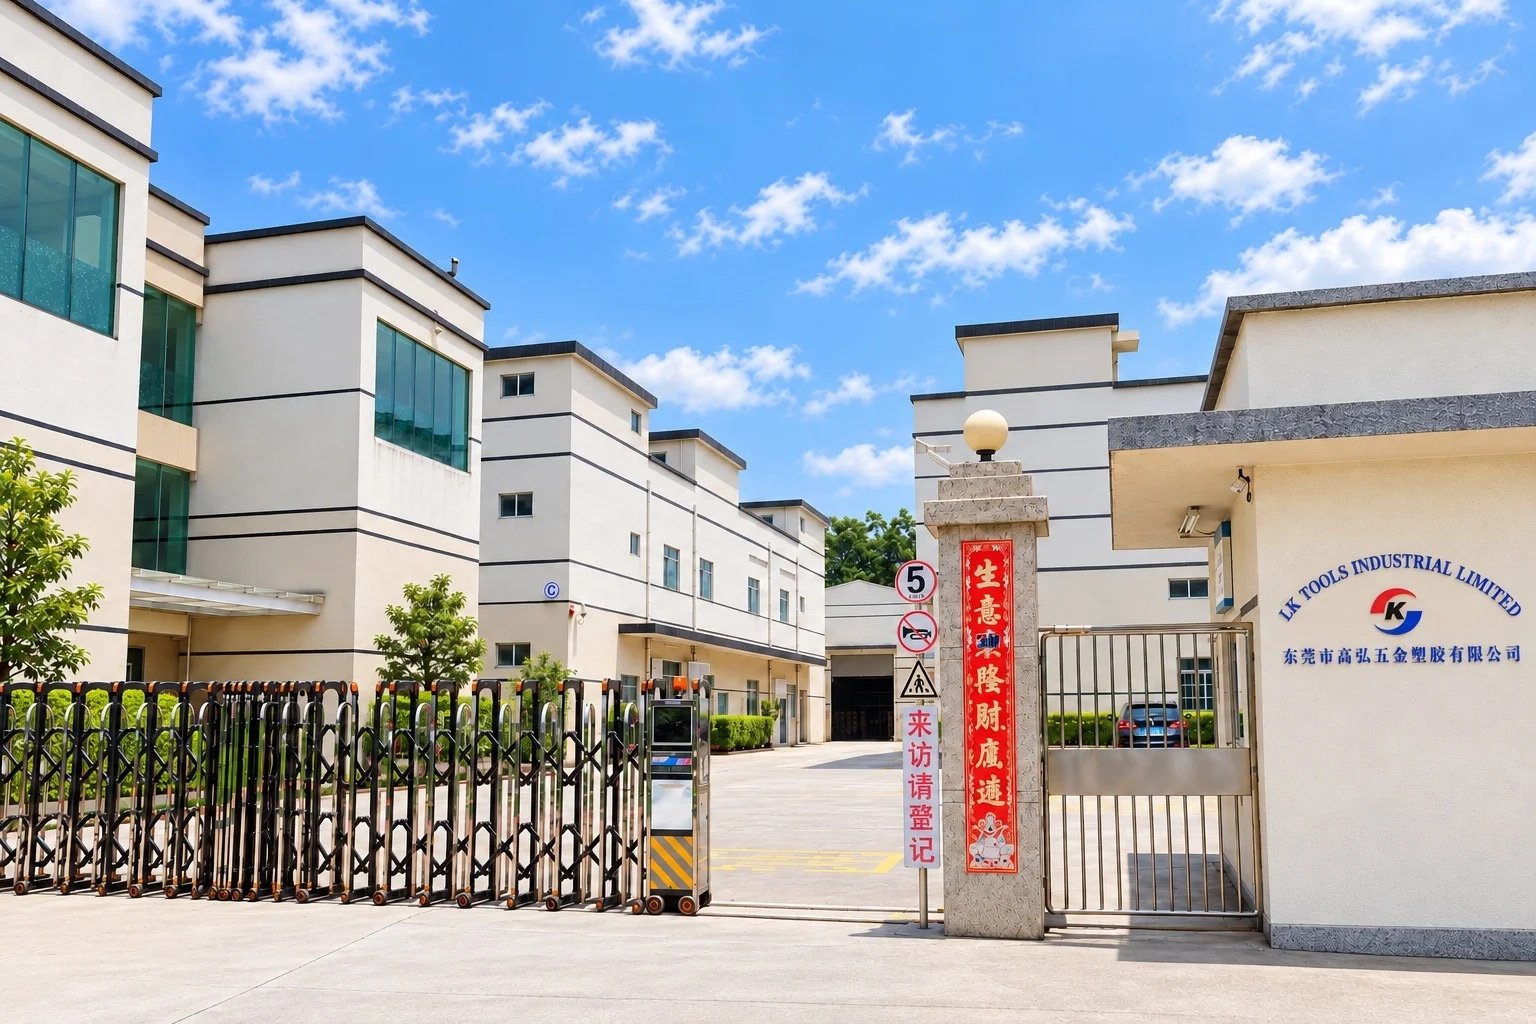
For your fuel rail program, distinguish where the part is made from where your project communication is supported.
Agree who owns the drawing and sample approval.
Confirm packing, delivery terms and import responsibilities.
Discuss local coordination and any inventory arrangement.
Genuine company and customer-discussion photographs. Manufacturing in China; U.S. support does not mean U.S. manufacture or a default local stock program.
Factory & Operations →Upload the drawing revision, material, finish and quantities. Include injector spacing, sealing geometry, mounting height, ports, material and required test records.
Clarify manufacturing scope, mating references and required evidence.
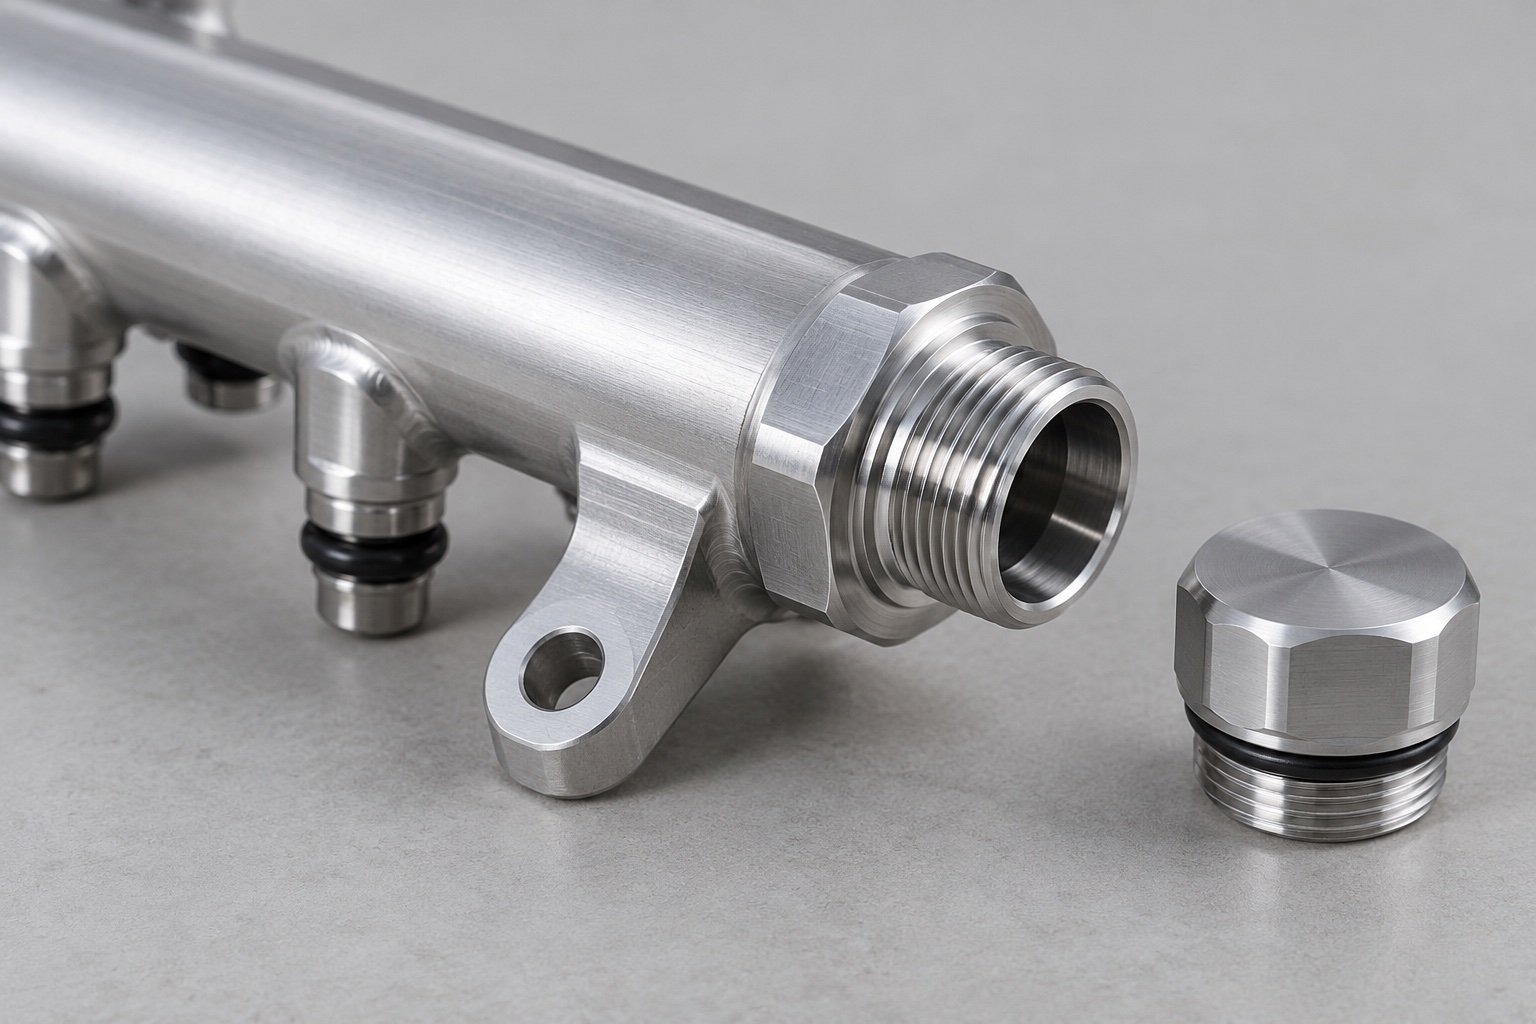
This page covers custom rail manufacturing to your approved definition. It is not a stocked fitment catalog.
Send CAD, drawing revision, injector and seal references, mounting geometry, port specifications, material, finish and quantities.
No. Installed injector height, sealing geometry, mounting datums and manifold clearances also need controlled references.
Testing is provided only within an expressly agreed scope. Define the method, medium, pressure, acceptance criteria and reporting requirements in your RFQ.
Review changes against the controlled interfaces and validation requirements before release. Similar nominal descriptions do not establish interchangeability.
Provide both quantities for review. Retain the approved revision and acceptance package for subsequent orders; lead time and quantity scope are confirmed in the quotation.









