

Injection Molding
Tooling and molding for your repeat plastic parts.
From prototype to production, coordinated manufacturing solutions for your custom parts.
View All Services →
Precision parts for your tight tolerances and complex geometry.
Tooling and molding for your repeat plastic parts.

Metal casting options for your part and production volume.

Cutting, forming and welding for your fabricated parts.

Custom profiles for your section, length and finish requirements.

Finishes for your appearance, corrosion and wear requirements.

Sub-assemblies and final builds for your production program.

Production tooling built around your process and volume.

Prototype parts to check fit, function and design.
DFM, process planning and production support for your project.
Inspection, documentation, inventory and delivery planning for your program.
Choose air- or liquid-cooling components around your thermal and mechanical requirements.

Manufacturing support for your cold plates, manifolds and cooling assemblies.

Find components for your power electronics, energy, laser and telecom application.

Components for your electronic systems.
Start with your functional and quality requirements.
Build around your operating environment.
From prototype to production, review material performance, manufacturability and cost for your part.
Review grade, temper and finish for your metal parts.
 AluminumStrength, weight and machining›
 Stainless SteelCorrosion and finish requirements›
 Carbon & Alloy SteelDiscuss grade and heat treatment›
 Tool SteelDiscuss tooling and wear needs›
 TitaniumReview grade and part geometry›
 Copper & Brass & BronzeDiscuss conductivity and machining›
Match your polymer to function, process and environment.
 ABSReview enclosure and molding needs›
 Polycarbonate (PC)Discuss clarity and impact needs›
 Nylon (PA)Review moisture and wear conditions›
 POM / AcetalReview fit and sliding features›
 PEEKDiscuss operating conditions›
 PTFEReview friction and chemical exposure›
 ULTEM / PEIDiscuss thermal and electrical needs›
Confirm grade availability and application requirements.
 Silicone / LSRDiscuss flexible component needs›
 TPU / TPEReview flexibility and processing›
 EPDMReview weathering and chemical exposure.›
 NBRReview oil and fuel exposure.›
 FKMReview temperature and chemical exposure.›
 G10 / FR4Review insulation and laminate needs›
 CompositesReview stiffness, weight and laminate.›Customer-Specified MaterialsConfirm your grade and requirements.›Other Specialty MaterialsDiscuss your application and grade.›
Practical guidance for your part geometry and material decisions.
Prepare your process, budget and sourcing questions.
Build your knowledge before production.
Learn who we are and how we operate.
Find our U.S. support team or start a conversation.
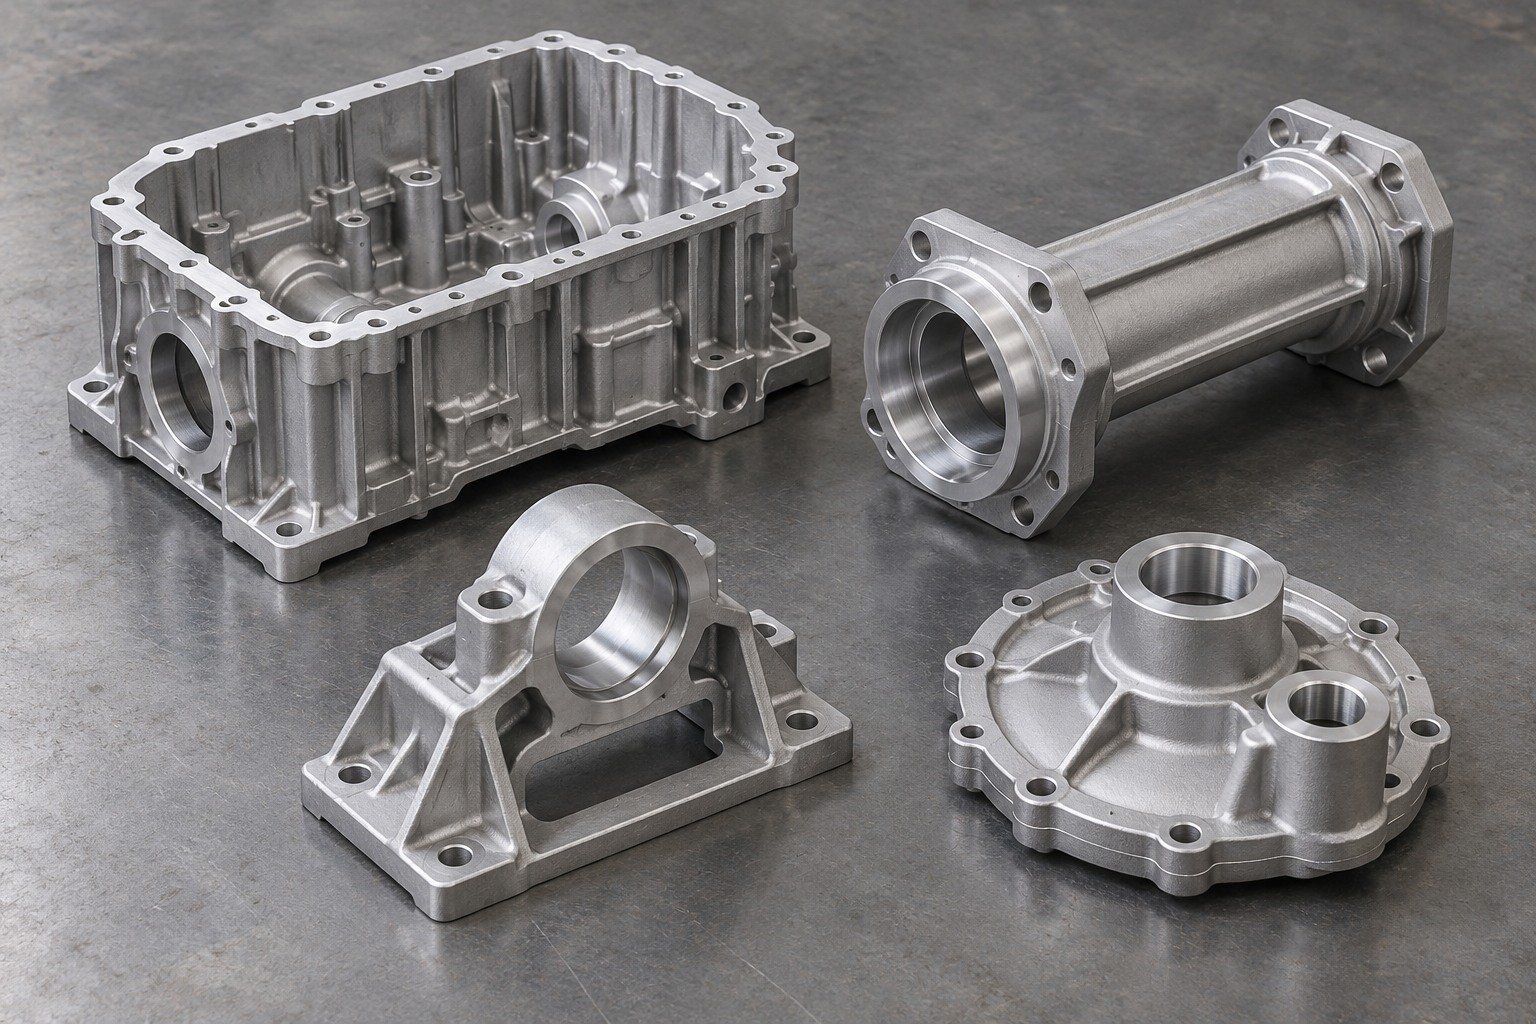
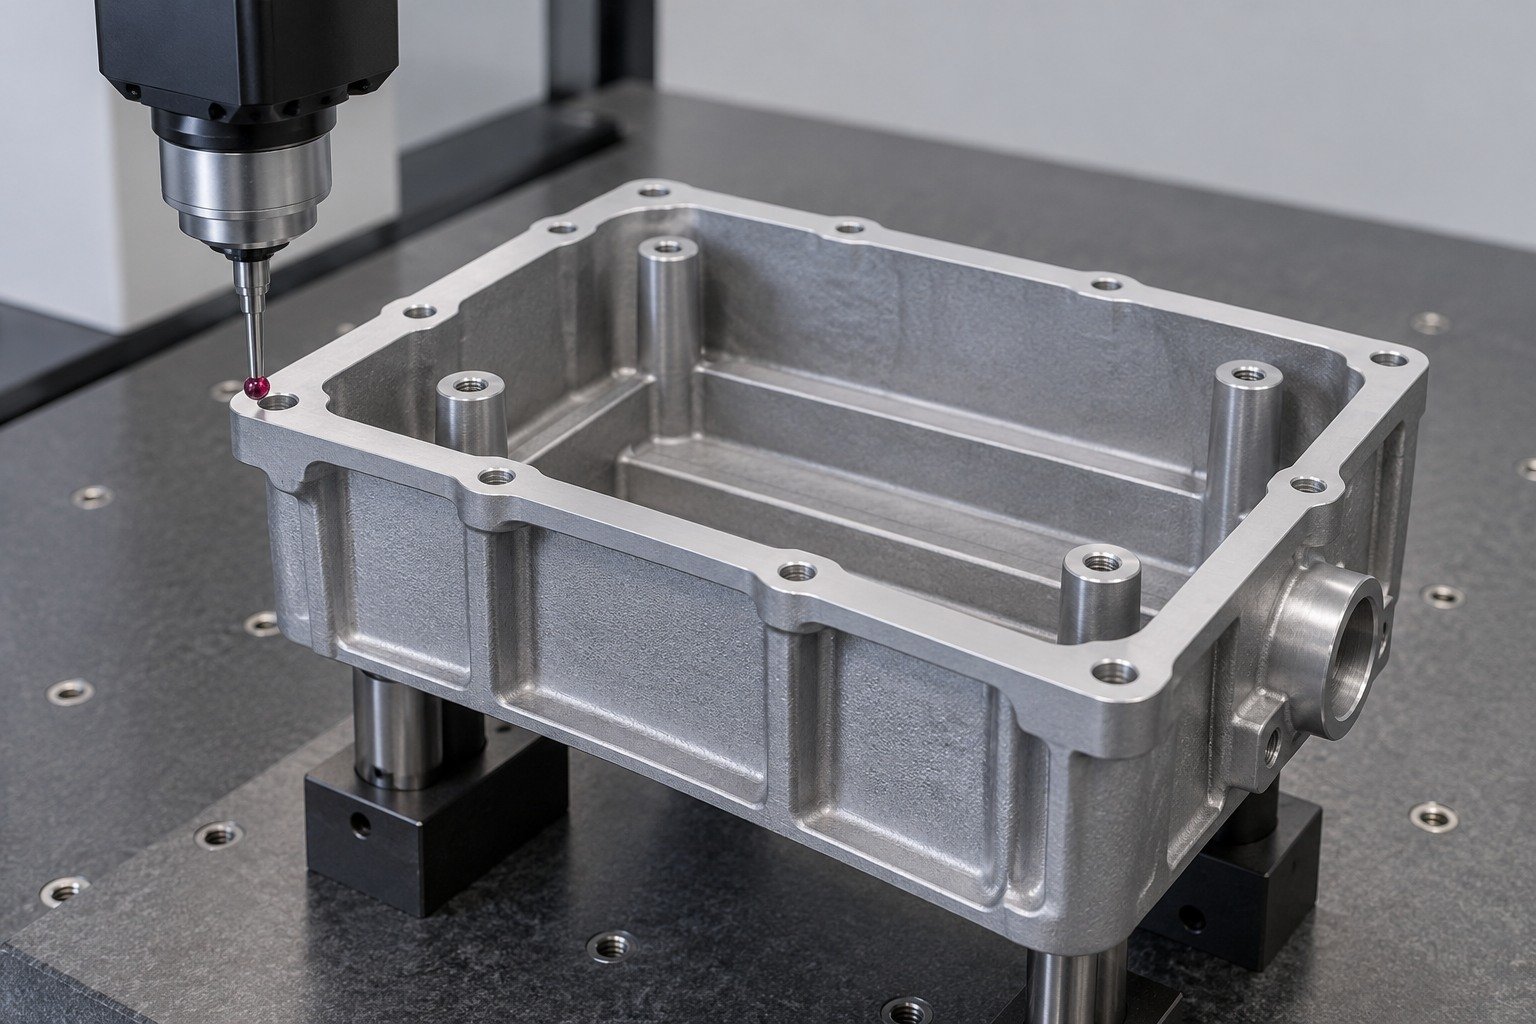
Bring your ZA-12 die casting and ZA-12 CNC machining requirements together before releasing the drawing. Define the casting route, supported locating surfaces and the finished bores or mounting lands for your custom ZA-12 parts.
Your ZA-12 casting manufacturer review should distinguish the cast envelope from the faces, bores and interfaces that need machining.
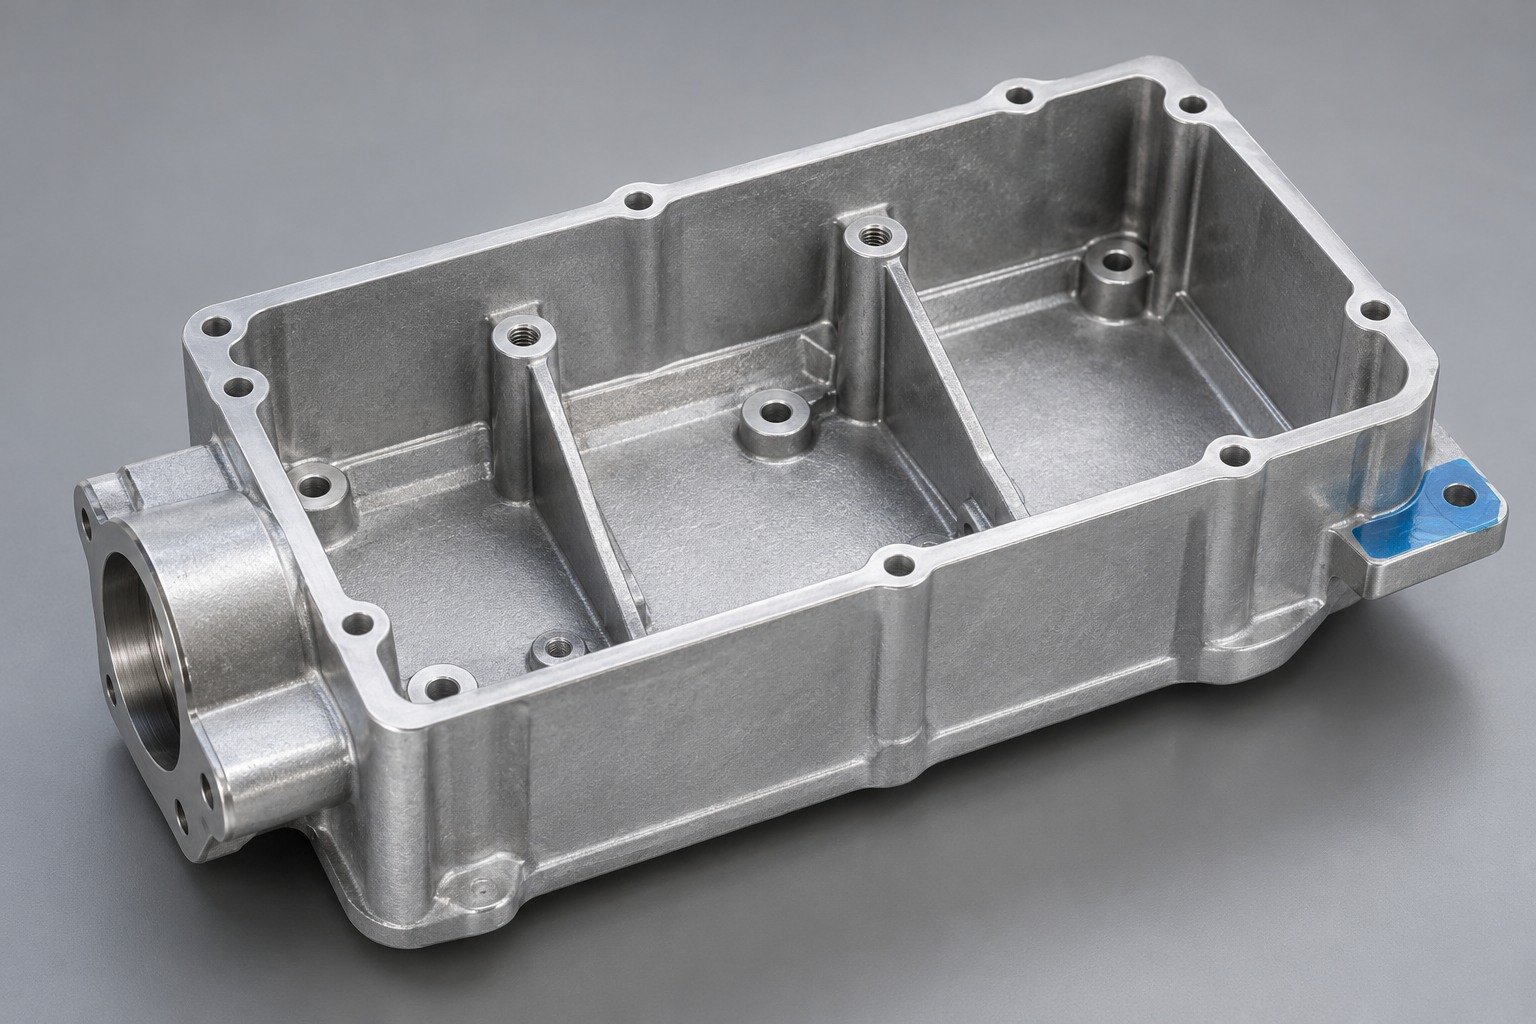
For your gearbox shell, identify internal boss access, flange flatness, side-port relationship and the faces located in each setup. Review ZA-12 die cast housings against the controlled assembly.
| Your fit | What to define |
|---|---|
| Working interface | Open cavity, bosses, mounting flange and side-port land. |
| Your route | Casting product, usable stock and supported machining. |
| Your approval | Free or installed measurement state, finish and receiving records. |
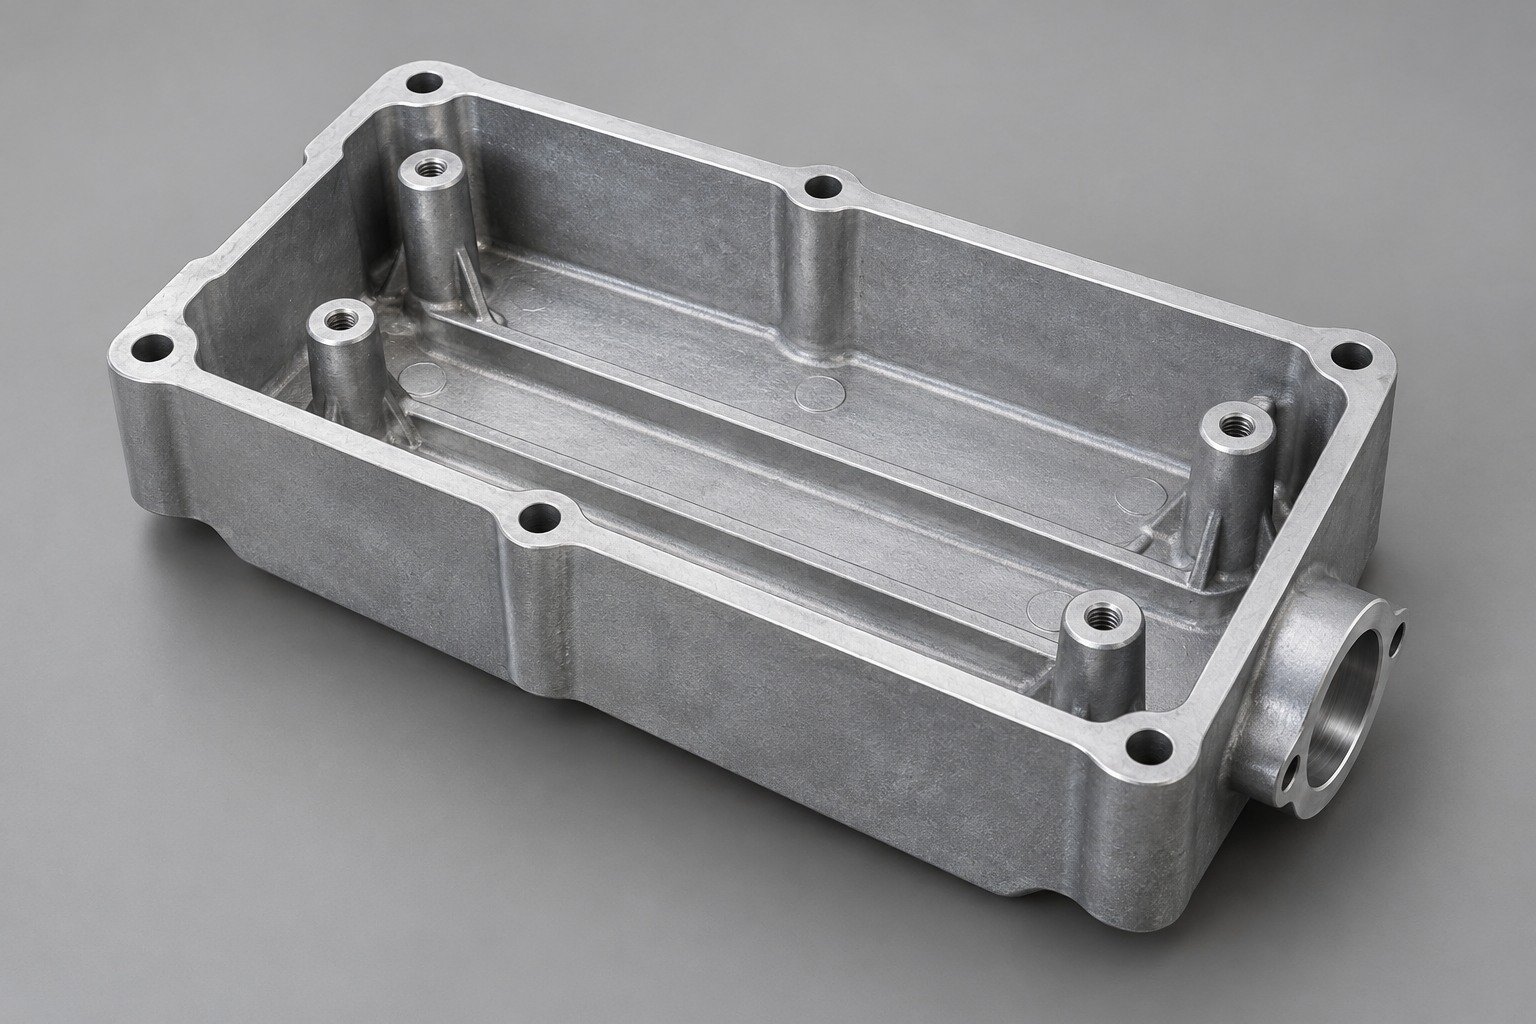
For your ZA-12 machining review, show usable stock, supported datums, cutter access and the final surfaces that determine assembly fit.
| Your fit | What to define |
|---|---|
| Working interface | Open cavity, bosses, mounting flange and side-port land. |
| Your route | Casting product, usable stock and supported machining. |
| Your approval | Free or installed measurement state, finish and receiving records. |
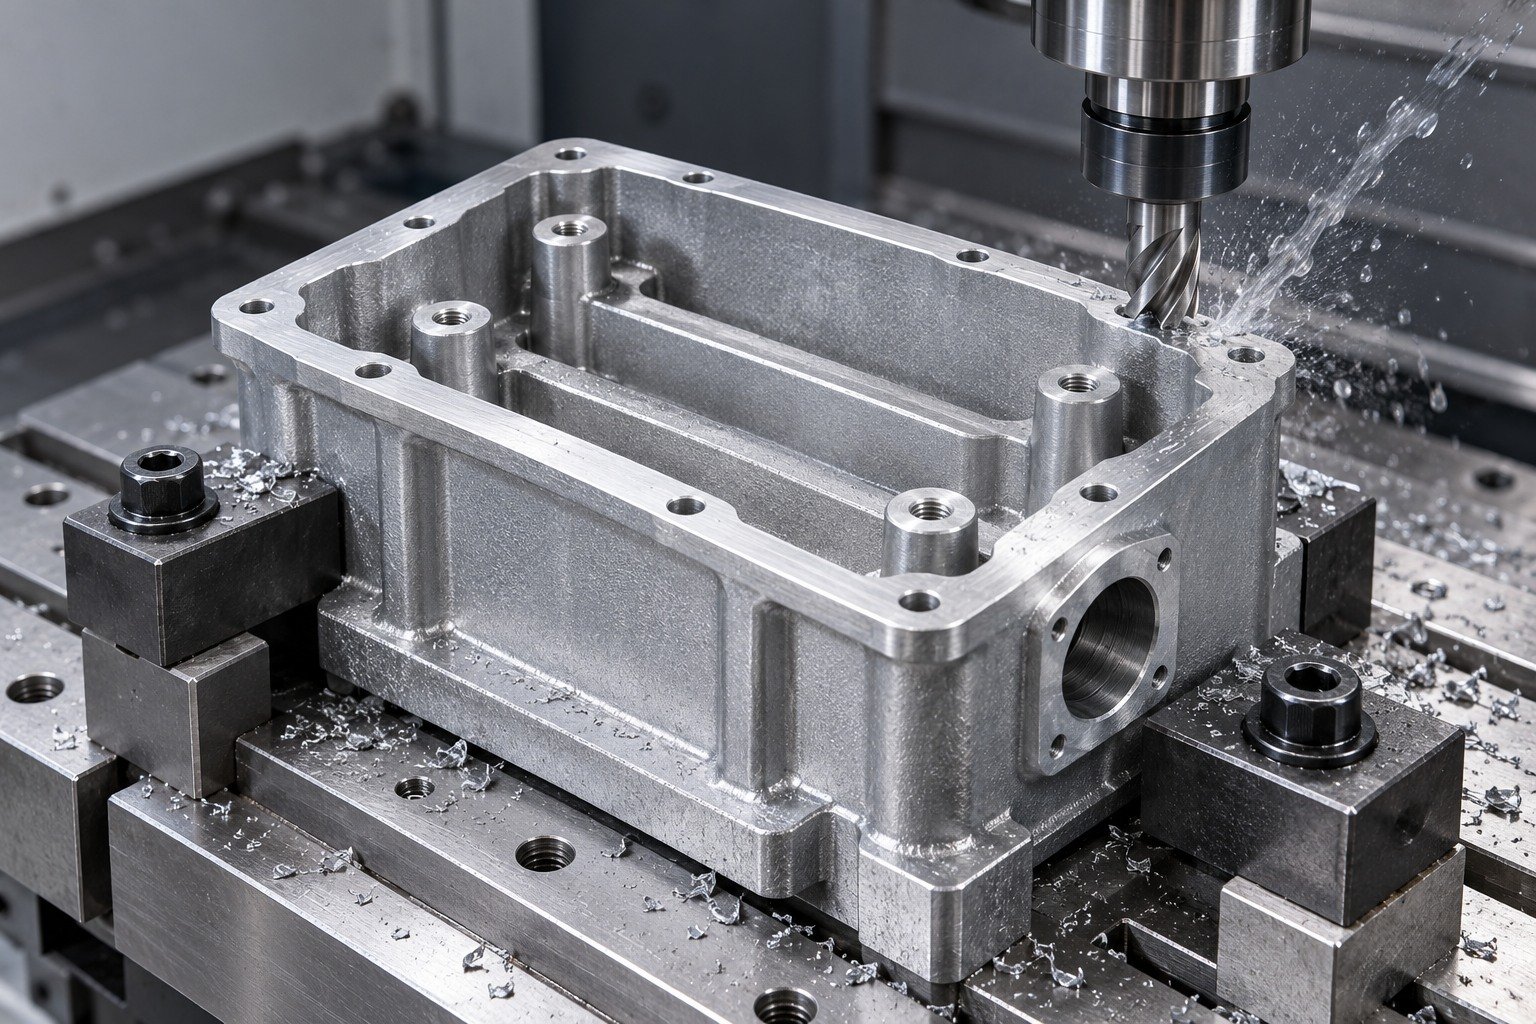
Specify the casting route, supplied state, usable stock and final coating requirements. Agree final inspection after the last dimension-changing operation.
| Your fit | What to define |
|---|---|
| Working interface | Open cavity, bosses, mounting flange and side-port land. |
| Your route | Casting product, usable stock and supported machining. |
| Your approval | Free or installed measurement state, finish and receiving records. |
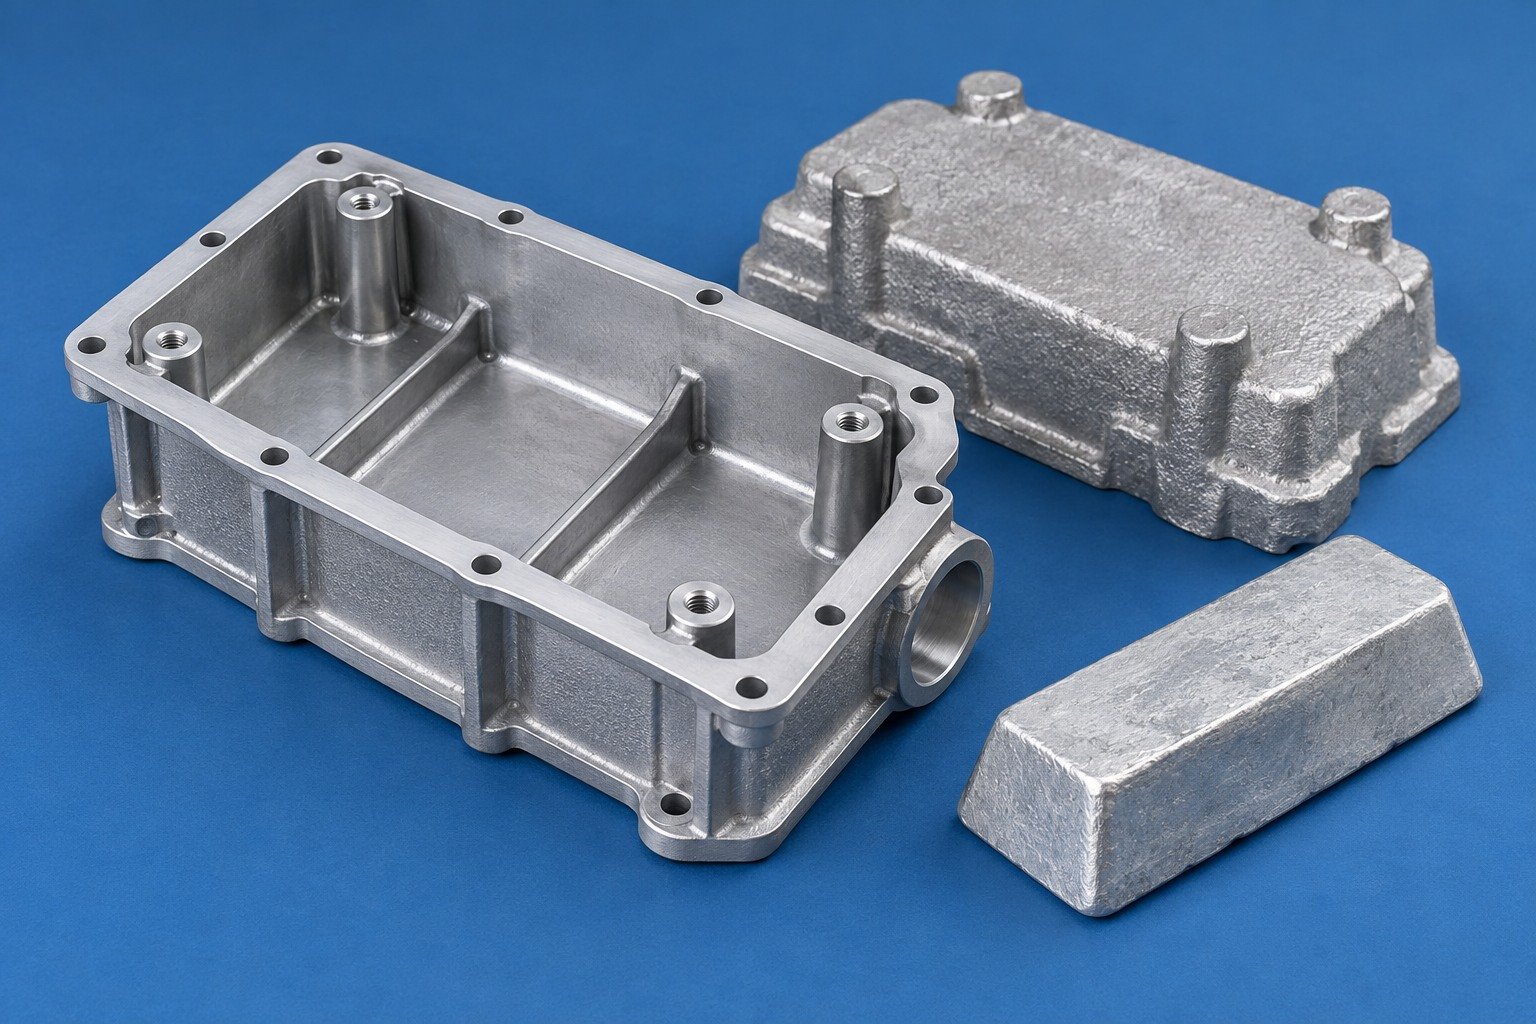
For your ZA-12 machined parts, identify the material records, final dimensions, accepted edges, cleanliness and individual protection.
| Your fit | What to define |
|---|---|
| Working interface | Open cavity, bosses, mounting flange and side-port land. |
| Your route | Casting product, usable stock and supported machining. |
| Your approval | Free or installed measurement state, finish and receiving records. |
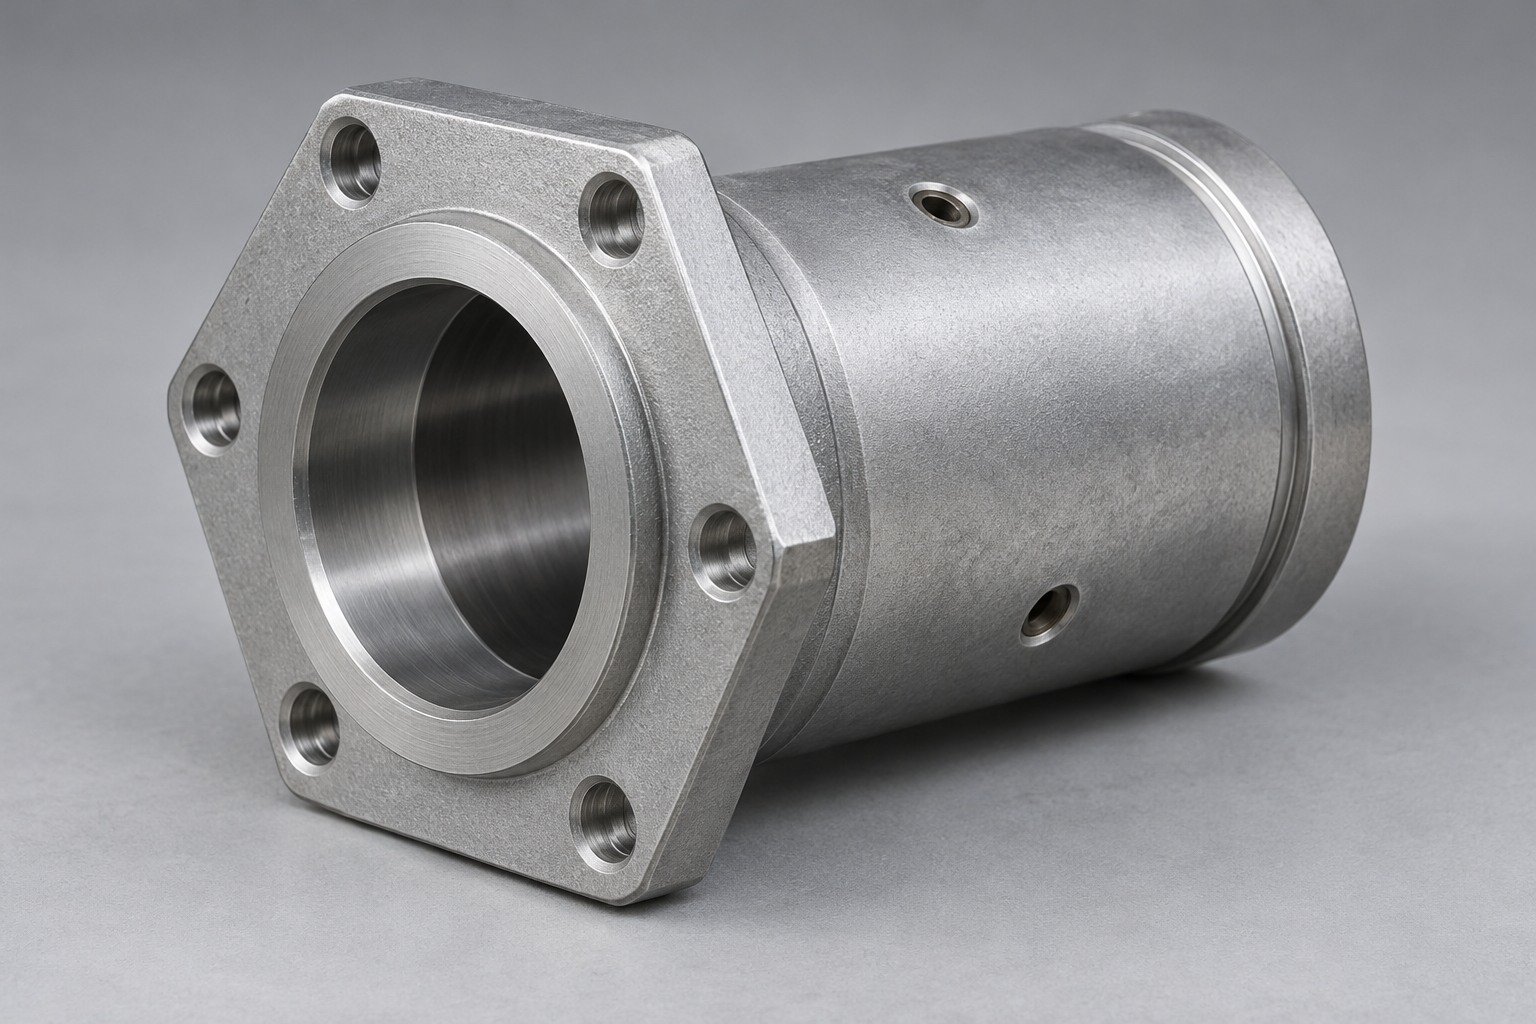
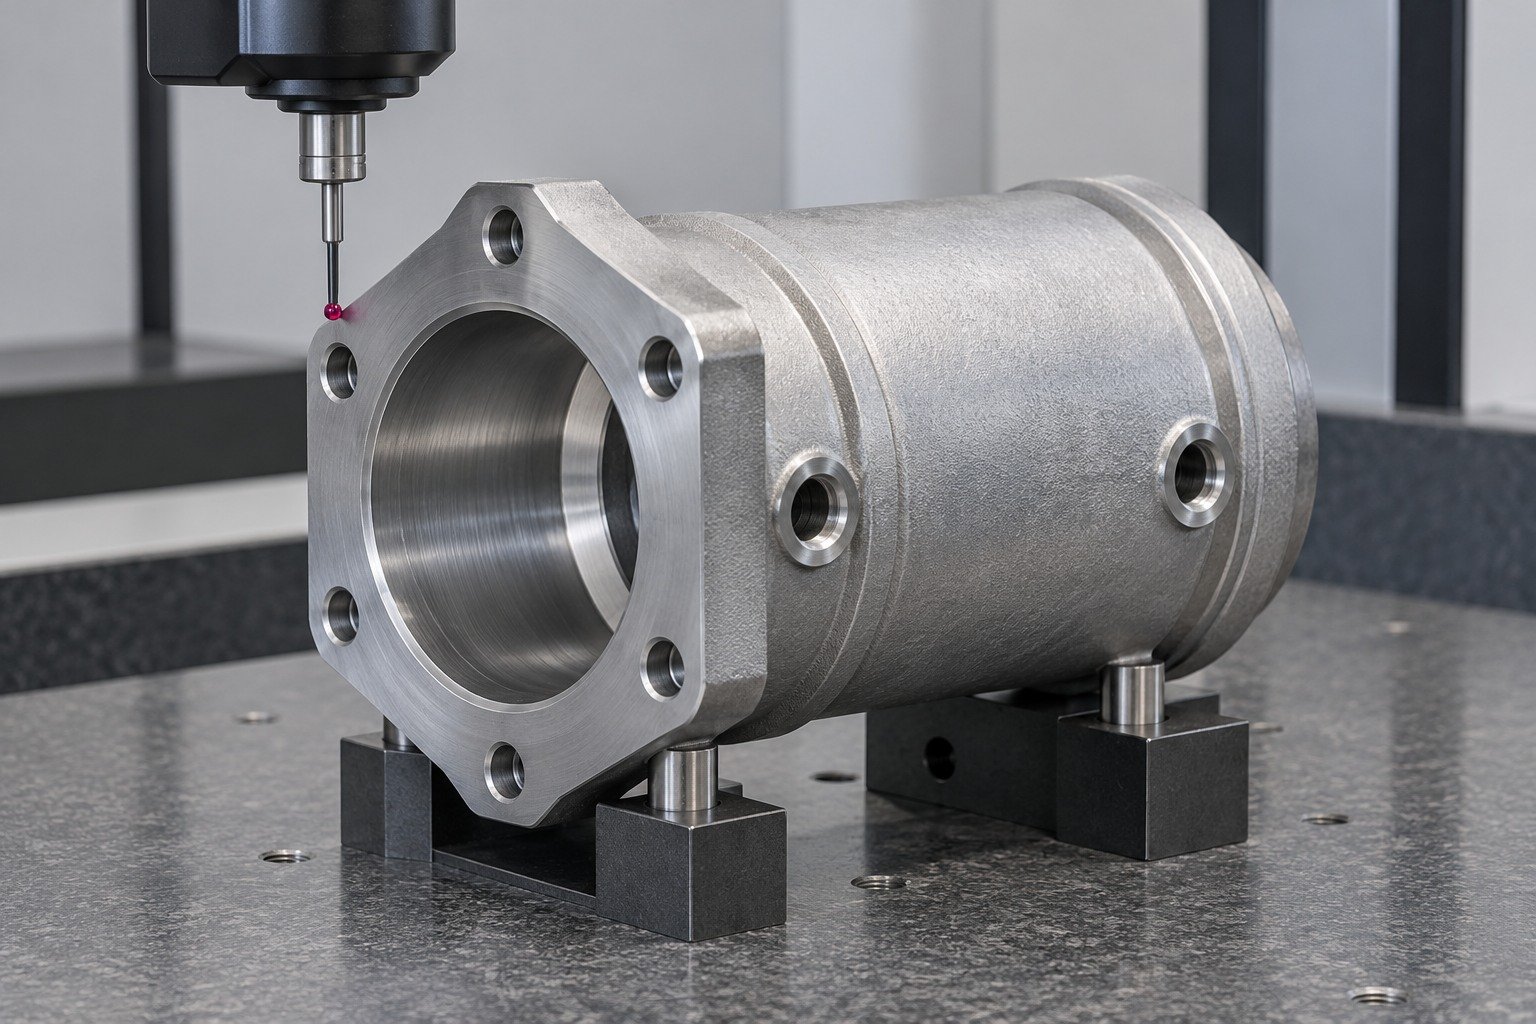
For your flanged sleeve, define the bore, outer locating land, oil ports and the dimensions inspected before or after installation. Review ZA-12 bearing components against the controlled assembly.
| Your fit | What to define |
|---|---|
| Working interface | Bore, hexagonal flange, outer land and oil ports. |
| Your route | Casting product, usable stock and supported machining. |
| Your approval | Free or installed measurement state, finish and receiving records. |
For your ZA-12 machining review, show usable stock, supported datums, cutter access and the final surfaces that determine assembly fit.
| Your fit | What to define |
|---|---|
| Working interface | Bore, hexagonal flange, outer land and oil ports. |
| Your route | Casting product, usable stock and supported machining. |
| Your approval | Free or installed measurement state, finish and receiving records. |

Specify the casting route, supplied state, usable stock and final coating requirements. Agree final inspection after the last dimension-changing operation.
| Your fit | What to define |
|---|---|
| Working interface | Bore, hexagonal flange, outer land and oil ports. |
| Your route | Casting product, usable stock and supported machining. |
| Your approval | Free or installed measurement state, finish and receiving records. |
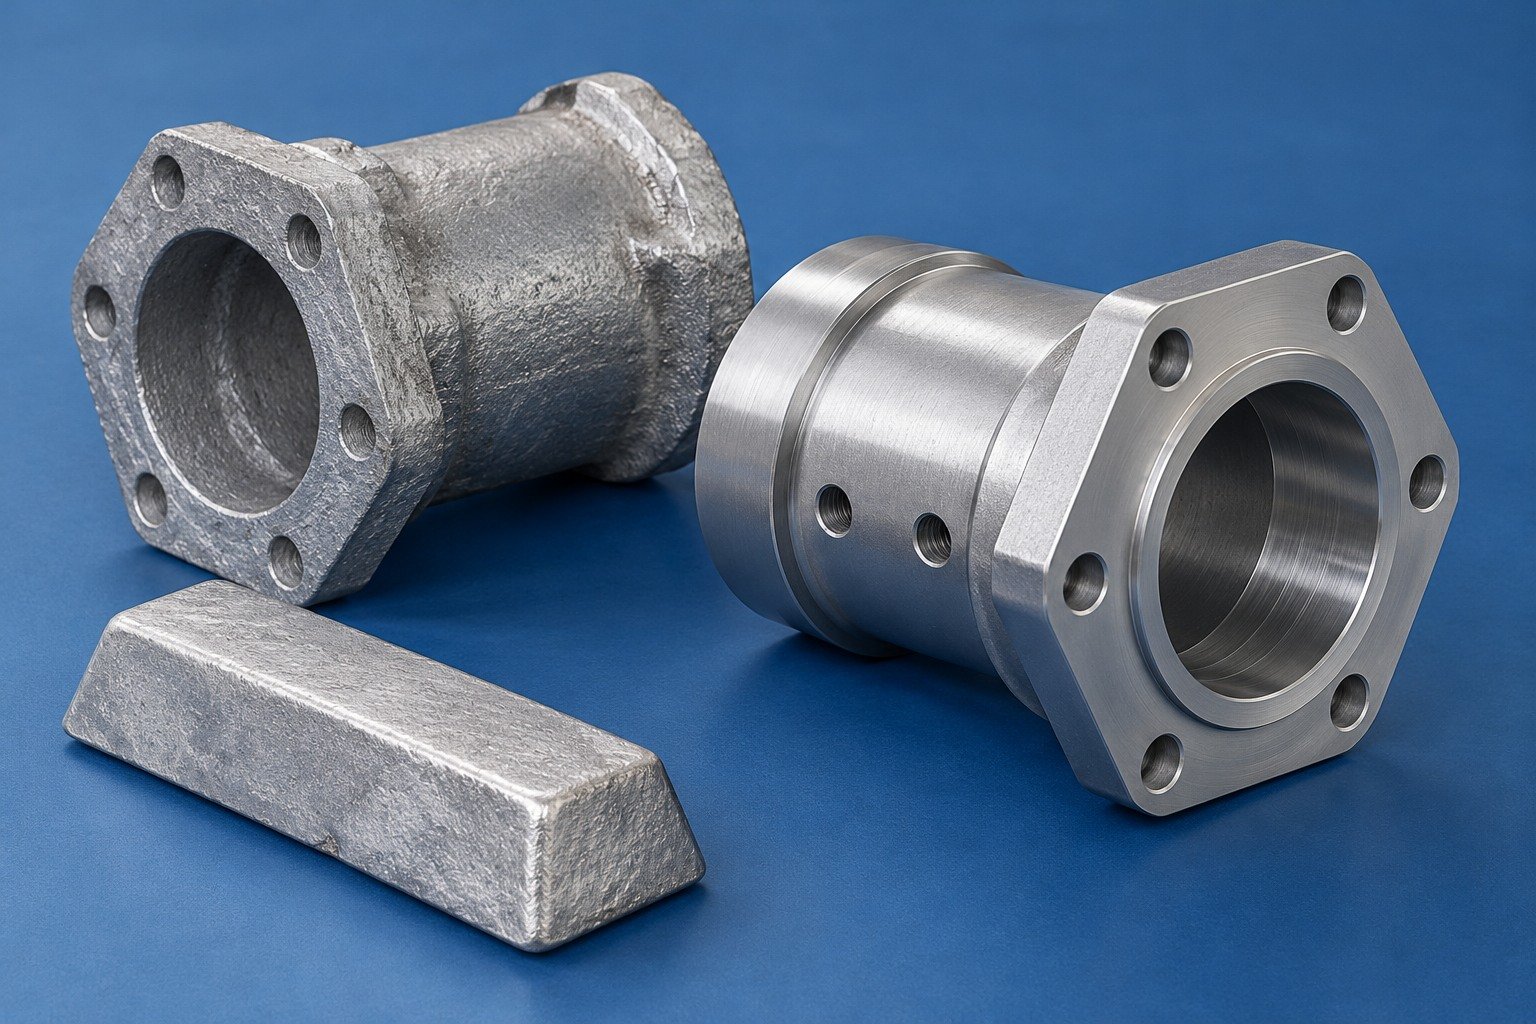
For your ZA-12 machined parts, identify the material records, final dimensions, accepted edges, cleanliness and individual protection.
| Your fit | What to define |
|---|---|
| Working interface | Bore, hexagonal flange, outer land and oil ports. |
| Your route | Casting product, usable stock and supported machining. |
| Your approval | Free or installed measurement state, finish and receiving records. |
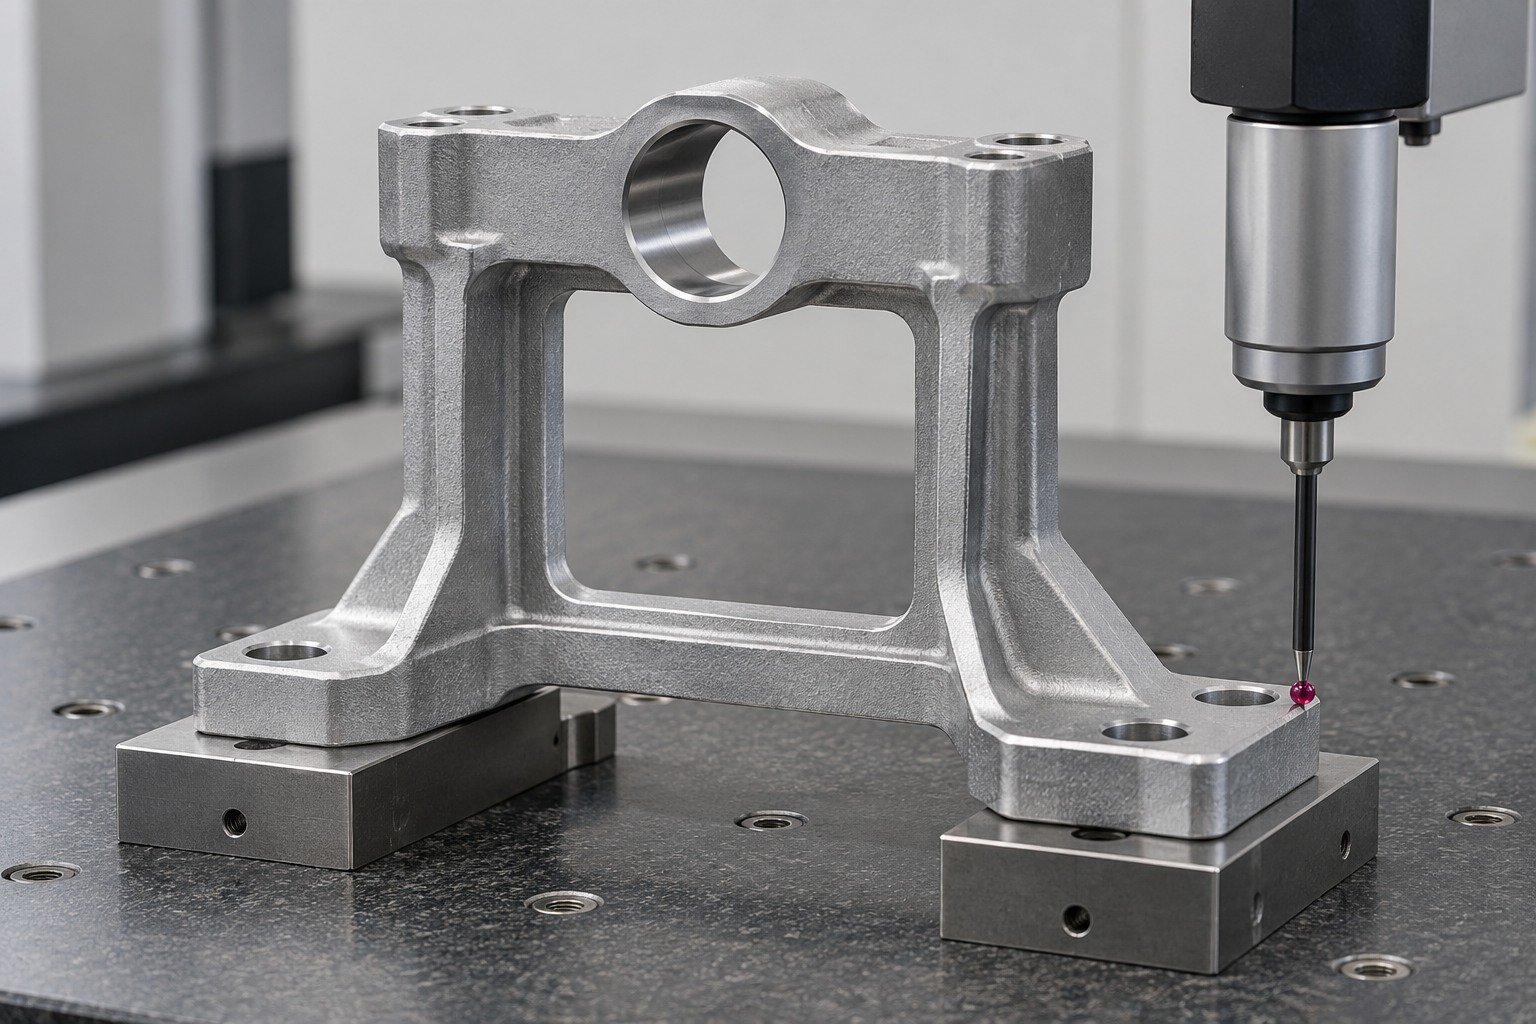
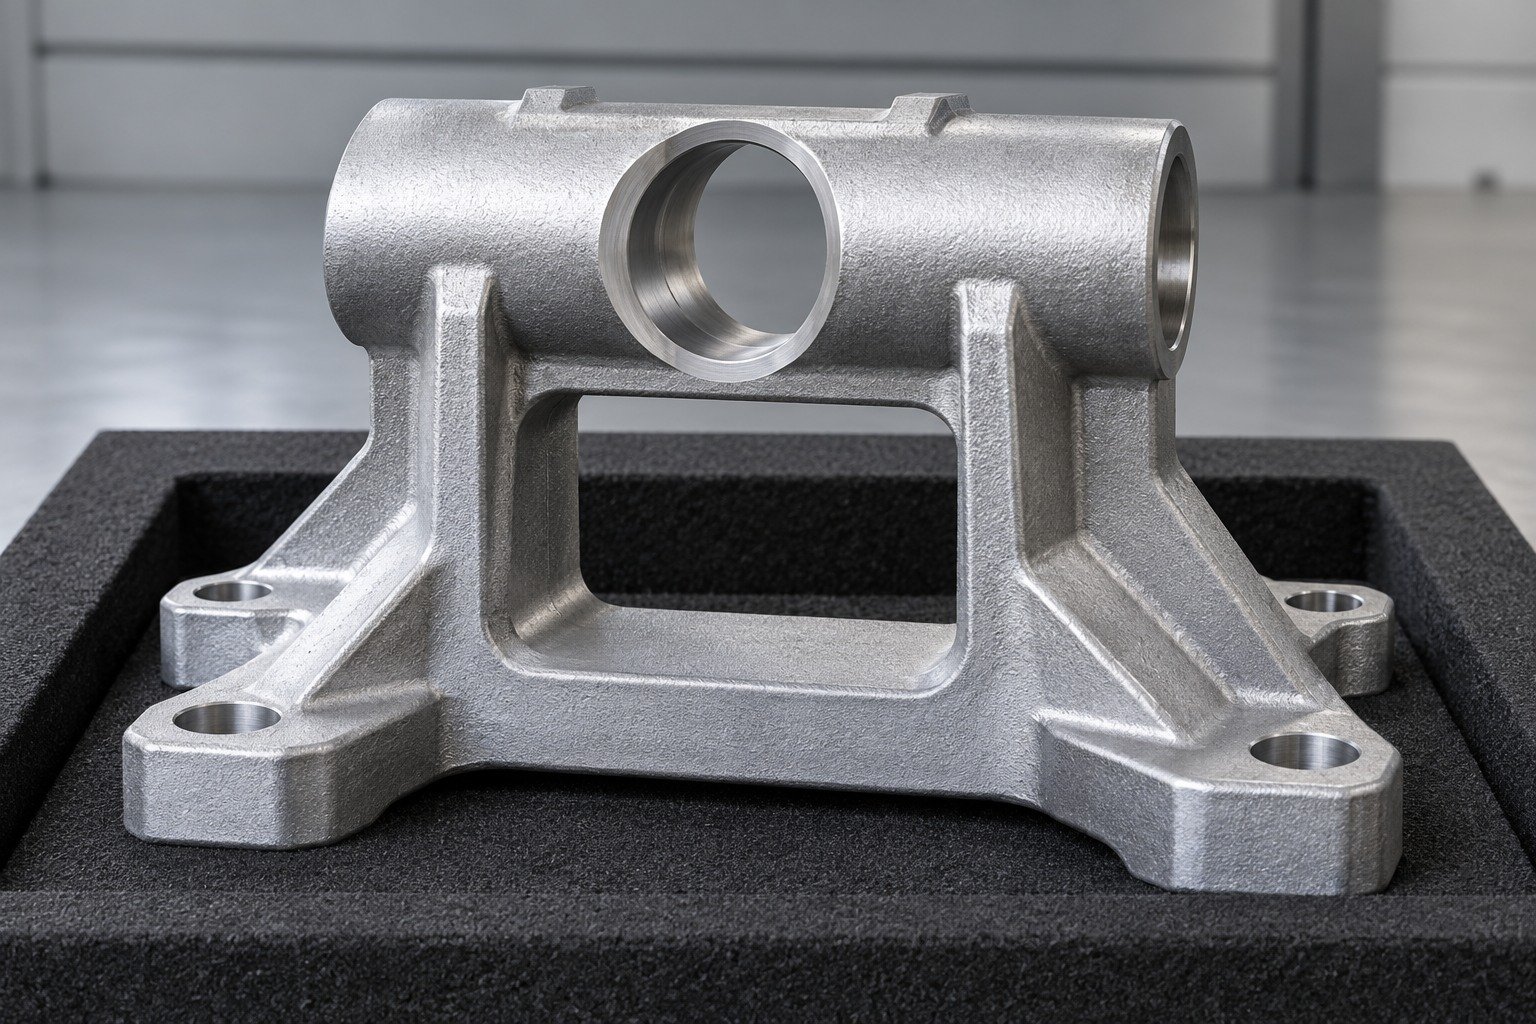
For your bridge frame, connect the bored crossbar to the mounting feet, mating shaft and service load. Review custom ZA-12 bridge frames against the controlled assembly.
| Your fit | What to define |
|---|---|
| Working interface | Crossbar bore, foot datums, columns and mating shaft. |
| Your route | Casting product, usable stock and supported machining. |
| Your approval | Free or installed measurement state, finish and receiving records. |
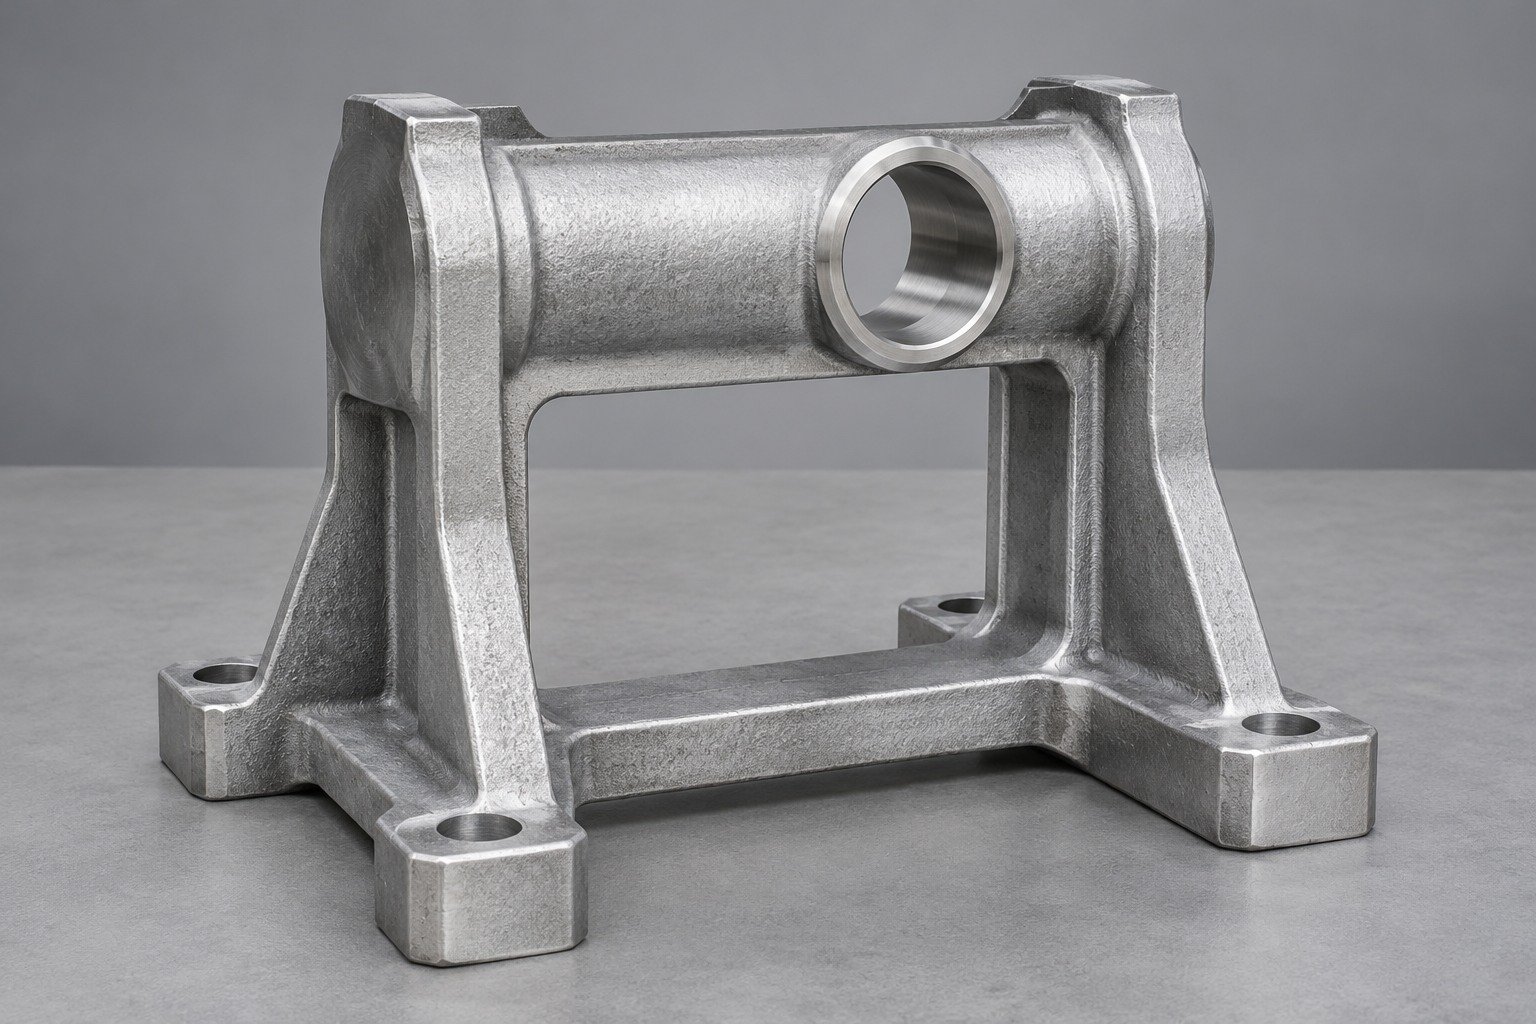
For your ZA-12 machining review, show usable stock, supported datums, cutter access and the final surfaces that determine assembly fit.
| Your fit | What to define |
|---|---|
| Working interface | Crossbar bore, foot datums, columns and mating shaft. |
| Your route | Casting product, usable stock and supported machining. |
| Your approval | Free or installed measurement state, finish and receiving records. |
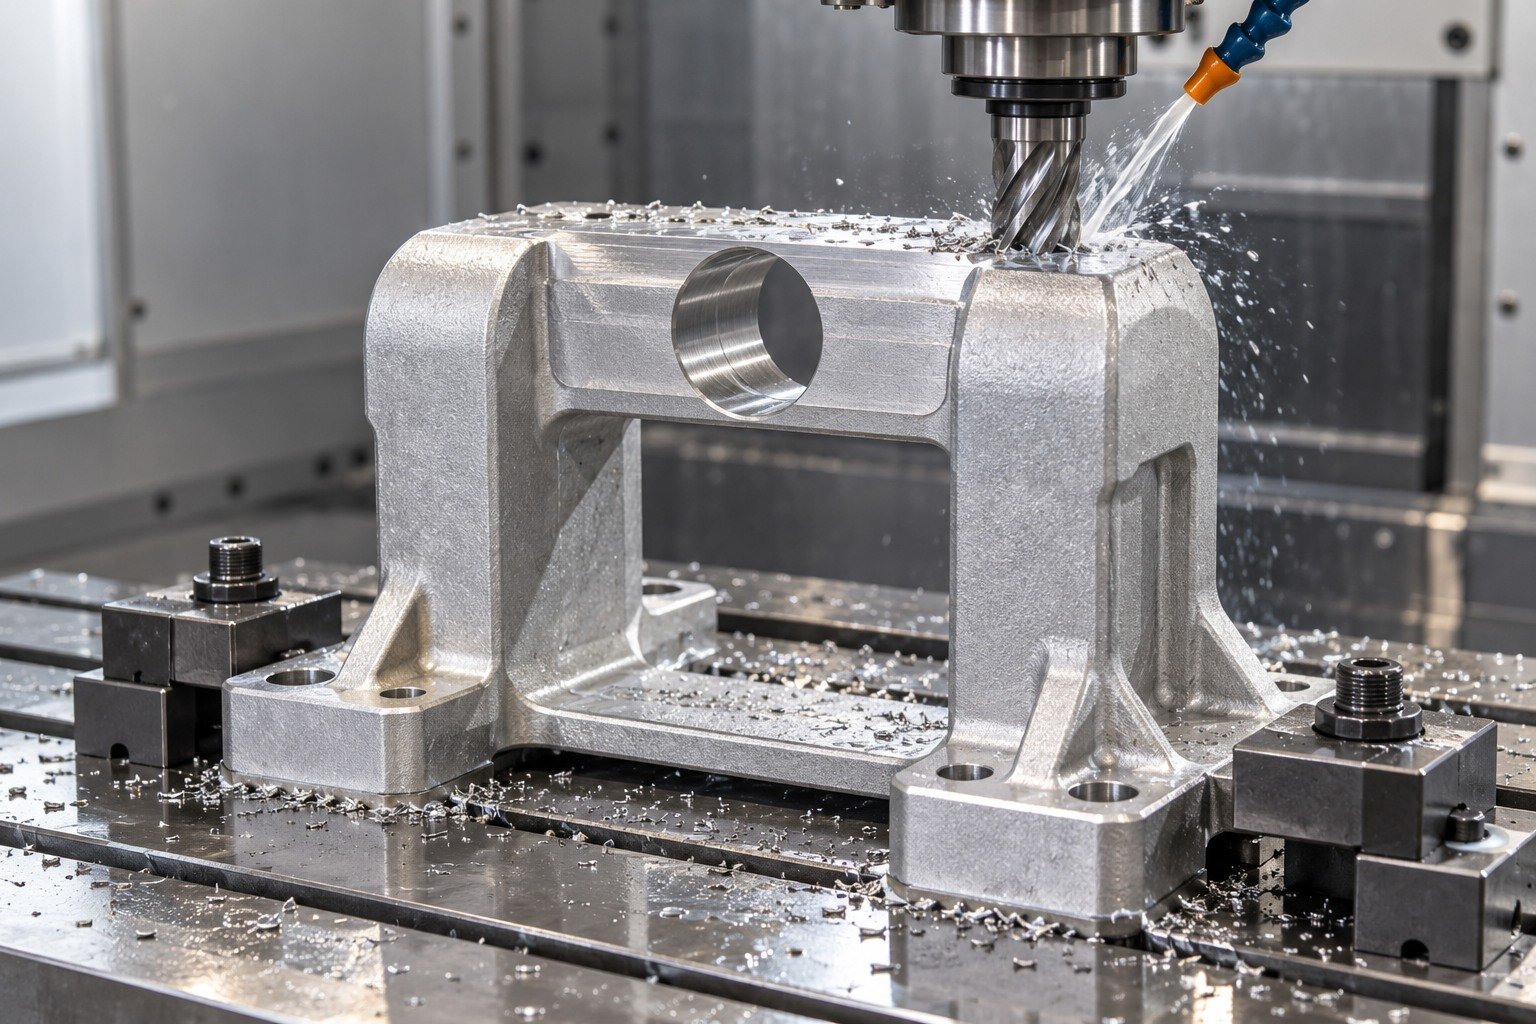
Specify the casting route, supplied state, usable stock and final coating requirements. Agree final inspection after the last dimension-changing operation.
| Your fit | What to define |
|---|---|
| Working interface | Crossbar bore, foot datums, columns and mating shaft. |
| Your route | Casting product, usable stock and supported machining. |
| Your approval | Free or installed measurement state, finish and receiving records. |
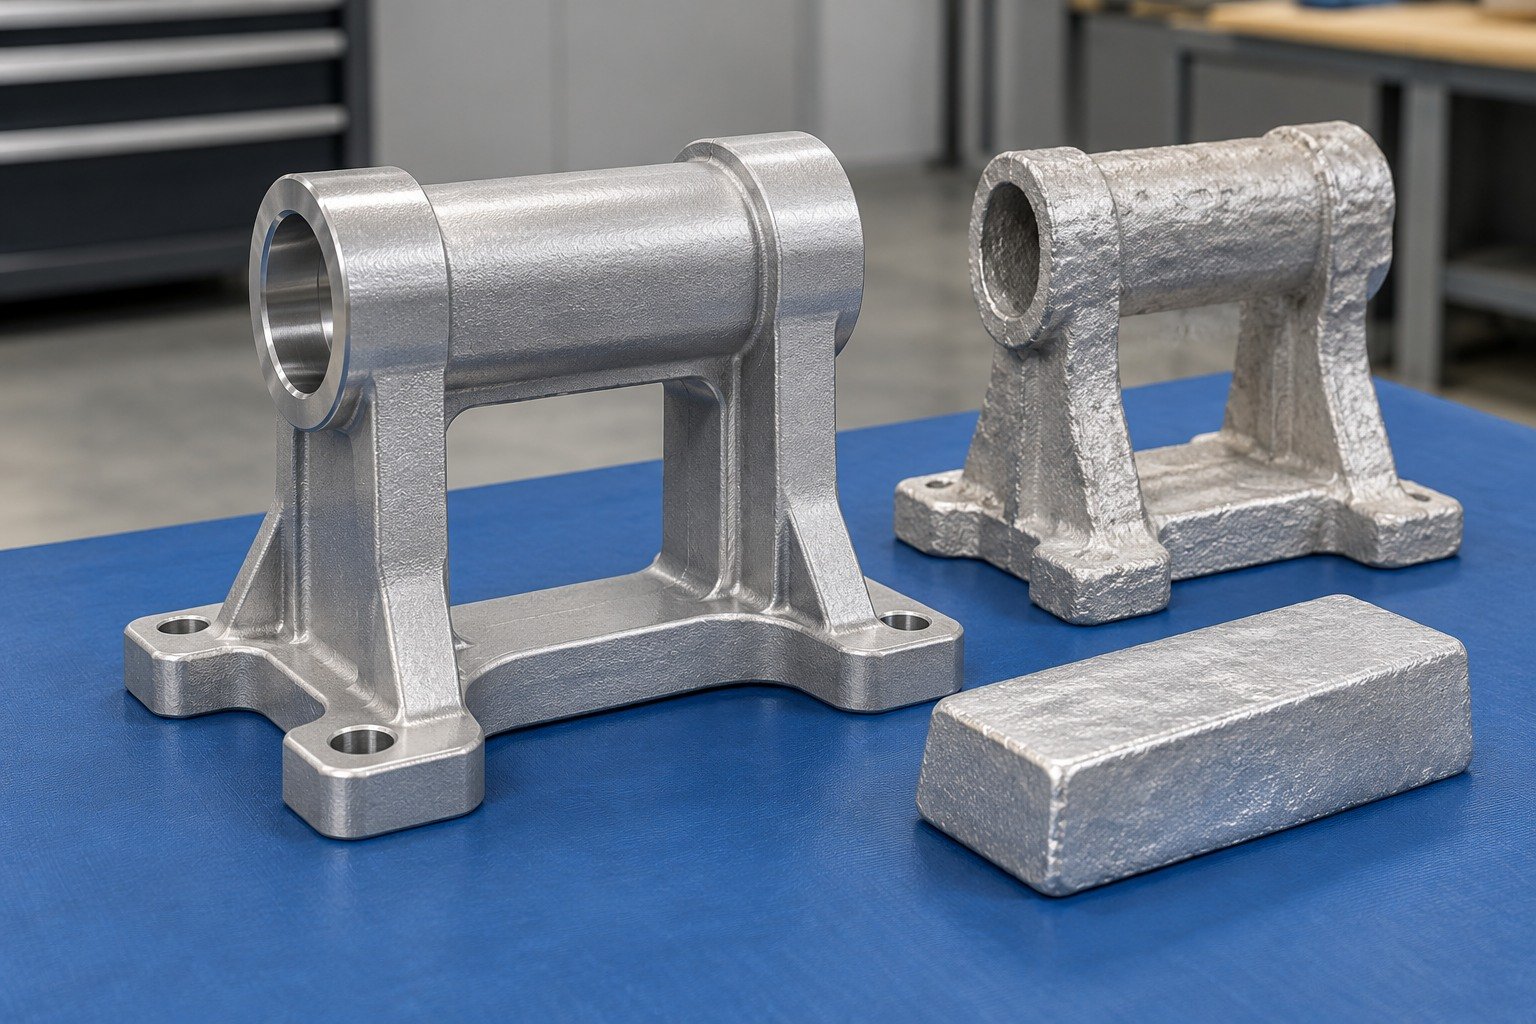
For your ZA-12 machined parts, identify the material records, final dimensions, accepted edges, cleanliness and individual protection.
| Your fit | What to define |
|---|---|
| Working interface | Crossbar bore, foot datums, columns and mating shaft. |
| Your route | Casting product, usable stock and supported machining. |
| Your approval | Free or installed measurement state, finish and receiving records. |
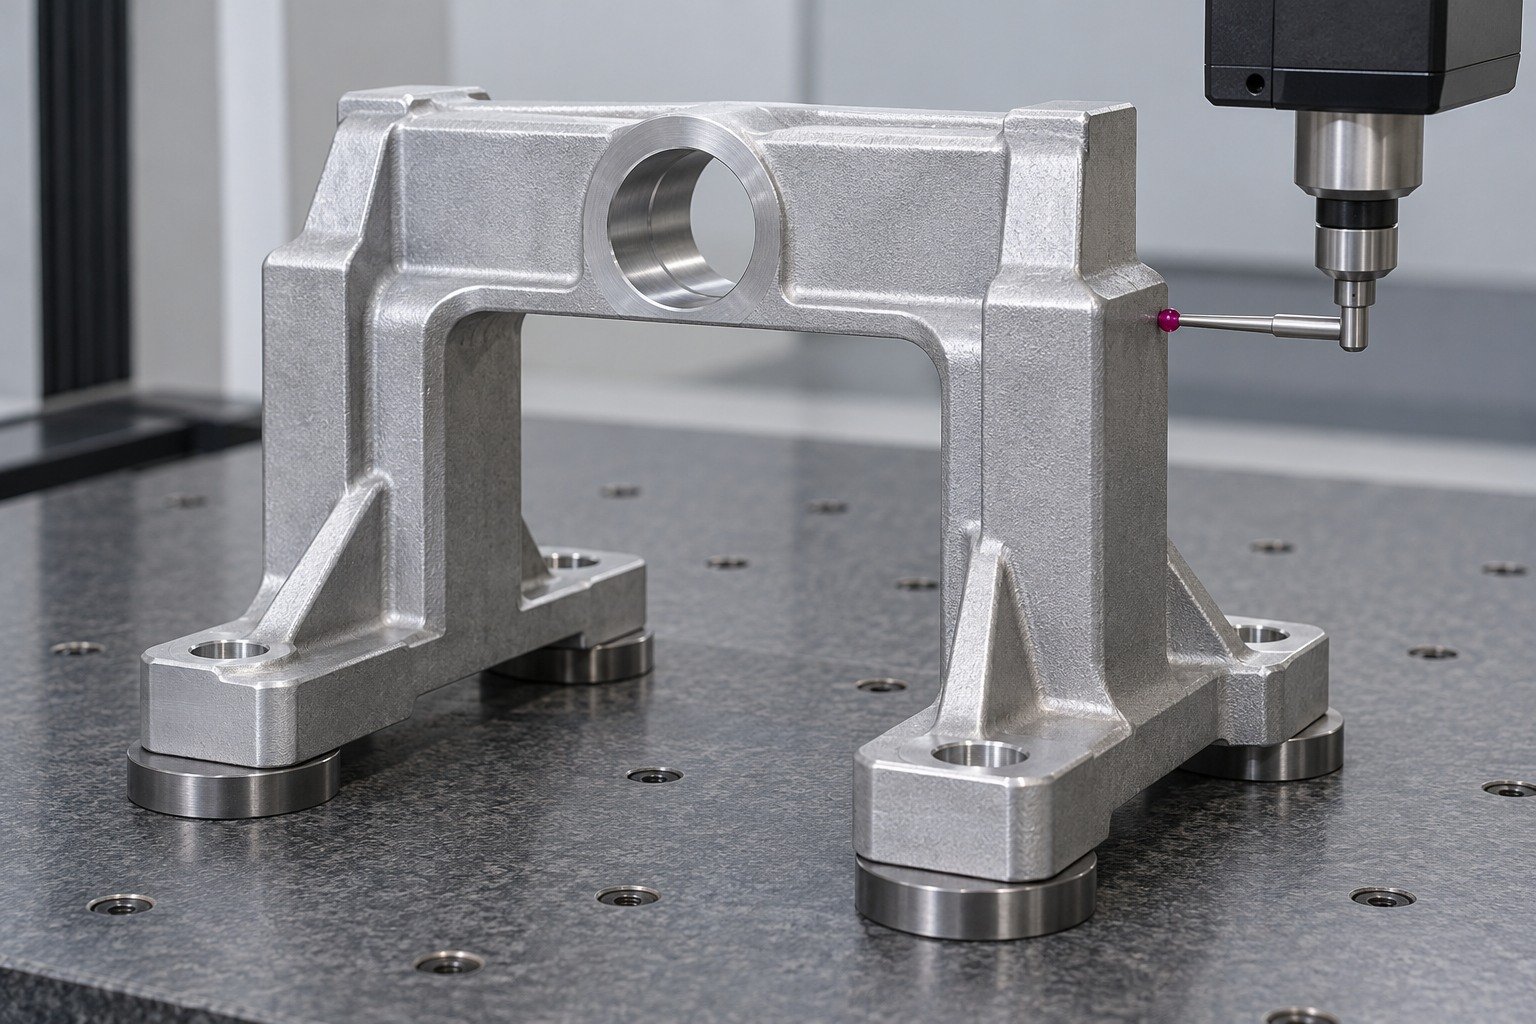
For your pump cover, define port-boss access, sealing lands, central bore and perimeter mounting relationship. Agree any leak test separately. Review custom ZA-12 pump covers against the controlled assembly.
| Your fit | What to define |
|---|---|
| Working interface | Central bore, service bosses, sealing land and bolt pattern. |
| Your route | Casting product, usable stock and supported machining. |
| Your approval | Free or installed measurement state, finish and receiving records. |

For your ZA-12 machining review, show usable stock, supported datums, cutter access and the final surfaces that determine assembly fit.
| Your fit | What to define |
|---|---|
| Working interface | Central bore, service bosses, sealing land and bolt pattern. |
| Your route | Casting product, usable stock and supported machining. |
| Your approval | Free or installed measurement state, finish and receiving records. |
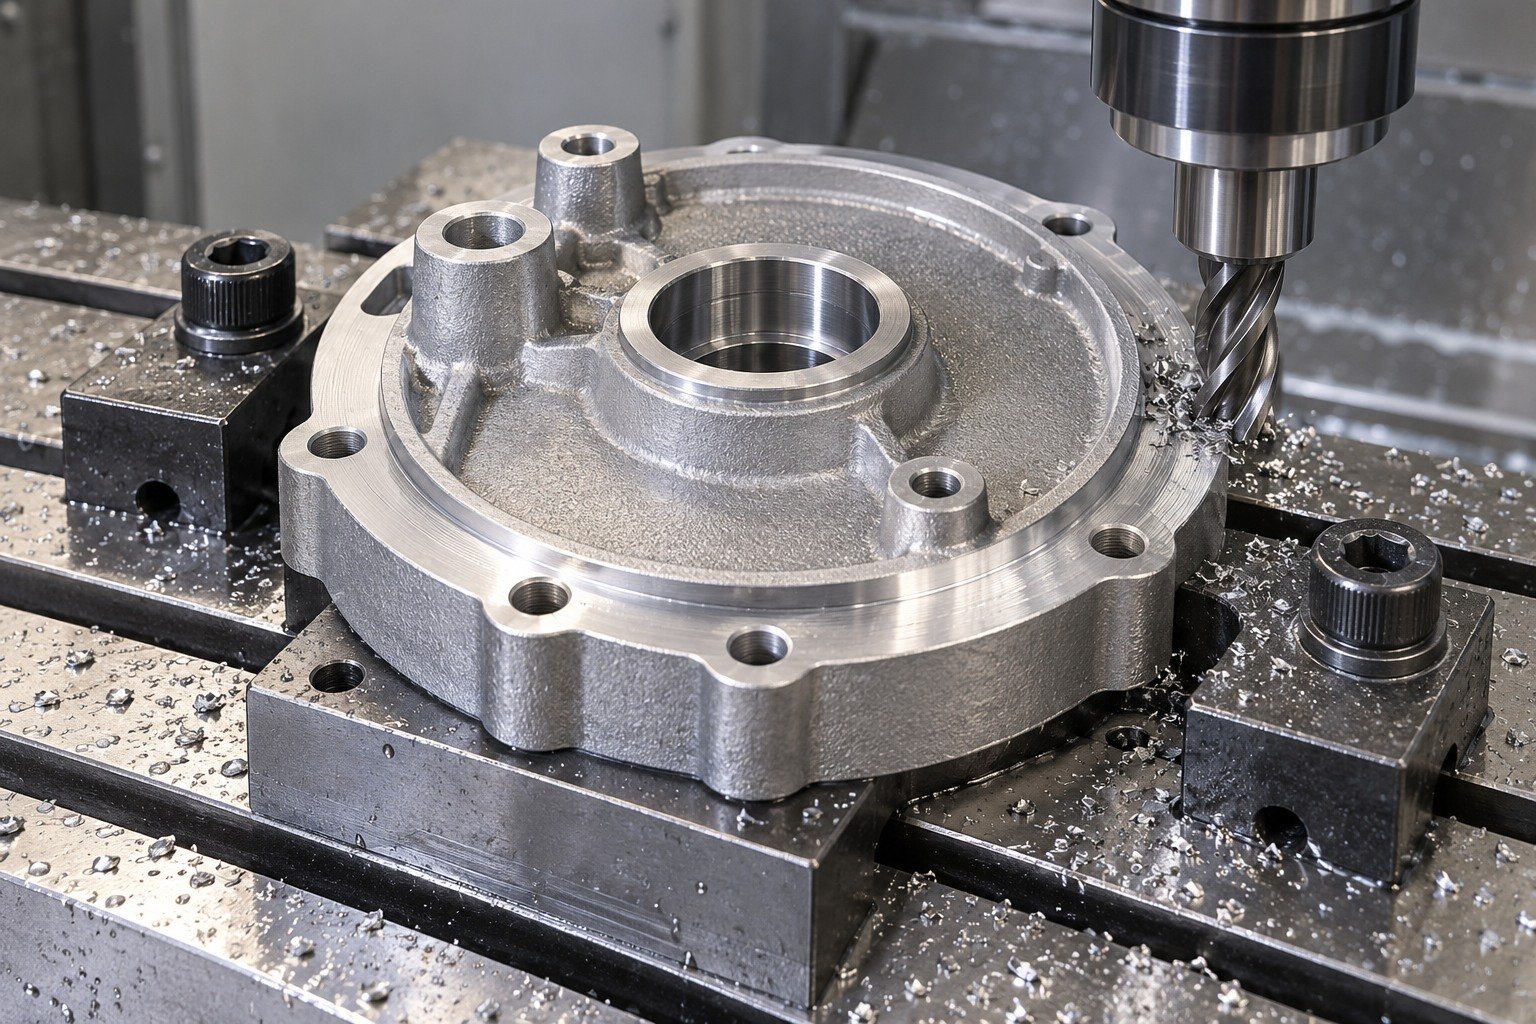
Specify the casting route, supplied state, usable stock and final coating requirements. Agree final inspection after the last dimension-changing operation.
| Your fit | What to define |
|---|---|
| Working interface | Central bore, service bosses, sealing land and bolt pattern. |
| Your route | Casting product, usable stock and supported machining. |
| Your approval | Free or installed measurement state, finish and receiving records. |
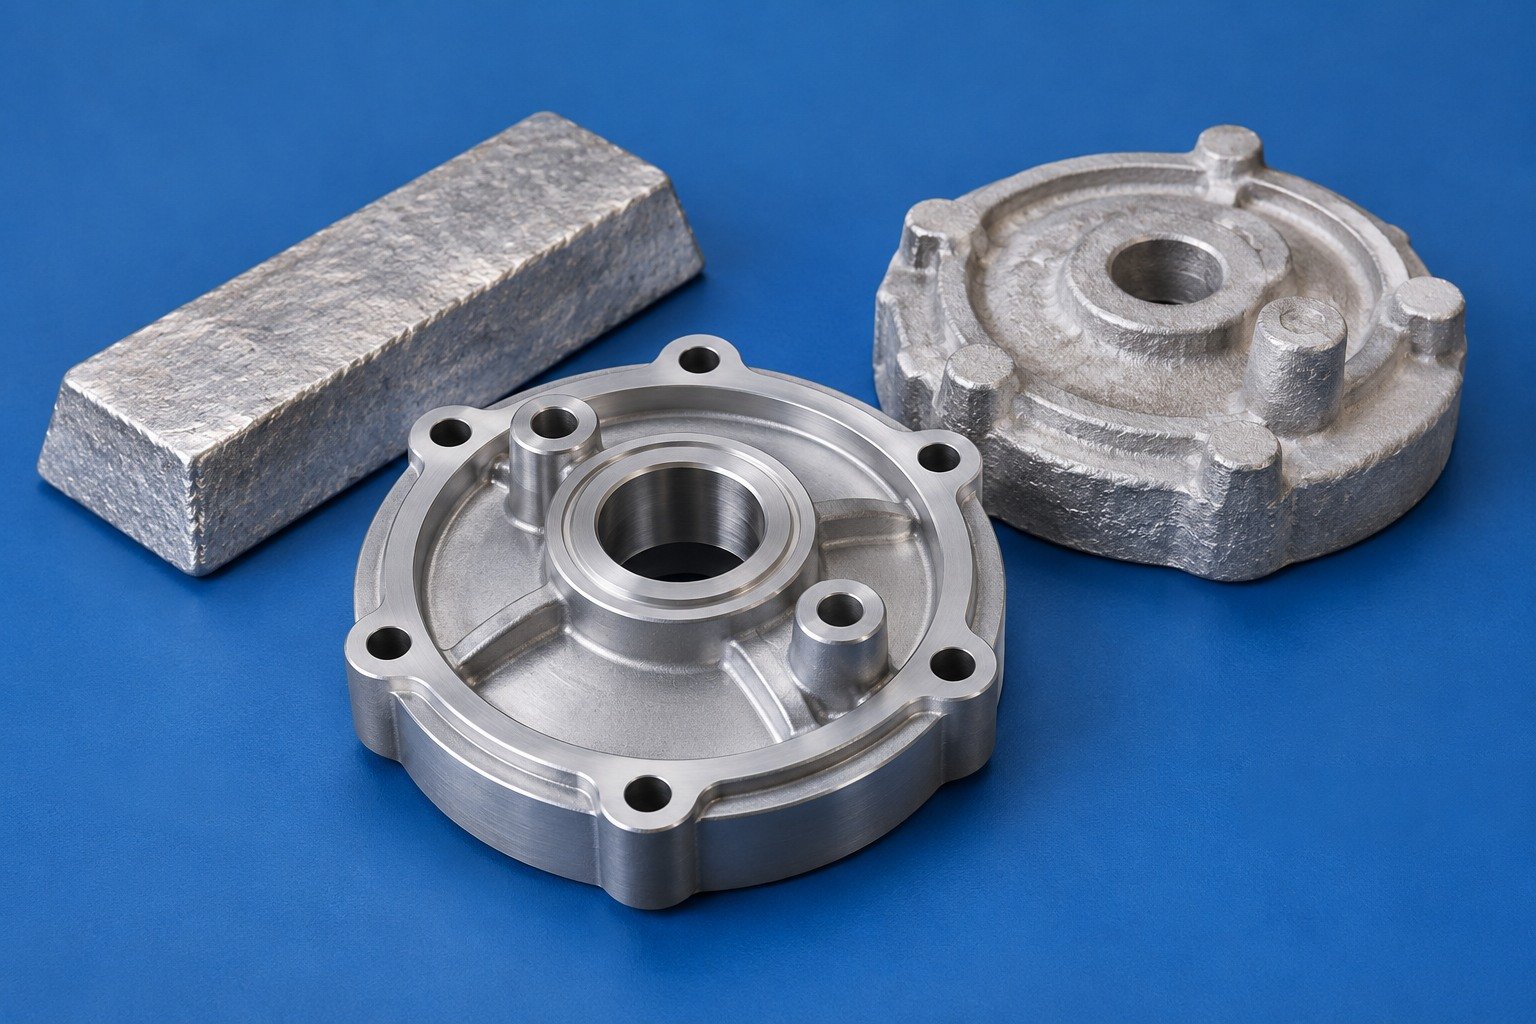
For your ZA-12 machined parts, identify the material records, final dimensions, accepted edges, cleanliness and individual protection.
| Your fit | What to define |
|---|---|
| Working interface | Central bore, service bosses, sealing land and bolt pattern. |
| Your route | Casting product, usable stock and supported machining. |
| Your approval | Free or installed measurement state, finish and receiving records. |
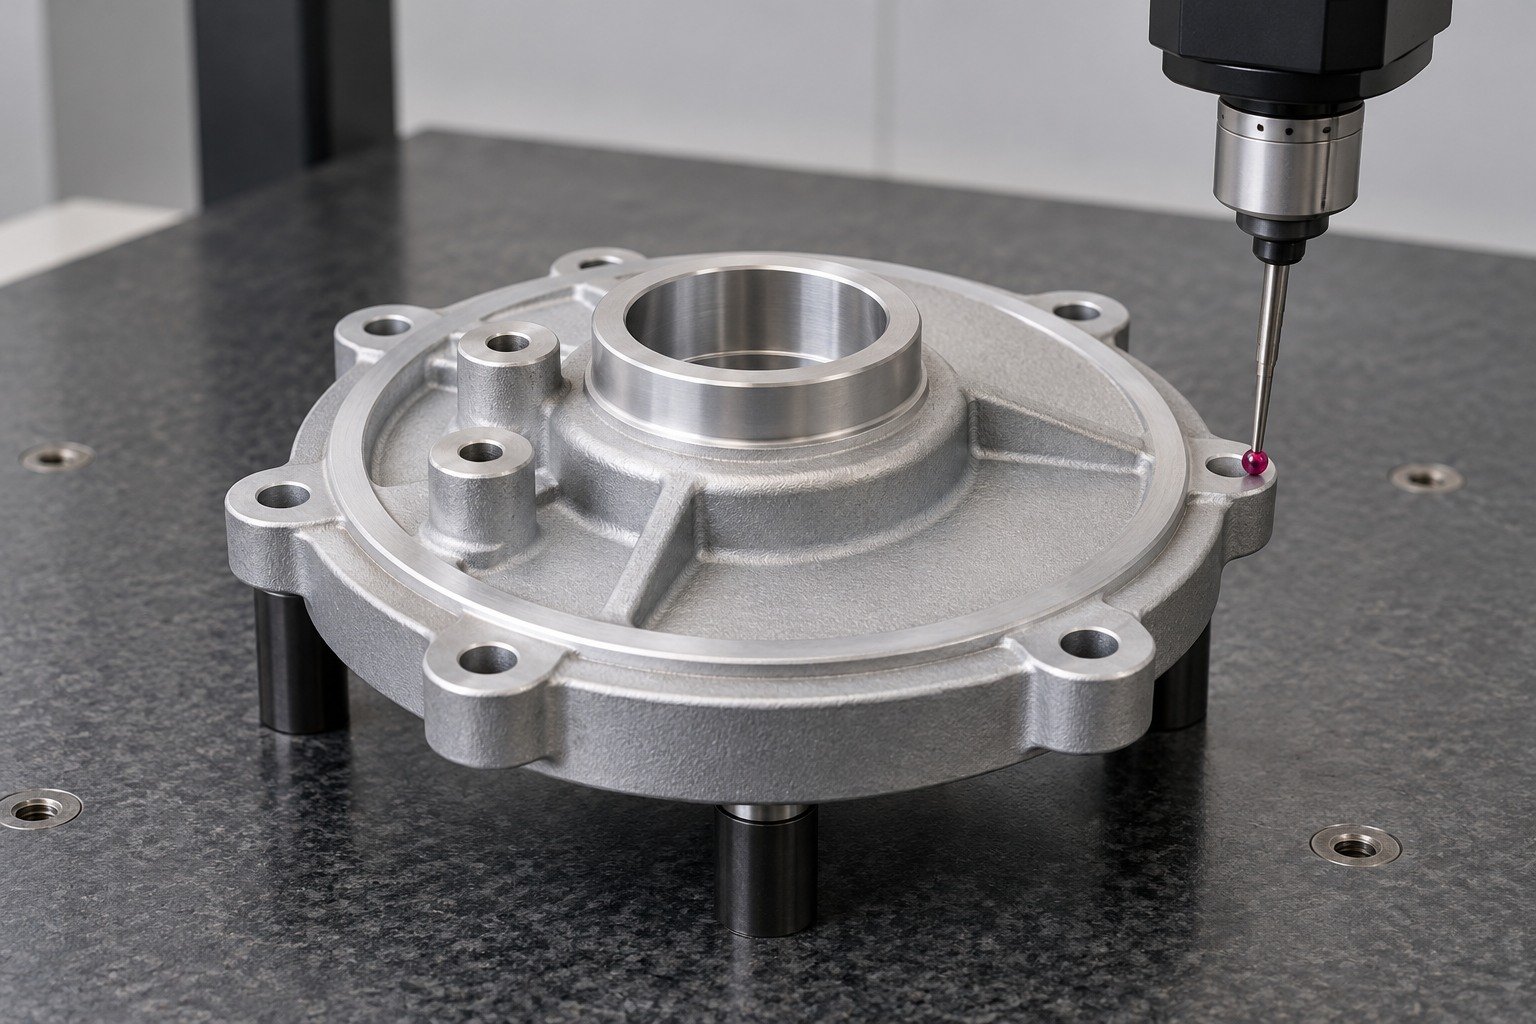
For your ZA-12 machining allowance review, identify where cast stock must clean up and how each critical feature is supported.

Connect bore length, outer land and flange relationship to the supported setup.
Review the Process →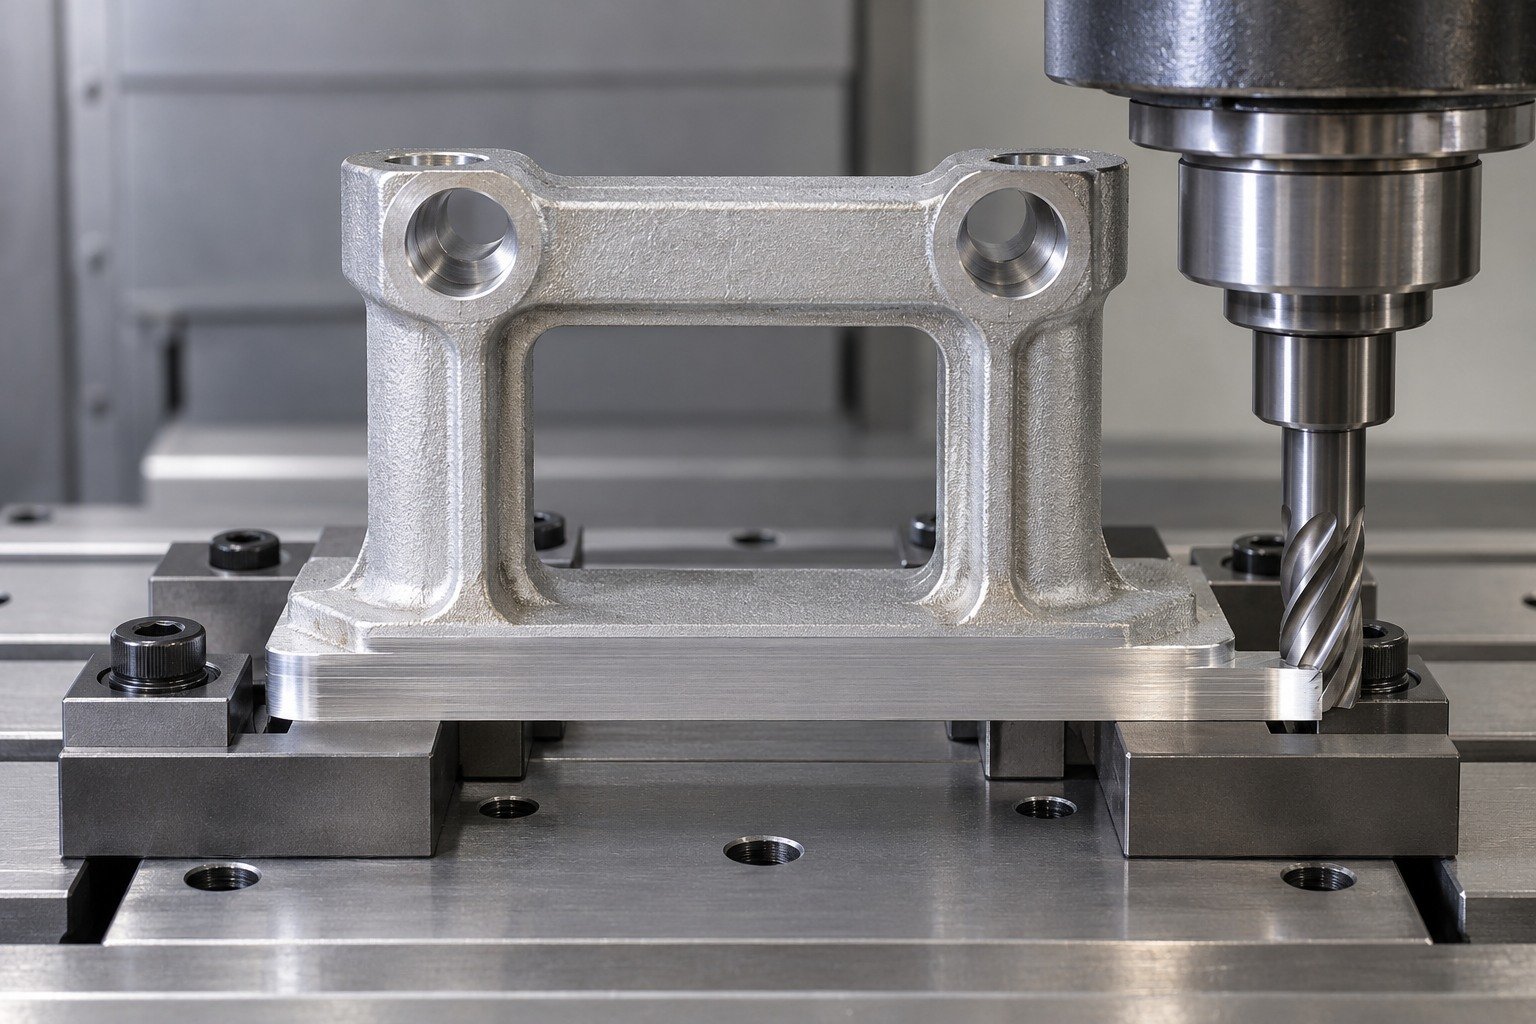
Machine foot datums with support around the crossbar and lower opening.
Review the Process →
Define backed drilling, port access and accepted internal edges.
Review the Process →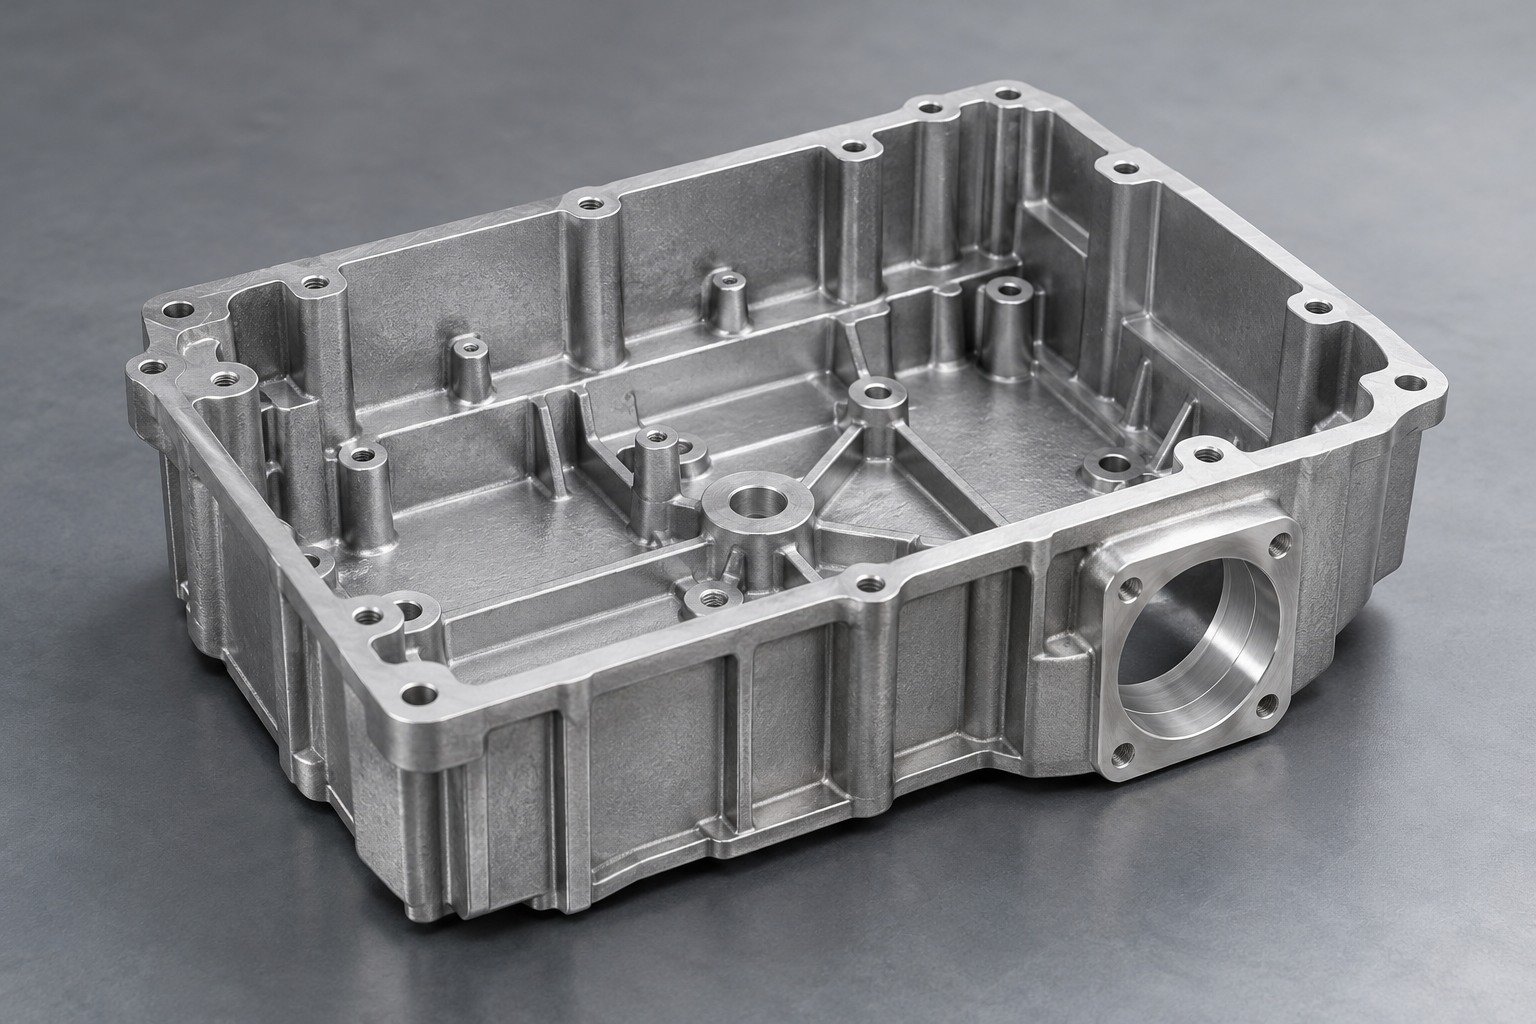
Connect the side port and sealing land to the agreed casting and machining route.
Review the Process →ZA-12 zinc aluminum alloy and ZA12 alloy are names used in purchasing. Your ZA-12 properties and ZA-12 composition review still needs a product standard, casting route and agreed final state.
| Element | Casting reference | Ingot reference |
|---|---|---|
| Al | 10.5–11.5 | 10.8–11.5 |
| Cu | 0.5–1.2 | 0.5–1.2 |
| Mg | 0.01–0.03 | 0.02–0.03 |
| Fe | ≤0.075 | ≤0.05 |
| Pb | ≤0.006 | ≤0.005 |
| Cd | ≤0.006 | ≤0.005 |
| Sn | ≤0.003 | ≤0.002 |
| Zn | Balance | Balance |
Selected NADCA 2021 casting data and Eastern Alloys ASTM B240 ingot reference. Verify ordered standard and revision; do not use an ingot range as a finished-casting acceptance range. This is not your material-lot report.
| Callout | Your product review |
|---|---|
| ZP12 / ZP1110 | Casting reference associated with ZA-12. |
| ZnAl11Cu1 | Alloy symbol; approve the complete ordered requirements. |
| ZL12 / ZL1210 | IZA prototype-alloy reference; distinguish from ZP1110. |
| ZA-12 cold chamber die casting | Die-casting route review, with actual stock and geometry. |
| ZA-12 gravity casting | Review sand or permanent-mold routes separately. |
ZA-12 density is typically 6.0 g/cm³ in the selected Eastern Alloys die-cast data. A prototype from a different casting route does not automatically reproduce production properties.
Common scale 0–12
Common scale 0–3
Selected product references. Chemistry differences do not rank machining time, part price, porosity or bearing performance. Agree the same product route and acceptance when comparing materials.
NADCA casting data ↗ Eastern Alloys ZA-12 ↗ Casting-route comparison ↗ IZA prototype product names ↗
Define the assembly inputs before repeating quantities.
For your ZP1110 die casting review, confirm the cold-chamber route. ZA-12 sand casting and ZA-12 permanent mold casting need their own stock, tooling and acceptance review.
Define shaft, housing and working surface.
Agree stock, support and lubrication access.
Inspect the defined final state.
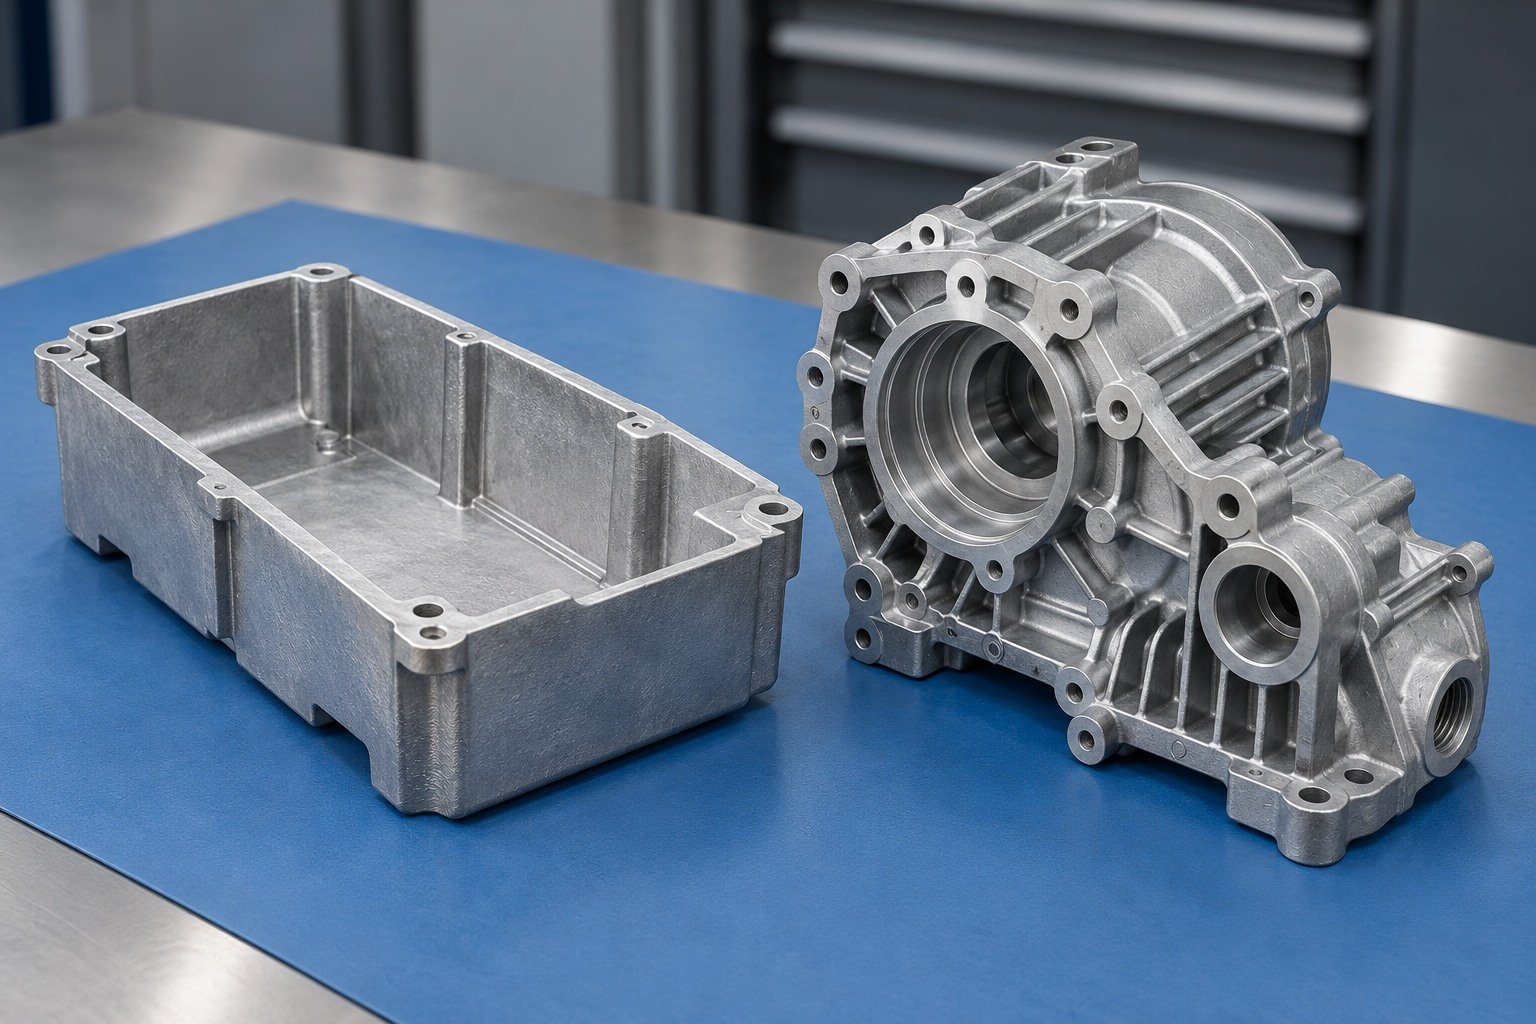
Define bore, outer locating land, mating part and free or installed clearance. Include oil-port and groove requirements where applicable.
Define shaft, housing and working surface.
Agree stock, support and lubrication access.
Inspect the defined final state.
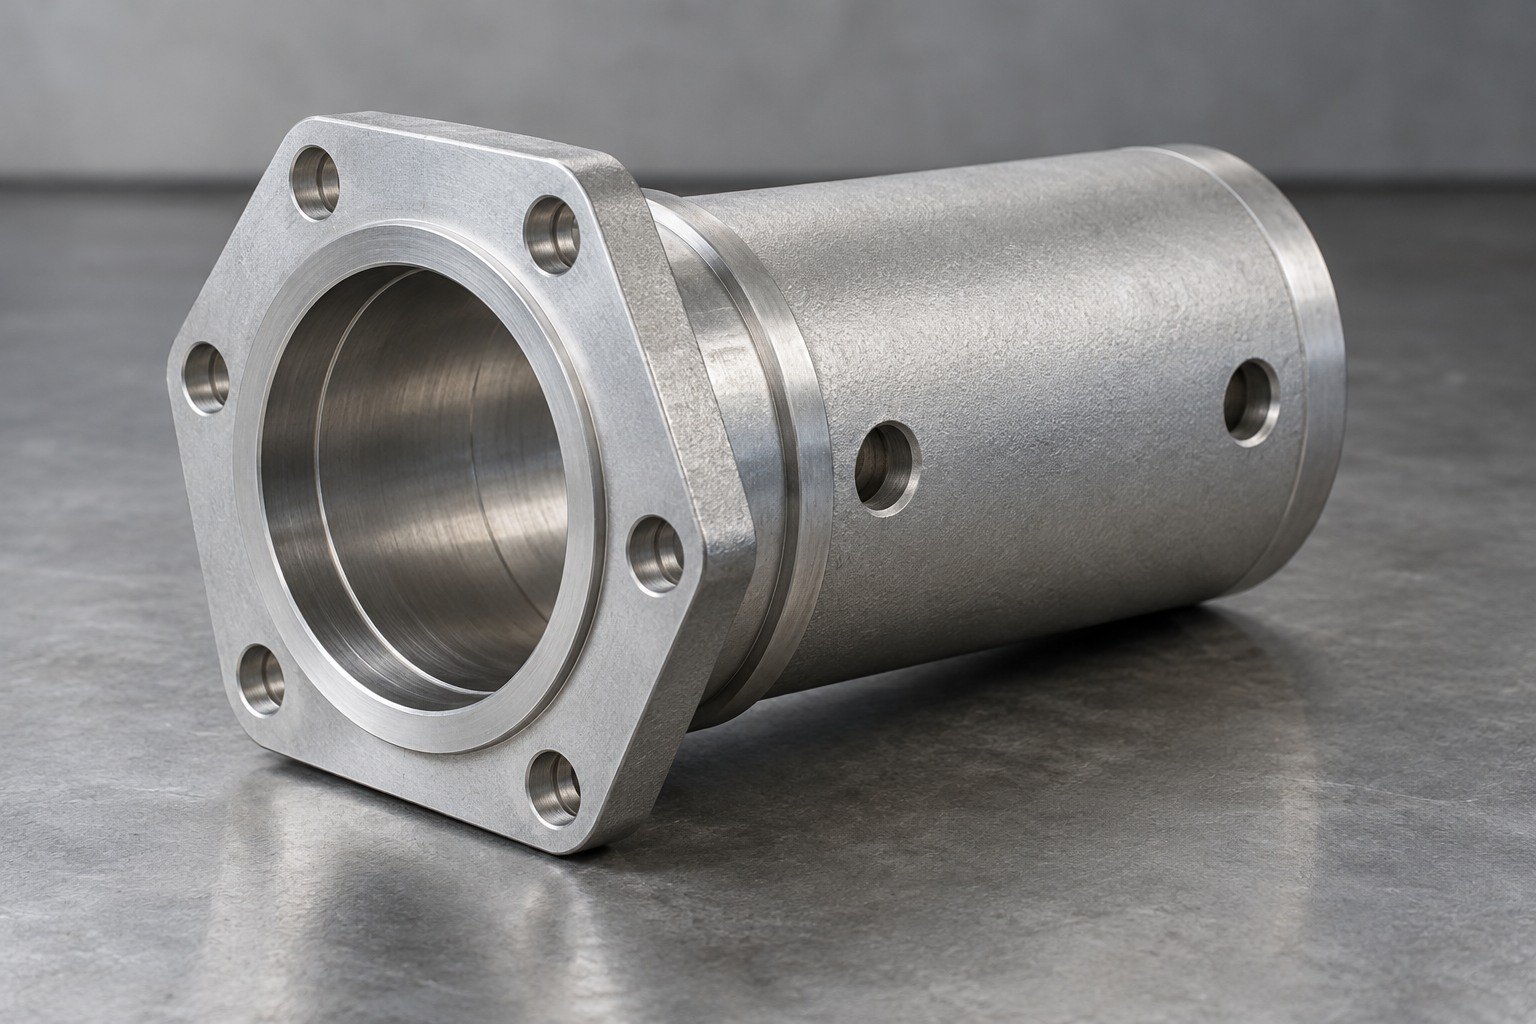
For ZA-12 creep resistance, define sustained load, temperature, duration, speed and lubrication. A room-temperature property does not approve long-term assembly duty.
Define shaft, housing and working surface.
Agree stock, support and lubrication access.
Inspect the defined final state.
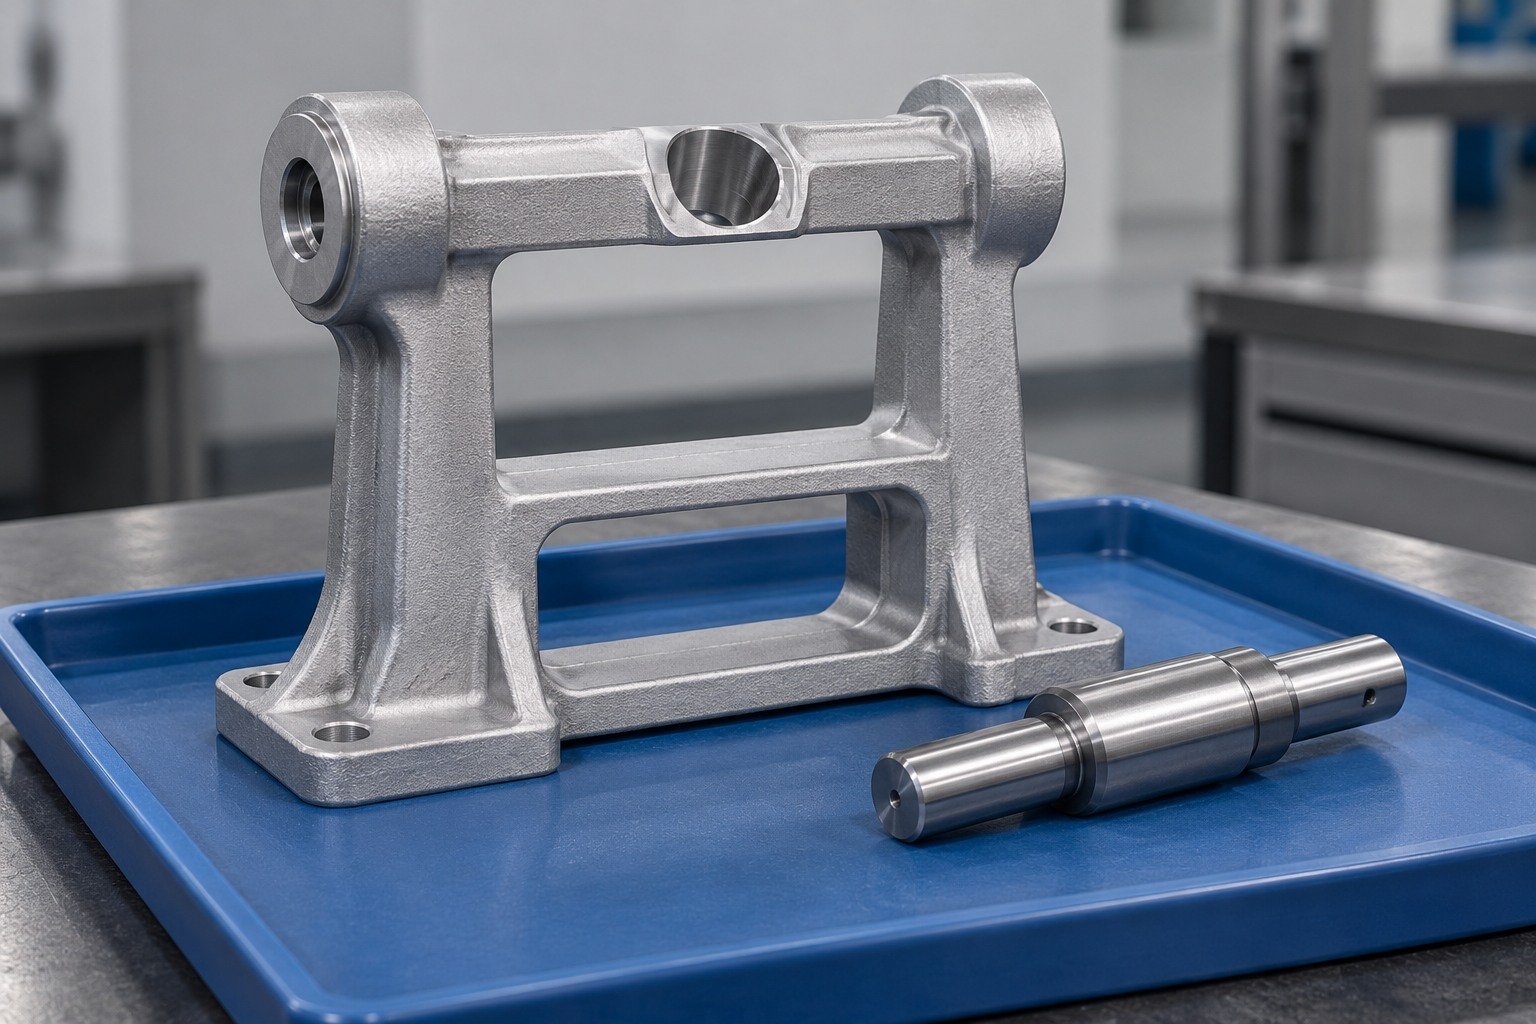
Specify thread engagement, blind-hole depth, port entrances and burr acceptance. Show the sealing and bearing lands that must remain intact.
Define shaft, housing and working surface.
Agree stock, support and lubrication access.
Inspect the defined final state.
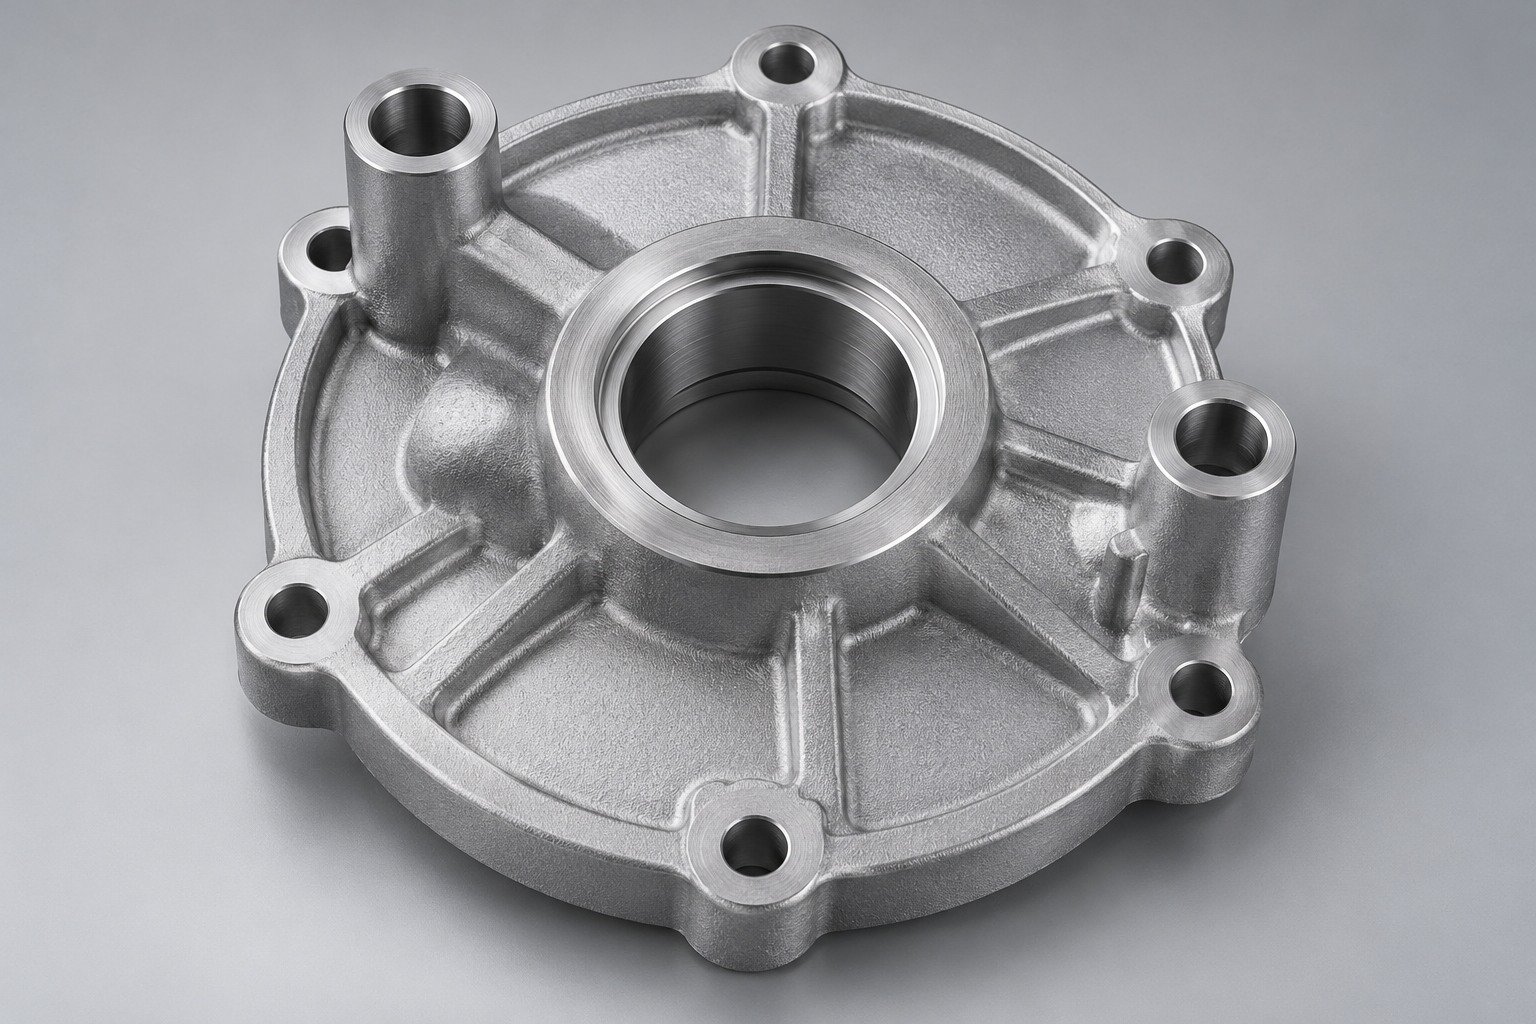
For ZA-12 plating, agree preparation, coating system, appearance and adhesion acceptance, masks and final dimensions.
Define shaft, housing and working surface.
Agree stock, support and lubrication access.
Inspect the defined final state.
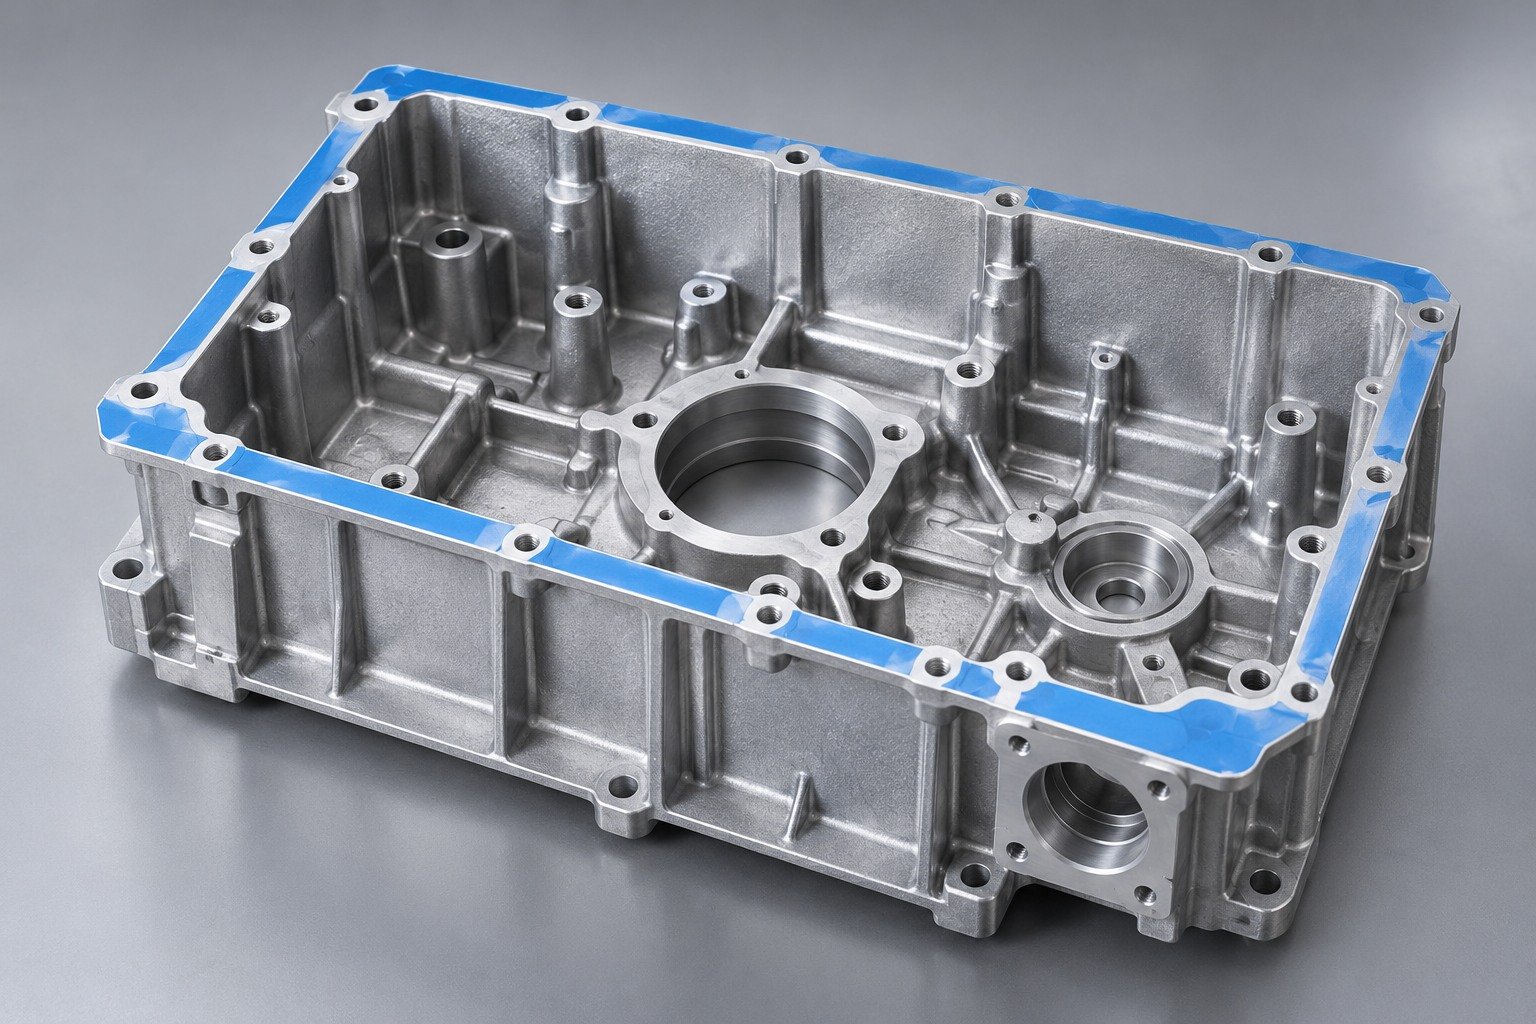
Your ZA12 die casting services review should agree lot identity, exact product route, final inspection state, sampling and any separate functional test.
Define shaft, housing and working surface.
Agree stock, support and lubrication access.
Inspect the defined final state.
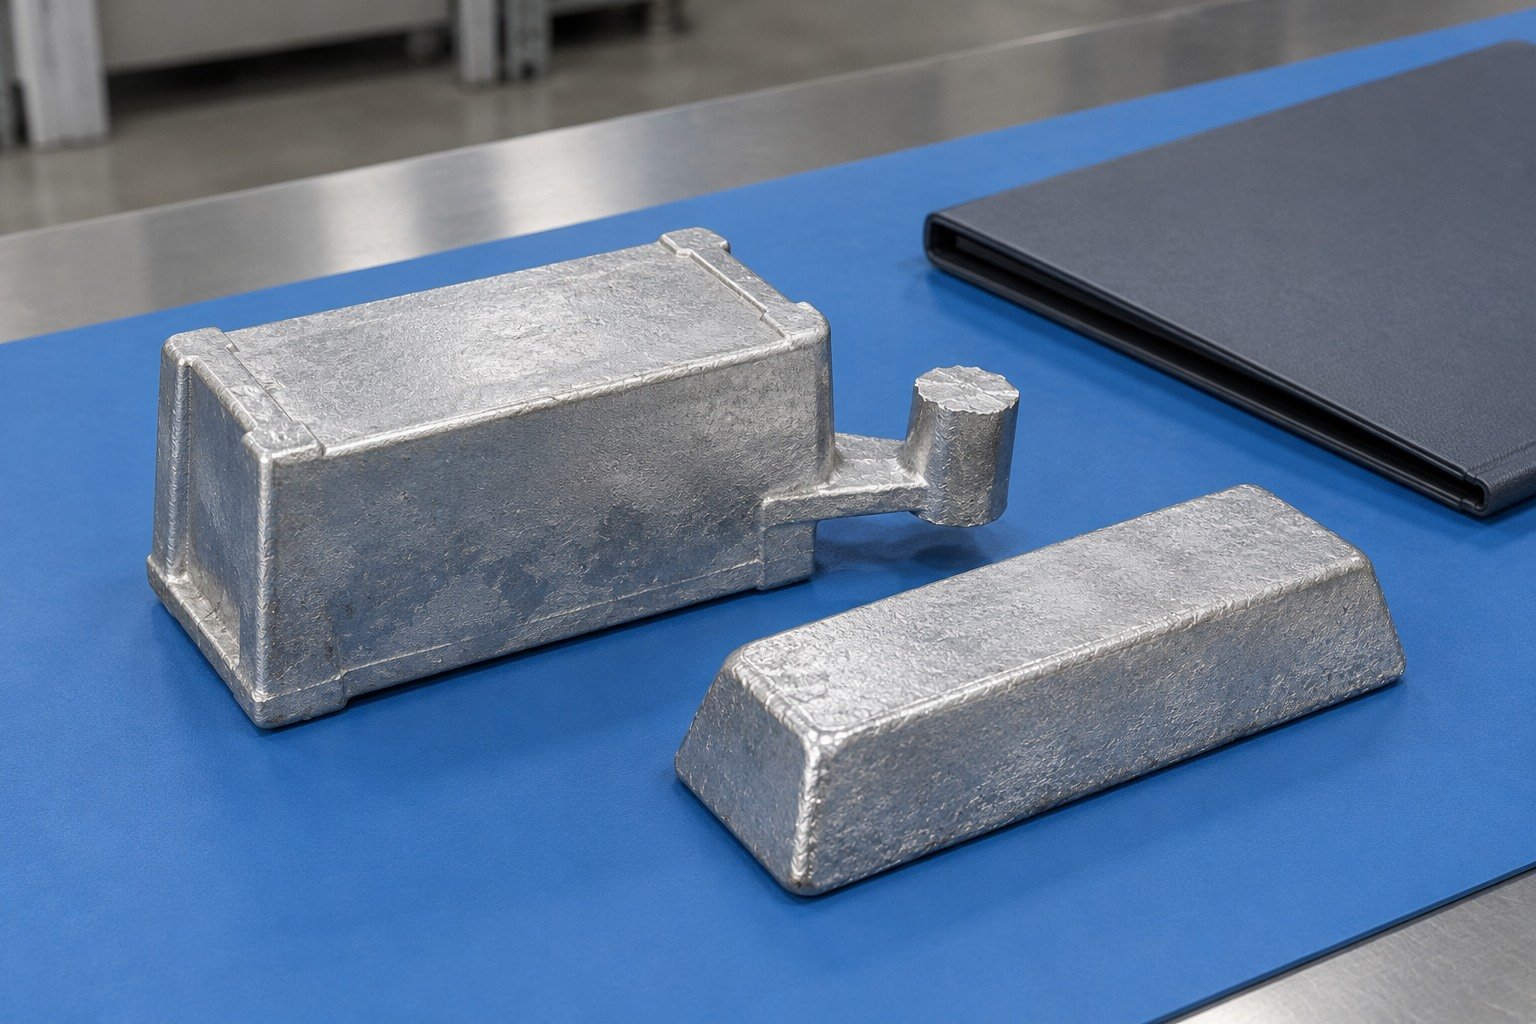
Product identity and ordered requirements.
Complete route and locating relationship.
Final working surfaces and evidence.
Identify the ZA-12 grade, ordered standard, revision, casting route, stock, lot identity and required records.
Approve flange, bore, foot and port relationships after the complete route. A first casting sample and a first finished-route sample answer different questions.
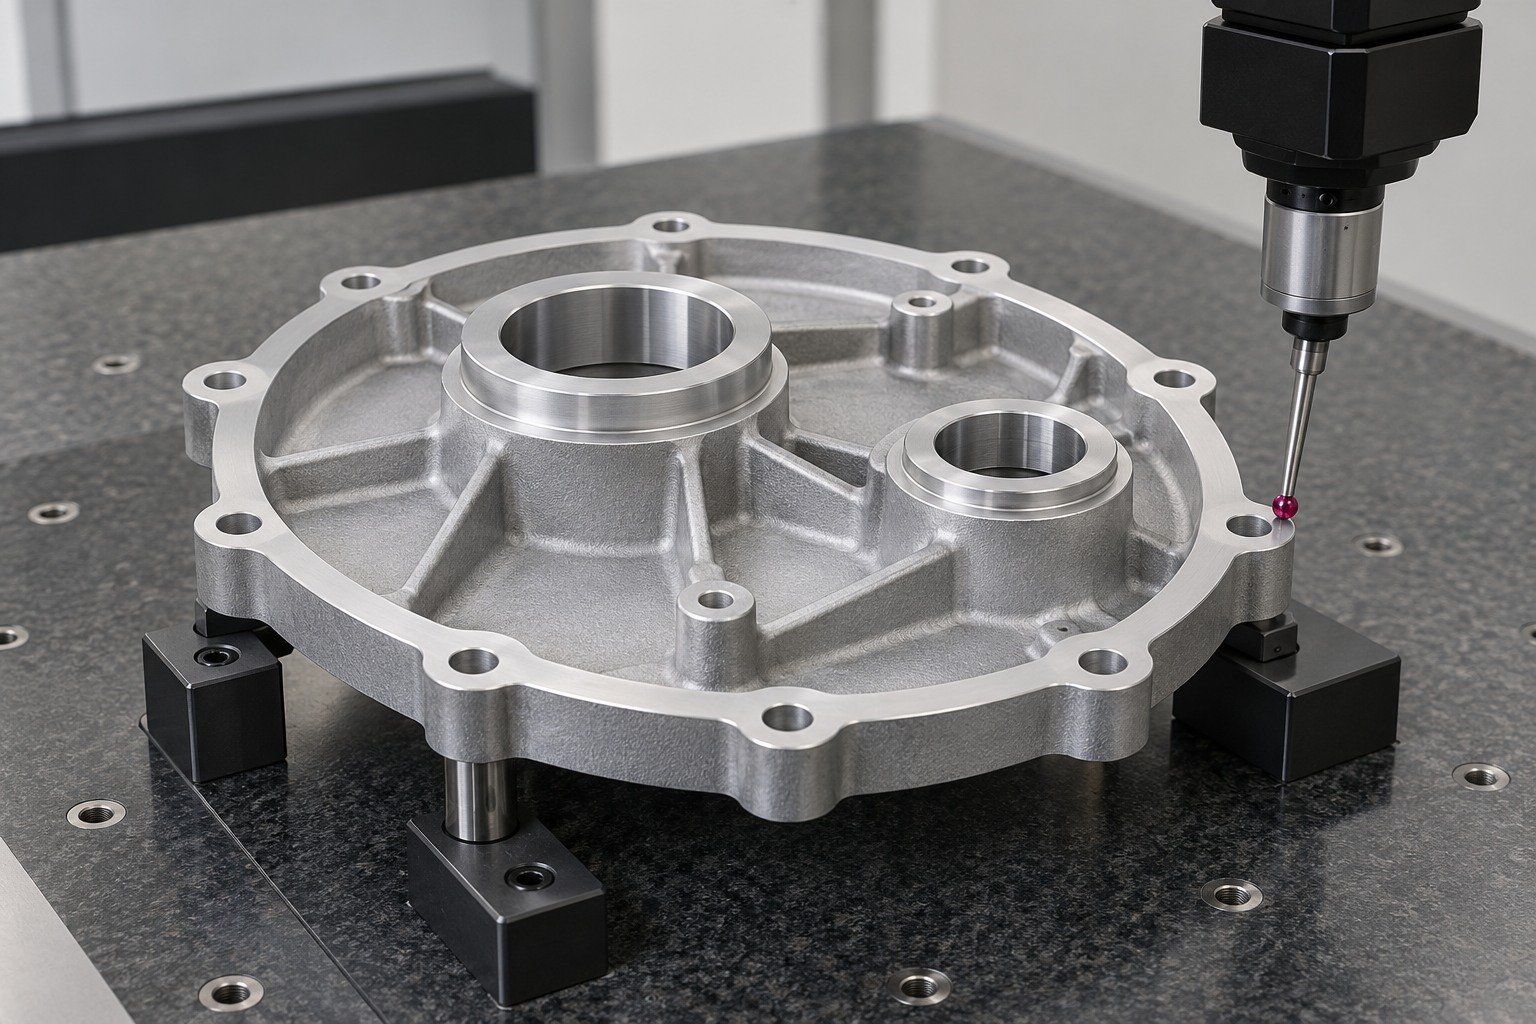
Verify the final sleeve bore, flange, port or frame mounting pattern in the measurement state specified on your drawing.

Agree protection, cleanliness, lot identity and receiving documents for the actual mating surfaces.
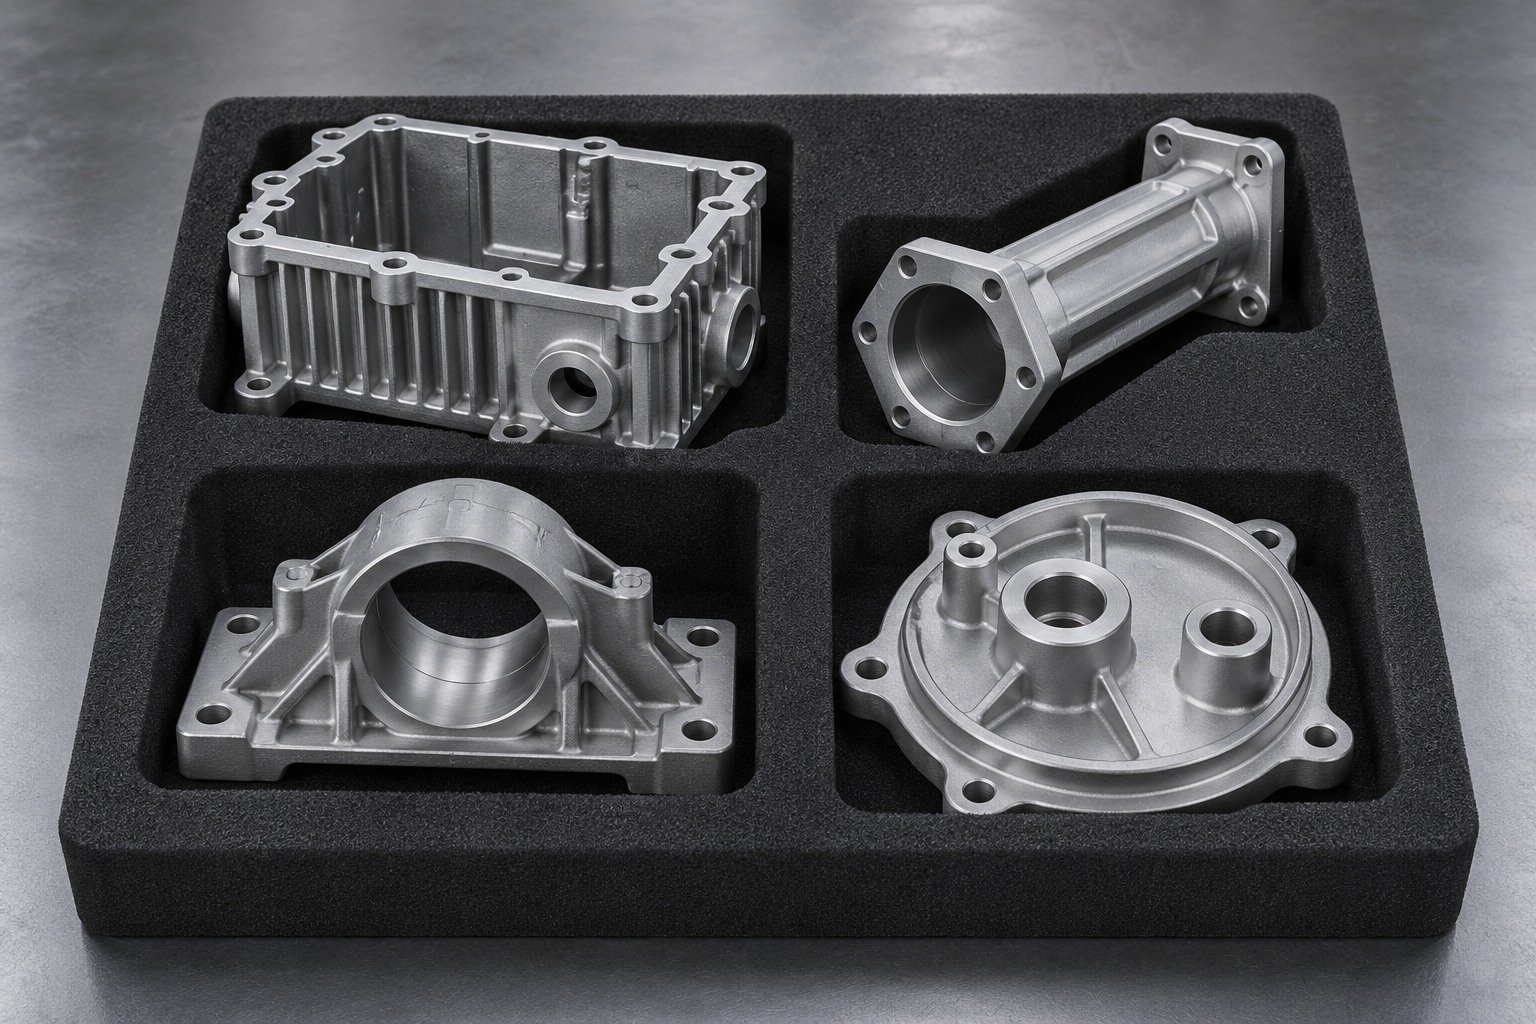
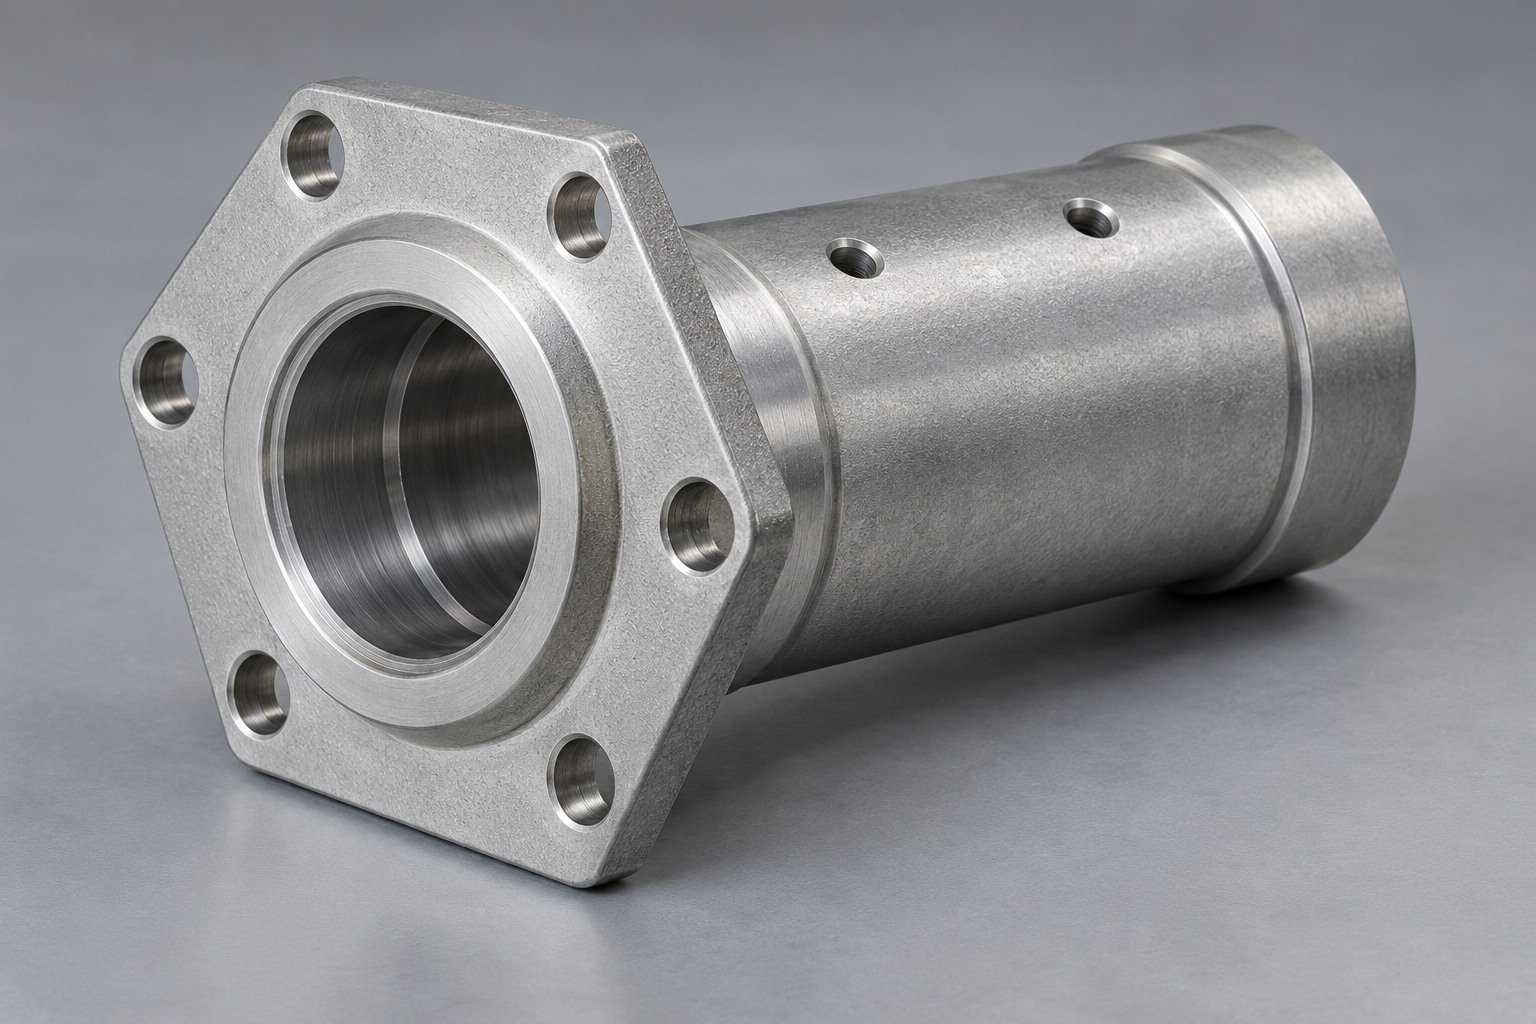
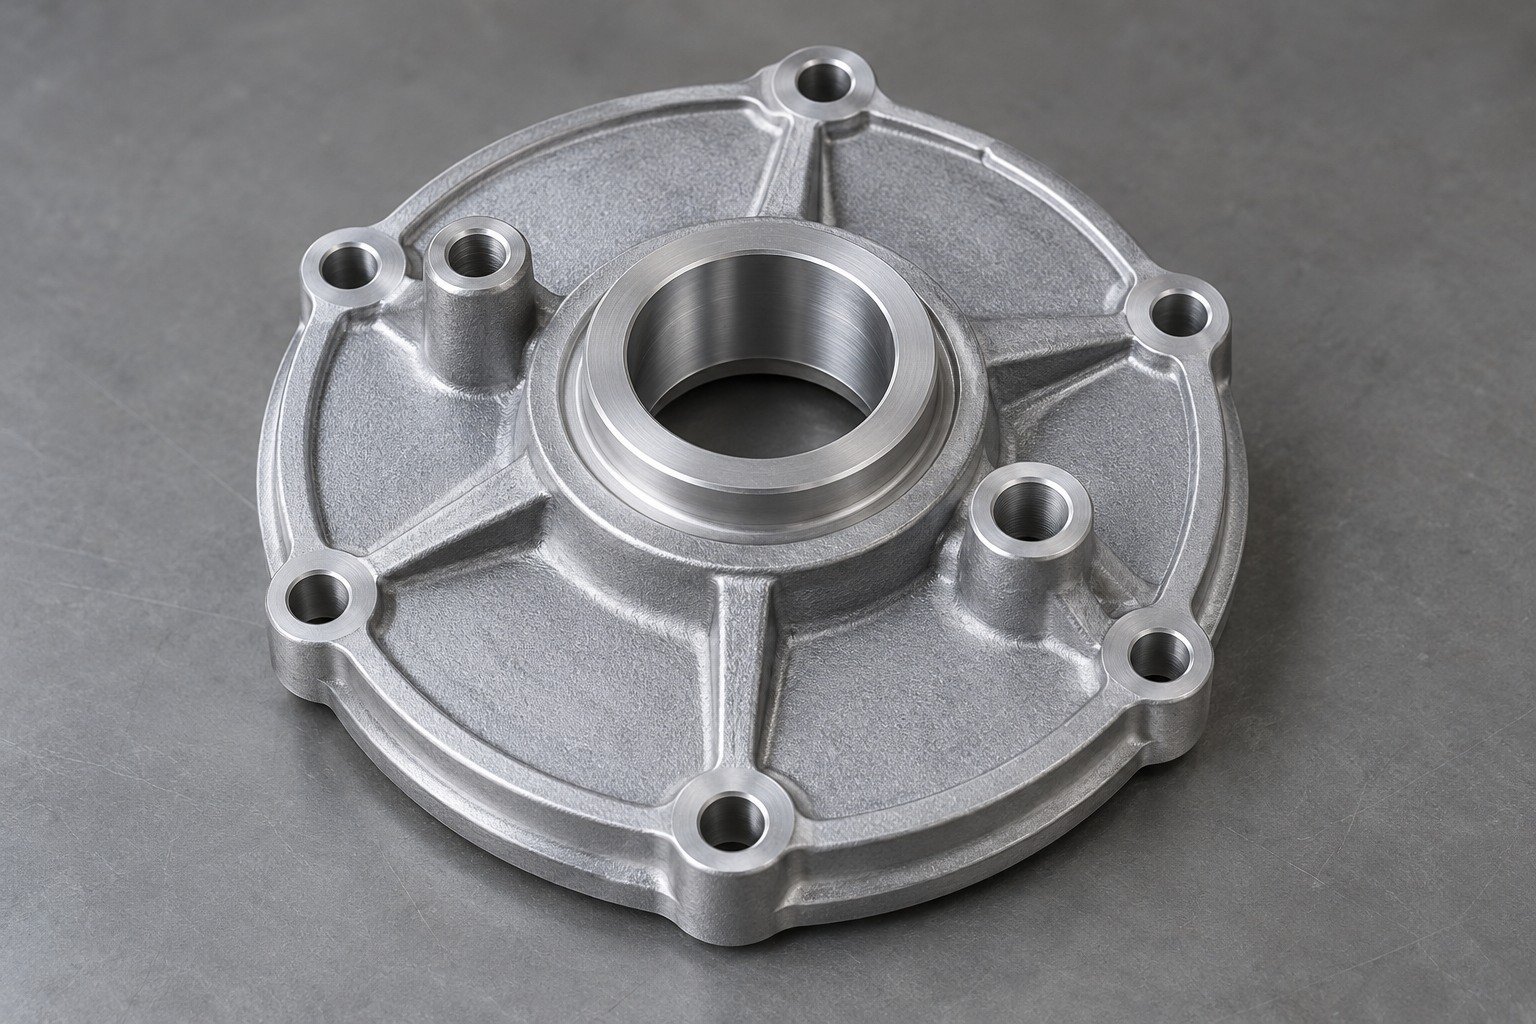
Agree visible marks, finish preparation, coating acceptance and protected delivery. Check dimensions in the final surface state.
Surface Finishing →| Your decision | What to confirm |
|---|---|
| Die casting or gravity route | Agree stock, geometry, tooling and inspection separately. |
| Prototype and production | Do not carry one route’s properties into another without review. |
| Bearing interface | Define load, speed, lubrication, mating material and final clearance. |
| Material change | Obtain drawing-authority approval and receiving criteria. |
ZA-12 material identity does not establish pressure tightness, bearing life or the final load capacity of your part.
Compare Zinc Alloys →
Connect China manufacturing with Dallas-area coordination for drawing review, sample decisions and delivery requirements.
Your ZA-12 casting quote should identify the same route, drawing revision, usable stock and final acceptance. Compare tooling and repeat demand on that basis.
ZP12 / ZP1110 and ZnAl11Cu1 are common casting references associated with ZA-12. Retain the complete specification and revision. IZA lists ZL12 / ZL1210 separately for prototype alloys.
Yes. Review the actual cold-chamber casting route, geometry, tooling and usable machining stock with your quote. Do not automatically apply a ZA-8 hot-chamber route.
Yes. Identify locating support, usable allowance, bore and port access, accepted burrs and the final condition inspected after machining and finishing.
Provide CAD and controlled drawing, grade and product standard, casting route, quantities, load and temperature, final finish, free or installed fit and receiving records.
Review load, speed, temperature, lubrication, mating material and installed clearance. Request appropriate duty data and acceptance; alloy identity alone does not establish service life.
Review casting route, section layout, feeding or filling approach and agreed defect limits with the foundry. Identify critical bores or sealing surfaces and any separately required integrity test.
Specify cast versus machined features, datums, limits and final finish. Your quote confirms the reviewed geometry and inspection scope, without a universal tolerance promise.
Compare the actual route, material state and the property being tested. A prototype made by another casting process does not automatically reproduce die-cast mechanical behavior.





