Injection Molding
Tooling and molding for your repeat plastic parts.
From prototype to production, coordinated manufacturing solutions for your custom parts.
View All Services →
Precision parts for your tight tolerances and complex geometry.
Tooling and molding for your repeat plastic parts.
Metal casting options for your part and production volume.
Cutting, forming and welding for your fabricated parts.
Custom profiles for your section, length and finish requirements.
Finishes for your appearance, corrosion and wear requirements.
Sub-assemblies and final builds for your production program.
Production tooling built around your process and volume.
Prototype parts to check fit, function and design.
DFM, process planning and production support for your project.
Inspection, documentation, inventory and delivery planning for your program.
Choose air- or liquid-cooling components around your thermal and mechanical requirements.
Manufacturing support for your cold plates, manifolds and cooling assemblies.
Find components for your power electronics, energy, laser and telecom application.
Components for your electronic systems.
Start with your functional and quality requirements.
Build around your operating environment.
From prototype to production, review material performance, manufacturability and cost for your part.
Review grade, temper and finish for your metal parts.
 AluminumStrength, weight and machining›
 Stainless SteelCorrosion and finish requirements›
 Carbon & Alloy SteelDiscuss grade and heat treatment›
 Tool SteelDiscuss tooling and wear needs›
 TitaniumReview grade and part geometry›
 Copper & Brass & BronzeDiscuss conductivity and machining›
Match your polymer to function, process and environment.
 ABSReview enclosure and molding needs›
 Polycarbonate (PC)Discuss clarity and impact needs›
 Nylon (PA)Review moisture and wear conditions›
 POM / AcetalReview fit and sliding features›
 PEEKDiscuss operating conditions›
 PTFEReview friction and chemical exposure›
 ULTEM / PEIDiscuss thermal and electrical needs›
Confirm grade availability and application requirements.
 Silicone / LSRDiscuss flexible component needs›
 TPU / TPEReview flexibility and processing›
 EPDMReview weathering and chemical exposure.›
 NBRReview oil and fuel exposure.›
 FKMReview temperature and chemical exposure.›
 G10 / FR4Review insulation and laminate needs›
 CompositesReview stiffness, weight and laminate.›Customer-Specified MaterialsConfirm your grade and requirements.›Other Specialty MaterialsDiscuss your application and grade.›
Practical guidance for your part geometry and material decisions.
Prepare your process, budget and sourcing questions.
Build your knowledge before production.
Learn who we are and how we operate.
Find our U.S. support team or start a conversation.
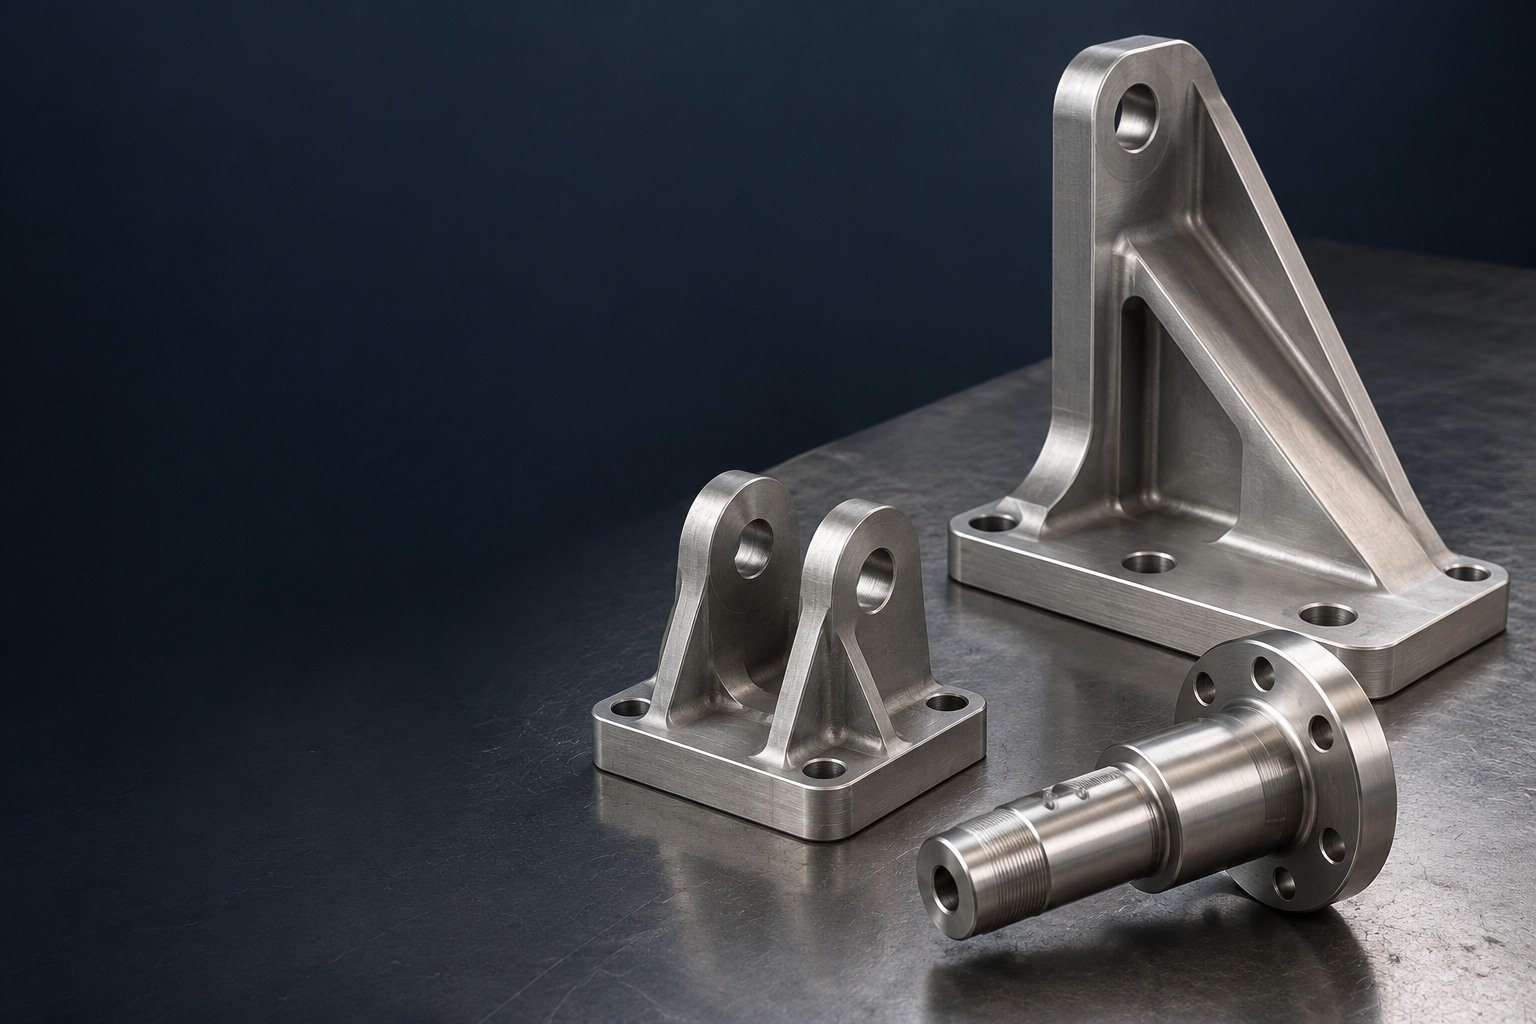
For your Grade 5 titanium machining services inquiry, connect Ti-6Al-4V identity and supplied condition to your ribs, cross bores and final assembly interfaces. Resolve workholding, finishing stock and inspection support before your first sample.
Grade 5 titanium / Ti-6Al-4V / Ti6Al4V / UNS R56400 is a titanium-aluminium-vanadium alloy. For your Grade 5 titanium properties review, distinguish the plate reference below from the actual bar, tube or plate specified on your purchase order.
Your U.S. grade identifier; state the applicable product standard and revision.
HSM lists 3.7164 and 3.7165 against Grade 5. These are supply comparison references; confirm the exact form and specification before approving a change.
Titanium Grade 5 is a material designation, not a complete purchase order. State bar, plate or tube and the applicable standard; a plate table does not accept a tube or finished pressure component.
| Element | ATI Grade 5 plate · wt.% |
|---|---|
| Al | 5.5–6.75 |
| V | 3.5–4.5 |
| Fe | ≤ 0.30 |
| O | ≤ 0.20 |
| C | ≤ 0.08 |
| N | ≤ 0.05 |
| H | ≤ 0.015 |
| Ti | Balance |
ATI published plate reference. Aluminium and vanadium are ranges; residual and interstitial figures are maxima. Verify the ordered form and lot certificate; bar limits are not silently substituted into this plate table.
ATI published plate minima · MPa · common axis 0–1000 MPa
Producer plate minima, not your lot report or finished-part rating. Grade 5 titanium tensile strength depends on the actual ordered form and condition. These values do not establish fatigue life, corrosion suitability or a substitution approval.
ATI Grade 5 plate ↗ ATI CP Grade 2 ↗ European comparison list ↗
Select your component, then connect machining, supplied condition and final acceptance.
For custom Grade 5 titanium parts such as ribbed angle brackets, connect the broad base, upright face and ribs to your assembly loads and datums. Provide the mating drawing and identify the released inspection state.
| Your decision | What to define |
|---|---|
| Your fit | Base flatness, upright datum, mounting slots and rib-root radii. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |

For Grade 5 titanium milling services, review cutter access at rib roots, secure clamping pads and cutting-fluid delivery. Avoid defining an inaccessible sharp internal corner.
| Your decision | What to define |
|---|---|
| Your fit | Base flatness, upright datum, mounting slots and rib-root radii. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |

For Grade 5 titanium structural parts, supply the applicable loading and acceptance requirements. A plate-strength reference does not approve your bracket design or service life.
| Your decision | What to define |
|---|---|
| Your fit | Base flatness, upright datum, mounting slots and rib-root radii. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |

Inspect the base and upright relationship after unclamping. Agree support points and recorded critical features before repeat quantities.
| Your decision | What to define |
|---|---|
| Your fit | Base flatness, upright datum, mounting slots and rib-root radii. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |

For your Grade 5 titanium CNC machining inquiry, identify the aligned cross bores, ear thickness and mounting base of your short clevis block. Connect the pin and mating component to the controlled drawing.
| Your decision | What to define |
|---|---|
| Your fit | Bore alignment, ear spacing, base datum and edge distance. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |

Connect Grade 5 titanium drilling to depth, access, chip escape and bore intersections. Review support behind each thick ear and the final bore-finishing route.
| Your decision | What to define |
|---|---|
| Your fit | Bore alignment, ear spacing, base datum and edge distance. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
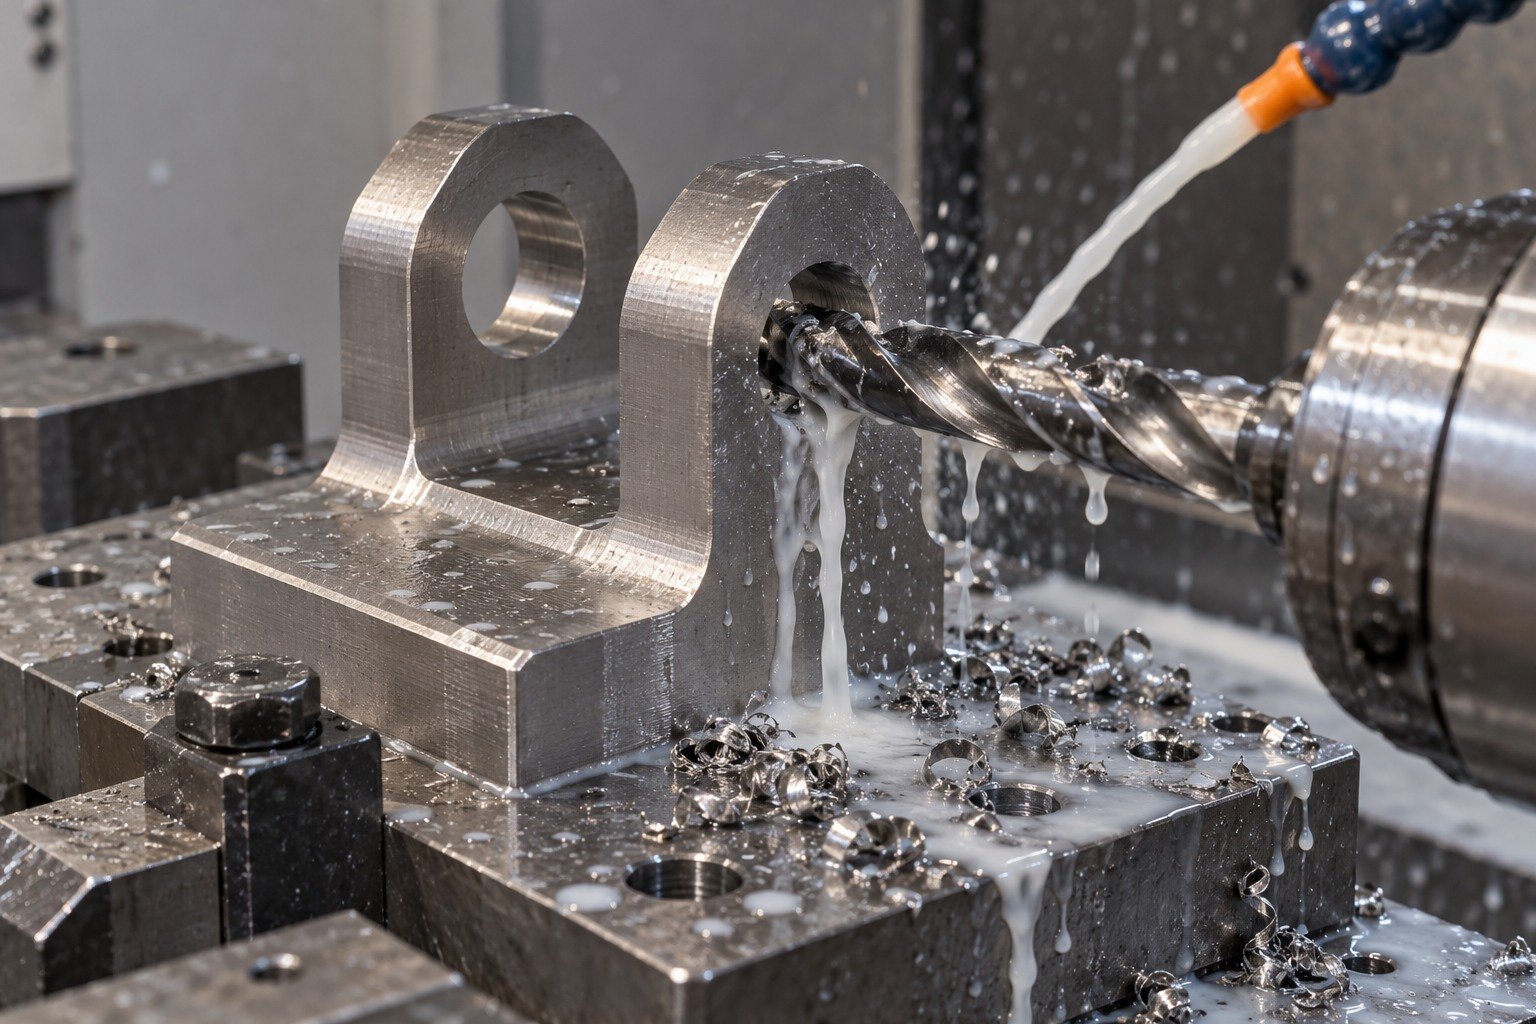
For Ti-6Al-4V CNC machining, identify stock form and supplied condition. Keep any specified treatment and final dimensional acceptance responsibilities explicit.
| Your decision | What to define |
|---|---|
| Your fit | Bore alignment, ear spacing, base datum and edge distance. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
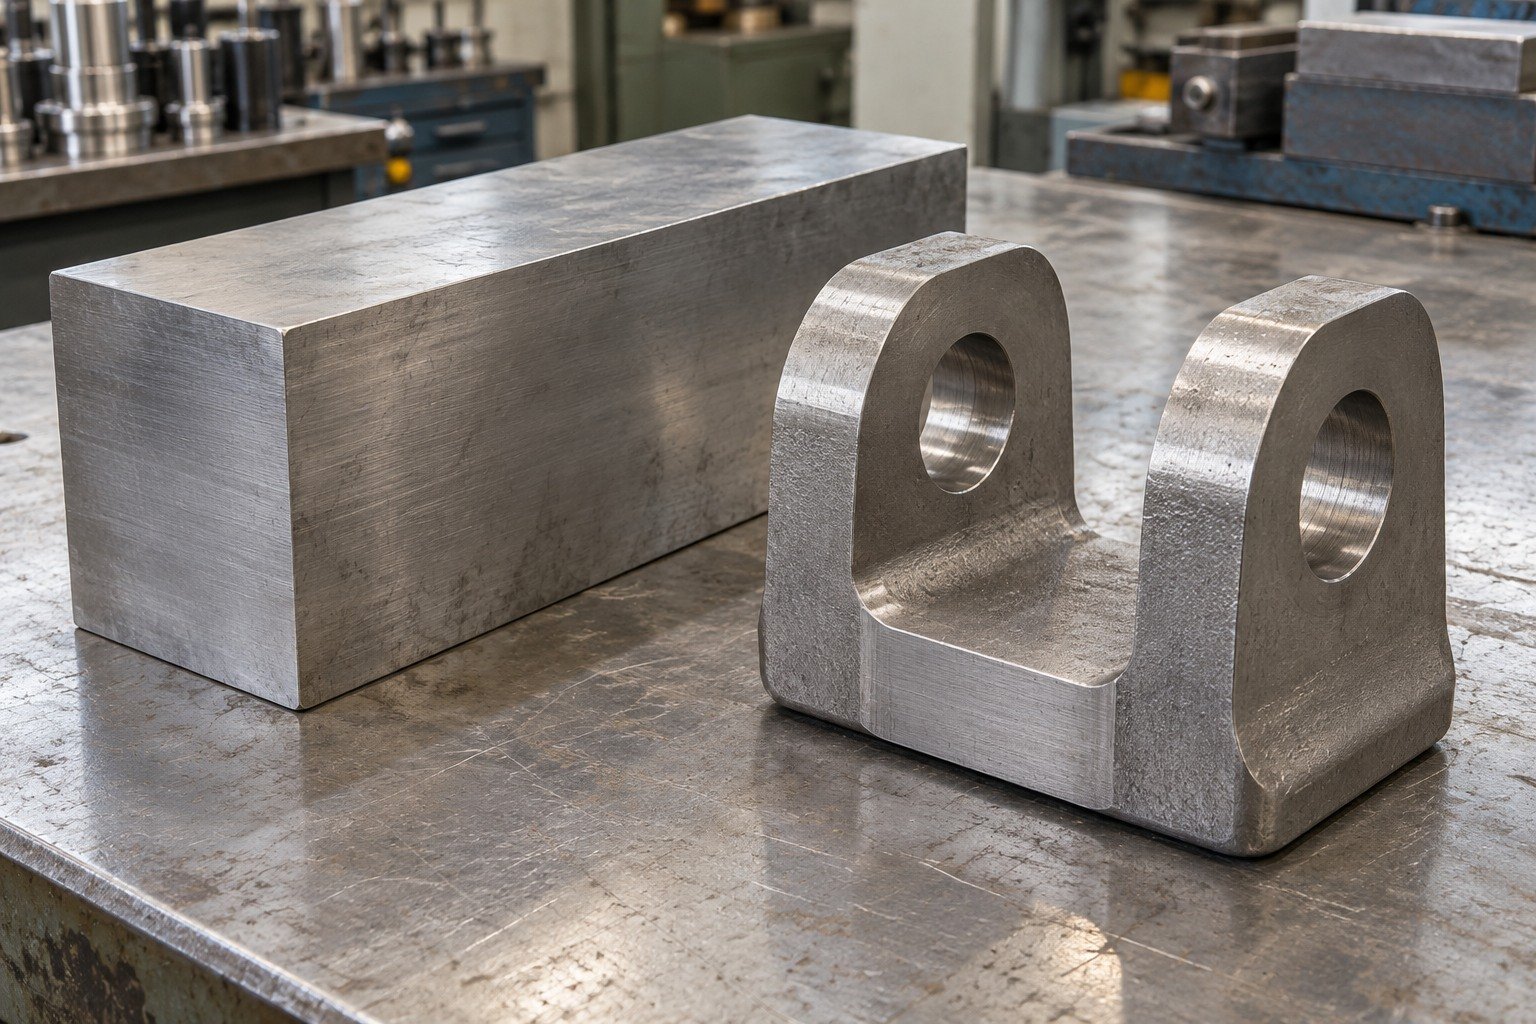
Verify the cross-bore relationship and external datums after the complete route. Agree the gauge and measurement support for the actual mating pin.
| Your decision | What to define |
|---|---|
| Your fit | Bore alignment, ear spacing, base datum and edge distance. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |

For your Ti-6Al-4V machining services inquiry, define the compact spindle, flange and axial bore together. Separate controlled locating surfaces from noncritical reliefs.
| Your decision | What to define |
|---|---|
| Your fit | Shaft diameter, flange face, axial bore and coaxial relationship. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
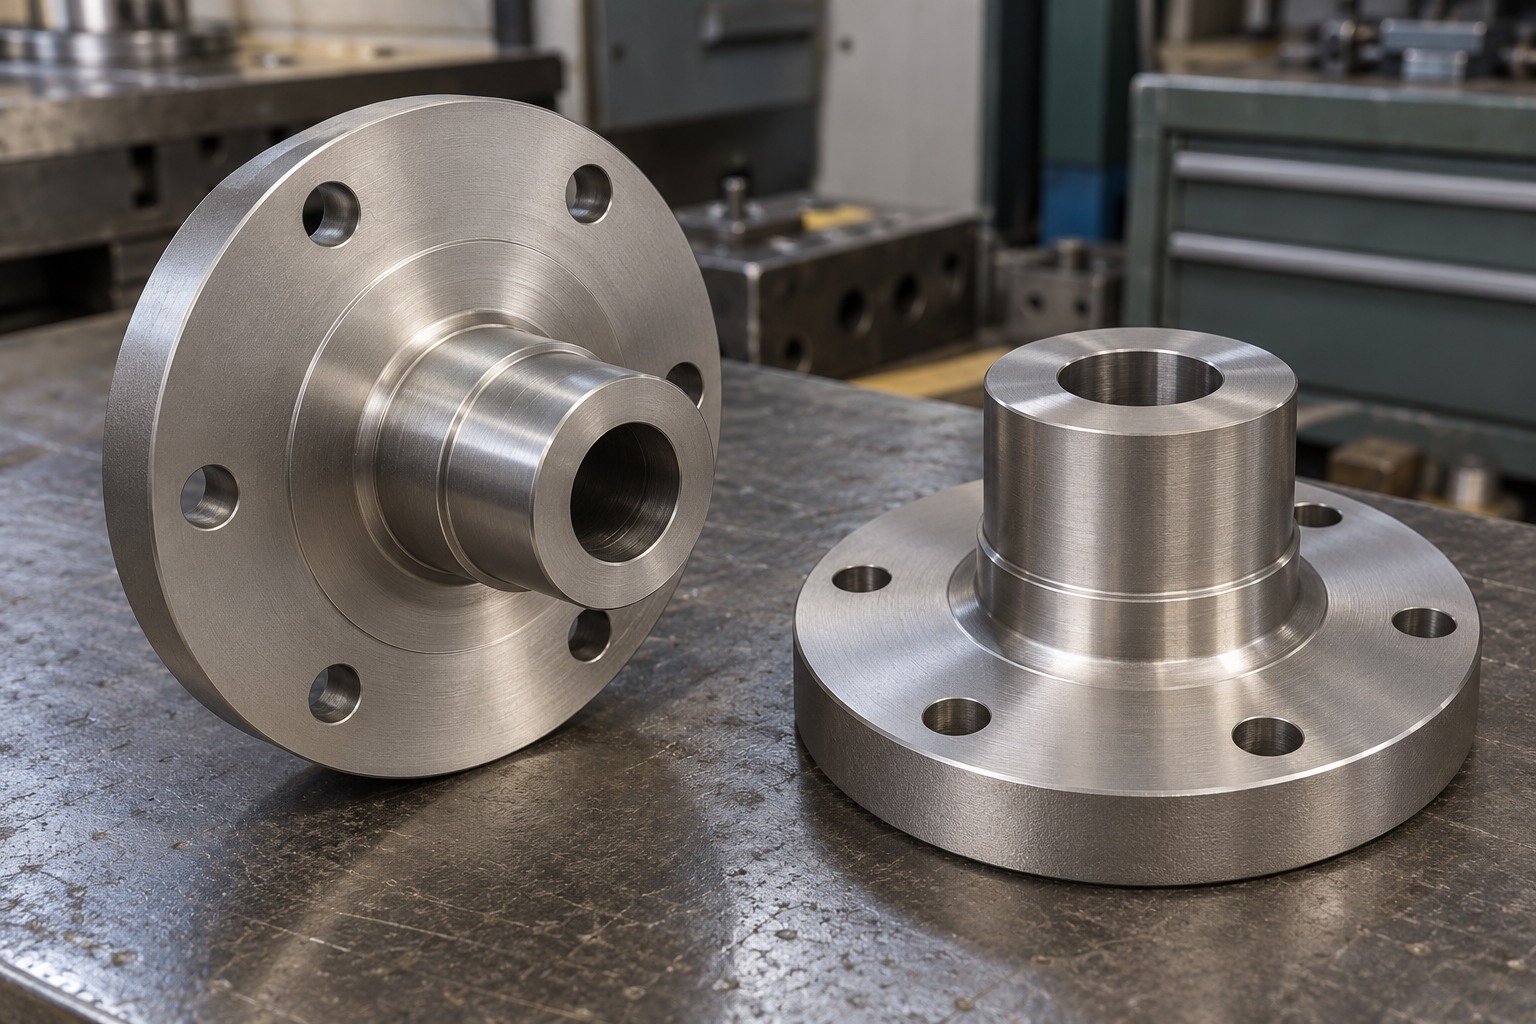
For Grade 5 titanium turning services, connect secure grip, tool engagement and coolant delivery to the short flanged geometry. Review the last setup that establishes the final datum.
| Your decision | What to define |
|---|---|
| Your fit | Shaft diameter, flange face, axial bore and coaxial relationship. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
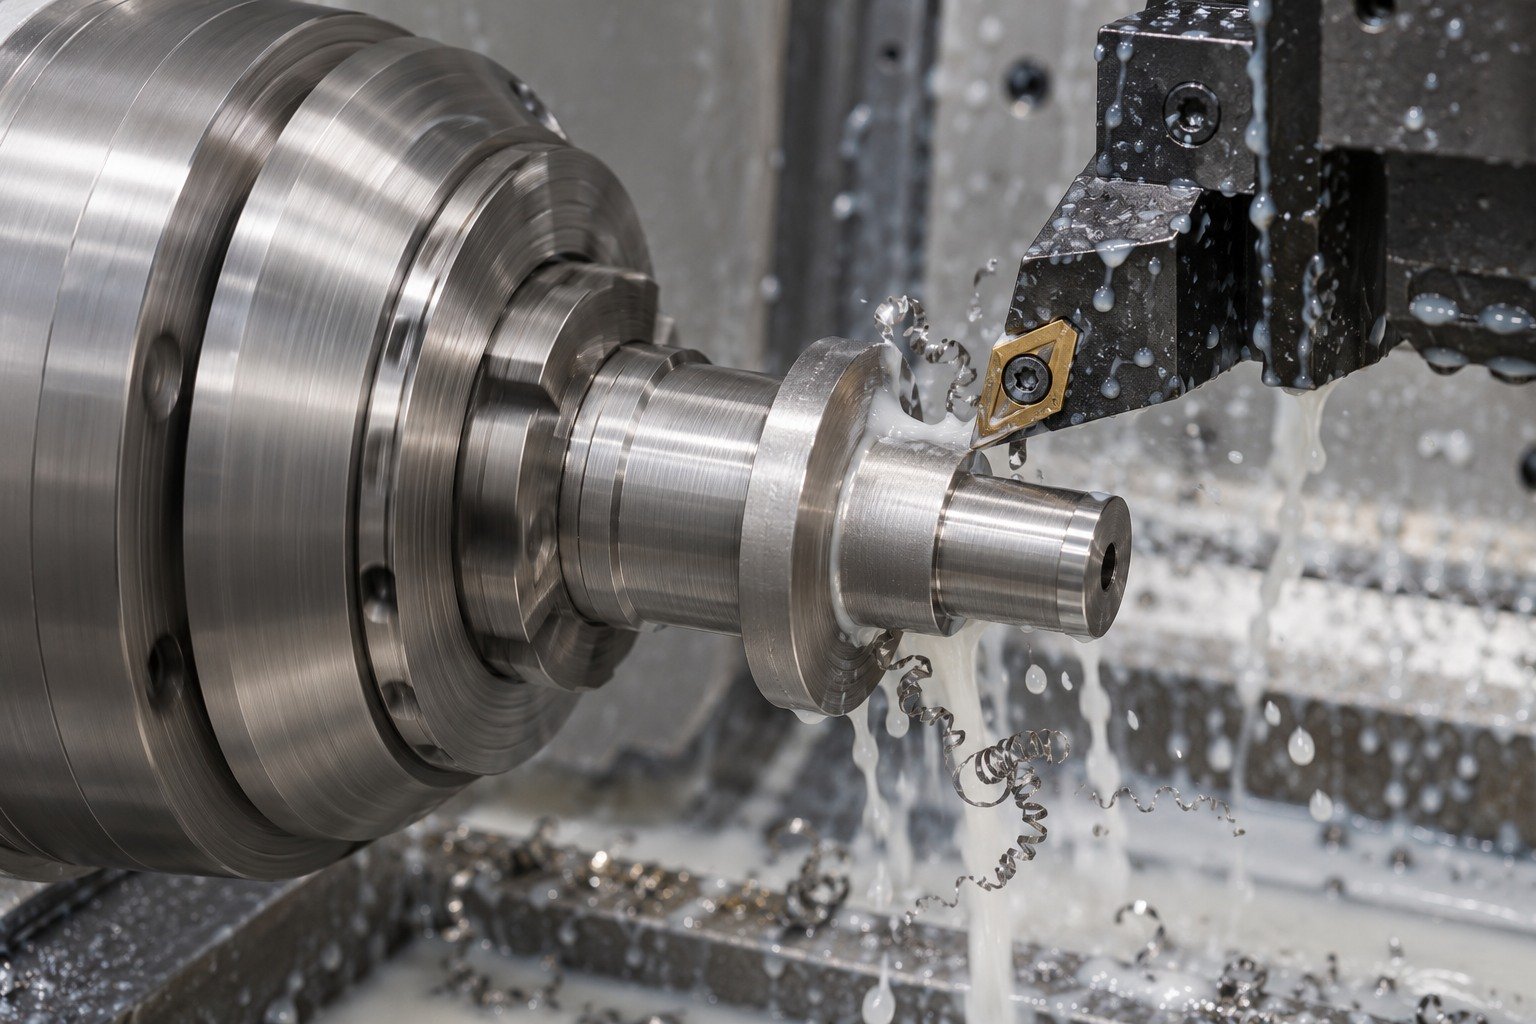
Specify round stock and the exact supplied state. Retained finishing stock and any treatment sequence depend on your drawing, rather than one generic allowance.
| Your decision | What to define |
|---|---|
| Your fit | Shaft diameter, flange face, axial bore and coaxial relationship. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
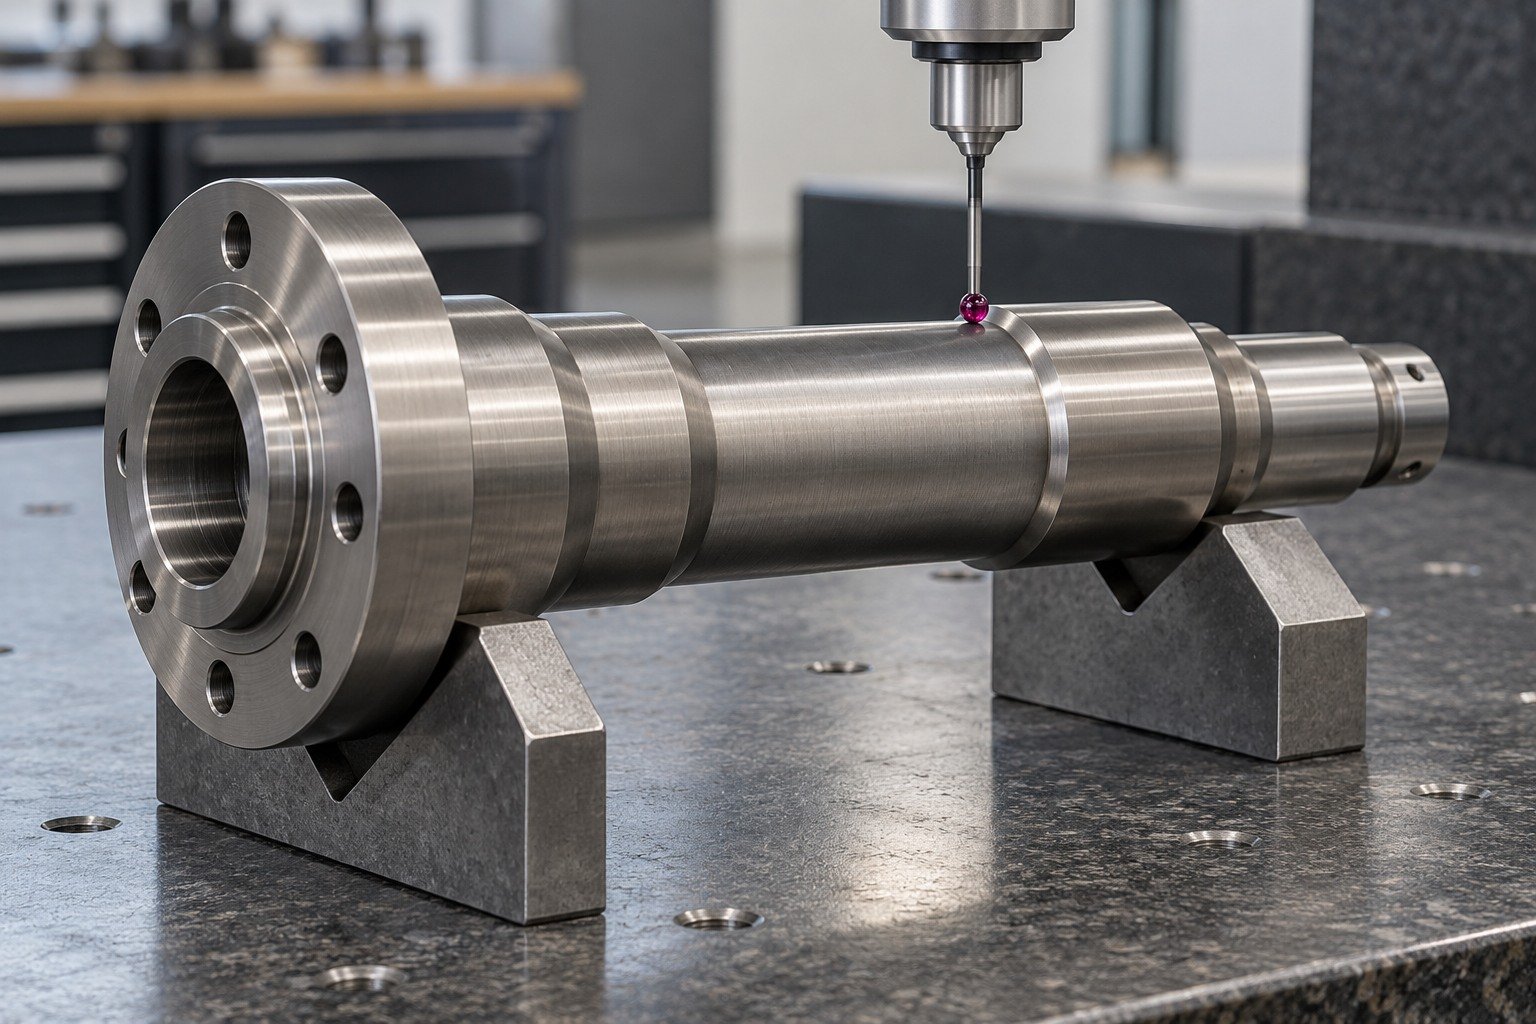
Inspect flange position, shaft diameter and bore relationship in the final condition. Protect the locating shoulder through handling and packing.
| Your decision | What to define |
|---|---|
| Your fit | Shaft diameter, flange face, axial bore and coaxial relationship. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
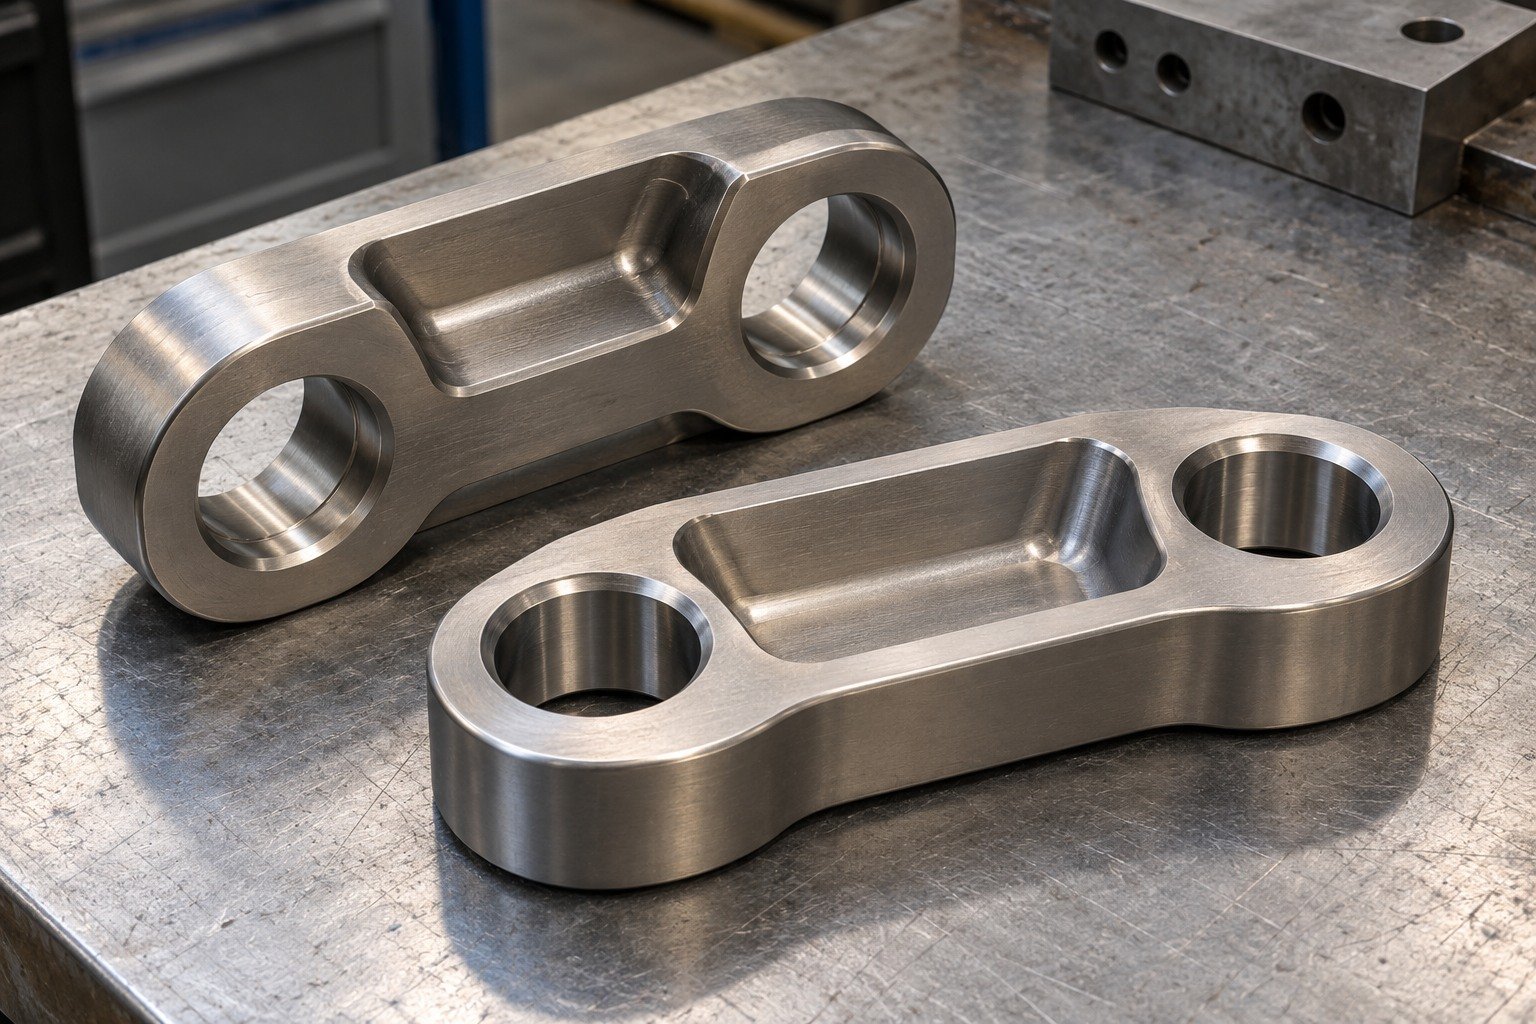
For Grade 5 titanium structural parts such as pocketed links, define bore spacing, thick ligaments and supported pockets against your actual loads. No application qualification follows from the illustrative geometry.
| Your decision | What to define |
|---|---|
| Your fit | Bore spacing, pocket depth, ligament section and flat datum. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
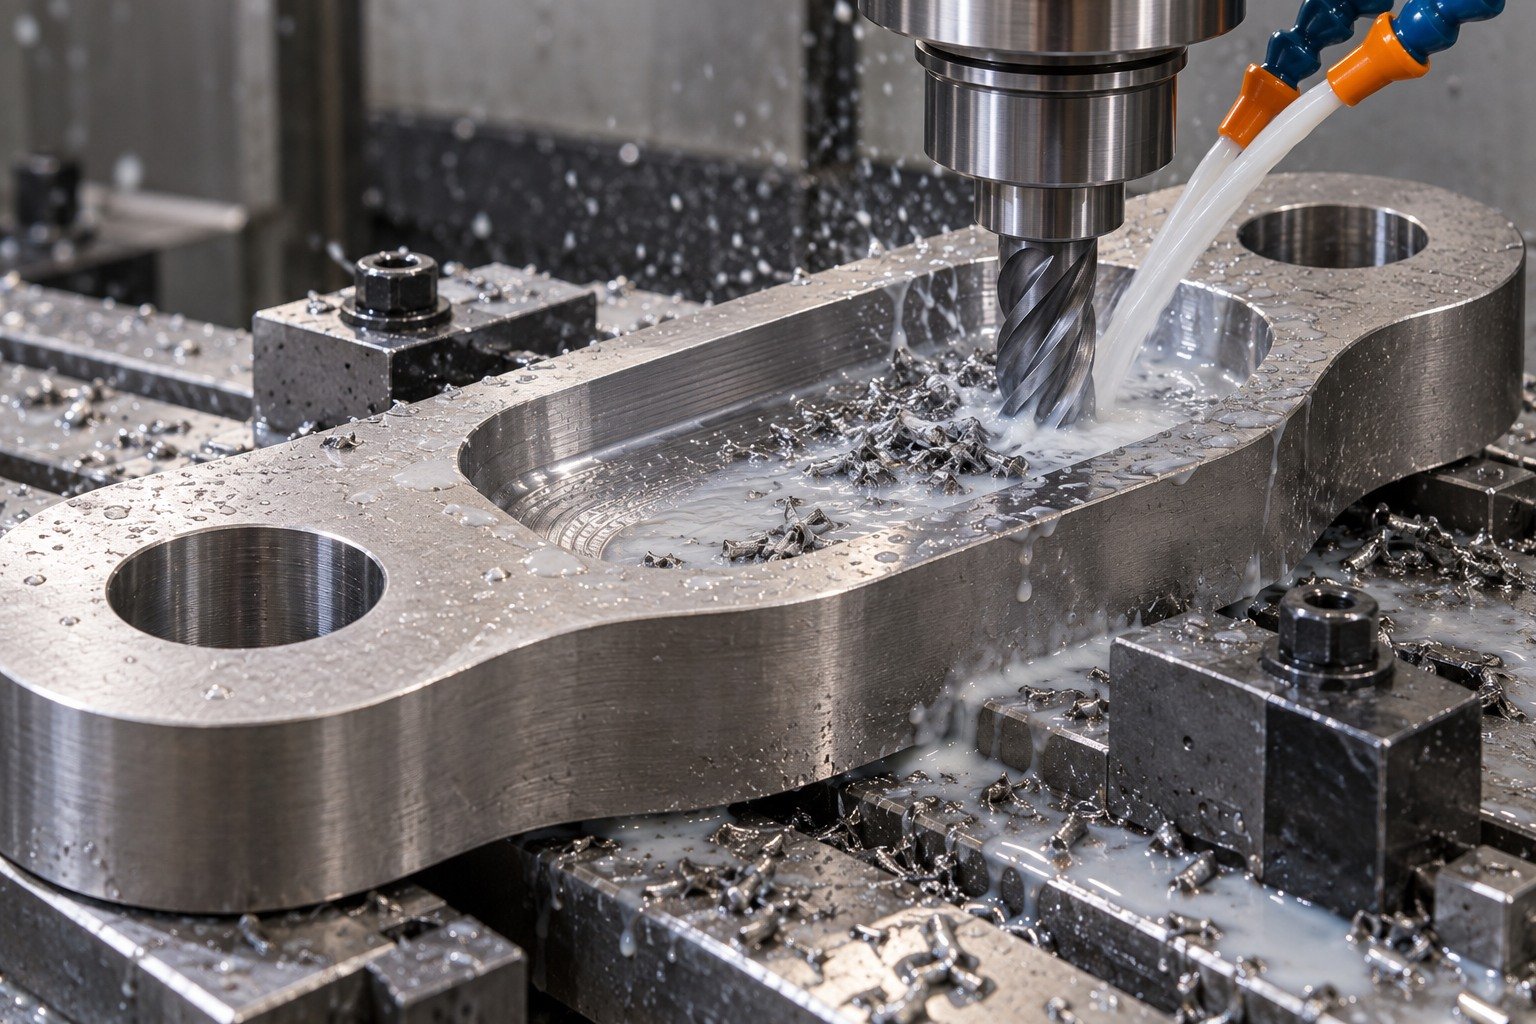
Review Grade 5 titanium threading with actual engagement, mating material and gauge access. Connect open pockets to stable backing, tool reach and chip evacuation.
| Your decision | What to define |
|---|---|
| Your fit | Bore spacing, pocket depth, ligament section and flat datum. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
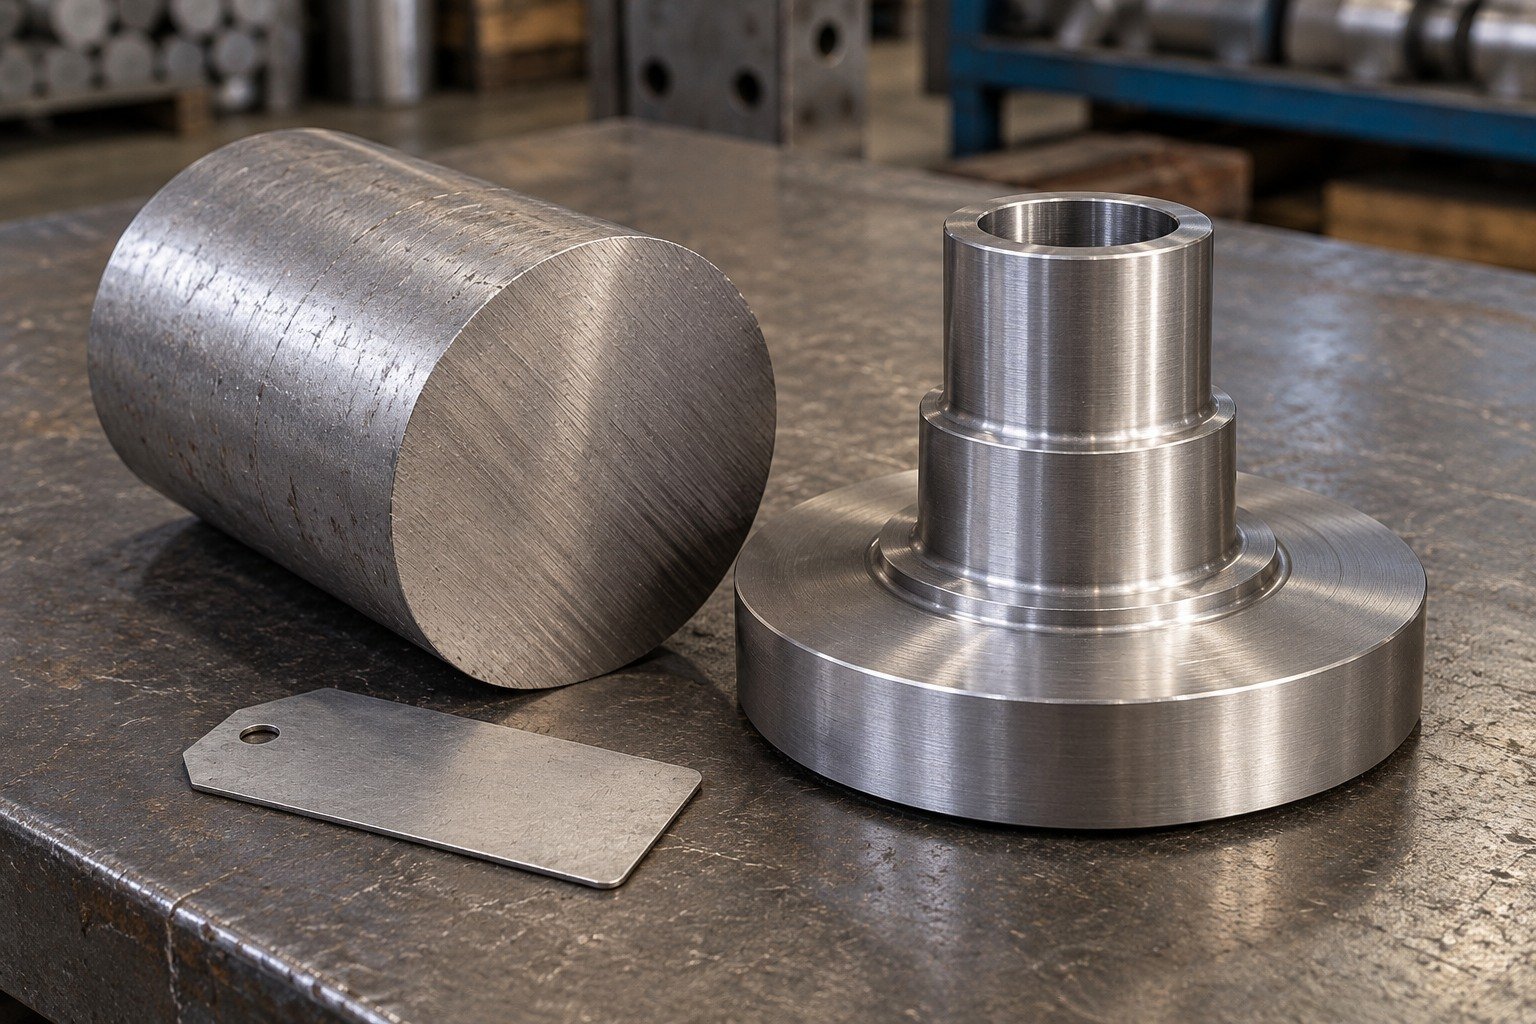
Retain Ti-6Al-4V identity through blank preparation. State plate condition and the responsibility for any later specified treatment before approving stock changes.
| Your decision | What to define |
|---|---|
| Your fit | Bore spacing, pocket depth, ligament section and flat datum. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |

Measure bore positions and released profile from the agreed datums. Keep material records and feature results linked to the same drawing revision.
| Your decision | What to define |
|---|---|
| Your fit | Bore spacing, pocket depth, ligament section and flat datum. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
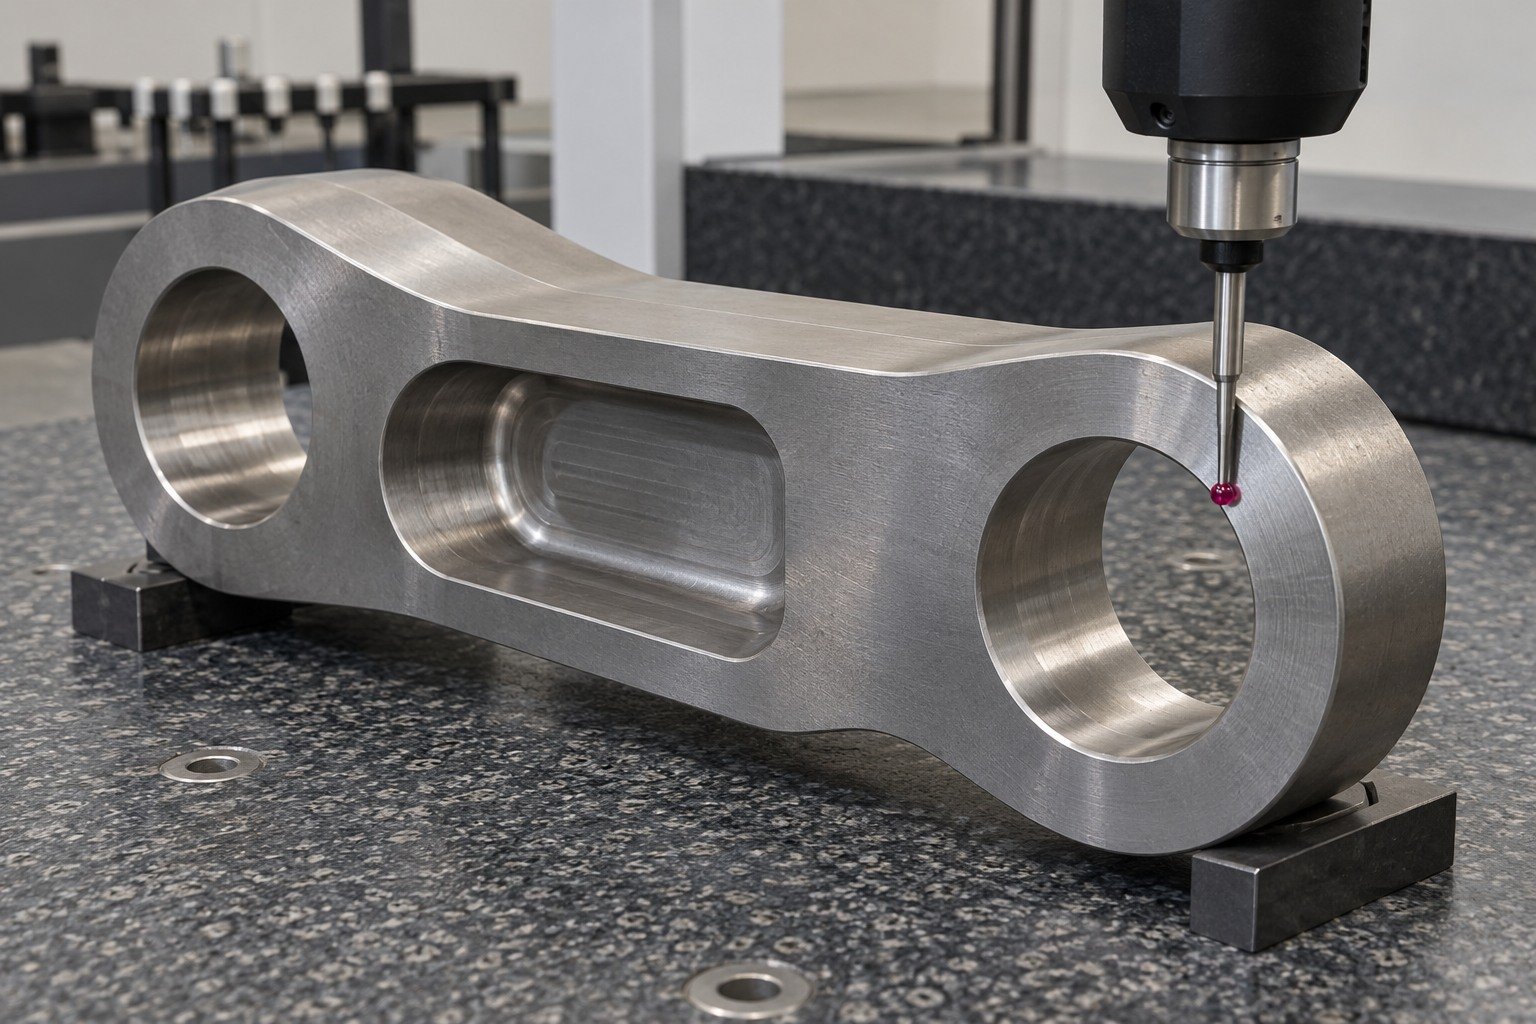
Identity, stock form and supplied state.
Condition, support and final mating features.
Functional geometry, protection and records.
Confirm grade, form, condition and heat or lot identity before cutting. Review the requested certificate against the actual purchase specification.
Sampling and document scope are agreed with your quotation.
Quality Assurance →
Review the first bracket, clevis or spindle sample against the mating features and drawing datums. Resolve workholding effects, controlled surface criteria and measurement support before repeat quantities.
Sampling and document scope are agreed with your quotation.
Quality Assurance →
Verify bores, flange position, controlled surfaces and agreed edges. State which dimensions require records and how the finished part is supported during inspection.
Sampling and document scope are agreed with your quotation.
Quality Assurance →
Agree separate pockets and protection for clevis ears, cross bores, flange shoulders and bracket pads. Link each delivered lot to the requested material and dimensional records.
Sampling and document scope are agreed with your quotation.
Quality Assurance →
Connect working profile, supplied state and final fit before approving the first route.
Specify UNS R56400, product standard, form, supplied condition and lot identity. State your Grade 5 titanium material certificate requirement at inquiry, including document type and required chemistry or condition evidence.
Identify the mating geometry and supported datum.
Connect stock, clamping access and final surface.
Agree feature results, condition and lot evidence.
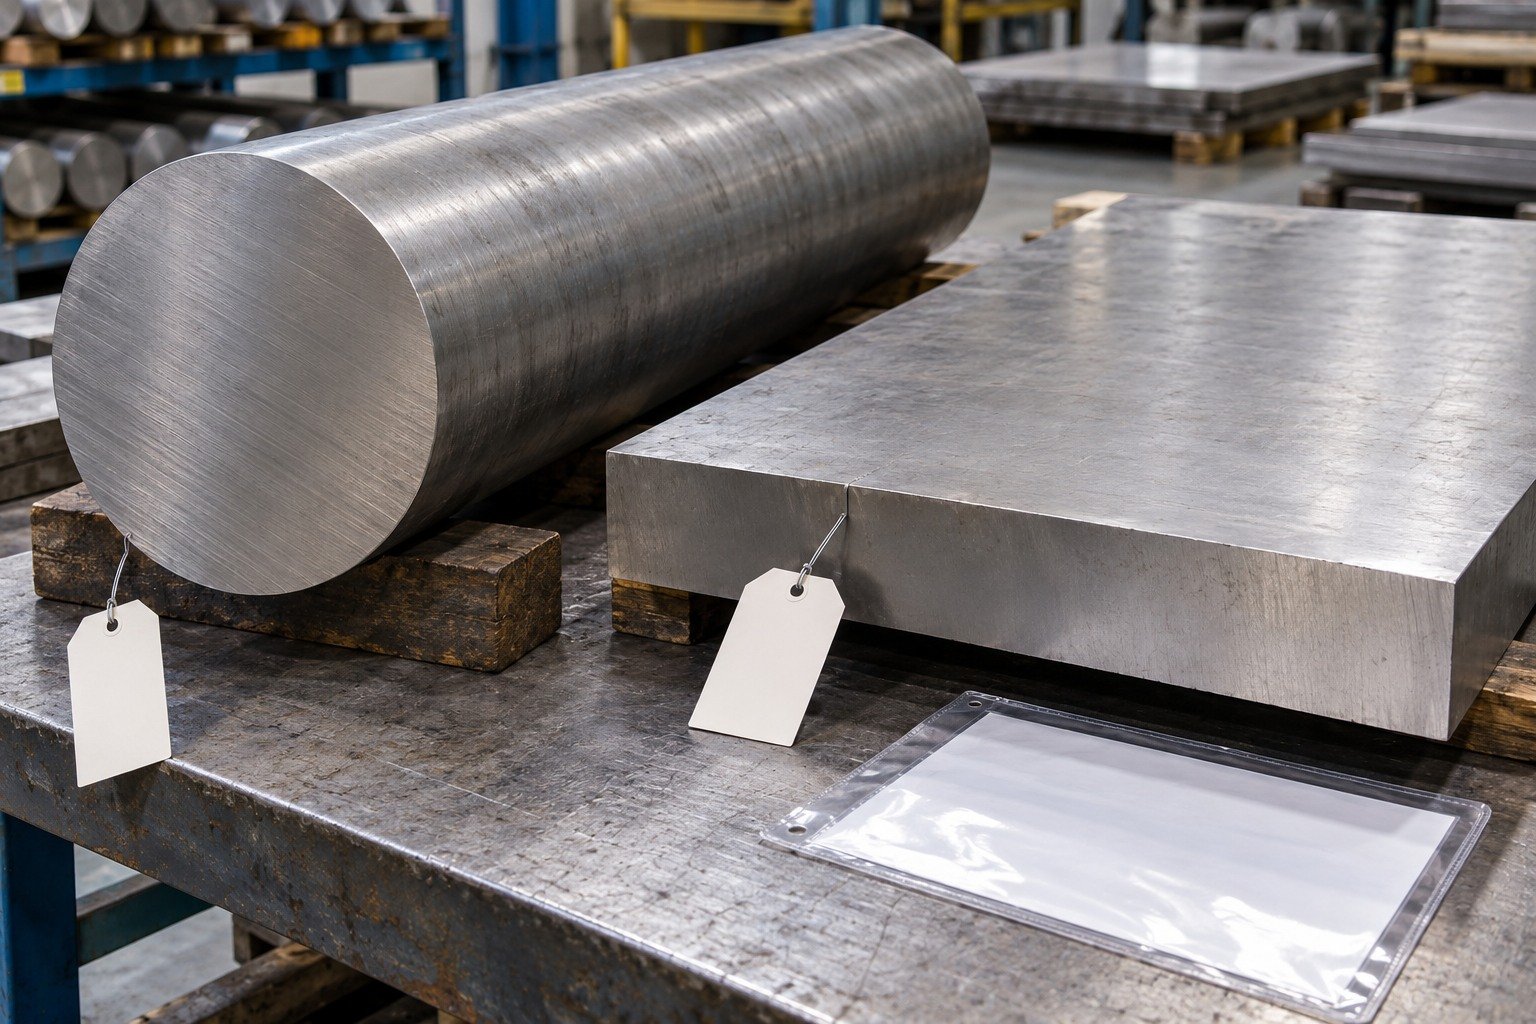
For intersecting bores and threads, define tool access, chip escape and burr-sensitive edges. Connect the mating specification and gauge method to the final assembled requirement.
Identify the mating geometry and supported datum.
Connect stock, clamping access and final surface.
Agree feature results, condition and lot evidence.
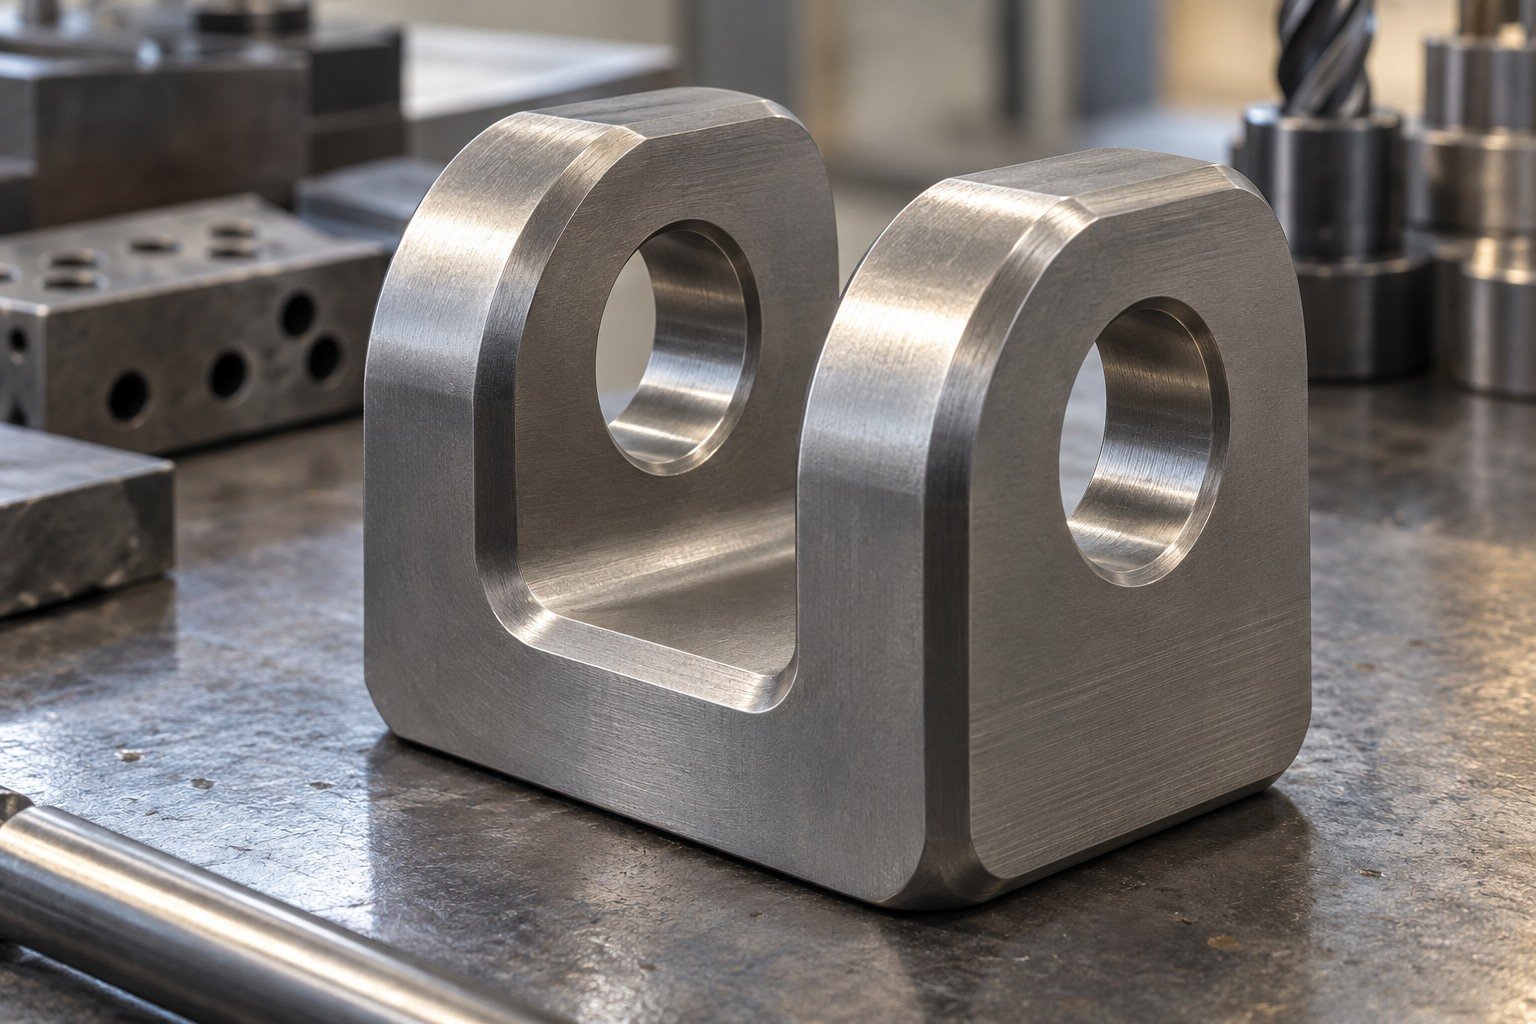
State the accepted unsupported geometry. Connect ribbed brackets and pocketed links to secure backing and broad clamping pads. Agree when finishing stock is removed and how the released part is held for its final measurement.
Identify the mating geometry and supported datum.
Connect stock, clamping access and final surface.
Agree feature results, condition and lot evidence.

Address Grade 5 titanium machining surface finish problems through defined roughness, visual criteria, tool access and edge acceptance. A roughness number alone does not define the appearance your buyer expects.
Identify the mating geometry and supported datum.
Connect stock, clamping access and final surface.
Agree feature results, condition and lot evidence.

For your Grade 5 titanium galling review, identify the mating material, contact load, relative movement and lubrication or surface requirements. A grade name does not establish wear performance.
Identify the mating geometry and supported datum.
Connect stock, clamping access and final surface.
Agree feature results, condition and lot evidence.

Define controlled dimensions, profile, surfaces and cleaning after the complete agreed route. Grade 5 titanium machining tolerances are reviewed feature by feature; no single tolerance applies to every part.
Identify the mating geometry and supported datum.
Connect stock, clamping access and final surface.
Agree feature results, condition and lot evidence.
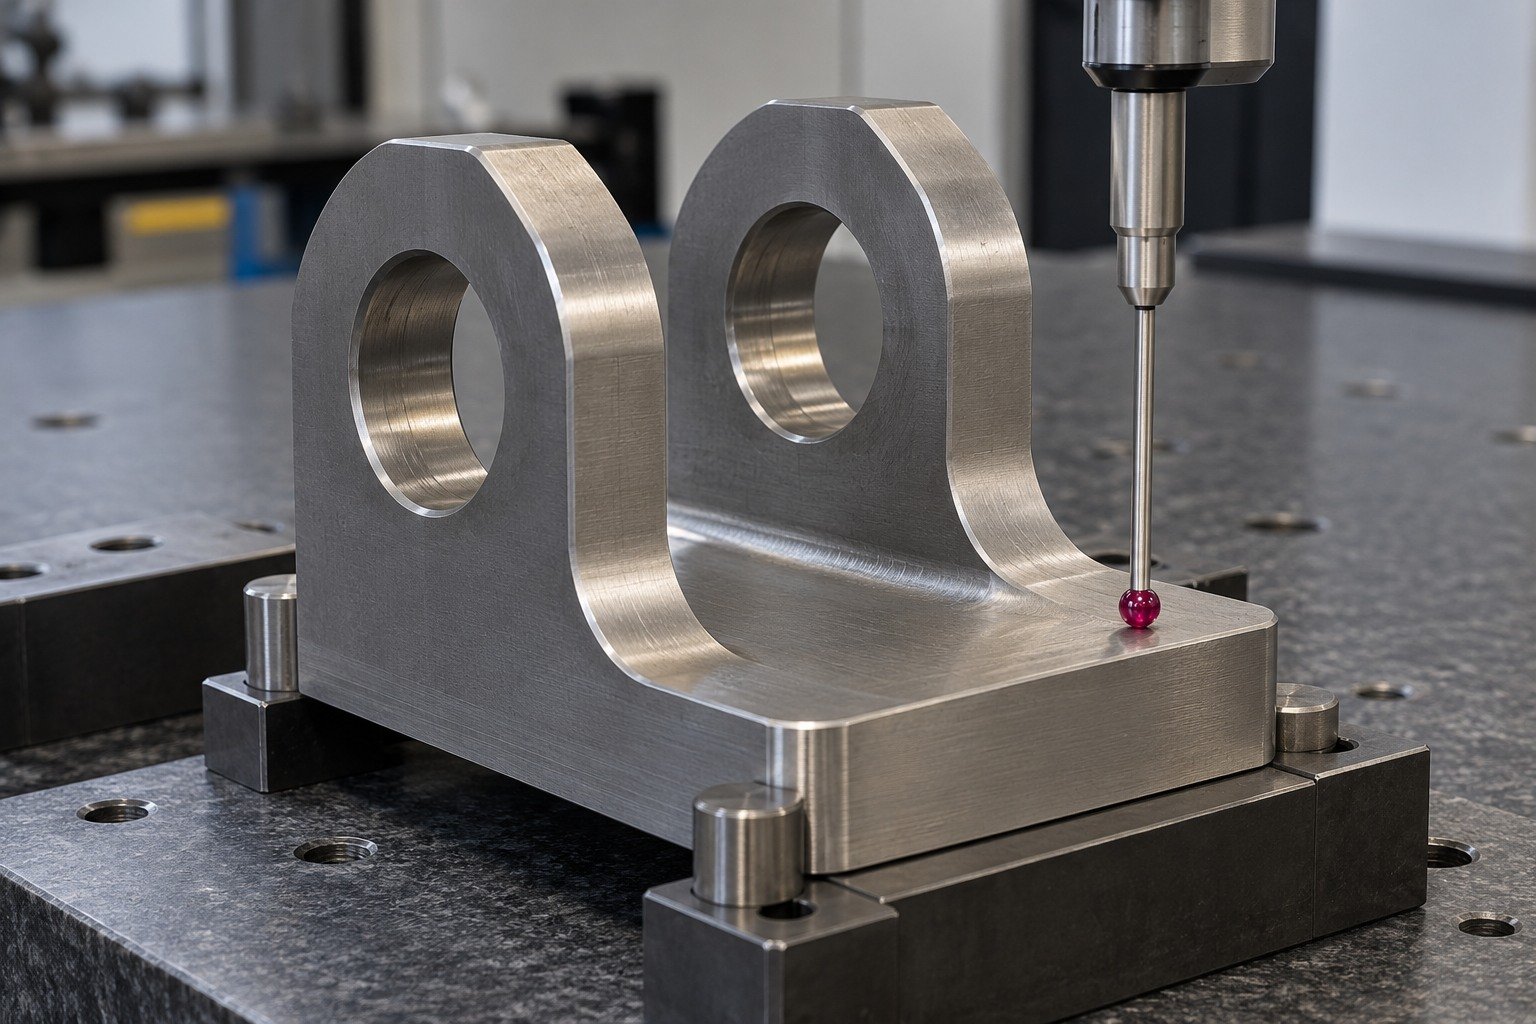

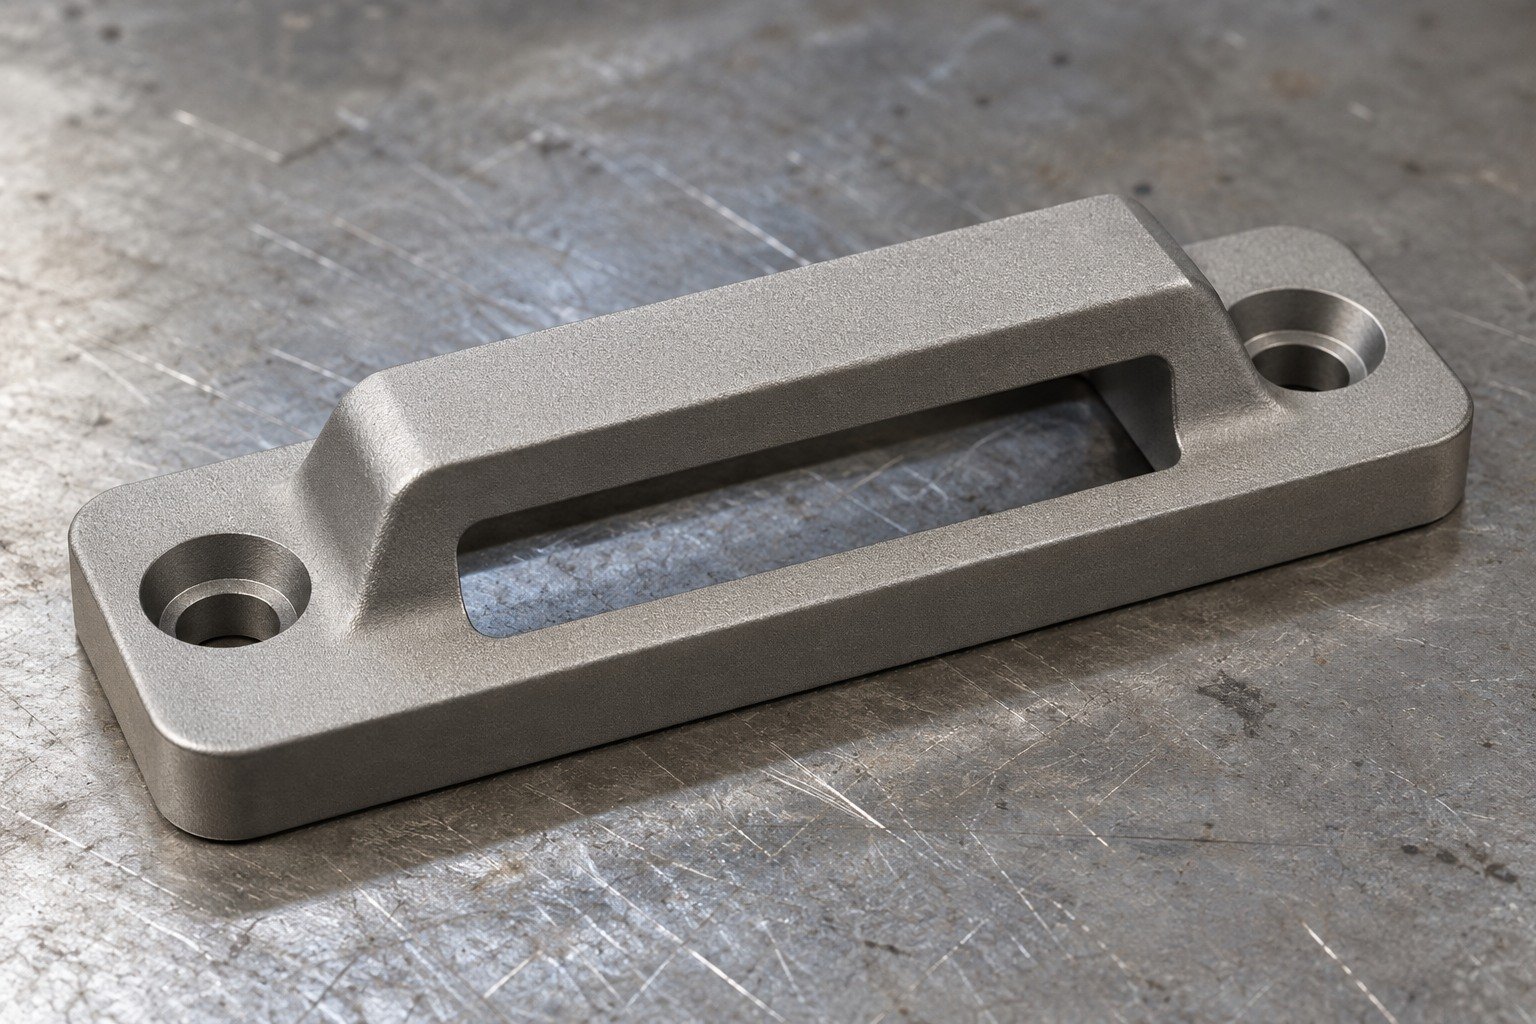
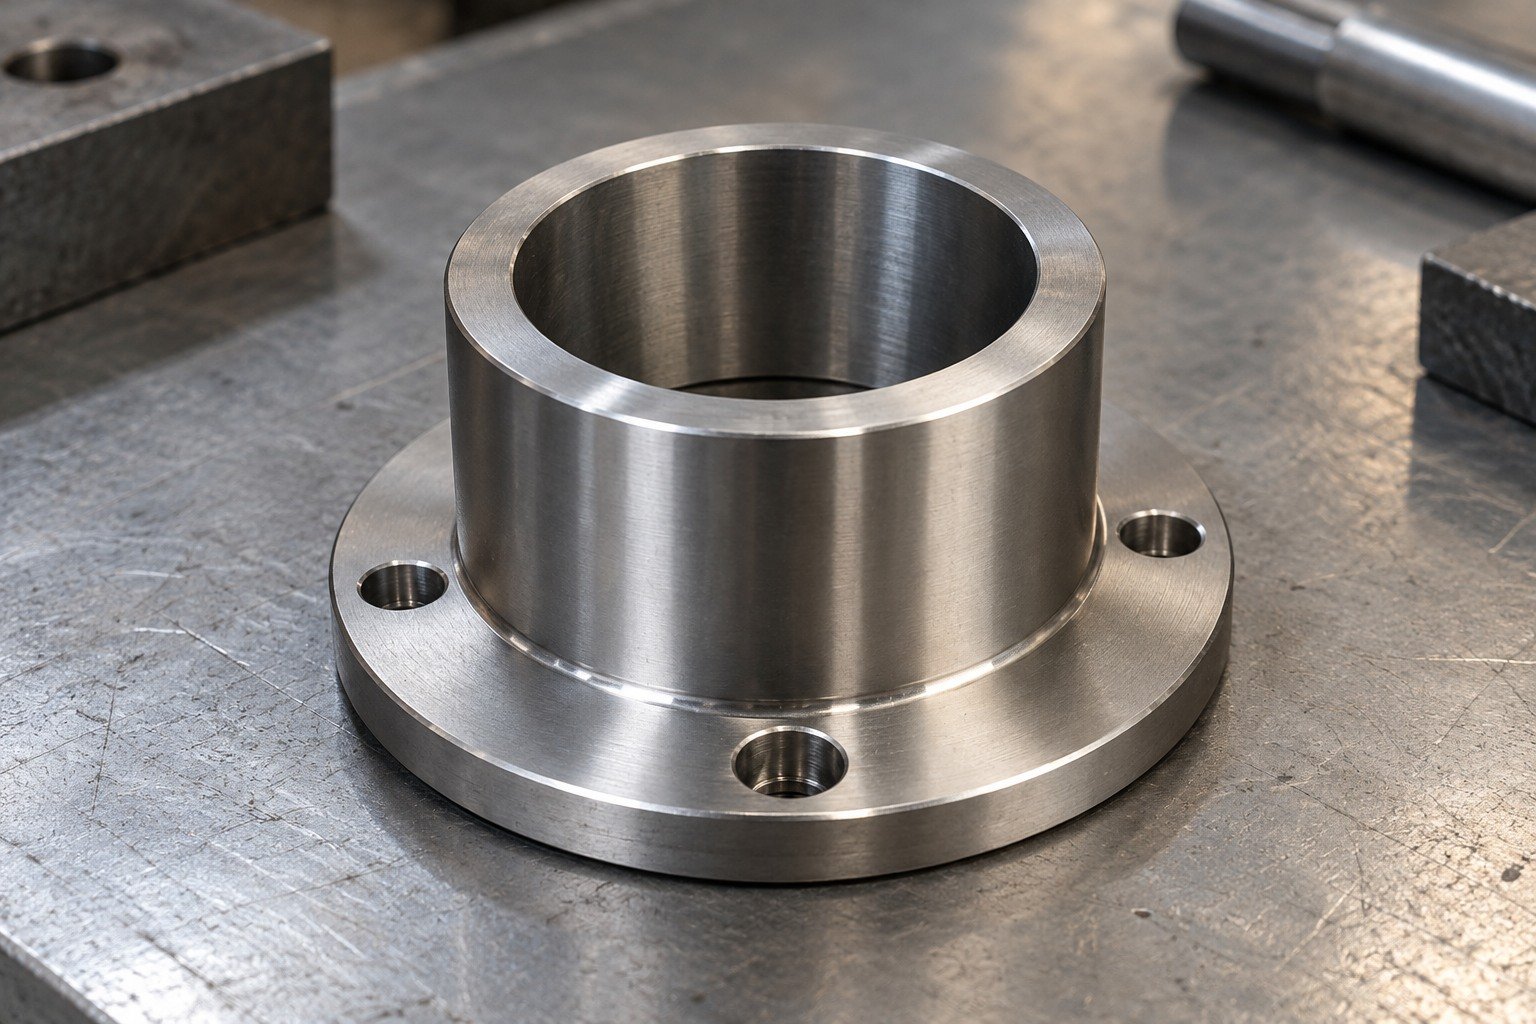

Illustrative appearances only. Agree finish suitability, cleaning, masking and final dimensions for your grade and service conditions. Colour does not prove alloy identity, coating thickness or corrosion life.
Surface Finishing →| Your decision | What to confirm |
|---|---|
| Material identity | Separate grades and the applicable product specification. |
| Material condition | Distinguish annealed stock from any specified solution-treated and aged condition. |
| Strength and loading | Product-form data and your actual design loads. |
| Service exposure | Medium, concentration, temperature and contact conditions. |
For Grade 5 vs Grade 23 titanium, distinguish UNS R56400 from ELI UNS R56407 and confirm the exact product form, condition and purchase specification. A similar Ti-6Al-4V name does not approve substitution or an application.
Compare the Titanium Family →For Grade 5 titanium prototype machining, use the first controlled sample to review datum recovery, supported machining and assembly fits before repeating your drawing. Quantities, timing and scope are confirmed with your quote.
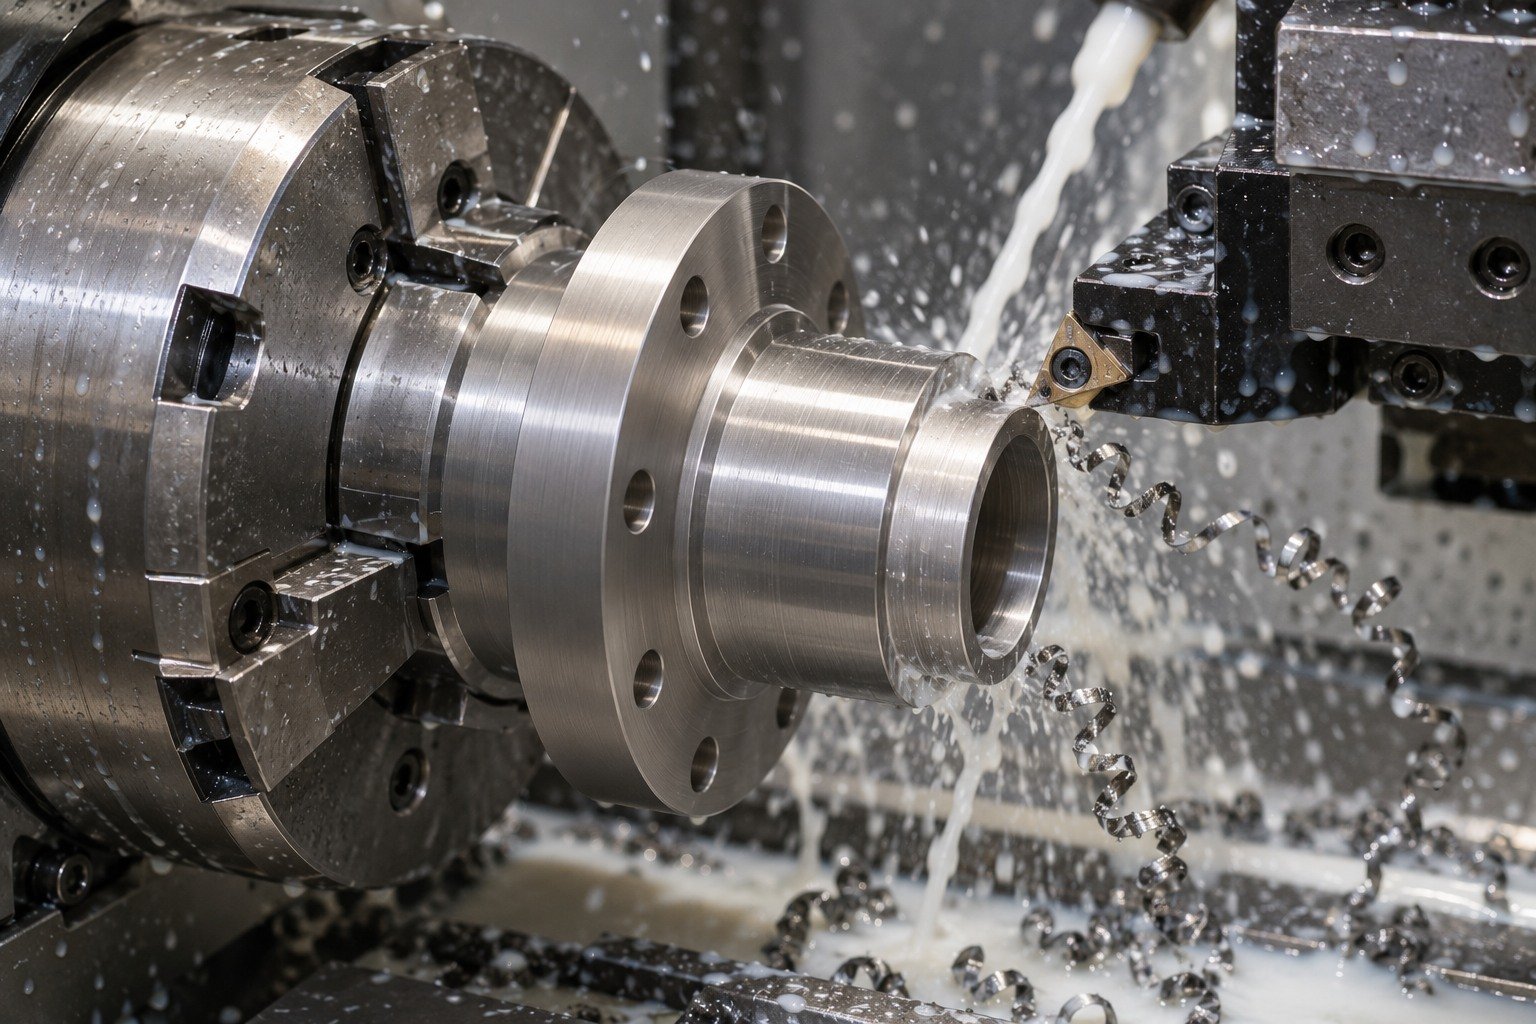
Grade 5 titanium turning: review compact flanged spindles and controlled locating diameters.
Explore CNC Turning →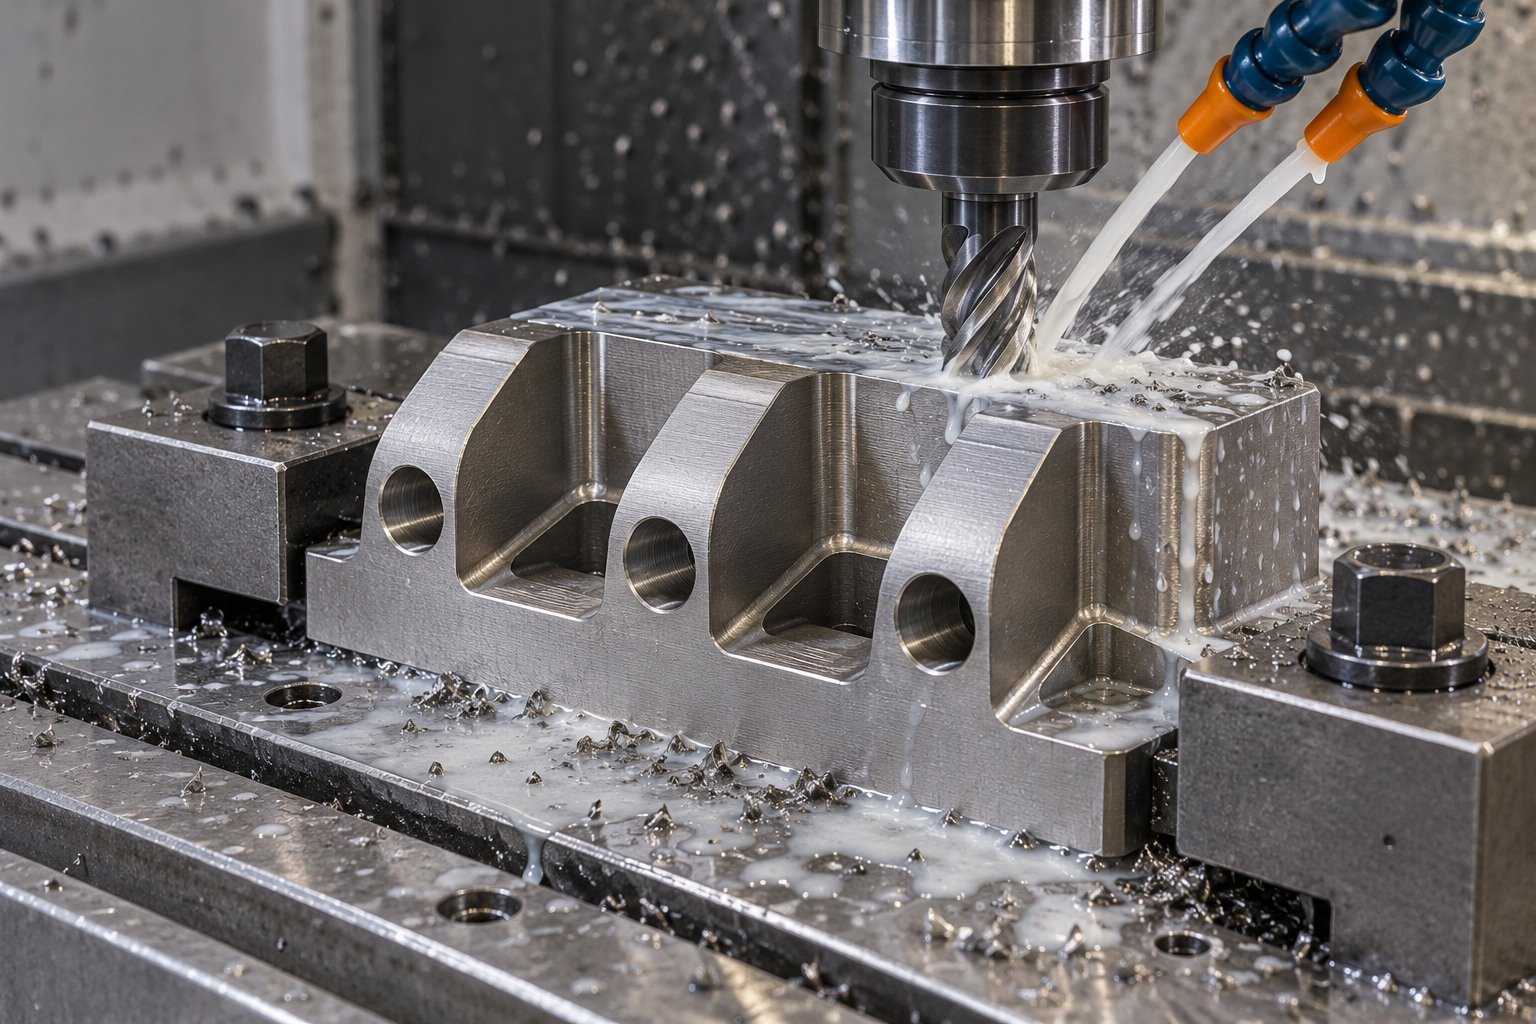
Grade 5 titanium milling: connect rib roots, bracket pads and pocketed link features.
Explore CNC Milling →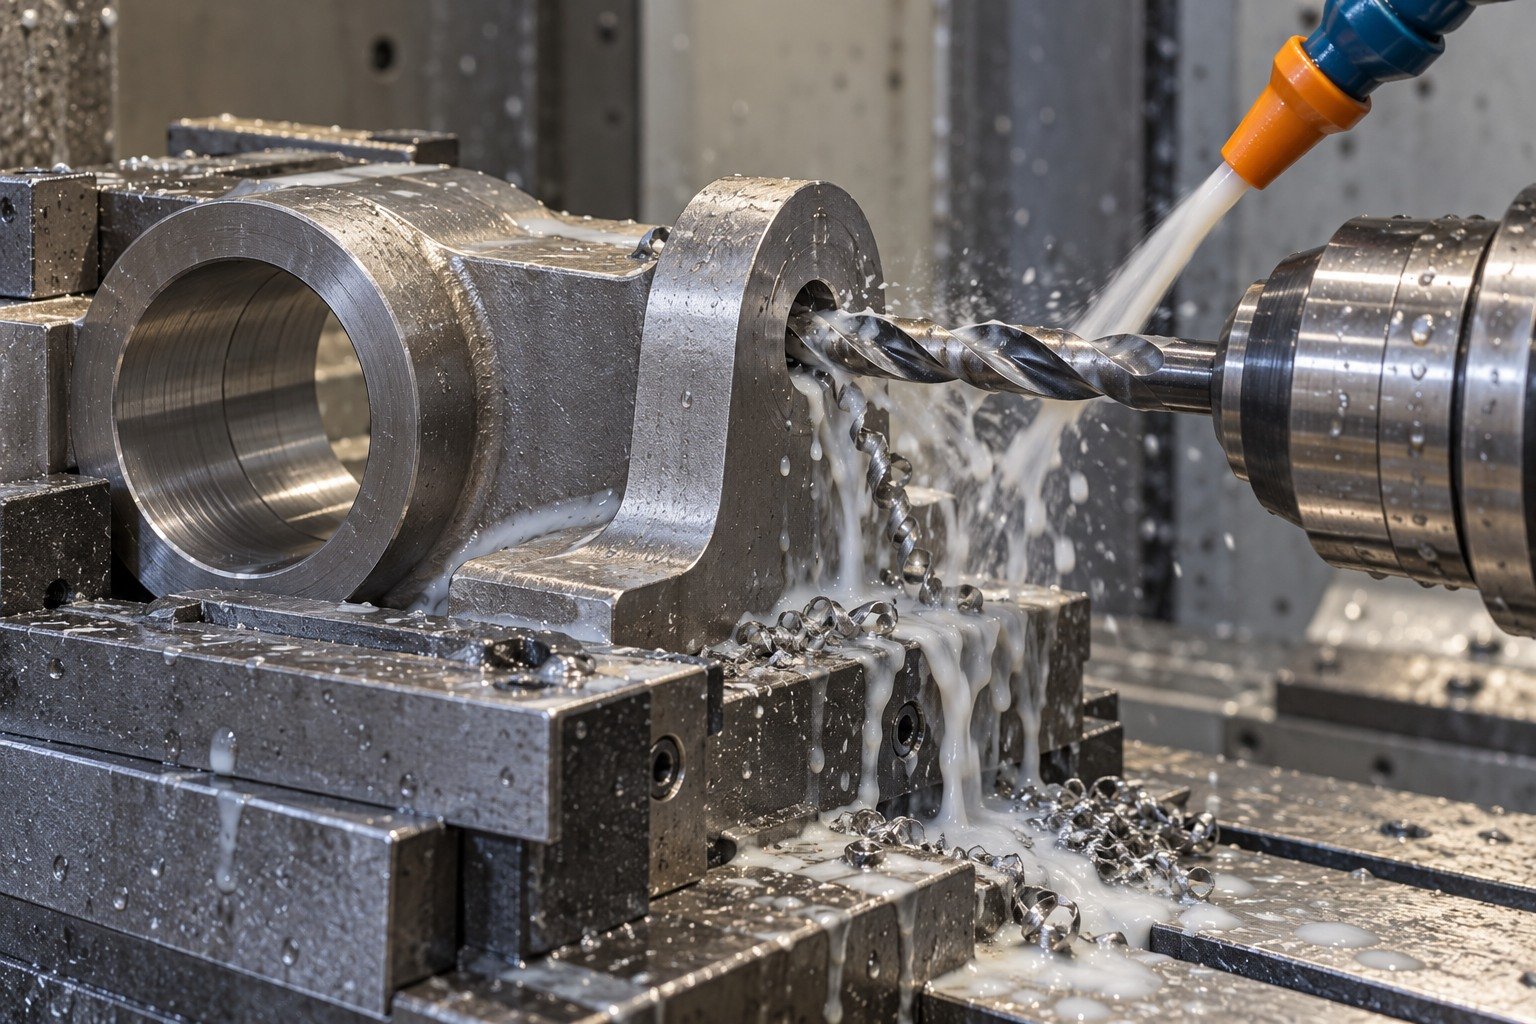
Define hole access, intersections, thread engagement and gauge requirements.
Explore Drilling & Thread Review →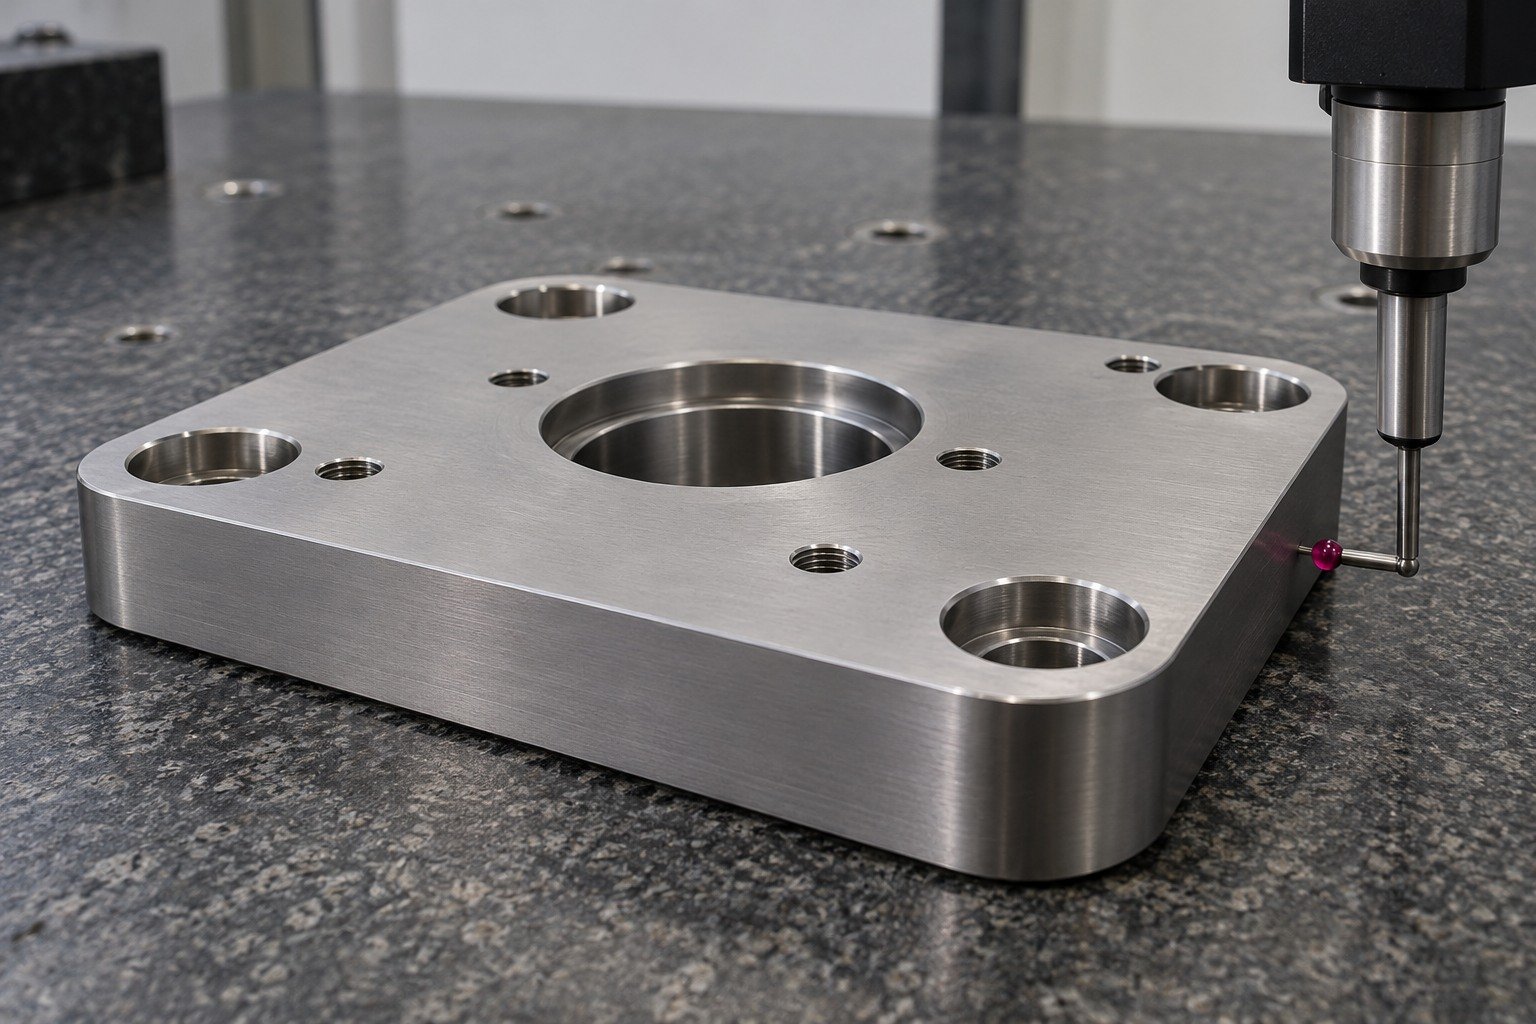
Verify clevis cross bores, link spacing and bracket datums against the controlled drawing.
Explore Final Interface Inspection →
Connect China manufacturing with Dallas-area coordination for your drawing review, sample decisions and delivery requirements.
Review ribbed brackets, clevis blocks, compact spindles and pocketed links against your drawing, loads and supplied condition. Ti-6Al-4V is a material designation; a component image does not establish application certification or project acceptance.
State the exact condition required by your drawing and purchase standard, including any aging step and final verification. Do not mix reference plate values with a different treatment state. Agree treatment responsibility, finishing allowance and inspection sequence for your geometry.
Review Grade 5 titanium corrosion resistance for the actual medium, temperature, concentration, crevices and dissimilar-metal contacts. No universal corrosion-life or immunity guarantee follows from the alloy name.
For your Grade 5 titanium welding inquiry, state the joint, applicable procedure, material condition, cleanliness, shielding and inspection requirements. Confirm procedure responsibility and project availability rather than assuming every machined part can be welded without review.
Review tool condition, secure support, cutting engagement, cutting-fluid delivery and chip removal for the actual feature. Review Grade 5 titanium galling separately for sliding or threaded interfaces, including mating material and surface requirements.
Grade 5 titanium machining cost depends on usable stock, quantities, setups, access, final condition and inspection scope. For your Grade 5 titanium machining quote, compare the same drawing revision and acceptance requirements rather than a generic per-kilogram machining price.
No. The chart reports selected ATI plate tensile and yield minima. Grade 5 titanium fatigue strength needs relevant design data, loading, geometry, surface condition and agreed evidence. No finished-part fatigue life follows from these plate bars.
For your Grade 5 titanium machining services inquiry, ask how the supplier connects Ti-6Al-4V stock identity, supported datums, a first sample and receiving records. Agree Grade 5 titanium machining tolerances feature by feature; a generic certificate or tolerance claim does not quote your drawing.