

Injection Molding
Tooling and molding for your repeat plastic parts.
From prototype to production, coordinated manufacturing solutions for your custom parts.
View All Services →
Precision parts for your tight tolerances and complex geometry.
Tooling and molding for your repeat plastic parts.

Metal casting options for your part and production volume.

Cutting, forming and welding for your fabricated parts.

Custom profiles for your section, length and finish requirements.

Finishes for your appearance, corrosion and wear requirements.

Sub-assemblies and final builds for your production program.

Production tooling built around your process and volume.

Prototype parts to check fit, function and design.
DFM, process planning and production support for your project.
Inspection, documentation, inventory and delivery planning for your program.
Choose air- or liquid-cooling components around your thermal and mechanical requirements.

Manufacturing support for your cold plates, manifolds and cooling assemblies.

Find components for your power electronics, energy, laser and telecom application.

Components for your electronic systems.
Start with your functional and quality requirements.
Build around your operating environment.
From prototype to production, review material performance, manufacturability and cost for your part.
Review grade, temper and finish for your metal parts.
 AluminumStrength, weight and machining›
 Stainless SteelCorrosion and finish requirements›
 Carbon & Alloy SteelDiscuss grade and heat treatment›
 Tool SteelDiscuss tooling and wear needs›
 TitaniumReview grade and part geometry›
 Copper & Brass & BronzeDiscuss conductivity and machining›
Match your polymer to function, process and environment.
 ABSReview enclosure and molding needs›
 Polycarbonate (PC)Discuss clarity and impact needs›
 Nylon (PA)Review moisture and wear conditions›
 POM / AcetalReview fit and sliding features›
 PEEKDiscuss operating conditions›
 PTFEReview friction and chemical exposure›
 ULTEM / PEIDiscuss thermal and electrical needs›
Confirm grade availability and application requirements.
 Silicone / LSRDiscuss flexible component needs›
 TPU / TPEReview flexibility and processing›
 EPDMReview weathering and chemical exposure.›
 NBRReview oil and fuel exposure.›
 FKMReview temperature and chemical exposure.›
 G10 / FR4Review insulation and laminate needs›
 CompositesReview stiffness, weight and laminate.›Customer-Specified MaterialsConfirm your grade and requirements.›Other Specialty MaterialsDiscuss your application and grade.›
Practical guidance for your part geometry and material decisions.
Prepare your process, budget and sourcing questions.
Build your knowledge before production.
Learn who we are and how we operate.
Find our U.S. support team or start a conversation.
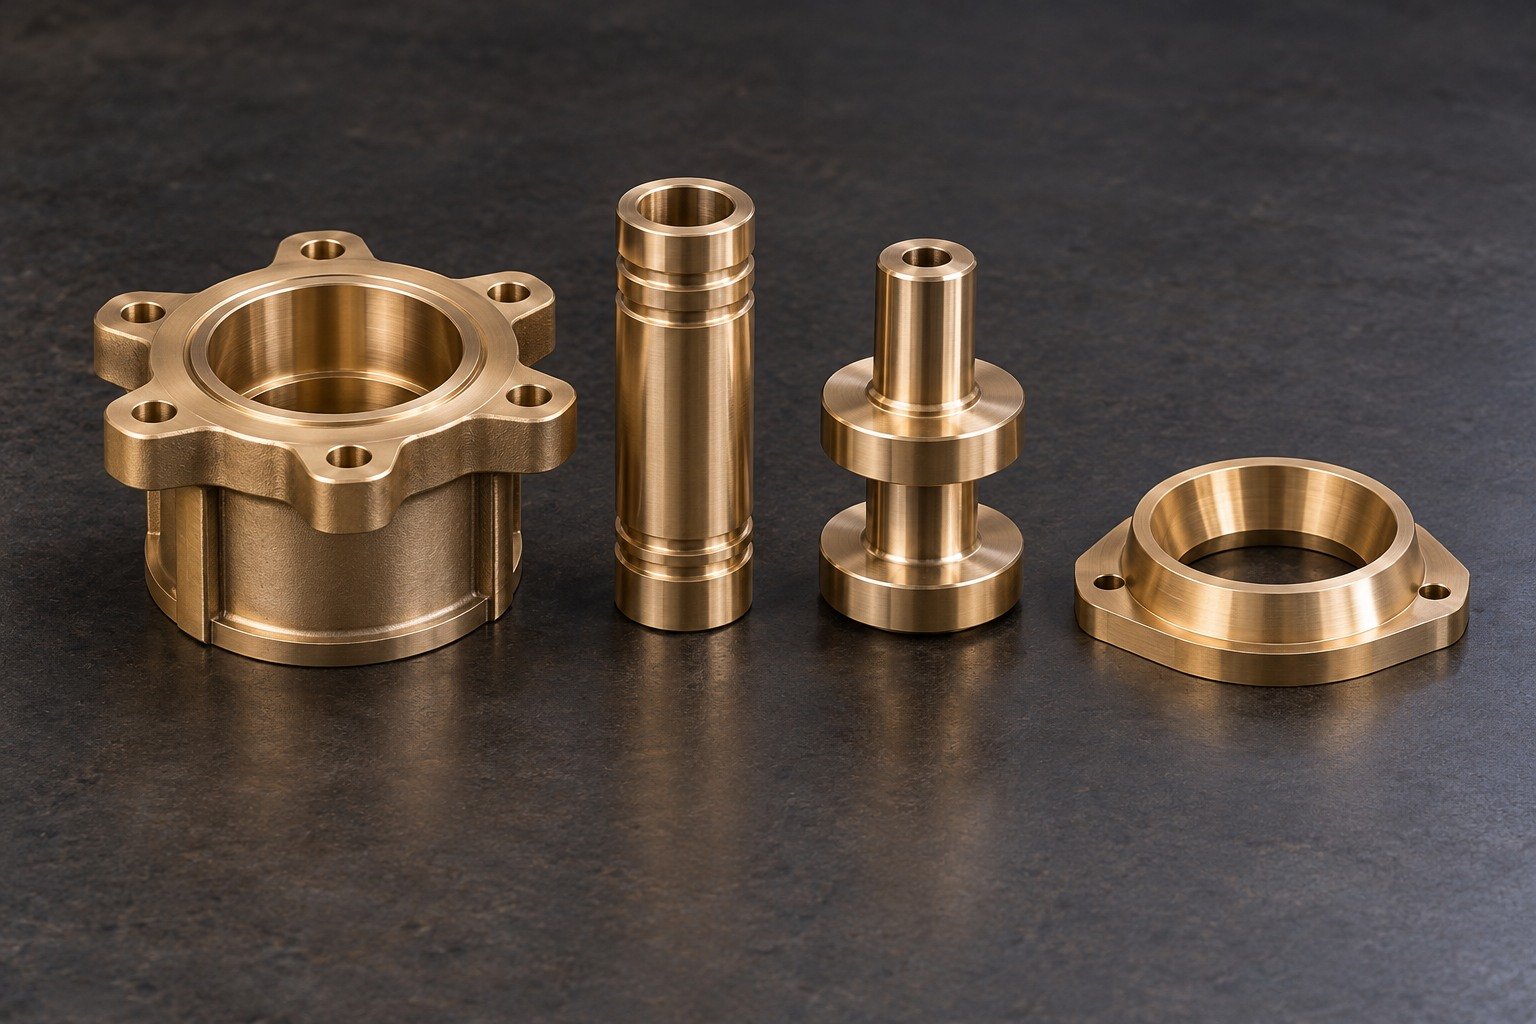
For your C63000 machining project, start with the supplied material state and the final loaded interface. Connect guides, journals and valve seats to the drawing, mating component and material evidence you need.
For your C63000 nickel aluminum bronze selection, specify C63000 chemical composition together with the product standard and supplied state. Do not treat a similar casting name as the same wrought material.
| Your callout | What to confirm |
|---|---|
| UNS C63000 | Wrought nickel-aluminum bronze; exact ordered product requirements. |
| Your C63000 AMS 4640 specification | Revision, stock form, dimensions, supplied condition and certificate scope. |
| Your C63000 HR50 stock | Selected supplier description: drawn and stress relieved. TQ50 is listed separately as temper annealed. |
| CuAl10Ni5Fe4 / CW307G | Similar European wrought reference; complete limits differ and require approval. |
C63000 hardness and mechanical acceptance depend on the actual product, dimensions and condition. HR50 and TQ50 are supplied-state references, not universal finished-part performance claims.
| Selected element | AMS 4640 producer reference · wt.% |
|---|---|
| Aluminum | 9.0–11.0 |
| Nickel | 4.0–5.5 |
| Iron | 2.0–4.0 |
| Manganese | ≤1.50 |
| Zinc | ≤0.30 |
| Silicon | ≤0.25 |
| Tin | ≤0.20 |
| Copper · includes Ag | Remainder |
Selected Concast AMS 4640 reference. Copper reporting includes Ag; Cu + named elements ≥99.5% is a combined total, not a pure-copper minimum. The complete ordered requirements govern.
Concast references · common scale 0–12
Free-cutting brass = 100 · common scale 0–100
Selected Concast references: C63000 wrought-product AMS 4640; C95800 and C95400 continuous-cast ASTM B505/B505M-23. Aluminum content does not approve substitution. Cutting indices are not ratios of cycle time, cost, tool life, load capacity or service life.
Concast C63000 ↗ Concast C95800 ↗ Concast C95400 ↗ Zollern similar wrought comparison ↗
Select the loaded bushing, guide, pump shaft or seat. Review the interface and required receiving evidence before repeating the route.
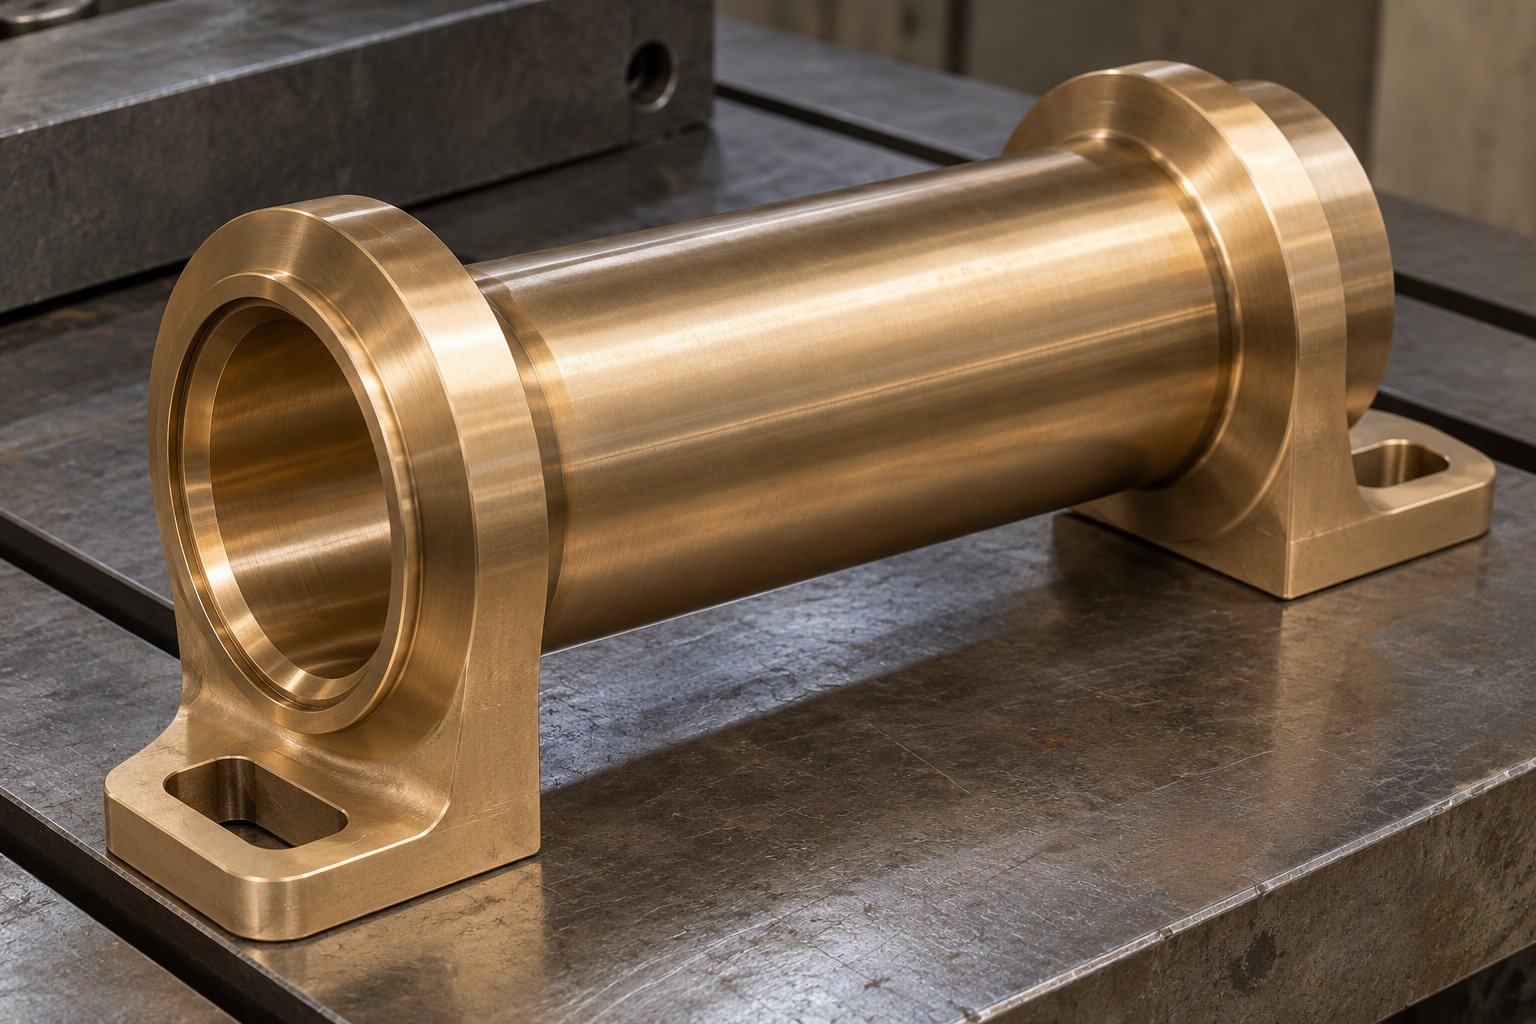
For your custom C63000 bushings, define the actual shaft, housing and working land. The drawing must identify the installation state and lubrication requirements.
| Your decision | What to define |
|---|---|
| Your fit | Bore, housing restraint, mounting lugs, working land and lubrication ports. |
| Your route | Stock condition, support and finishing sequence. |
| Your approval | Final geometry, surface and receiving evidence. |

For C63000 boring, review support and inspection access through the entire working length.
| Your decision | What to define |
|---|---|
| Your fit | Bore, housing restraint, mounting lugs, working land and lubrication ports. |
| Your route | Stock condition, support and finishing sequence. |
| Your approval | Final geometry, surface and receiving evidence. |
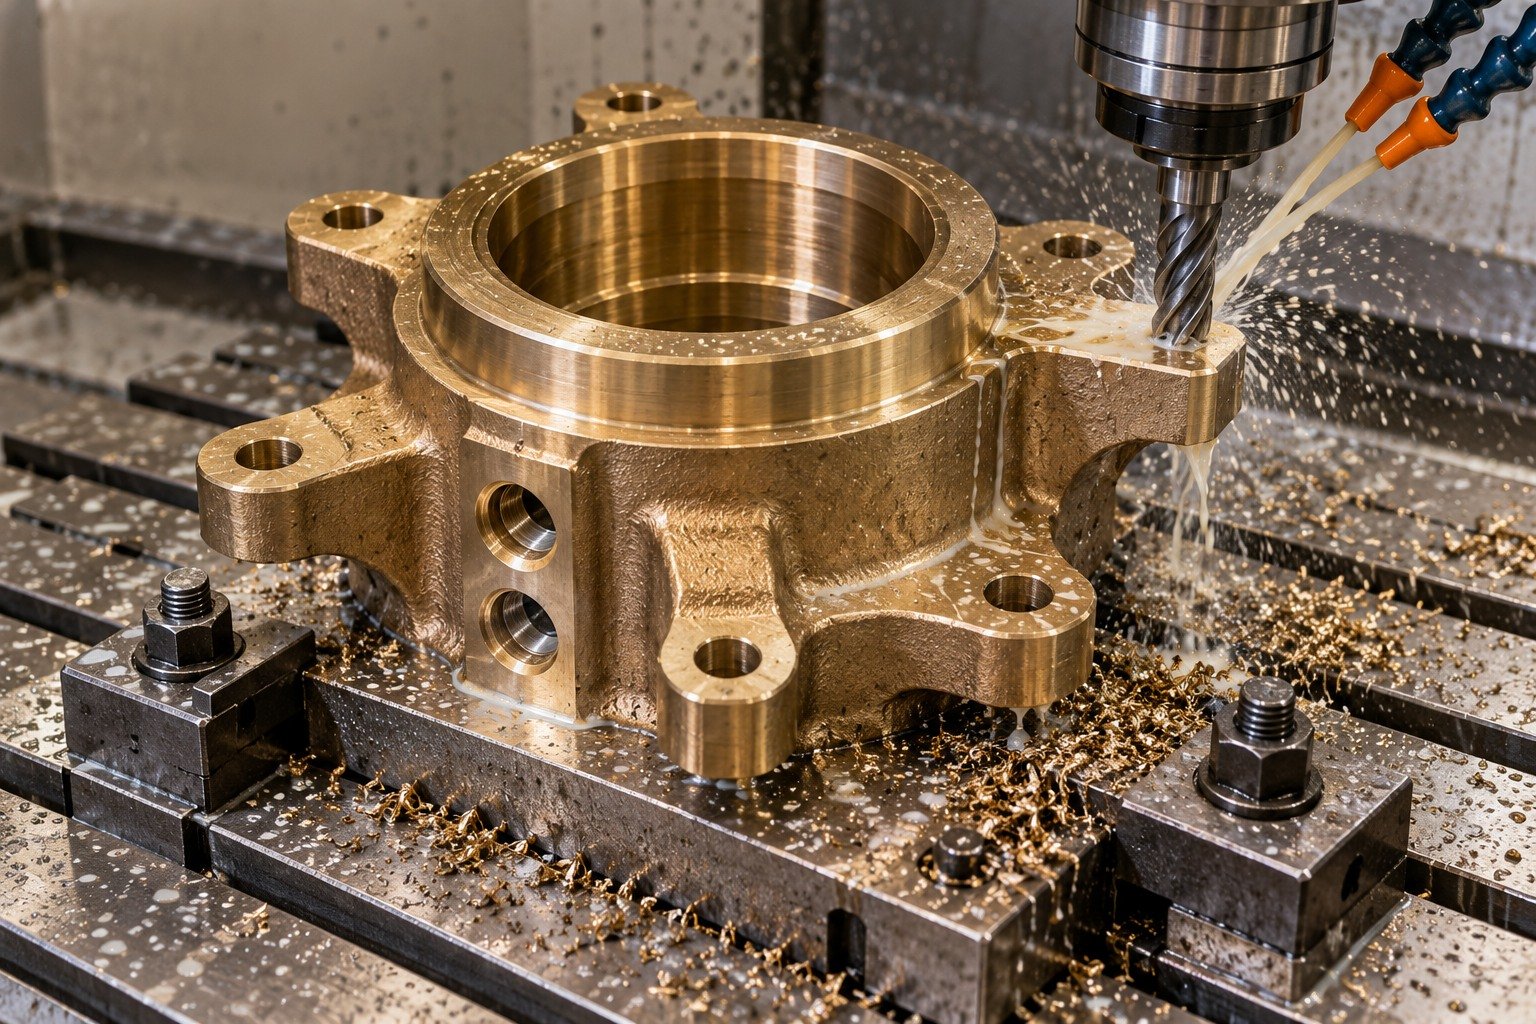
Identify exact wrought stock, ordered standard, supplied state and final material requirements.
| Your decision | What to define |
|---|---|
| Your fit | Bore, housing restraint, mounting lugs, working land and lubrication ports. |
| Your route | Stock condition, support and finishing sequence. |
| Your approval | Final geometry, surface and receiving evidence. |
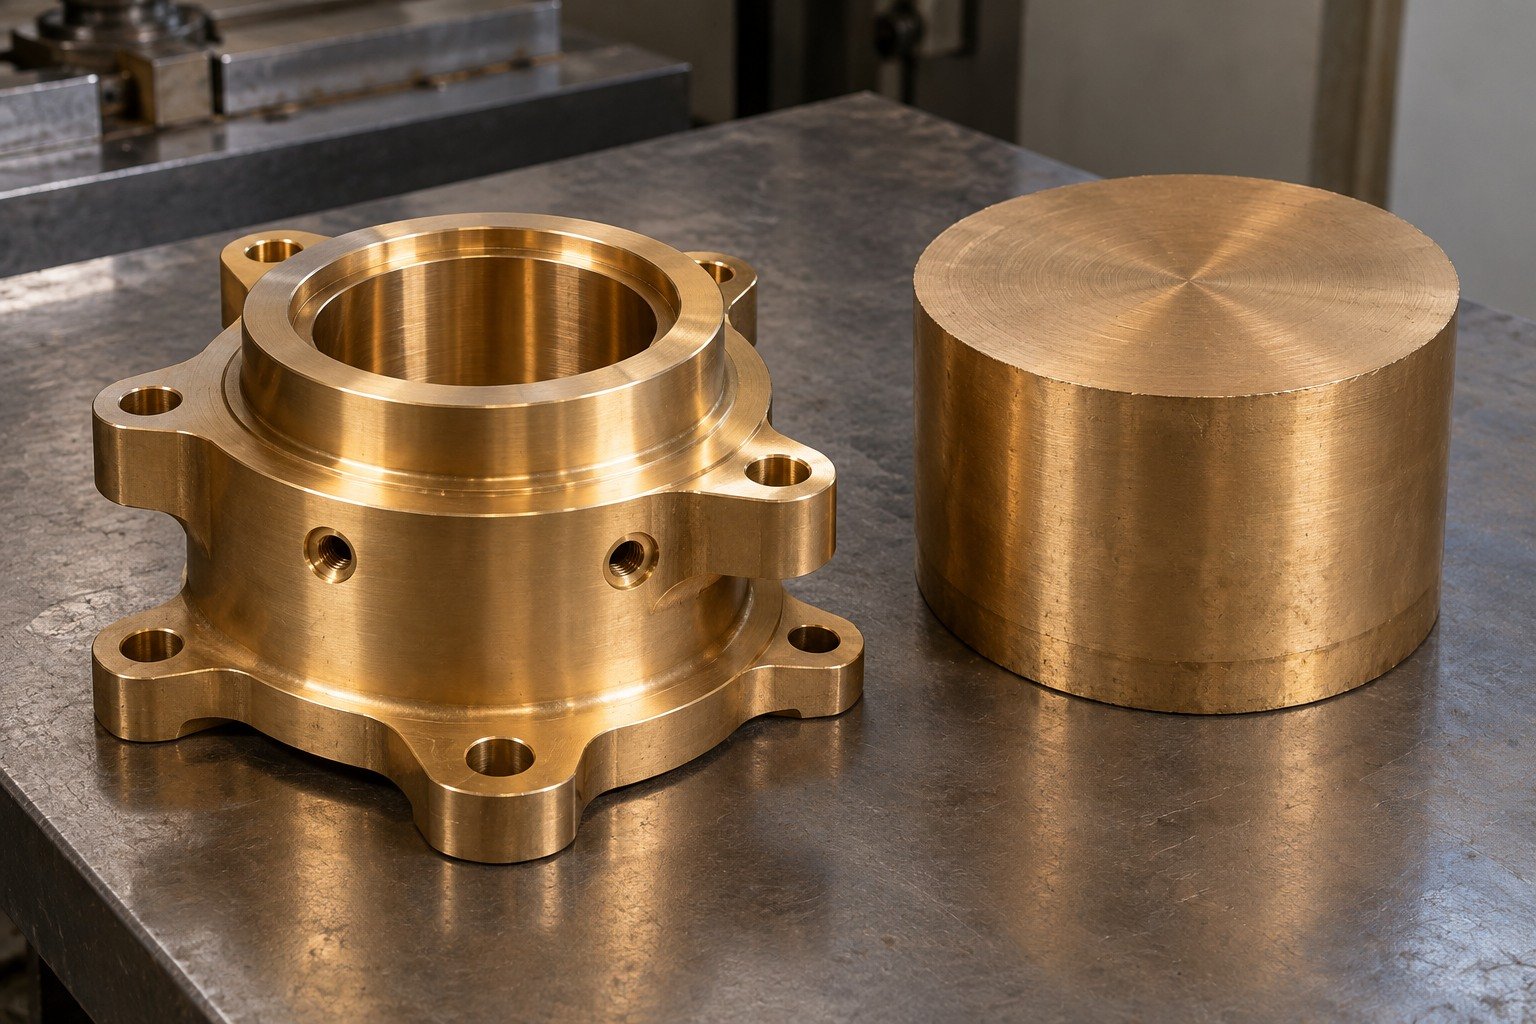
For C63000 bushings, agree free or installed measurement, accepted contact surface and any separate functional test.
| Your decision | What to define |
|---|---|
| Your fit | Bore, housing restraint, mounting lugs, working land and lubrication ports. |
| Your route | Stock condition, support and finishing sequence. |
| Your approval | Final geometry, surface and receiving evidence. |
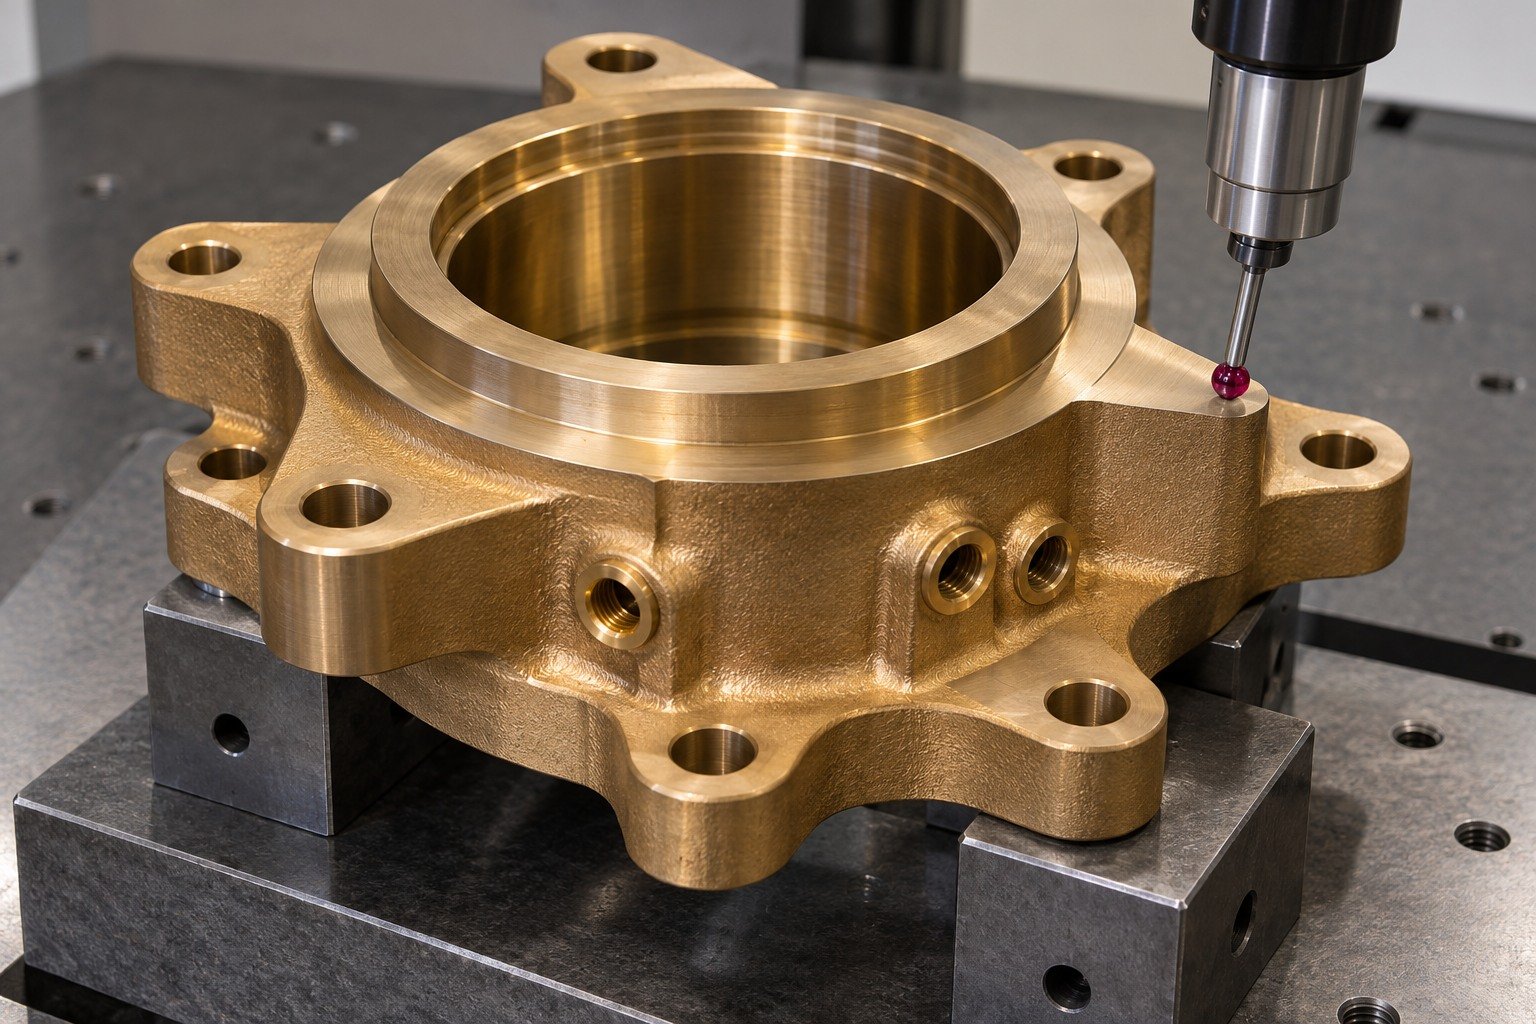
For your custom C63000 valve guides, connect the guide bore and outside lands to the valve stem and housing. Agree which features are measured after installation.
| Your decision | What to define |
|---|---|
| Your fit | Guide bore, outside lands, shoulder, mounting datum and stem relationship. |
| Your route | Stock condition, support and finishing sequence. |
| Your approval | Final geometry, surface and receiving evidence. |
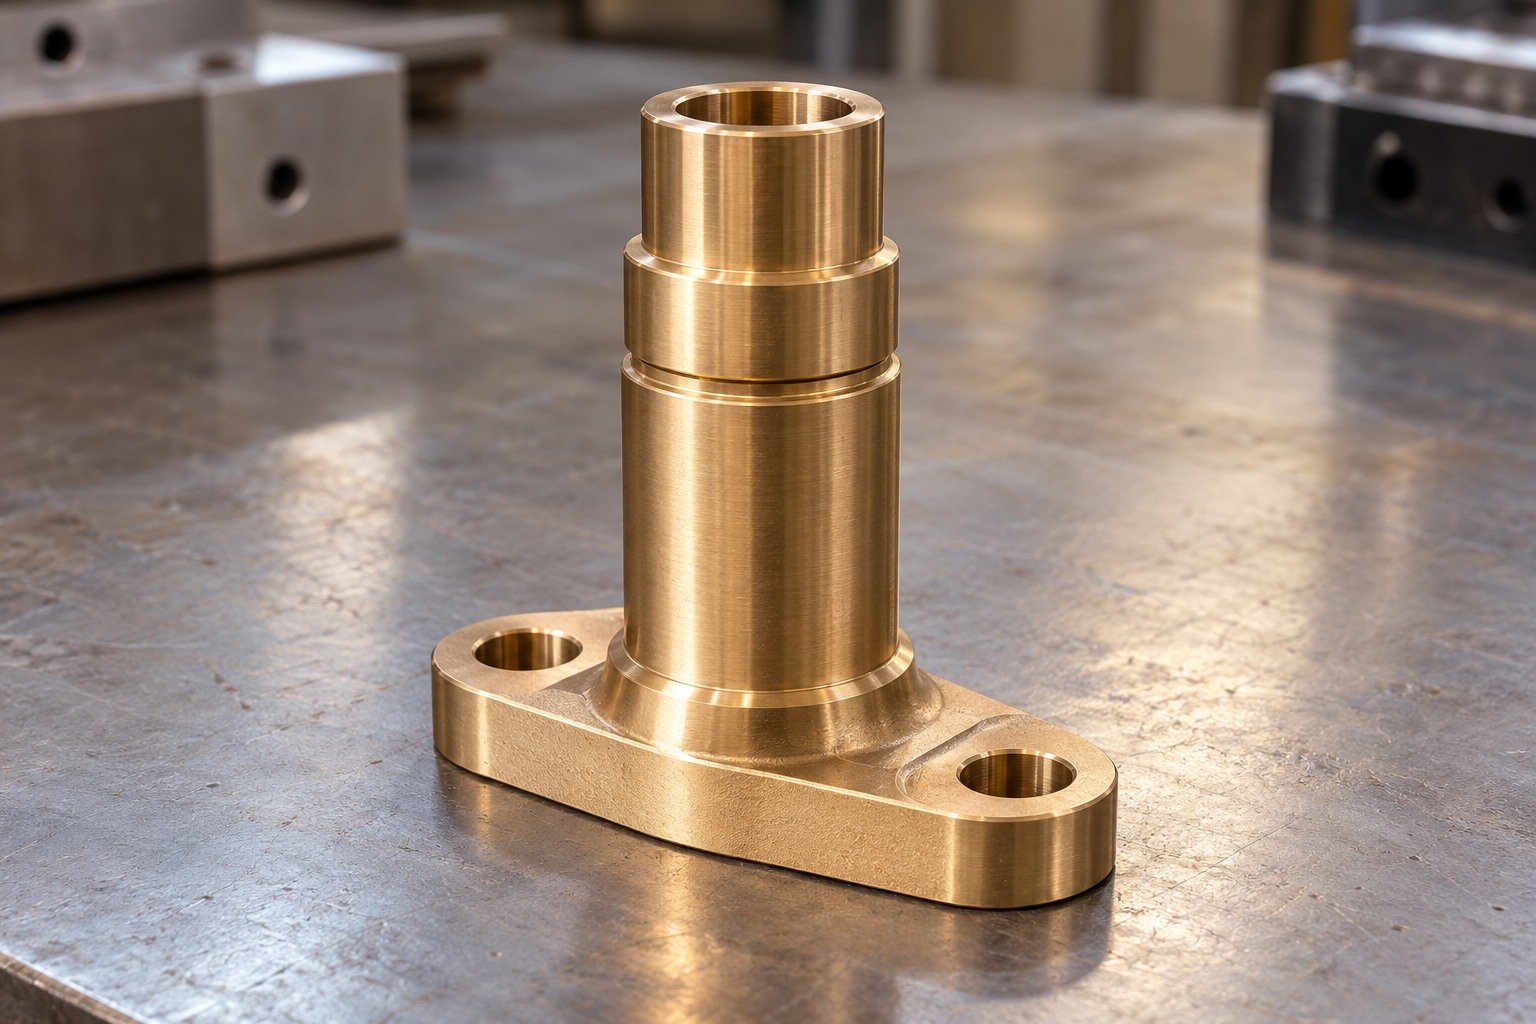
For C63000 drilling, support the mounting base and keep port intersections accessible for accepted edge removal.
| Your decision | What to define |
|---|---|
| Your fit | Guide bore, outside lands, shoulder, mounting datum and stem relationship. |
| Your route | Stock condition, support and finishing sequence. |
| Your approval | Final geometry, surface and receiving evidence. |
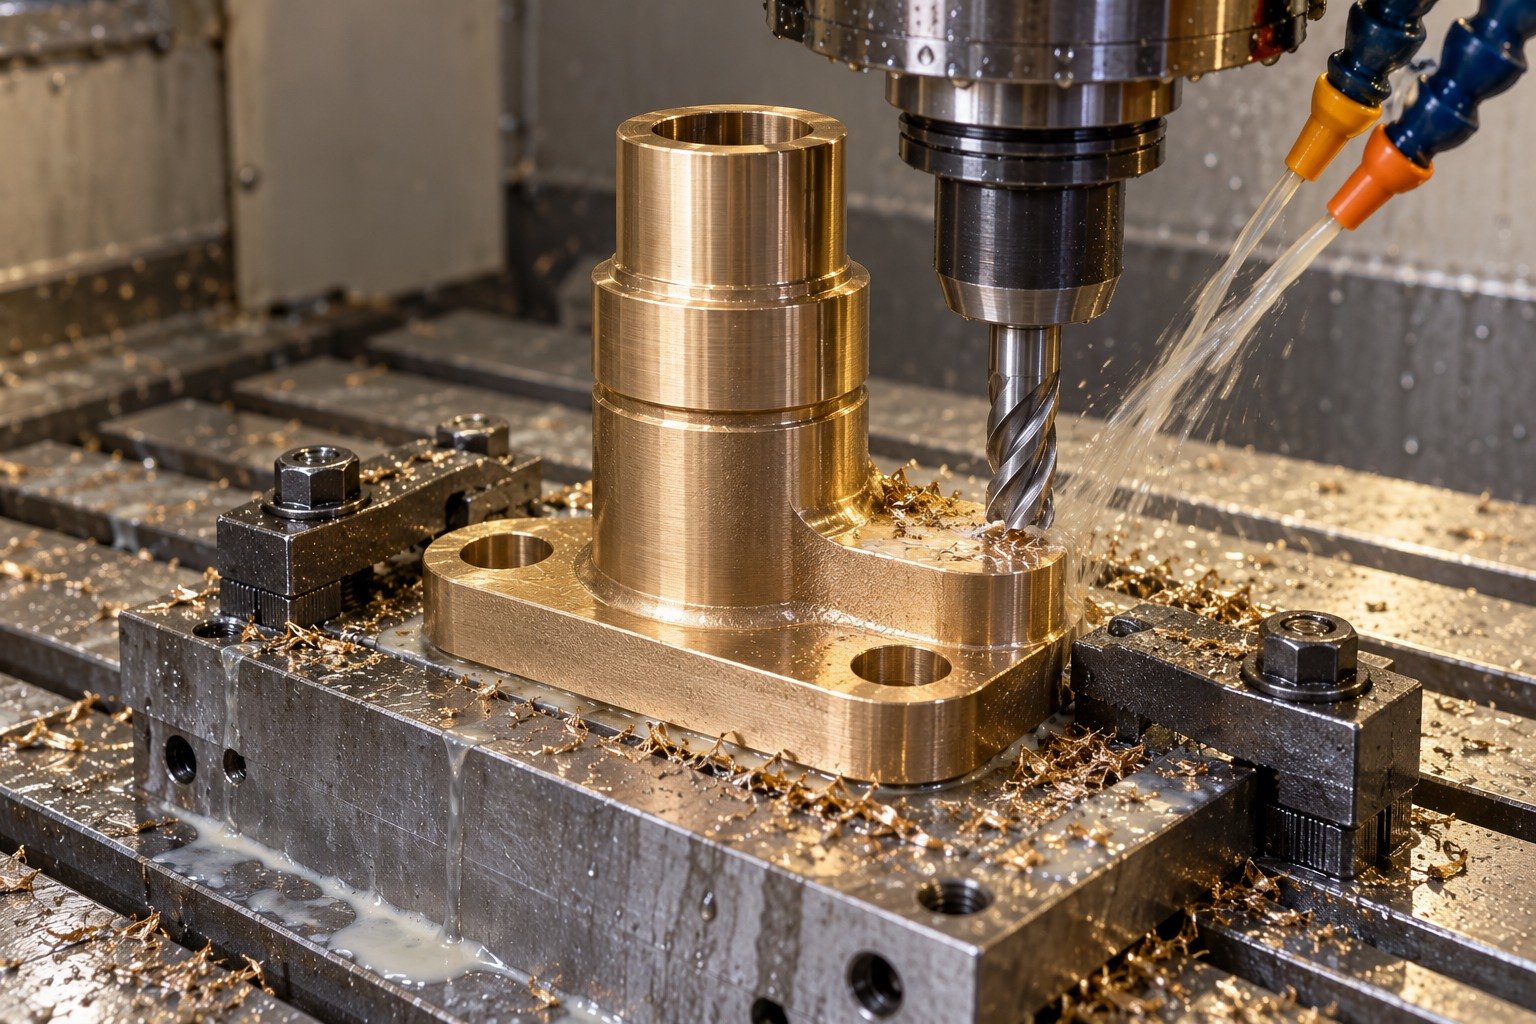
Specify stock form and supplied state before agreeing bore and external-land machining sequence.
| Your decision | What to define |
|---|---|
| Your fit | Guide bore, outside lands, shoulder, mounting datum and stem relationship. |
| Your route | Stock condition, support and finishing sequence. |
| Your approval | Final geometry, surface and receiving evidence. |
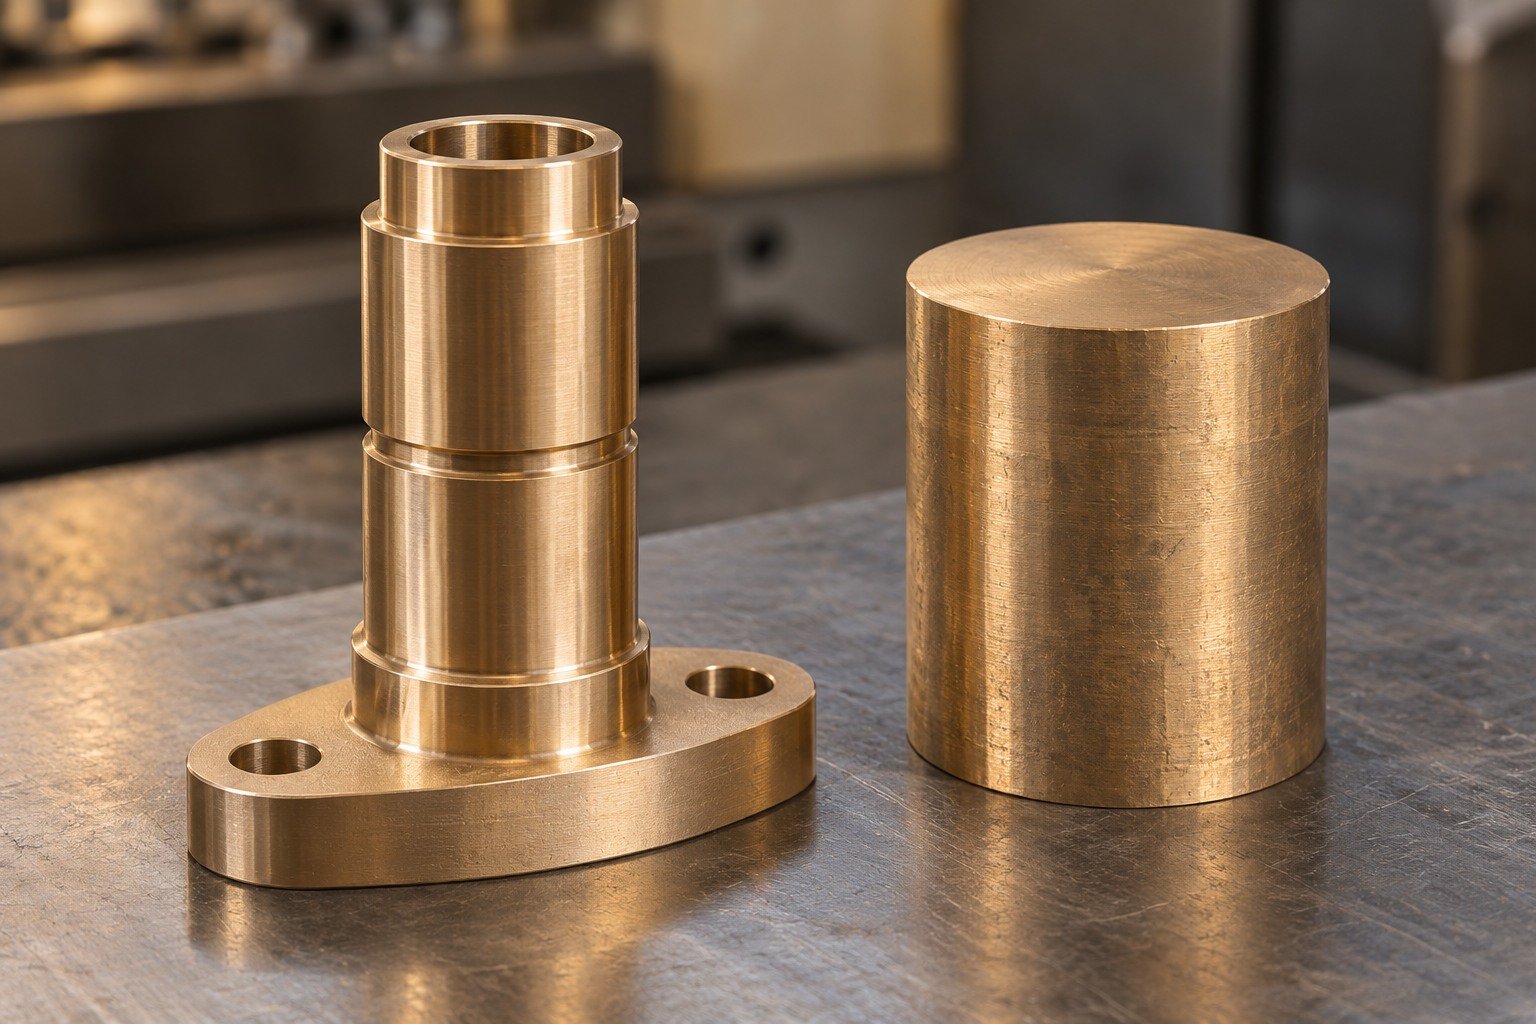
For C63000 valve guides, inspect final bore and land relationships; any functional test needs a defined method.
| Your decision | What to define |
|---|---|
| Your fit | Guide bore, outside lands, shoulder, mounting datum and stem relationship. |
| Your route | Stock condition, support and finishing sequence. |
| Your approval | Final geometry, surface and receiving evidence. |

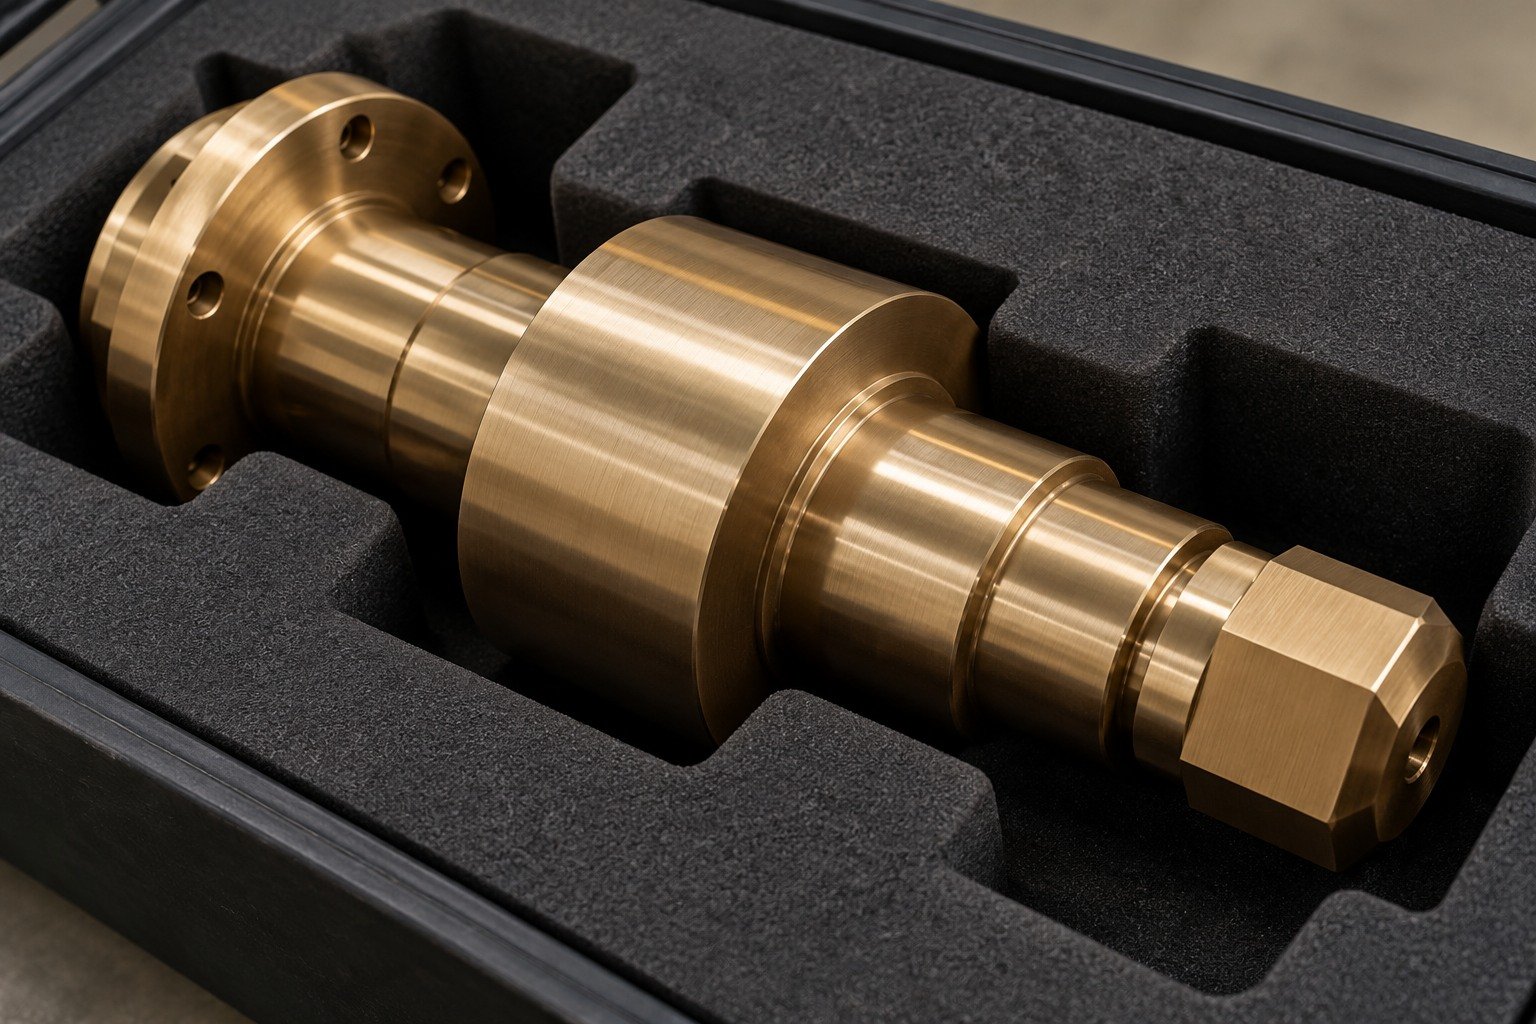
For your custom C63000 pump shafts, locate journals, shoulder and keyway from the actual coupling and bearing datums. State the finished measurement support.
| Your decision | What to define |
|---|---|
| Your fit | Journal axes, shoulder positions, keyway, end engagement and assembly datums. |
| Your route | Stock condition, support and finishing sequence. |
| Your approval | Final geometry, surface and receiving evidence. |
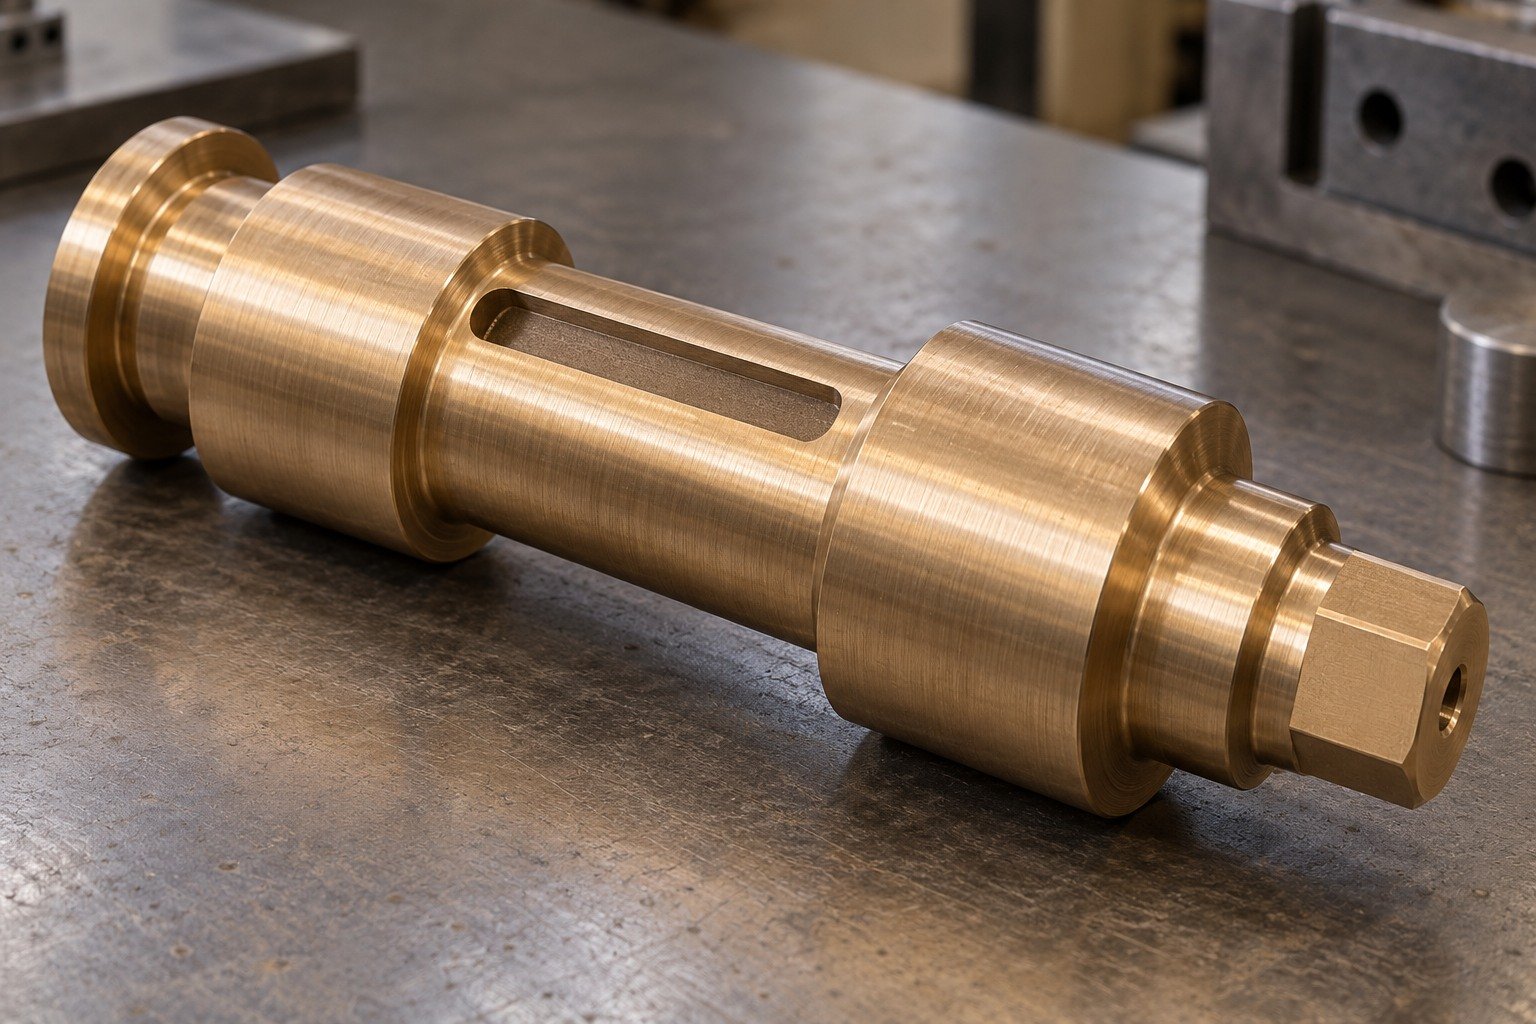
For C63000 turning and C63000 milling, agree journal support, setup sequence and keyway access.
| Your decision | What to define |
|---|---|
| Your fit | Journal axes, shoulder positions, keyway, end engagement and assembly datums. |
| Your route | Stock condition, support and finishing sequence. |
| Your approval | Final geometry, surface and receiving evidence. |
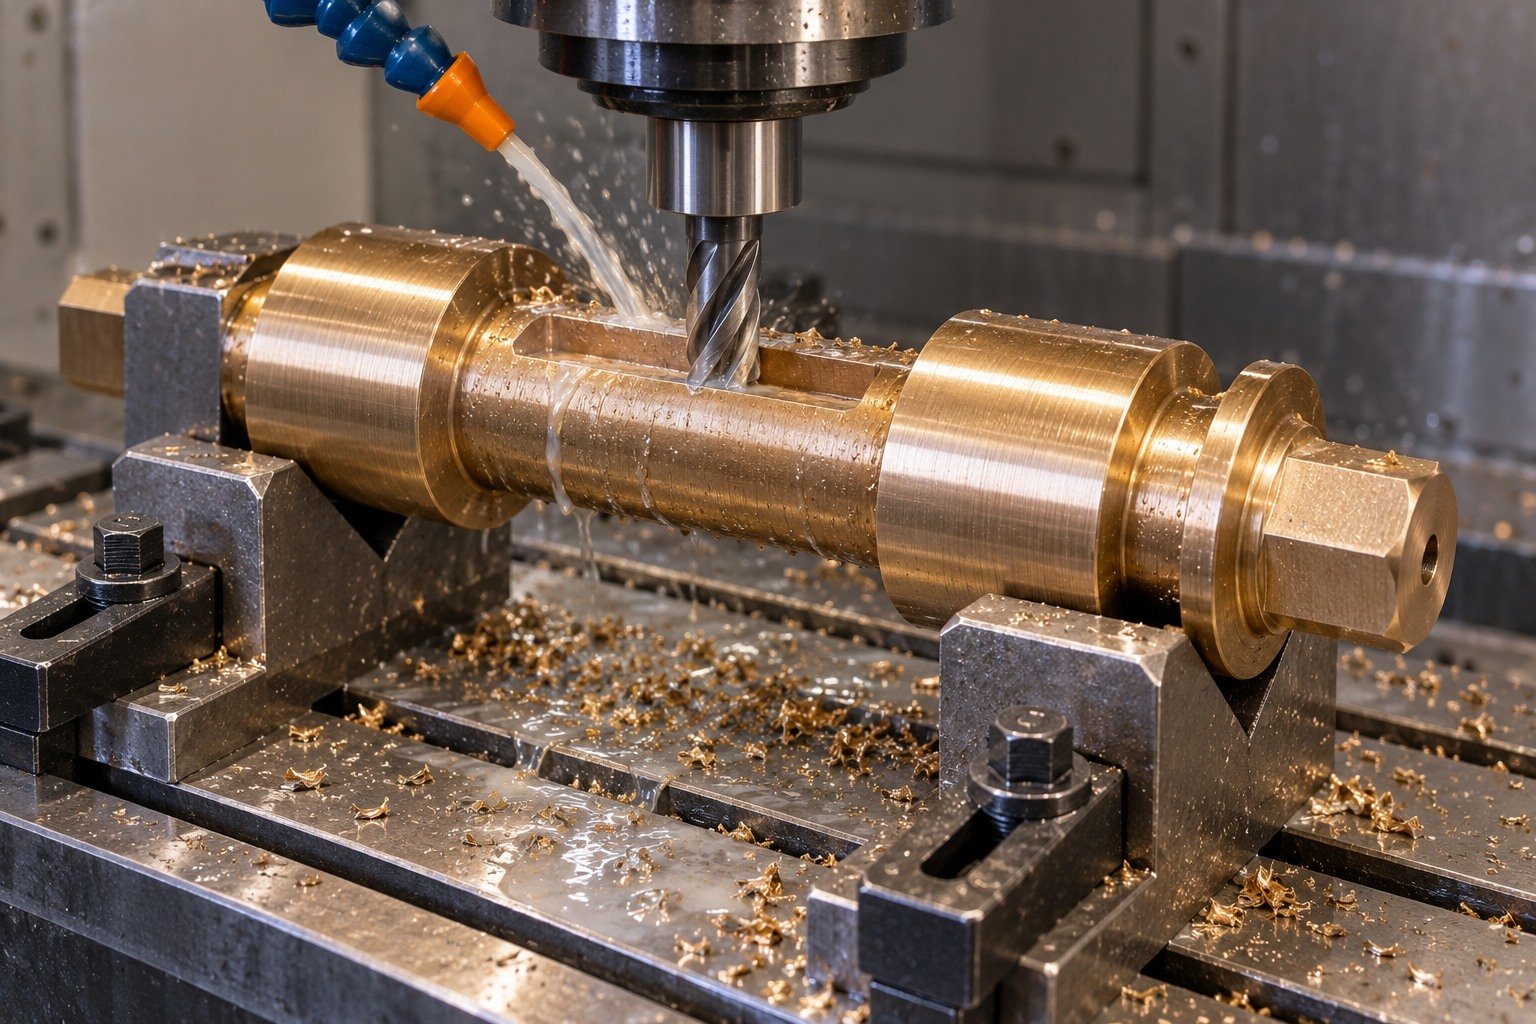
Confirm stock diameter, supplied condition, usable allowance and required material evidence.
| Your decision | What to define |
|---|---|
| Your fit | Journal axes, shoulder positions, keyway, end engagement and assembly datums. |
| Your route | Stock condition, support and finishing sequence. |
| Your approval | Final geometry, surface and receiving evidence. |

For C63000 pump shafts, agree runout datums and final land acceptance. Any pump-level performance requires its own test.
| Your decision | What to define |
|---|---|
| Your fit | Journal axes, shoulder positions, keyway, end engagement and assembly datums. |
| Your route | Stock condition, support and finishing sequence. |
| Your approval | Final geometry, surface and receiving evidence. |

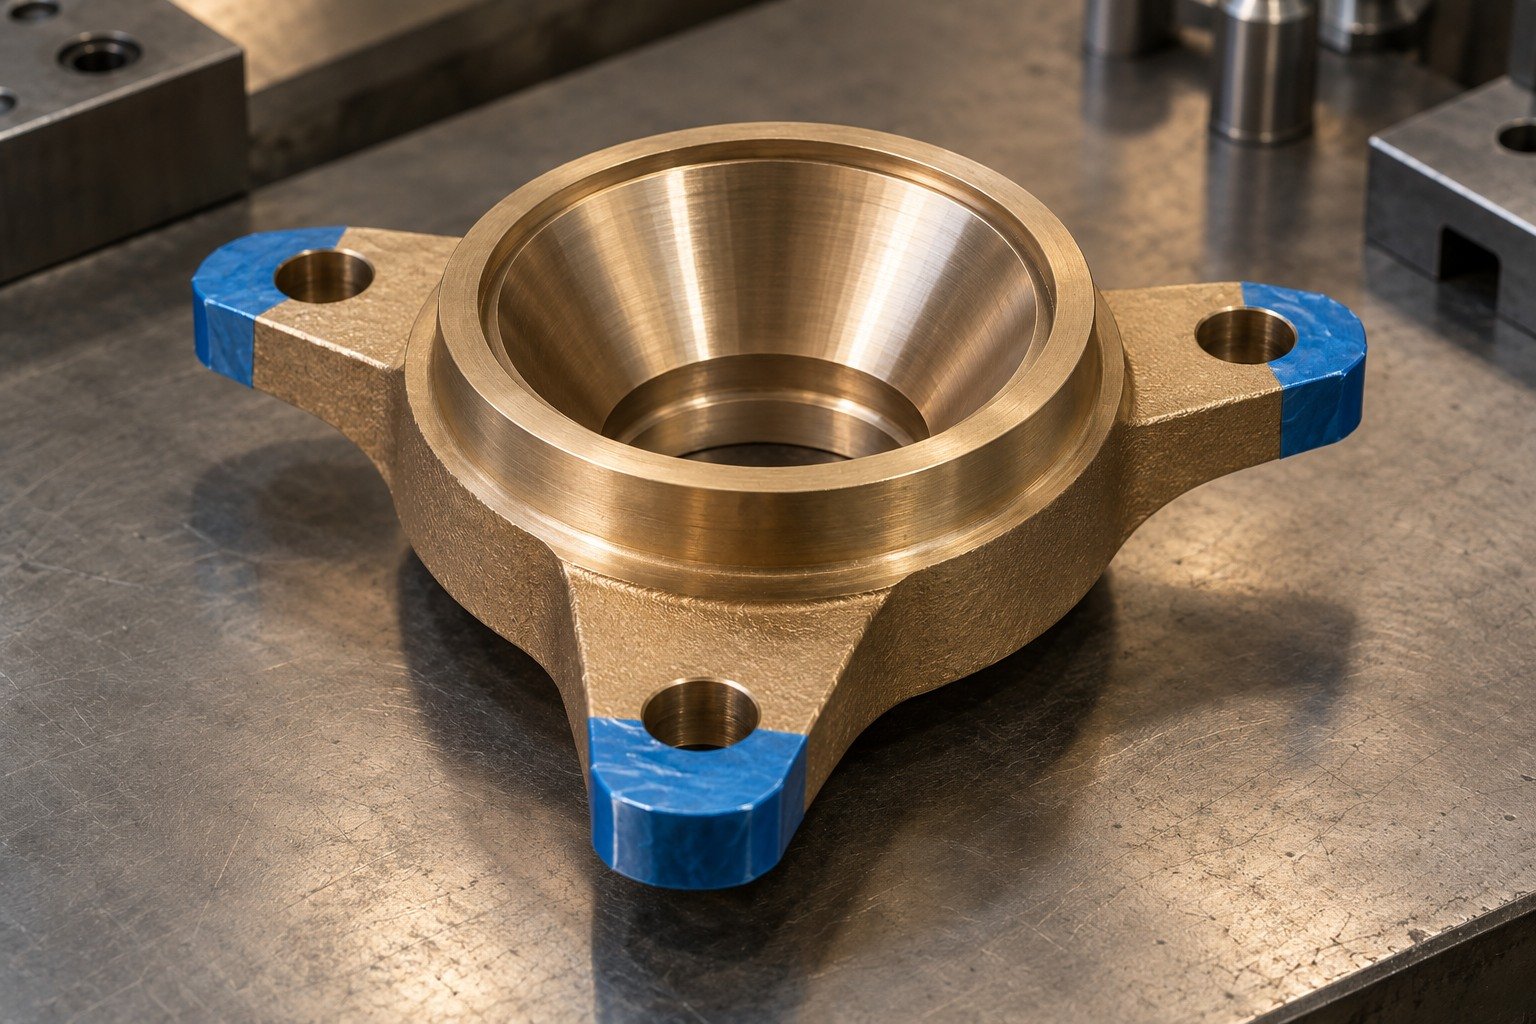
For your custom C63000 valve seats, distinguish the conical working land, locating diameter and threaded attachment. Material identity alone does not establish a pressure rating.
| Your decision | What to define |
|---|---|
| Your fit | Working cone, locating diameter, shoulder, attachment thread and accepted contact region. |
| Your route | Stock condition, support and finishing sequence. |
| Your approval | Final geometry, surface and receiving evidence. |

For C63000 threading, specify thread standard, run-out, gauge access and separation from the finished seat.
| Your decision | What to define |
|---|---|
| Your fit | Working cone, locating diameter, shoulder, attachment thread and accepted contact region. |
| Your route | Stock condition, support and finishing sequence. |
| Your approval | Final geometry, surface and receiving evidence. |

Identify exact stock and supplied state; agree final land machining after any separately specified processing.
| Your decision | What to define |
|---|---|
| Your fit | Working cone, locating diameter, shoulder, attachment thread and accepted contact region. |
| Your route | Stock condition, support and finishing sequence. |
| Your approval | Final geometry, surface and receiving evidence. |
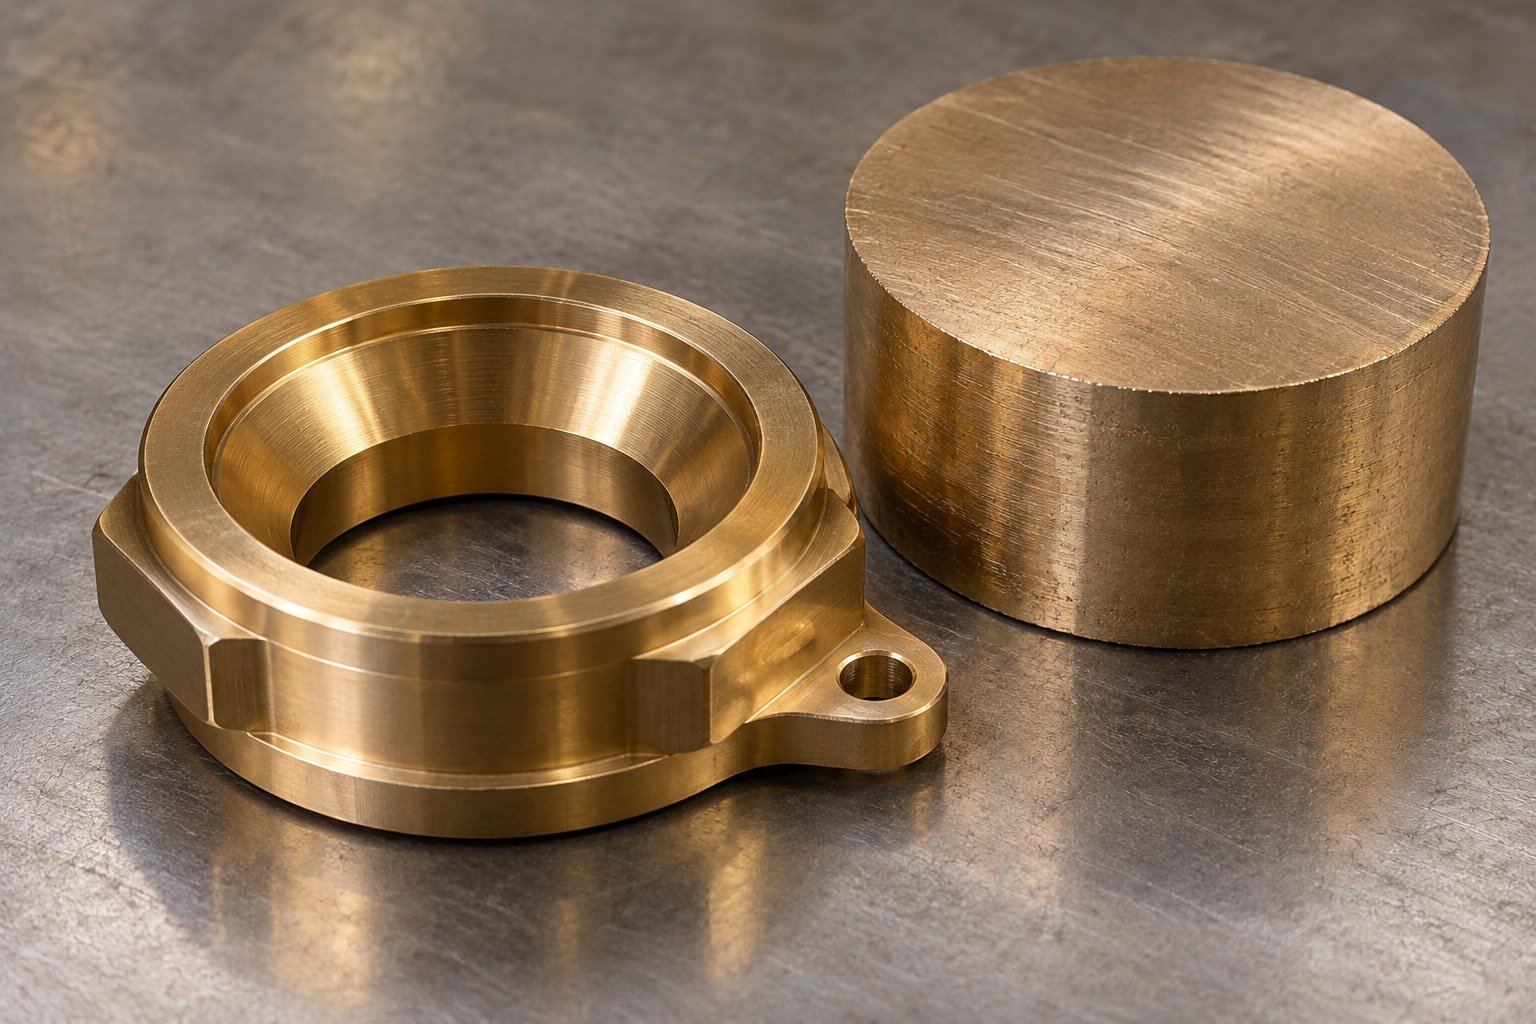
For C63000 valve seats, inspect final geometry and surface. Leak or pressure testing needs an agreed procedure and acceptance.
| Your decision | What to define |
|---|---|
| Your fit | Working cone, locating diameter, shoulder, attachment thread and accepted contact region. |
| Your route | Stock condition, support and finishing sequence. |
| Your approval | Final geometry, surface and receiving evidence. |
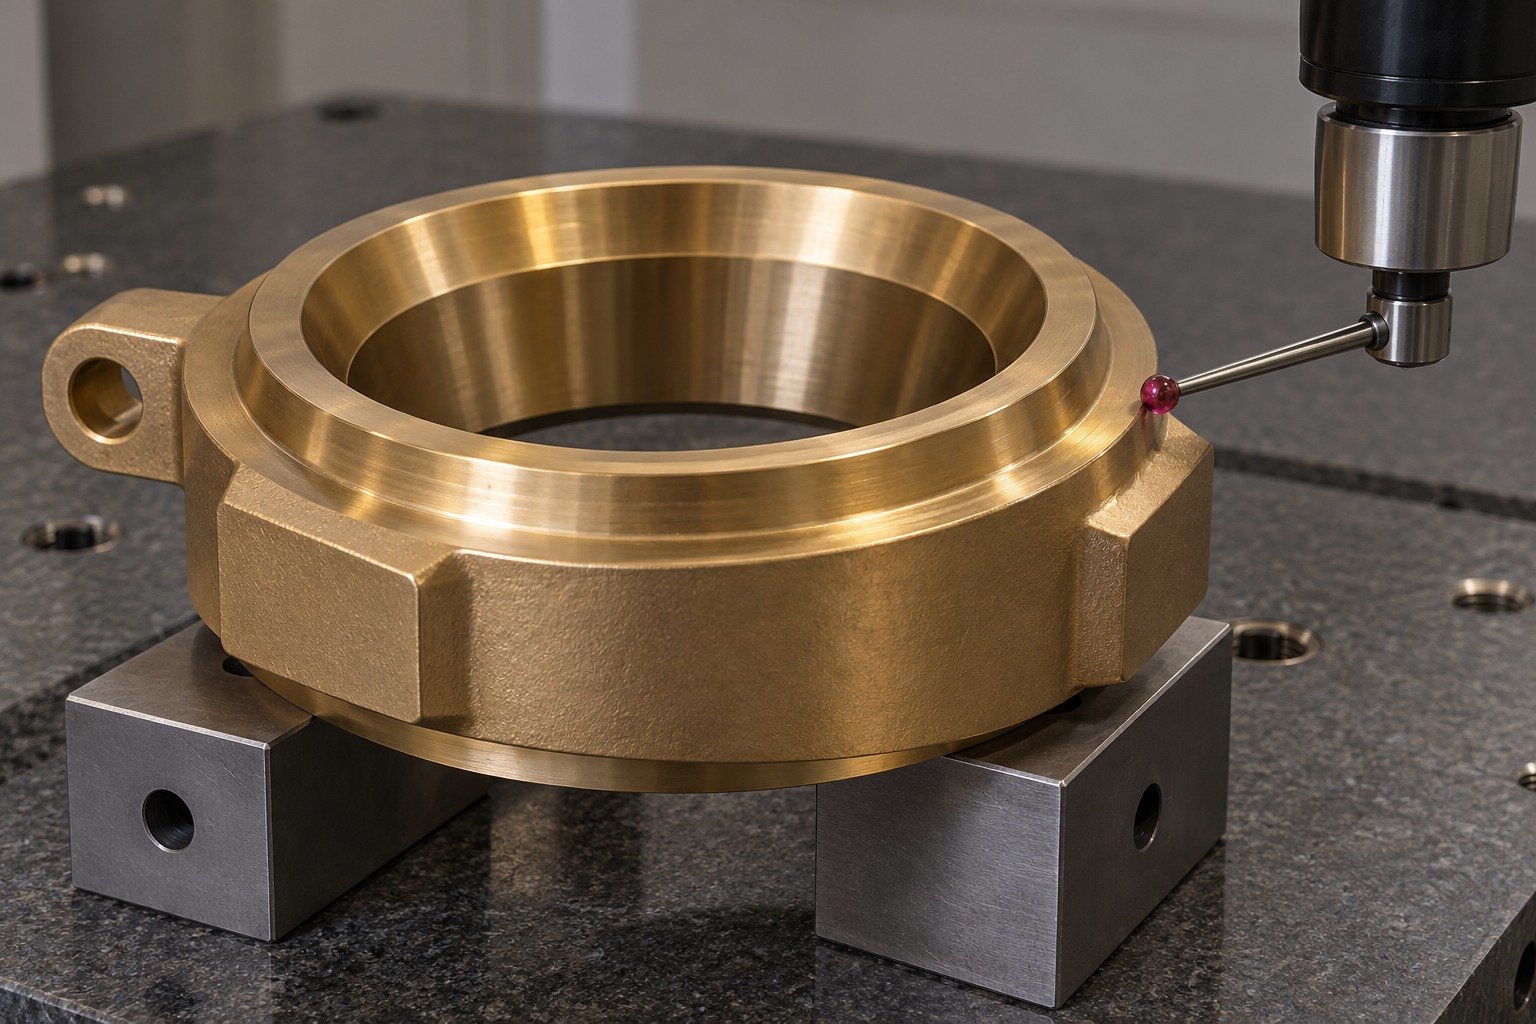
Grade, product standard and supplied state.
Supported dimensions and accepted edges.
Final function requirements and receiving records.
For your custom C63000 parts, define product standard, supplied condition and lot identity. State your C63000 material certification scope before ordering stock.
Sampling and evidence scope are agreed with your quote.
Quality Assurance →
Review bore length, lands, datums and accepted edges on a complete first sample. Resolve the measurement support before repeating quantities.
Sampling and evidence scope are agreed with your quote.
Quality Assurance →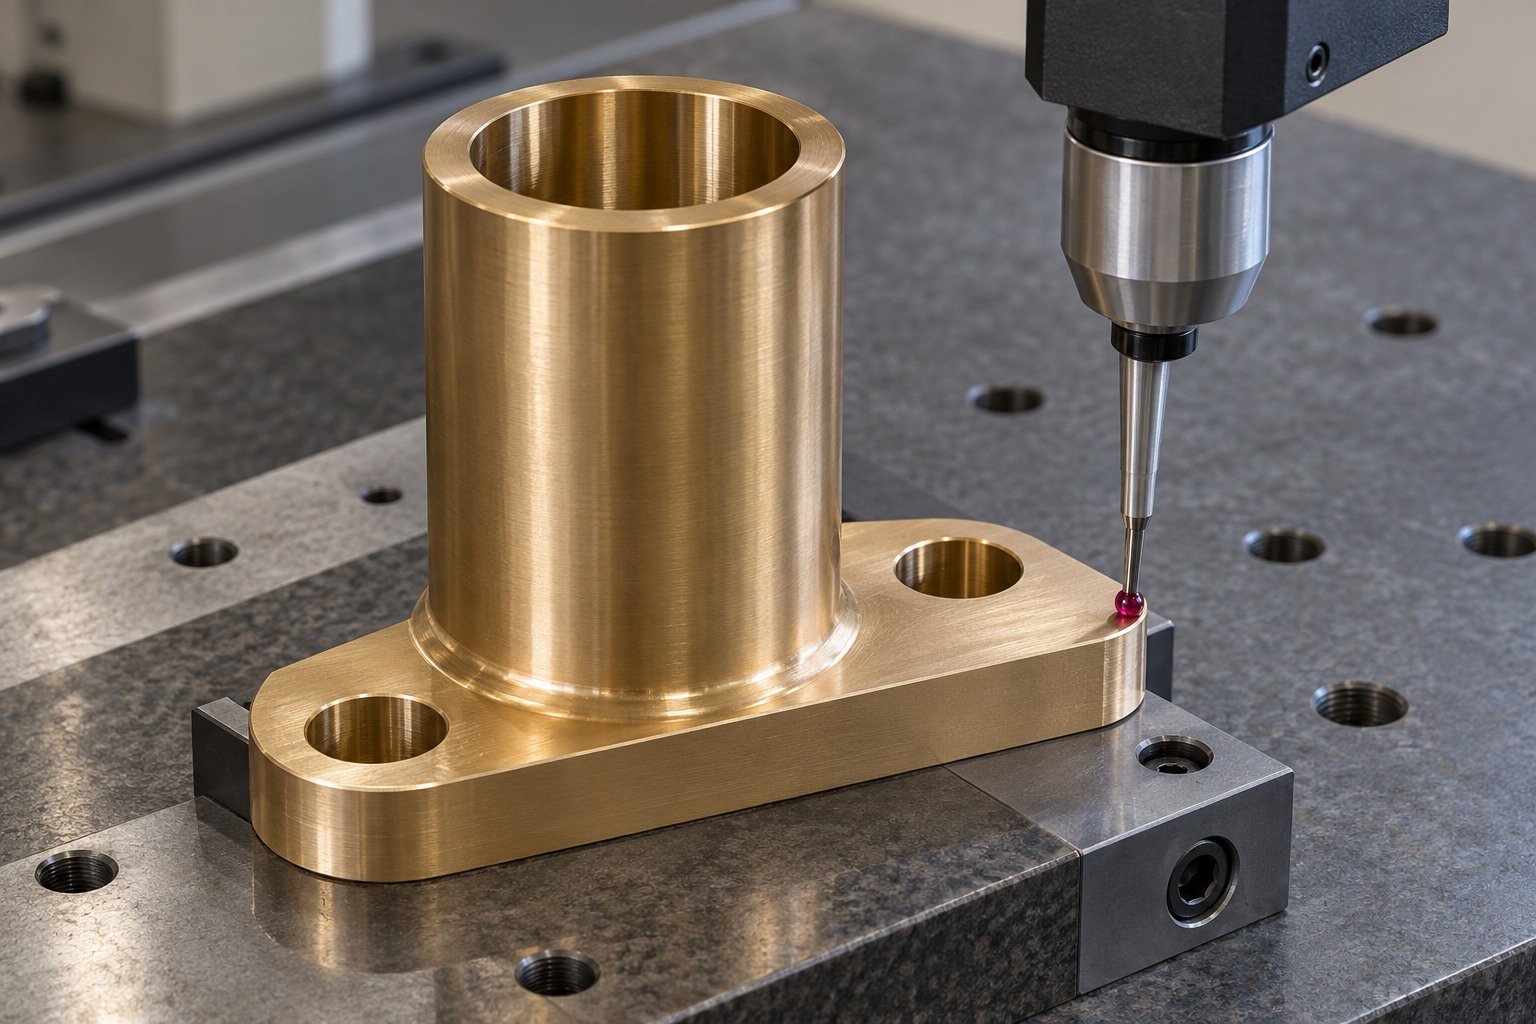
Inspect the actual final working land and attachment geometry after agreed processing. Material evidence and dimensional evidence answer separate questions.
Sampling and evidence scope are agreed with your quote.
Quality Assurance →
Your C63000 machined parts manufacturer review should agree individual protection, lot identity, material documents and inspection scope for the receiving team.
Sampling and evidence scope are agreed with your quote.
Quality Assurance →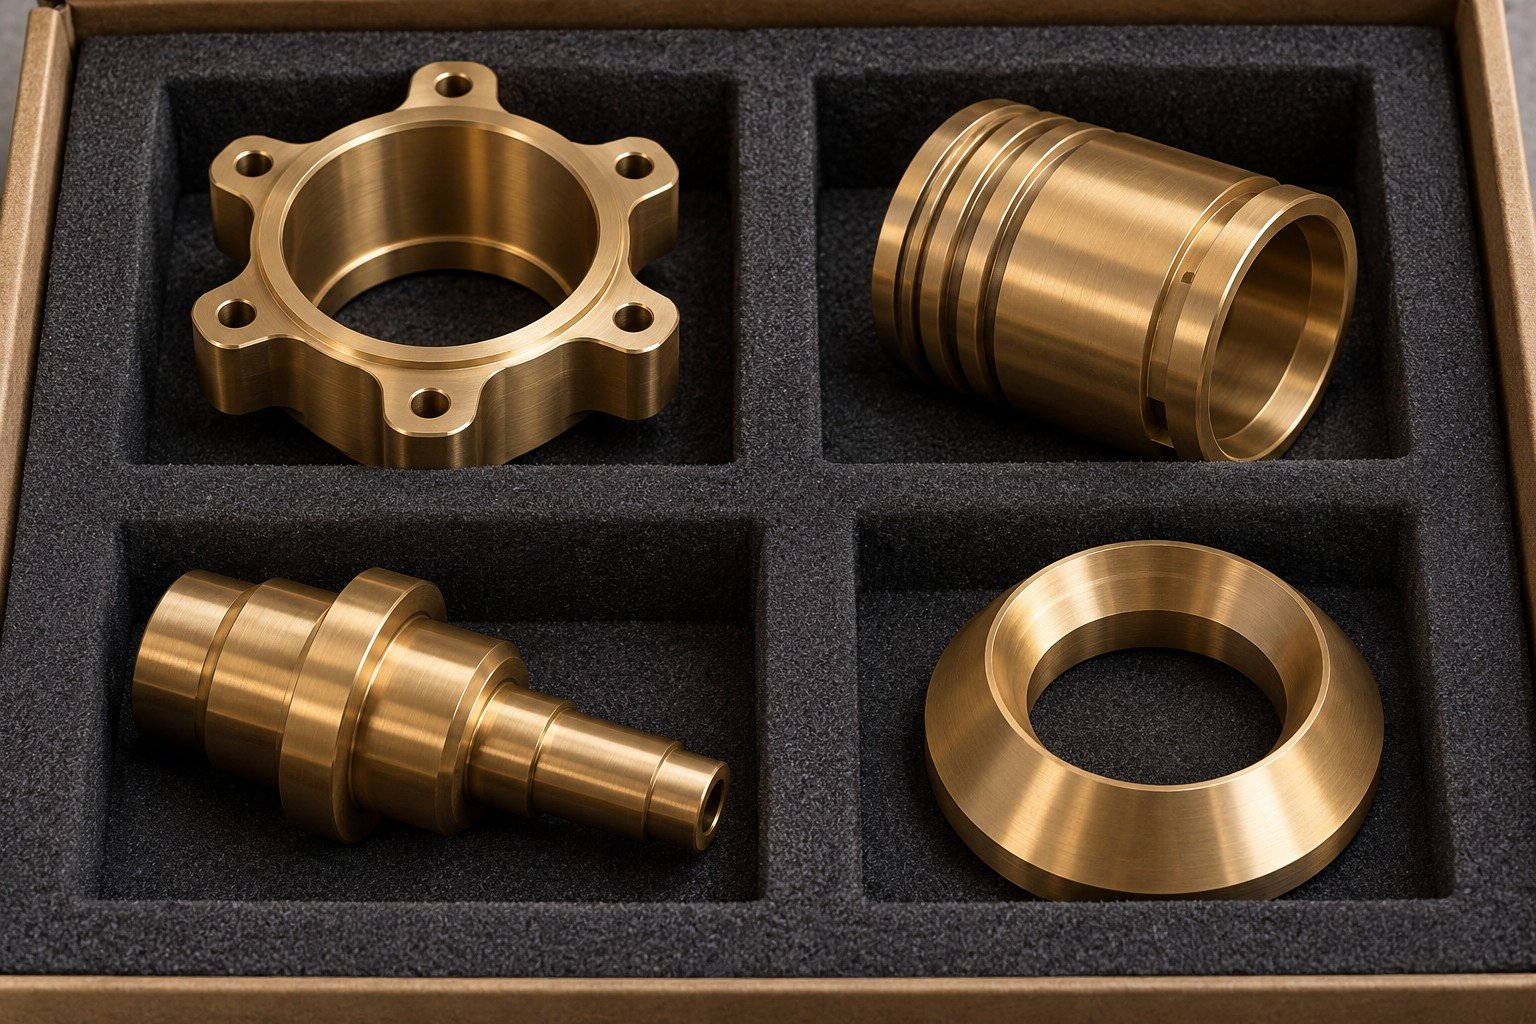
For C63000 CNC machining, agree material standard, ordered revision, stock form, supplied state and certificate scope. Preserve the identity through machining and delivery.
Show the working feature and allowed edge condition.
Agree stock, support and final surface.
Inspect the actual finished state.

Show bore length, port intersections, locating lands and accepted edges. Define inspection access along the working feature rather than only at its entrance.
Show the working feature and allowed edge condition.
Agree stock, support and final surface.
Inspect the actual finished state.
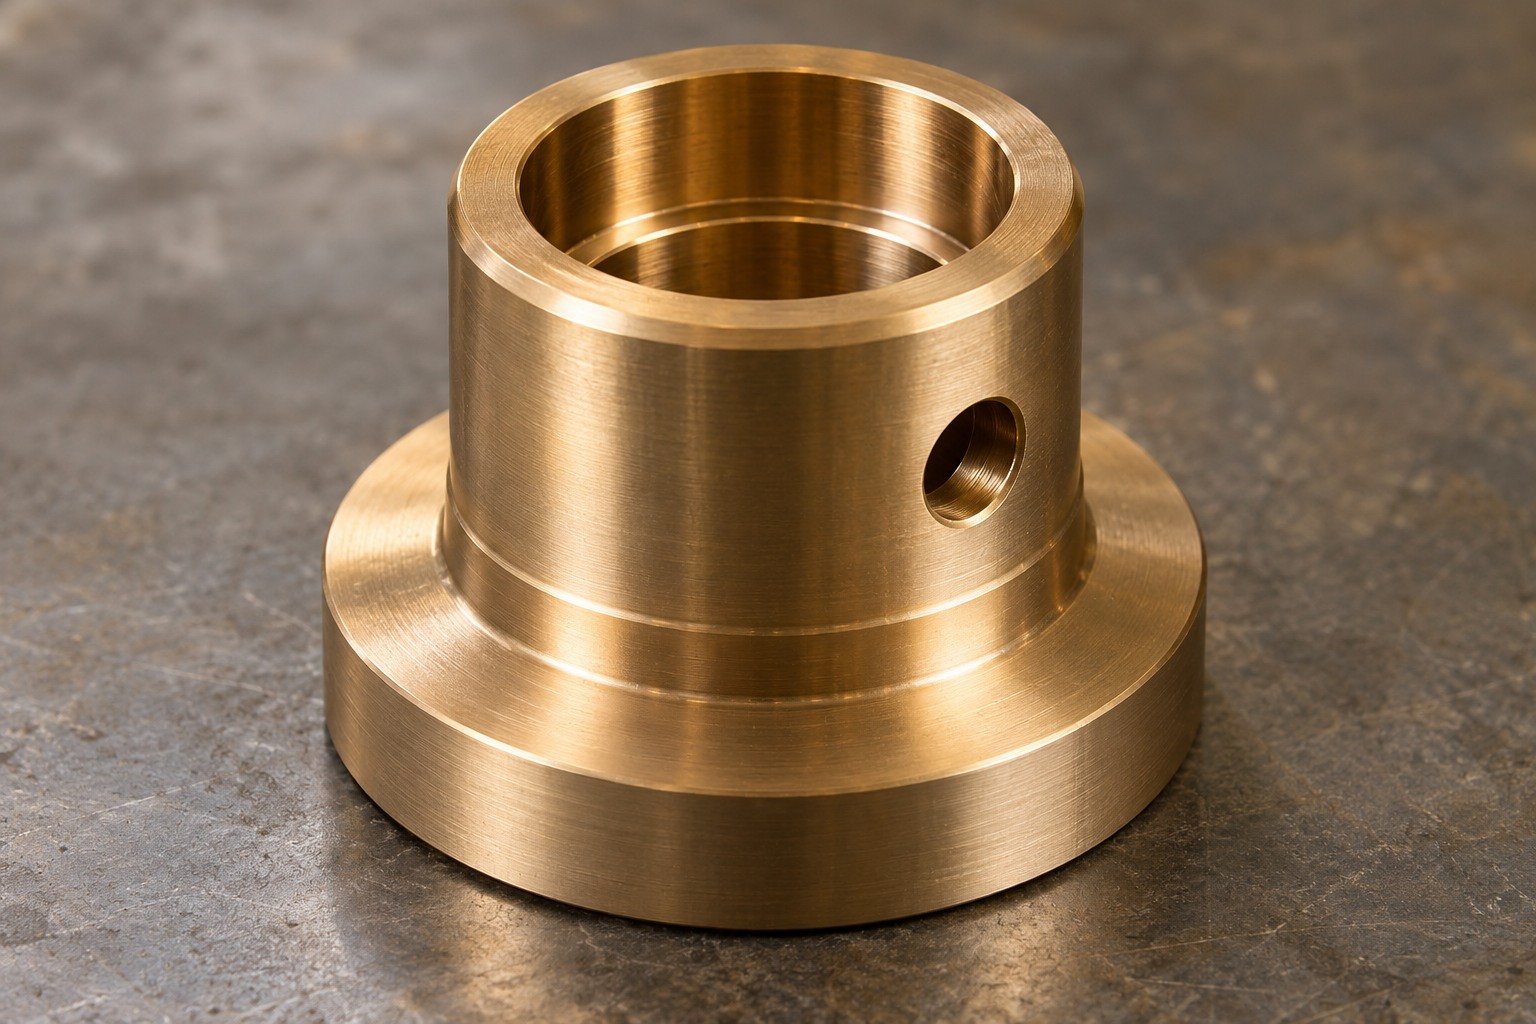
For your C63000 HR50 callout, confirm the actual stock certificate and supplied condition. Agree any later thermal or forming route and final material acceptance separately; do not transfer one condition to every part.
Show the working feature and allowed edge condition.
Agree stock, support and final surface.
Inspect the actual finished state.

Identify the working cone, guide land, allowable edge breaks and tool-mark acceptance. A material name does not specify your final contact.
Show the working feature and allowed edge condition.
Agree stock, support and final surface.
Inspect the actual finished state.
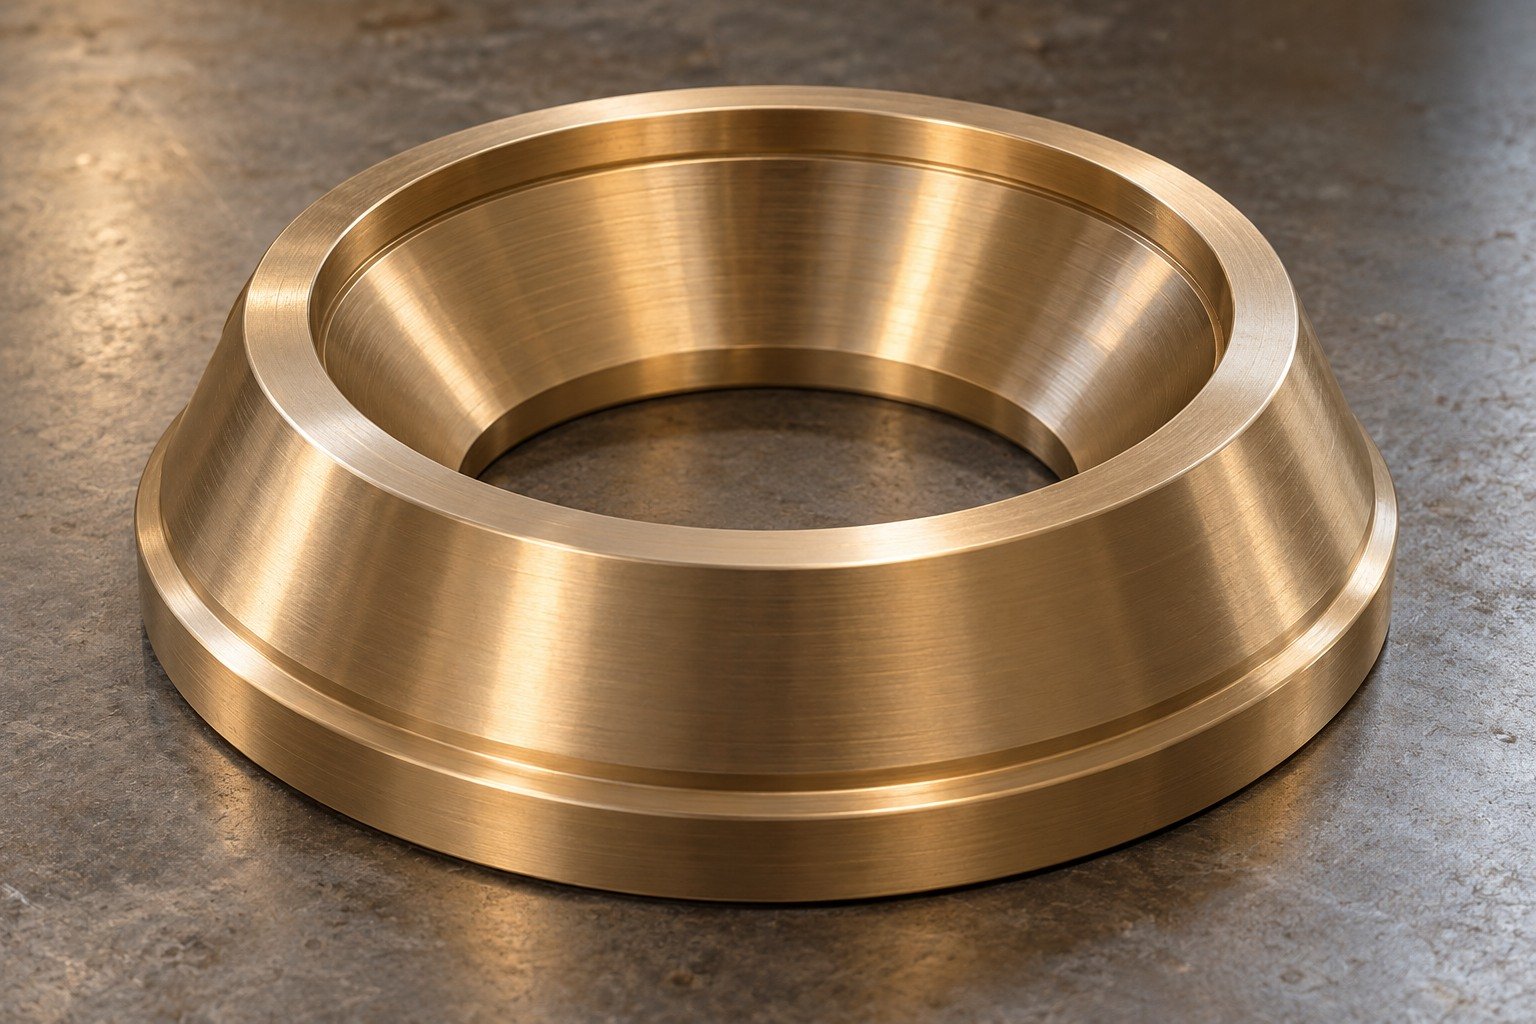
Agree roughness, cleaning, masking and protection. Any coating or surface treatment requires its own substrate, preparation, thickness and final-fit review.
Show the working feature and allowed edge condition.
Agree stock, support and final surface.
Inspect the actual finished state.

Show shaft, stem or housing, installation restraint and measurement datums. Agree any load, wear, leak or other functional test with explicit conditions.
Show the working feature and allowed edge condition.
Agree stock, support and final surface.
Inspect the actual finished state.
For your C63000 machining services inquiry, connect material state, setups, final working lands and inspection to one controlled drawing. Your quote confirms the accepted route and evidence scope.

Support the guide base and define port exits and internal-edge access.
Review the Process →
Connect bore length, seat geometry, run-out and final gauge access.
Review the Process →| Your check | What to approve |
|---|---|
| C63000 vs C95800 | Wrought and cast-product references differ; compare complete standard and supplied state. |
| HR50 or TQ50 | Confirm the actual ordered condition and final receiving requirements. |
| European comparison | CuAl10Ni5Fe4 / CW307G is similar, with different full limits. |
| Final function | Define mating geometry, operating medium and any separately specified test. |
Similar alloy-family names do not approve substitution or establish assembly performance.
Bronze Alloy Overview →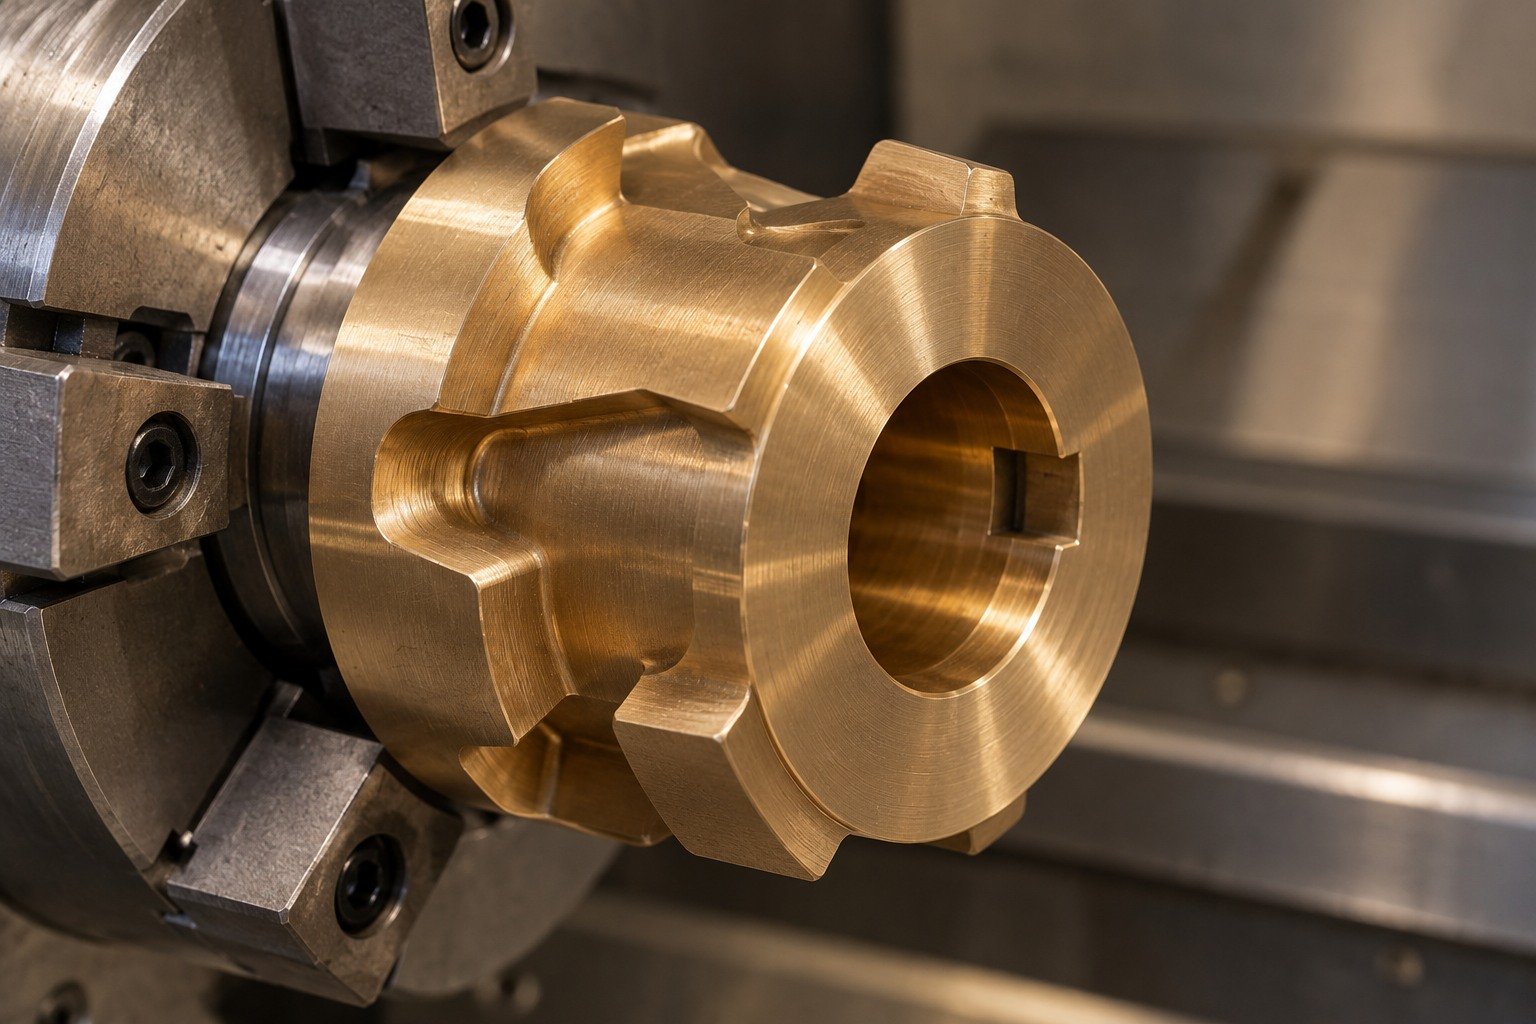
Illustrative concepts. Agree final texture, accepted marks, edge condition and handling protection. Coating, if specified, needs a separate final-fit and material review.
Surface Finishing →
Connect China manufacturing with Dallas-area coordination for drawing review, sample decisions and delivery requirements.
Your C63000 machining quote should compare the same stock state, controlled drawing, final interface and material-evidence scope.
C63000 is a wrought nickel-aluminum-bronze designation. Identify the exact product standard, dimensions and supplied condition, then define the final mating interface and receiving evidence.
For C63000 machinability, selected Concast data lists an indicative index of 30 on the free-cutting-brass scale. Review actual stock state, geometry, support and finish requirements; the index does not predict your cycle time or cost.
Provide CAD and controlled drawing, exact grade and product standard or ordered AMS revision, stock dimensions and condition, quantities, mating details, working surfaces and material-record needs.
Specify feature limits, datums, support and the final free or installed state. Your quote confirms reviewed acceptance for the actual geometry; no universal tolerance is promised.
Identify the ordered product standard and revision, supplied and final condition, lot traceability and required certificate content. Do not treat a generic datasheet as your material-lot evidence.
No automatic equivalence applies. Selected Concast C63000 data describes wrought AMS 4640 material, while C95800 uses a continuous-cast ASTM B505/B505M-23 reference. Chemistry, product requirements and supplied state differ; obtain drawing-authority approval.
Selected Concast data describes HR50 as drawn and stress relieved, with TQ50 listed separately as temper annealed. Confirm the actual ordered product, revision, certificate and final required state rather than assuming one condition for every component.
Zollern identifies it as a similar wrought reference. Compare the complete chemistry, product requirements and supplied condition, and obtain approval before substitution; the short names do not establish identical acceptance.





