

Injection Molding
Tooling and molding for your repeat plastic parts.
From prototype to production, coordinated manufacturing solutions for your custom parts.
View All Services →
Precision parts for your tight tolerances and complex geometry.
Tooling and molding for your repeat plastic parts.

Metal casting options for your part and production volume.

Cutting, forming and welding for your fabricated parts.

Custom profiles for your section, length and finish requirements.

Finishes for your appearance, corrosion and wear requirements.

Sub-assemblies and final builds for your production program.

Production tooling built around your process and volume.

Prototype parts to check fit, function and design.
DFM, process planning and production support for your project.
Inspection, documentation, inventory and delivery planning for your program.
Choose air- or liquid-cooling components around your thermal and mechanical requirements.

Manufacturing support for your cold plates, manifolds and cooling assemblies.

Find components for your power electronics, energy, laser and telecom application.

Components for your electronic systems.
Start with your functional and quality requirements.
Build around your operating environment.
From prototype to production, review material performance, manufacturability and cost for your part.
Review grade, temper and finish for your metal parts.
 AluminumStrength, weight and machining›
 Stainless SteelCorrosion and finish requirements›
 Carbon & Alloy SteelDiscuss grade and heat treatment›
 Tool SteelDiscuss tooling and wear needs›
 TitaniumReview grade and part geometry›
 Copper & BrassDiscuss conductivity and machining›
Match your polymer to function, process and environment.
 ABSReview enclosure and molding needs›
 Polycarbonate (PC)Discuss clarity and impact needs›
 Nylon (PA)Review moisture and wear conditions›
 POM / AcetalReview fit and sliding features›
 PEEKDiscuss operating conditions›
 PTFEReview friction and chemical exposure›
 ULTEM / PEIDiscuss thermal and electrical needs›
Confirm grade availability and application requirements.
 Silicone / LSRDiscuss flexible component needs›
 TPU / TPEReview flexibility and processing›
 EPDMReview weathering and chemical exposure.›
 NBRReview oil and fuel exposure.›
 FKMReview temperature and chemical exposure.›
 G10 / FR4Review insulation and laminate needs›
 CompositesReview stiffness, weight and laminate.›Customer-Specified MaterialsConfirm your grade and requirements.›Other Specialty MaterialsDiscuss your application and grade.›
Practical guidance for your part geometry and material decisions.
Prepare your process, budget and sourcing questions.
Build your knowledge before production.
Learn who we are and how we operate.
Find our U.S. support team or start a conversation.
YOUR GRADE. YOUR CONDITION. YOUR FINISHED FIT.
Plan your 4130 steel machining around the product form, supplied condition, joining and final-fit requirements. Agree the thermal route and inspection before production.
1 part model + 1 controlled drawing · Material condition · Quantity
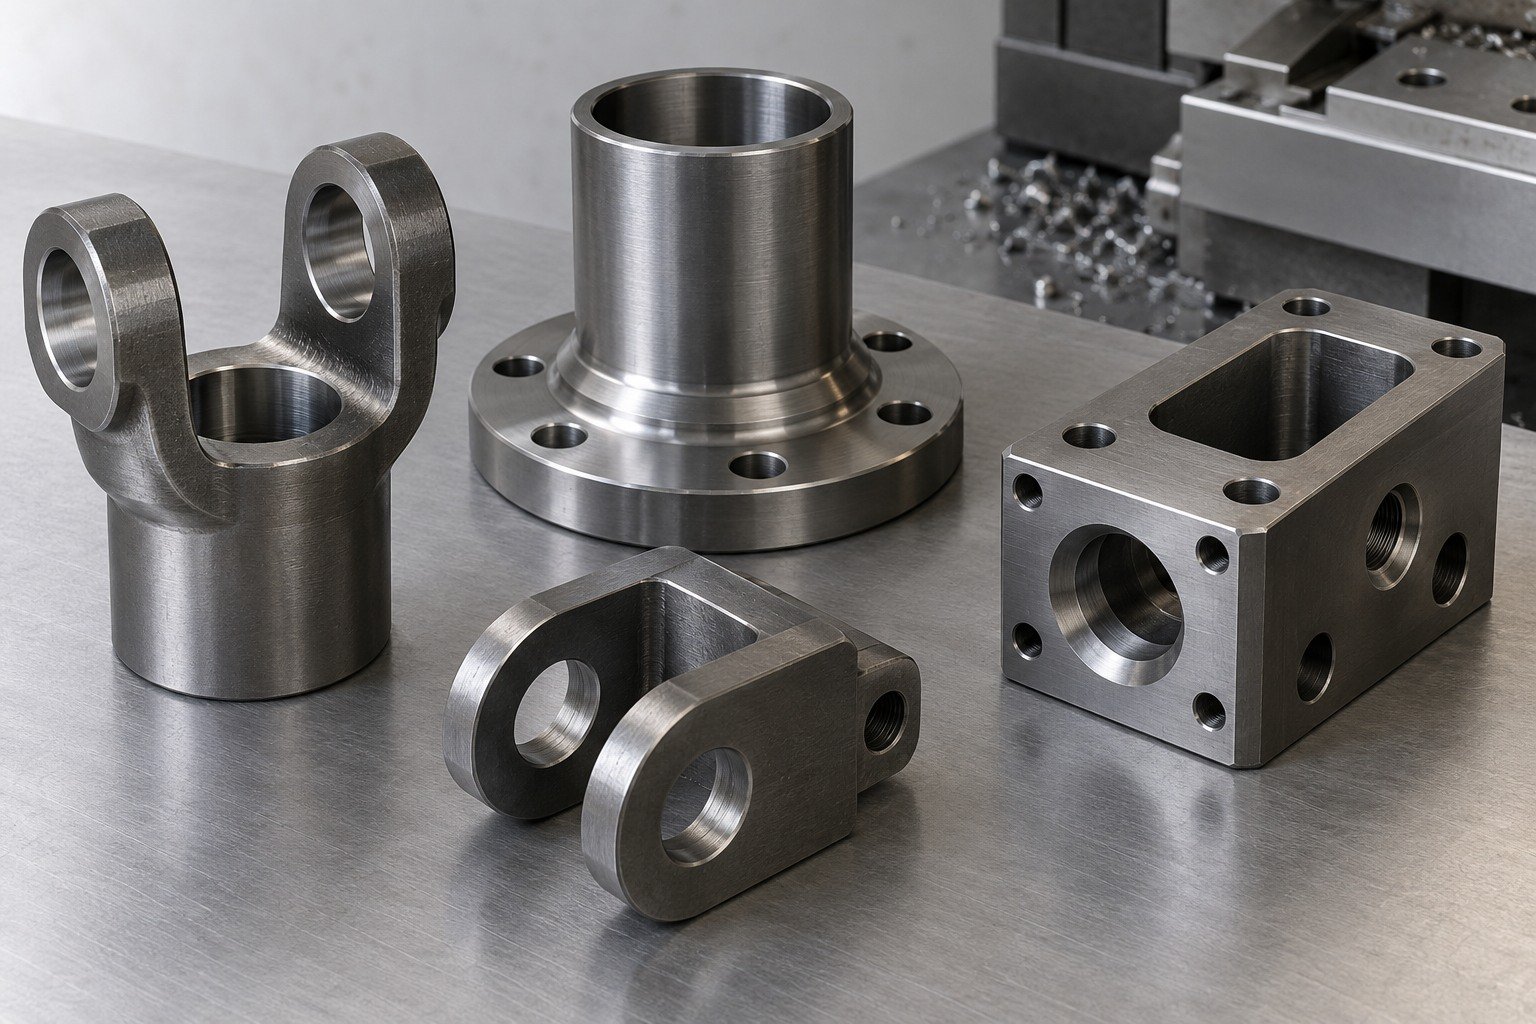
4130 is chromium-molybdenum alloy steel, often called 4130 chromoly steel. Confirm the actual product specification and supplied condition for your drawing.
Specify the requested grade with product form and condition.
Eaton bar reference · not a batch analysis.
Product form, wall or section and supplied state.
Treatment, joining, protection and final size.
Material identity, lot records and agreed inspection.
Select your part family, then review the four decisions that control your order.
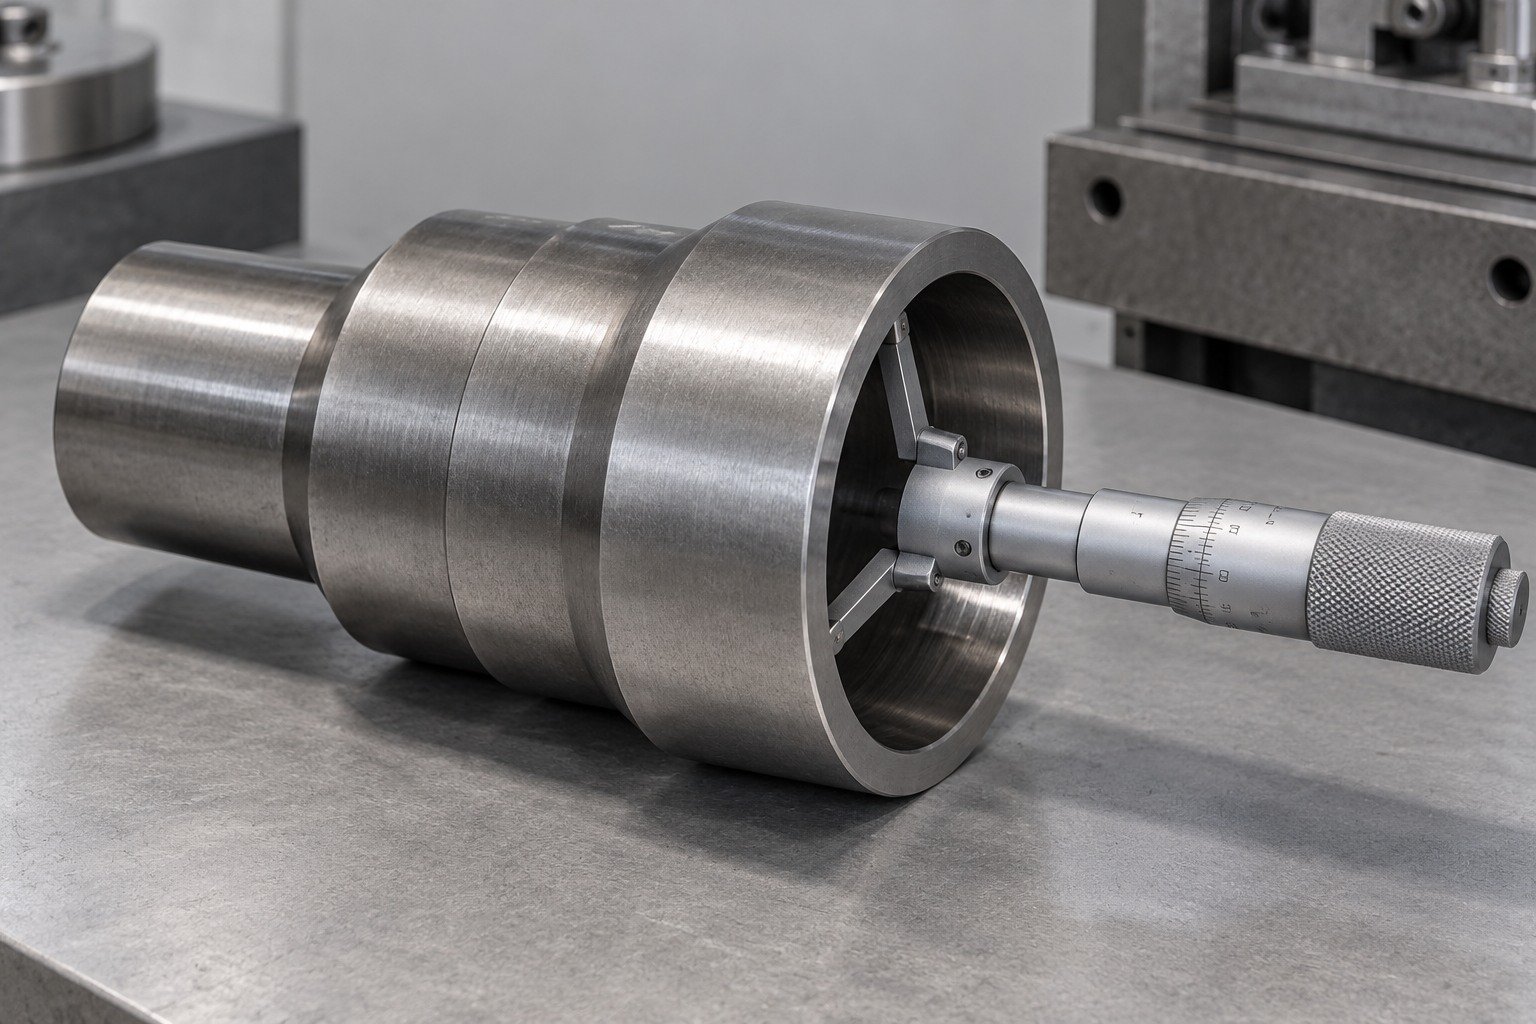
For your 4130 alloy steel machining review, identify wall thickness, tube ends, bores and mating shoulders. Do not treat bar and tube product requirements as interchangeable.
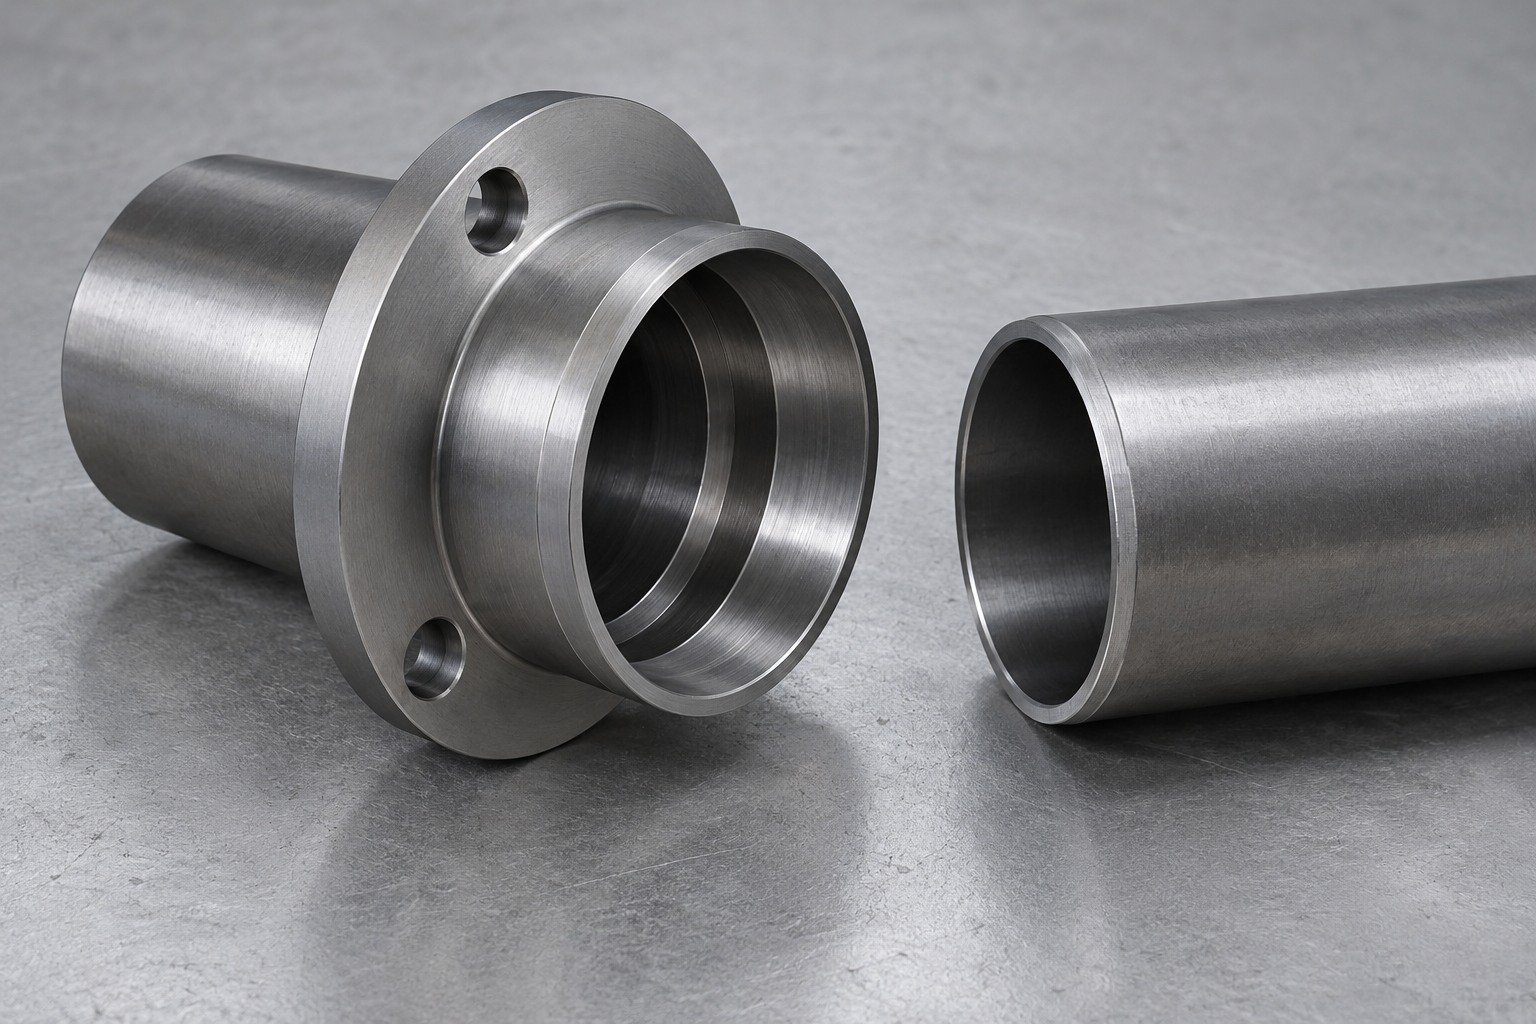
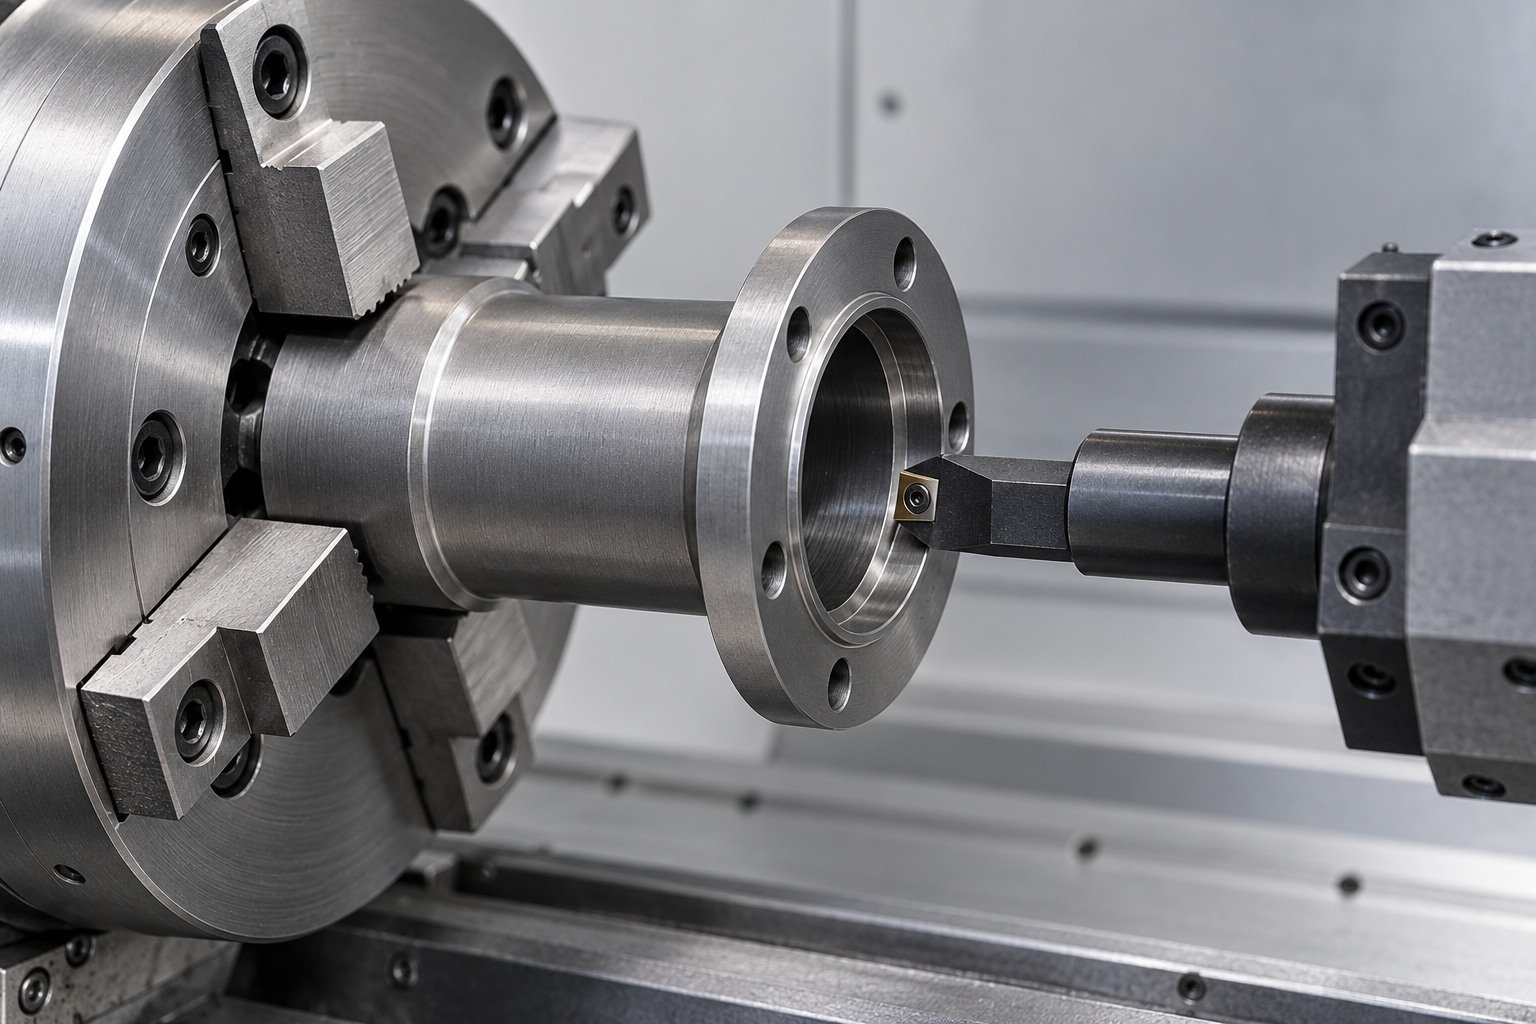
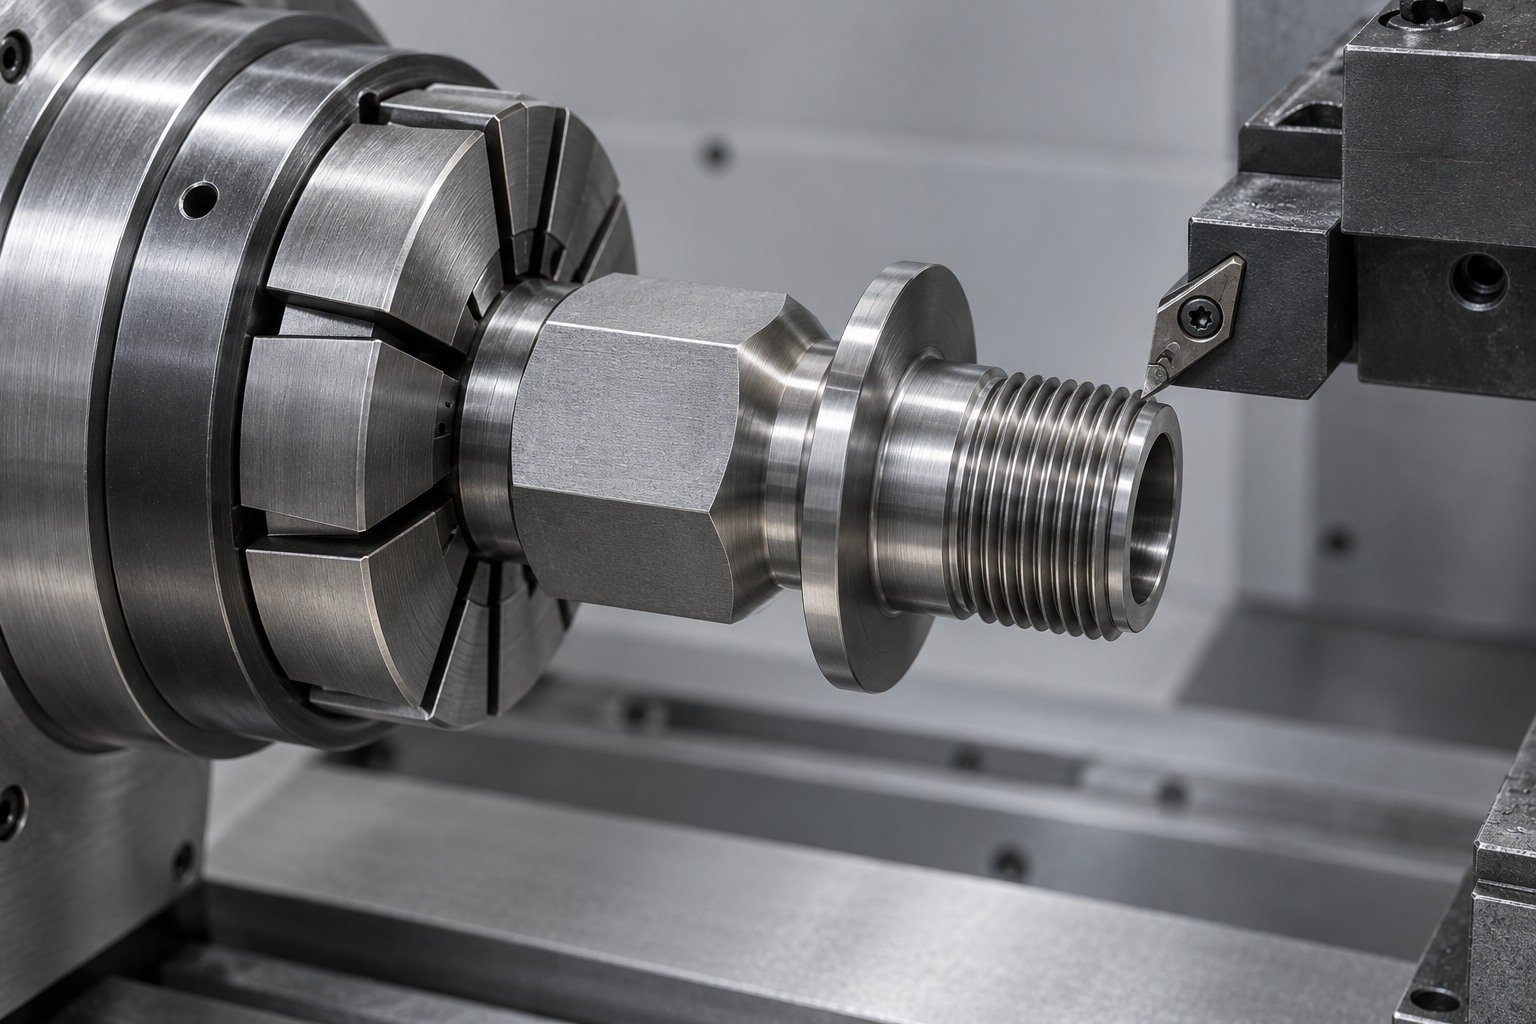
Define gripping allowance, internal support and access to the bore. For your 4130 steel turning inquiry, show which shoulder and diameter control the assembly.
Identify incoming condition, any required treatment and joining. Agree distortion allowance and final machining before accepting the tube interface.
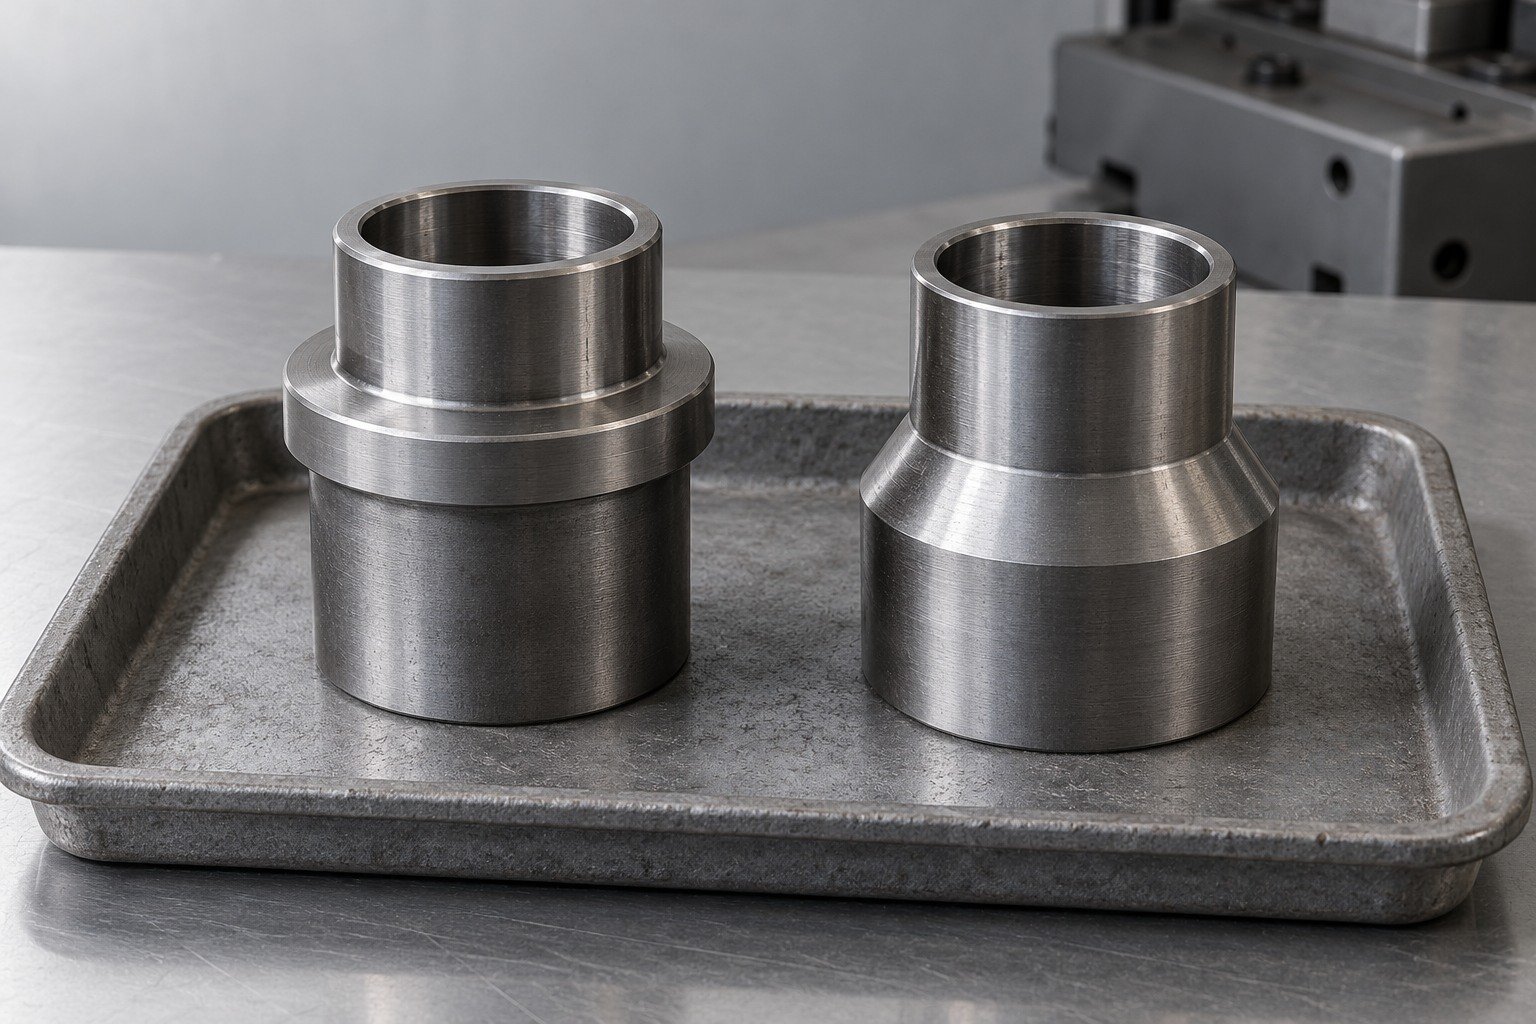
State bore size, wall-sensitive checks, datum scheme and final surface condition. Agree which material and dimensional records your receiving team needs.
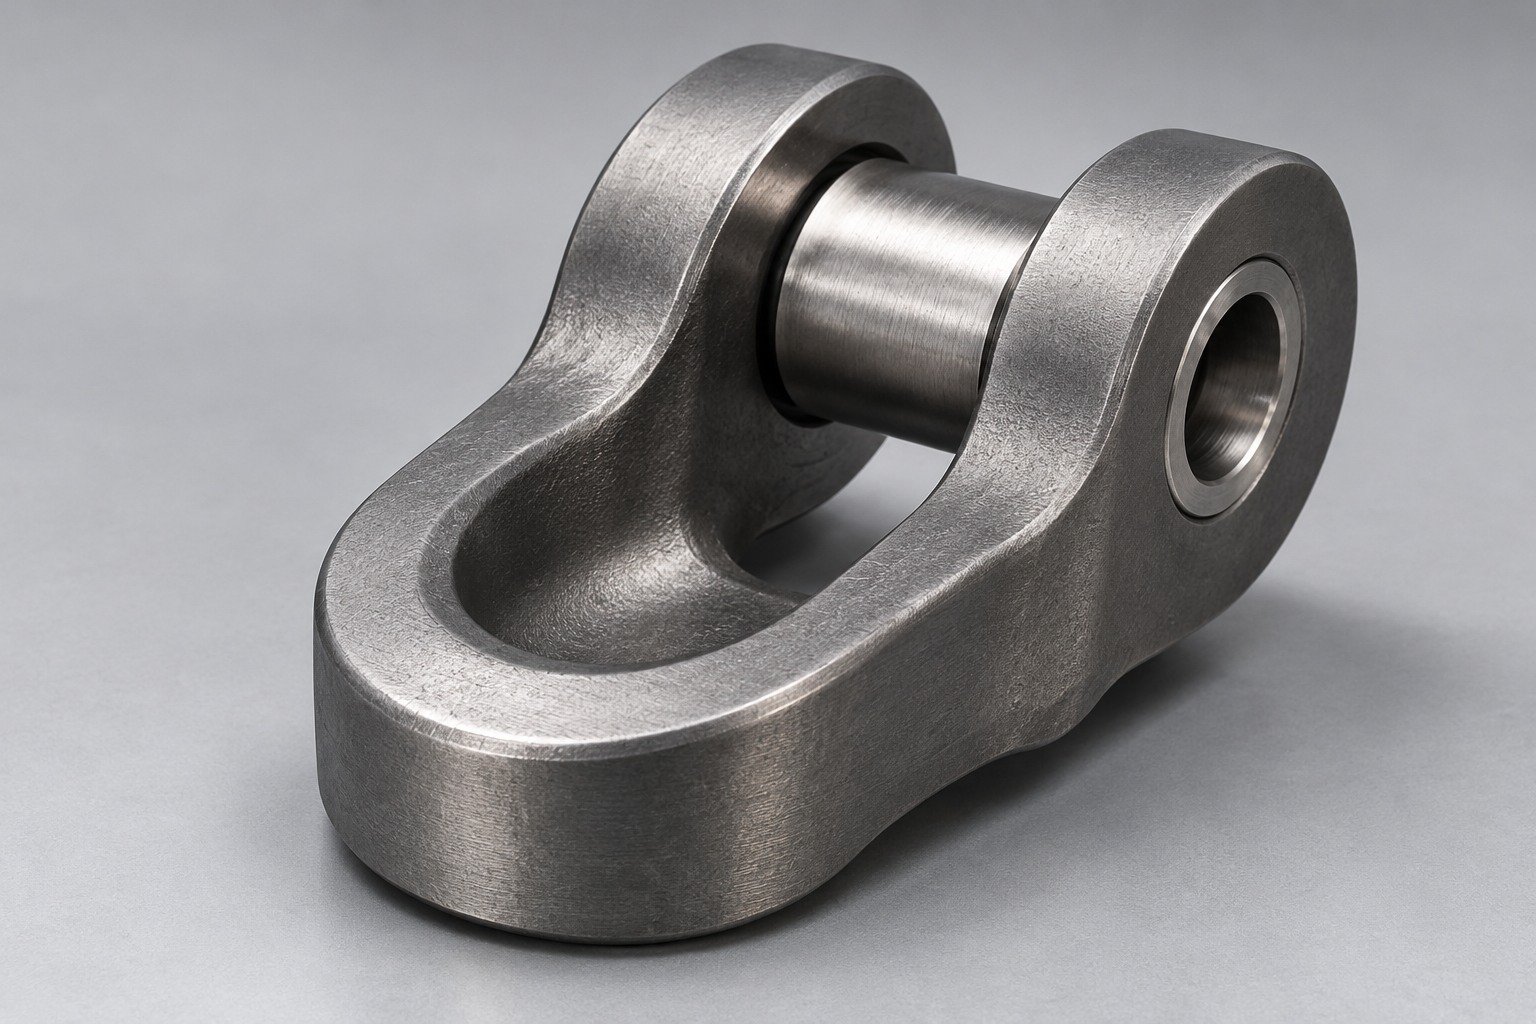
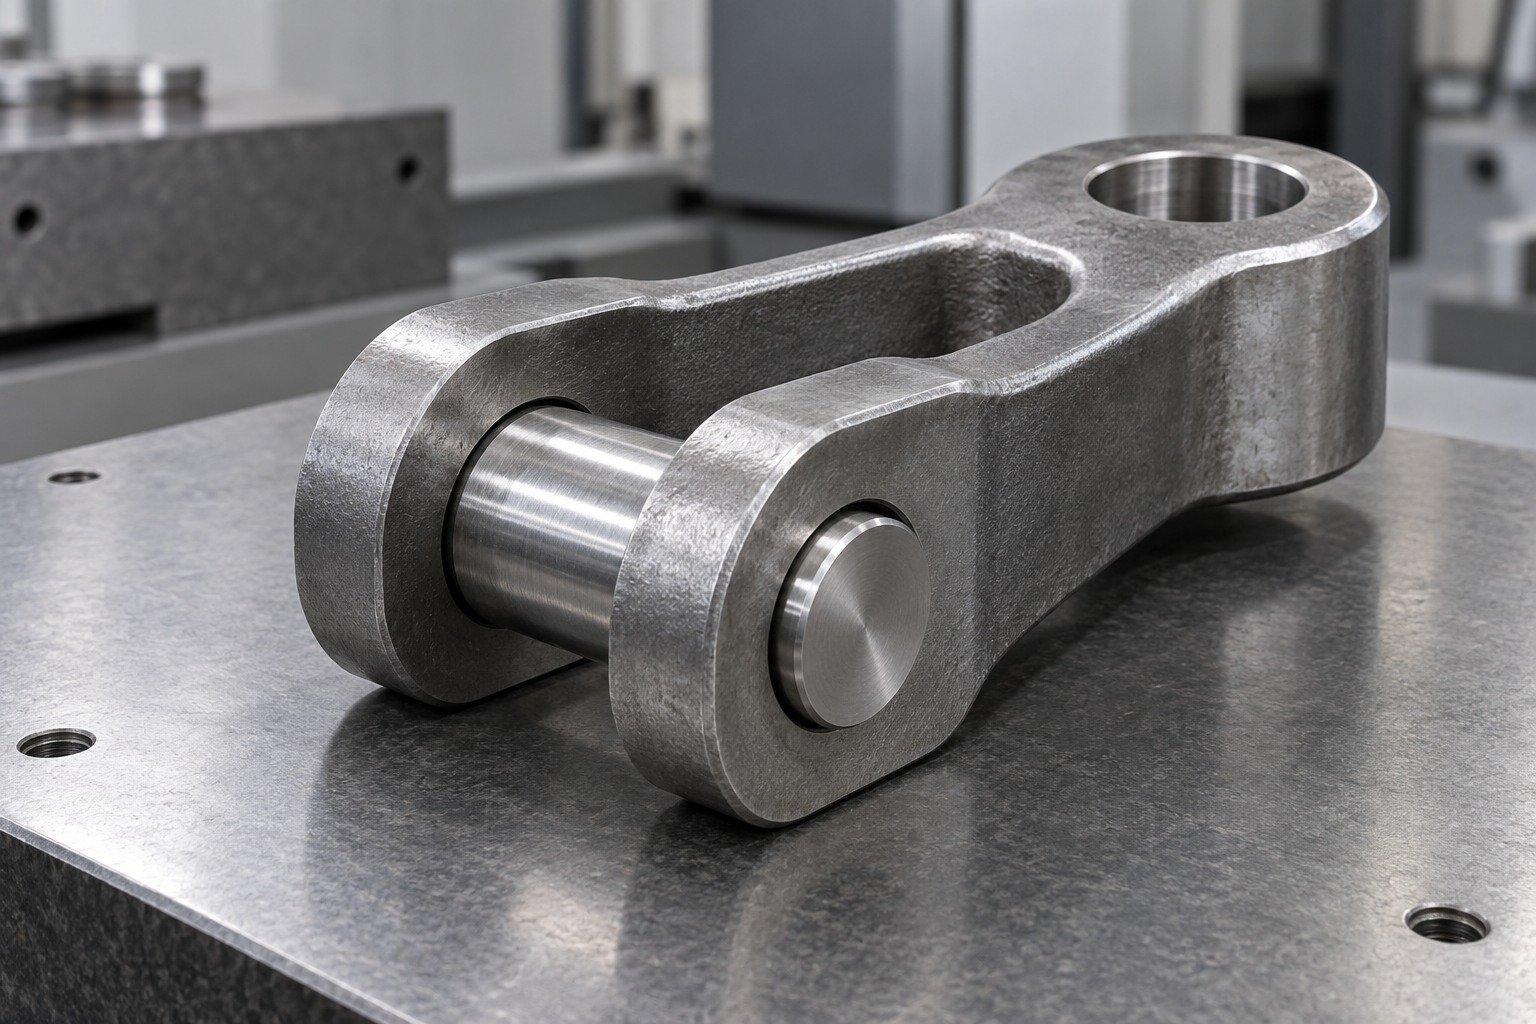
For your custom 4130 steel parts, identify the pin interface, ear alignment, throat radius and locating faces. Supply the mating drawing when it controls fit.
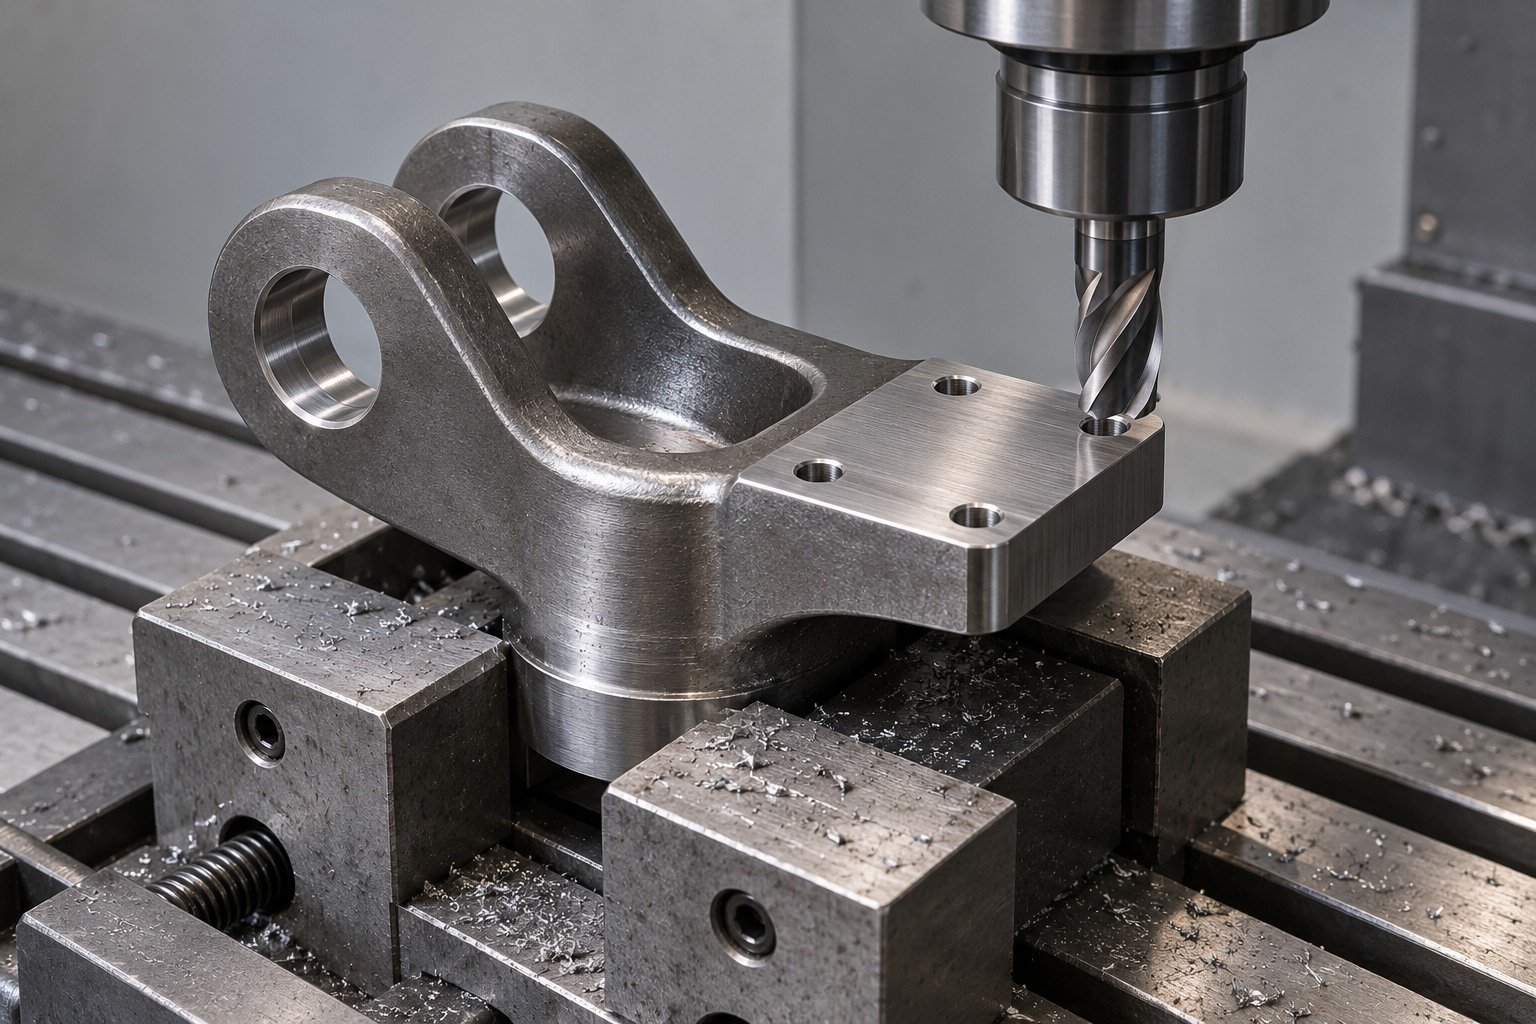
For your 4130 steel milling review, show cutter access, datum faces and how aligned bores will be accepted. Include allowed edge breaks.
For a joined clevis, define the weld details, material condition and final inspection state. Do not assume that a machined bore stays unchanged after joining.
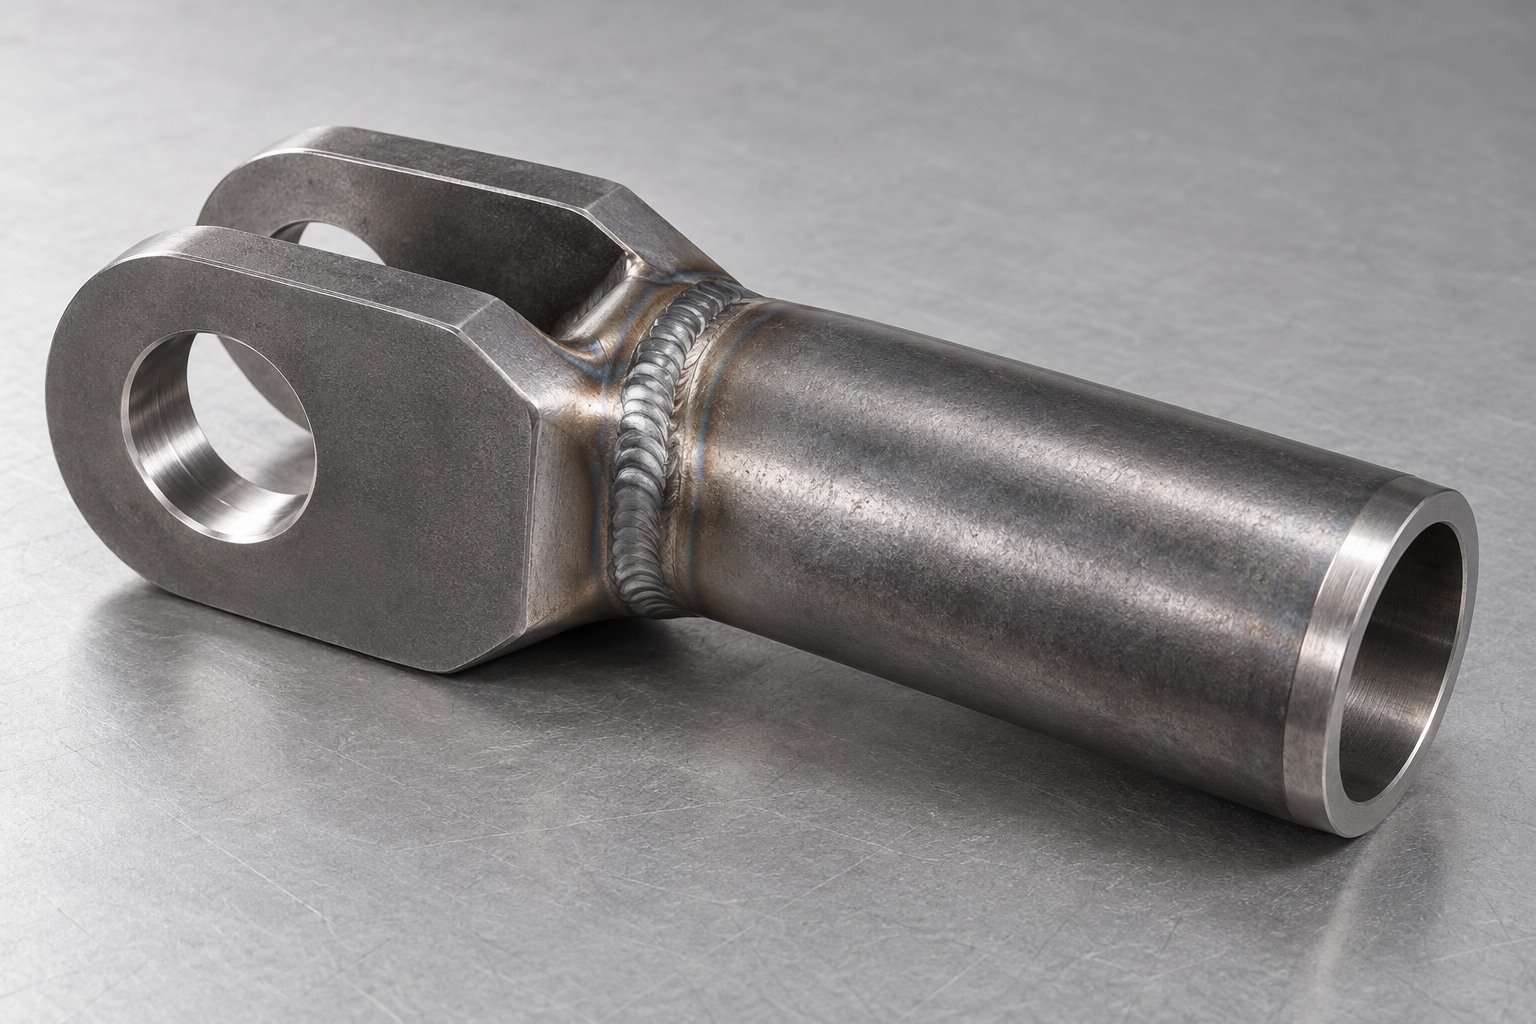
Define how ear alignment, bore size and the pin interface are measured. Specify records for your final assembled condition.
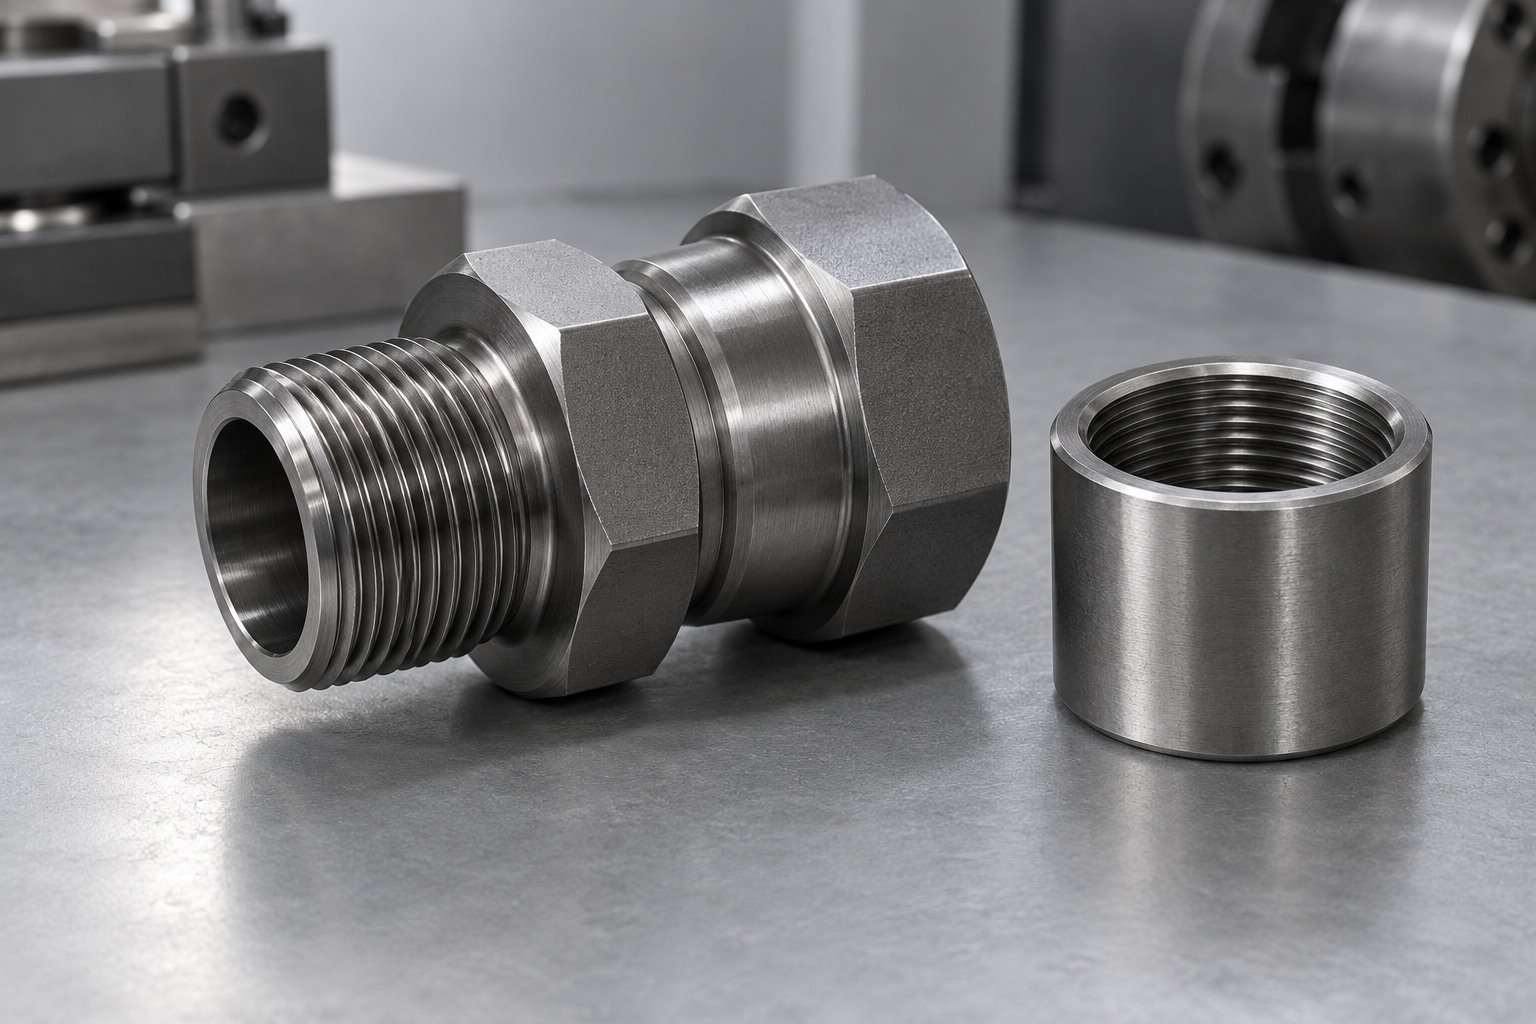
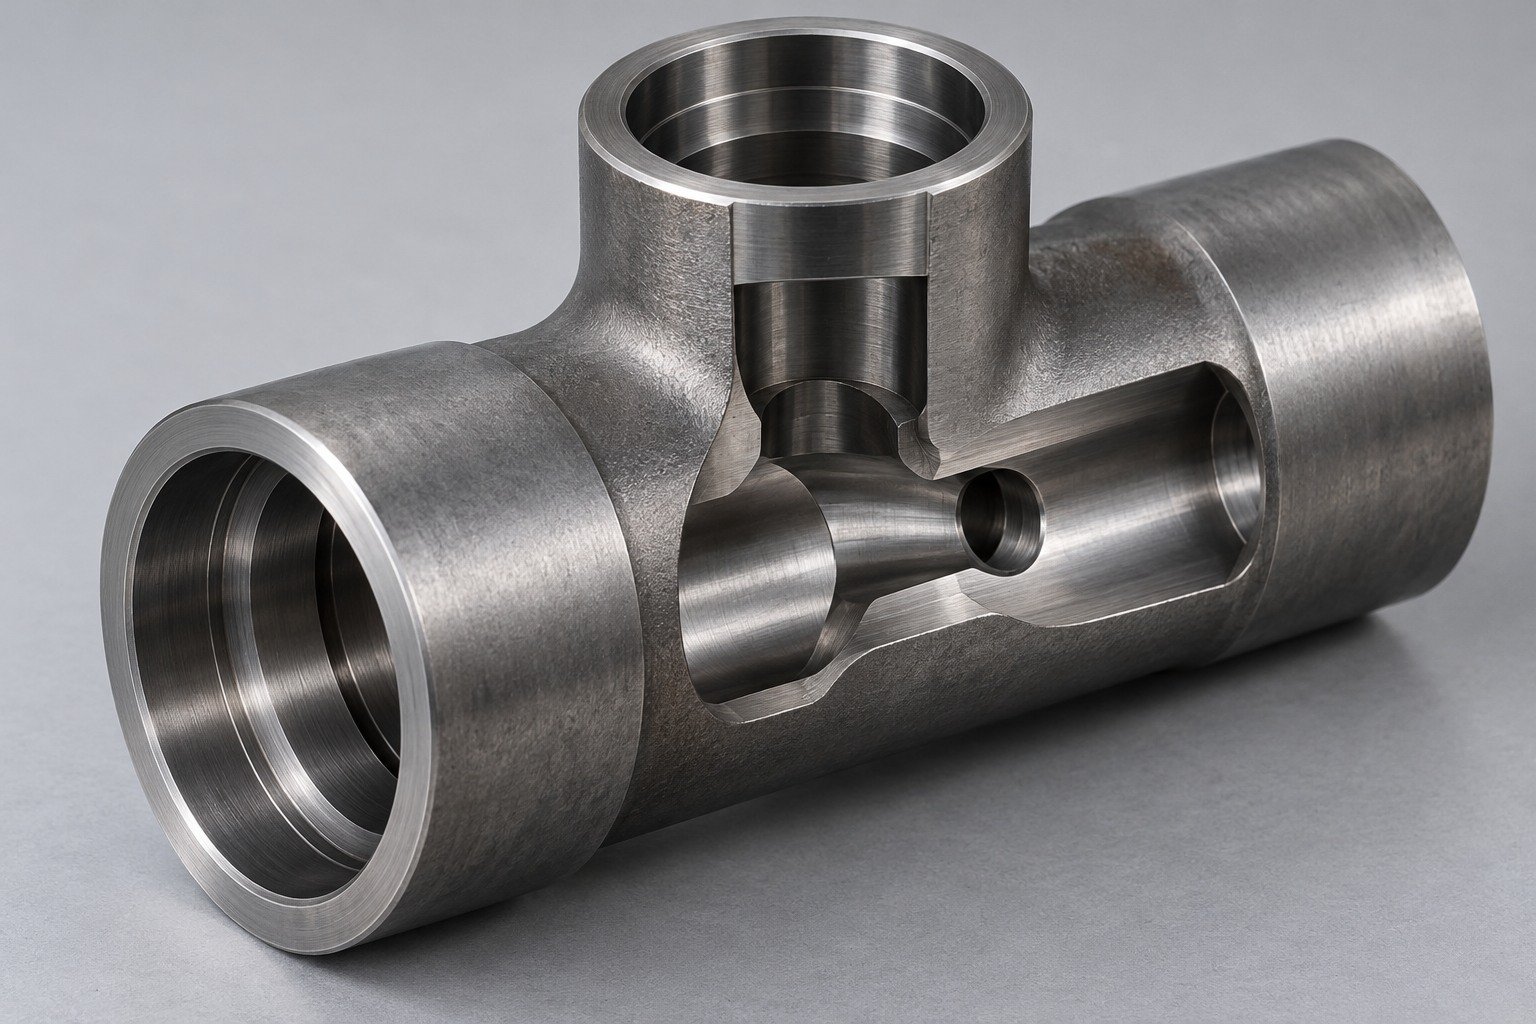
For your 4130 steel threaded parts, identify useful engagement, mating shoulders, sealing faces and internal passages. Specify the final functional fit.
For 4130 steel drilling and tapping, show intersections and burr access. Locate wrench flats and radial features from the turned datum.
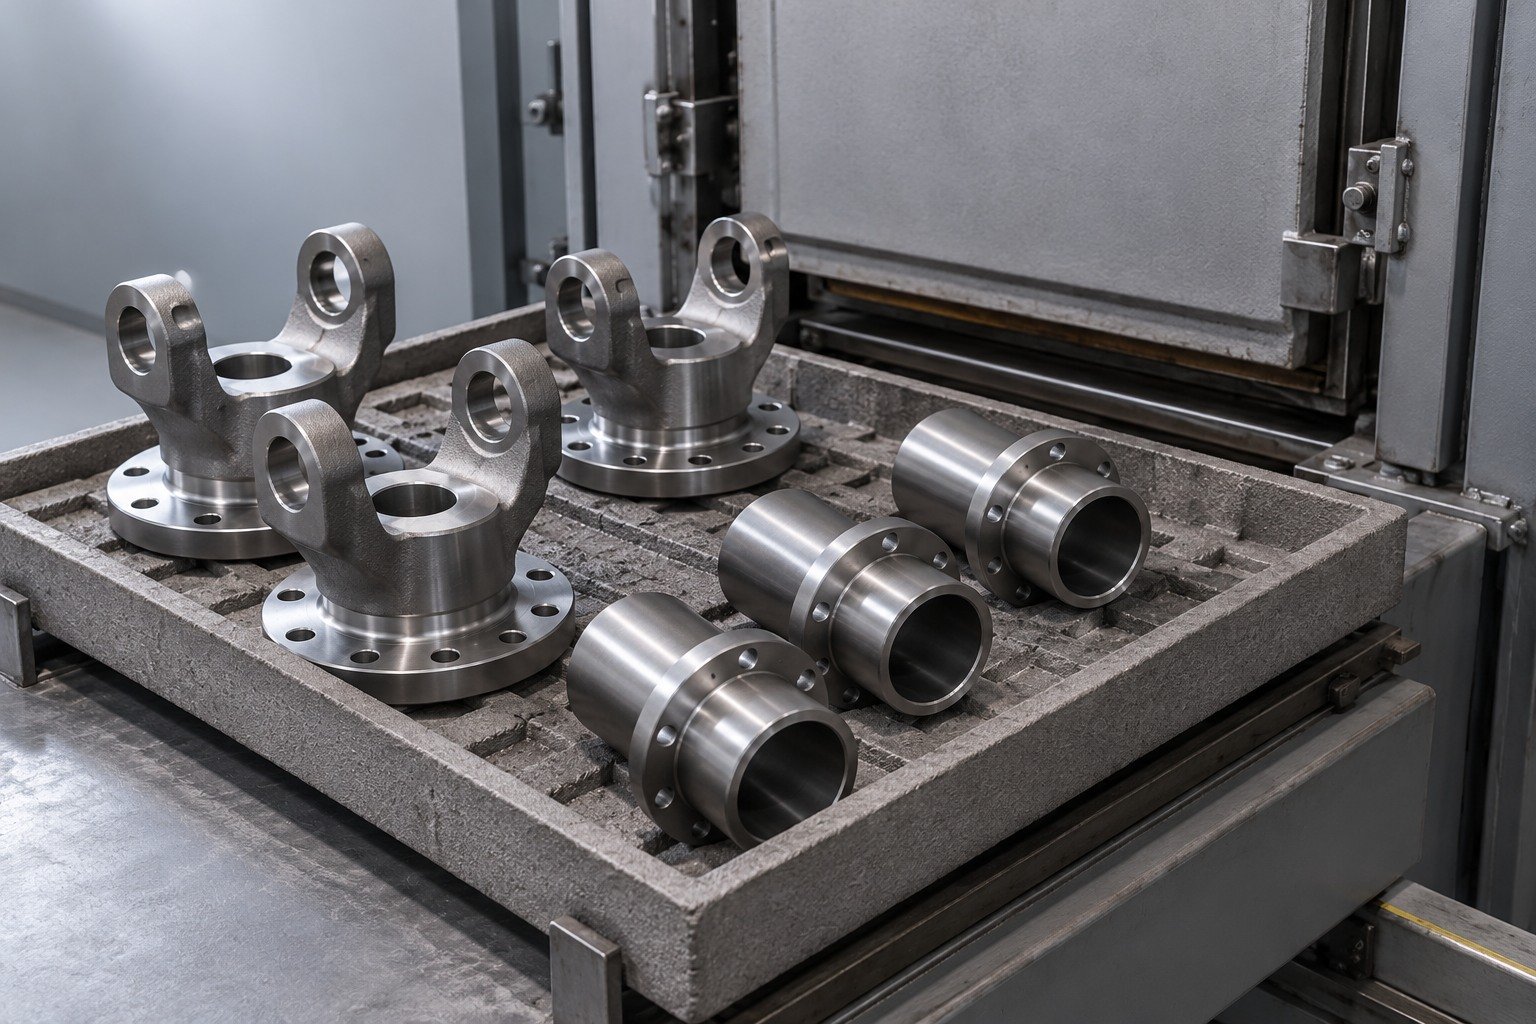
State the specified thermal route and final property or hardness requirements. Keep section size, test locations and machining allowance explicit.
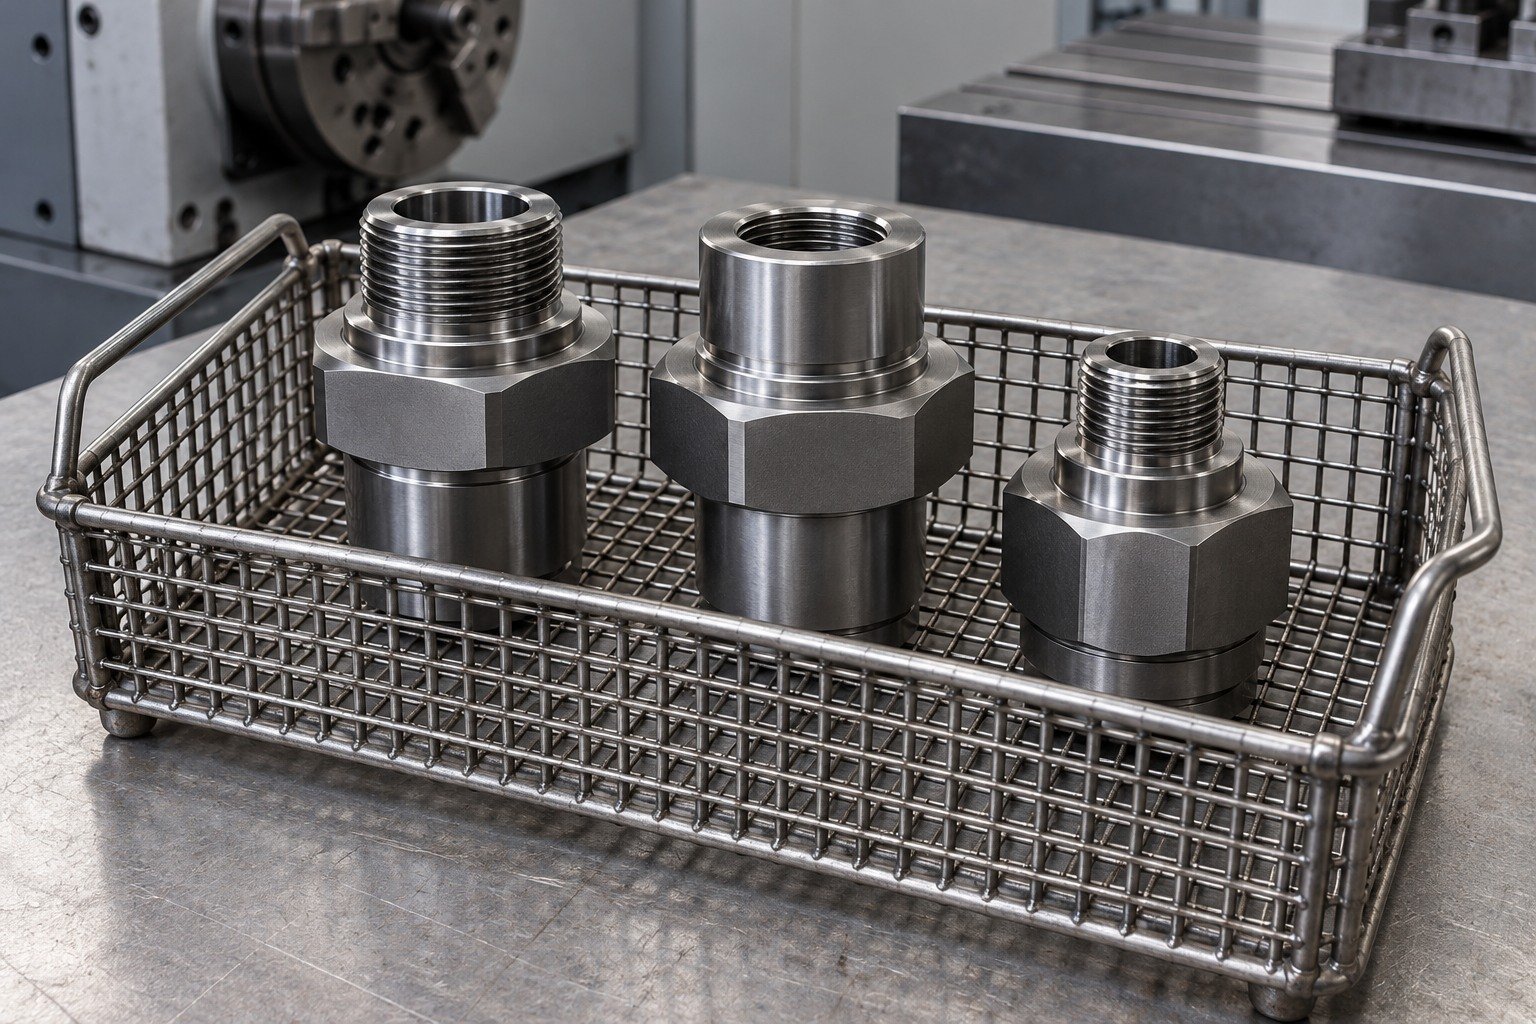
Agree thread gauging, passage cleaning, sealing-face protection and final dimensional records before quoting.
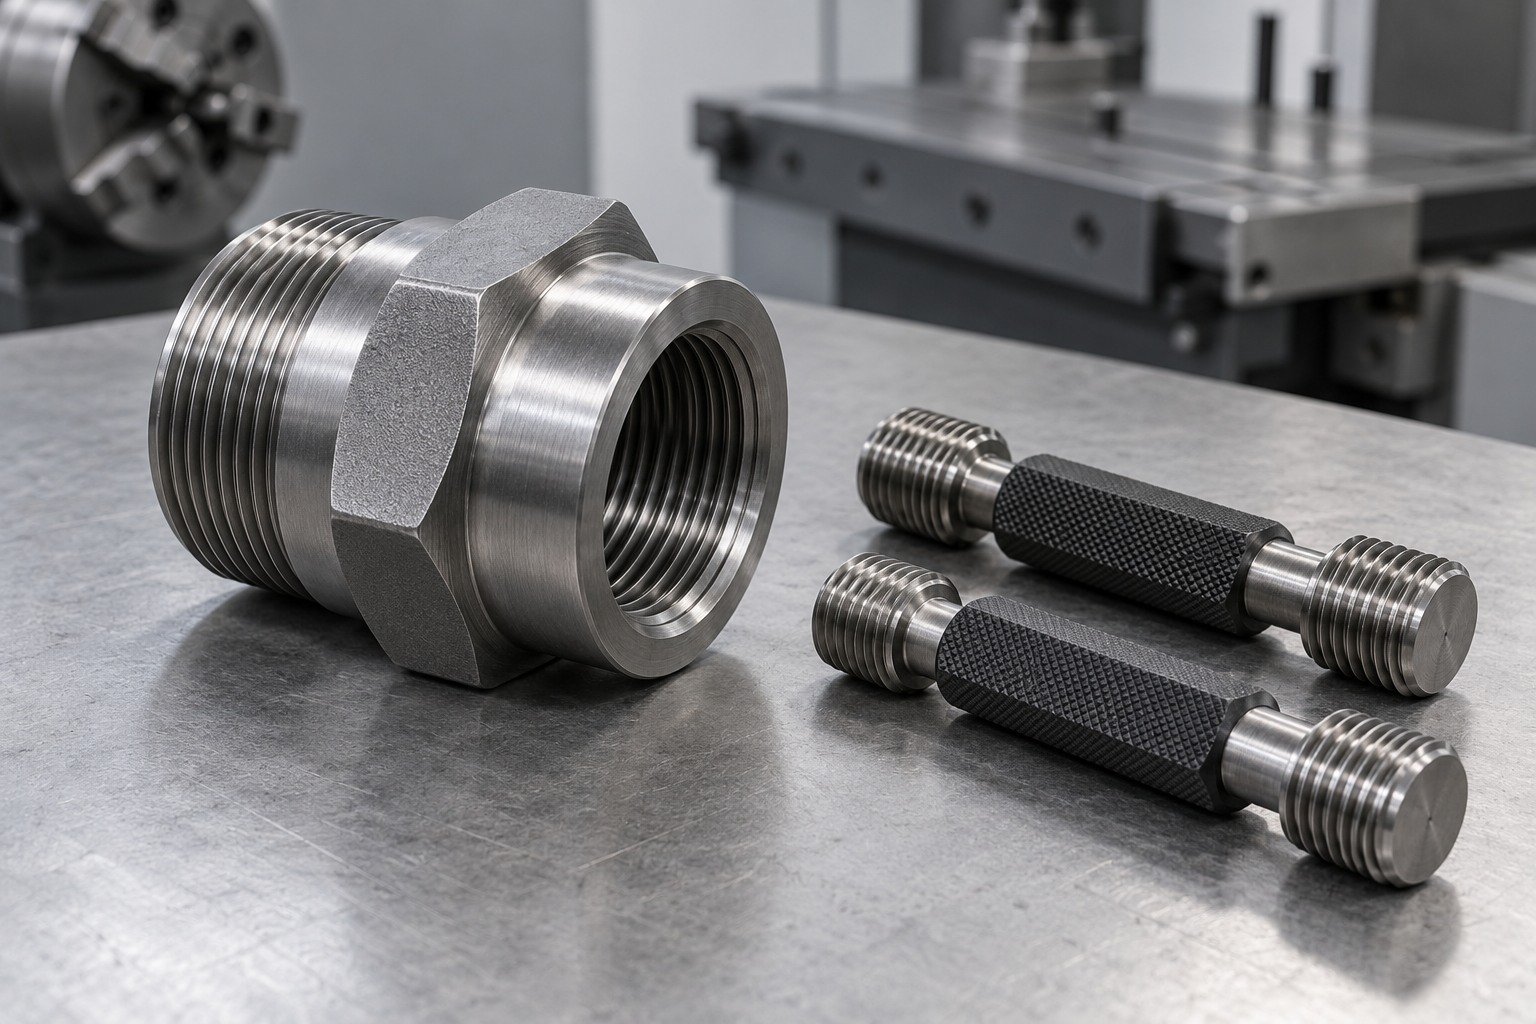
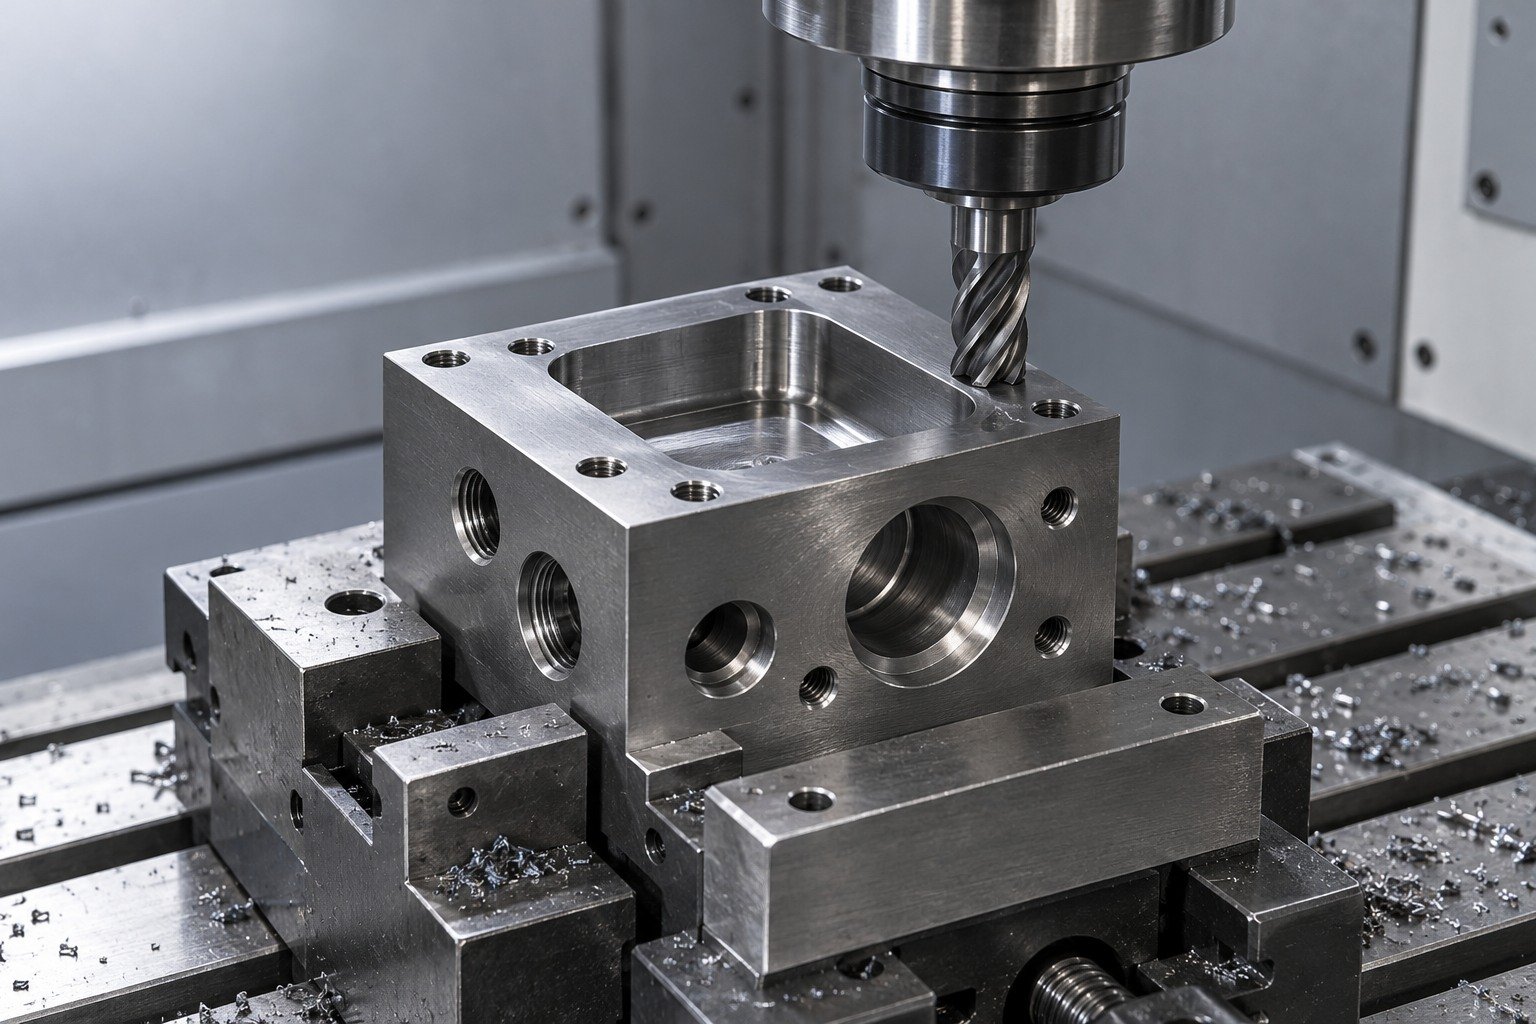
For your 4130 steel CNC machining inquiry, define mounting datums, port locations, bore fits and critical pocket relationships.
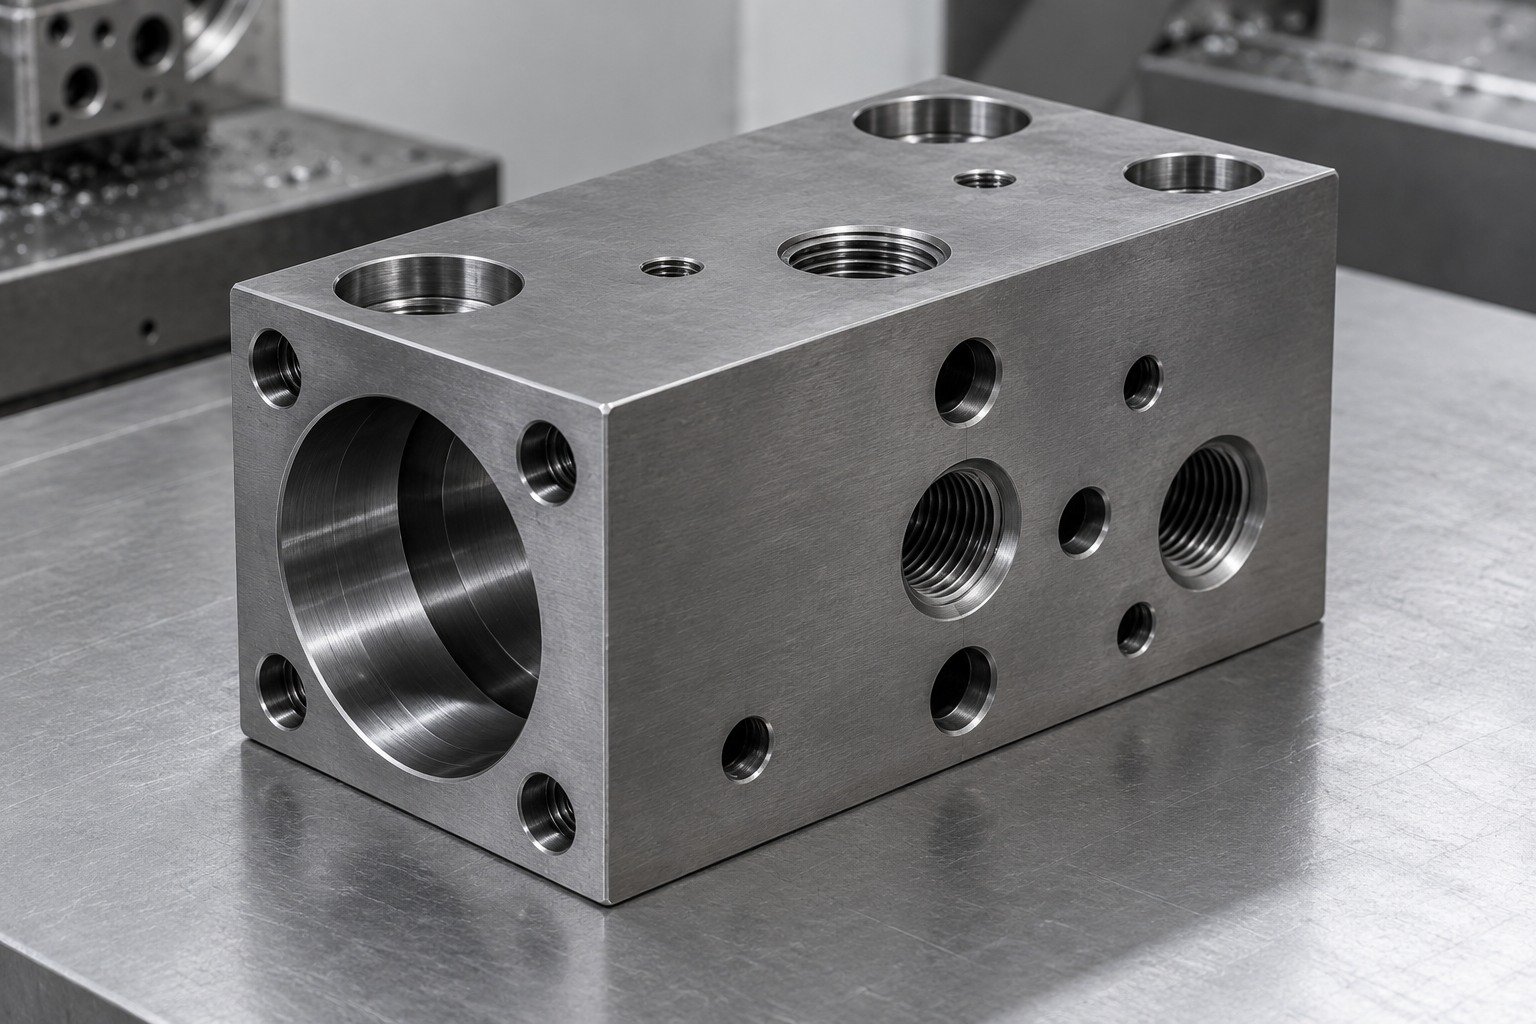
Show entry direction, tool clearance and intersections. Identify features that must be related in one datum scheme and where burr inspection is possible.
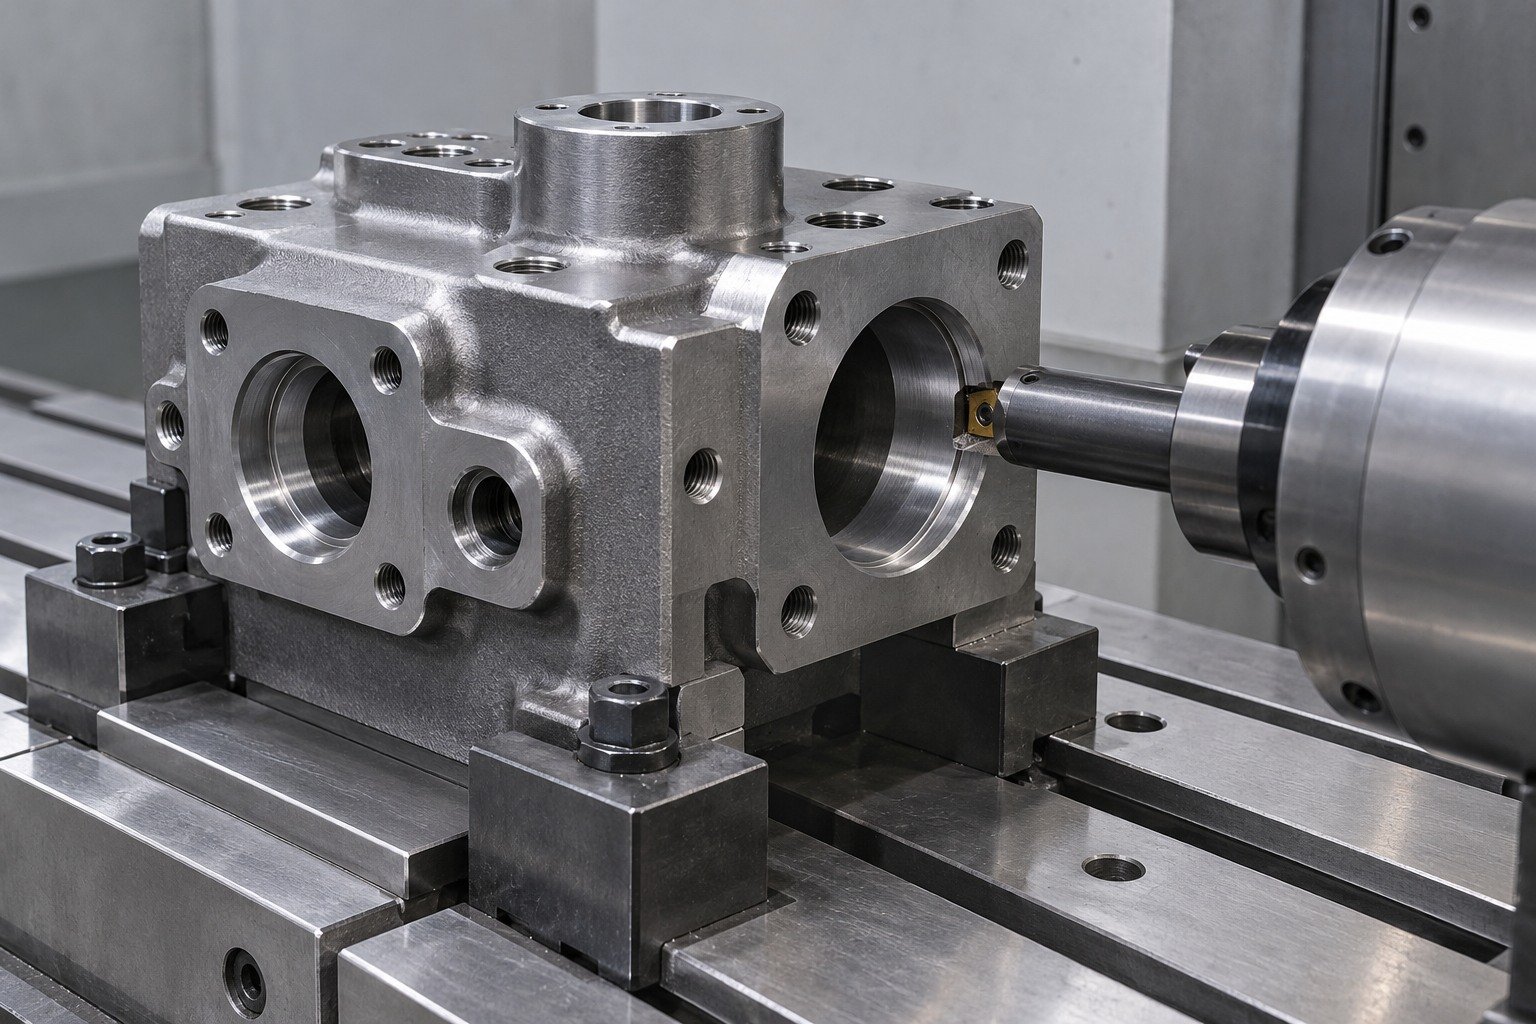
Connect supplied condition, any required treatment and final machining. Mark functional pads and protected bores for surface finishing.
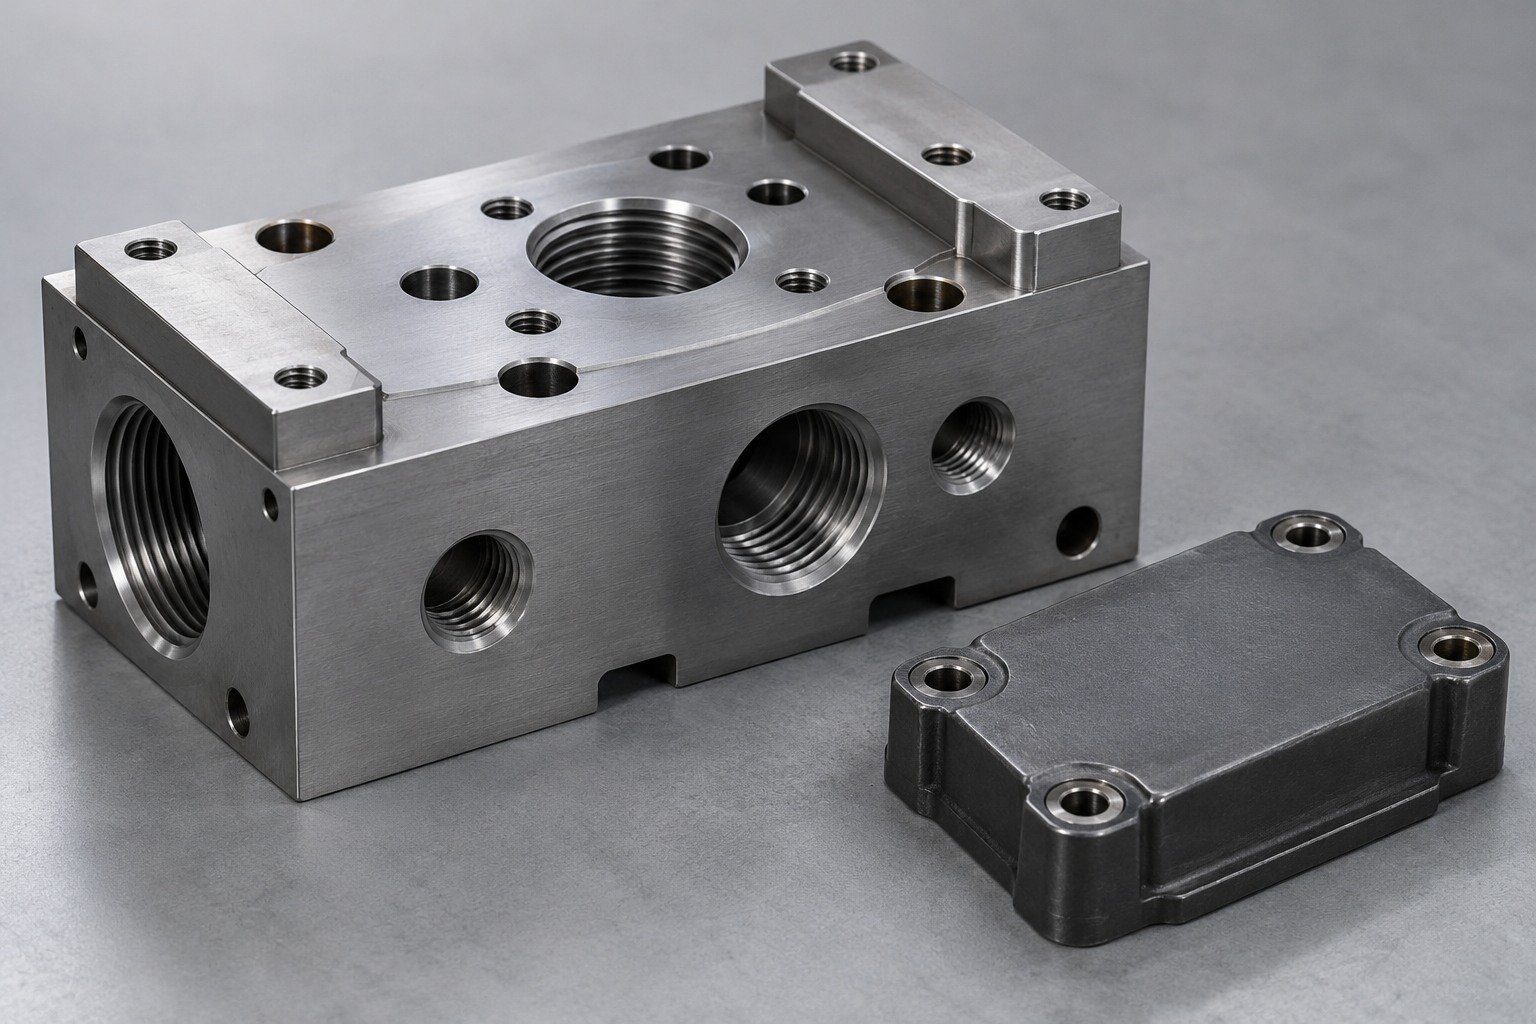
Agree positional checks, critical sizes, finish acceptance and required material records for the completed block.
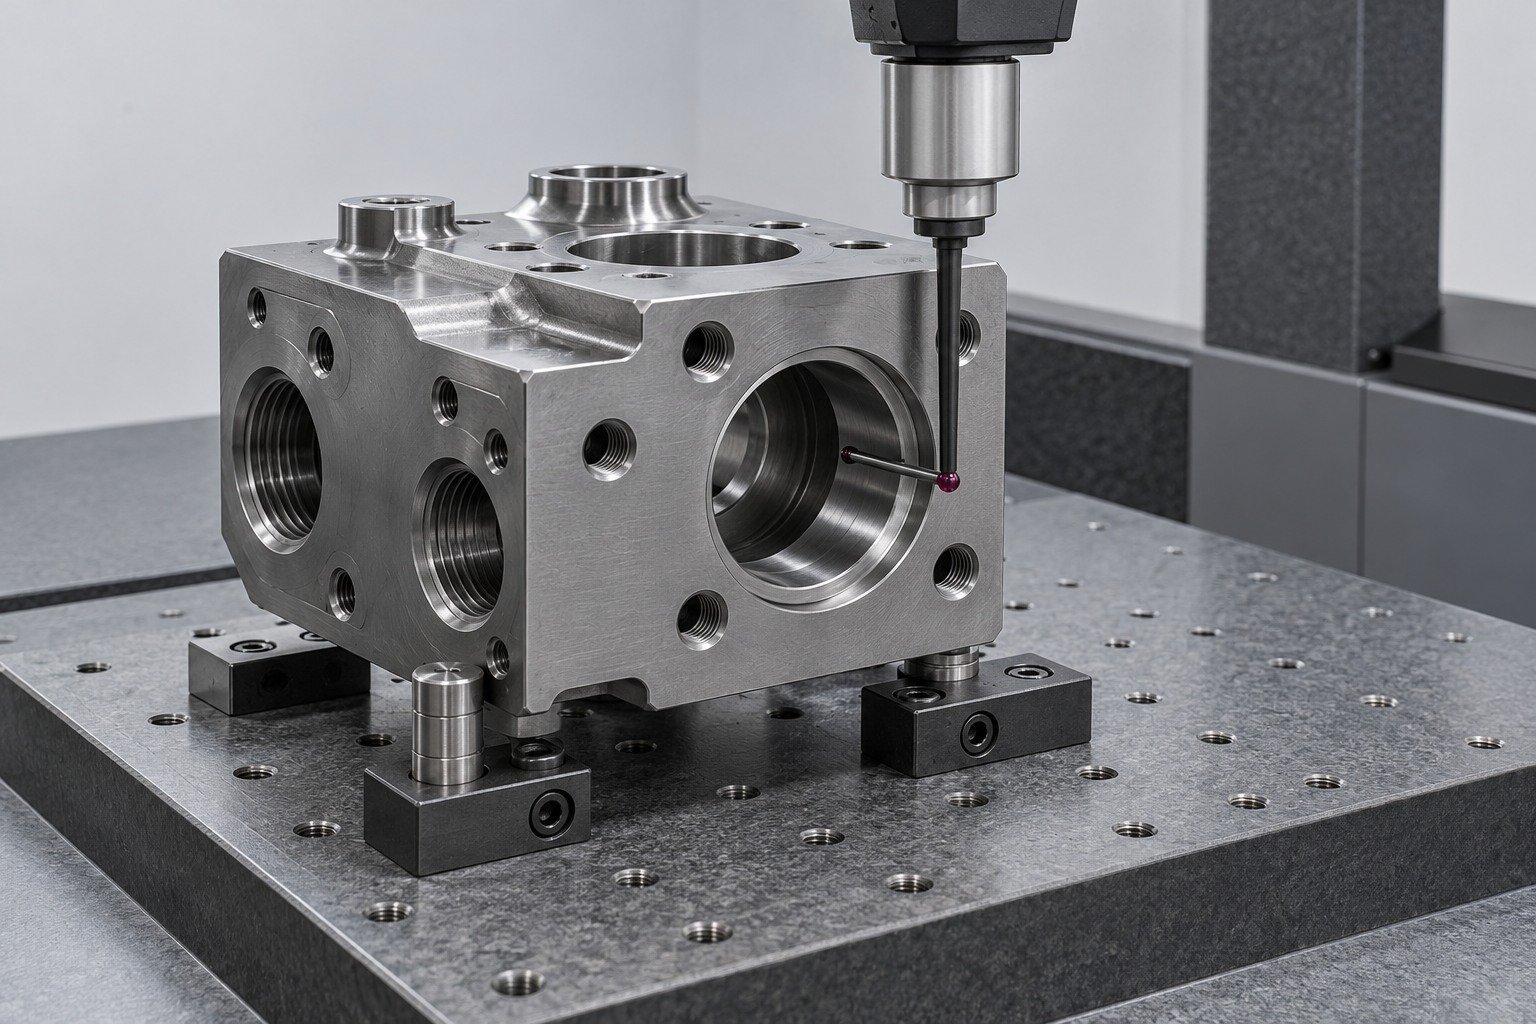
Do not transfer a generic strength or hardness value to your finished component.
| Your callout | What to confirm |
|---|---|
| As-rolled, annealed or normalized | Actual product form, supplied condition and material record |
| Cold-drawn product | Drawing revision, wall or section, and supplied state |
| Specified treatment | Target condition, section, distortion allowance and final inspection |
Confirm the product standard for your drawing.
European names do not approve substitution without checking the complete specification.
Compare the selected product references before reviewing a substitute.
Mass % · common axis 0–1.25%
Producer reference limits · not LK lot analysis.
| Mass % | 4130 · Eaton bar | 25CrMo4 · Ovako EN ISO 683-2 |
|---|---|---|
| C | 0.28–0.33 | 0.22–0.29 |
| Mn | 0.40–0.60 | 0.60–0.90 |
| Si | 0.15–0.35 | 0.10–0.40 |
| Cr | 0.80–1.10 | 0.90–1.20 |
| Mo | 0.15–0.25 | 0.15–0.30 |
| P max | 0.035 | 0.025 |
| S max | 0.040 | 0.035 |
European comparison: 25CrMo4 / 1.7218 is listed as a similar designation. The limits differ. Review product standard, supplied condition and required performance; do not apply this table as blanket equivalence.
Review 4130 steel machinability together with geometry, material condition and the final manufacturing route.
For your 4130 cold drawn steel inquiry, state the actual product standard, tube wall or bar section and supplied condition. “4130 cold rolled steel” is not a substitute for a complete product description.
Define the condition and acceptance method.
State locations and final inspection scope.
Agree dimensions after the full sequence.
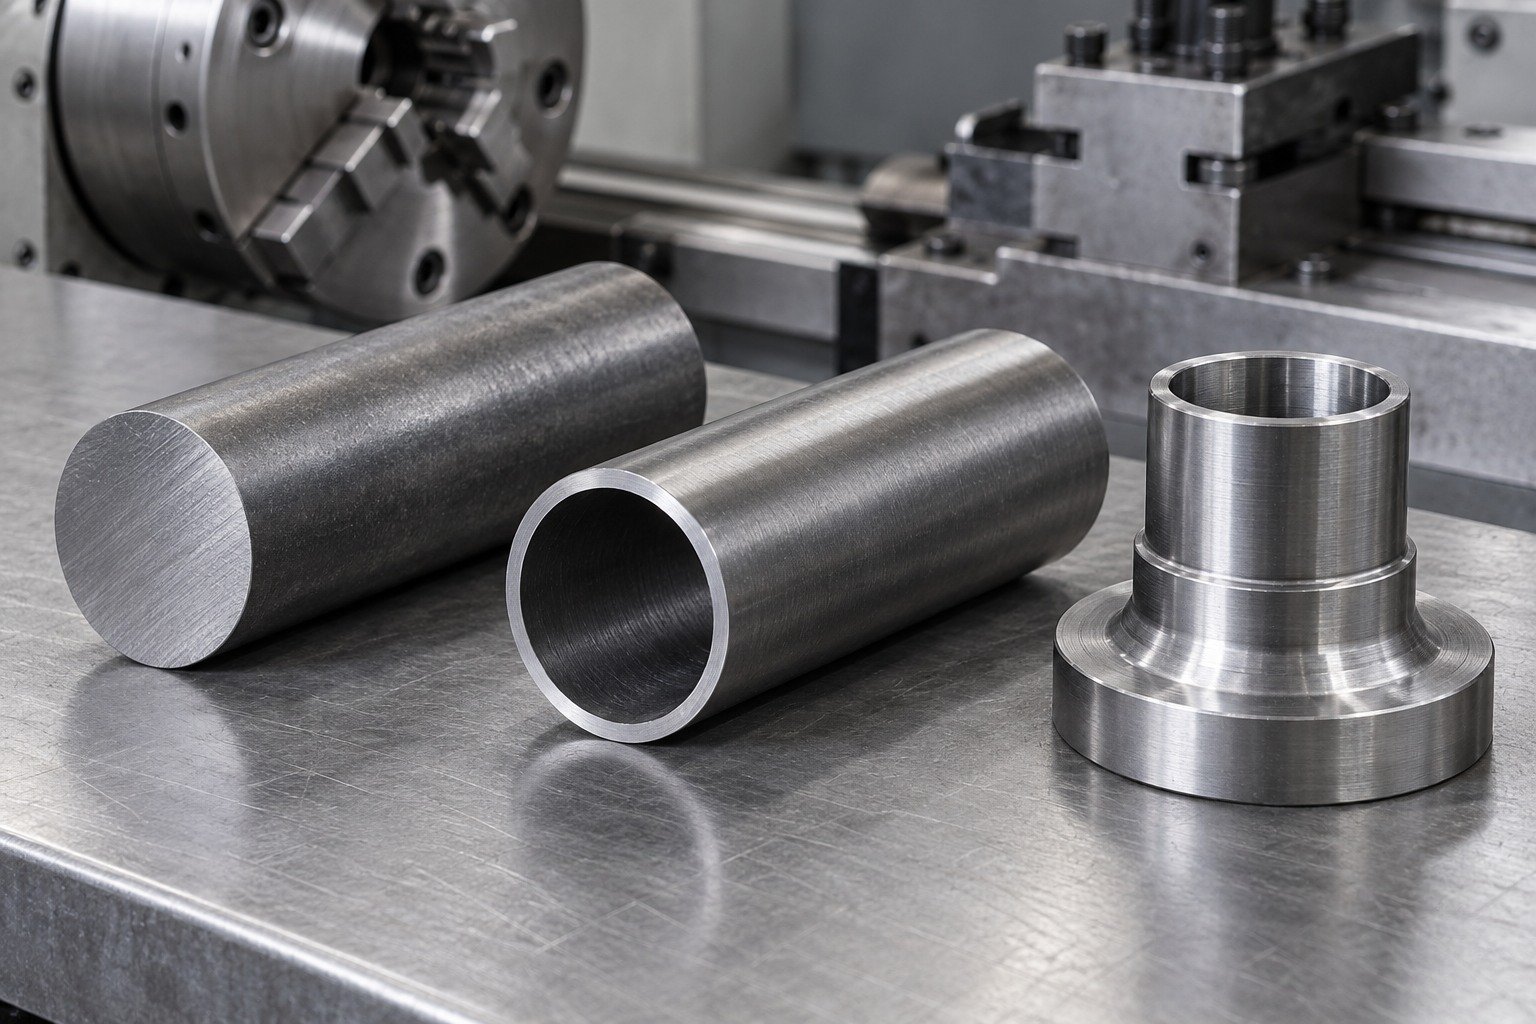
Identify drilling entry, useful thread engagement, runout and burr access. Separate sealing surfaces from edges that may be broken.
Define the condition and acceptance method.
State locations and final inspection scope.
Agree dimensions after the full sequence.
For your 4130 steel heat treatment or 4130 steel quench and temper requirement, agree target condition, section, test locations and final machining allowance.
Define the condition and acceptance method.
State locations and final inspection scope.
Agree dimensions after the full sequence.
For 4130 steel welding, identify the joint, wall or section, supplied state and final acceptance. Agree the actual procedure and any post-weld requirements before release.
Define the condition and acceptance method.
State locations and final inspection scope.
Agree dimensions after the full sequence.
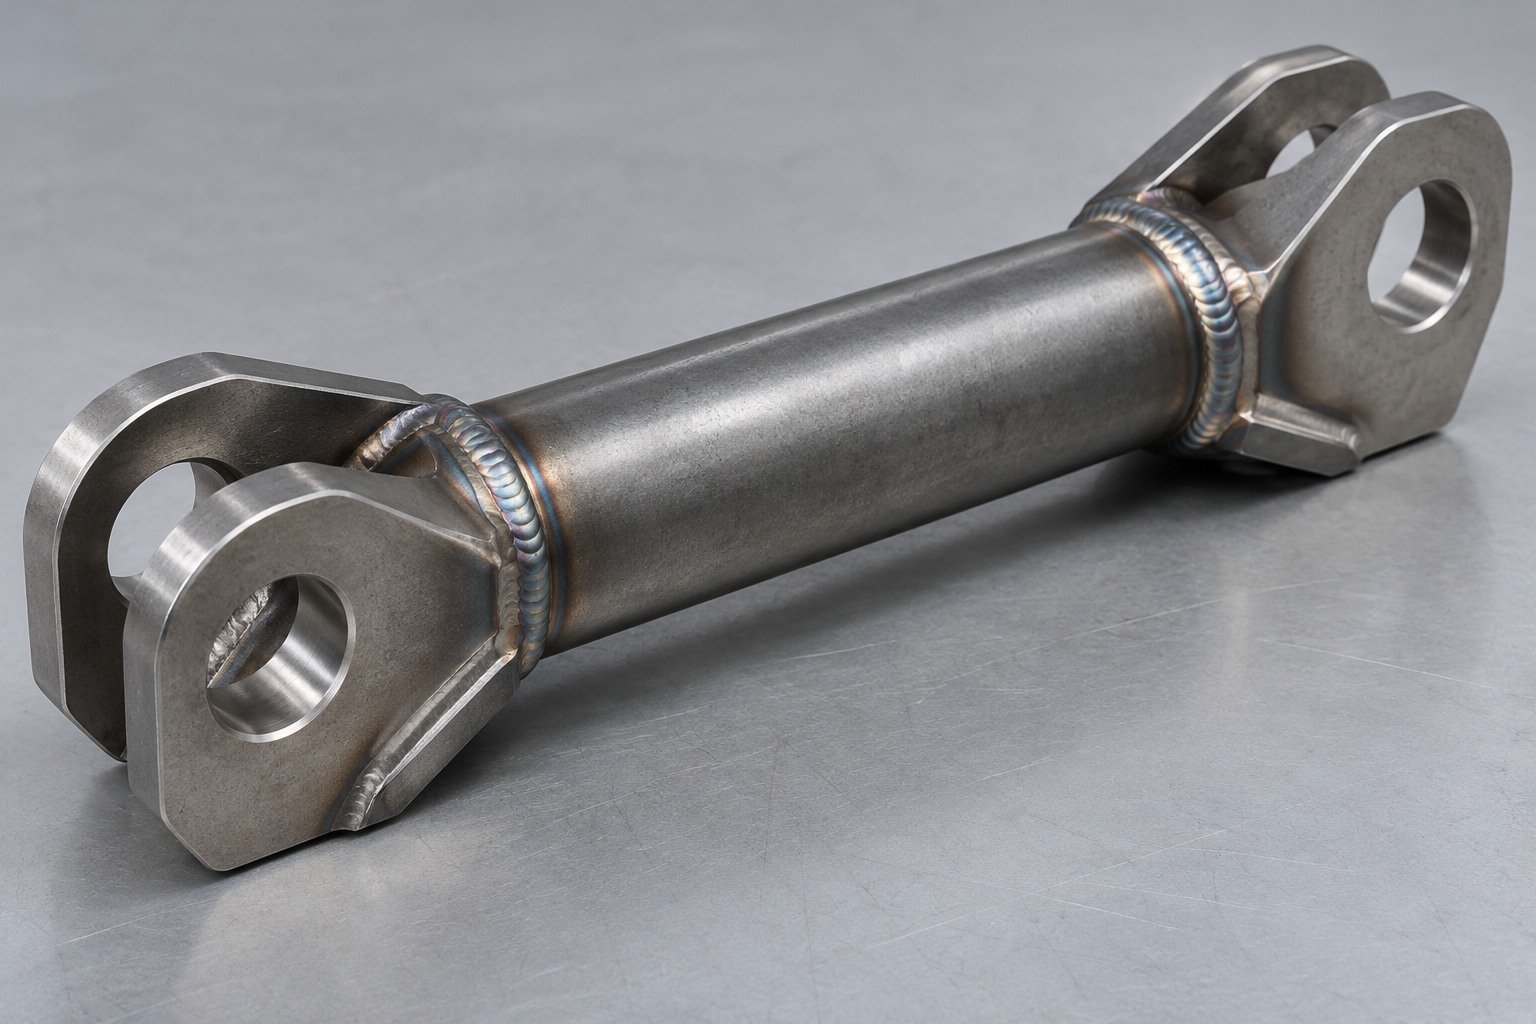
For a 4130 steel black oxide or 4130 steel zinc plating inquiry, specify exposure, full finish system, masked areas and dimensional acceptance. Review condition-specific controls.
Define the condition and acceptance method.
State locations and final inspection scope.
Agree dimensions after the full sequence.
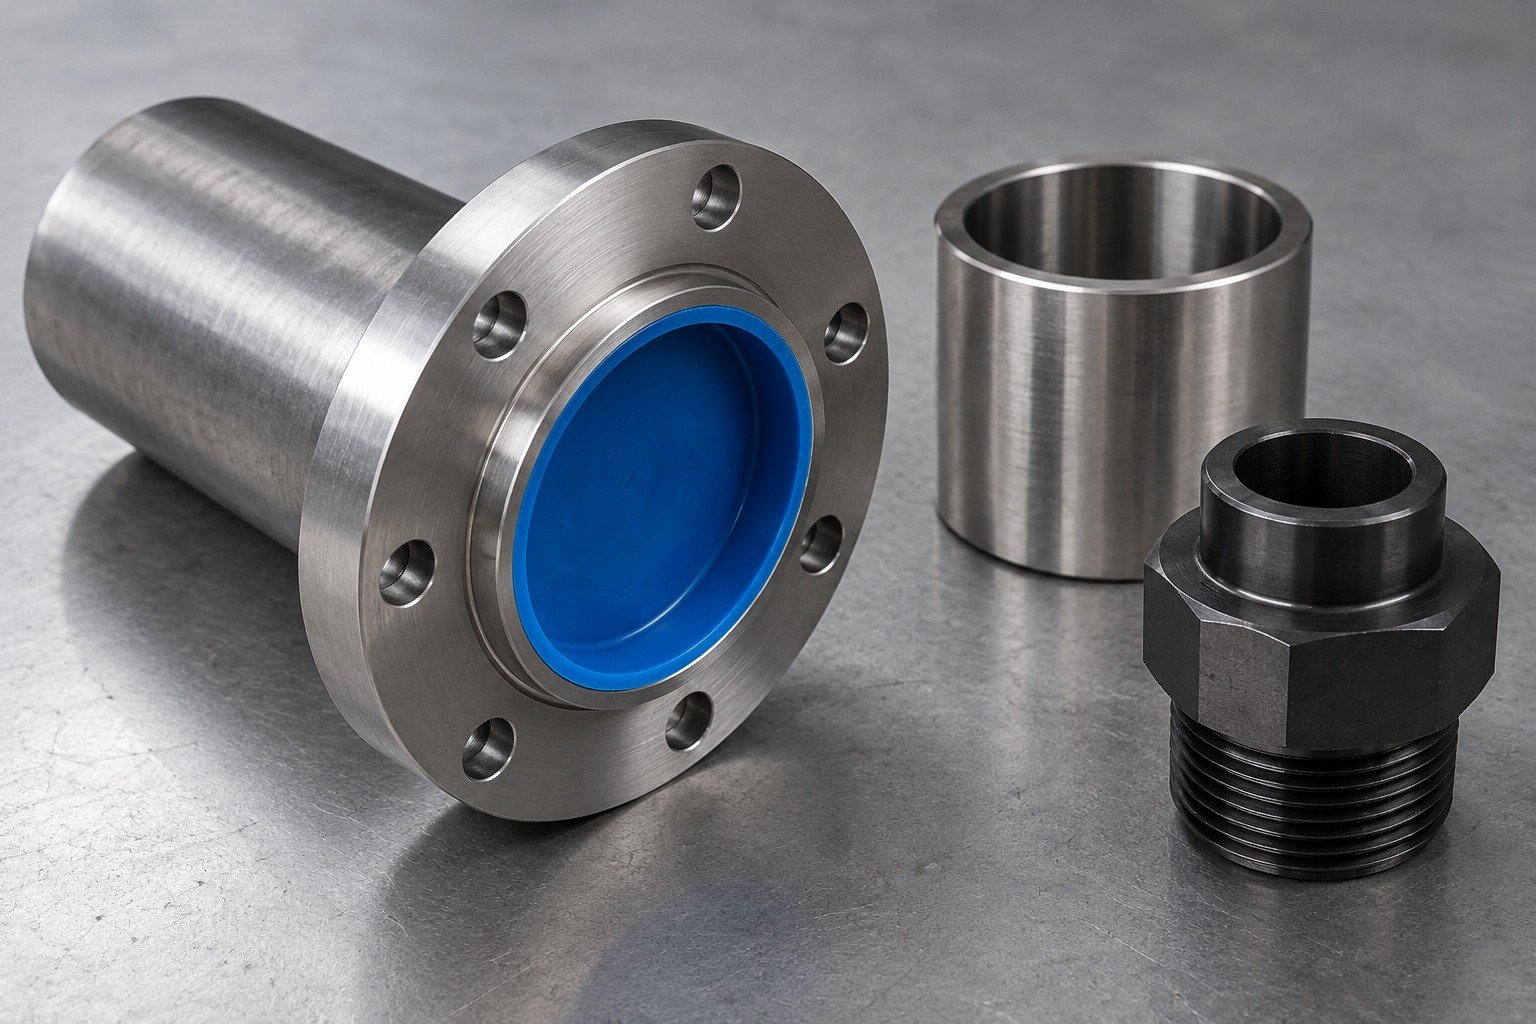
Identify datums, mating fits, runout or alignment and final inspection state. A pre-treatment measurement is not final acceptance after a changed thermal or joining route.
Define the condition and acceptance method.
State locations and final inspection scope.
Agree dimensions after the full sequence.
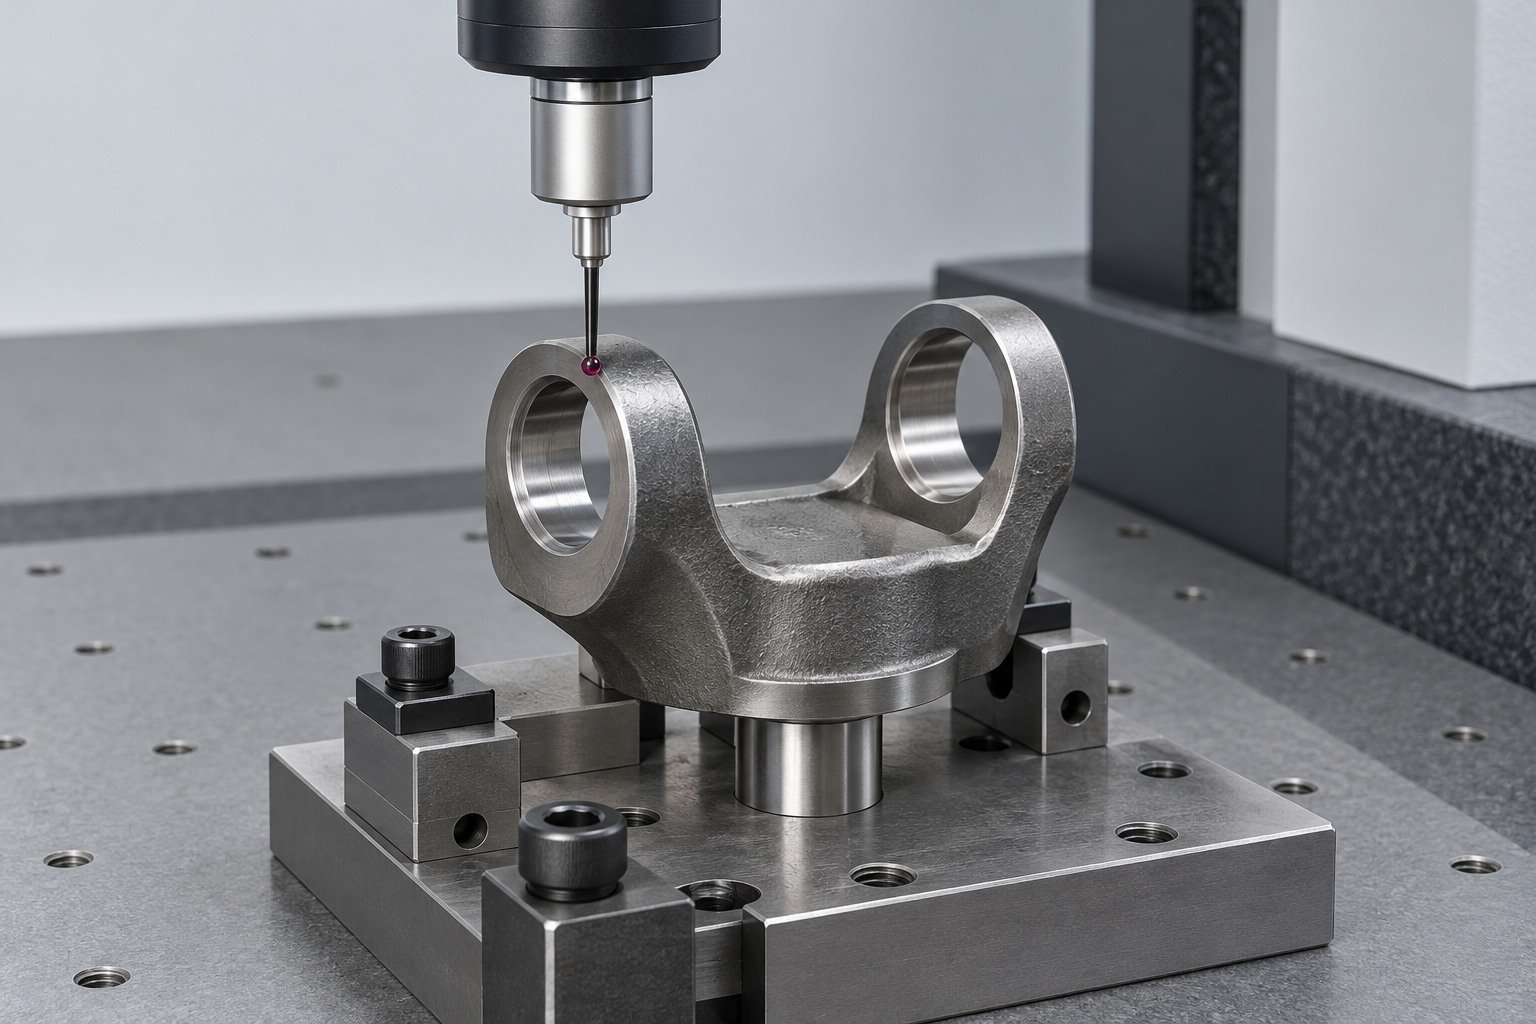
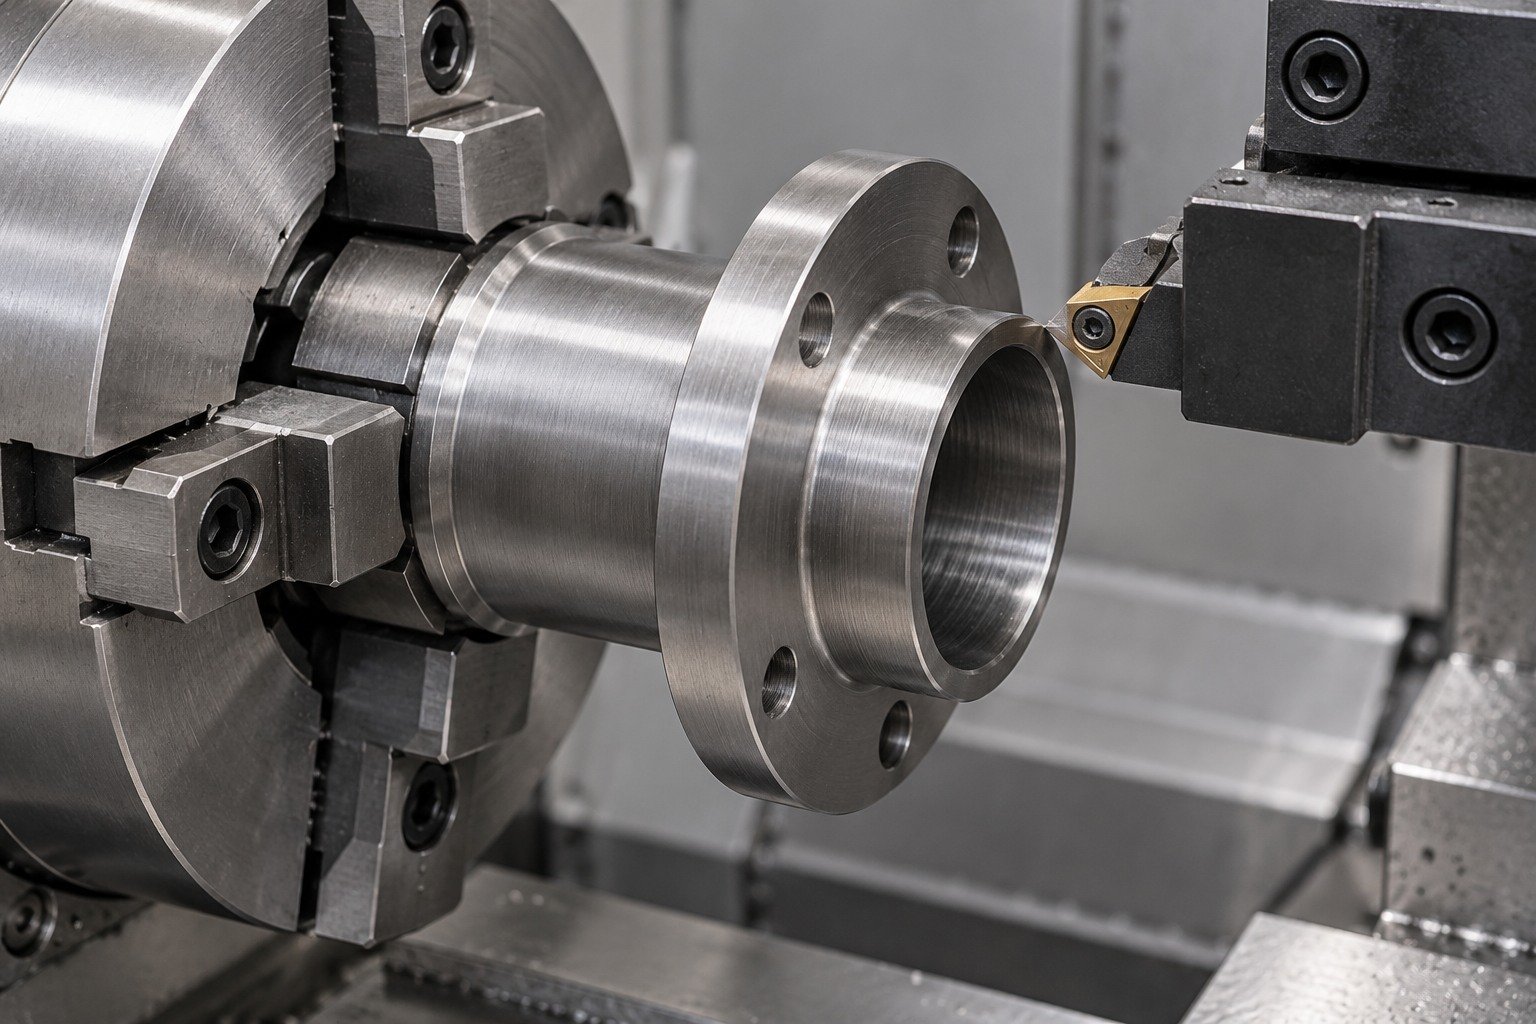
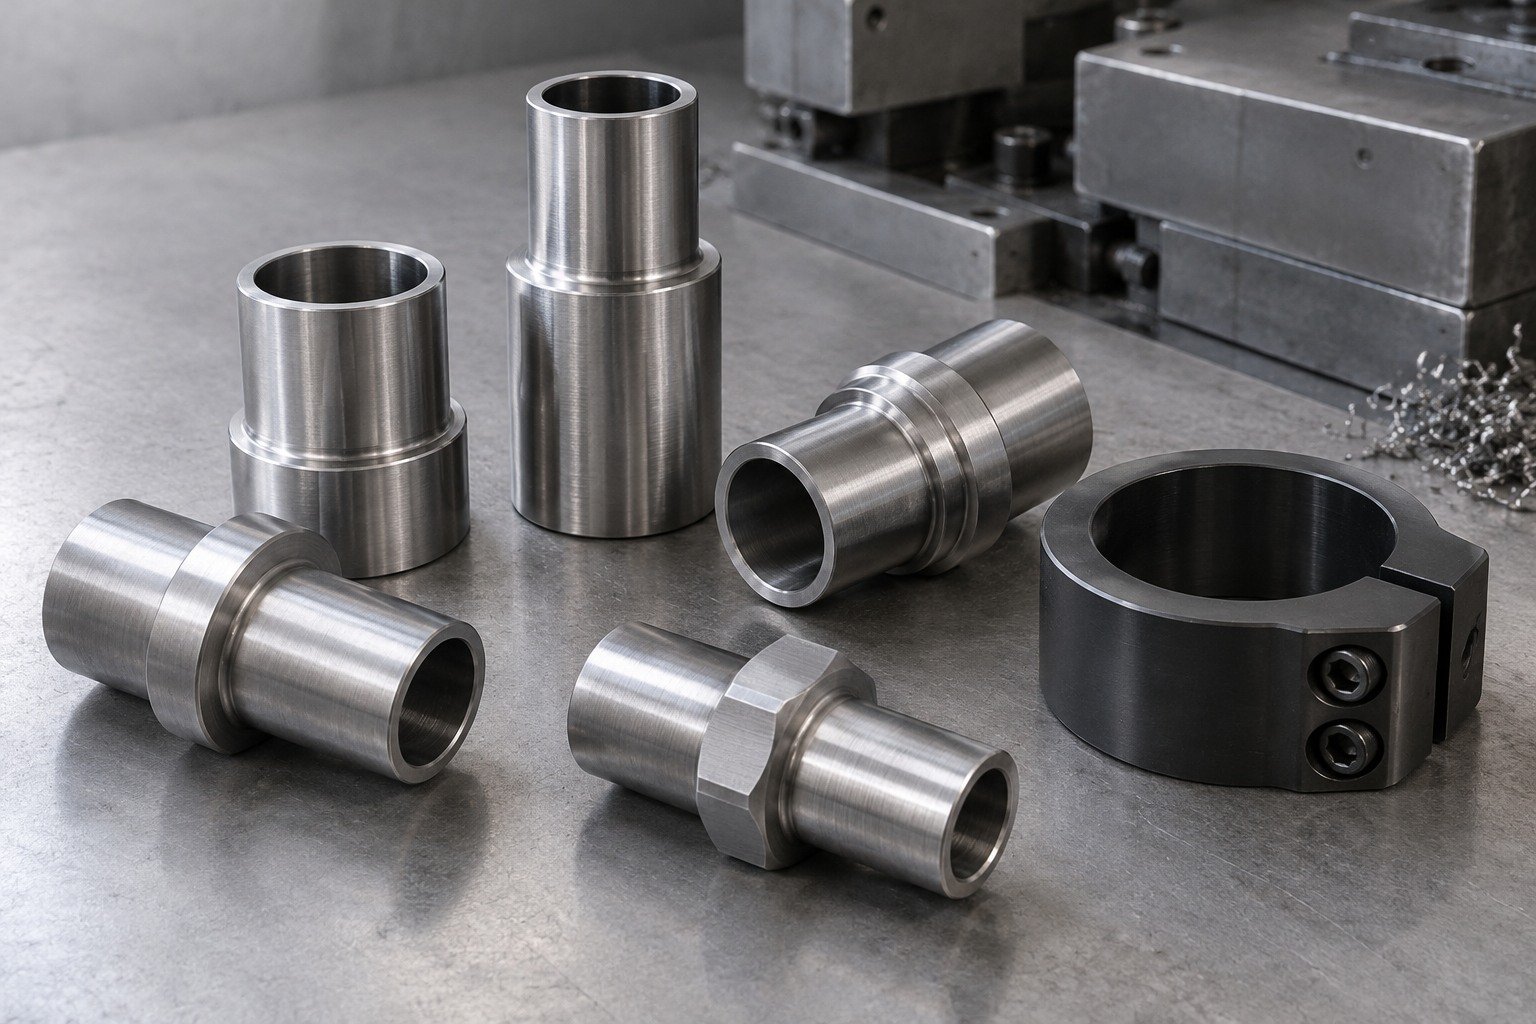
Illustrative components. Operations and availability are confirmed for your drawing.
Grade, product form, wall or section, condition and lot identity.
Thermal or joining route, distortion and remaining allowance.
Final fits, surface protection and agreed acceptance evidence.
Review grade, product standard, form, condition and lot identity. Agree any required material declarations at inquiry.
Sampling, methods and document scope are agreed with your quotation.
Quality Assurance →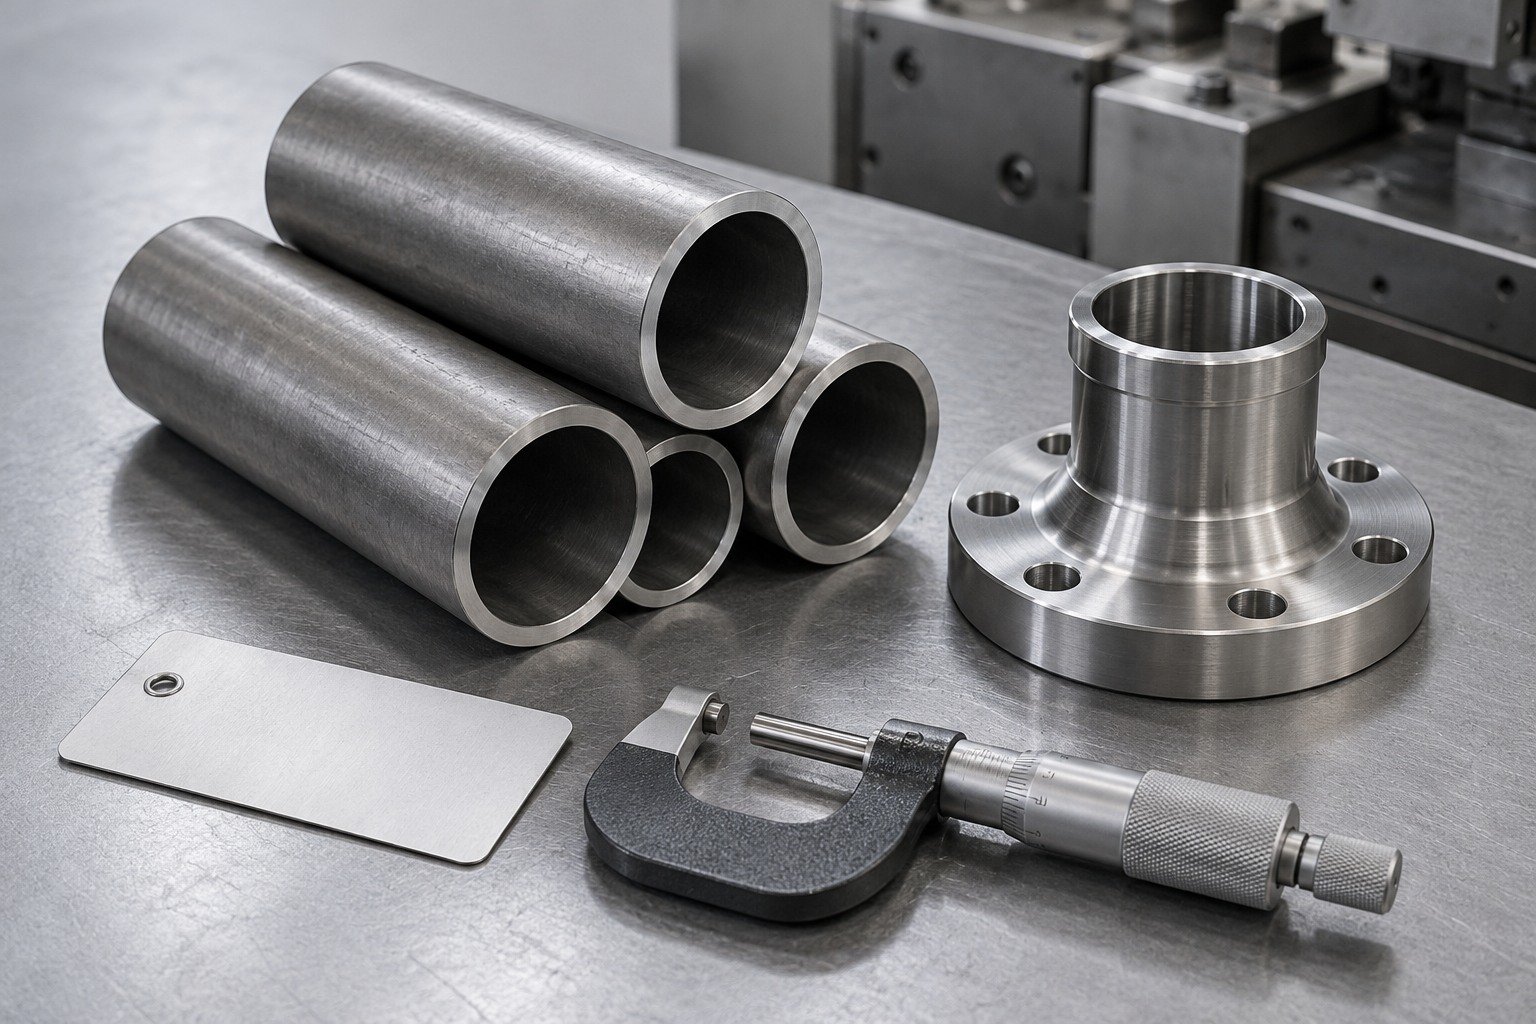
Connect critical dimensions and mating fits to the planned treatment, joining and finishing sequence.
Sampling, methods and document scope are agreed with your quotation.
Quality Assurance →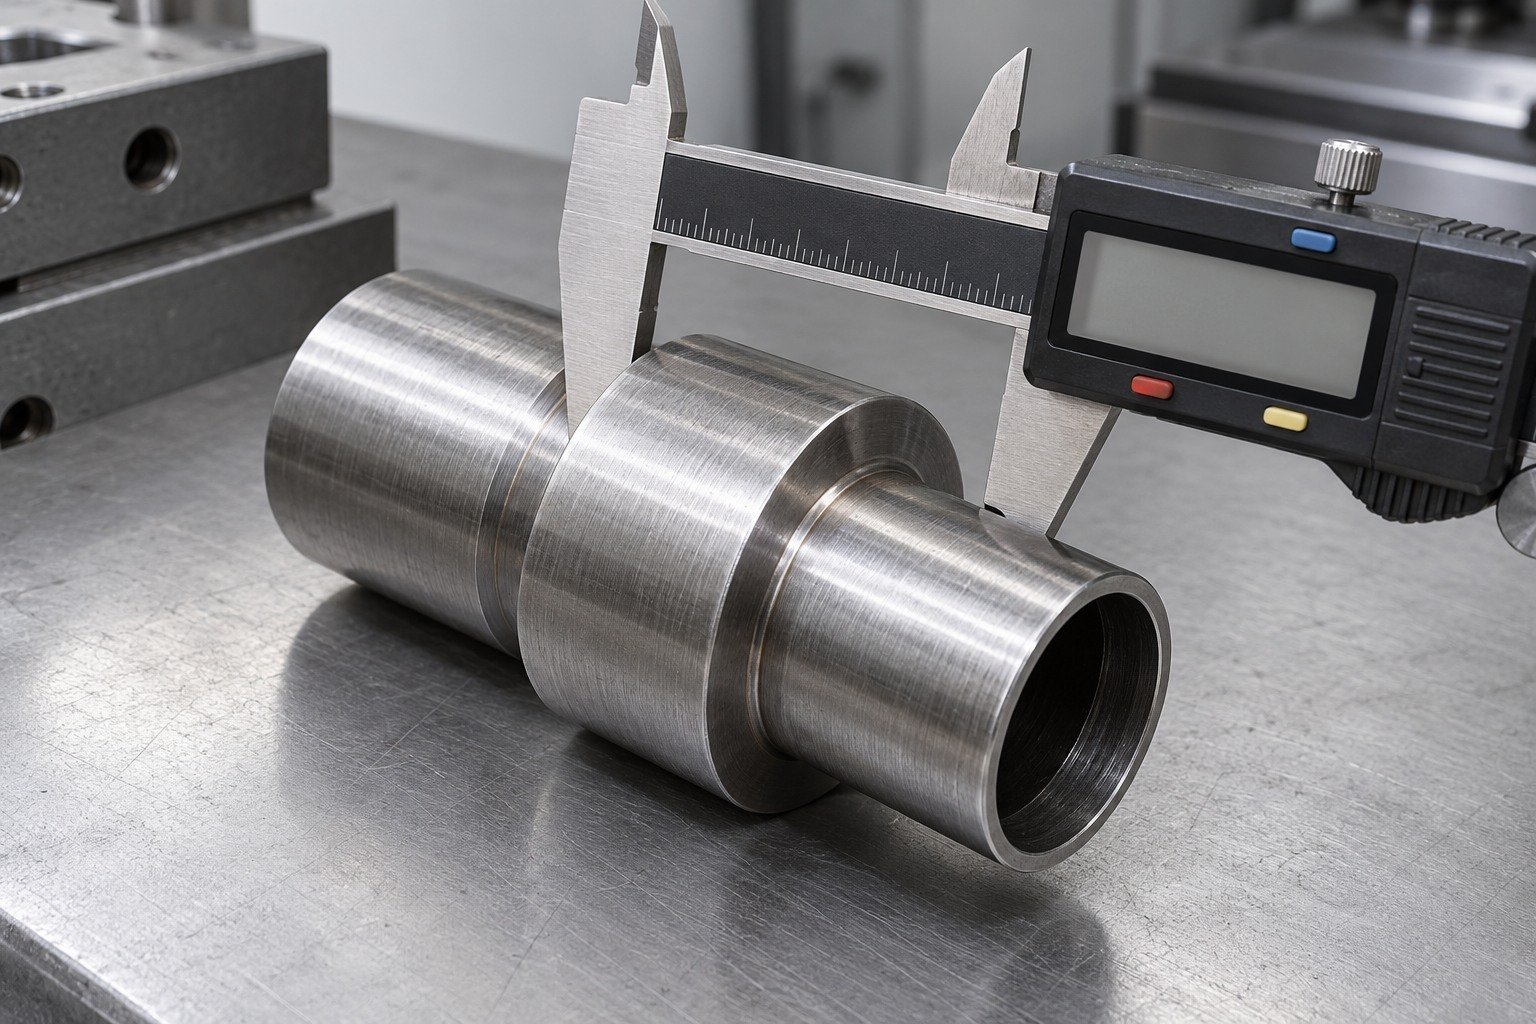
Identify bores, thread fits, datum relationships and final inspection scope. Keep the approved drawing revision with the records.
Sampling, methods and document scope are agreed with your quotation.
Quality Assurance →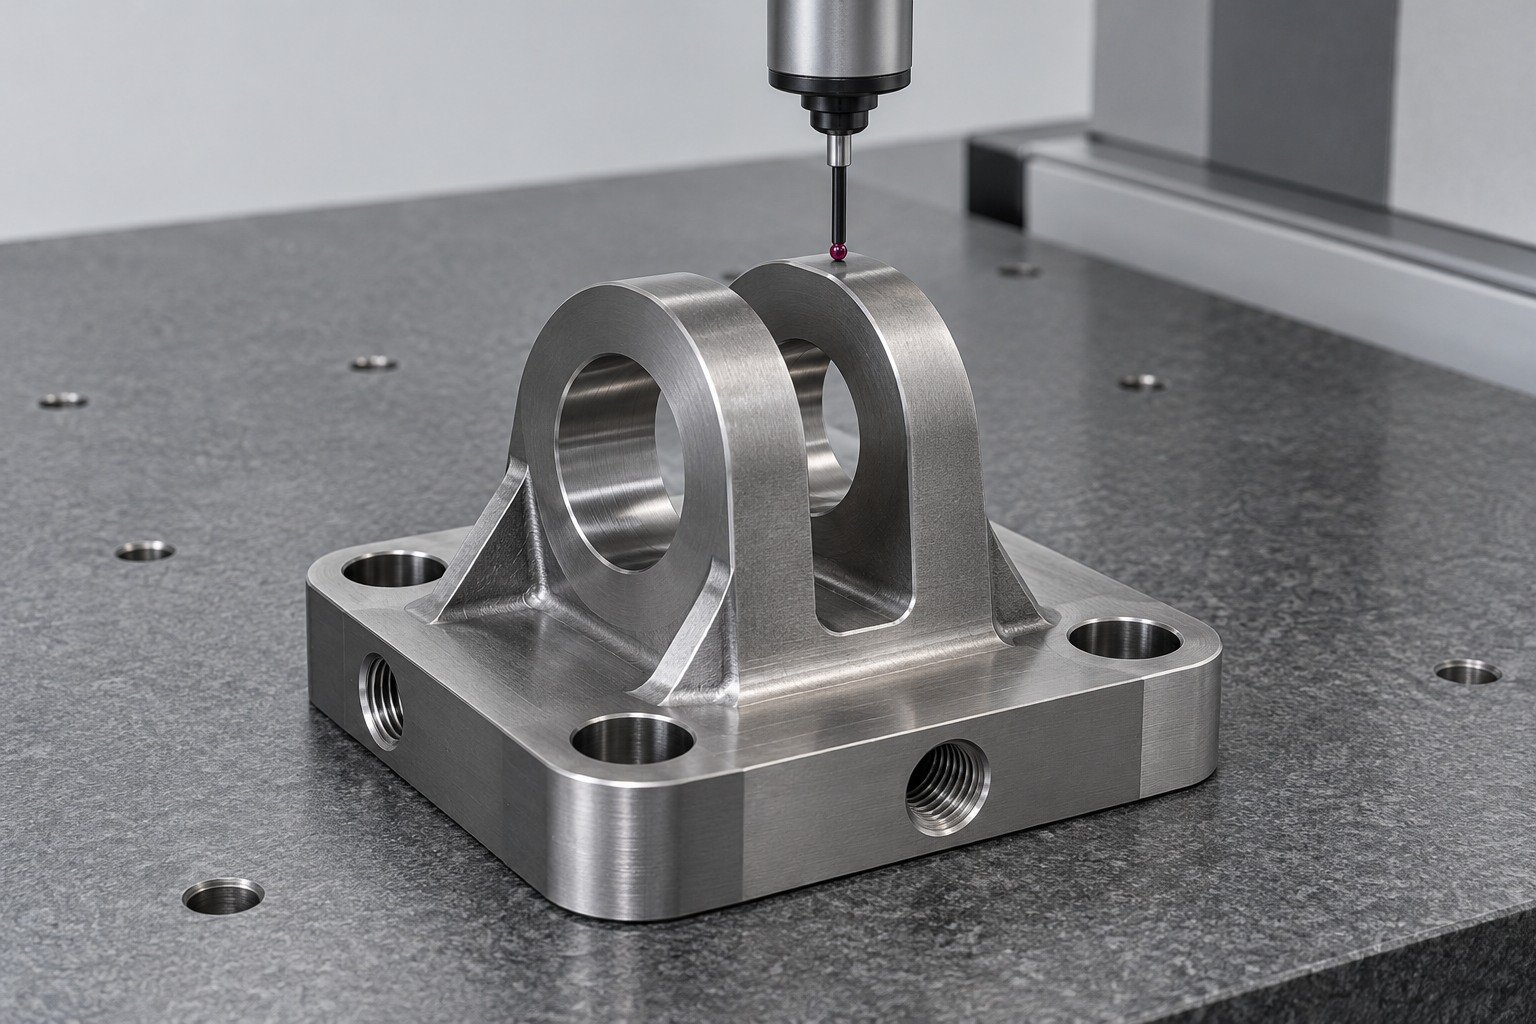
Confirm handling protection, packaging, part identification and the documents needed by your receiving team.
Sampling, methods and document scope are agreed with your quotation.
Quality Assurance →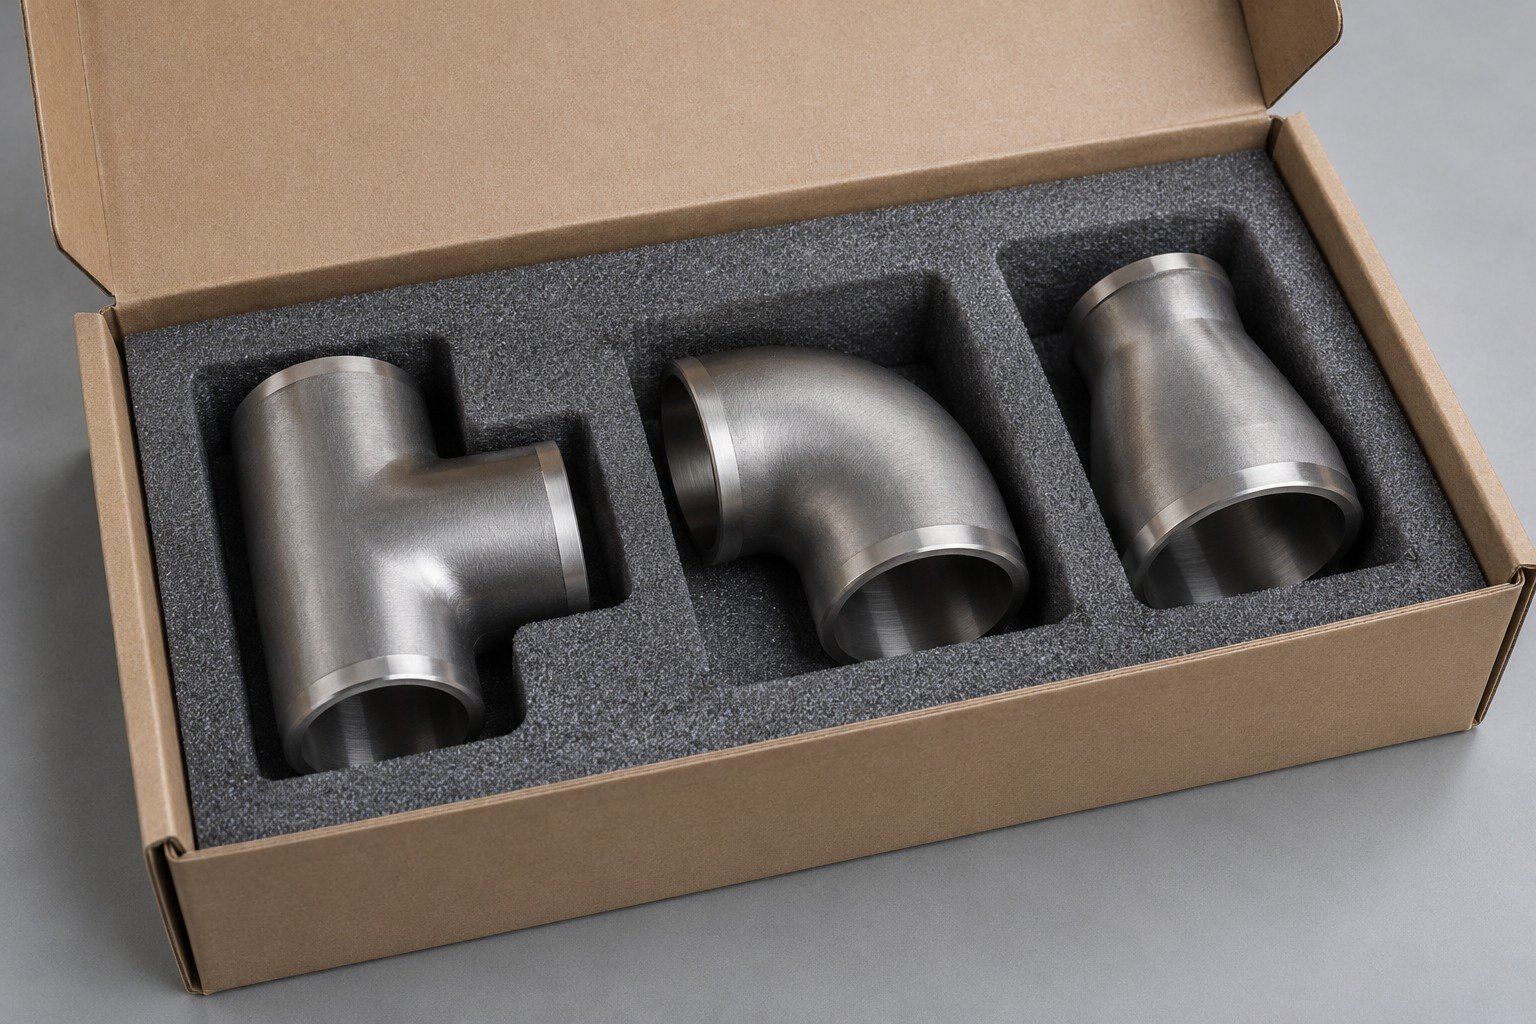
Coordinate your drawing review, material condition, sample decisions and receiving requirements.
It can be reviewed for welding under specified conditions. Product form, section, supplied state, joint and procedure matter. Agree the final acceptance and any required post-weld route.
Compare required properties, section, stock condition, joining and thermal route. These are different grades; approve the complete specification before substitution.
Review load, required condition, section and verification requirements. Do not select a grade from a generic strength ranking.
It is an alloy steel, not stainless steel. Define exposure, protective finish, storage and shipping protection for your component.
A specified thermal route can be reviewed. State target properties or hardness, section, test locations and final machining; the grade alone does not define acceptance.
Send the controlled drawing, product form, supplied condition, quantity, process sequence, finish and inspection scope for your quotation.
Tubular connections, fittings and general mechanical components are selection examples. Your actual load, joint, final condition and acceptance govern suitability.
Compare Carbon & Alloy Steel →
References support material selection. Your order specification and material records govern.





