

Injection Molding
Tooling and molding for your repeat plastic parts.
From prototype to production, coordinated manufacturing solutions for your custom parts.
View All Services →
Precision parts for your tight tolerances and complex geometry.
Tooling and molding for your repeat plastic parts.

Metal casting options for your part and production volume.

Cutting, forming and welding for your fabricated parts.

Custom profiles for your section, length and finish requirements.

Finishes for your appearance, corrosion and wear requirements.

Sub-assemblies and final builds for your production program.

Production tooling built around your process and volume.

Prototype parts to check fit, function and design.
DFM, process planning and production support for your project.
Inspection, documentation, inventory and delivery planning for your program.
Choose air- or liquid-cooling components around your thermal and mechanical requirements.

Manufacturing support for your cold plates, manifolds and cooling assemblies.

Find components for your power electronics, energy, laser and telecom application.

Components for your electronic systems.
Start with your functional and quality requirements.
Build around your operating environment.
From prototype to production, review material performance, manufacturability and cost for your part.
Review grade, temper and finish for your metal parts.
 AluminumStrength, weight and machining›
 Stainless SteelCorrosion and finish requirements›
 Carbon & Alloy SteelDiscuss grade and heat treatment›
 Tool SteelDiscuss tooling and wear needs›
 TitaniumReview grade and part geometry›
 Copper & BrassDiscuss conductivity and machining›
Match your polymer to function, process and environment.
 ABSReview enclosure and molding needs›
 Polycarbonate (PC)Discuss clarity and impact needs›
 Nylon (PA)Review moisture and wear conditions›
 POM / AcetalReview fit and sliding features›
 PEEKDiscuss operating conditions›
 PTFEReview friction and chemical exposure›
 ULTEM / PEIDiscuss thermal and electrical needs›
Confirm grade availability and application requirements.
 Silicone / LSRDiscuss flexible component needs›
 TPU / TPEReview flexibility and processing›
 EPDMReview weathering and chemical exposure.›
 NBRReview oil and fuel exposure.›
 FKMReview temperature and chemical exposure.›
 G10 / FR4Review insulation and laminate needs›
 CompositesReview stiffness, weight and laminate.›Customer-Specified MaterialsConfirm your grade and requirements.›Other Specialty MaterialsDiscuss your application and grade.›
Practical guidance for your part geometry and material decisions.
Prepare your process, budget and sourcing questions.
Build your knowledge before production.
Learn who we are and how we operate.
Find our U.S. support team or start a conversation.
YOUR DESIGN QUESTIONS. YOUR TRIAL PARTS. YOUR INTERIM SUPPLY.
Review your prototype tooling around what your molded part must prove. Connect design changes, resin, trial acceptance and interim demand before committing to a mold.
2 different purposes: learn from a prototype mold; plan temporary supply with bridge tooling. Your project may need either route, both, or a direct production tool.
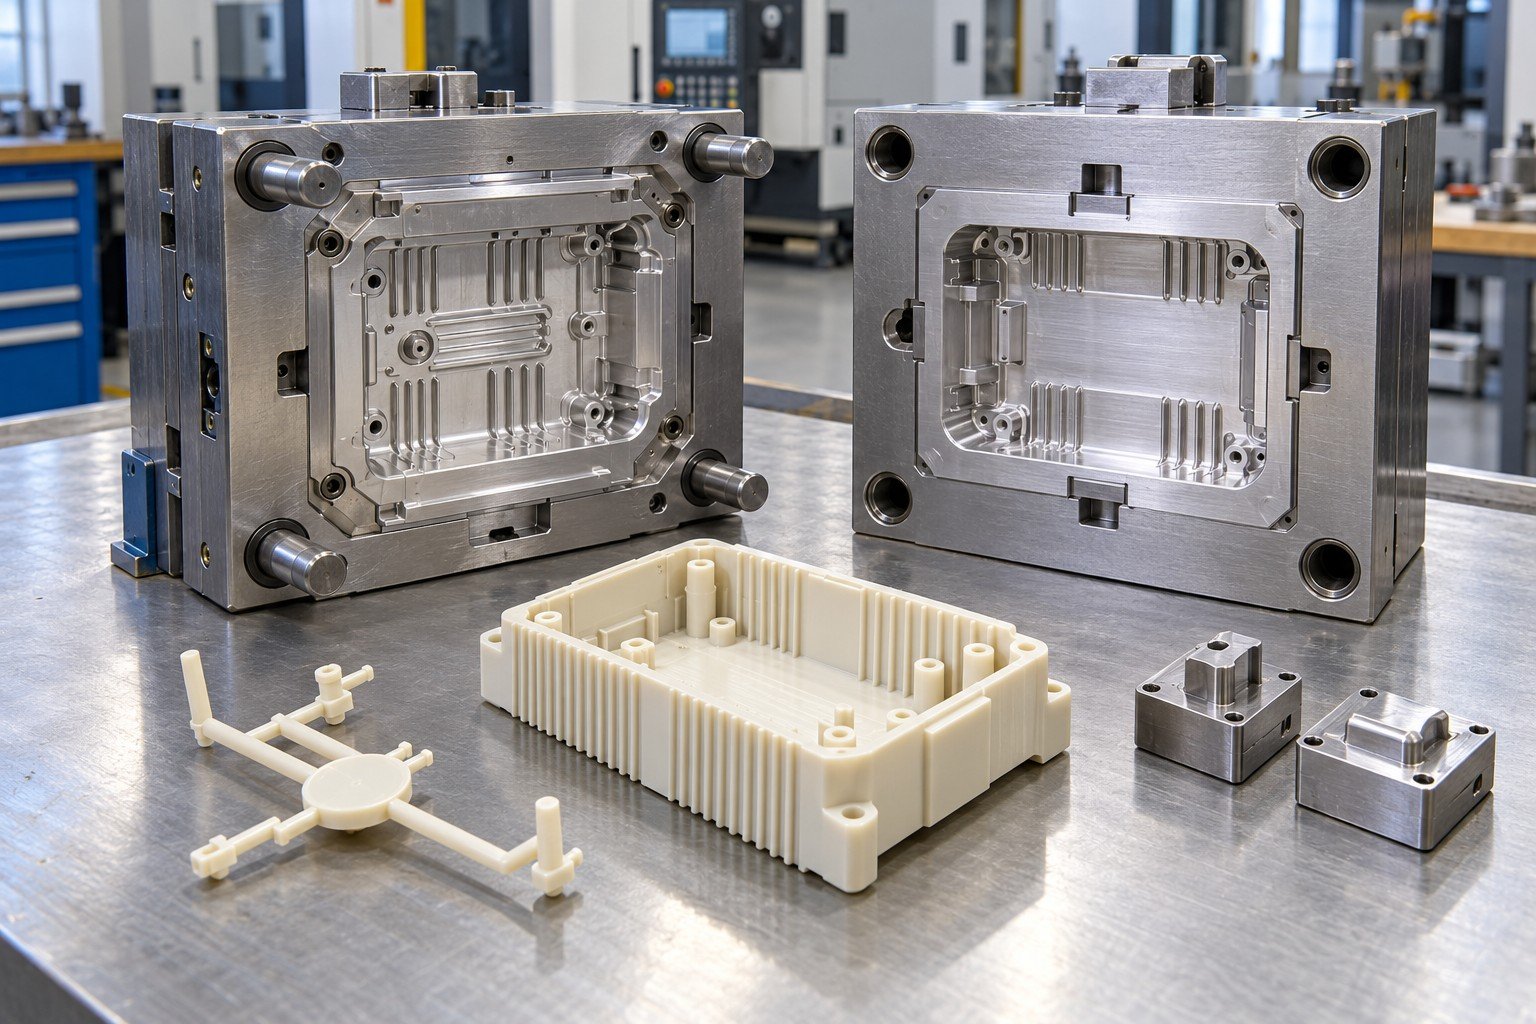
Validation or interim supply
Exact grade and conditions
Inserts, holder and machine
Trial and part acceptance
Change, repeat or transfer
Give your tool a clear learning or supply objective rather than buying a smaller production mold by assumption.
Name the fit, appearance, assembly or material question the molded sample must answer.
Control CAD, revision, resin grade, critical features and visible surfaces.
Separate stable interfaces from features that may need replaceable inserts.
Provide trial quantities and any interim supply demand as separate inputs.
Agree trial evidence, corrections, ownership, storage and release conditions.
Keep prototype validation, interim supply and production release as distinct scopes.
Prototype tooling services should connect the mold concept to a defined part-validation objective. A molded sample is useful when you know what decision it supports.
| Your input | CAD, revision and the question your sample must answer. |
|---|---|
| Your decision | Agree trial quantity, resin and evidence before mold build. |
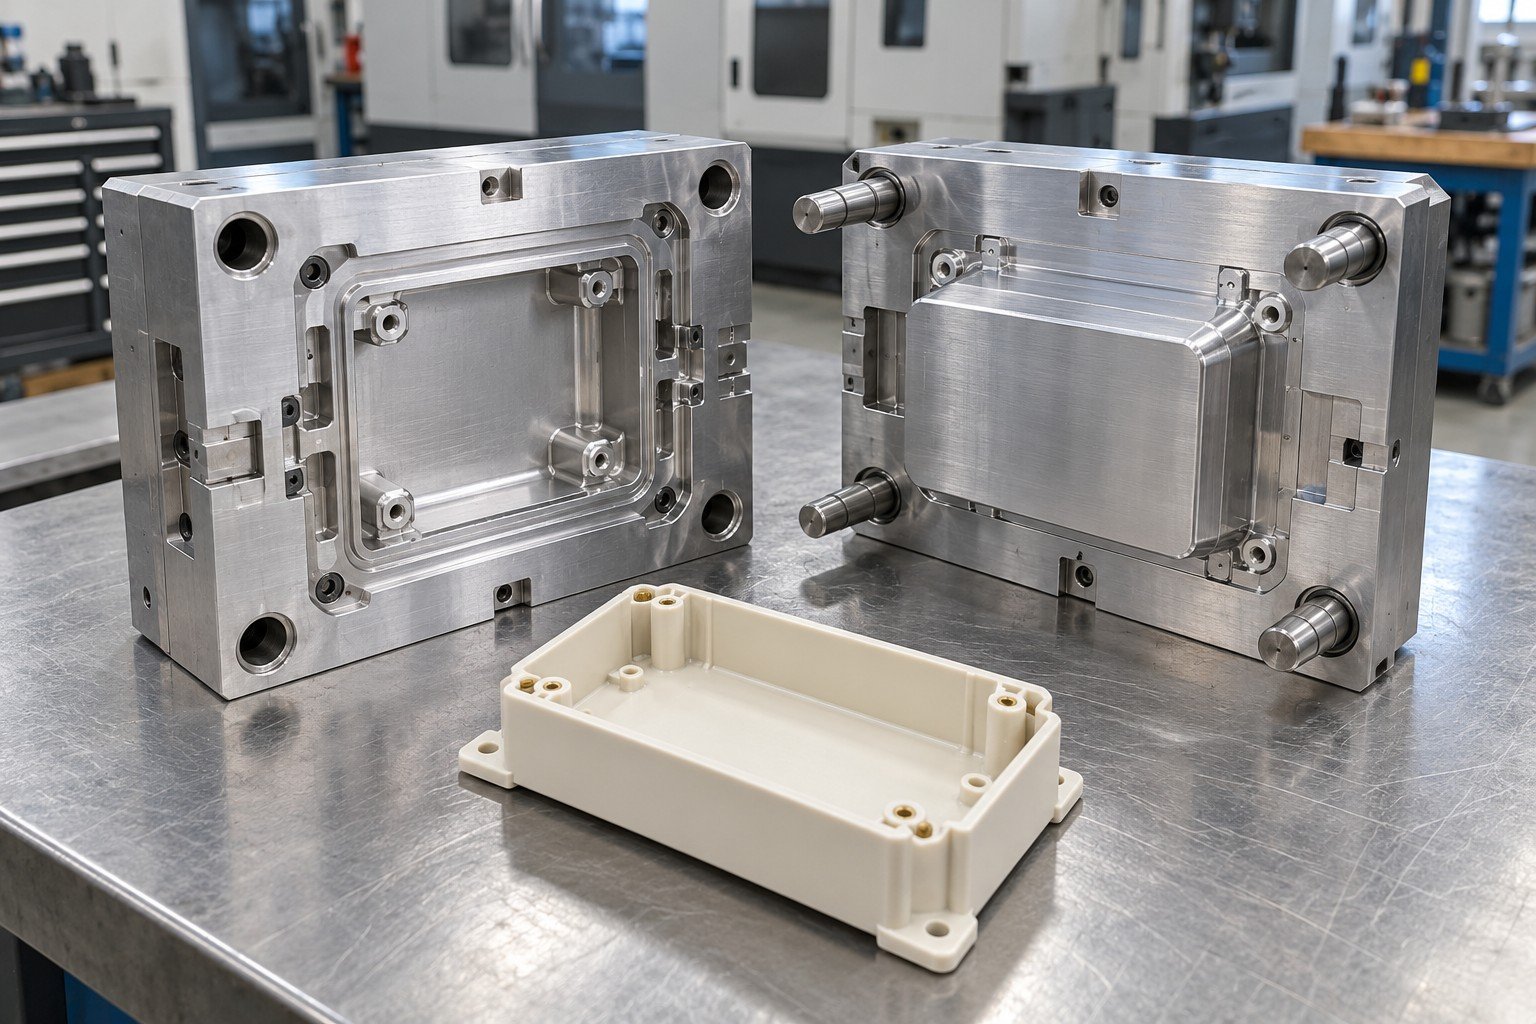
Prototype mold making can include a holder, core, cavity, ejectors and replaceable details. Record what is supplied and what remains part of the molding setup.
| Your input | Required tool components and receiving machine information. |
|---|---|
| Your decision | Define holder ownership, compatibility and included spares. |
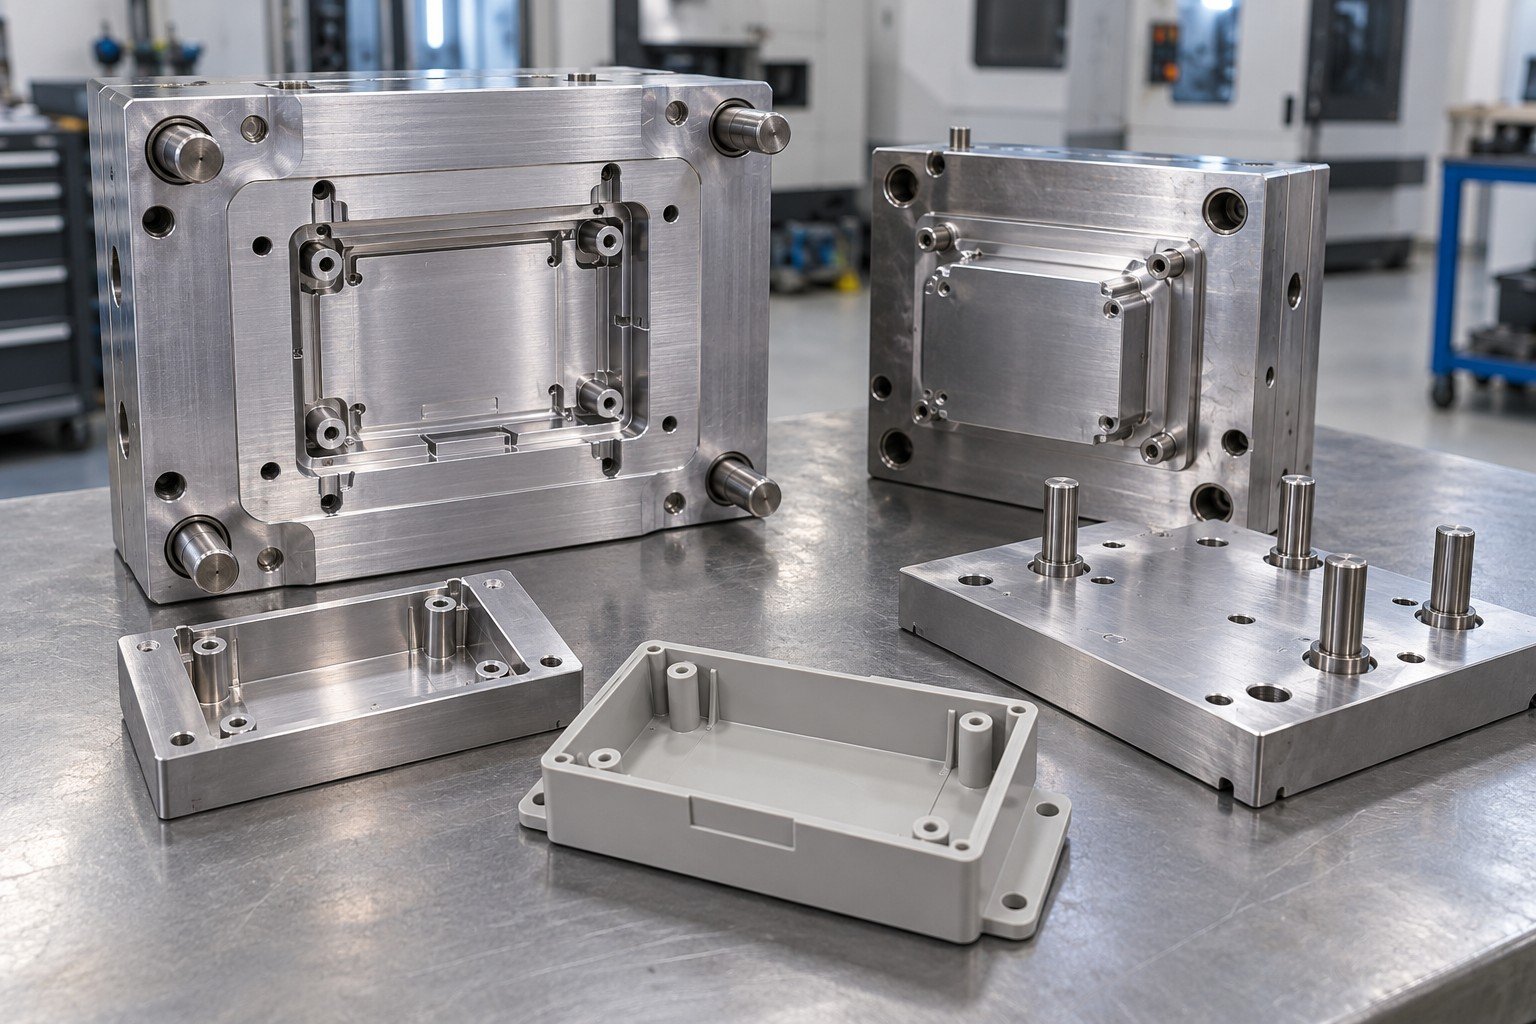
Prototype mold validation needs agreed dimensions, appearance and mating conditions. A tool photograph or a simulation alone cannot establish part acceptance.
| Your input | Critical features, mating parts and inspection method. |
|---|---|
| Your decision | Record actual resin, trial conditions, measurements and exceptions. |
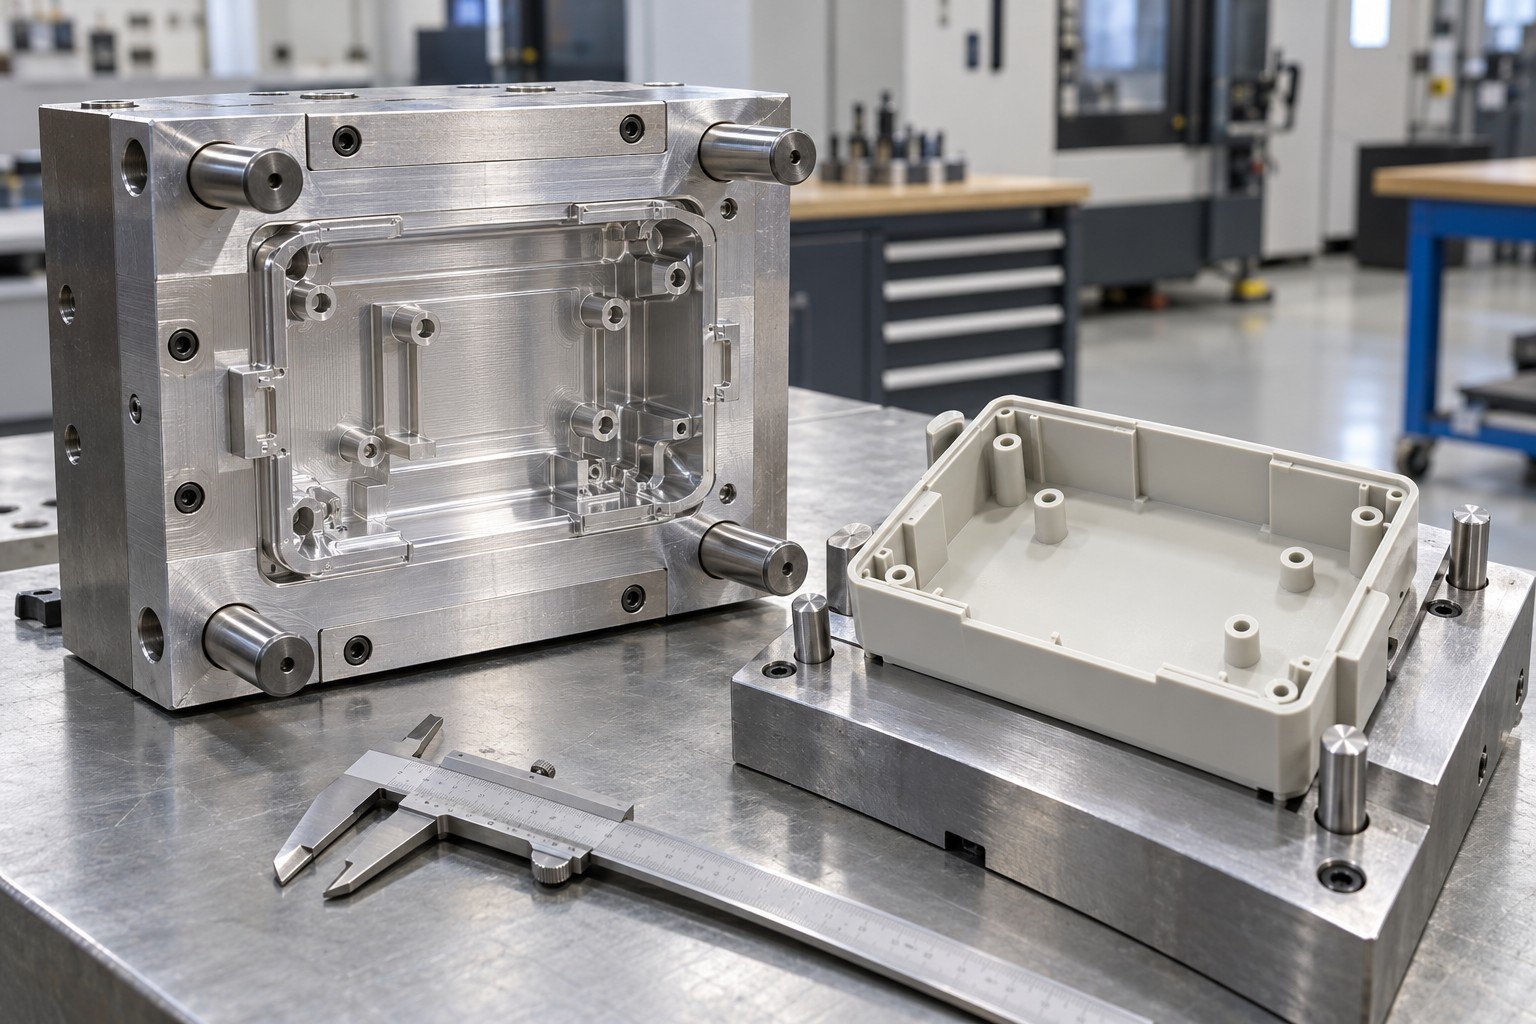
For prototype molds for plastic parts, distinguish a sample that answers a design question from a tool approved for repeat supply.
| Your input | Trial observations and authorized correction list. |
|---|---|
| Your decision | Decide which changes are needed and whether another trial is required. |
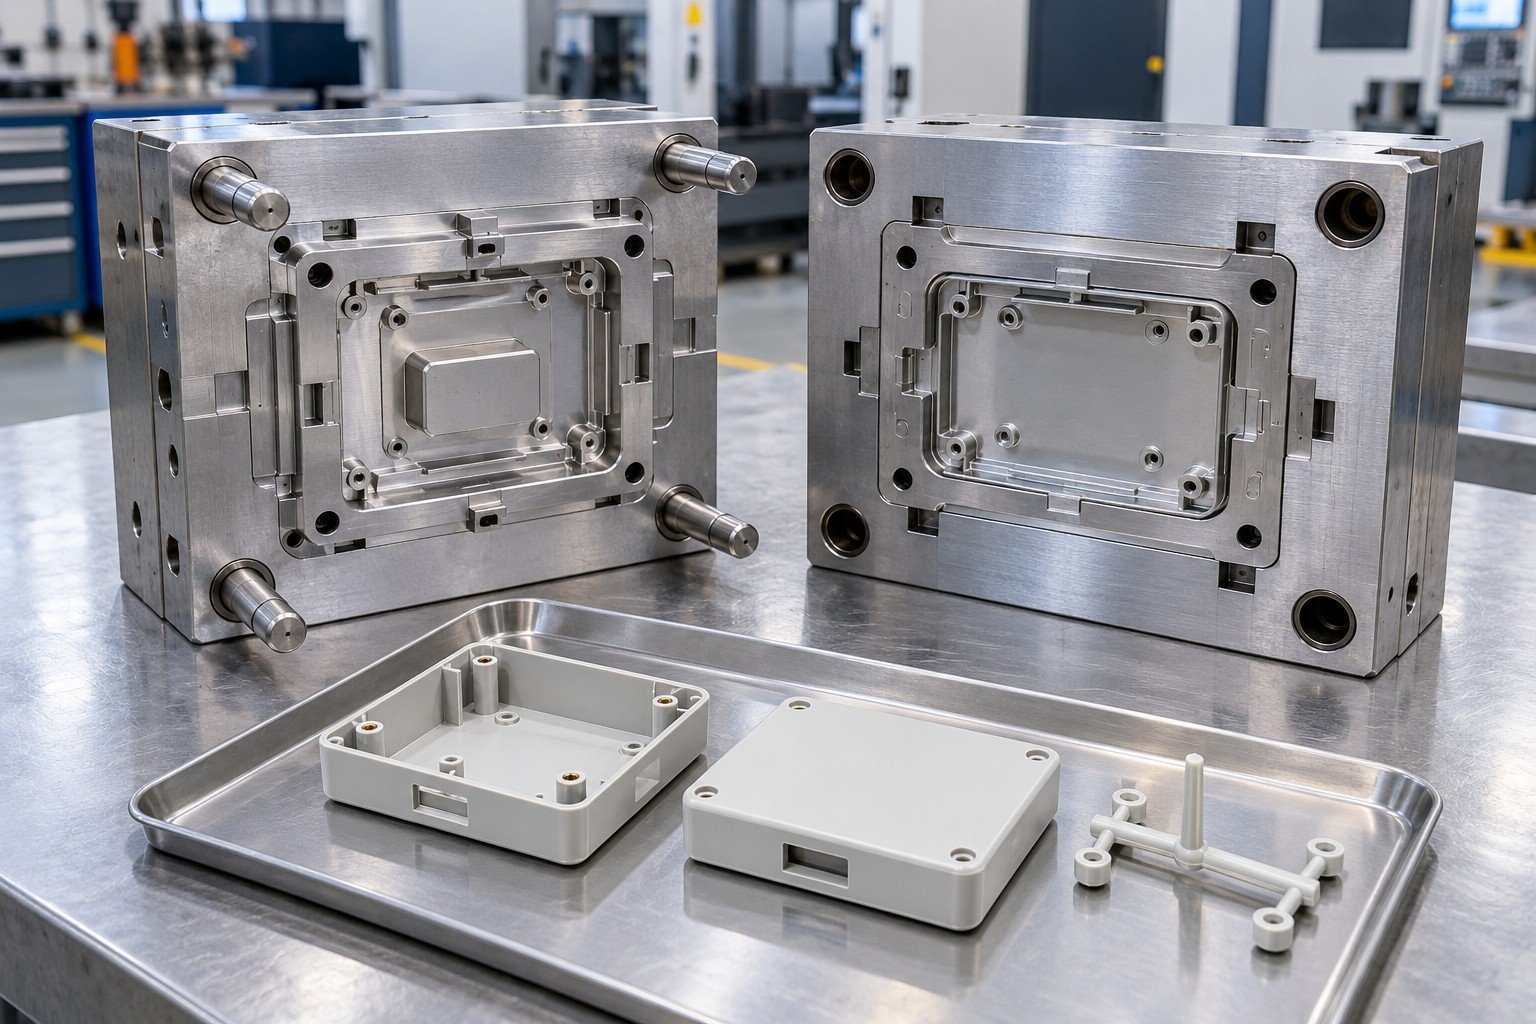
Bridge tooling services address an agreed interim need while your longer-term supply route is developed or approved. Temporary supply still needs controlled acceptance.
| Your input | Interim quantity, requested dates and production-route status. |
|---|---|
| Your decision | Agree the supply boundary and review the tool against expected use. |
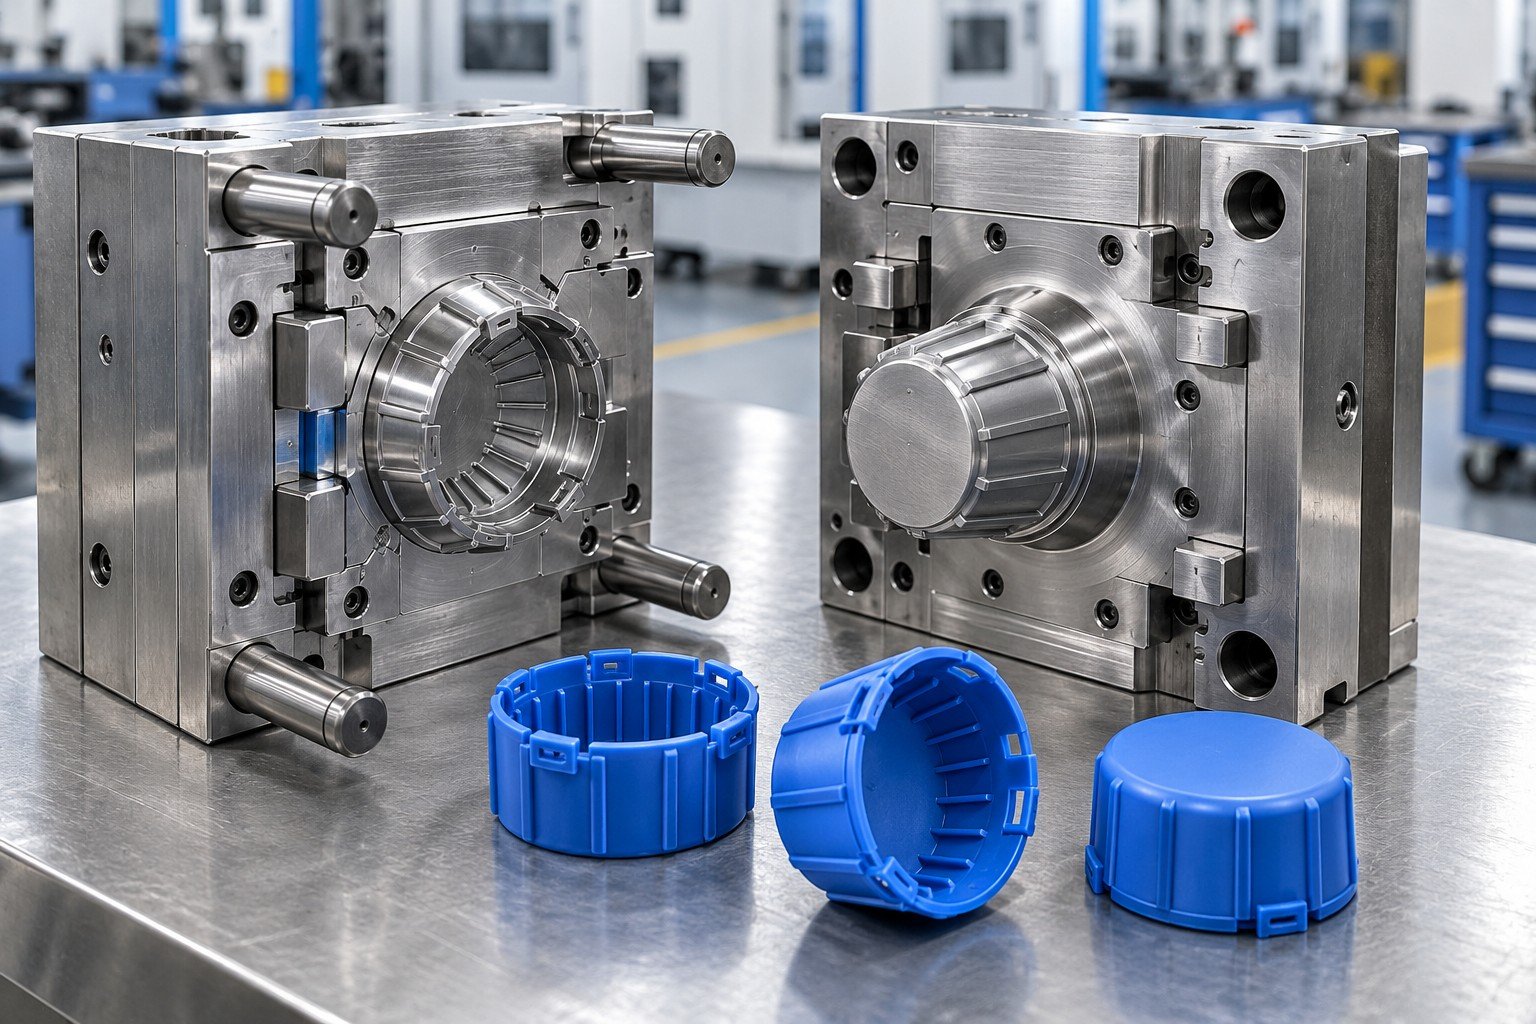
Bridge mold manufacturing may require a holder, cooling, ejection and replaceable wear details. Do not assume a bridge mold has no cooling or uses only aluminum.
| Your input | Resin, part geometry, expected use and machine interface. |
|---|---|
| Your decision | Define a workable construction and maintenance scope. |
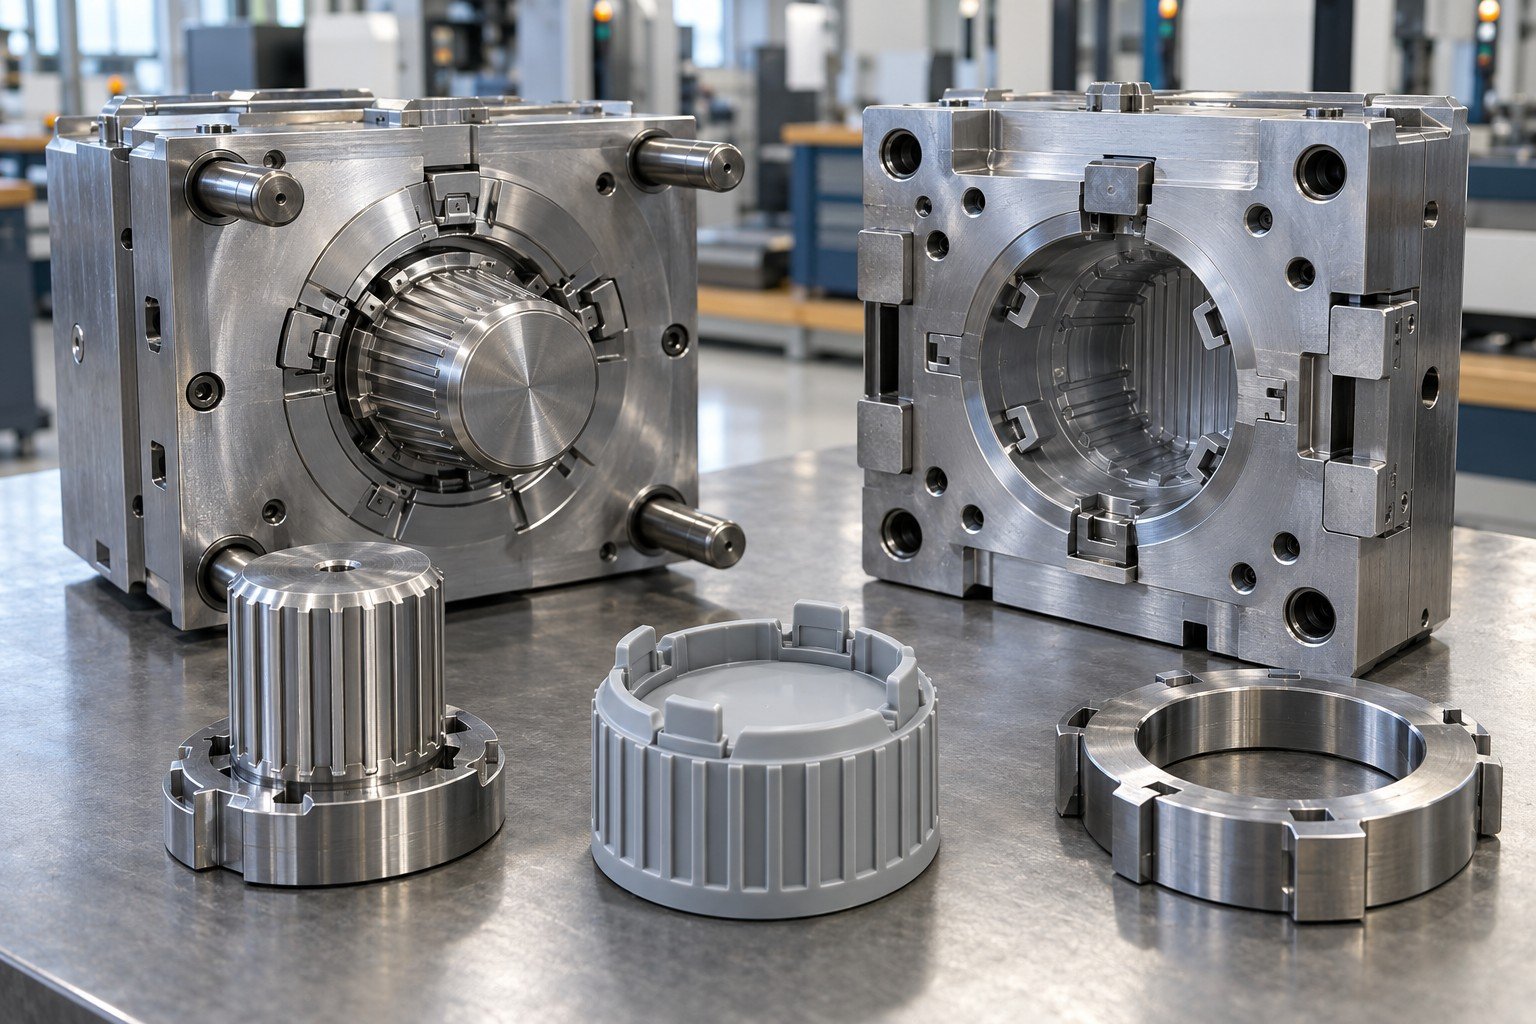
Low volume injection mold tooling does not make dimensions or appearance optional. State the acceptance plan for the actual supply period.
| Your input | Drawing limits, appearance reference and sampling requirements. |
|---|---|
| Your decision | Record approved samples and repeat-supply checks. |
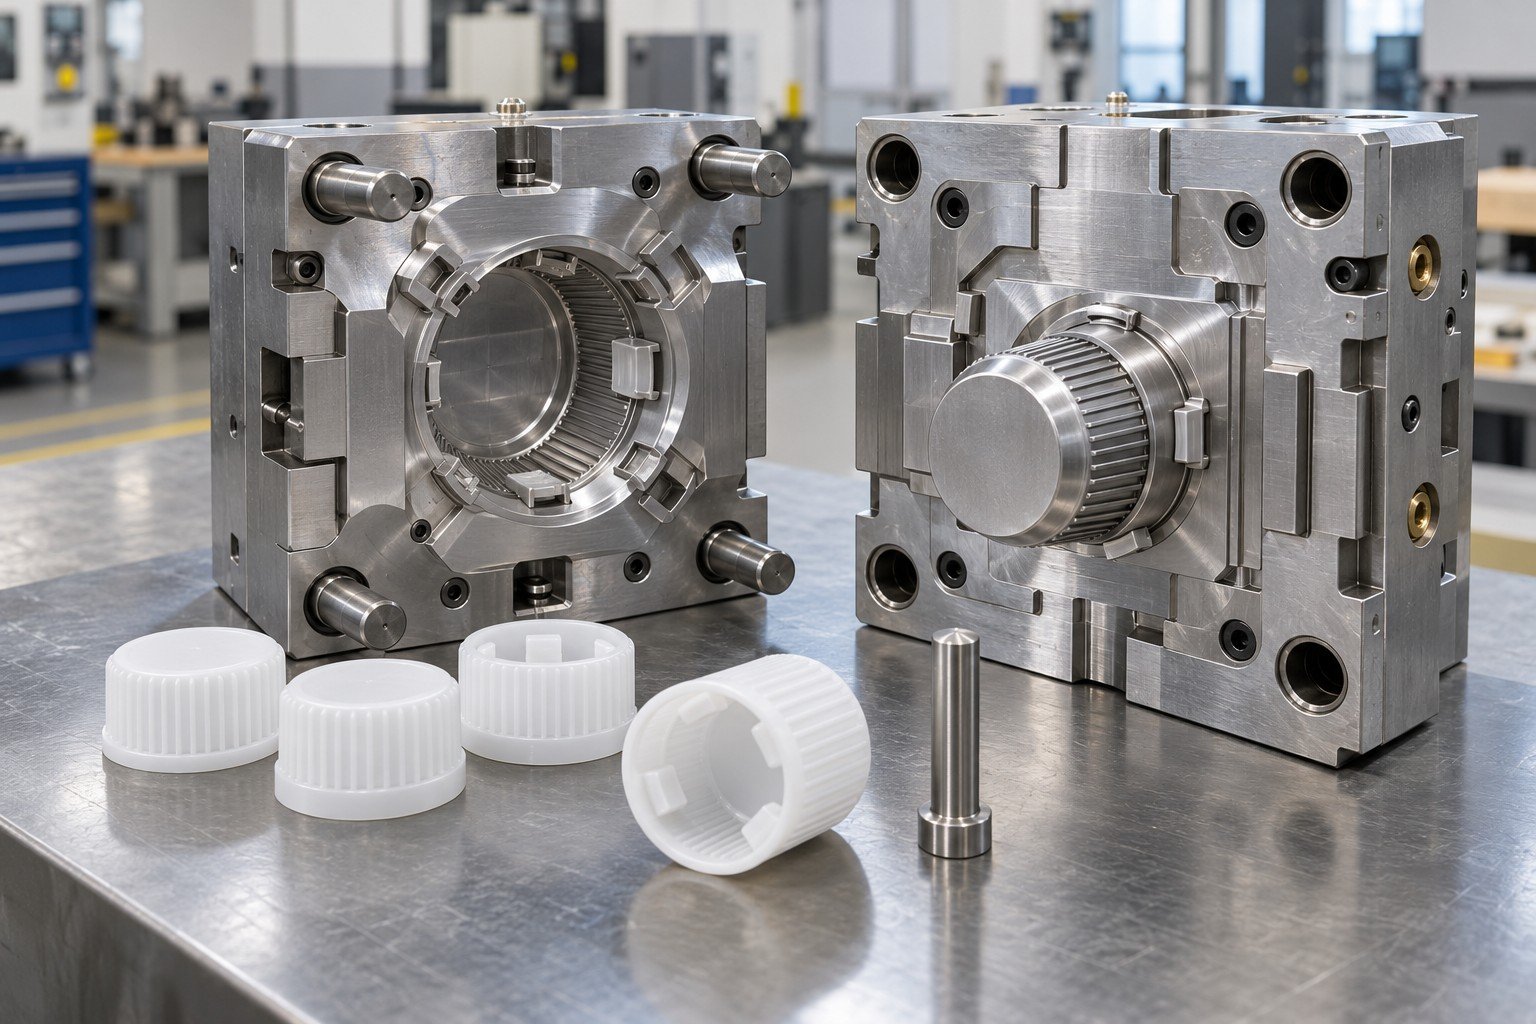
For bridge molds, record when interim production ends and what triggers repair, transfer or a new production tool review.
| Your input | Updated demand and approved long-term route. |
|---|---|
| Your decision | Confirm tool condition and remaining responsibilities before handoff. |
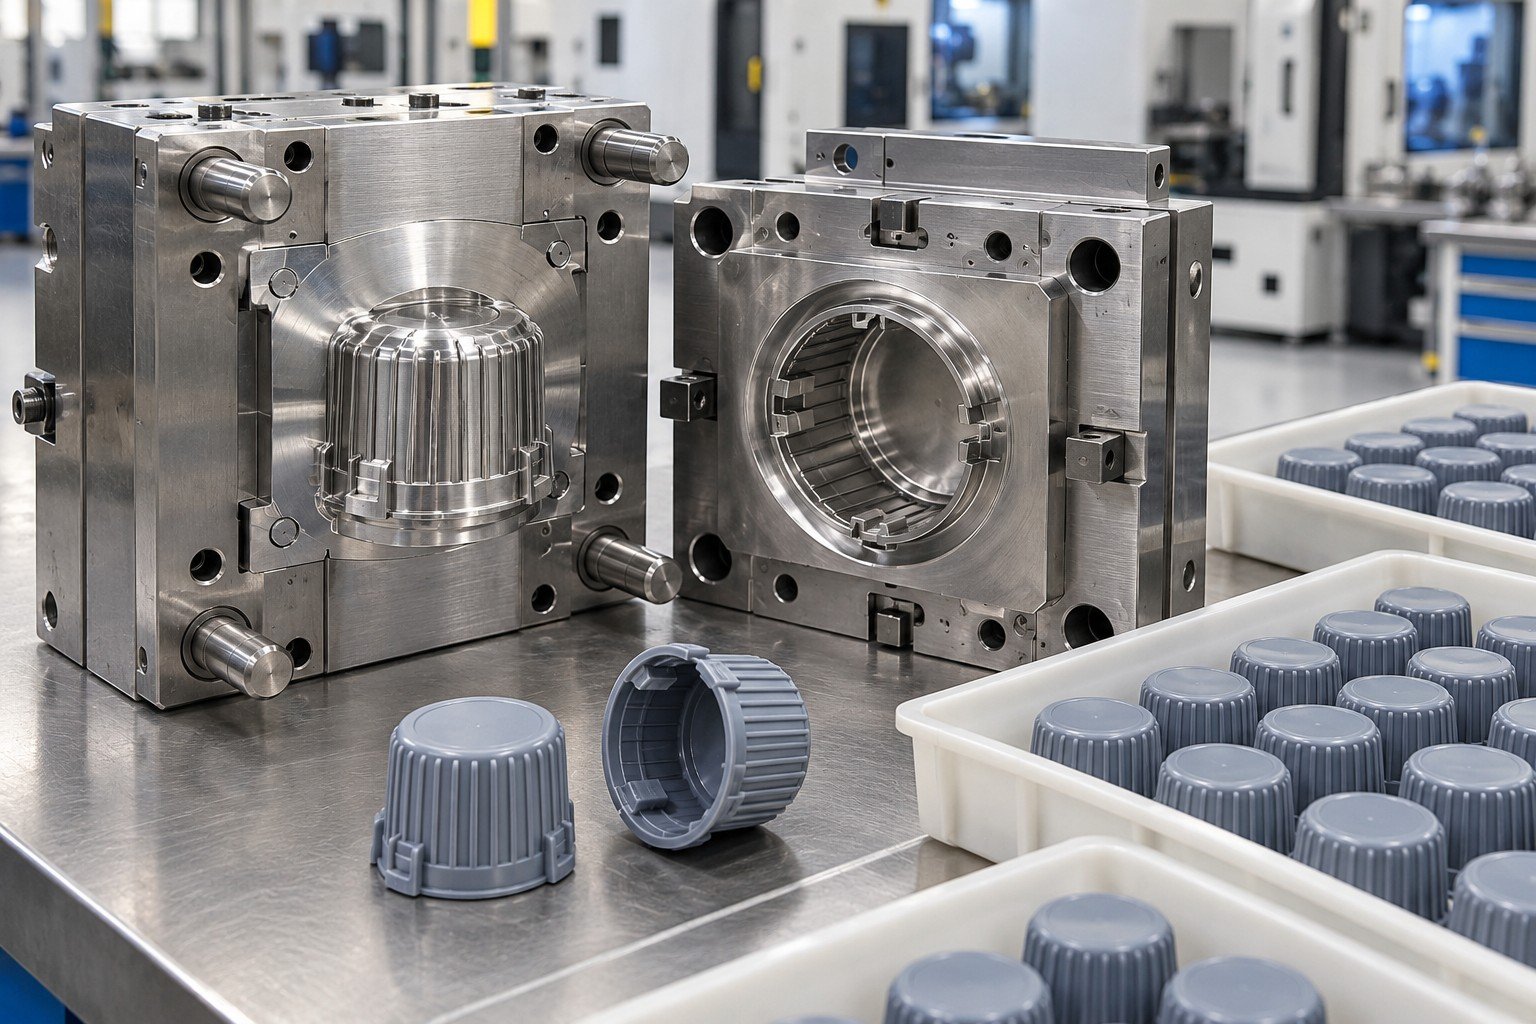
Interchangeable mold inserts can support selected geometry revisions when the holder, locating faces, clamping and ejection are designed for them.
| Your input | Stable envelope and features expected to change. |
|---|---|
| Your decision | Review which details can be replaced without rebuilding the entire tool. |
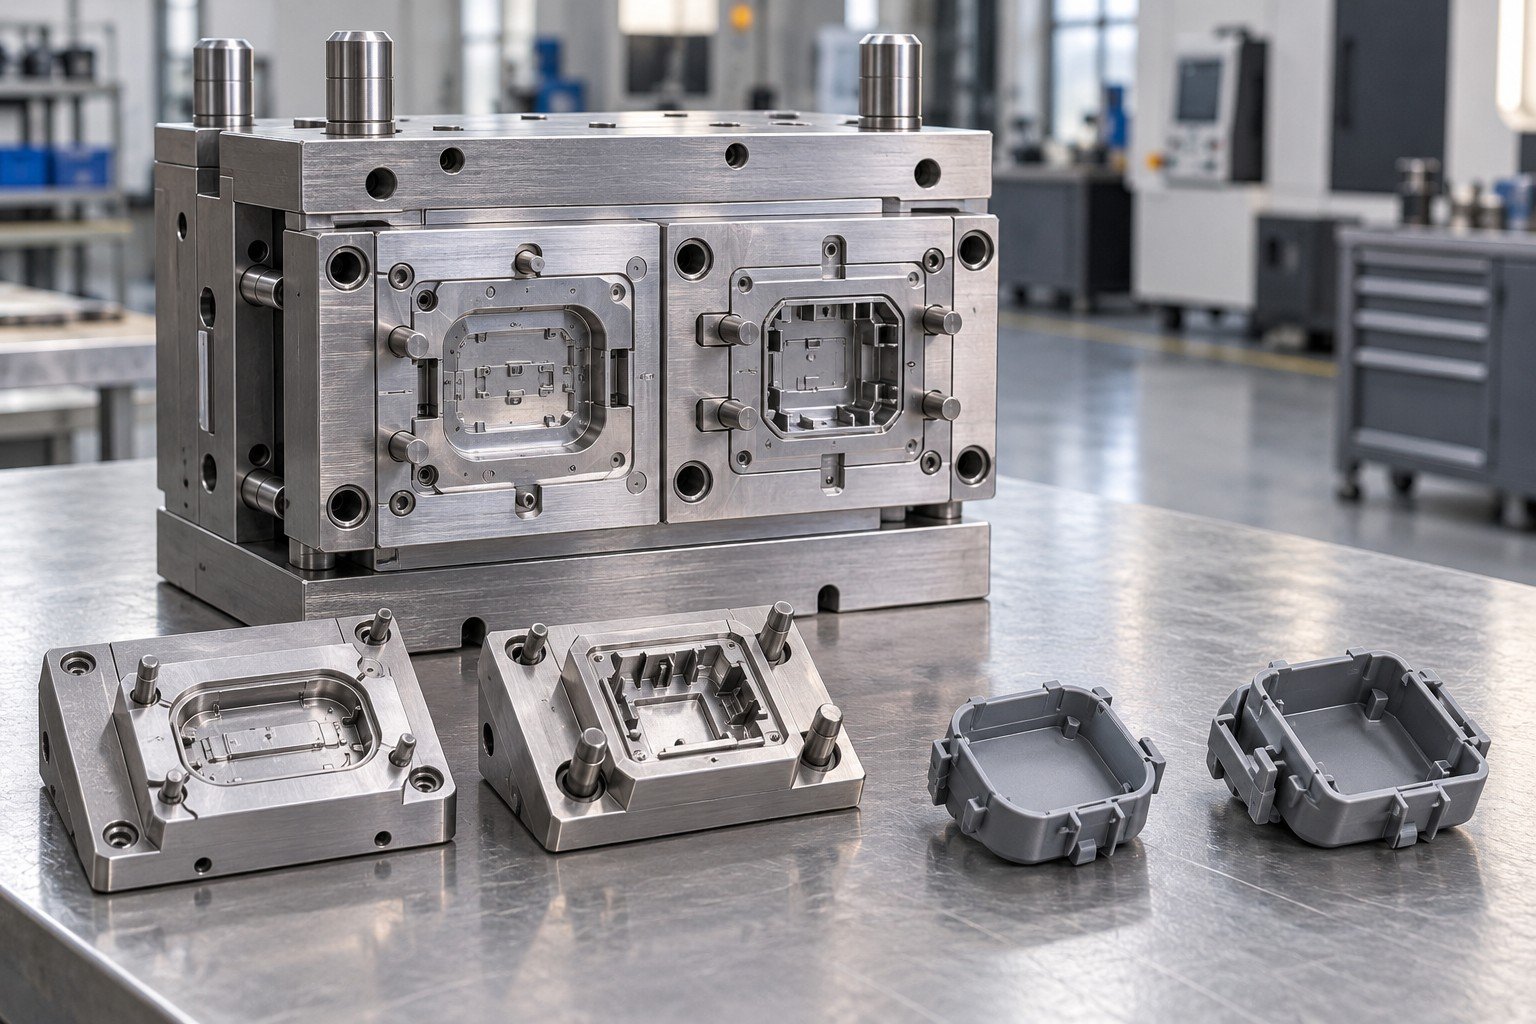
A single cavity prototype mold is one option, not a universal answer. Holder access, insert handling and the molding machine affect the choice.
| Your input | Part layout, resin, trial plan and available machine. |
|---|---|
| Your decision | Agree cavity count, insert interfaces and supplied components. |
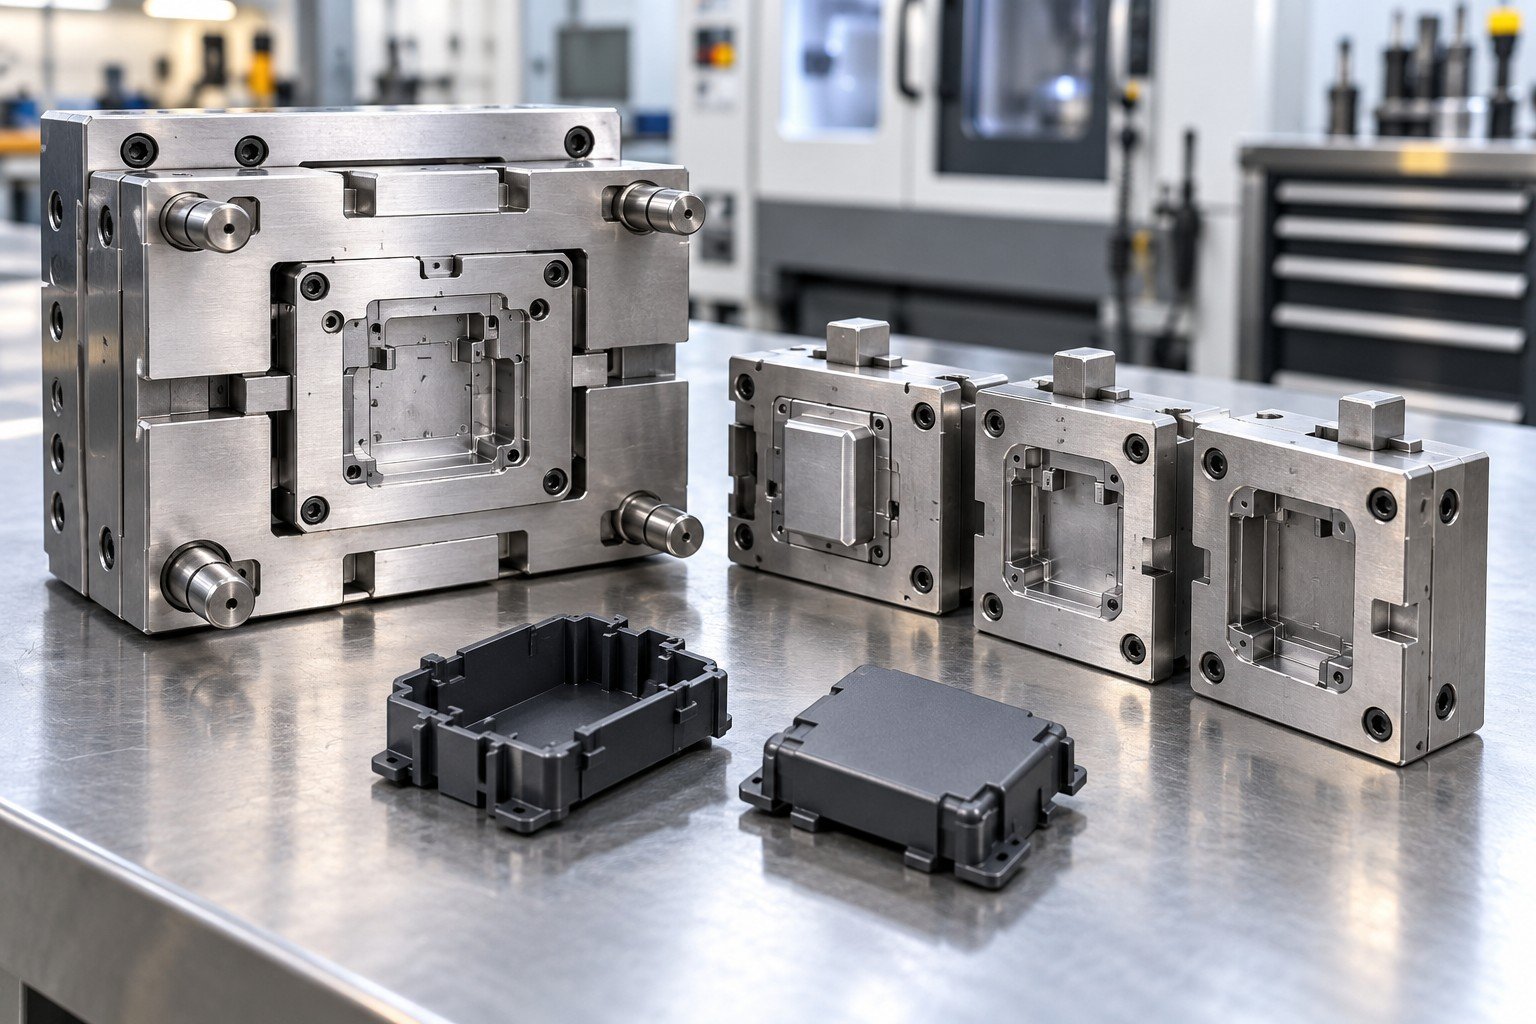
An insert that seats differently can change flash, alignment or local fit. Include locating and shutoff details in the review.
| Your input | Critical mating dimensions and insert seating requirements. |
|---|---|
| Your decision | Check alignment, contact and trial evidence after an insert change. |
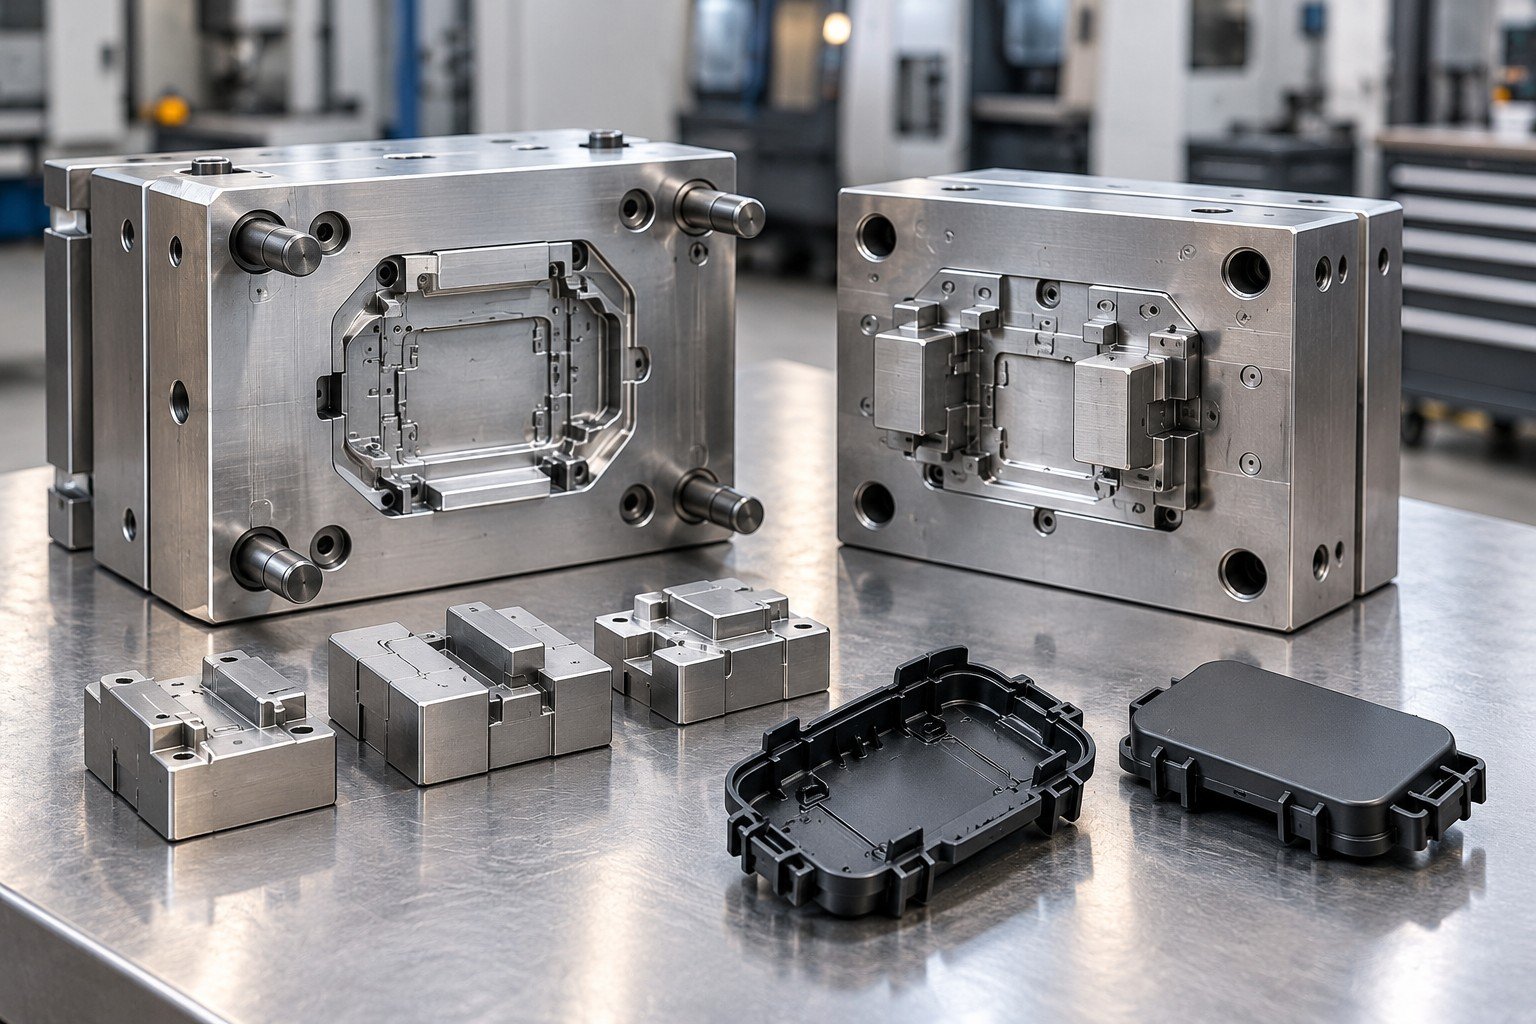
Keep part revision, insert identity and sample identity connected. A tray of similar samples is not a controlled comparison.
| Your input | Variant matrix and approved revision names. |
|---|---|
| Your decision | Separate samples and identify the insert and conditions used for each. |
Production-resin trials can answer questions a substitute material cannot. Exact grade, filler, shrinkage and processing conditions affect the mold review.
| Your input | Resin grade, datasheet, conditioning and intended service. |
|---|---|
| Your decision | Confirm material availability and trial suitability for your project. |
Prototype tooling for nylon parts needs a different review from an unfilled ABS enclosure. Filled or abrasive resins may change wear and material choices.
| Your input | Filler, moisture requirements, temperature and expected use. |
|---|---|
| Your decision | Review insert material, venting, ejection and maintenance. |
Conditioning and measurement timing matter when comparing fit. Do not compare one resin trial to another without recording the conditions.
| Your input | Critical features, conditioning and measurement method. |
|---|---|
| Your decision | Record resin, drying or conditioning and inspection basis. |
For bridge tooling for polypropylene, retain the approved grade and change-control process. Similar material names do not establish equivalence.
| Your input | Approved resin and permitted alternatives. |
|---|---|
| Your decision | Review substitutions before treating repeat parts as equivalent. |
Prototype mold design should start with the interfaces your assembly depends on: snaps, bosses, seals, clips and locating faces.
| Your input | Mating CAD, critical limits and assembly condition. |
|---|---|
| Your decision | Identify features needing direct sample checks. |
Parting, gates, draft and ejection can affect both function and appearance. Agree the acceptable locations before manufacturing the mold.
| Your input | Visible surfaces, gate restrictions and required texture. |
|---|---|
| Your decision | Review release strategy and cosmetic compromises explicitly. |
A loose part dimension does not establish assembled behavior. Use defined mating parts, orientation and acceptance conditions.
| Your input | Mating components and fit acceptance. |
|---|---|
| Your decision | Record assembly observations alongside dimensional evidence. |
Design revisions can change flow, cooling and mating fit together. Keep the trial correction list tied to the controlled model.
| Your input | Revised CAD and documented observations. |
|---|---|
| Your decision | Agree correction scope and recheck affected features. |
Prototype and bridge tooling should support decisions about the part and the interim route. Name the unresolved question before authorizing a change.
| Your input | Observed issue and the decision needed. |
|---|---|
| Your decision | Separate part-design changes from tool-process corrections. |
A small CAD change may require a replacement insert or affect other mold features. Define approval and cost responsibility before cutting.
| Your input | Revision comparison and requested change. |
|---|---|
| Your decision | Review insert reuse, machining access and retrial scope. |
Mold flow analysis for prototype tooling can inform gate, filling or cooling decisions when included in the project. It does not replace an actual trial.
| Your input | Model, resin data and analysis assumptions. |
|---|---|
| Your decision | Confirm simulation scope and then check the molded result. |
A corrected feature may influence adjacent dimensions, appearance or ejection. Agree what needs to be measured again.
| Your input | Approved correction and affected features. |
|---|---|
| Your decision | Retain trial records and confirm acceptance before repeat work. |
Prototype tooling transfer requires more than a shipping address. Confirm holder, inserts, spares, drawings and sample records included in release.
| Your input | Tool inventory and receiving machine. |
|---|---|
| Your decision | Review condition, compatibility and handover responsibilities. |
Tool payment alone should not be used to assume every drawing, holder or design right transfers. Record the agreed scope in the order.
| Your input | Ownership, use, storage and release requirements. |
|---|---|
| Your decision | Separate customer-owned items and any shared holder arrangements. |
A mold that ran on one machine may need a compatibility review or trial on another. Include ejector, clamping and utility interfaces.
| Your input | Receiving-machine data and current tool condition. |
|---|---|
| Your decision | Agree inspection, repairs, transport protection and receiving trial. |
Prototype tooling vs production tooling is a scope decision. Do not assume an interim tool can be upgraded for unlimited production.
| Your input | Updated demand, resin and accepted part requirements. |
|---|---|
| Your decision | Compare continued use, refurbishment and a new production mold. |
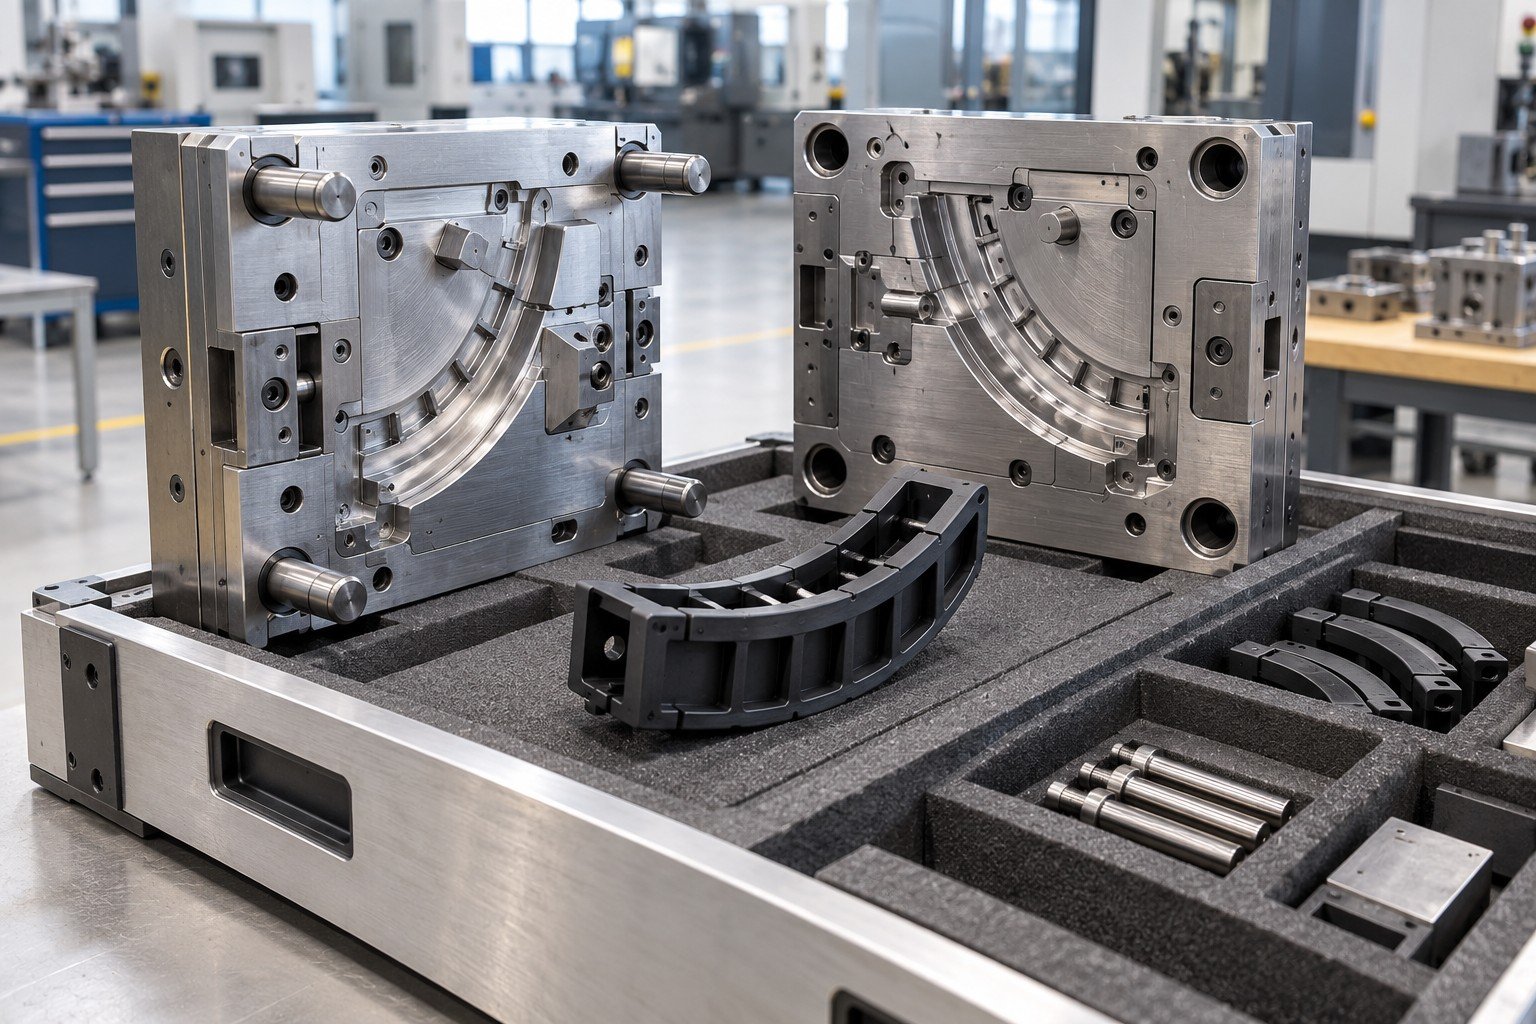
Keep every design topic available in a compact review rather than stretching a short panel.
Review ribs, wall transitions, draft and critical mating details together.
| Your input | Part CAD, exact resin and critical requirements. |
|---|---|
| Our review | Tool concept, trial method and project-specific risks. |
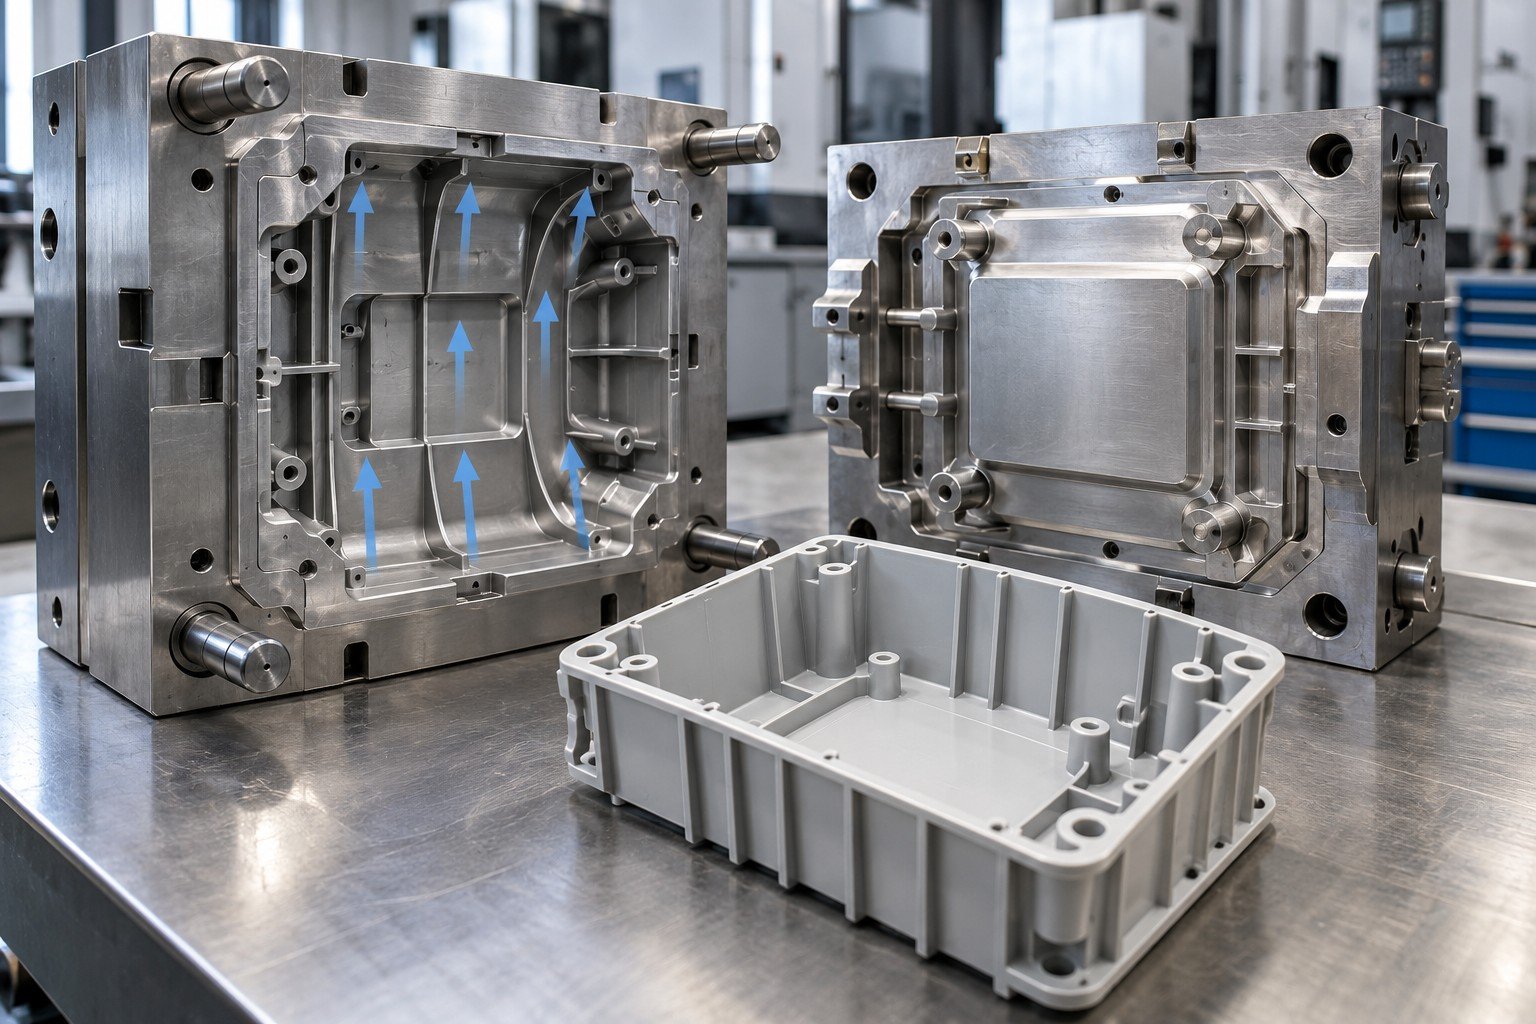
Review flash-sensitive edges, shutoffs and visible surfaces.
| Your input | Part CAD, exact resin and critical requirements. |
|---|---|
| Our review | Tool concept, trial method and project-specific risks. |
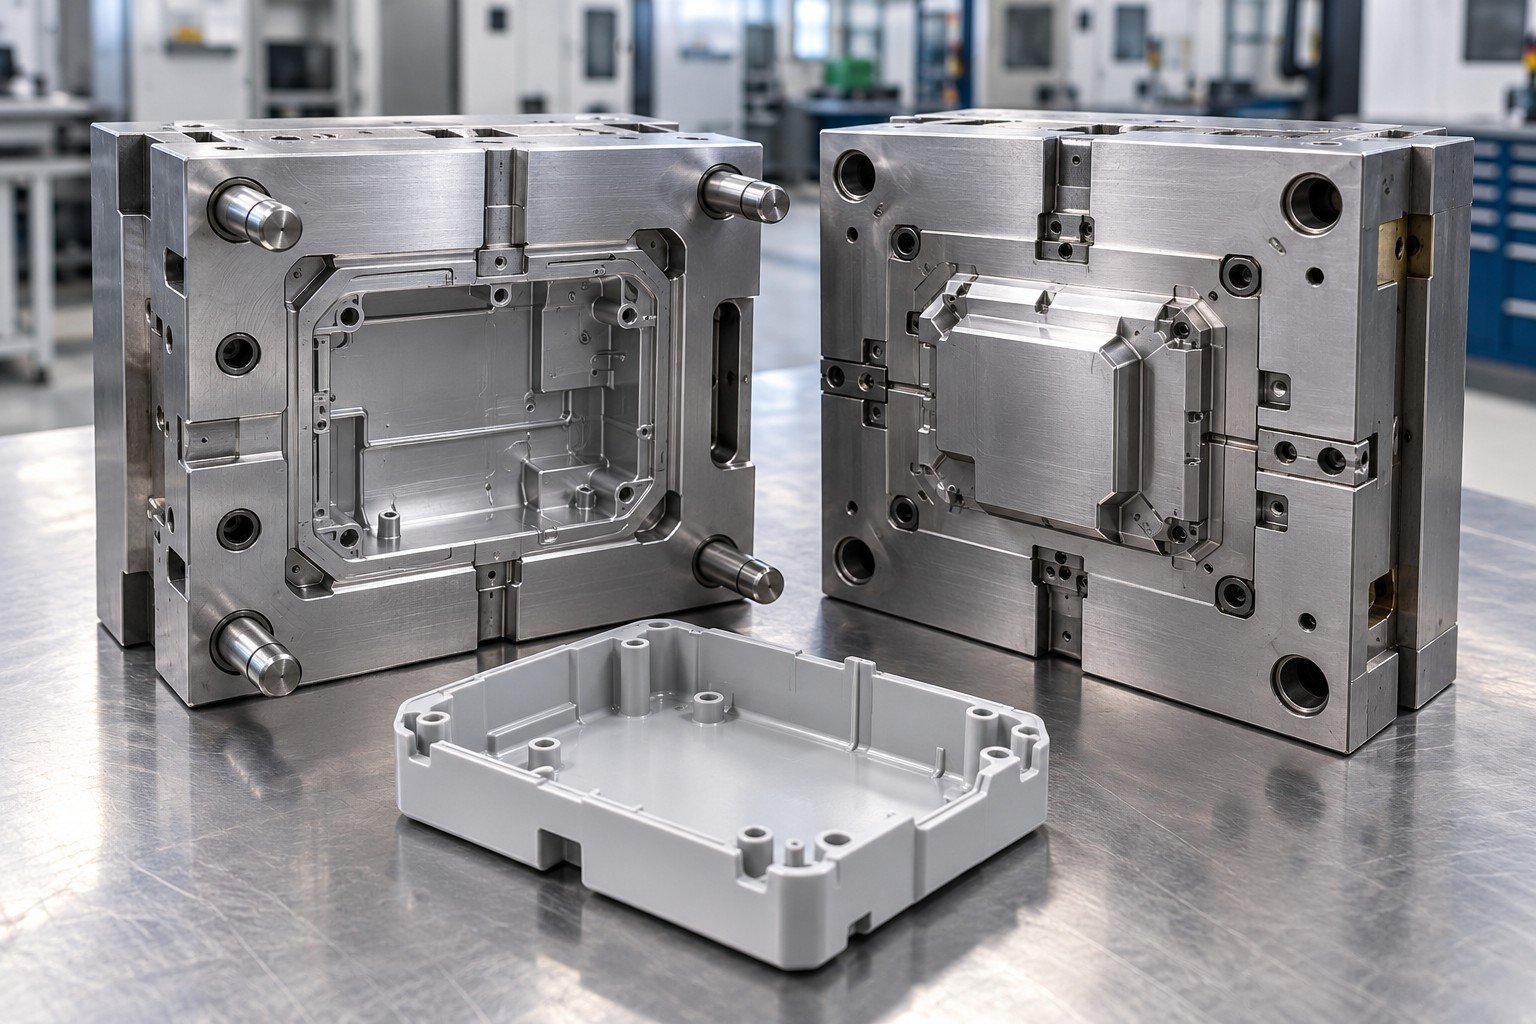
Review gate access, runner concept and any cosmetic restriction.
| Your input | Part CAD, exact resin and critical requirements. |
|---|---|
| Our review | Tool concept, trial method and project-specific risks. |
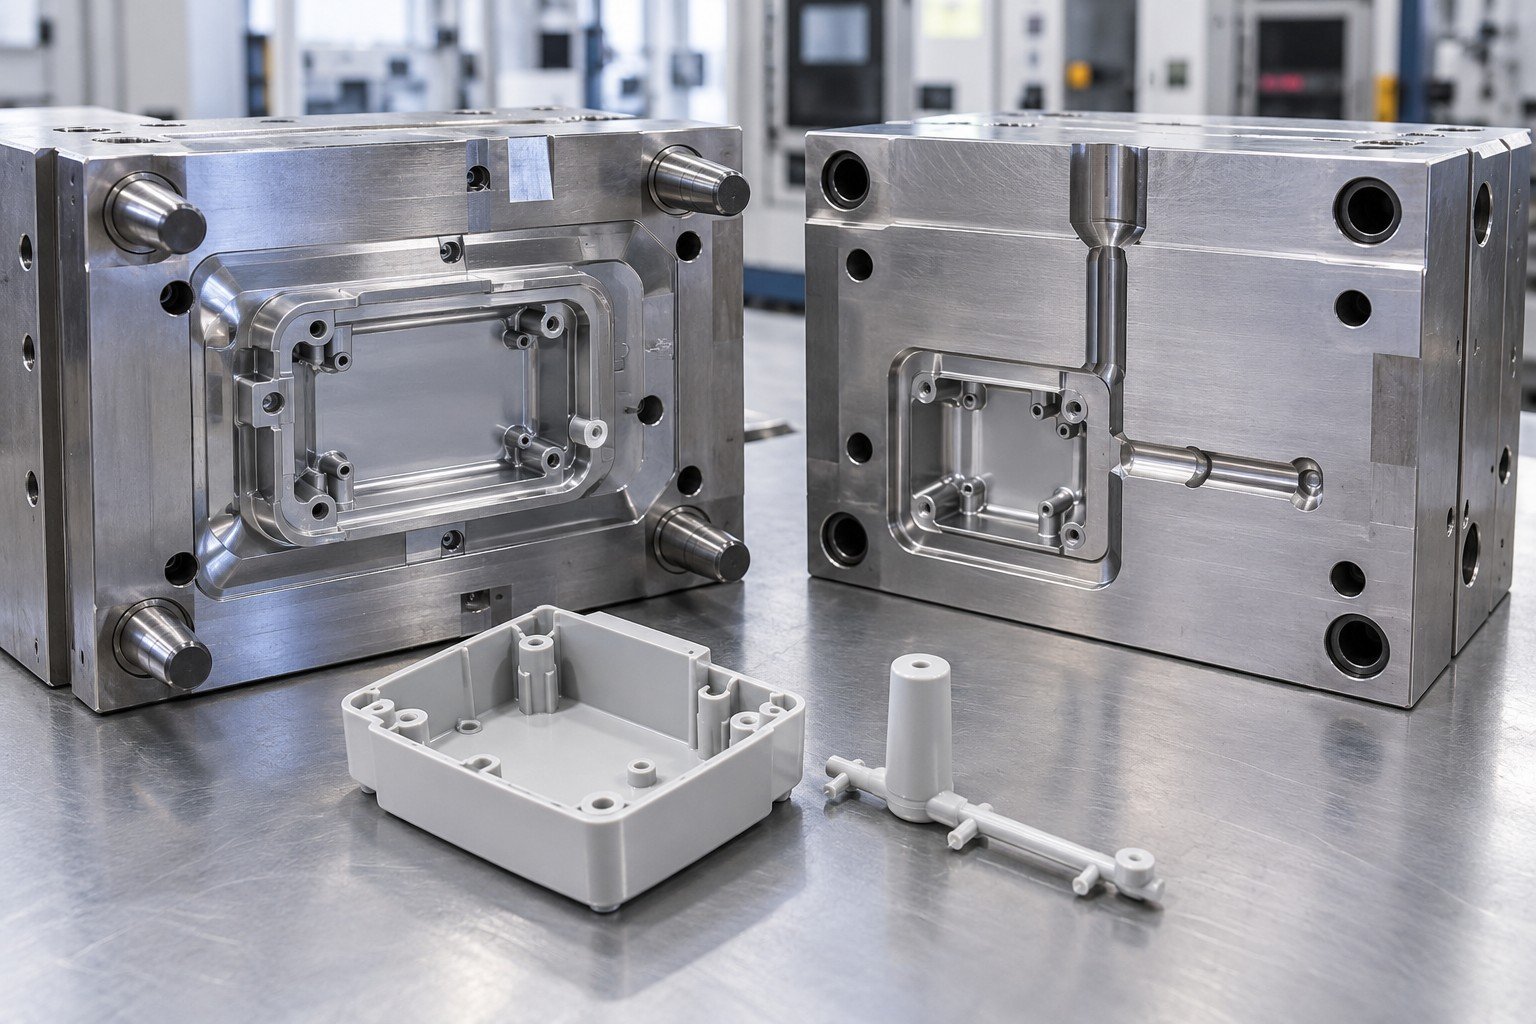
Consider resin, cooling access and measurement conditions together.
| Your input | Part CAD, exact resin and critical requirements. |
|---|---|
| Our review | Tool concept, trial method and project-specific risks. |
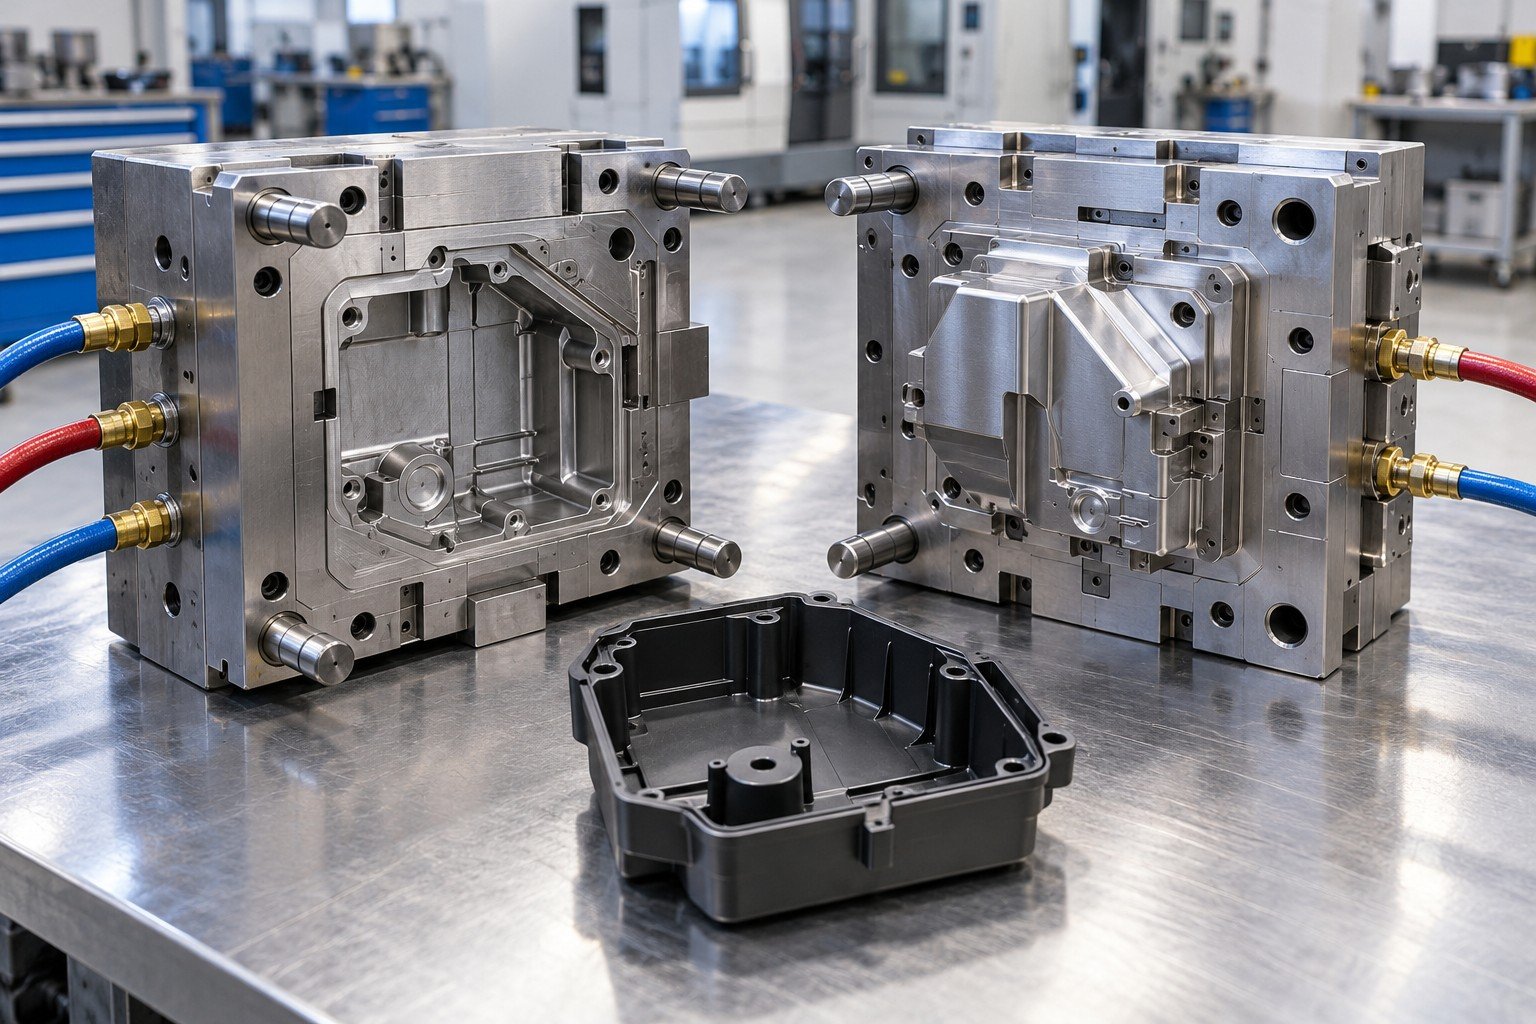
Review contact marks, support and the risk of distortion during ejection.
| Your input | Part CAD, exact resin and critical requirements. |
|---|---|
| Our review | Tool concept, trial method and project-specific risks. |
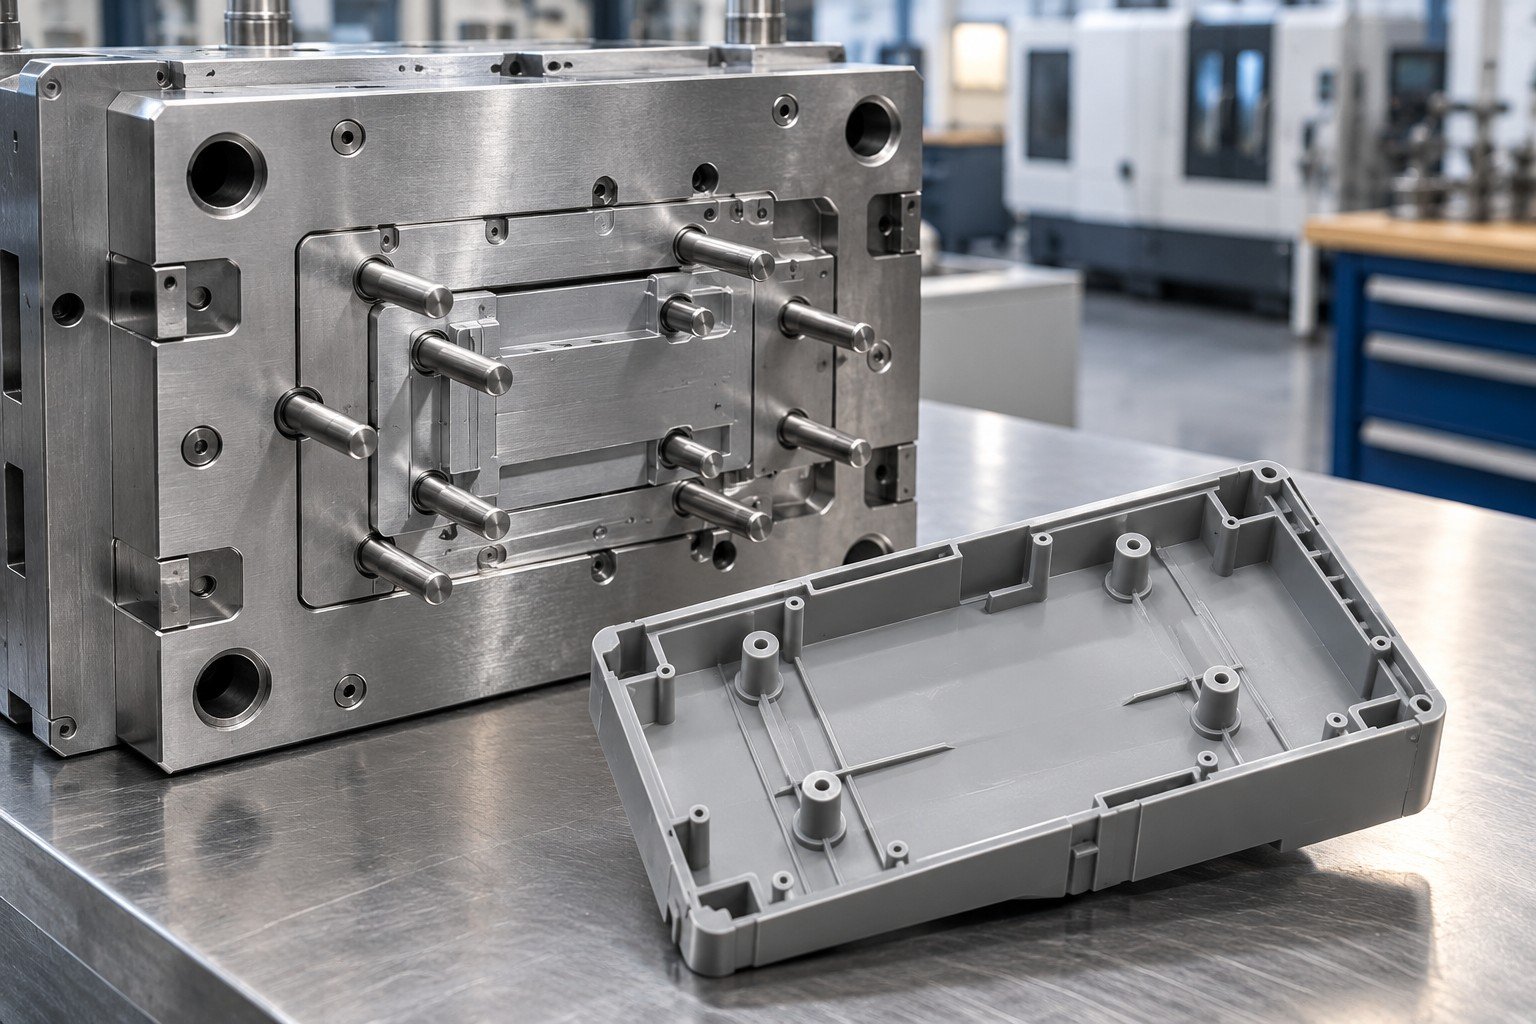
Use controlled mating parts and an agreed assembly condition.
| Your input | Part CAD, exact resin and critical requirements. |
|---|---|
| Our review | Tool concept, trial method and project-specific risks. |
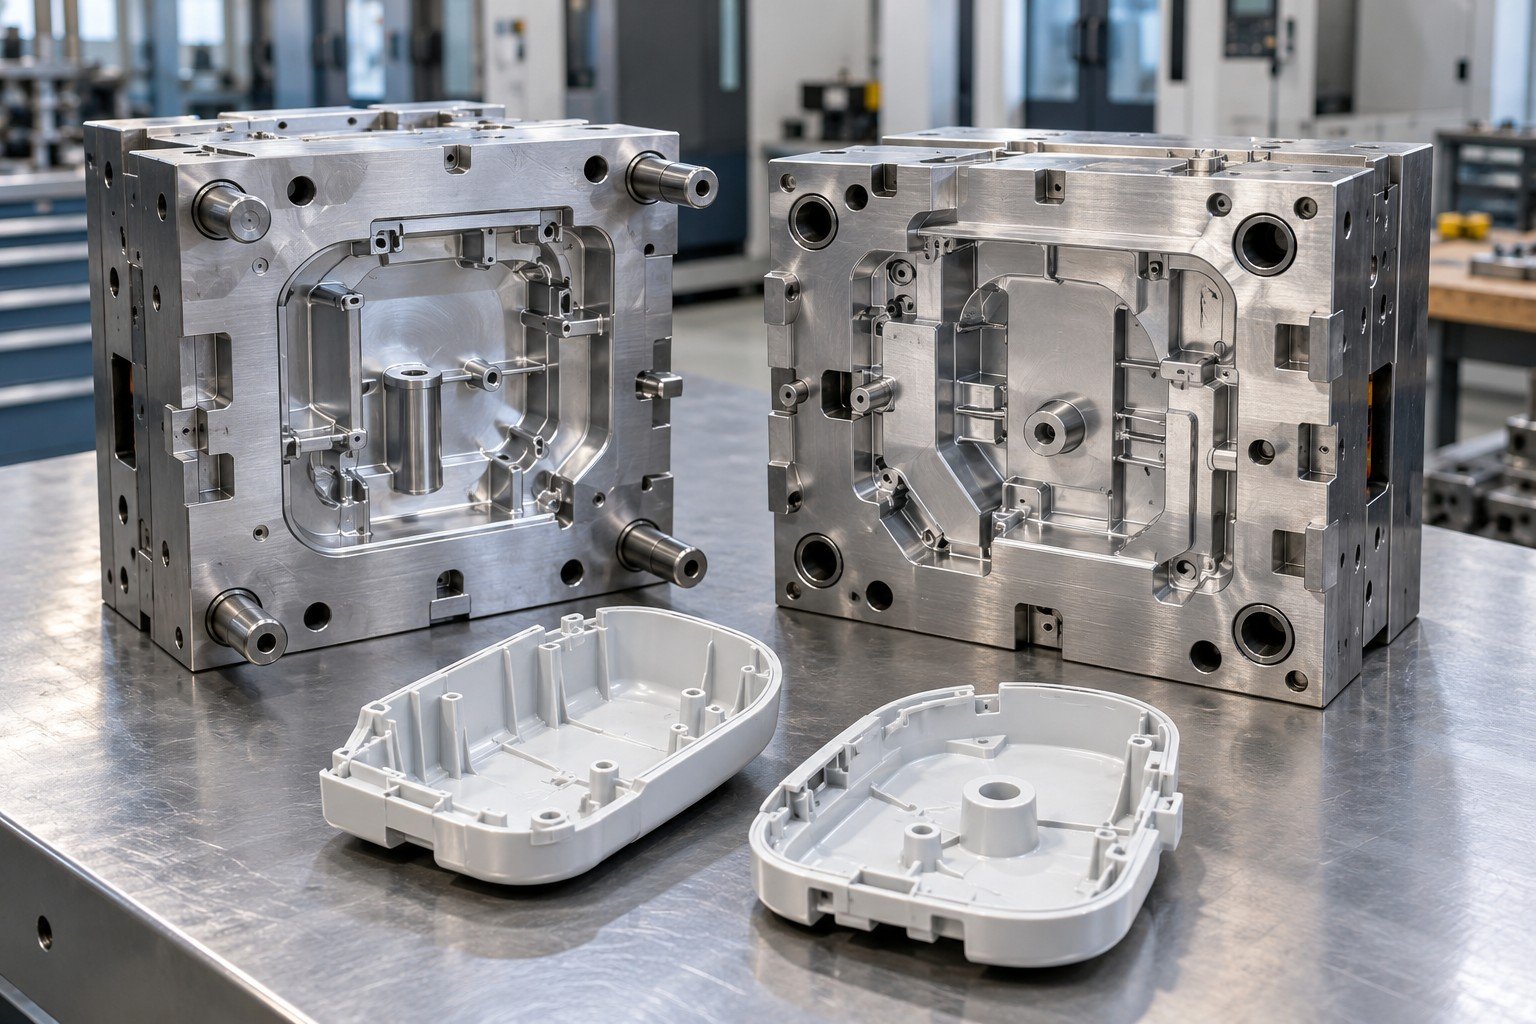
Agree gate marks, parting lines, texture and an acceptable reference.
| Your input | Part CAD, exact resin and critical requirements. |
|---|---|
| Our review | Tool concept, trial method and project-specific risks. |
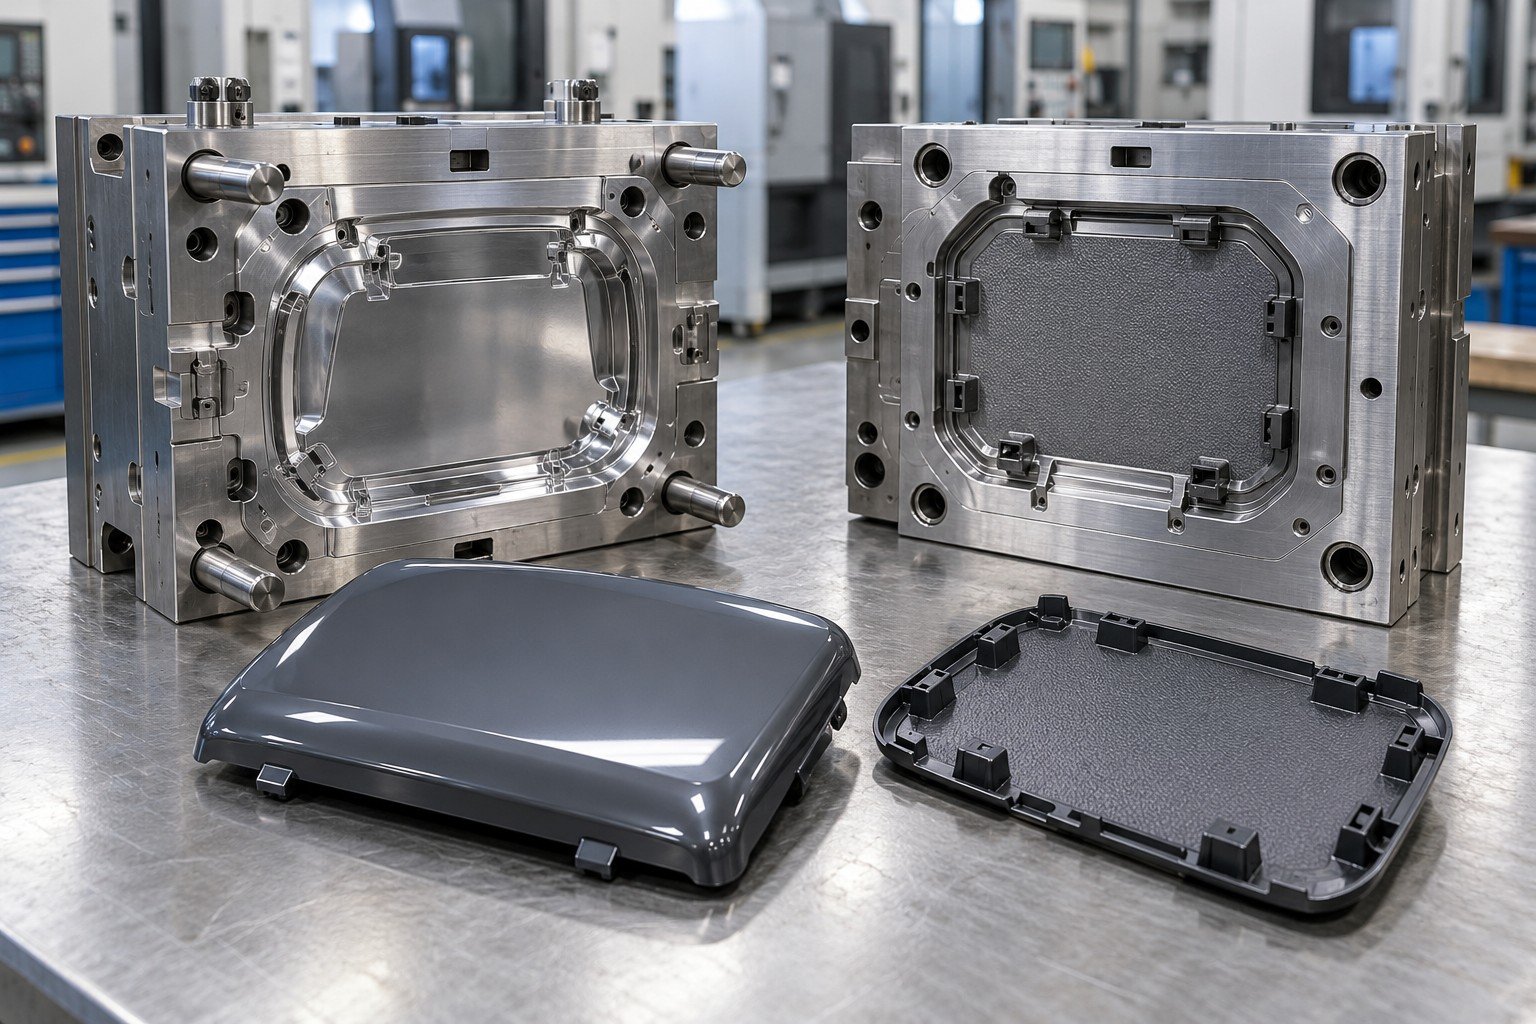
Review clamping, locating ring, ejection, utilities and handling.
| Your input | Part CAD, exact resin and critical requirements. |
|---|---|
| Our review | Tool concept, trial method and project-specific risks. |
T1 is the first trial, not automatic final acceptance.
State the design question, part revision and trial demand.
| Your input | Controlled drawings, resin and project-specific acceptance. |
|---|---|
| Your record | Decision owner, revision and agreed next action. |
Review exact resin, inserts, holder and expected use.
| Your input | Controlled drawings, resin and project-specific acceptance. |
|---|---|
| Your record | Decision owner, revision and agreed next action. |
Agree parting, gates, release, cooling and machine interfaces.
| Your input | Controlled drawings, resin and project-specific acceptance. |
|---|---|
| Your record | Decision owner, revision and agreed next action. |
Record actual material, setup, samples and visible issues.
| Your input | Controlled drawings, resin and project-specific acceptance. |
|---|---|
| Your record | Decision owner, revision and agreed next action. |
Approve corrections and check the affected part features.
| Your input | Controlled drawings, resin and project-specific acceptance. |
|---|---|
| Your record | Decision owner, revision and agreed next action. |
Release interim supply or hand over the agreed tool inventory.
| Your input | Controlled drawings, resin and project-specific acceptance. |
|---|---|
| Your record | Decision owner, revision and agreed next action. |
Tool material and part resin are different specifications. Availability and construction are confirmed for your drawing.
Review grade, geometry, resin and expected use together; aluminum is not a universal shortcut.
Prototype molds may use steel when the part, resin or trial scope warrants it.
Specify grade and condition when considering P20; do not infer tool life from a material name.
Review this grade only against the actual insert design and processing conditions.
Define the actual mold material and construction. These shorthand terms alone do not establish capability.
Review replaceable gates, ejectors and inserts where resin or geometry makes wear relevant.
Rapid aluminum tooling and steel construction both require a project-specific review. No fixed mold-life or cycle-count guarantee is implied by these examples.
Approve the evidence required for your project before treating samples as released.
Control part CAD, tool concept, resin and revision before machining.
| Drawing & Revision | Controlled part and tool baseline. |
|---|---|
| Resin & Condition | Grade, filler and conditioning recorded. |
| Critical Features | Agreed dimensions, datums and method. |
| Appearance & Fit | Reference and actual mating condition. |
| Corrections | Authorized changes and repeat checks. |
| Release Records | Sample identity, approval and exceptions. |
Record the actual grade, process conditions and sample identities.
| Drawing & Revision | Controlled part and tool baseline. |
|---|---|
| Resin & Condition | Grade, filler and conditioning recorded. |
| Critical Features | Agreed dimensions, datums and method. |
| Appearance & Fit | Reference and actual mating condition. |
| Corrections | Authorized changes and repeat checks. |
| Release Records | Sample identity, approval and exceptions. |
Agree method, limits, conditioning, sampling and any required mating checks.
| Drawing & Revision | Controlled part and tool baseline. |
|---|---|
| Resin & Condition | Grade, filler and conditioning recorded. |
| Critical Features | Agreed dimensions, datums and method. |
| Appearance & Fit | Reference and actual mating condition. |
| Corrections | Authorized changes and repeat checks. |
| Release Records | Sample identity, approval and exceptions. |
Identify tool components, spares, records, ownership and receiving conditions.
| Drawing & Revision | Controlled part and tool baseline. |
|---|---|
| Resin & Condition | Grade, filler and conditioning recorded. |
| Critical Features | Agreed dimensions, datums and method. |
| Appearance & Fit | Reference and actual mating condition. |
| Corrections | Authorized changes and repeat checks. |
| Release Records | Sample identity, approval and exceptions. |
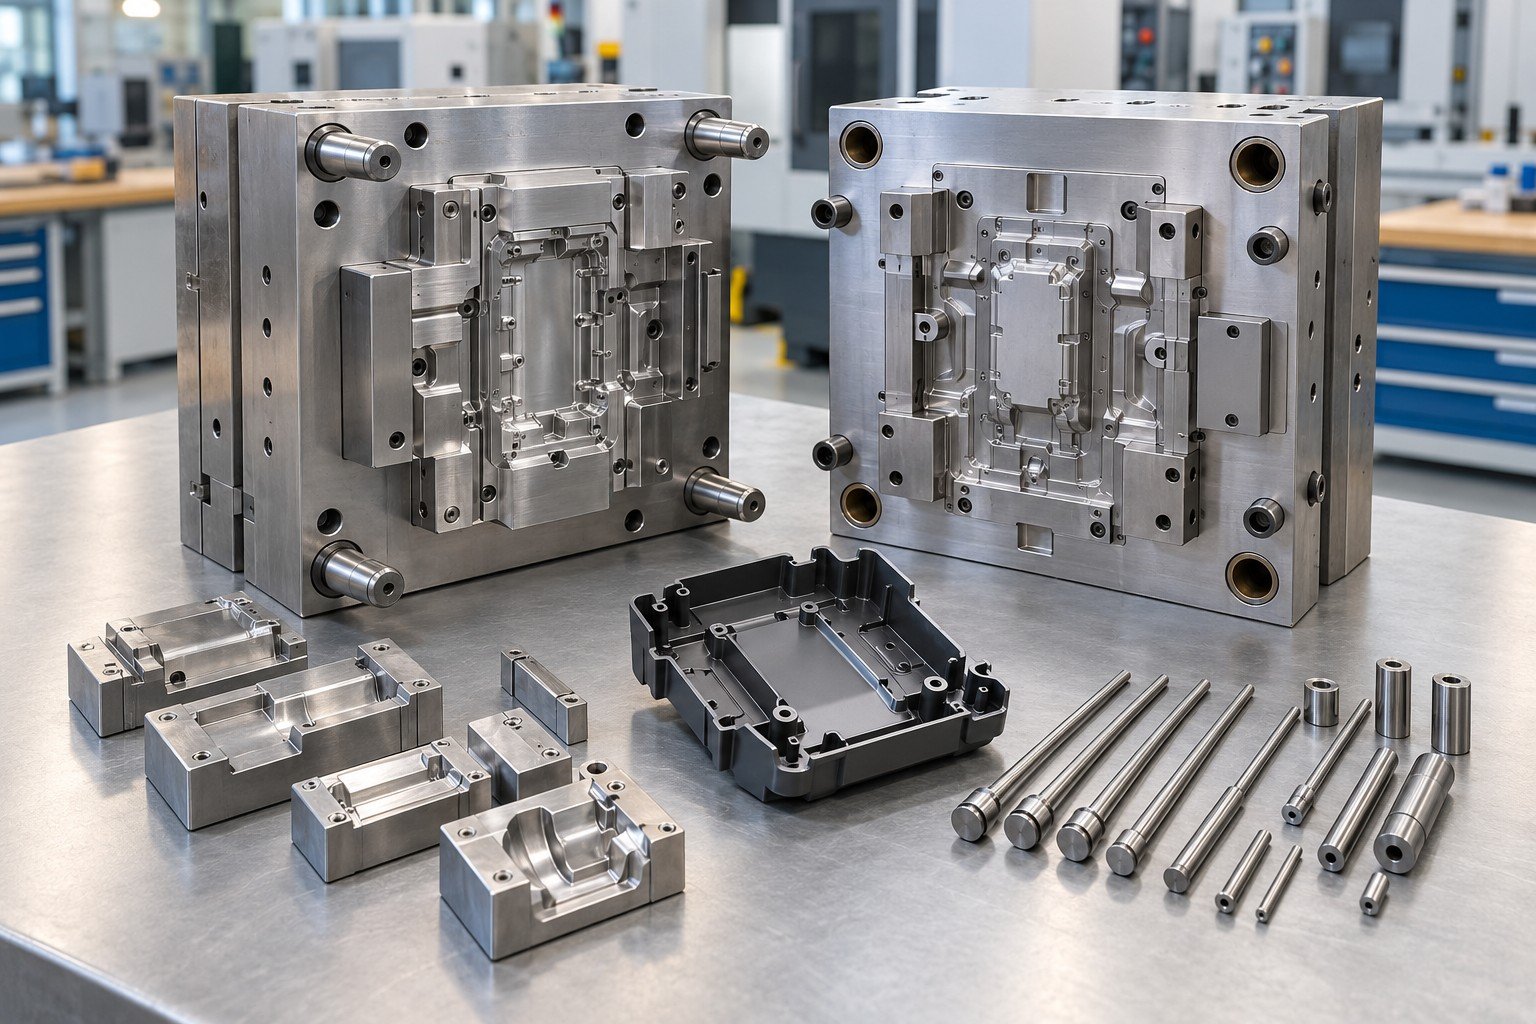
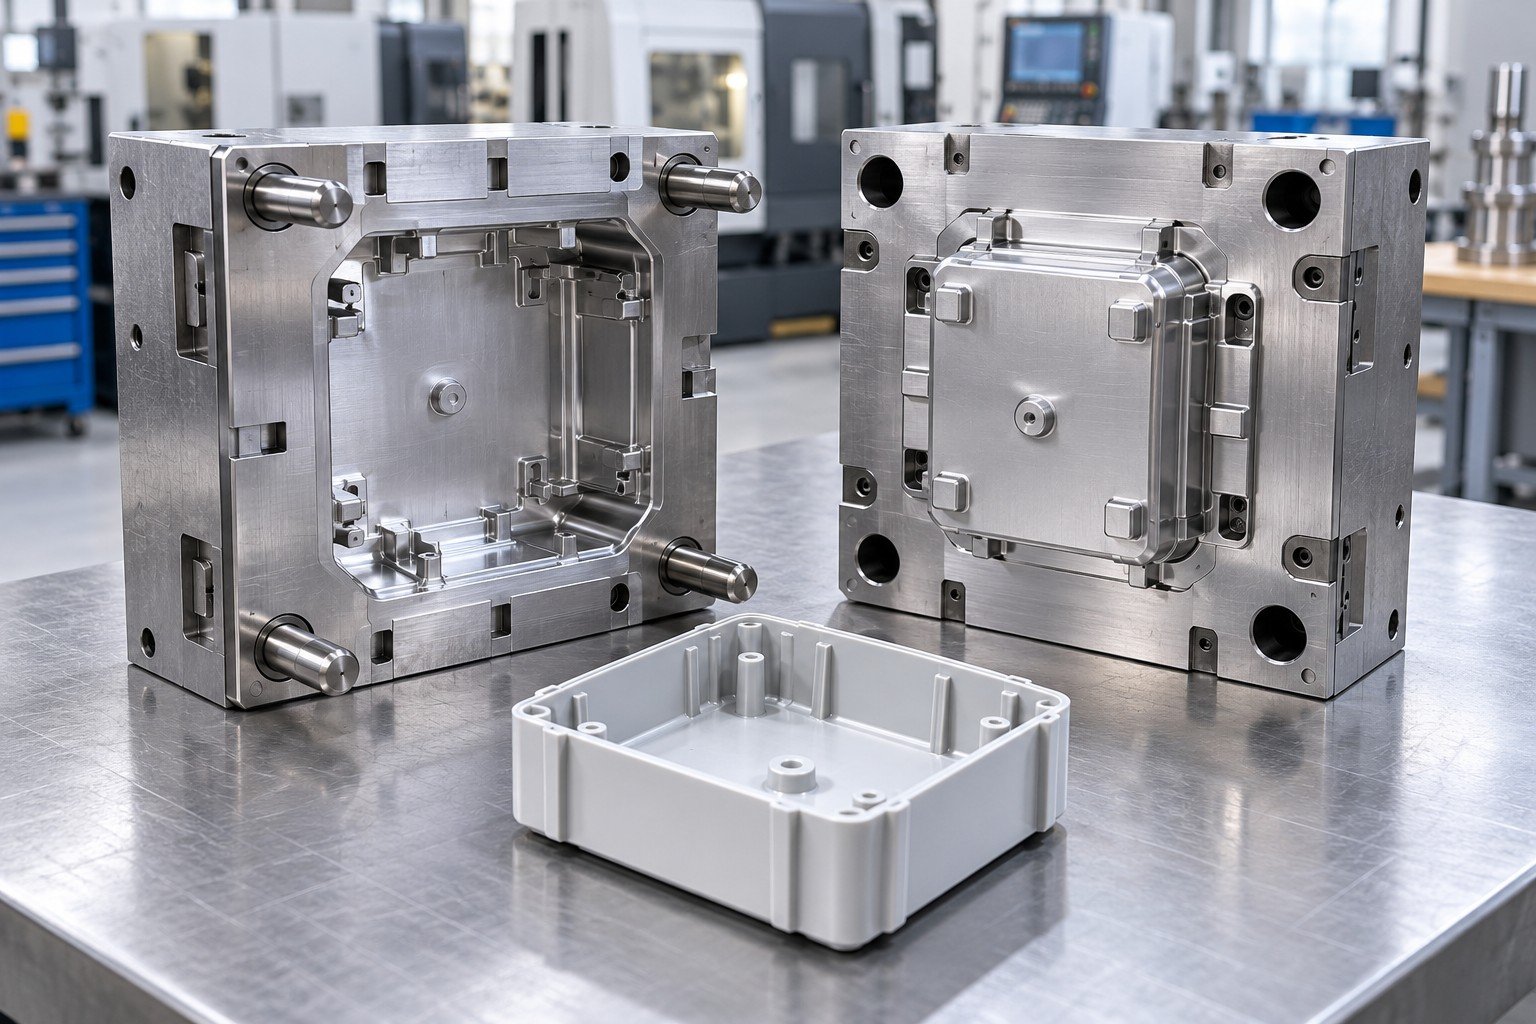
Control geometry, resin, open questions and acceptance.
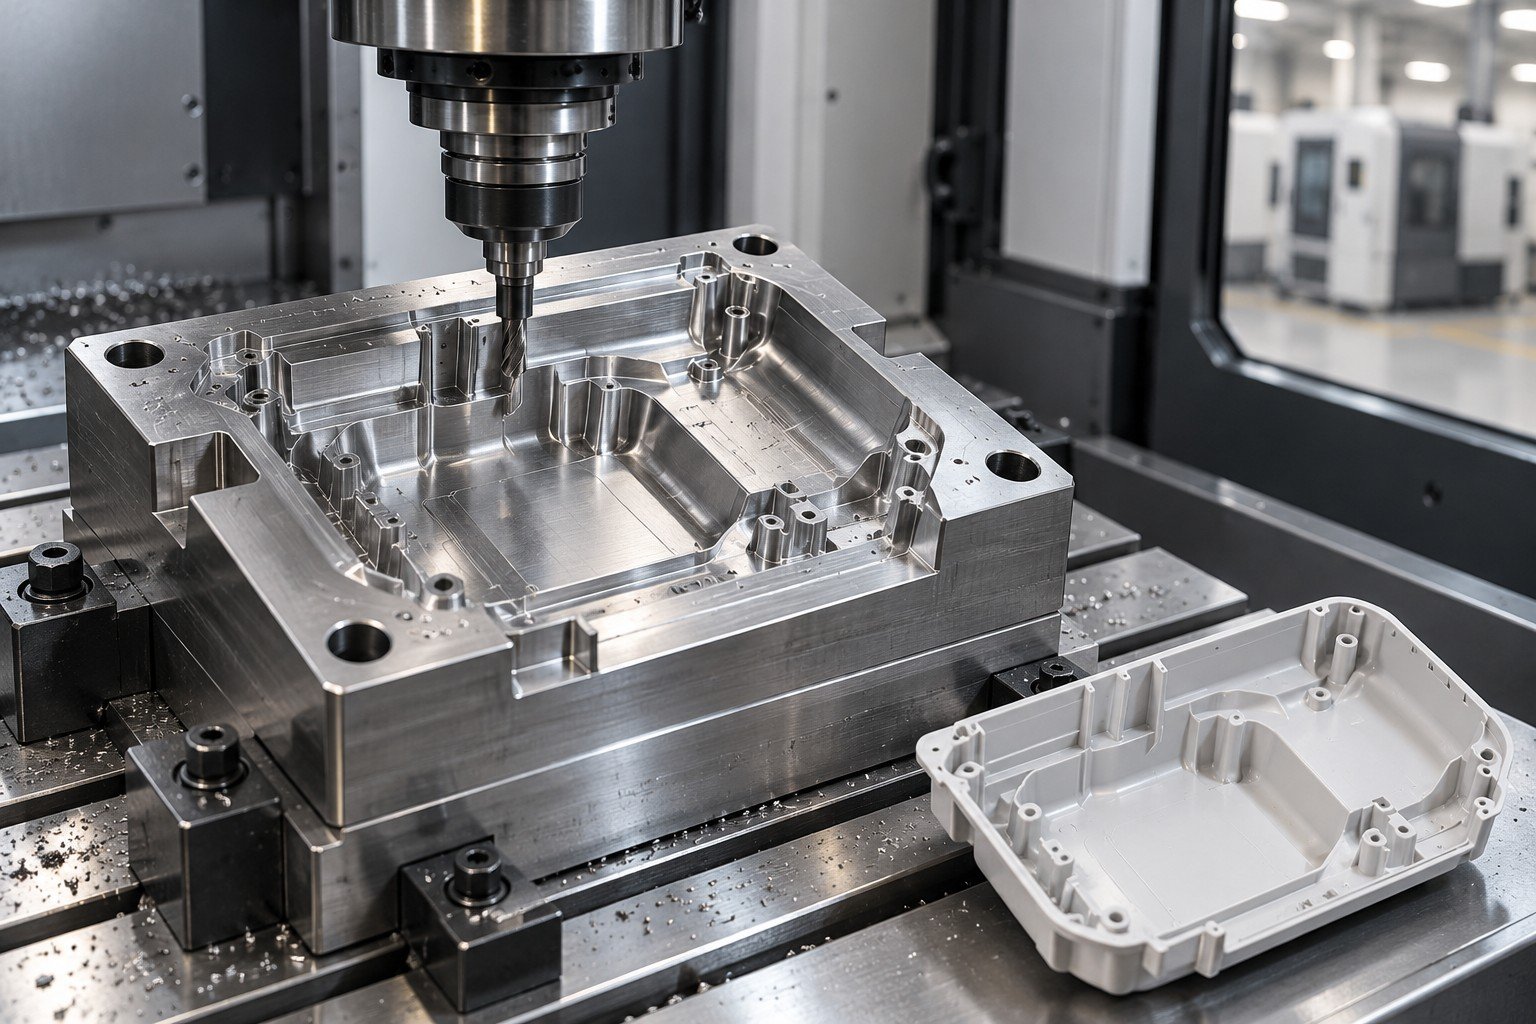
Make the agreed tool, holder and replaceable details.
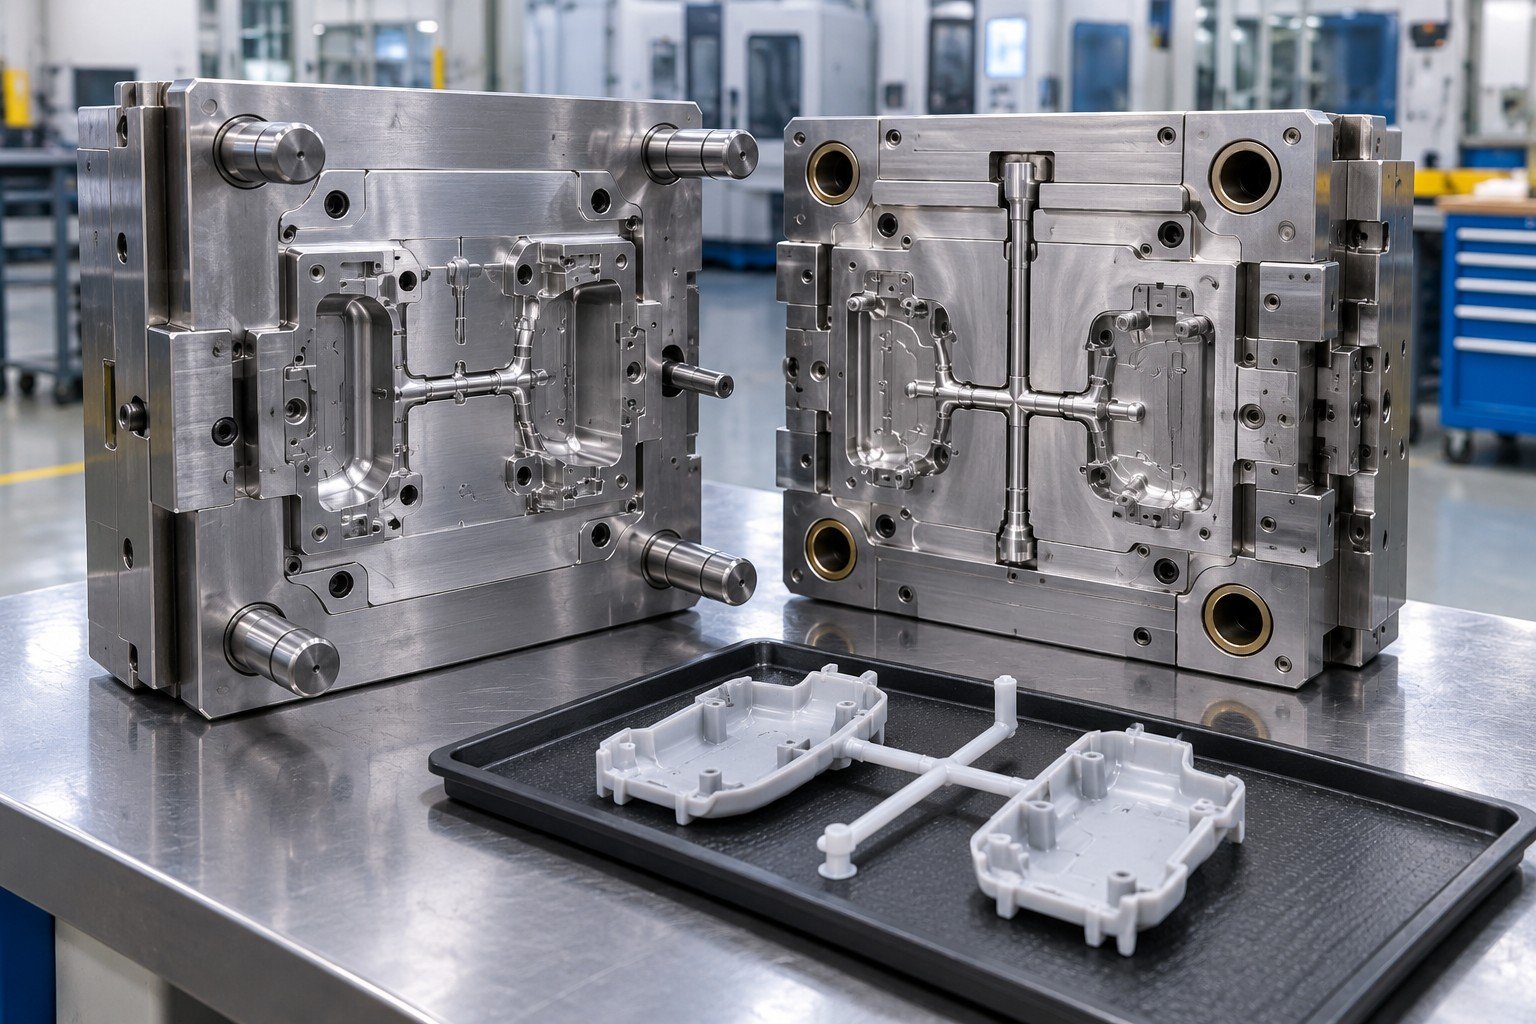
Mold, measure, review and record corrections.
Approve interim use or the agreed handoff inventory.
A cavity price alone does not describe the complete trial or interim-supply project.
Separate design, holder, inserts and supplied tool components.
Name trials, sample quantities, changes and inspection records.
Distinguish molding orders, maintenance, storage and transport.
Ownership, use and release
Changes and retrial responsibility
Maintenance and expected-use review
Storage, transfer and receiving trial
For a prototype tooling quote, request a milestone plan for design approval, build, first trial, correction and acceptance. Prototype mold lead time depends on the actual scope, material availability and decisions still open.
ILLUSTRATIVE SAMPLE-PLAN MATH — NOT MOQ OR A PRICE
An arithmetic planning example only. Trial quantities, repeat demand, spare samples and process allowances are agreed for your project. Bridge tooling cost also depends on the intended supply period and maintenance scope.
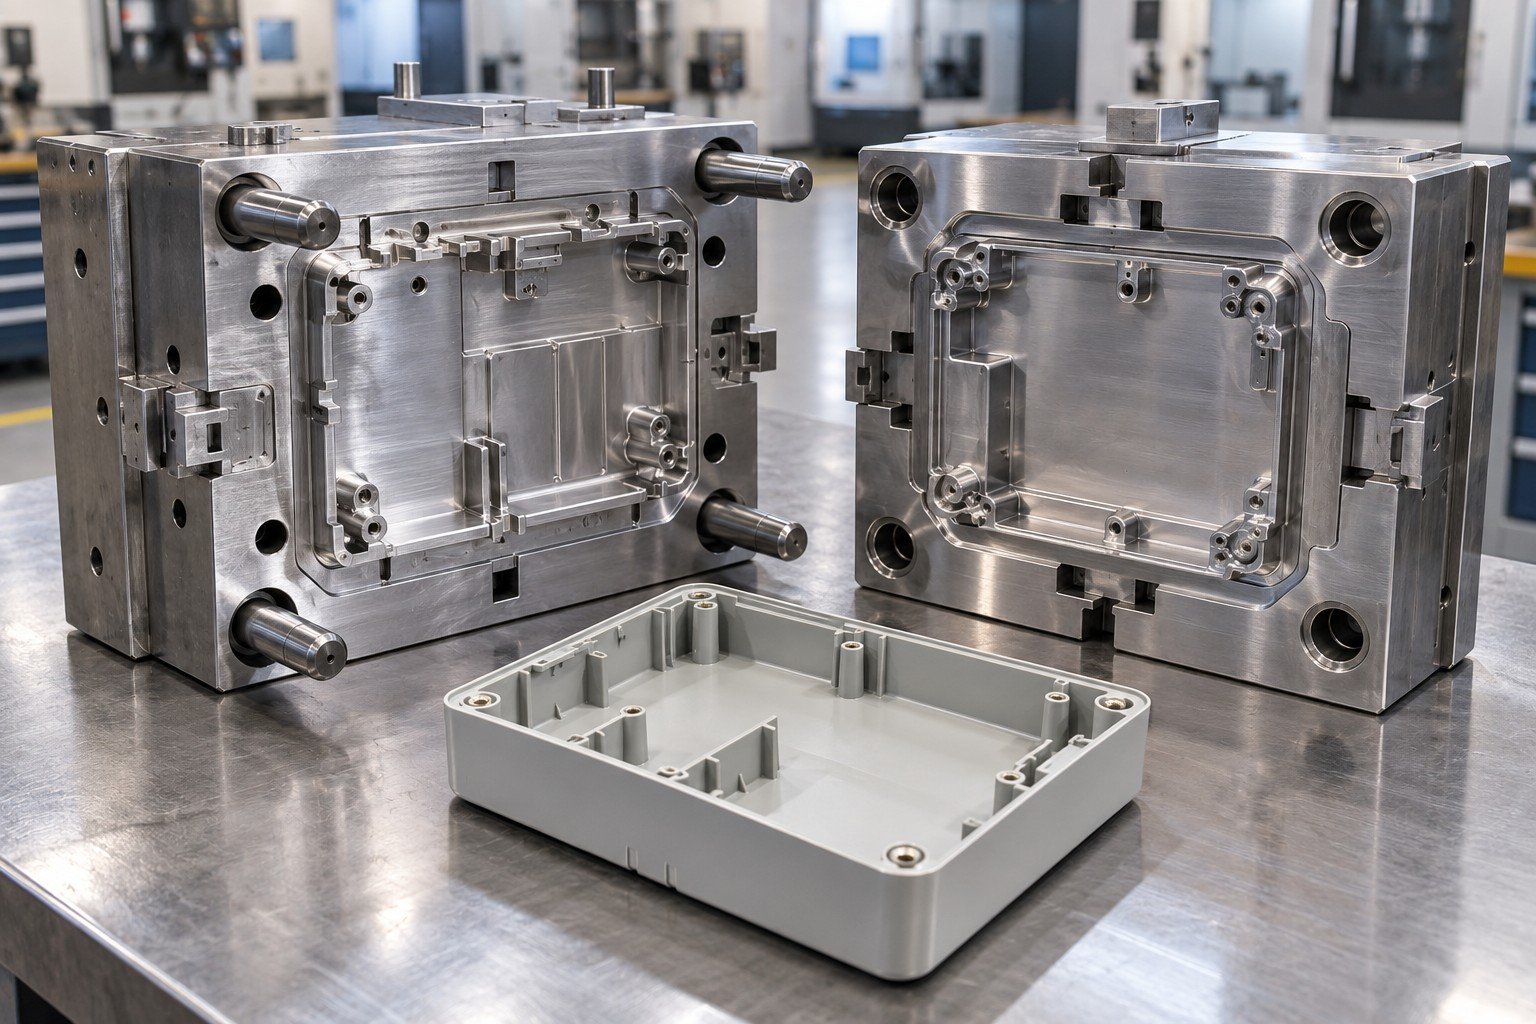
Prototype tooling for ABS parts can focus on cover fit, bosses and visible faces.
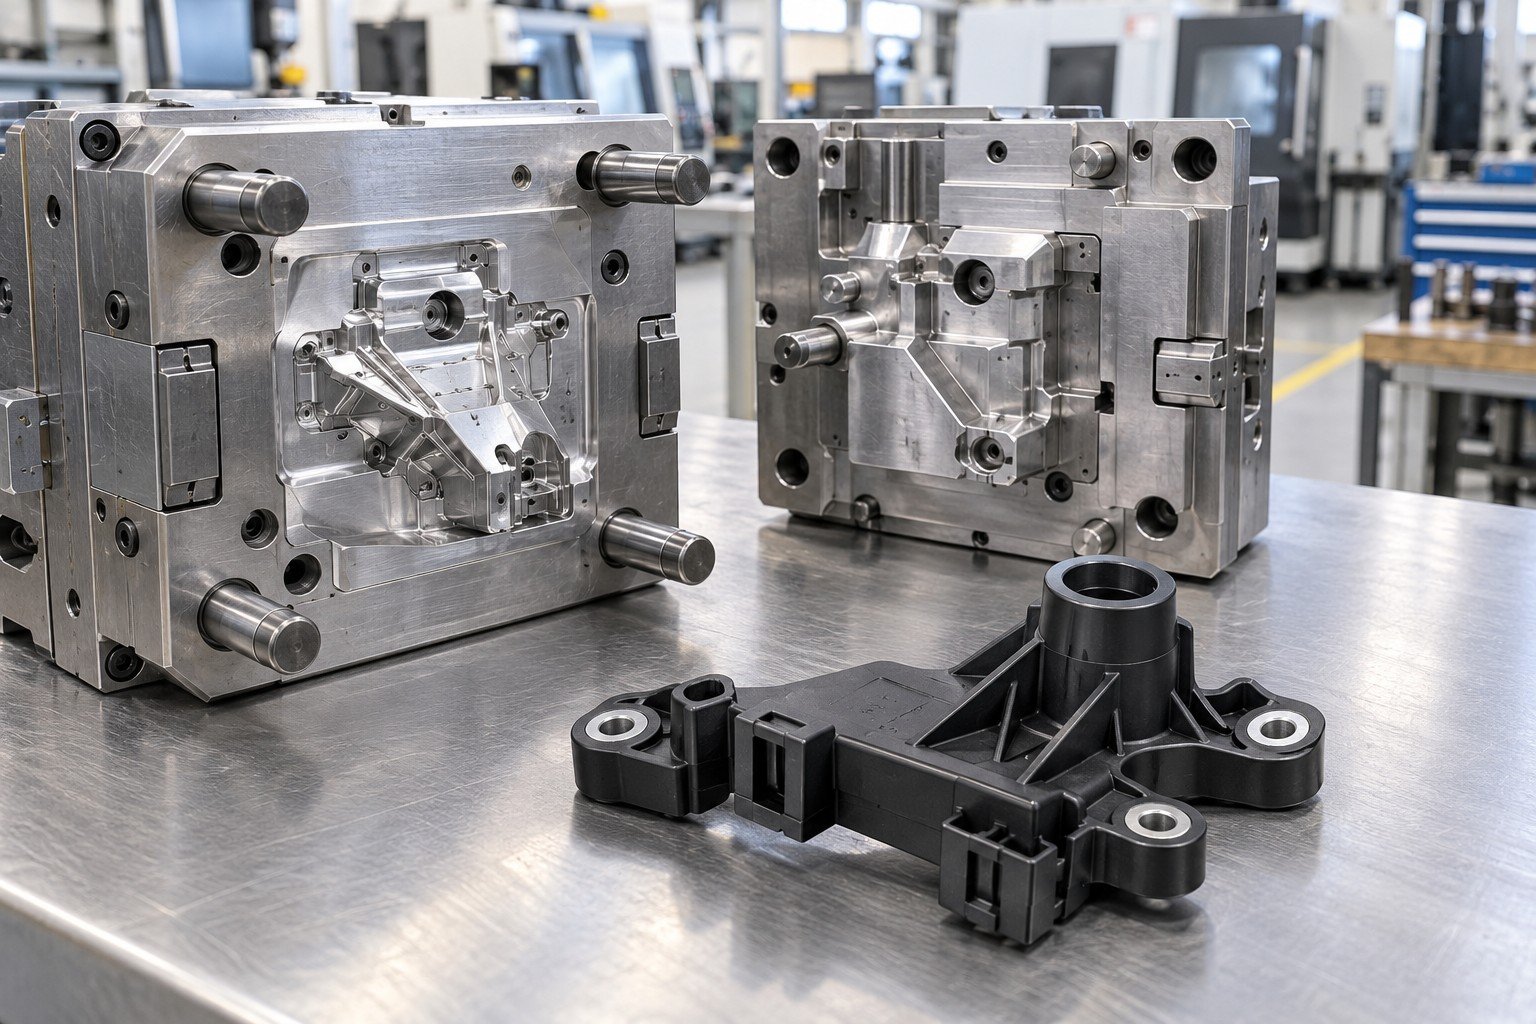
Automotive prototype tooling examples need project-specific acceptance; no automotive qualification is implied.
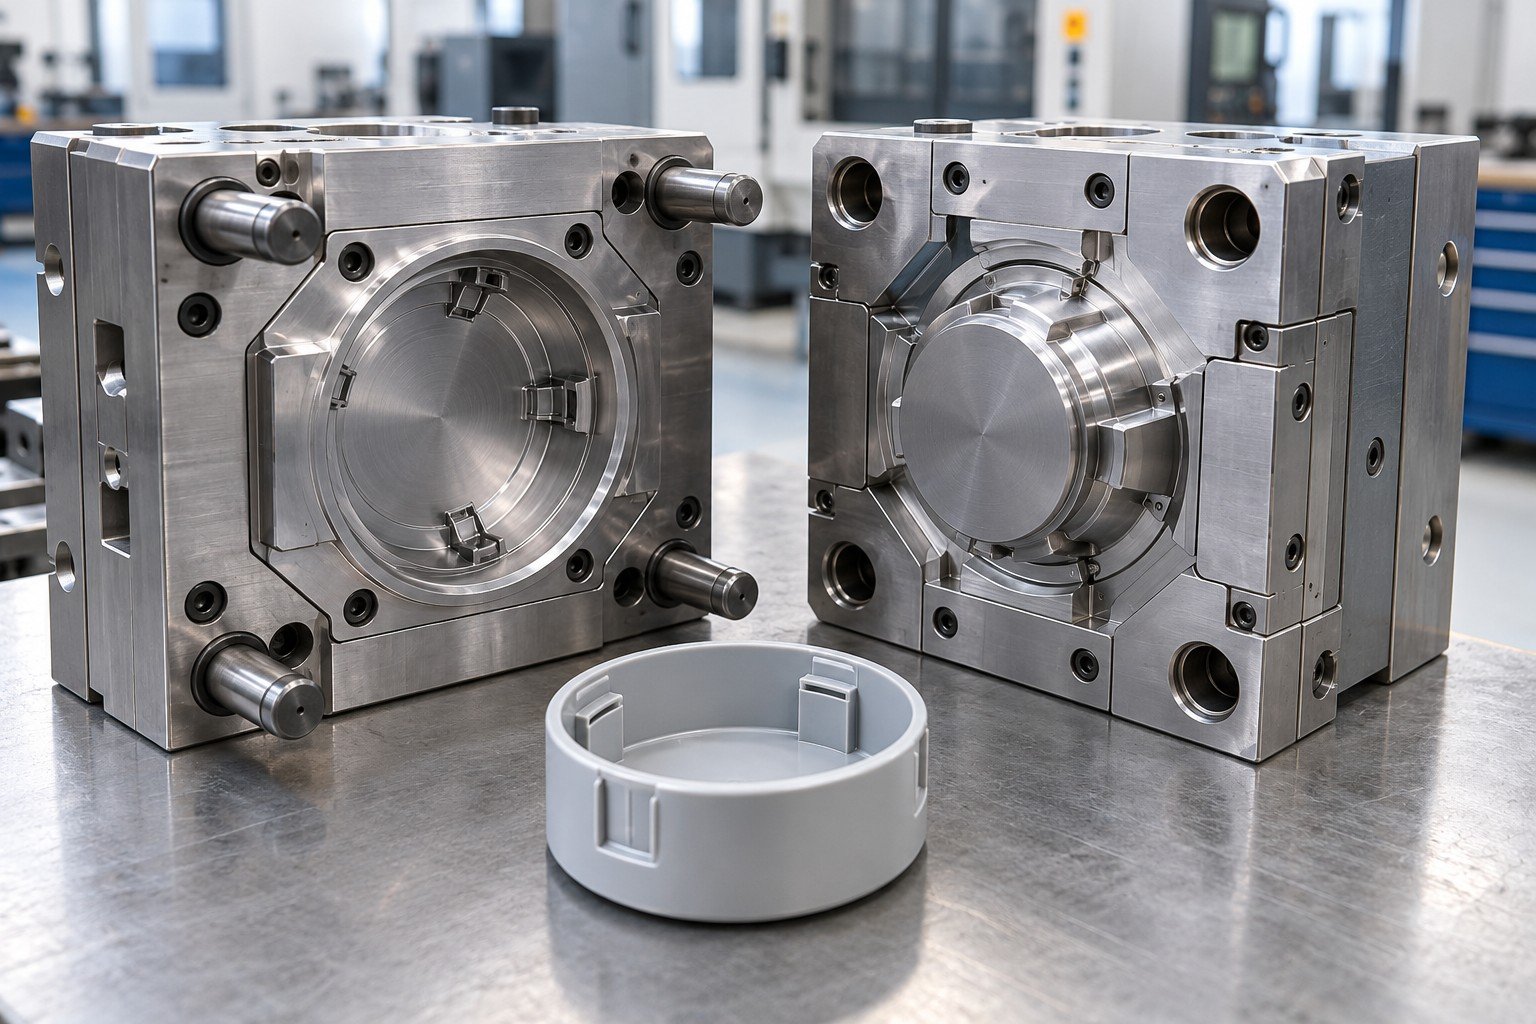
Review snap fit, resin behavior and interim supply for polypropylene covers.
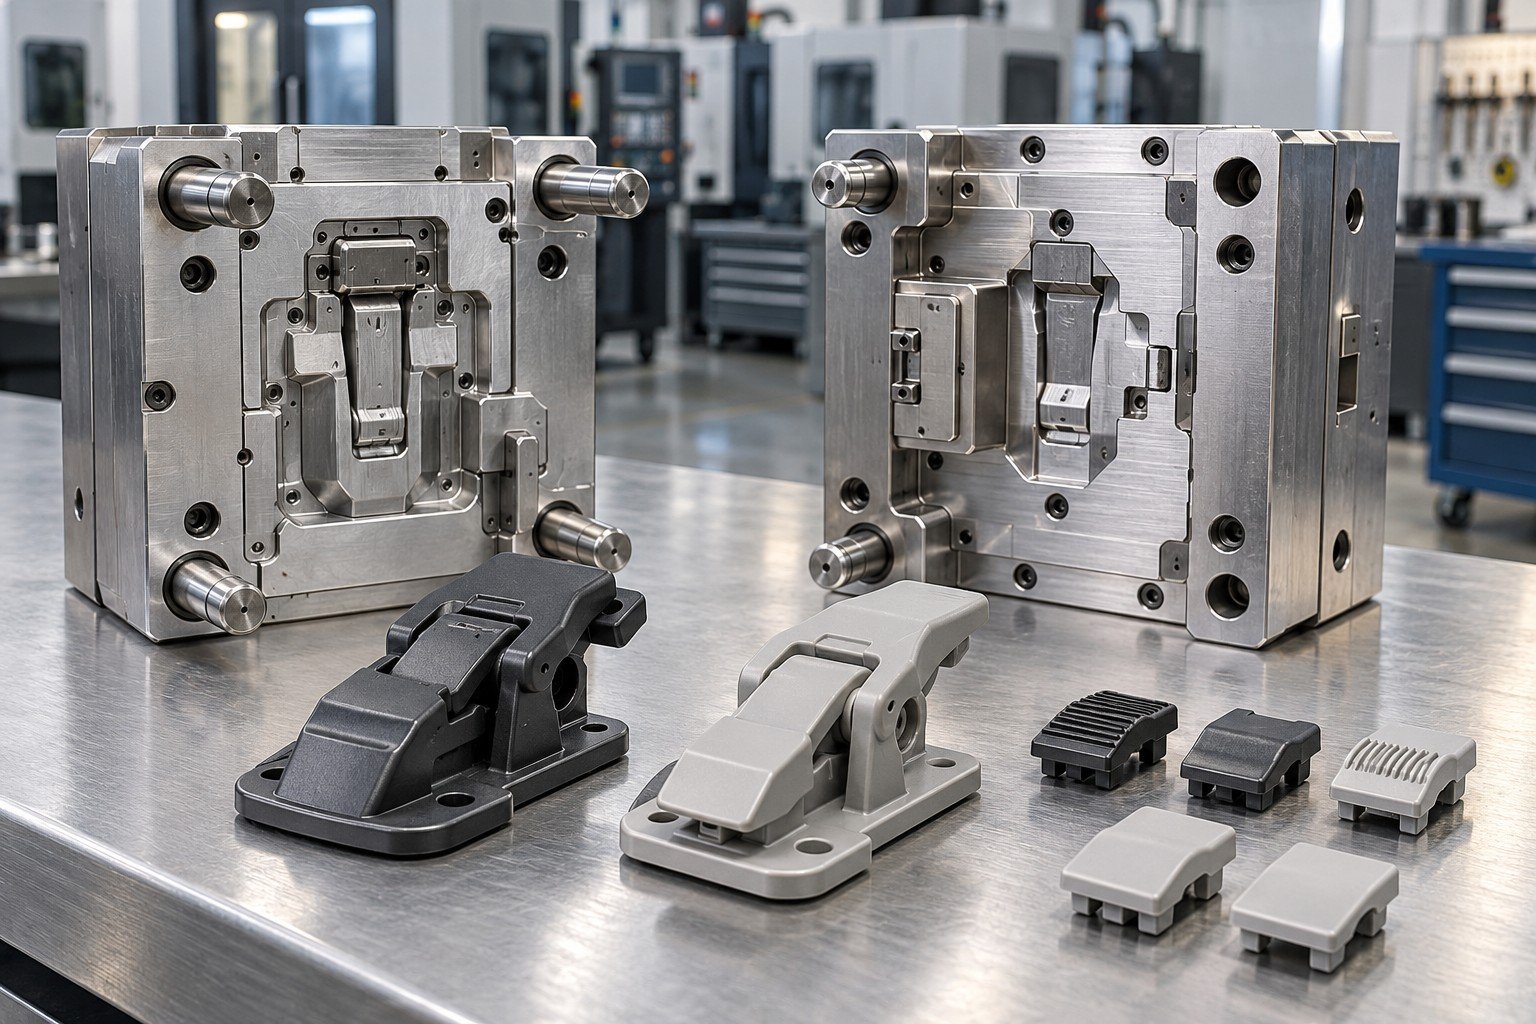
Compare selected feature revisions with controlled inserts and sample identities.
Illustrative tooling and part concepts, not customer case studies or qualification evidence. Your manufacturing route and acceptance are confirmed in the project scope.
Connect your mold review, sample decisions and delivery requirements to the responsible team.
Coordinate drawings, open questions and approval decisions.
Confirm supplied mold components, holder and spares.
Agree samples, inspection and correction records.
Coordinate interim use, preservation and delivery requirements.
Request an NDA before sending confidential files. Identify missing inputs so they can be reviewed rather than treated as approved assumptions.
Part, resin, tool concept and changeable features.
Dimensions, appearance, fit and documented exceptions.
Interim scope, records, ownership and delivery terms.
An approved sample and an accepted tool inventory answer different questions. Record both where your project needs them.
Prototype tooling is a mold or related tool built to support defined part-development questions. For plastic injection molding, it can produce samples in an agreed resin for fit, appearance or functional review. Prototype mold tooling still needs controlled geometry and trial acceptance.
Bridge tooling supports an agreed interim supply need while a longer-term route is developed or approved. It may be useful when trial demand and temporary supply overlap, but the expected use, acceptance and exit plan need review. It is not a mandatory stage for every project.
Prototype mold cost depends on geometry, tool material, cavity count, holder, inserts, cooling, ejection and trial scope. Compare your prototype mold manufacturer quotations on the same basis. Separate build, trials, corrections, inspection, molded parts, storage and transport.
Timing depends on design readiness, material availability, tool complexity, machine compatibility, first trial and correction cycles. Ask for milestones and approval inputs rather than treating a generic advertised lead time as your project schedule.
Production resin can be considered when the exact grade, availability and tool suitability are confirmed. Prototype tooling for nylon parts, filled resins or higher processing temperatures needs a corresponding construction review. A substitute resin may not answer the same validation question.
Continued use requires review of condition, expected demand, resin, wear, maintenance and acceptance. Bridge tooling mold life is project-specific. Do not assume a prototype tool can be converted to unlimited production or that a fixed shot count applies to every geometry.
These terms are used differently by suppliers. Specify actual material, grade, condition and construction. Aluminum prototype molds and steel prototype molds can both serve development work. Review the tool against your resin, part geometry, expected use and change plan.
Record ownership, permitted use, holder arrangements, drawings, storage, maintenance, release conditions and transfer charges in the order. Ask your bridge tooling manufacturer to identify supplied items and any shared components. Ownership and design-right terms should not be assumed from a tool payment alone.
The objectives, expected use, maintenance, cavity layout and acceptance scope can differ. A prototype tool may prioritize a design question; a production tool supports a defined repeat-supply program. A prototype mold is not necessarily aluminum, and a bridge mold is not necessarily simpler in every feature.
Agree the tool inventory, holder, inserts, spares, drawings, approved samples and trial records. Review current condition, preservation and receiving-machine compatibility. A receiving trial or further corrections may be required; a shipping receipt alone does not establish production readiness.





