








































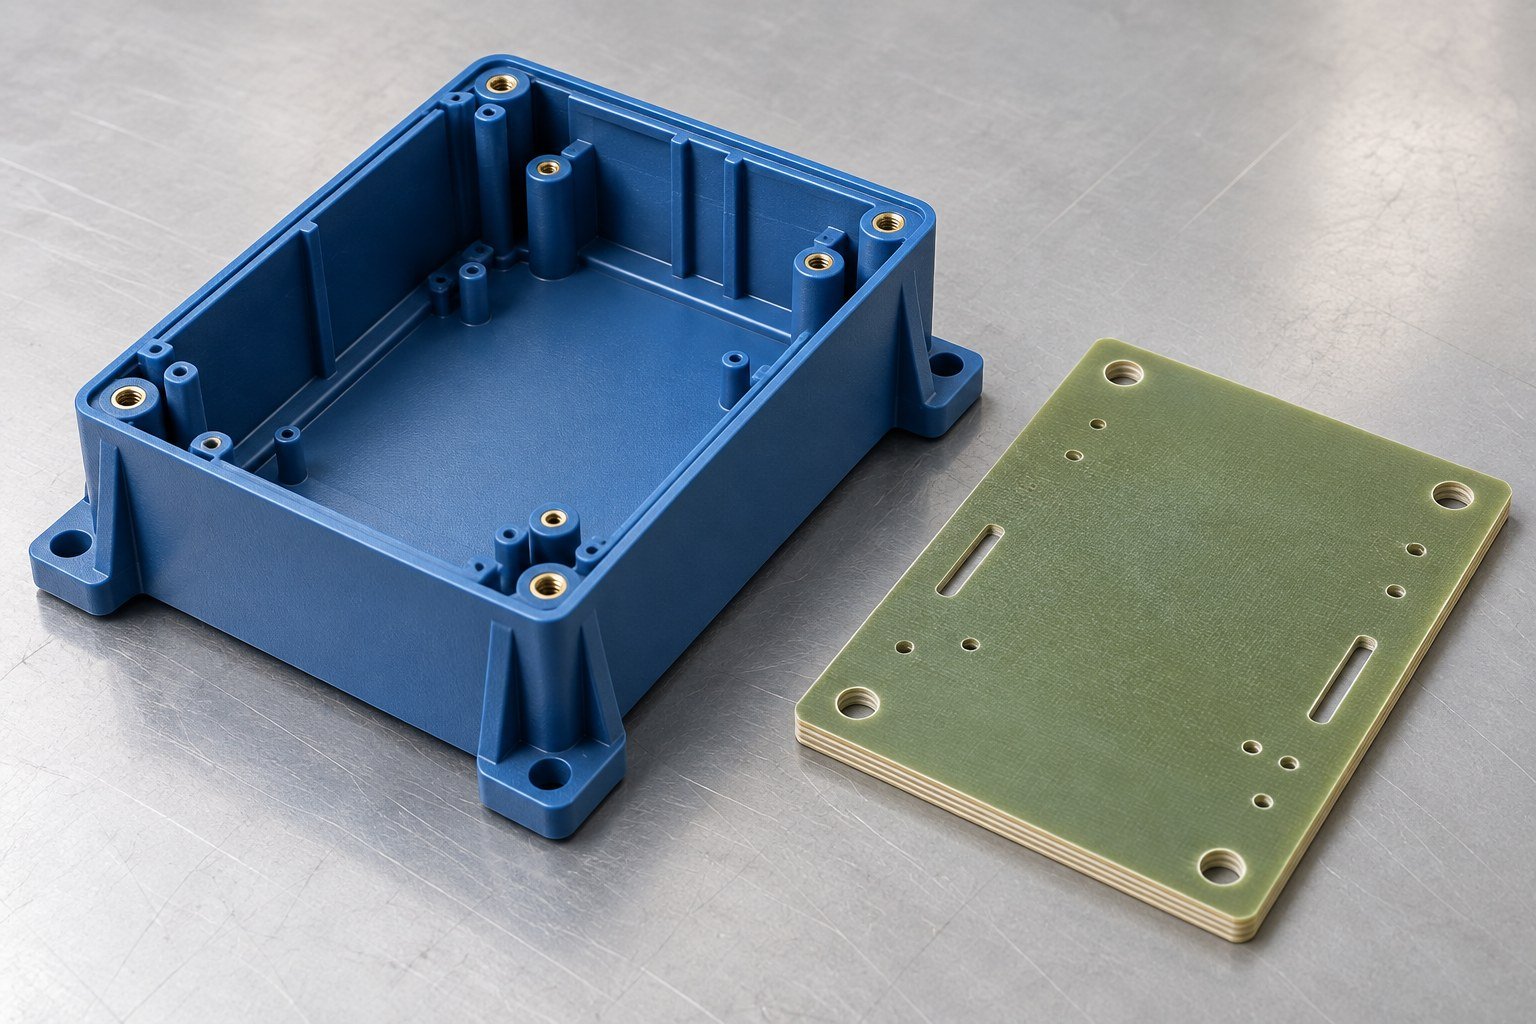
Choosing thermoplastic vs thermoset starts with what your part must do, how it will be made and what must remain stable in service. A material-family name alone cannot confirm temperature capability, chemical resistance or fit. Define those requirements before selecting a resin grade or committing to tooling.
This guide compares the two families for a custom-part review. It complements the thermoplastic injection molding service and elastomer and specialty material options; it does not replace a grade-specific datasheet or application testing.
The practical difference: cooling versus curing
A thermoplastic softens with heat and becomes firm again as it cools. Its structure allows another forming cycle within an appropriate processing window. A conventional thermoset develops a crosslinked network during cure. After that reaction, reheating does not return it to a melt that can be molded again in the same way.
For your project, that distinction affects the manufacturing route and what happens to process scrap. It does not establish which finished part is stronger, cheaper or more durable. Those comparisons need a specified grade, geometry, production process and test conditions.
Compare the decisions that affect your part
| Your decision | Thermoplastic review | Thermoset review |
|---|---|---|
| How the shape is established | Heat and forming, followed by cooling; the route depends on the resin and part. | A curing reaction establishes the network; review the selected molding or laminate route. |
| Examples to investigate | PP, ABS, PC and PA grades for different functions. | Epoxy-based systems and cured silicone systems for different functions. |
| What to specify | Exact grade, fillers, conditioning and relevant performance tests. | Exact formulation or laminate designation, cure requirements and relevant performance tests. |
| End-of-life question | Ask whether the actual grade and waste stream can be collected and reprocessed. | Do not assume conventional melt recycling; investigate an available, suitable recovery route. |
Start with the service conditions
Describe the environment your part will experience: continuous and occasional heat, applied load, chemicals, moisture, sunlight and repeated movement. Identify which conditions occur together. An unloaded short heat exposure is a different requirement from a loaded assembly operating for an extended period.
Then define the outcome you need to preserve. For an enclosure, it may be assembly fit and the position of a sealing surface. For an insulating plate, it may be dimensional stability and the specified electrical performance. Share the applicable test method and acceptance criteria rather than asking for the “best plastic.”
Match the family to a manufacturing route
Thermoplastic injection molding is one route for repeat molded parts; extrusion and machining of suitable stock shapes answer different geometry and quantity needs. Thermoset processing depends on the particular system. A cured laminate machined into a plate should not be treated as interchangeable with an injection-molded resin.
Discuss the actual route before freezing your drawing. Ask which surfaces establish assembly position, which features need inspection and where a design change could simplify manufacture. If you are comparing a prototype with a later molded part, record the material and process differences so that a successful prototype is not mistaken for complete production validation.
Do not group every flexible material together
Flexible behavior does not identify a material as thermoplastic. A thermoplastic elastomer and a cured rubber can both feel flexible while belonging to different processing families. When reviewing a seal, grip or compliant interface, provide the material designation and function instead of specifying only “rubber” or a color.
Use the TPU and TPE material page to frame a thermoplastic-elastomer discussion, and the silicone and LSR molding information for a separate cured-silicone review. Confirm the final formulation and processing scope for your application.
Ask a specific recycling question
Being remeltable does not guarantee that a used part will be recycled. Separate the technical possibility from the collection and processing route available for your actual material stream. Ask about the exact grade, additives, contamination and the requirements governing any proposed reuse.
For a purchasing decision, request a documented answer for the proposed material and program. Do not turn a broad material-family description into a recycling promise for your finished product.
Prepare a useful material comparison package
- Part definition: CAD, drawing revision, critical interfaces and inspection requirements.
- Operating environment: heat exposure, load, fluids and other relevant conditions.
- Material scope: required grade or candidate grades, fillers, color and documentation needs.
- Manufacturing plan: prototype purpose, expected order quantities and the process routes being compared.
- Acceptance: tests and evidence needed before you approve the material and finished part.
Keep unresolved requirements visible. A material comparison is useful when it explains what has been verified, what still needs testing and who approves the final choice. For a broader review, see material and process selection.
Your thermoplastic and thermoset questions
Is a thermoset always better at high temperature?
No family label establishes your allowable service temperature. Compare the proposed grades under the relevant load, exposure duration and acceptance conditions.
Can a cured thermoset be melted and molded again?
A conventional cured thermoset cannot be remelted for ordinary molding in the same way as a thermoplastic. Discuss any proposed recovery method separately.
Does this comparison identify a drop-in replacement?
No. A substitution needs a review of the specific grade, process, drawing and application. Preserve the approval record for any change.

