Injection Molding
Tooling and molding for your repeat plastic parts.
From prototype to production, coordinated manufacturing solutions for your custom parts.
View All Services →
Precision parts for your tight tolerances and complex geometry.
Tooling and molding for your repeat plastic parts.

Metal casting options for your part and production volume.

Cutting, forming and welding for your fabricated parts.

Custom profiles for your section, length and finish requirements.

Finishes for your appearance, corrosion and wear requirements.

Sub-assemblies and final builds for your production program.

Production tooling built around your process and volume.

Prototype parts to check fit, function and design.
DFM, process planning and production support for your project.
Inspection, documentation, inventory and delivery planning for your program.
Choose air- or liquid-cooling components around your thermal and mechanical requirements.

Manufacturing support for your cold plates, manifolds and cooling assemblies.

Find components for your power electronics, energy, laser and telecom application.

Components for your electronic systems.
Start with your functional and quality requirements.
Build around your operating environment.
From prototype to production, review material performance, manufacturability and cost for your part.
Review grade, temper and finish for your metal parts.
 AluminumStrength, weight and machining›
 Stainless SteelCorrosion and finish requirements›
 Carbon & Alloy SteelDiscuss grade and heat treatment›
 Tool SteelDiscuss tooling and wear needs›
 TitaniumReview grade and part geometry›
 Copper & Brass & BronzeDiscuss conductivity and machining›
Match your polymer to function, process and environment.
 ABSReview enclosure and molding needs›
 Polycarbonate (PC)Discuss clarity and impact needs›
 Nylon (PA)Review moisture and wear conditions›
 POM / AcetalReview fit and sliding features›
 PEEKDiscuss operating conditions›
 PTFEReview friction and chemical exposure›
 ULTEM / PEIDiscuss thermal and electrical needs›
Confirm grade availability and application requirements.
 Silicone / LSRDiscuss flexible component needs›
 TPU / TPEReview flexibility and processing›
 EPDMReview weathering and chemical exposure.›
 NBRReview oil and fuel exposure.›
 FKMReview temperature and chemical exposure.›
 G10 / FR4Review insulation and laminate needs›
 CompositesReview stiffness, weight and laminate.›Customer-Specified MaterialsConfirm your grade and requirements.›Other Specialty MaterialsDiscuss your application and grade.›
Practical guidance for your part geometry and material decisions.
Prepare your process, budget and sourcing questions.
Build your knowledge before production.
Learn who we are and how we operate.
Find our U.S. support team or start a conversation.
YOUR LOCATING FEATURES. YOUR MASS OFFSET. YOUR MOTION SYSTEM.
Review your custom robot gripper fingers, mounting plates and sensor brackets against the mating equipment drawing. Define functional interfaces, material and acceptance before approving the manufacturing route.
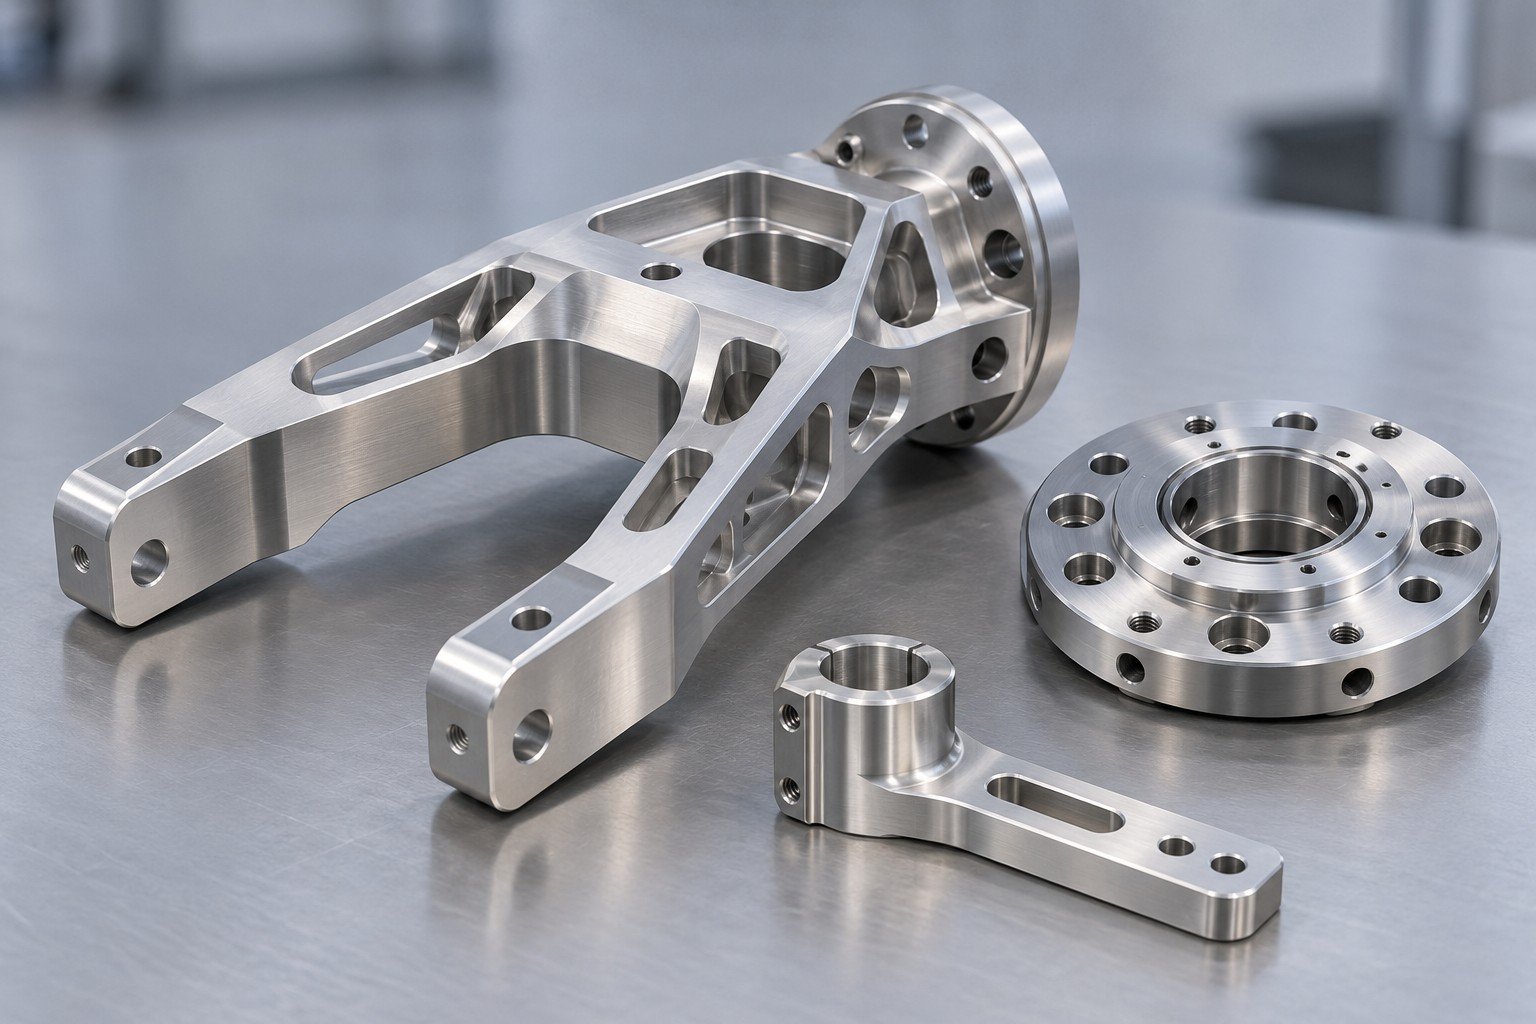
Which shoulders, bores or datums set the tool position?
What are the complete assembly mass and center of gravity?
Which clearances, cables and motion conditions matter?
Which dimensions and records support sample approval?
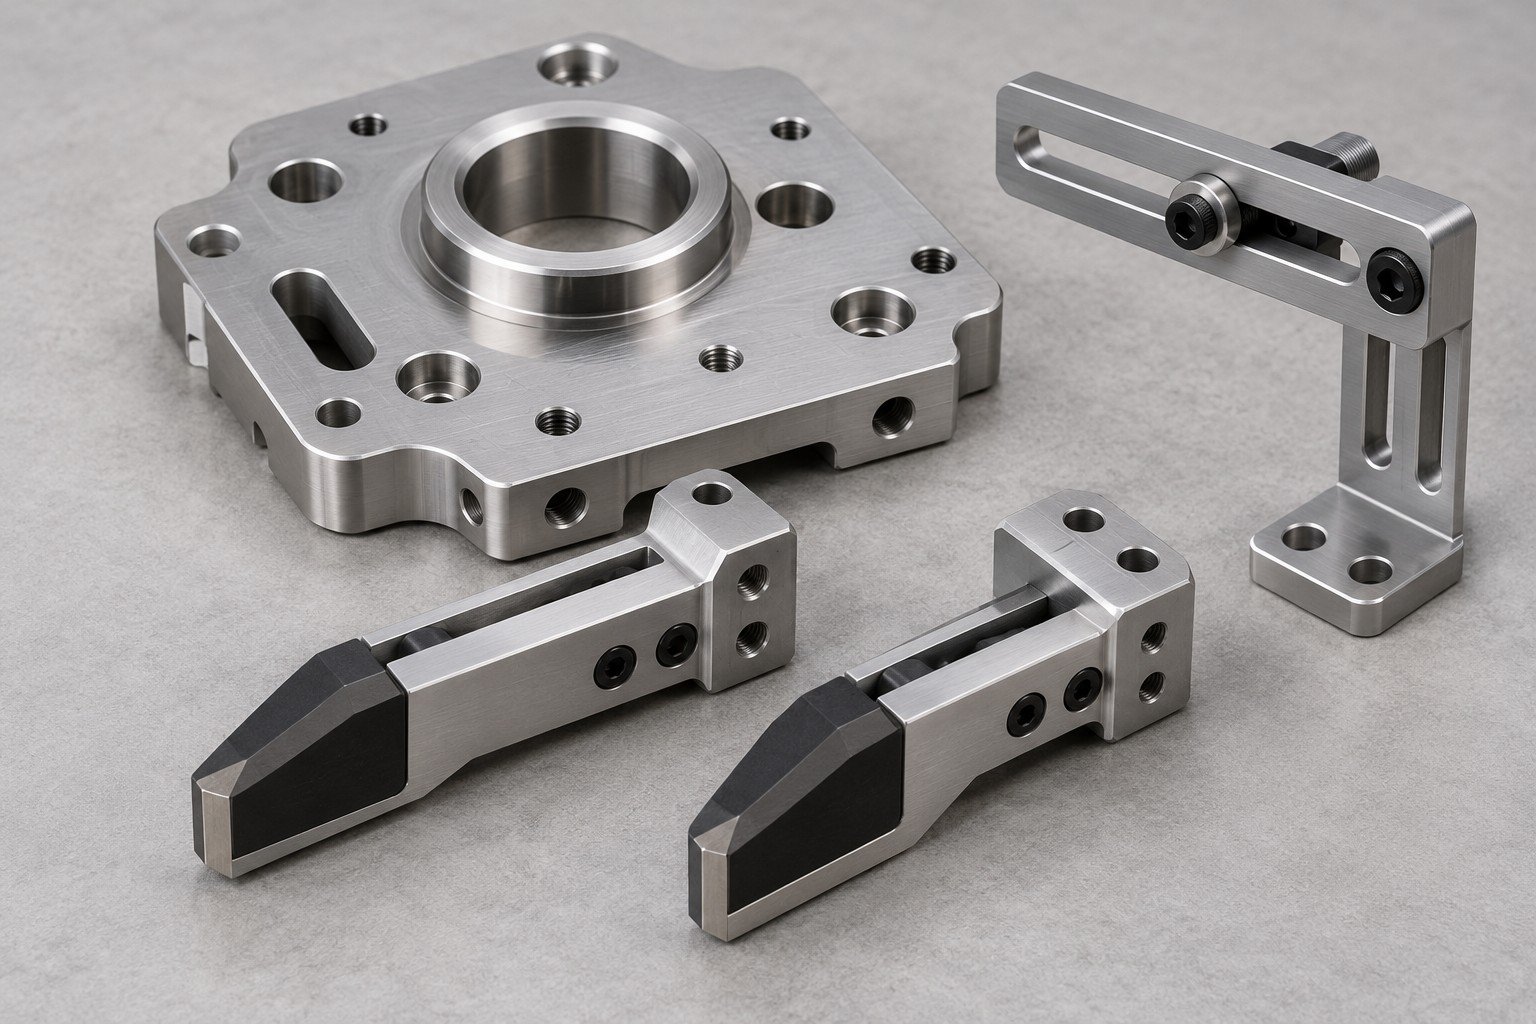
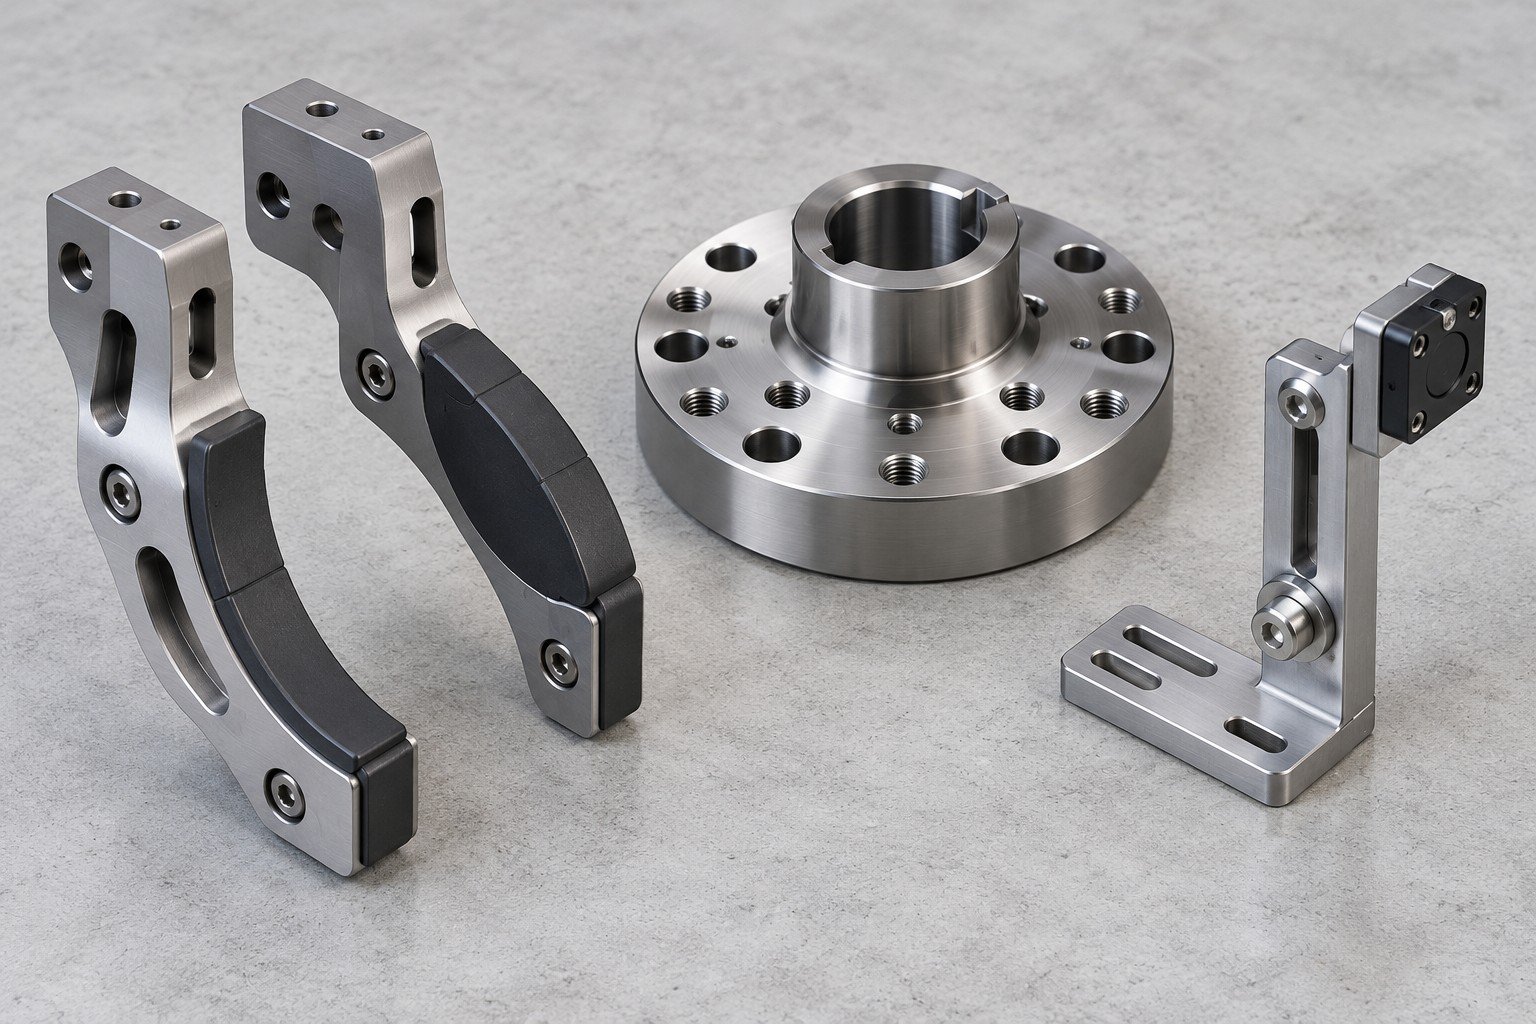
Review contact geometry, fastening, wear surfaces and the actual workpiece interface.
Match flange patterns, locating shoulders and accessible fasteners.
Review adjustment slots, travel clearance, cable routing and assembly access.
For a robot end effector manufacturer inquiry, distinguish the custom mechanical components from complete gripper design, controls and robot-cell approval.
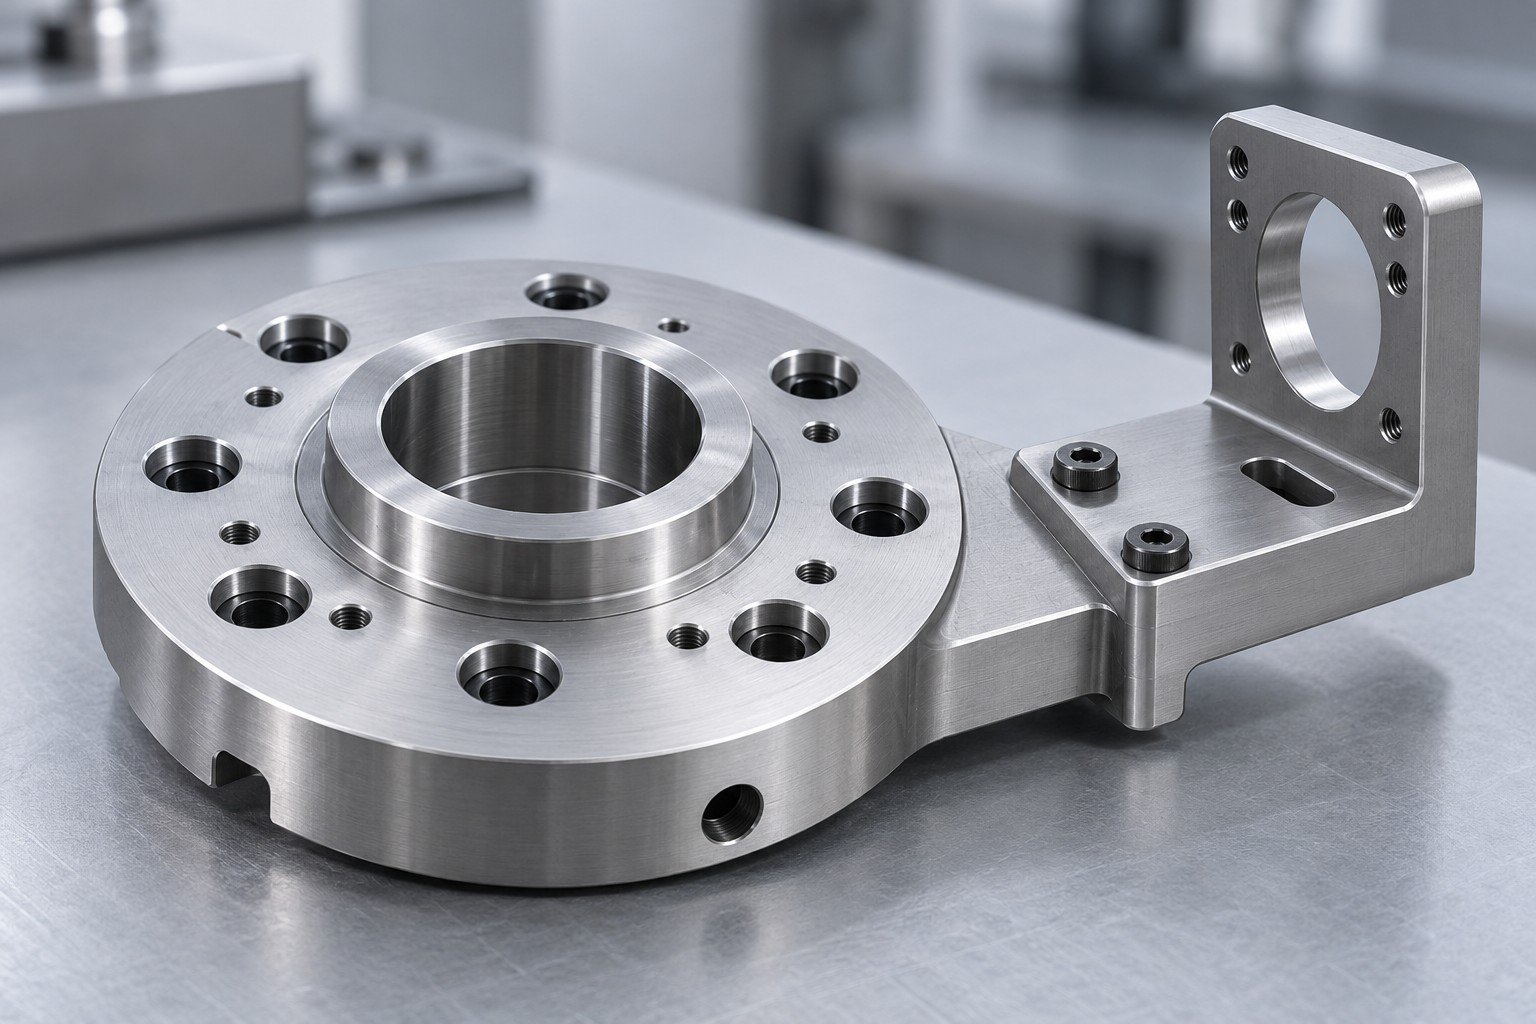
For robot mounting plate CNC machining, identify the locating relationship before assigning tolerances to every feature.
Lightweight aluminum robot components still need an installed mass-and-offset review. This example compares geometry; it does not establish a robot payload or bracket strength rating.
Assumed mass 0.5 kg; g=9.8m/s²;perpendicular offset; zero baseline 0–1.0 N·m.
M=mgr. Offsets 0.05/0.10/0.20m give 0.245/0.490/0.980 N·m. Static gravity only:inertia, acceleration, impact, cables and structural flexibility are outside this example.
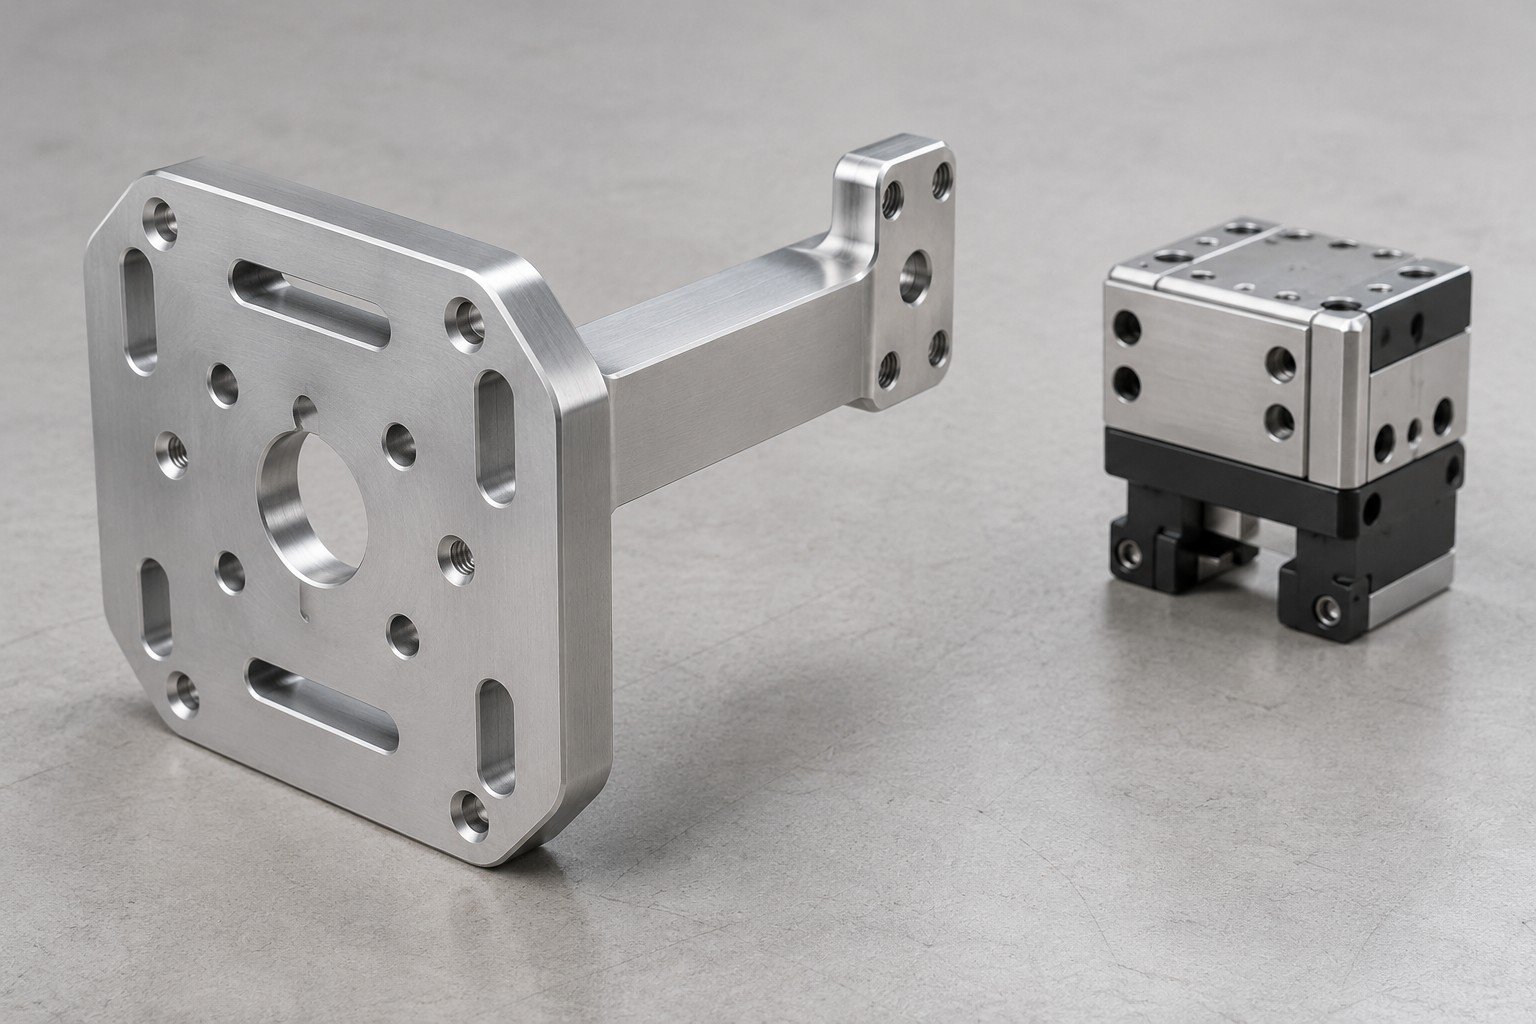
The machine or cell owner determines the applicable load and safety validation.
NIST · near-Earth gravity reference → · Robot OEM · payload and center-of-gravity setup →
For your robotics machined parts supplier review, connect tool access, critical features and repeat demand before adding unnecessary precision to the whole part.
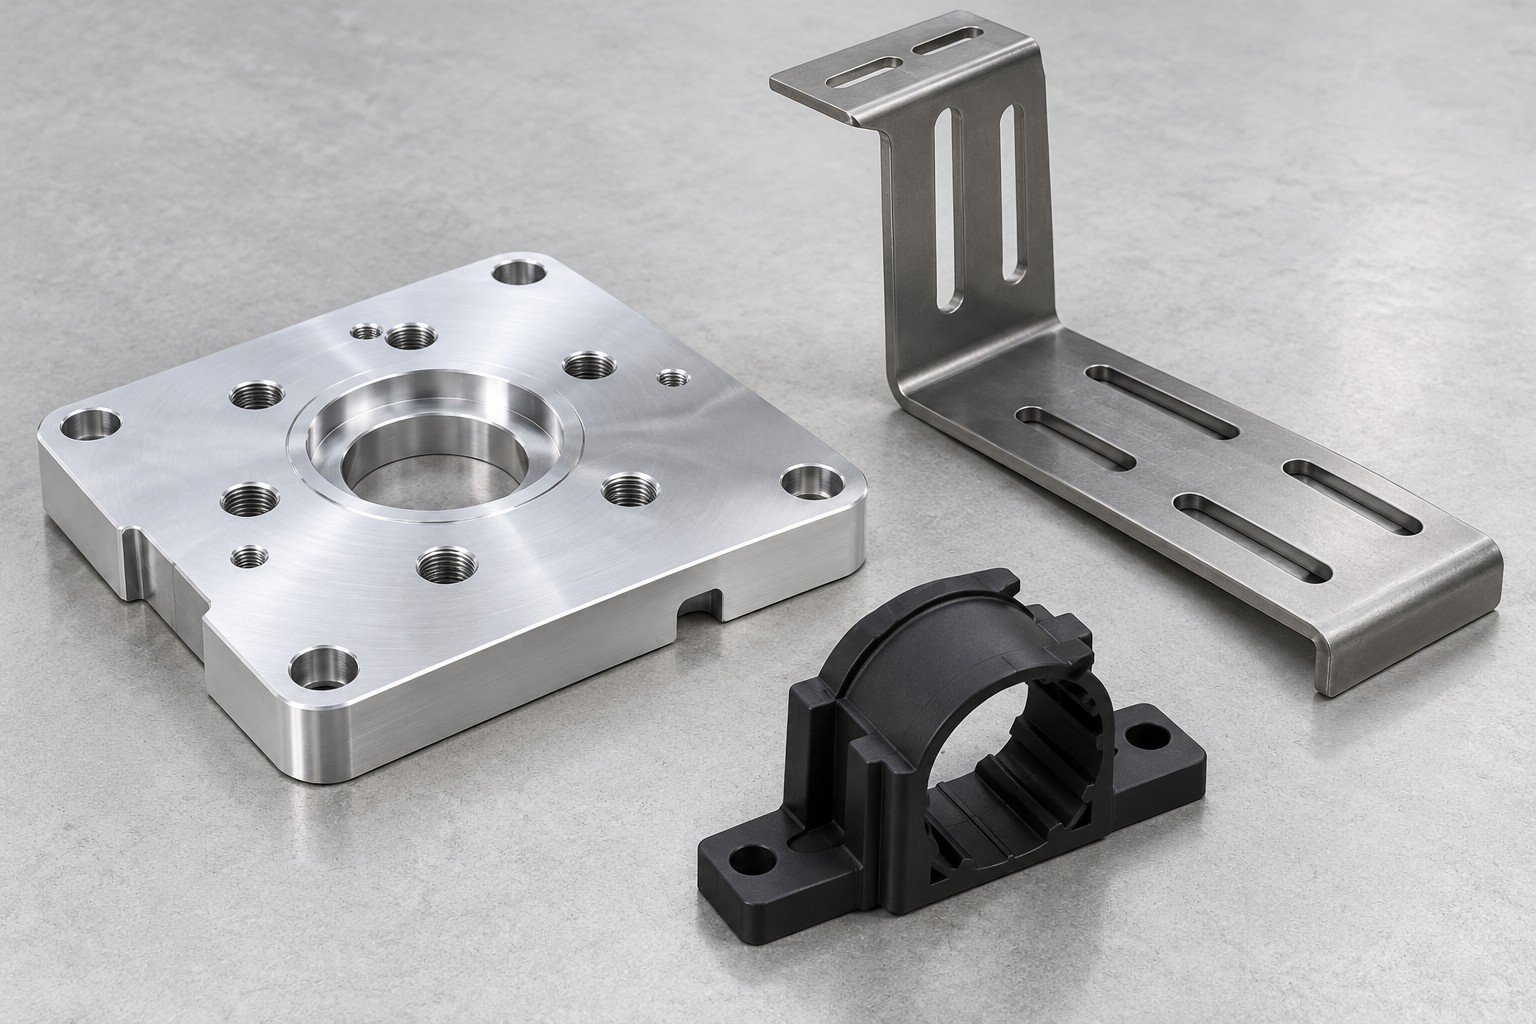
Tie critical dimensions to locating and mating function before choosing the process and final finishing.
| Your feature | Route to review | Drawing input |
|---|---|---|
| Locating shoulders and mounting faces | CNC machining | Functional datums, fit and final condition |
| Slotted supports and covers | Sheet-metal fabrication | Thickness, bends, slot travel and hardware |
| Repeated support section | Extrusion with secondary machining | Profile choice, ends and mounting details |
| Multi-part tooling group | Mechanical assembly | Component revisions, fasteners and agreed sample checks |
Review locating bores, mounting faces and selected fit dimensions.
Confirm grade, condition, protected contacts and required records.
Check the defined mating hardware and fastener access.
Define payload, motion and required machine/cell approval with its owner.
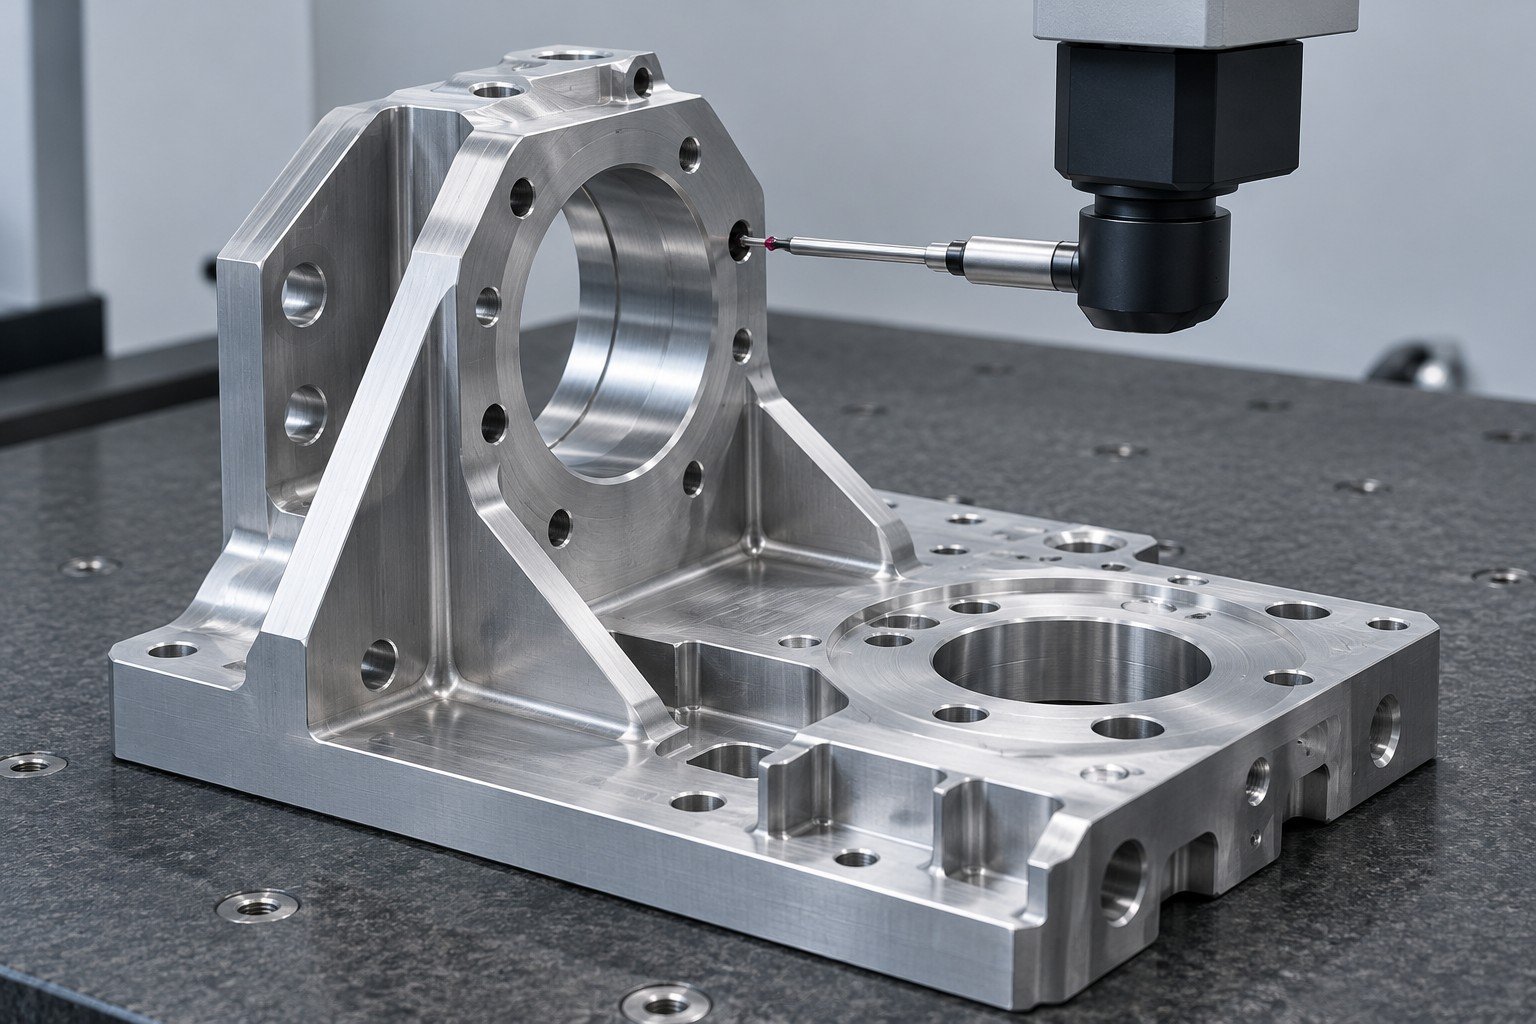
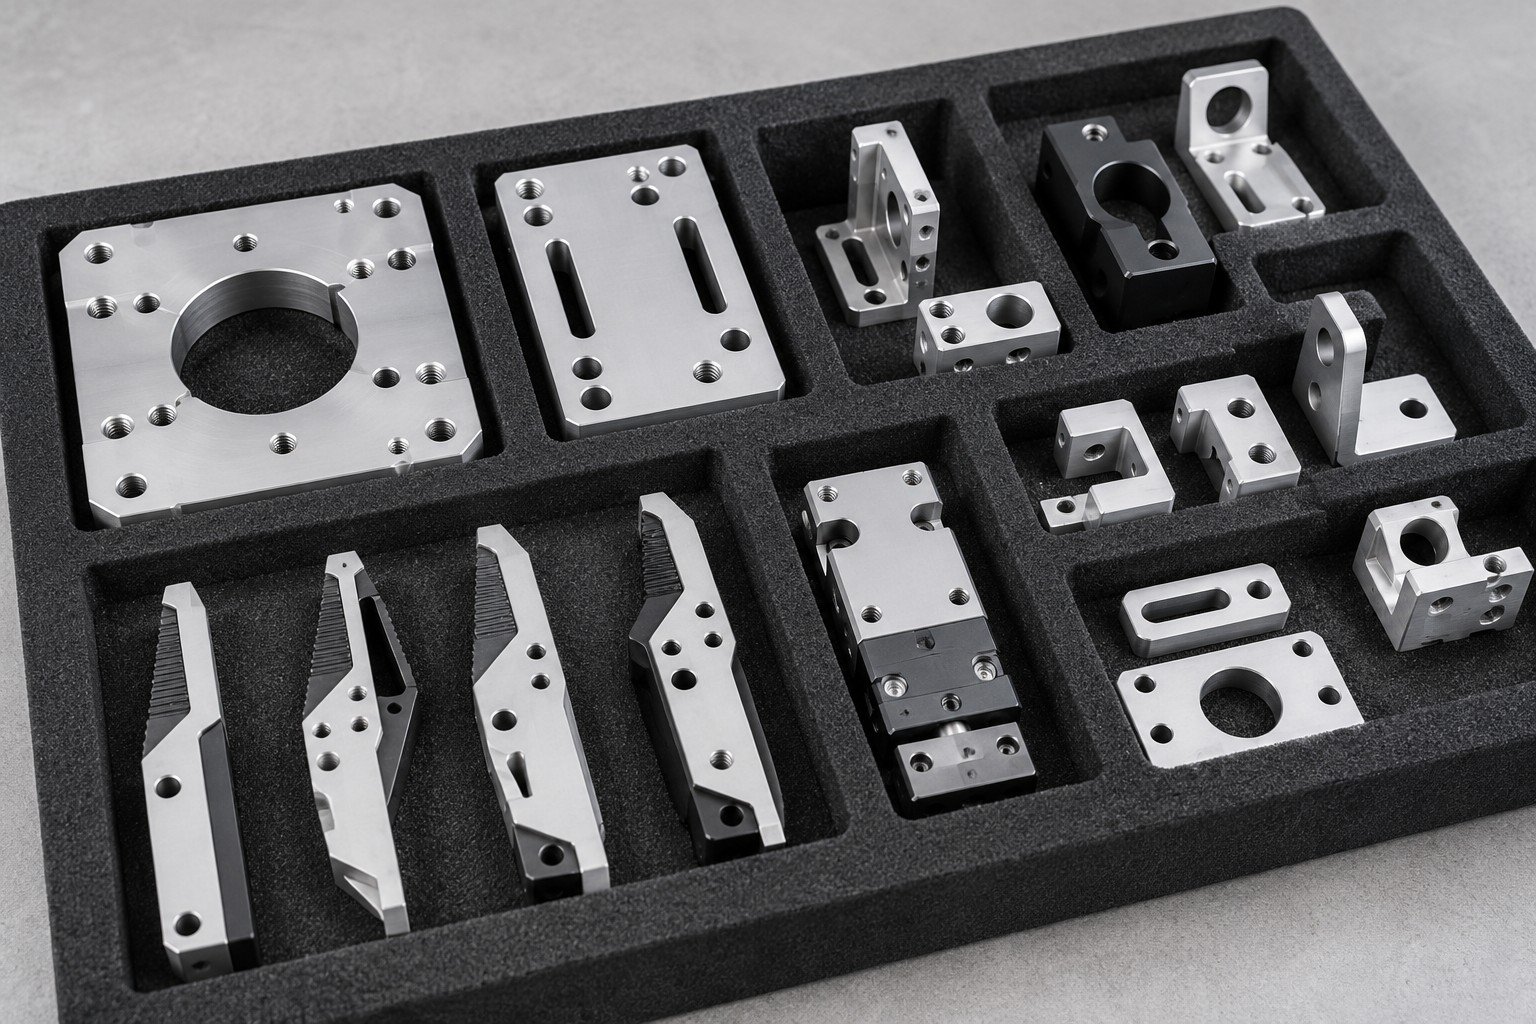
Confirm drawing revision and actual application.
Review material, geometry and manufacturing sequence.
Build the agreed sample and check defined interfaces.
Record accepted features, finish and required evidence.
Coordinate repeat scope, packing and delivery requirements.
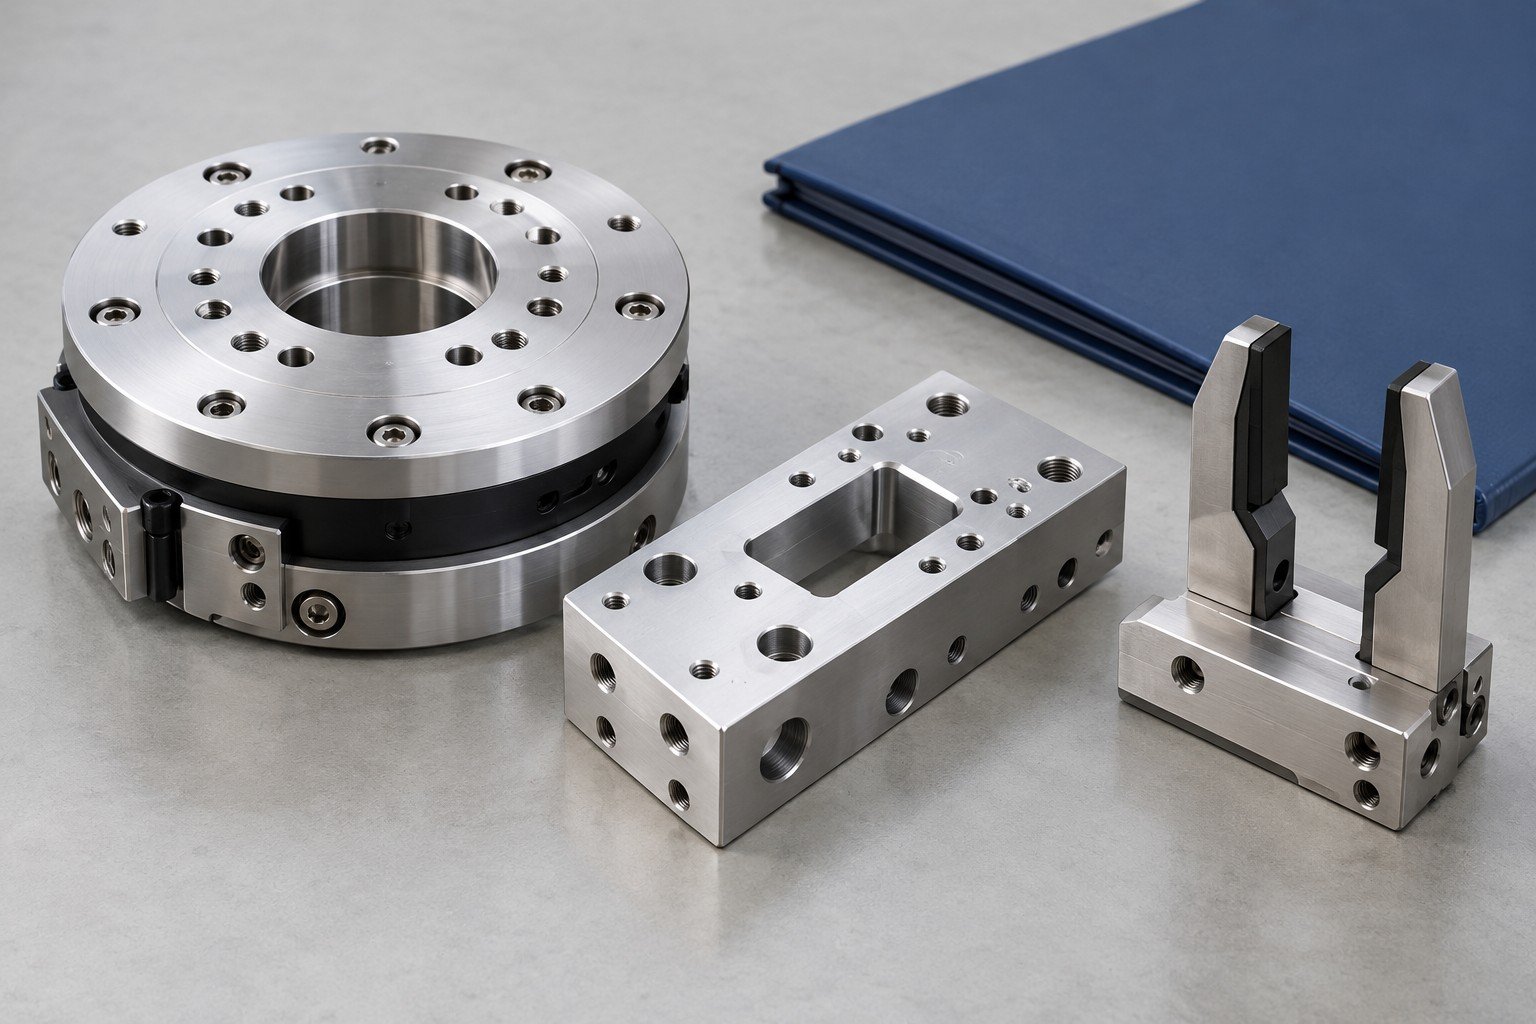
Keep tolerances tied to function, review accessible machining features and avoid unnecessary finish operations on hidden faces. Compare the same geometry, quantity and inspection scope before changing the route.
No. Review the complete tool assembly, center of gravity, motion profile, stiffness and equipment limits. Material density or appearance alone cannot establish the result.
Identify the intended datum or locating features on the mating assembly. Distinguish those features from fasteners that clamp the joint, and agree how they will be inspected.
Provide CAD, controlled drawing, mating interfaces, material/finish, complete installed load information, quantities and required inspection records.
Compare mounting and inspection planning for equipment parts.
Explore equipment interfaces →