

Injection Molding
Tooling and molding for your repeat plastic parts.
From prototype to production, coordinated manufacturing solutions for your custom parts.
View All Services →
Precision parts for your tight tolerances and complex geometry.
Tooling and molding for your repeat plastic parts.

Metal casting options for your part and production volume.

Cutting, forming and welding for your fabricated parts.

Custom profiles for your section, length and finish requirements.

Finishes for your appearance, corrosion and wear requirements.

Sub-assemblies and final builds for your production program.

Production tooling built around your process and volume.

Prototype parts to check fit, function and design.
Choose air- or liquid-cooling components around your thermal and mechanical requirements.

Manufacturing support for your cold plates, manifolds and cooling assemblies.

Find components for your power electronics, energy, laser and telecom application.

Components for your electronic systems.
Start with your functional and quality requirements.
Build around your operating environment.
From prototype to production, review material performance, manufacturability and cost for your part.
Review grade, temper and finish for your metal parts.
 AluminumStrength, weight and machining›
 Stainless SteelCorrosion and finish requirements›
 Carbon & Alloy SteelDiscuss grade and heat treatment›
 Tool SteelDiscuss tooling and wear needs›
 TitaniumReview grade and part geometry›
 Copper & BrassDiscuss conductivity and machining›
Match your polymer to function, process and environment.
 ABSReview enclosure and molding needs›
 Polycarbonate (PC)Discuss clarity and impact needs›
 Nylon (PA)Review moisture and wear conditions›
 POM / AcetalReview fit and sliding features›
 PEEKDiscuss operating conditions›
 PTFEReview friction and chemical exposure›
 ULTEM / PEIDiscuss thermal and electrical needs›
Confirm grade availability and application requirements.
 Silicone / LSRDiscuss flexible component needs›
 TPU / TPEReview flexibility and processing›
 EPDMReview weathering and chemical exposure.›
 NBRReview oil and fuel exposure.›
 FKMReview temperature and chemical exposure.›
 G10 / FR4Review insulation and laminate needs›
 CompositesReview stiffness, weight and laminate.›Customer-Specified MaterialsConfirm your grade and requirements.›Other Specialty MaterialsDiscuss your application and grade.›
Practical guidance for your part geometry and material decisions.
Prepare your process, budget and sourcing questions.
Build your knowledge before production.
Learn who we are and how we operate.
Find our U.S. support team or start a conversation.
PROGRESSIVE STAMPING DIES
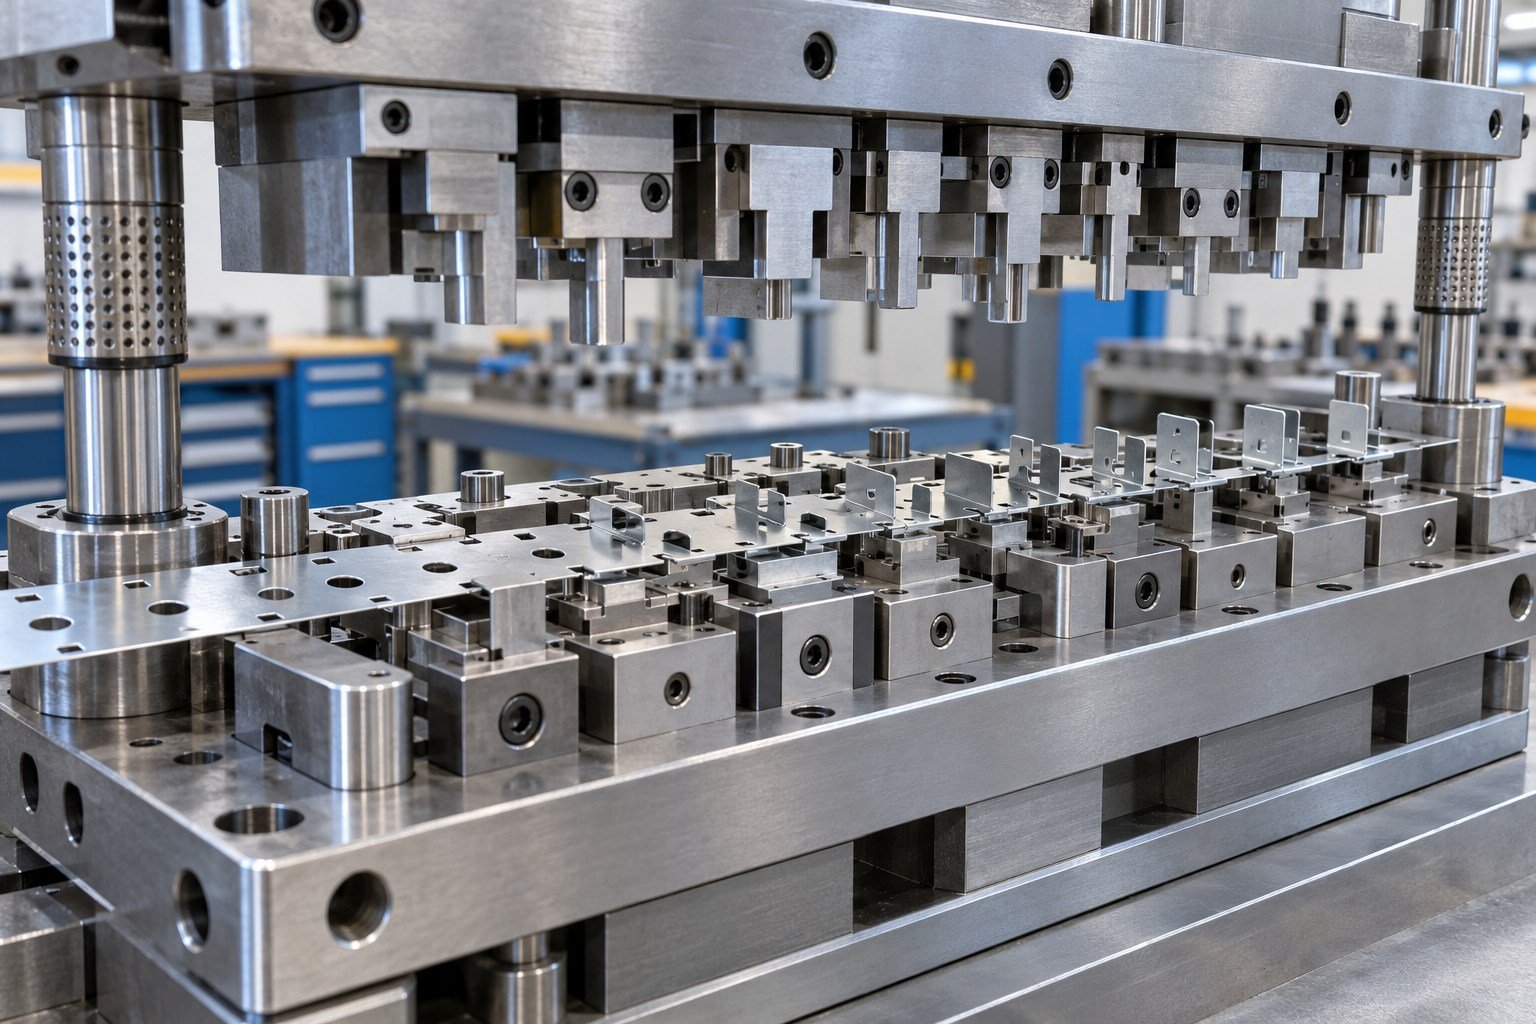
Plan your progressive stamping dies around the finished part, coil specification, strip layout and receiving press. Review pilots, forming sequence, scrap removal and trial evidence before tool manufacture.
1 connected strip. A controlled sequence of stations.
Review Your Stamping Tool →6 quote inputs ↓Drawing approved · Tryout reviewed · Handover defined
FOR YOUR STAMPING PROGRAM
Compare the complete operation plan. Tool purchase and stamped-part production are separate scopes.
COMPARE THE OTHER ROUTE
For your discrete operation, staged route or secondary feature.
Review single-station tooling →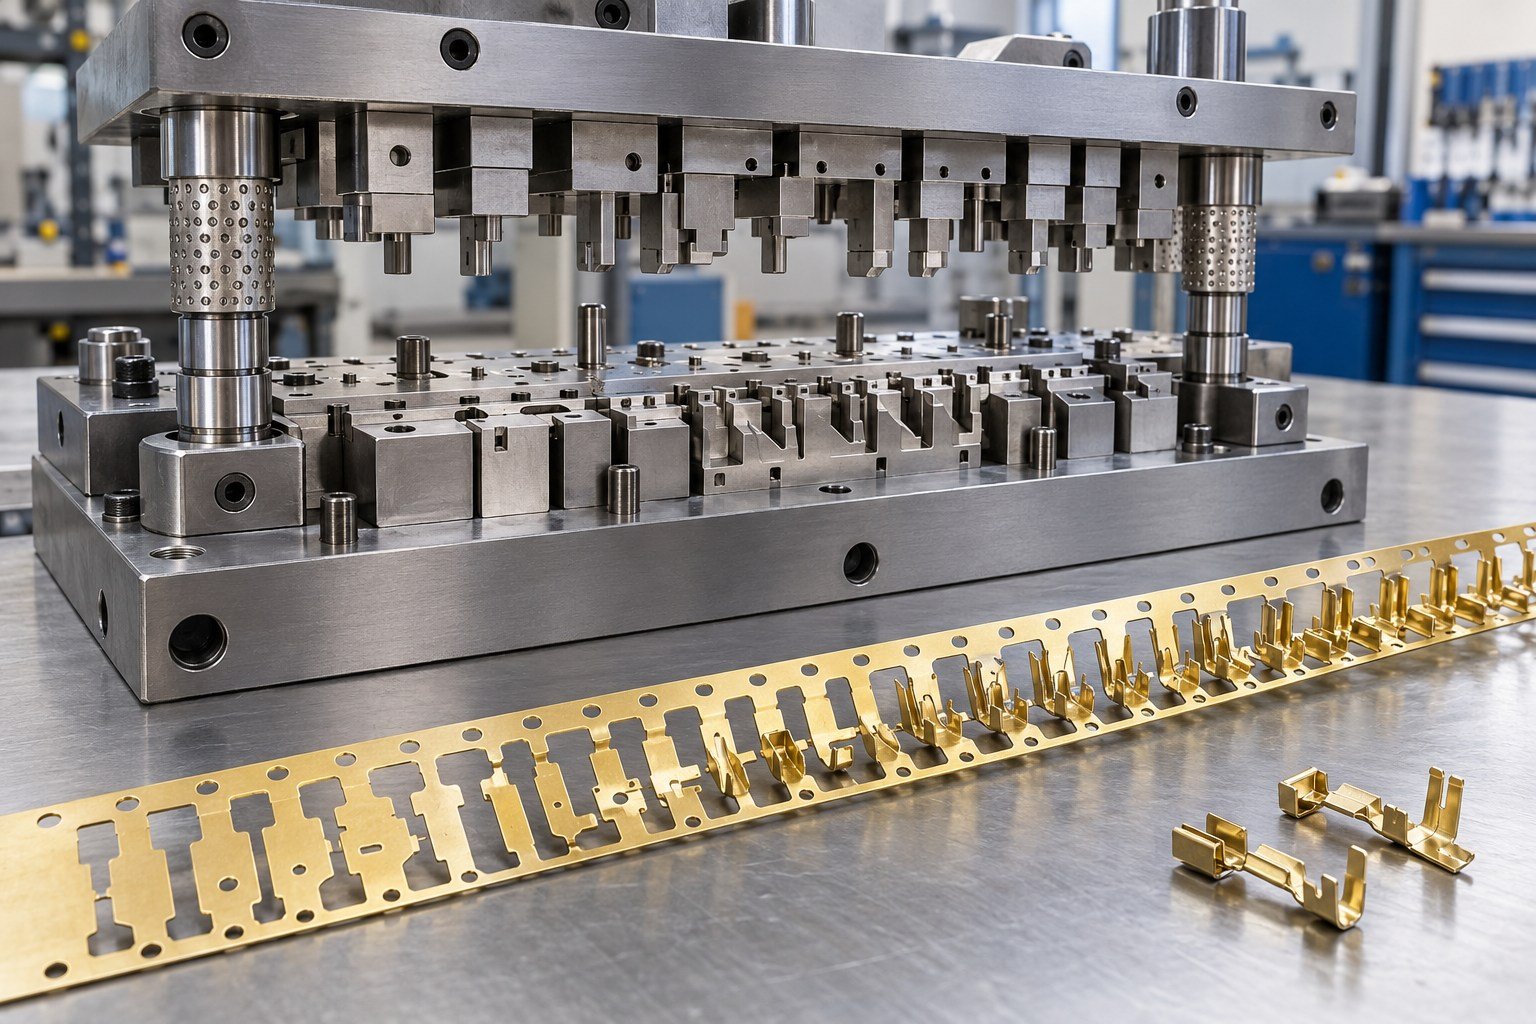
ON THIS PAGE
For your connected-strip sequence, pilots and repeated supply.
Review progressive tooling →FOR YOUR STAMPING PROGRAM
Resolve these inputs early so the quote addresses the part and equipment you will actually use.
Grade, condition, thickness, width and supply basis.
Pitch, carriers, pilots and station sequence.
Bed, shut height, stroke, feed and available capacity.
Part results plus strip and process evidence.
Replaceable components, care and ownership.
FOR YOUR STAMPING PROGRAM
A tool price is useful only when the operation, trial and delivery scope match.
Align the part model, drawing and tool concept before manufacture.
Confirm the press, handling and relevant feed interfaces.
Identify datums, sample quantity, burr, geometry and fit checks.
Separate tooling, trial stock, corrections, spares, production and freight.
FOR YOUR STAMPING PROGRAM
Specify the operation and deliverables, then compare suppliers on the same basis.
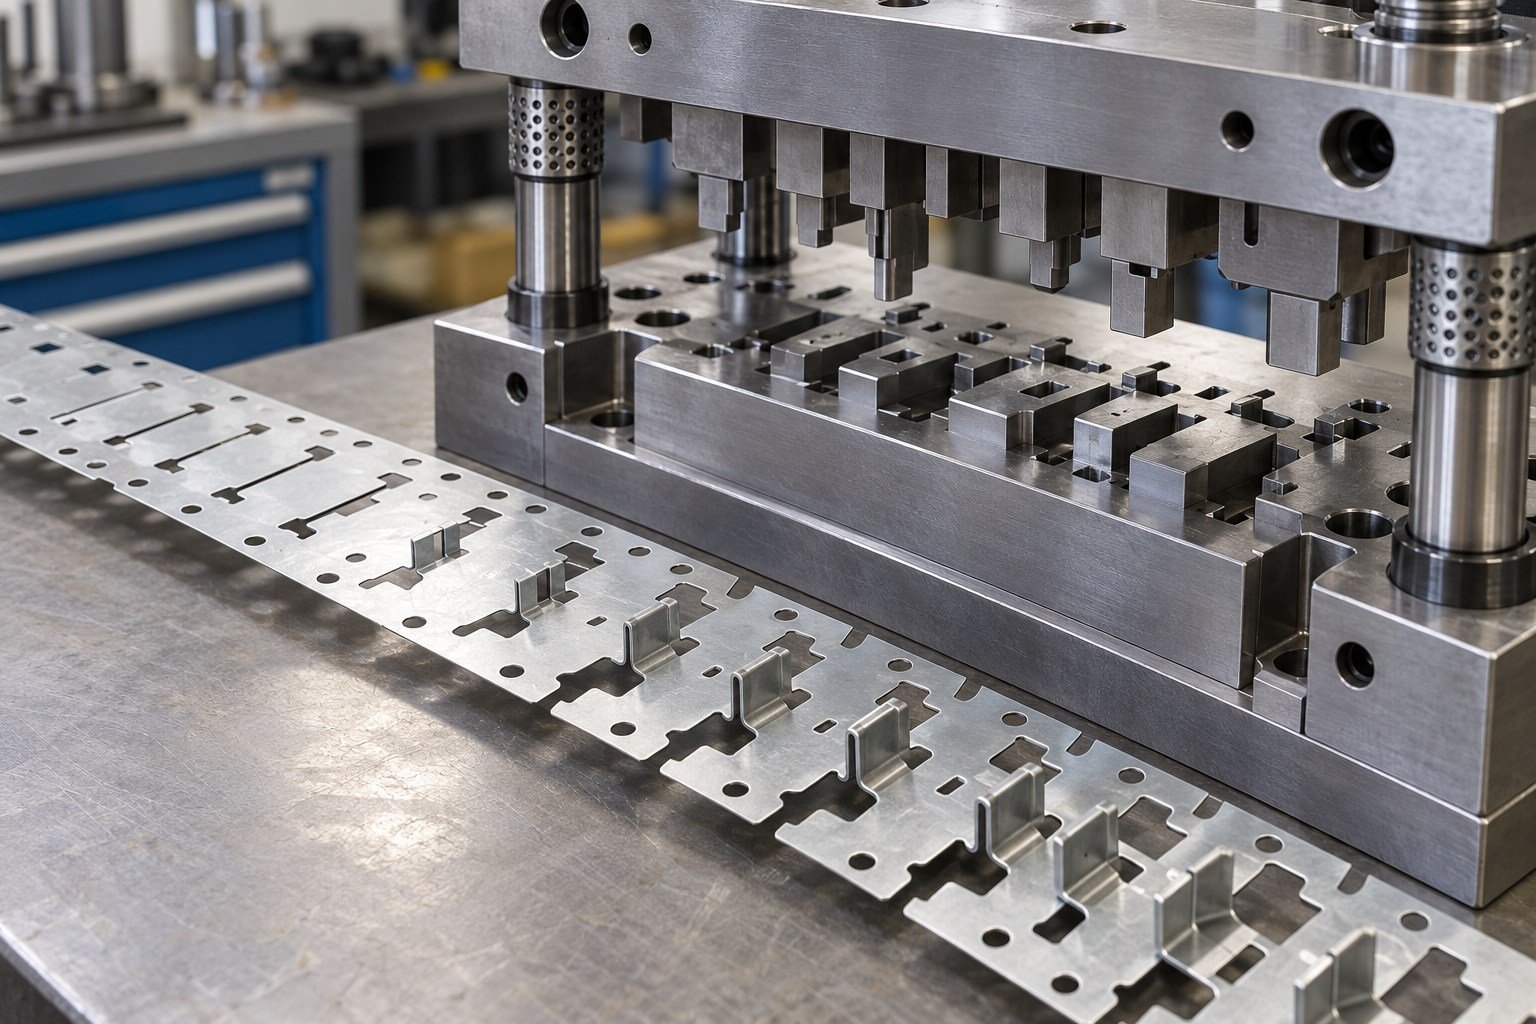
Plan how each feature develops while the part stays supported.
Review this tooling scope ↓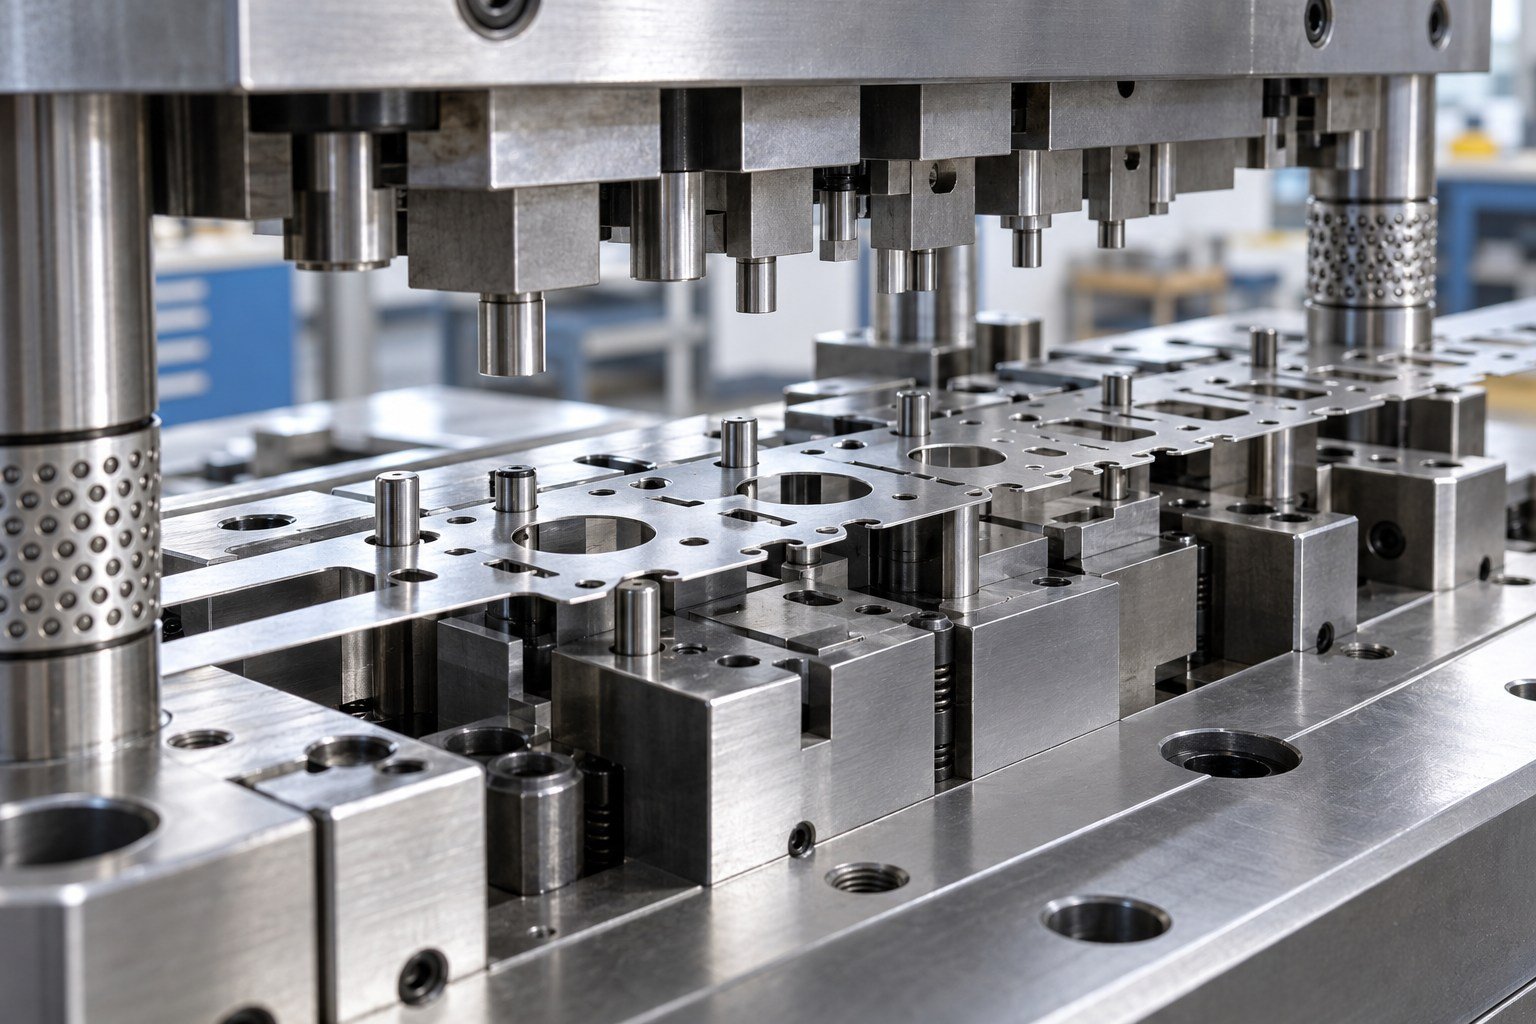
Connect feed progression to the strip features used for final location.
Review this tooling scope ↓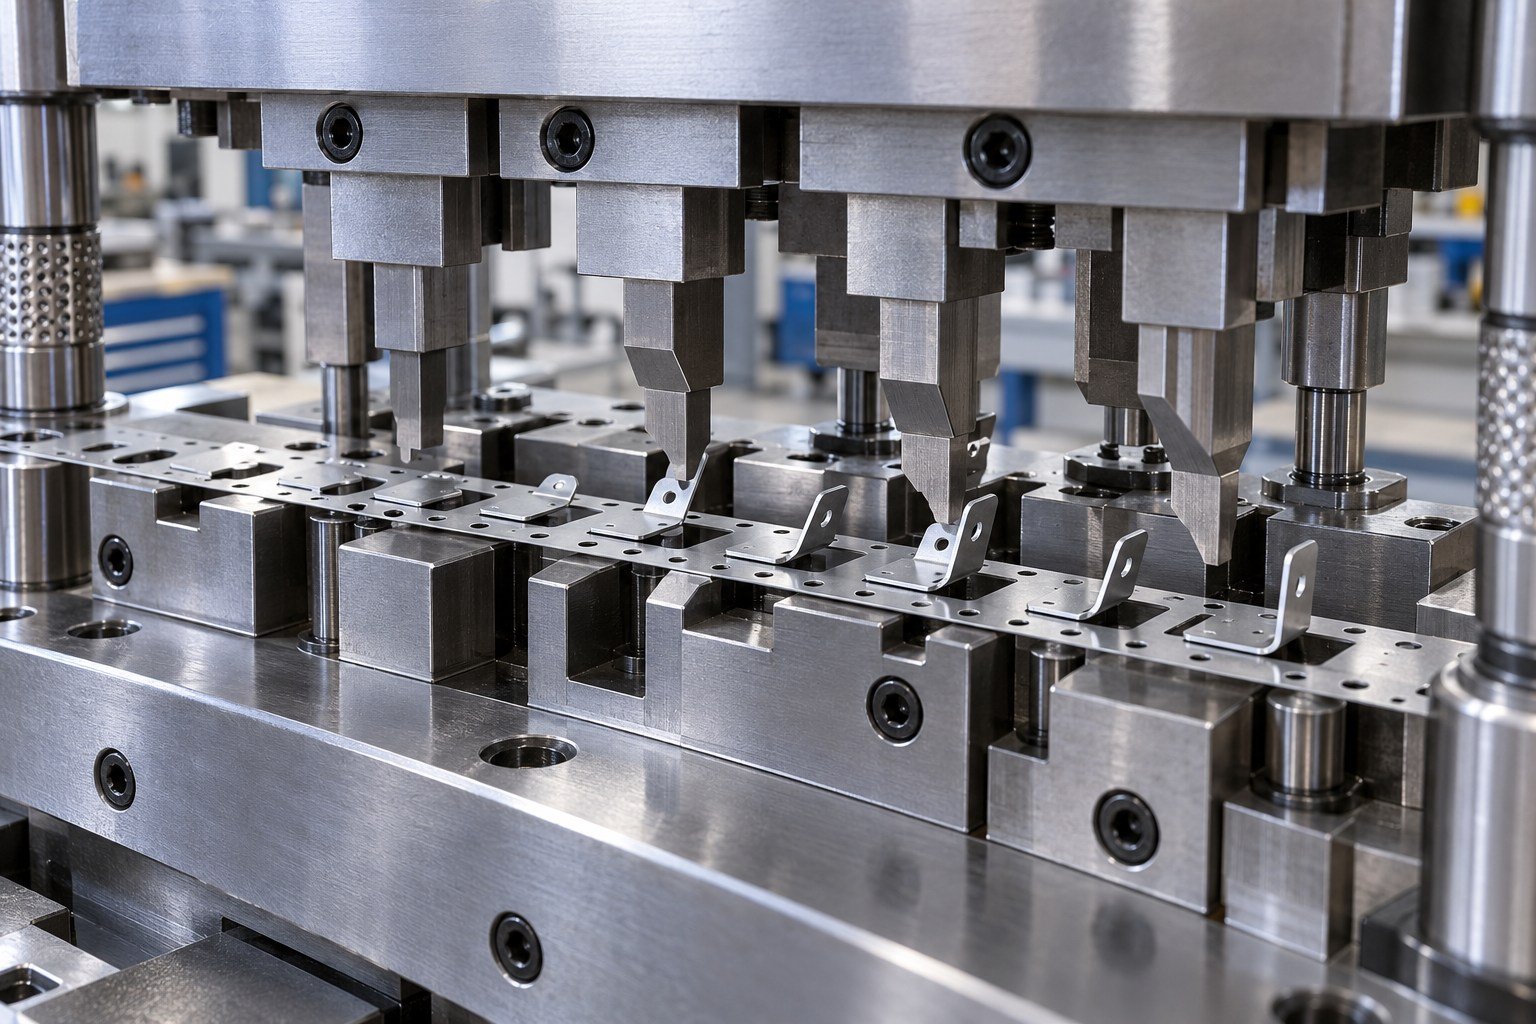
Review staged bends, stripping, clearance and final separation.
Review this tooling scope ↓FOR YOUR STAMPING PROGRAM
Design, manufacture, tryout, corrections and delivery are separate schedule items.
Share the controlled part, stock specification, quantities and receiving-equipment data.
Resolve location, work sequence, stripping, removal and machine interfaces before cutting the tool.
Define material, treatment, machining, purchased components and assembly checks. Approve substitutions.
Use the agreed stock and equipment basis. Identify samples and record relevant trial observations.
Assign cause review, correction scope, cost responsibility and the next sample requirement.
Confirm the tool revision, records, spares, preservation, ownership and receiving requirements.
FOR YOUR STAMPING PROGRAM
Stock names, tool-steel names and press capacity are different inputs; record each clearly.
Use the actual alloy, temper or condition.
State nominal thickness and the agreed variation.
Identify grain direction and protected faces.
Confirm discrete blanks or coil and strip requirements.
Select the grade for stock, geometry, wear and service duty.
Define heat treatment and verification as quoted.
Identify replaceable punches, dies, pilots or inserts.
Agree material identification and available evidence.
Die footprint, fastening and access.
Shut height, stroke and opening requirements.
Evaluate the operation and press characteristics.
Part, slug, scrap and handling interfaces.
Define visible faces and permitted tool witness marks.
Agree the trial and production basis.
Define service and adjustment allowances.
Identify preservation and maintenance responsibility.
FOR YOUR STAMPING PROGRAM
Agree the relevant input, design decision and check for each operation.
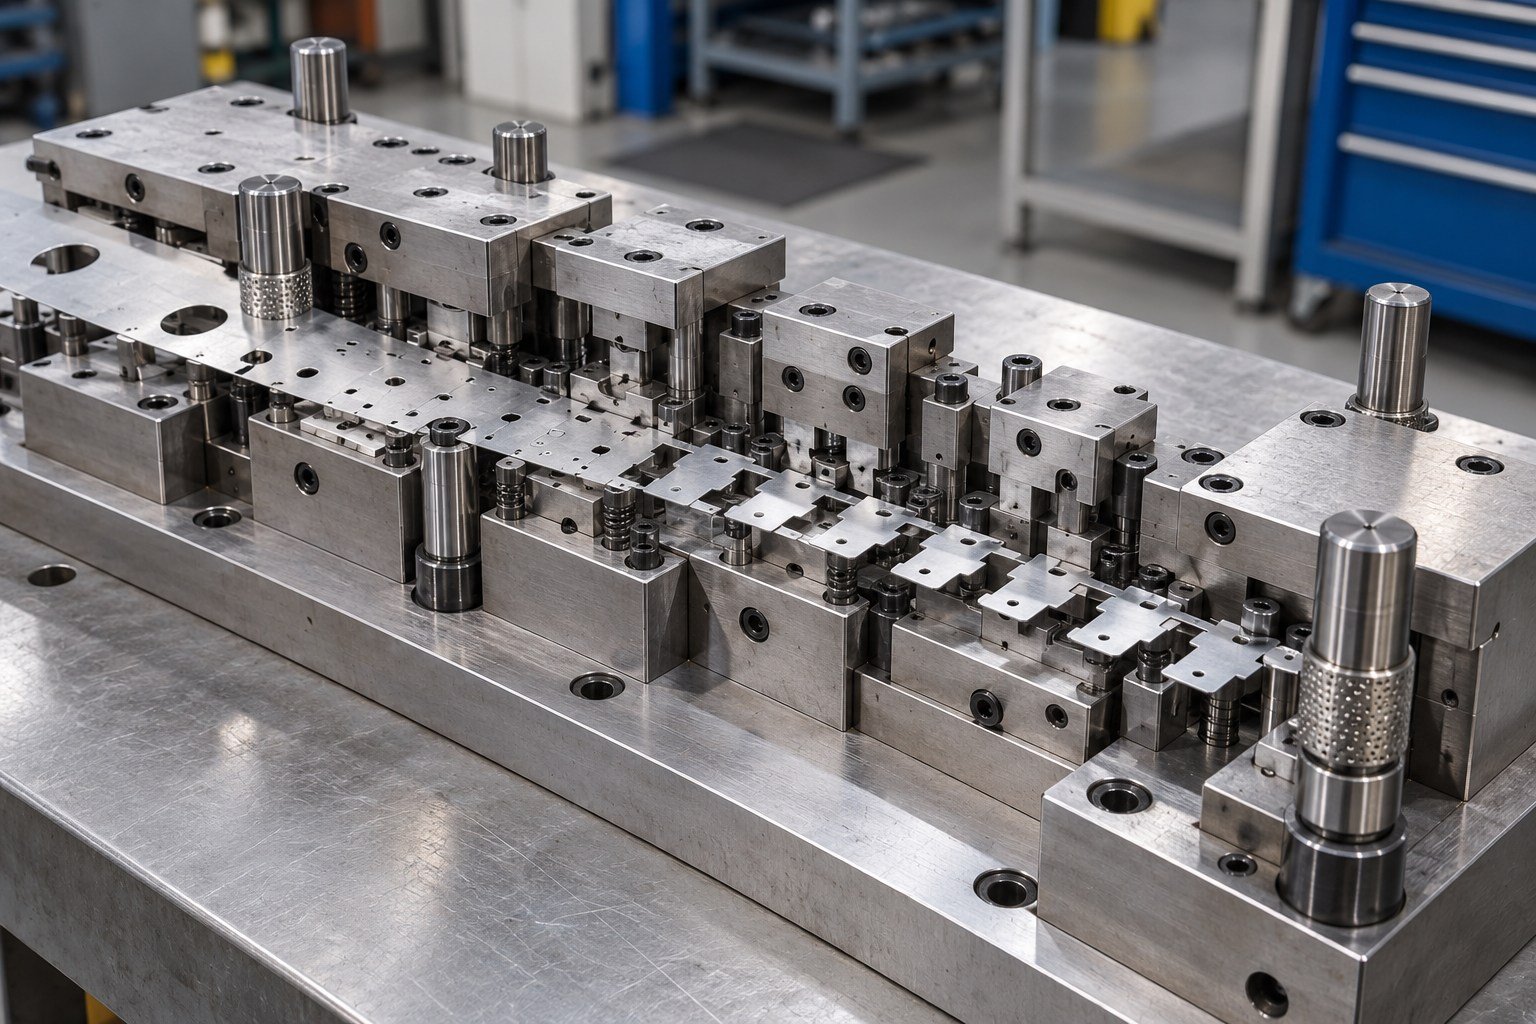
A strip layout links part orientation, pitch, carrier design, stations and scrap. Review the entire sequence, not a single isolated feature.
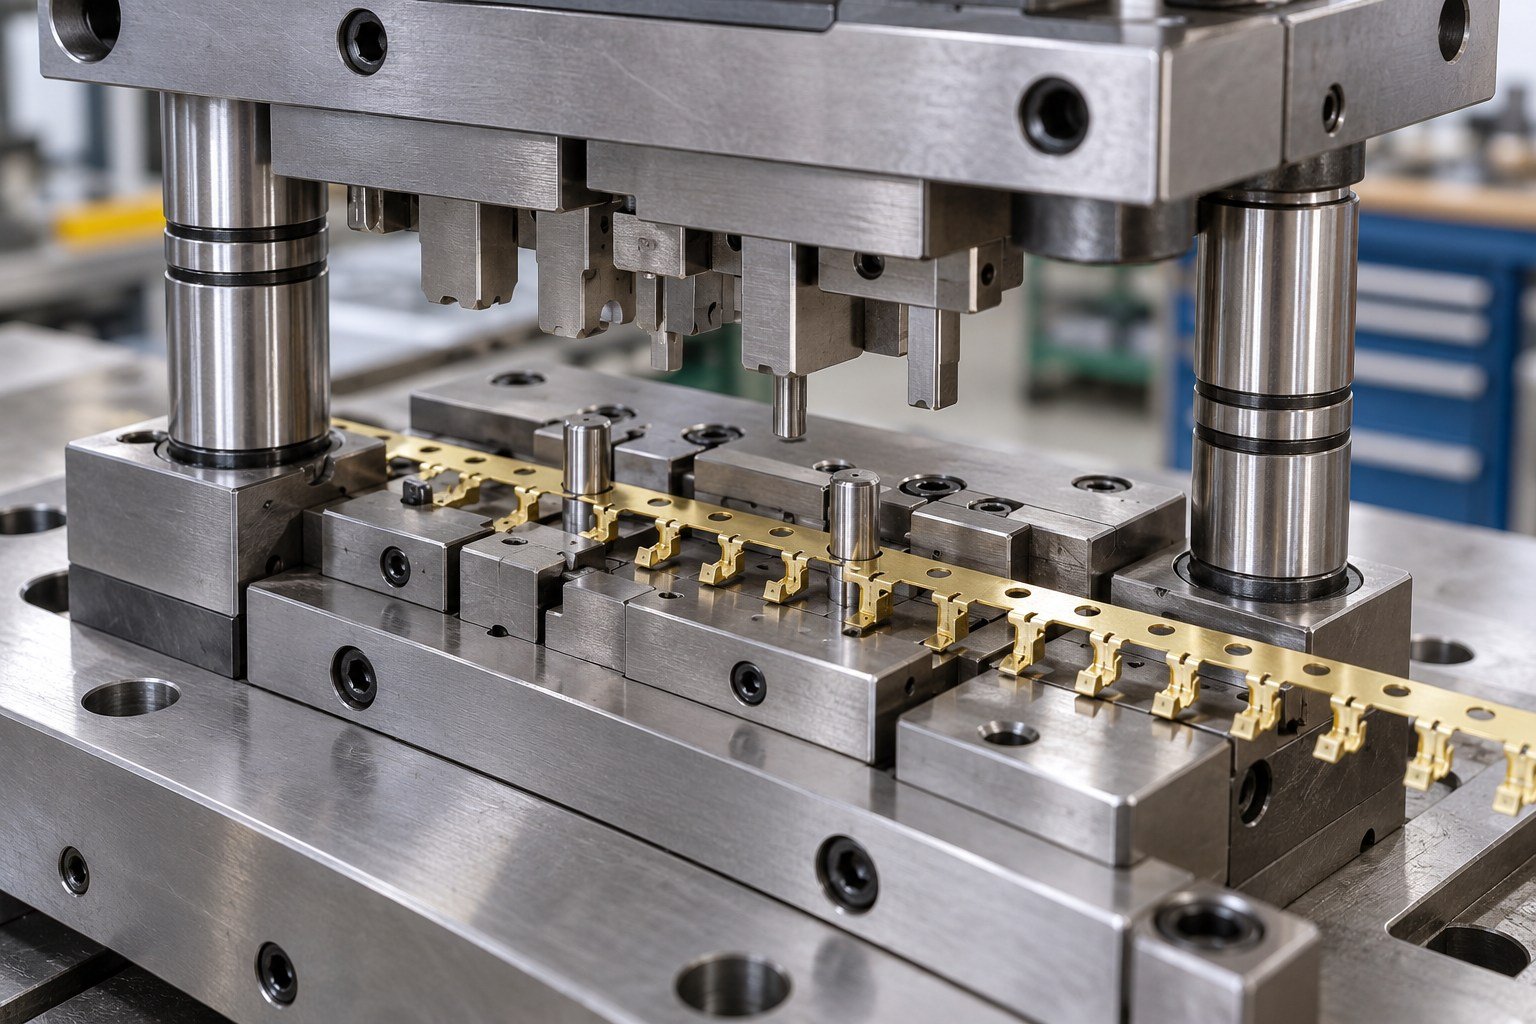
Feeding advances the strip; pilots locate the strip at the agreed points in the cycle. Review their interaction with the press and feeder.
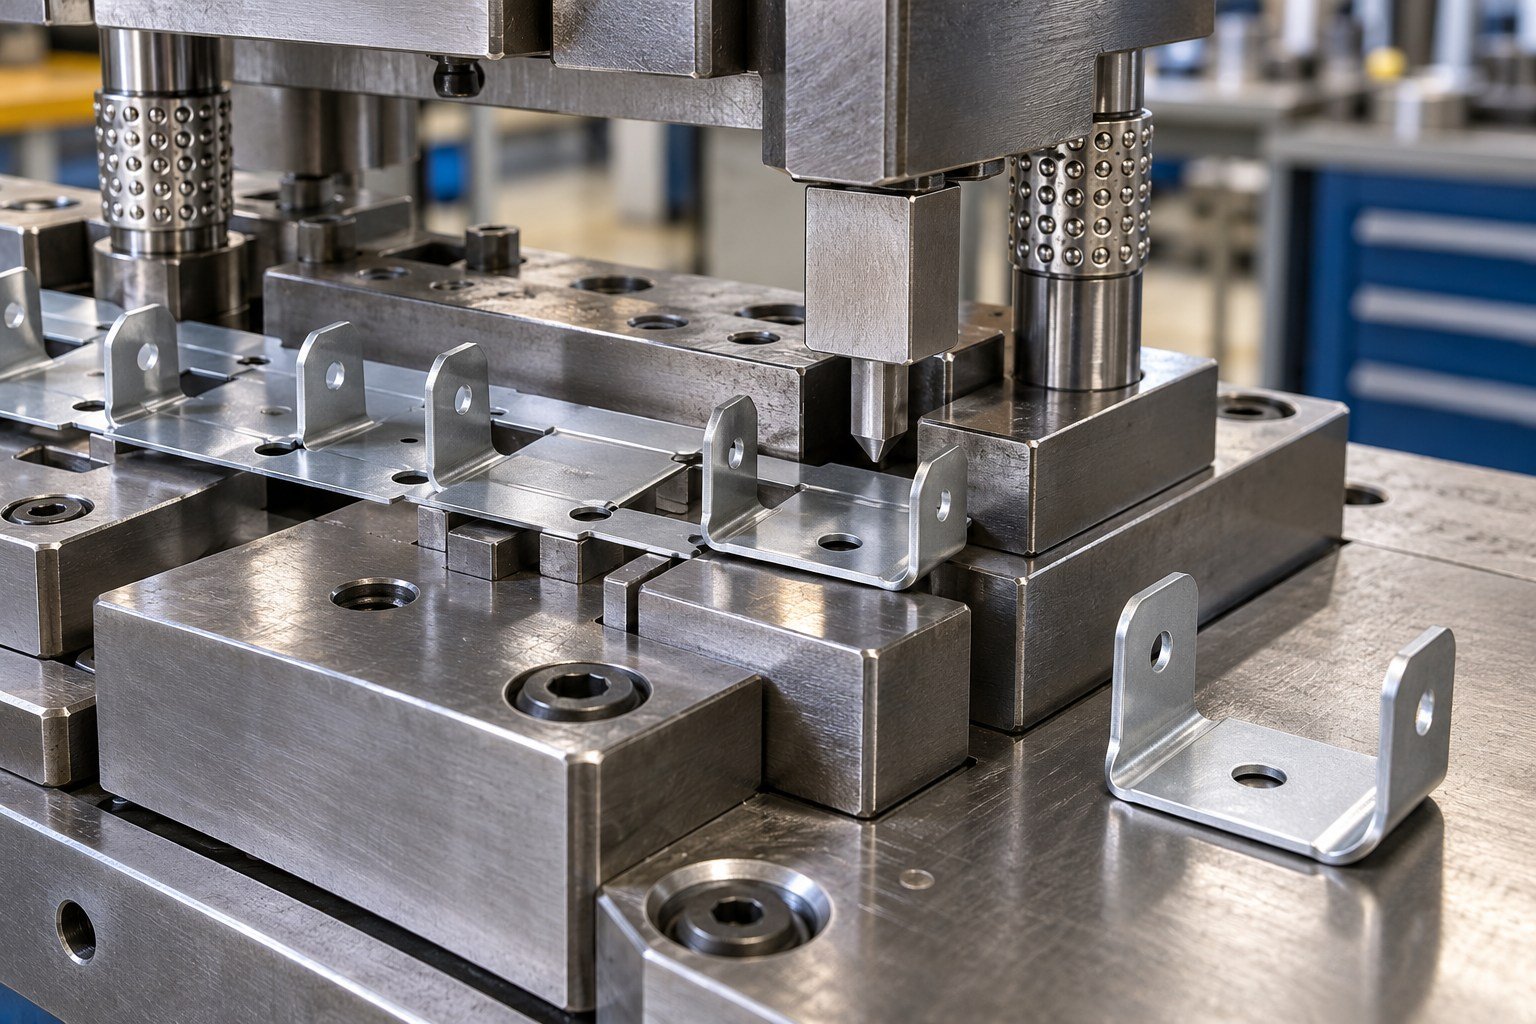
Keep the partly formed part supported until the agreed release operation. Confirm how the finished part and scrap leave the tool.
FOR YOUR STAMPING PROGRAM
Your finished-part drawing, strip development and die concept must describe the same controlled route.
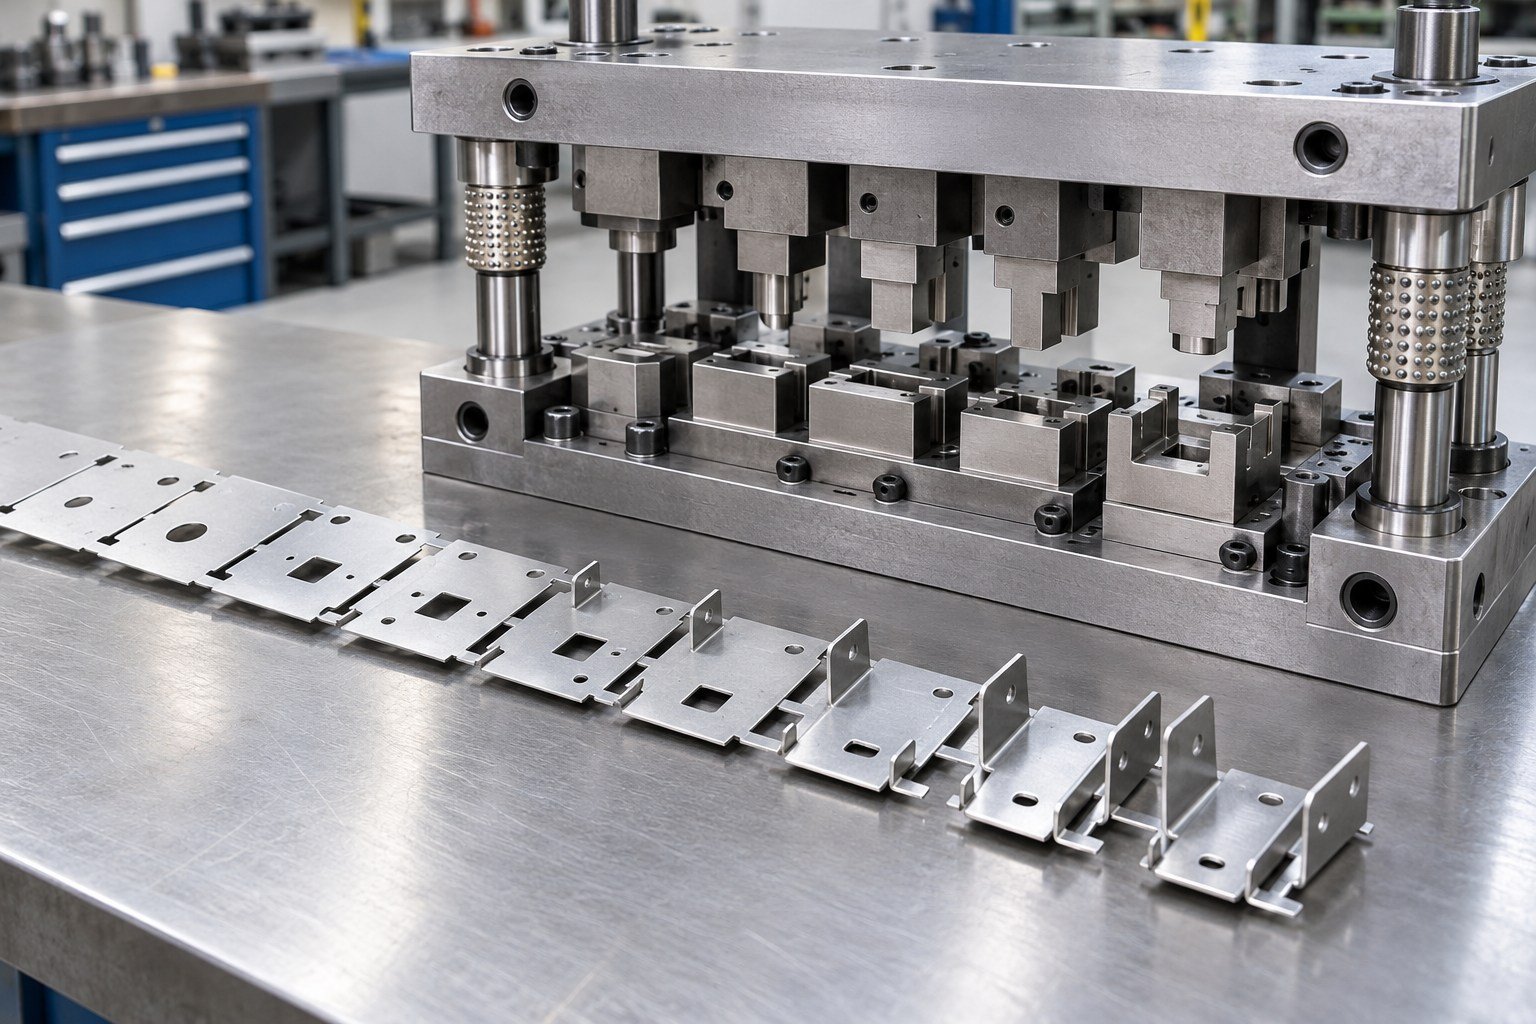
Record these decisions on controlled documents so later operations use the same basis.
FOR YOUR STAMPING PROGRAM
Resolve the features that control cutting, location, forming and repeat use; avoid one-size-fits-all promises.
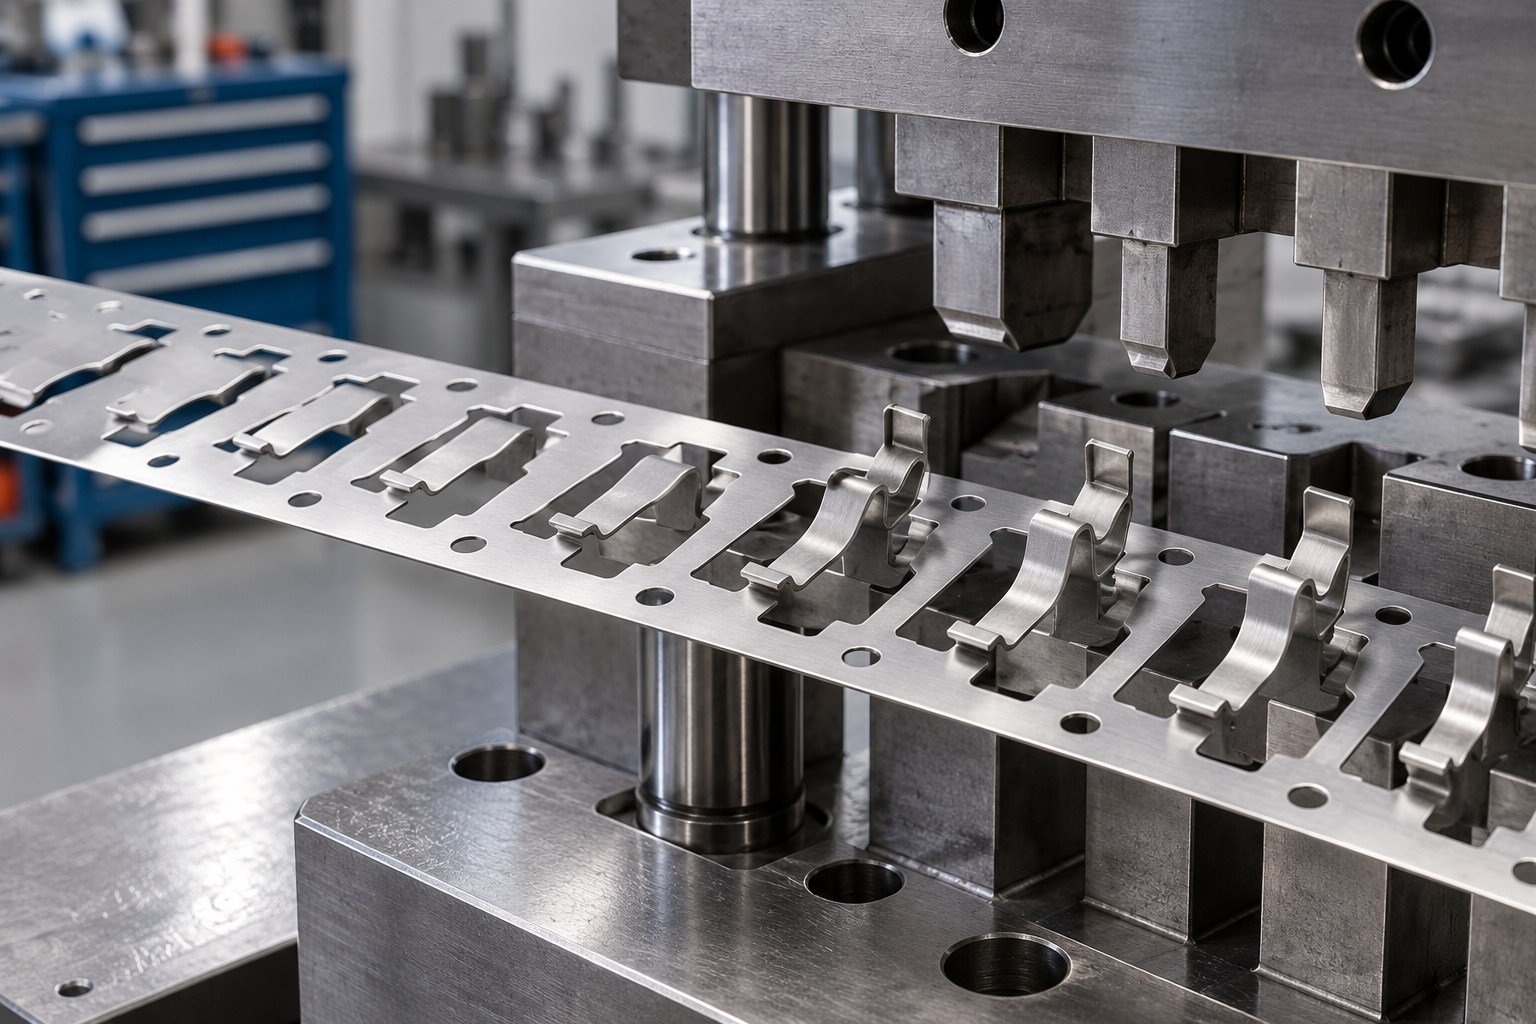
A carrier must maintain the agreed location and support as the part is pierced and formed.
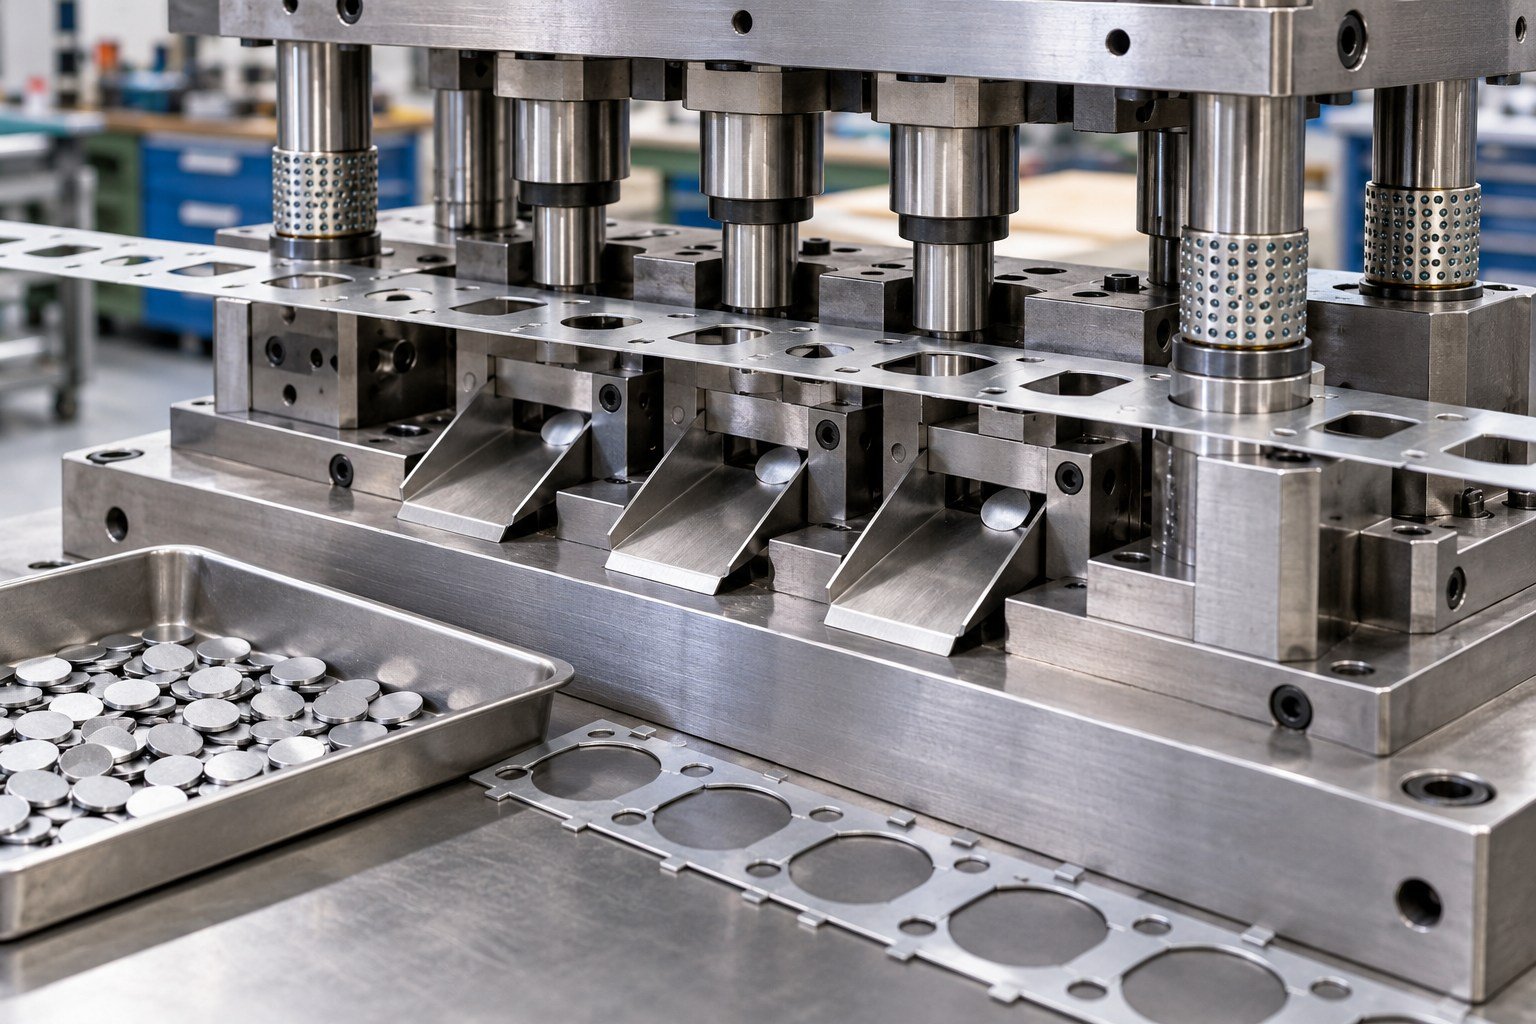
Review slug control, scrap chutes and strip-skeleton removal with the die and press layout.
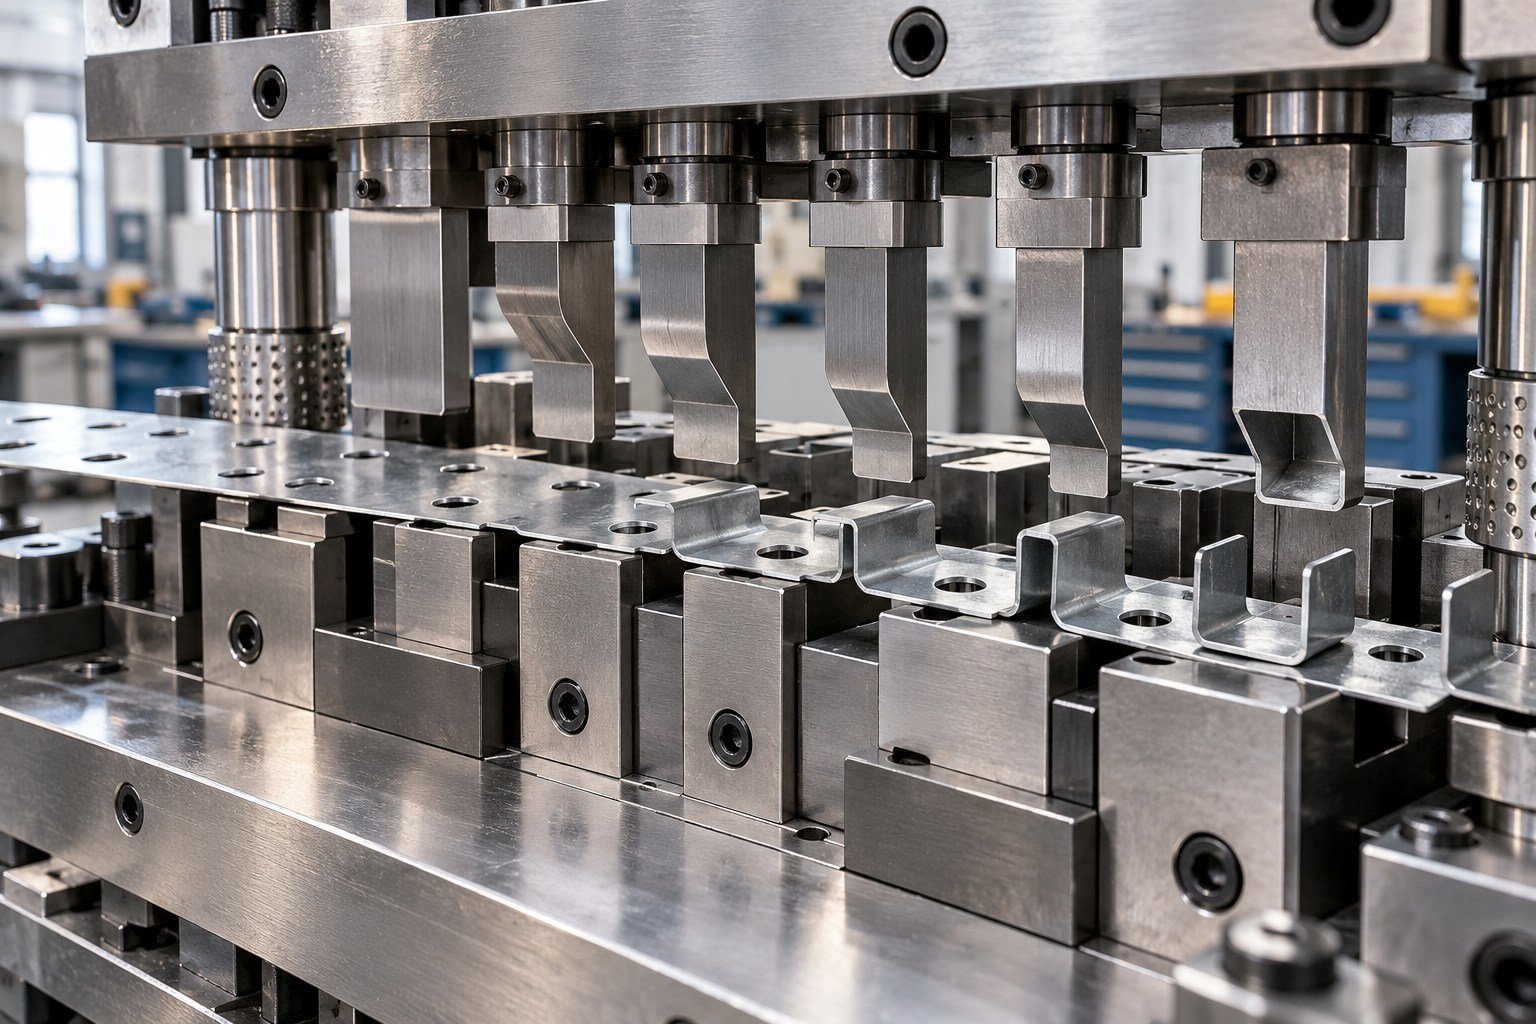
Later stations need room for punches, strips and already formed features.
FOR YOUR STAMPING PROGRAM
Define condition, compatibility and reapproval before committing to work.
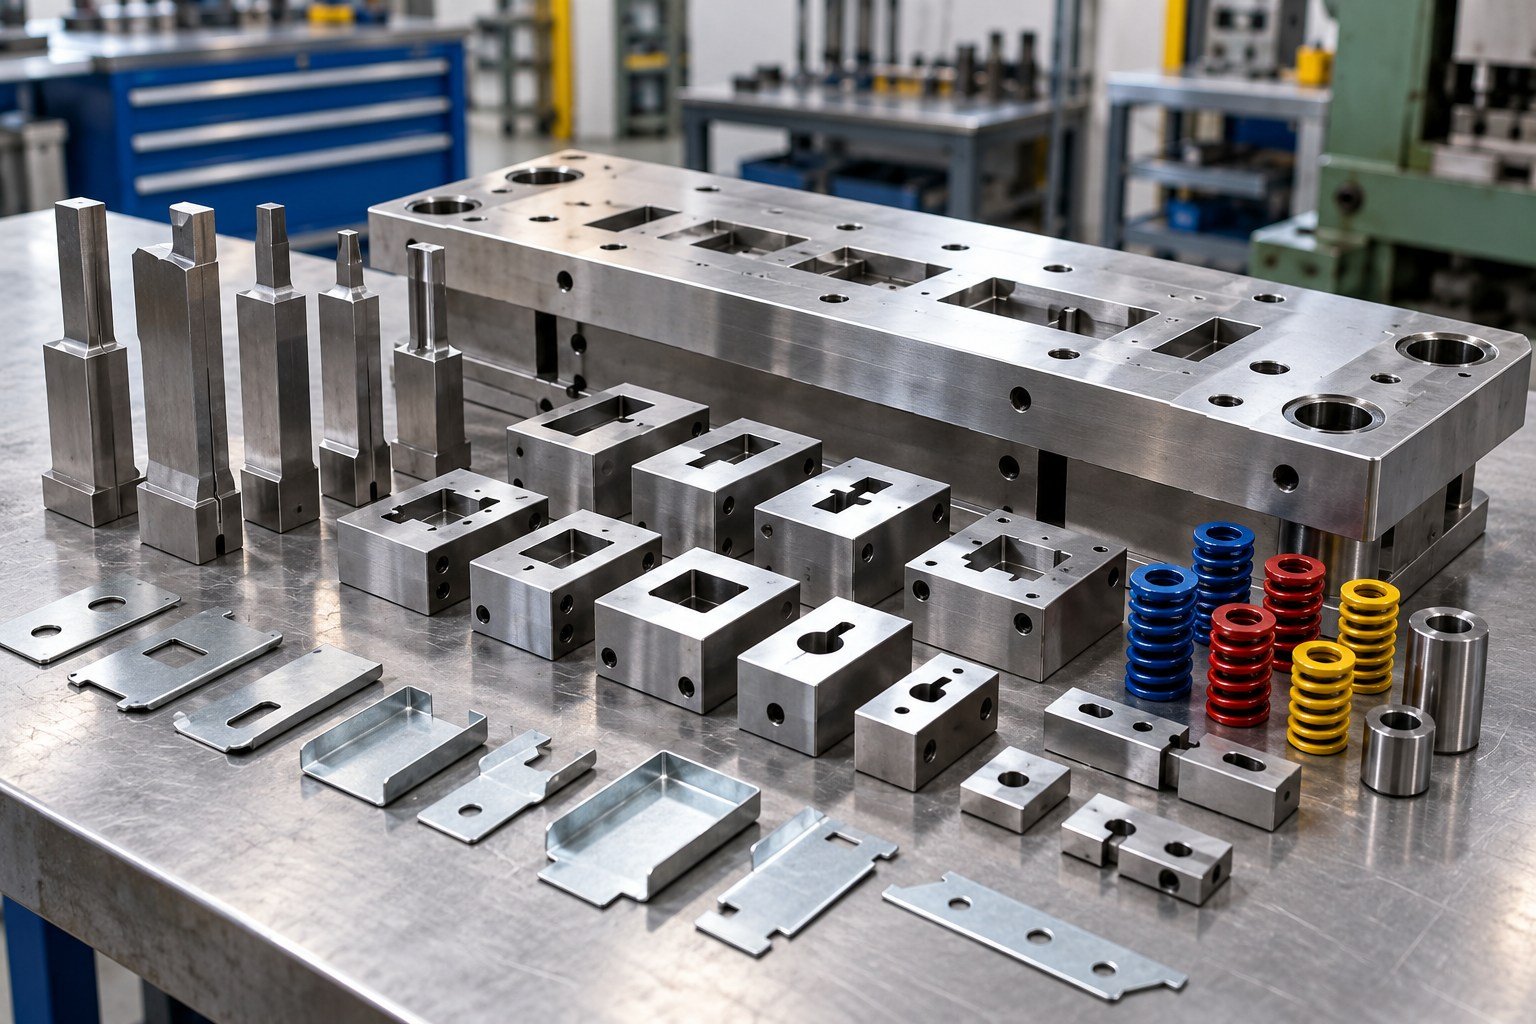
A maintenance plan should identify the components most likely to need sharpening, replacement or adjustment.
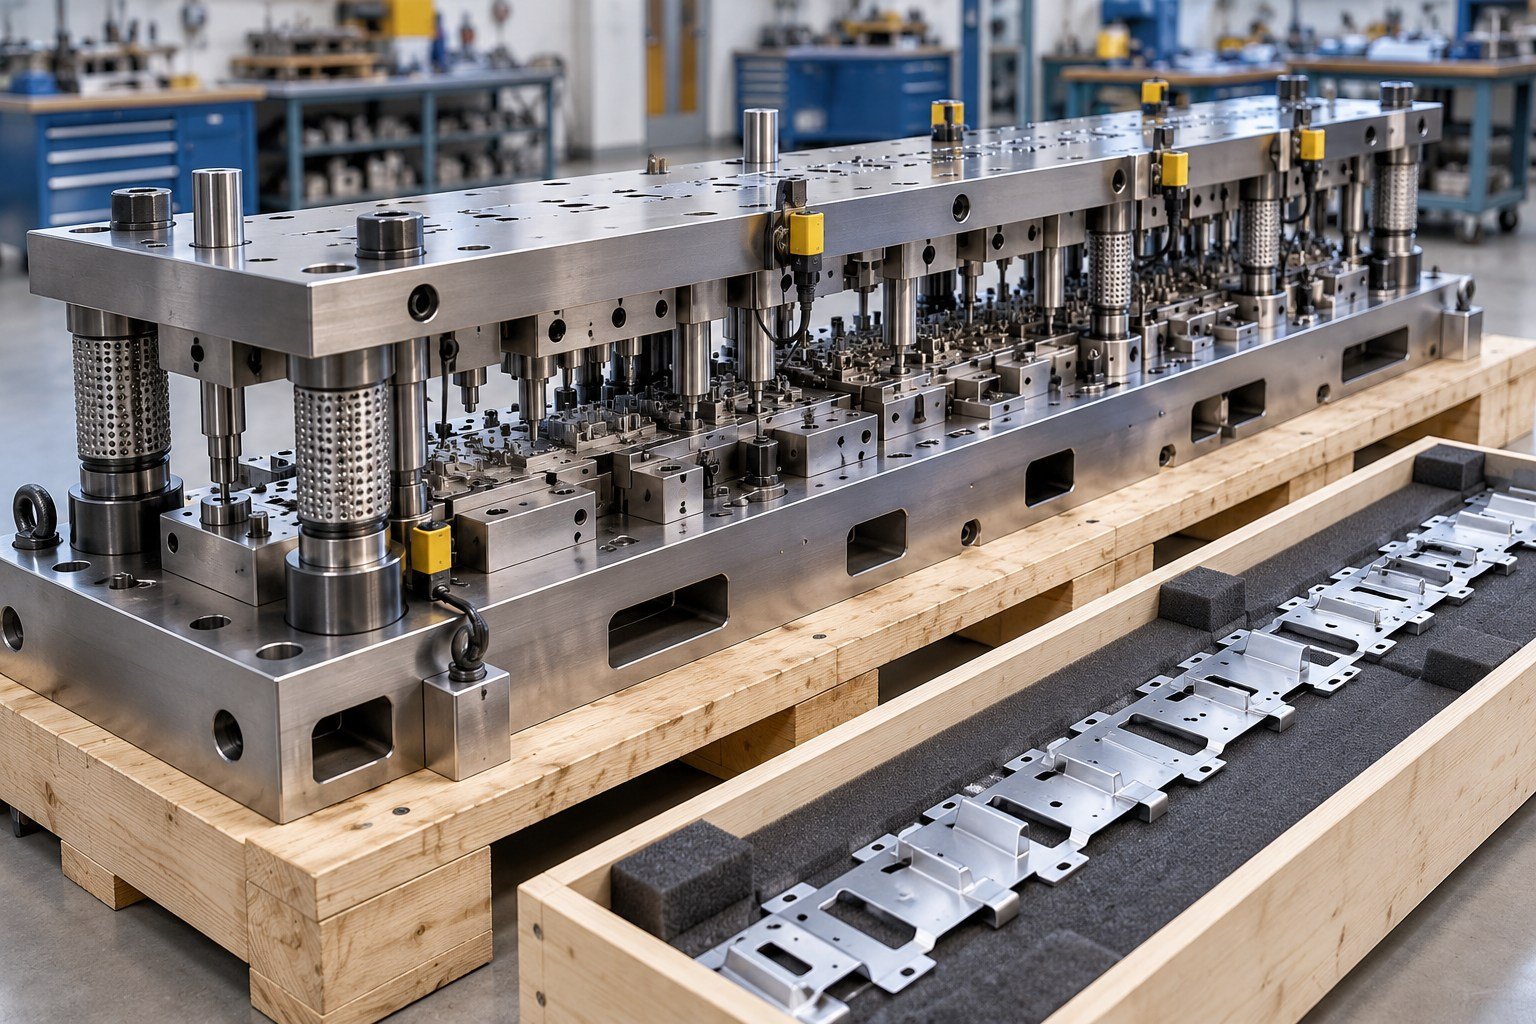
A tool transfer needs press, feed, part and scrap-interface review before shipment.
FOR YOUR STAMPING PROGRAM
Verify the working tool and the produced part as related but separate evidence.
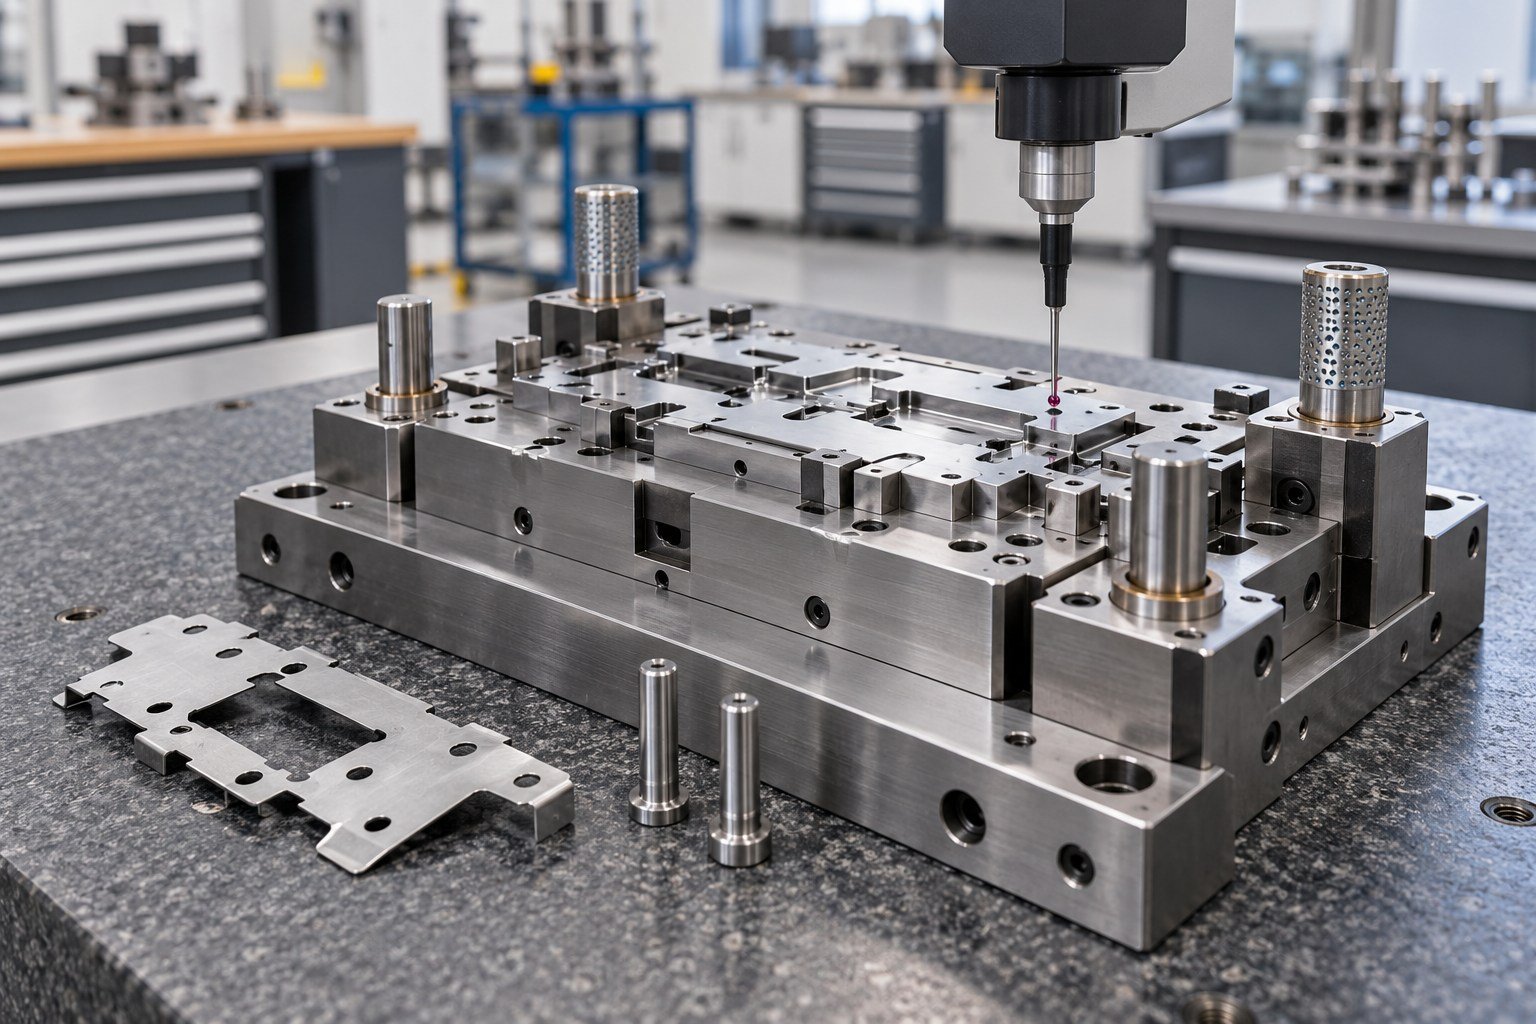
Check the agreed component and interface features against the approved tool design.
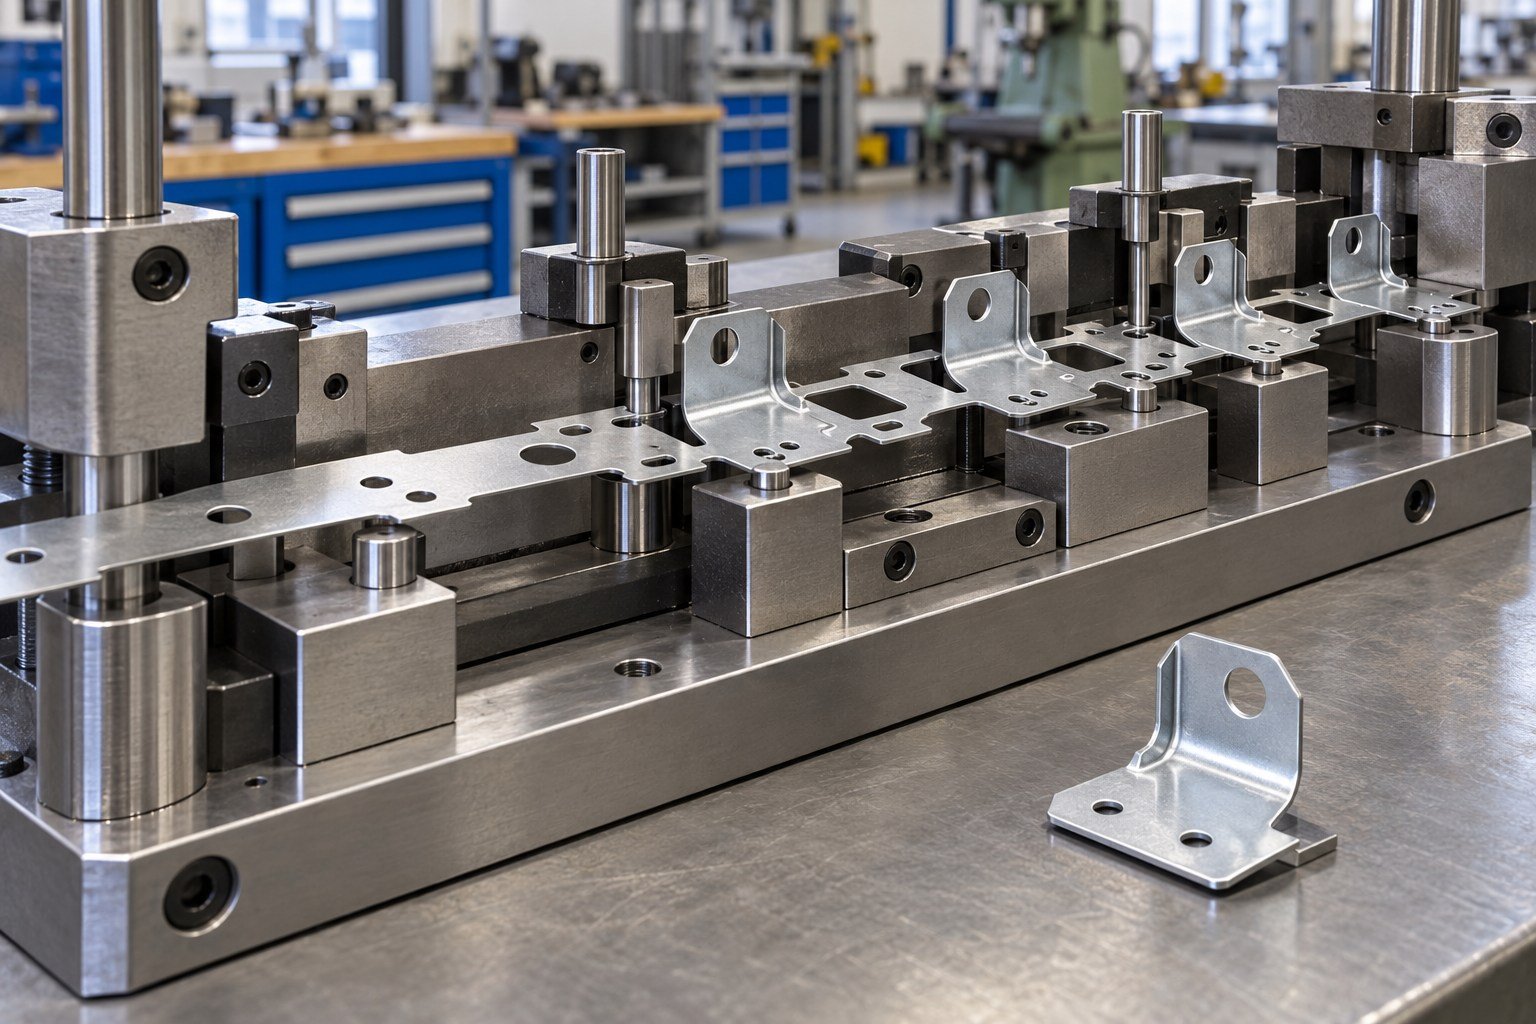
A progressive die tryout should document both the process route and the parts it produces.
FOR YOUR STAMPING PROGRAM
Agree availability, scope and responsibilities. Images illustrate tooling concepts, not customer reports.
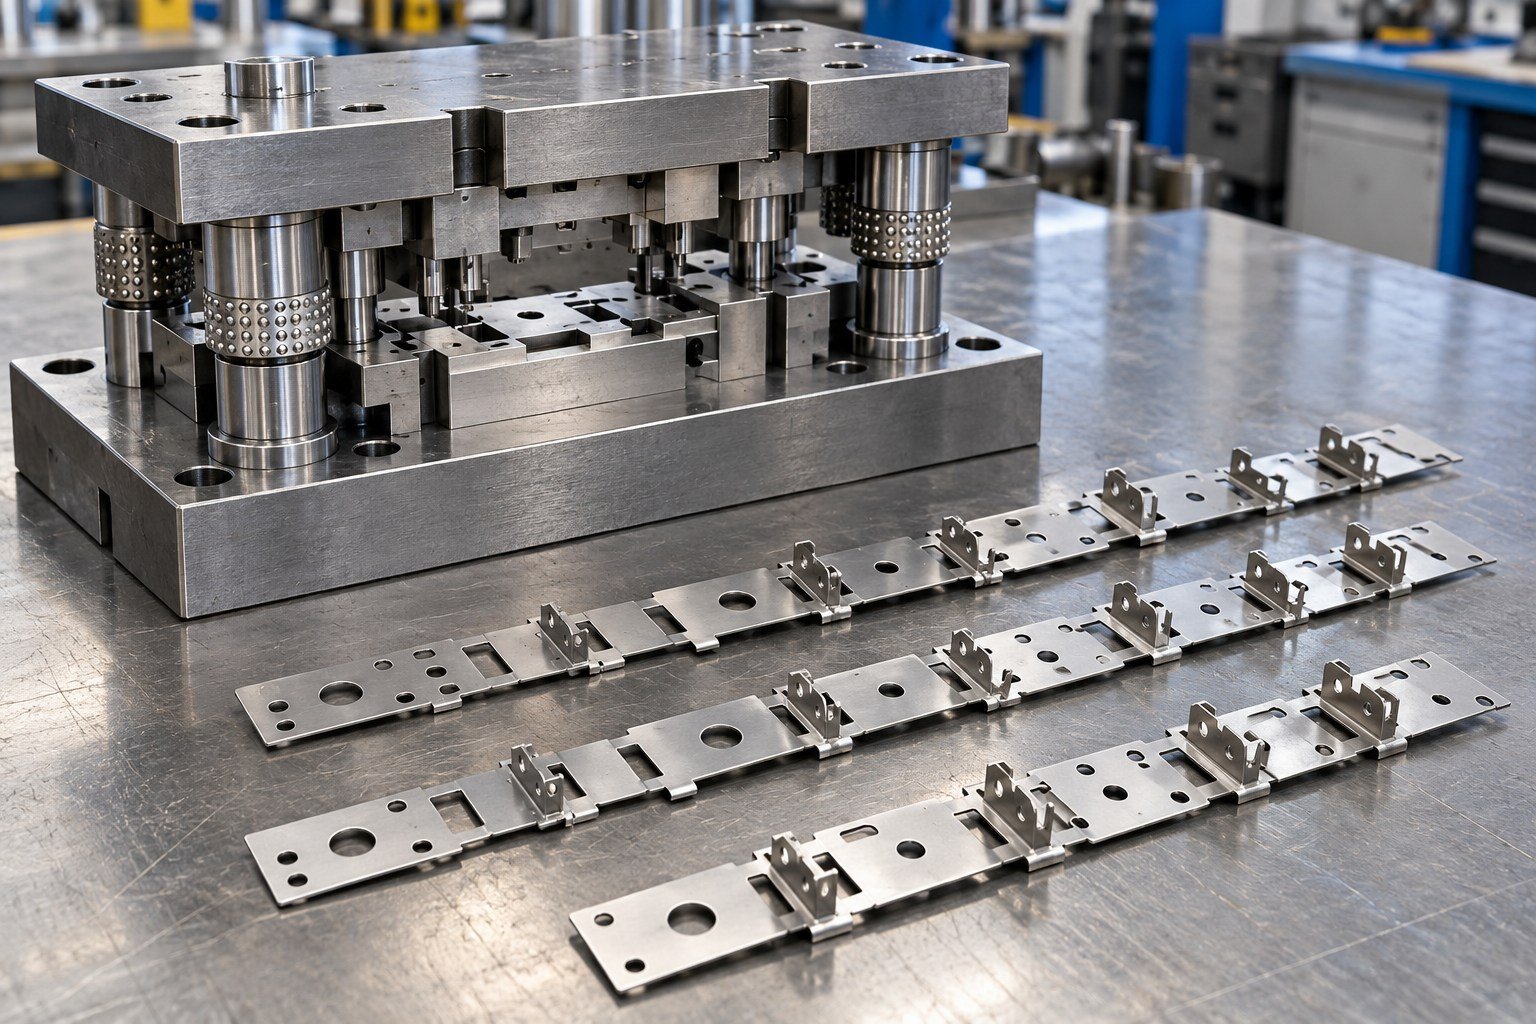
Link trial evidence to the controlled tool and strip design.
Planning checklist only; not an issued customer or inspection record.
Agree reviewer, evidence, open actions and release responsibility.
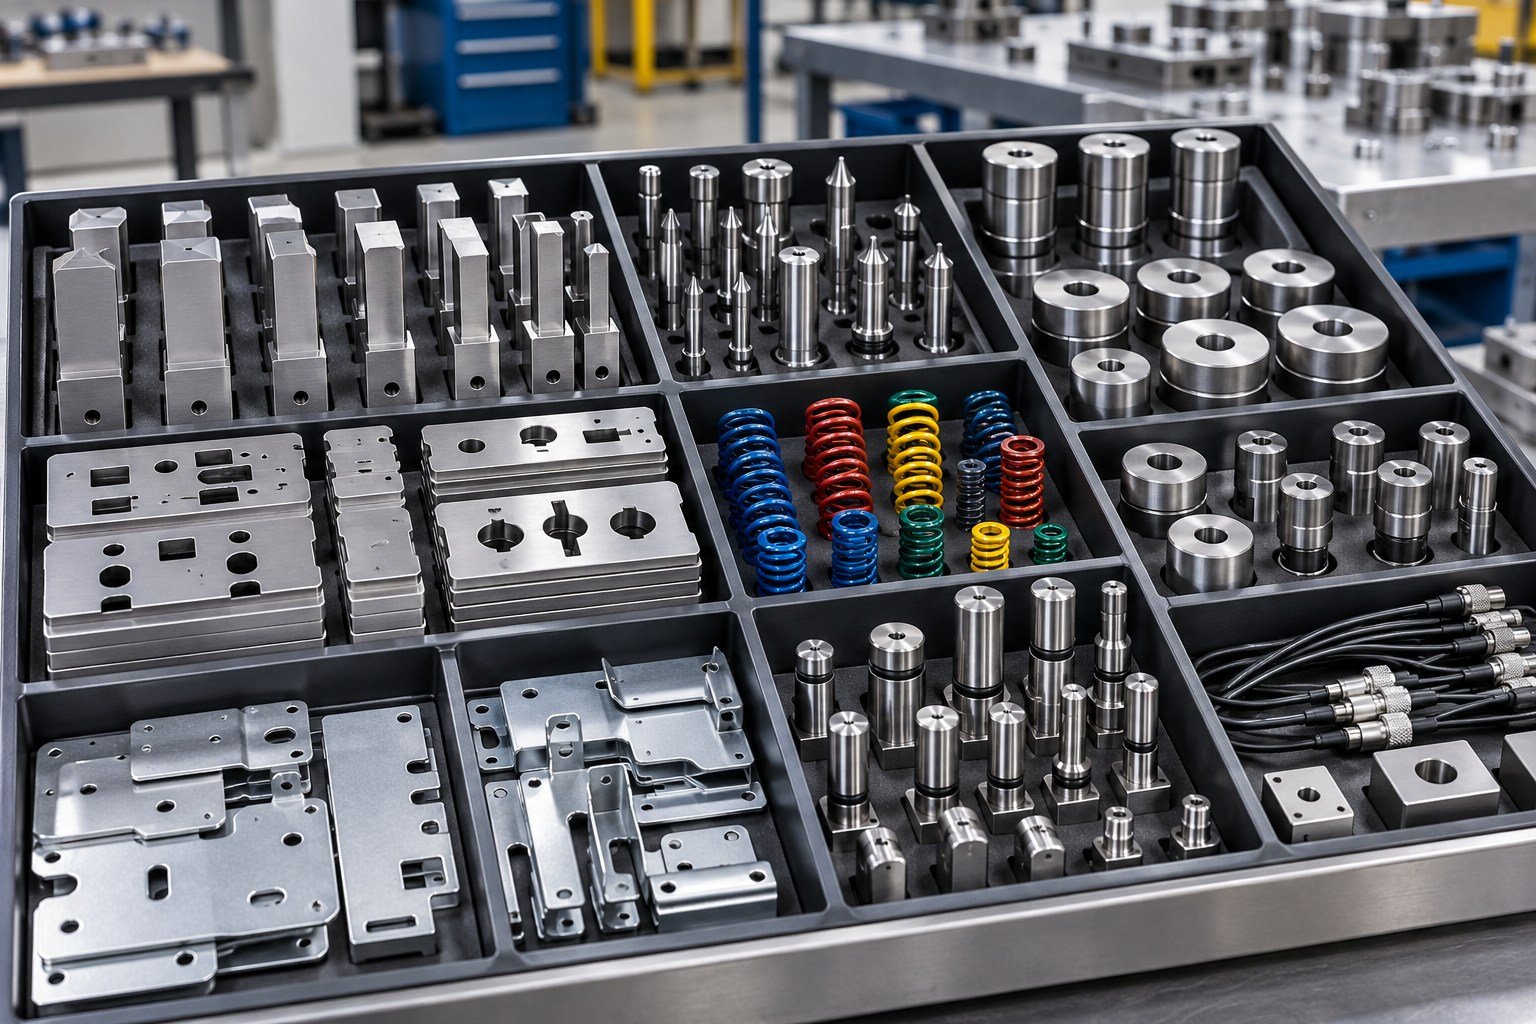
Make the supplied die, components and records checkable.
Planning checklist only; not an issued customer or inspection record.
Agree reviewer, evidence, open actions and release responsibility.
FOR YOUR STAMPING PROGRAM
An industry name does not establish qualification. Define the actual function and acceptance.
Mounting holes, flange geometry and assembly datums.
Small features, burr direction and finish.
Customer validation and traceability requirements.
Repeat location and mating-part fit.
Visible faces, formed edges and hardware interfaces.
Appearance, handling and service conditions.
FOR YOUR STAMPING PROGRAM
China manufacturing and Dallas-area coordination connect drawing questions, trial decisions and delivery planning.
Record tool identification, title, permitted use and retrieval conditions.
Define inspections, sharpening, replacement parts and authorization.
Agree drawings, component IDs and revision information supplied.
Plan spares, preservation, receiving trials and future changes.
FOR YOUR STAMPING PROGRAM
Use these questions to define your actual purchase and approval scope.
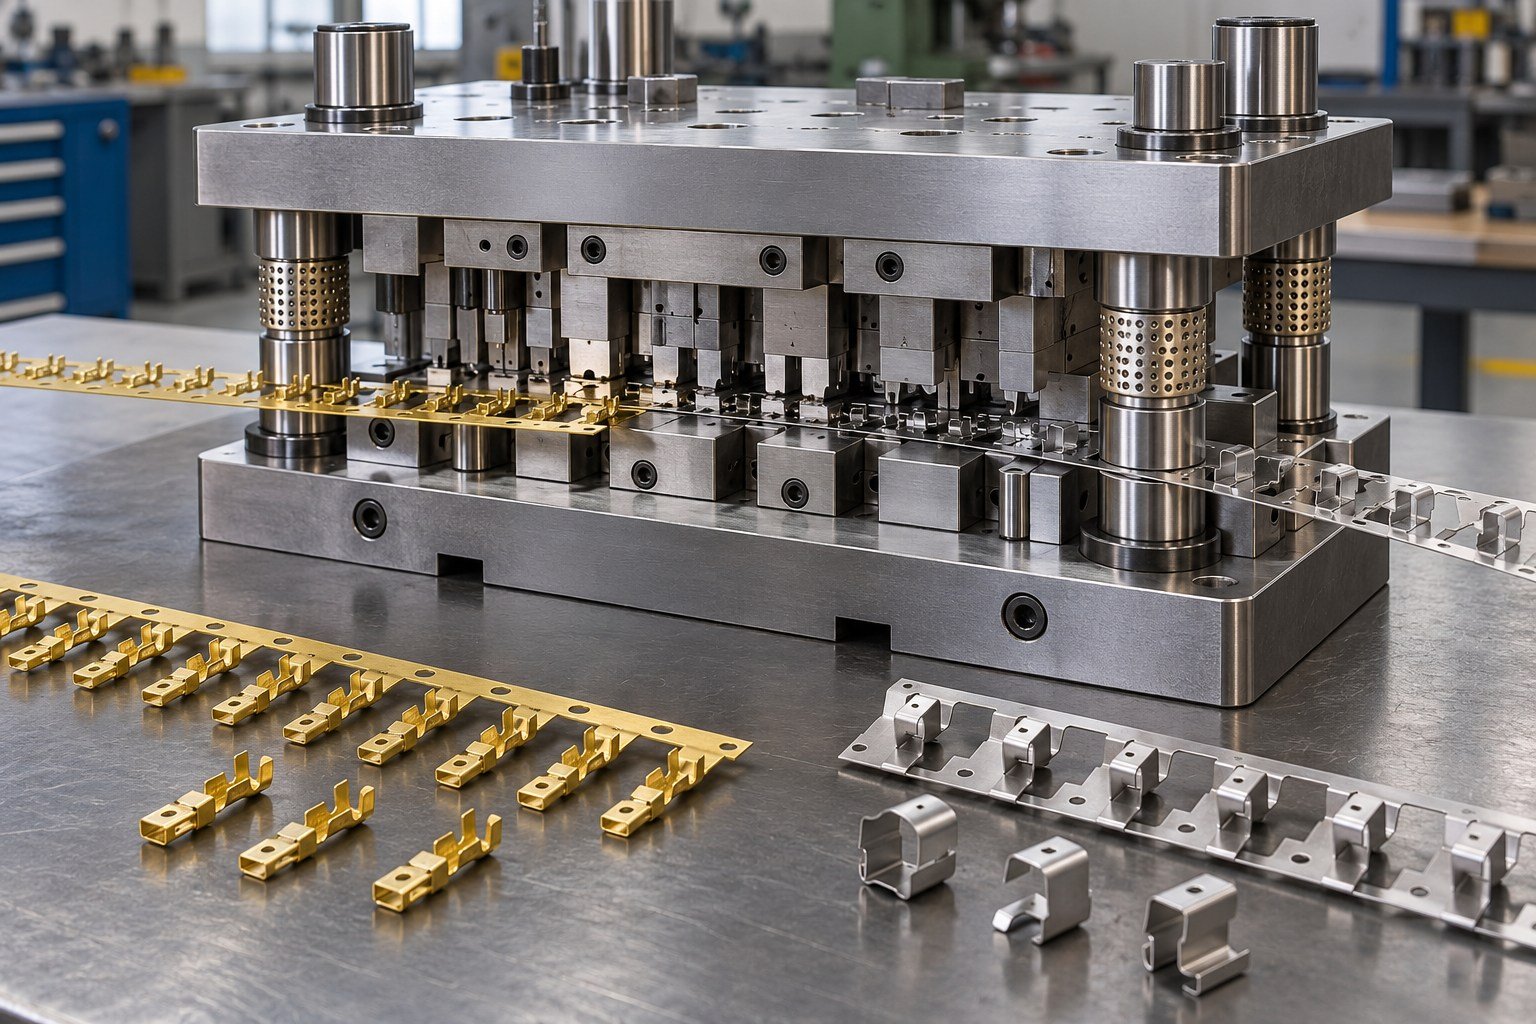
A progressive die combines sequential cutting or forming stations. A connected strip advances by the specified pitch, with different work performed at different stations. The finished part is released at the agreed cut-off stage; it does not complete every operation at one position in a single stroke.
Compare demand, product stability, stock format, handling, required equipment and the total quoted program cost. Progressive tooling can integrate a repeated sequence, while single-station tooling can support discrete or secondary operations. Do not choose on annual quantity alone.
Define part orientation, pitch, carriers, pilots, station work, intermediate forms, scrap and final separation. Review support and access at each stage. Agree which layout, analysis and approval documents are included in the tooling quotation.
No. The feeder advances the strip; pilots use defined strip features to establish location at the required point in the cycle. Their timing and interaction need review with the die, press and feed equipment.
Size, station count and work, stock, forming complexity, bought-in components, protection, trials, inspection, corrections, spares and delivery affect the quote. Compare the same build and approval scope rather than a universal price or savings percentage.
Separate design approval, material and purchased components, machining, treatment, assembly, tryout, corrections and transport. Confirm customer review time and receiving-press readiness. A schedule starts from agreed inputs and release conditions.
Provide controlled CAD and a part drawing, stock grade and thickness, critical features, appearance and burr requirements, quantities and the receiving press/feed-line data. Share any existing strip layout, trial samples and known issues. Request an NDA for confidential material.
Review geometry, sequence, carriers and output mix. Interchangeable or adjustable details may support agreed variants, but they need identification and separate approval. A shared die base does not automatically make the strip routes compatible.
Agree how strip progression, location, support, scrap, finished dimensions and appearance will be checked. Identify samples and relevant conditions. Close or disposition deviations; completing a trial does not automatically approve repeated production.
Specify the required sensing, interfaces, responsibilities and validation in the quotation. Avoid assuming protection is included or that a generic sensor list covers your press and feed line. Machine and tool safety require the applicable operating procedures and review.
Check mounting, bed, shut height, stroke, feed direction and capability, strip and scrap handling, controls and protection interfaces. Agree receiving-trial responsibilities and available records before moving the tool.
Record ownership, permitted use, drawings, storage, service authorization, spares, retrieval and replacement conditions. Keep recurring stamping production charges separate from tool purchase and maintenance terms.
FOR YOUR STAMPING PROGRAM
Keep the tooling purchase separate from recurring part-production charges.
Operation, layout and approved revisions.
Die set, punches, inserts and bought-in parts.
Press, feed, handling and scrap interfaces.
Stock, sample quantities and trial conditions.
Datums, measurements, edge and fit checks.
Responsibility, charges and repeat sampling.
Drawings, service, storage and retrieval.
Spares, preservation, packing and receiving trial.





