

Injection Molding
Tooling and molding for your repeat plastic parts.
From prototype to production, coordinated manufacturing solutions for your custom parts.
View All Services →
Precision parts for your tight tolerances and complex geometry.
Tooling and molding for your repeat plastic parts.

Metal casting options for your part and production volume.

Cutting, forming and welding for your fabricated parts.

Custom profiles for your section, length and finish requirements.

Finishes for your appearance, corrosion and wear requirements.

Sub-assemblies and final builds for your production program.

Production tooling built around your process and volume.

Prototype parts to check fit, function and design.
DFM, process planning and production support for your project.
Inspection, documentation, inventory and delivery planning for your program.
Choose air- or liquid-cooling components around your thermal and mechanical requirements.

Manufacturing support for your cold plates, manifolds and cooling assemblies.

Find components for your power electronics, energy, laser and telecom application.

Components for your electronic systems.
Start with your functional and quality requirements.
Build around your operating environment.
From prototype to production, review material performance, manufacturability and cost for your part.
Review grade, temper and finish for your metal parts.
 AluminumStrength, weight and machining›
 Stainless SteelCorrosion and finish requirements›
 Carbon & Alloy SteelDiscuss grade and heat treatment›
 Tool SteelDiscuss tooling and wear needs›
 TitaniumReview grade and part geometry›
 Copper & Brass & BronzeDiscuss conductivity and machining›
Match your polymer to function, process and environment.
 ABSReview enclosure and molding needs›
 Polycarbonate (PC)Discuss clarity and impact needs›
 Nylon (PA)Review moisture and wear conditions›
 POM / AcetalReview fit and sliding features›
 PEEKDiscuss operating conditions›
 PTFEReview friction and chemical exposure›
 ULTEM / PEIDiscuss thermal and electrical needs›
Confirm grade availability and application requirements.
 Silicone / LSRDiscuss flexible component needs›
 TPU / TPEReview flexibility and processing›
 EPDMReview weathering and chemical exposure.›
 NBRReview oil and fuel exposure.›
 FKMReview temperature and chemical exposure.›
 G10 / FR4Review insulation and laminate needs›
 CompositesReview stiffness, weight and laminate.›Customer-Specified MaterialsConfirm your grade and requirements.›Other Specialty MaterialsDiscuss your application and grade.›
Practical guidance for your part geometry and material decisions.
Prepare your process, budget and sourcing questions.
Build your knowledge before production.
Learn who we are and how we operate.
Find our U.S. support team or start a conversation.
YOUR INTERFACES. YOUR OPERATING CASE. YOUR APPROVAL.
Plan your custom AI cooling components around the server interface and the supplied assembly boundary. Compare cold plates, rack manifolds and defined loop assemblies before freezing your drawing, material and sample acceptance.
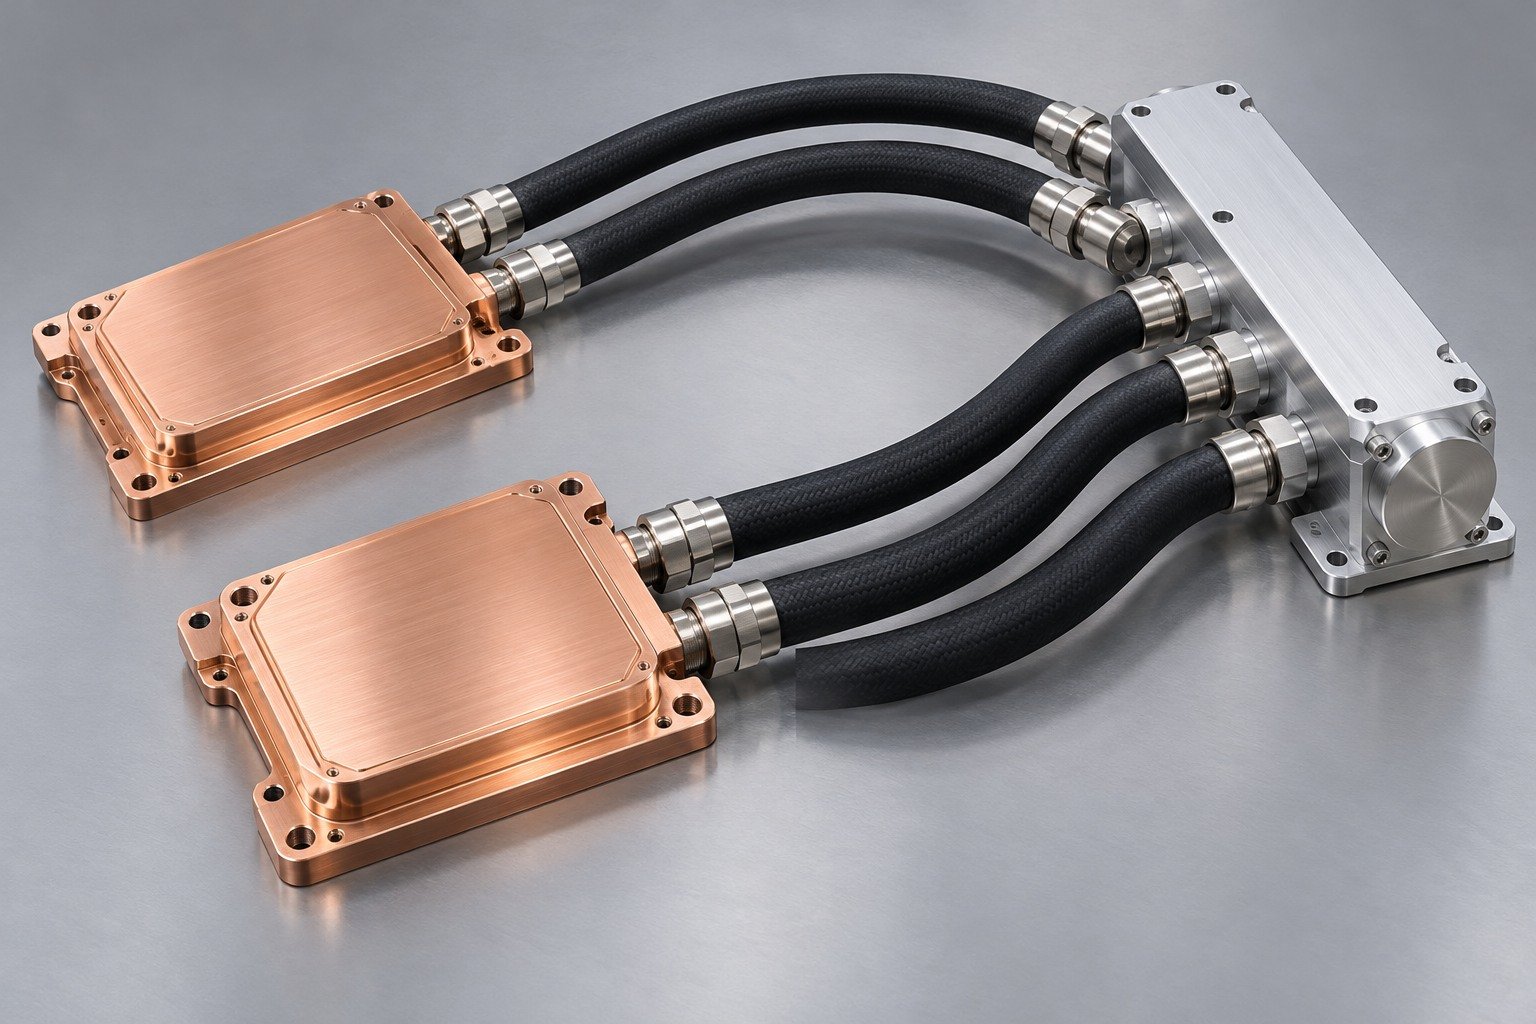
Illustrative manufactured-component concepts
List what is included
Name your operating case
Review all wetted items
Assign checks and owners
Review platform mounting, contact stack and connection access.
Match package keep-outs, mounting load and the contact footprint.
Define manufactured parts, purchased items and integration responsibility.
Illustrative concepts; open each topic for drawing-review details
Review rail position, insertion travel, connector access and service clearance.
Define branch ports, supports and the component boundary inside your CDU.
Coordinate hoses, fittings, assembly revision and agreed integrity records.
Illustrative concepts; open each topic for drawing-review details
Illustrative interface review; thermal validation is a separate scope
For direct to chip cooling components, review the contact stack and the complete path from cold plate to rack connection. Port size alone does not establish available flow. Specify your fluid, temperature, flow, pressure-drop allowance and service state.
Compare bulk conduction and mass alongside your contact stack, coolant, coatings and manufacturing route. These references are not finished server-cooling tests or material substitution approvals.
Hydro 6061-T6 at 25°C. KME Cu-ETP annealed at 20°C.
Calculate finished mass from the actual geometry. A material conductivity difference does not establish a device-temperature reduction.
| Grade | European reference | Si | Fe | Cu | Mn | Mg | Zn | Al |
|---|---|---|---|---|---|---|---|---|
| 6061 | EN AW-6061 · AlMg1SiCu | 0.40–0.80 | ≤0.70 | 0.15–0.40 | ≤0.15 | 0.80–1.20 | ≤0.25 | Balance |
| C11000 | Cu-ETP · CW004A | — | — | ≥99.90 | — | — | — | — |
Selected elements only. Dash means not specified in this summary, not zero. 6061: Cr 0.04–0.35%, Ti ≤0.15%; C11000: O ≤0.040%; do not relabel Cu-ETP as oxygen-free copper. Aluminum other elements ≤0.05% each / ≤0.15% total. The purchasing standard and certificate govern. Confirm product form, temper, joining compatibility and required final condition.
Sources: Hydro 6061 → · KME Cu-ETP →
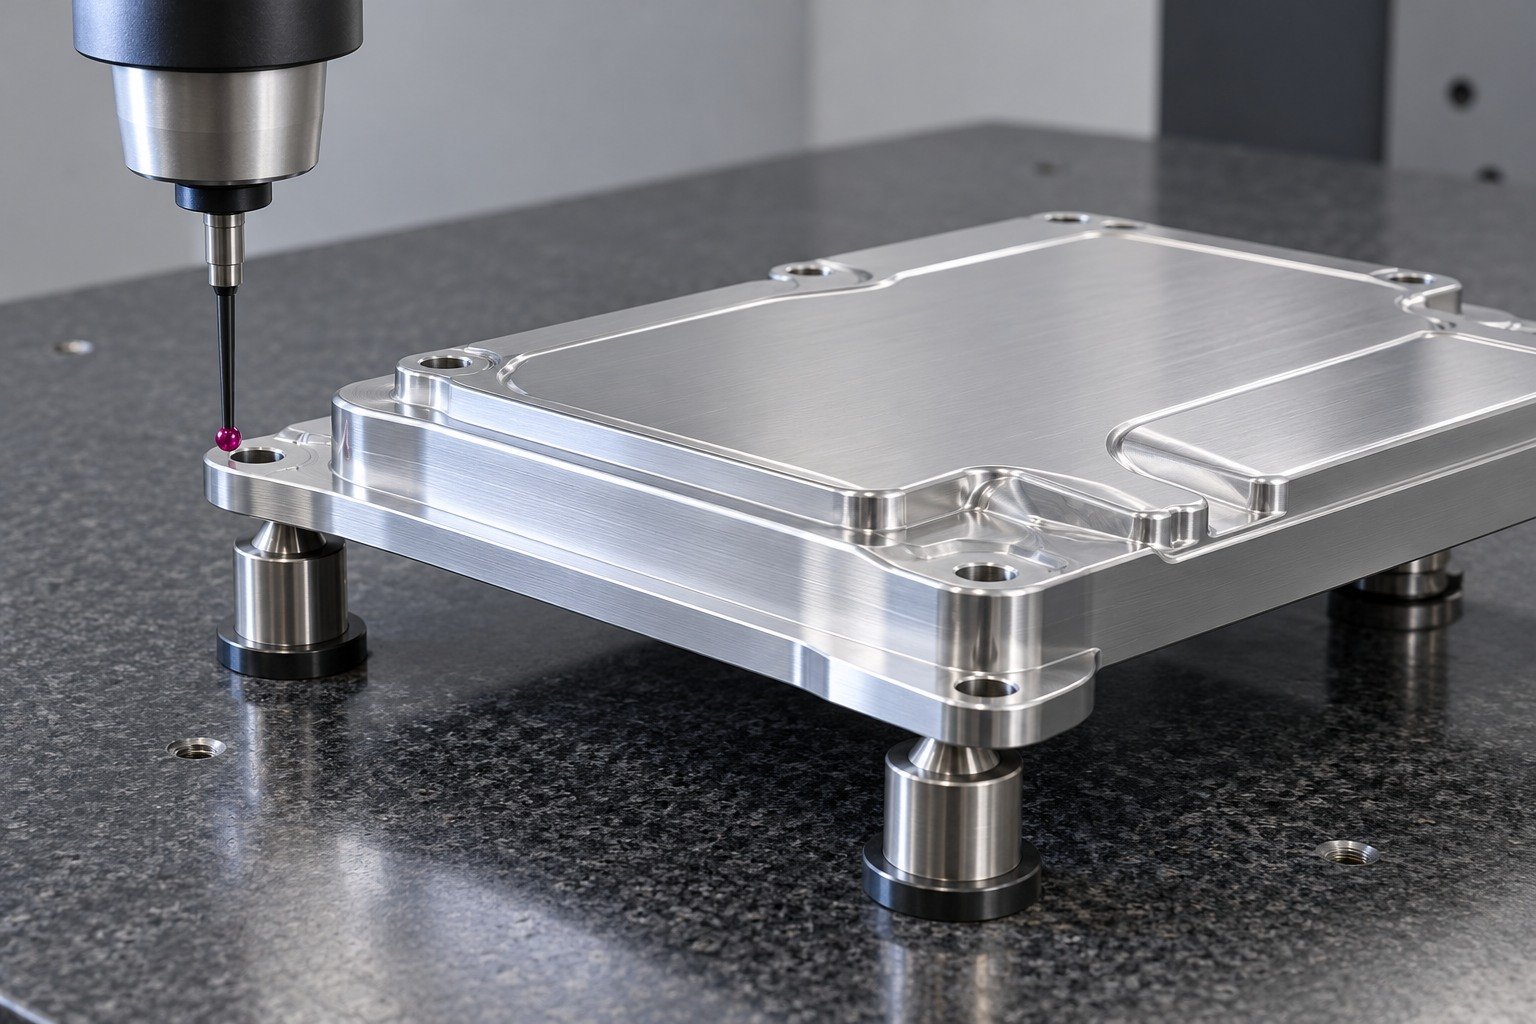
Confirm contact, mounting and ports against the released interface drawing.
Agree AI cooling component leak testing by test medium, pressure, duration, acceptance limit, assembled state and records. Specify cleaning, drying and port protection separately.
Identify the heat map, contact stack, inlet state, flow, pressure measurement boundary and sensor positions. A dimensional report is not a finished cooling-performance result.
When comparing an AI cooling components manufacturer, confirm the supplied boundary before approving AI cooling prototype manufacturing.
Provide AI cooling component drawings, platform interface, heat map, contact stack, coolant/inlet/flow conditions, ports, quantities and required records. Separate made parts, purchased items and validation responsibility.
Component supply does not by itself include a complete CDU, chiller, server or commissioned facility system. List each deliverable and integration responsibility in the quotation.
Agree material identity, drawing revision, dimensional evidence, specified cleanliness and integrity checks. Define thermal and hydraulic testing separately with named conditions and owners.
Review every wetted metal, coating, seal and approved fluid together under actual conditions. A bulk conductivity figure or a plated appearance does not establish compatibility.
Define the part and operating case.
Agree material, machining and joining.
Trace the controlled revision.
Review fit and specified checks.
Approve the part and supply records.









