

Injection Molding
Tooling and molding for your repeat plastic parts.
From prototype to production, coordinated manufacturing solutions for your custom parts.
View All Services →
Precision parts for your tight tolerances and complex geometry.
Tooling and molding for your repeat plastic parts.

Metal casting options for your part and production volume.

Cutting, forming and welding for your fabricated parts.

Custom profiles for your section, length and finish requirements.

Finishes for your appearance, corrosion and wear requirements.

Sub-assemblies and final builds for your production program.

Production tooling built around your process and volume.

Prototype parts to check fit, function and design.
DFM, process planning and production support for your project.
Inspection, documentation, inventory and delivery planning for your program.
Choose air- or liquid-cooling components around your thermal and mechanical requirements.

Manufacturing support for your cold plates, manifolds and cooling assemblies.

Find components for your power electronics, energy, laser and telecom application.

Components for your electronic systems.
Start with your functional and quality requirements.
Build around your operating environment.
From prototype to production, review material performance, manufacturability and cost for your part.
Review grade, temper and finish for your metal parts.
 AluminumStrength, weight and machining›
 Stainless SteelCorrosion and finish requirements›
 Carbon & Alloy SteelDiscuss grade and heat treatment›
 Tool SteelDiscuss tooling and wear needs›
 TitaniumReview grade and part geometry›
 Copper & Brass & BronzeDiscuss conductivity and machining›
Match your polymer to function, process and environment.
 ABSReview enclosure and molding needs›
 Polycarbonate (PC)Discuss clarity and impact needs›
 Nylon (PA)Review moisture and wear conditions›
 POM / AcetalReview fit and sliding features›
 PEEKDiscuss operating conditions›
 PTFEReview friction and chemical exposure›
 ULTEM / PEIDiscuss thermal and electrical needs›
Confirm grade availability and application requirements.
 Silicone / LSRDiscuss flexible component needs›
 TPU / TPEReview flexibility and processing›
 EPDMReview weathering and chemical exposure.›
 NBRReview oil and fuel exposure.›
 FKMReview temperature and chemical exposure.›
 G10 / FR4Review insulation and laminate needs›
 CompositesReview stiffness, weight and laminate.›Customer-Specified MaterialsConfirm your grade and requirements.›Other Specialty MaterialsDiscuss your application and grade.›
Practical guidance for your part geometry and material decisions.
Prepare your process, budget and sourcing questions.
Build your knowledge before production.
Learn who we are and how we operate.
Find our U.S. support team or start a conversation.
YOUR INTERFACES · YOUR CONDITIONS · YOUR ACCEPTANCE
Review the channel base and cover as one finished assembly. Define tool access, weld support, material condition, final machining and the leak or pressure evidence your drawing needs before selecting friction stir welding.
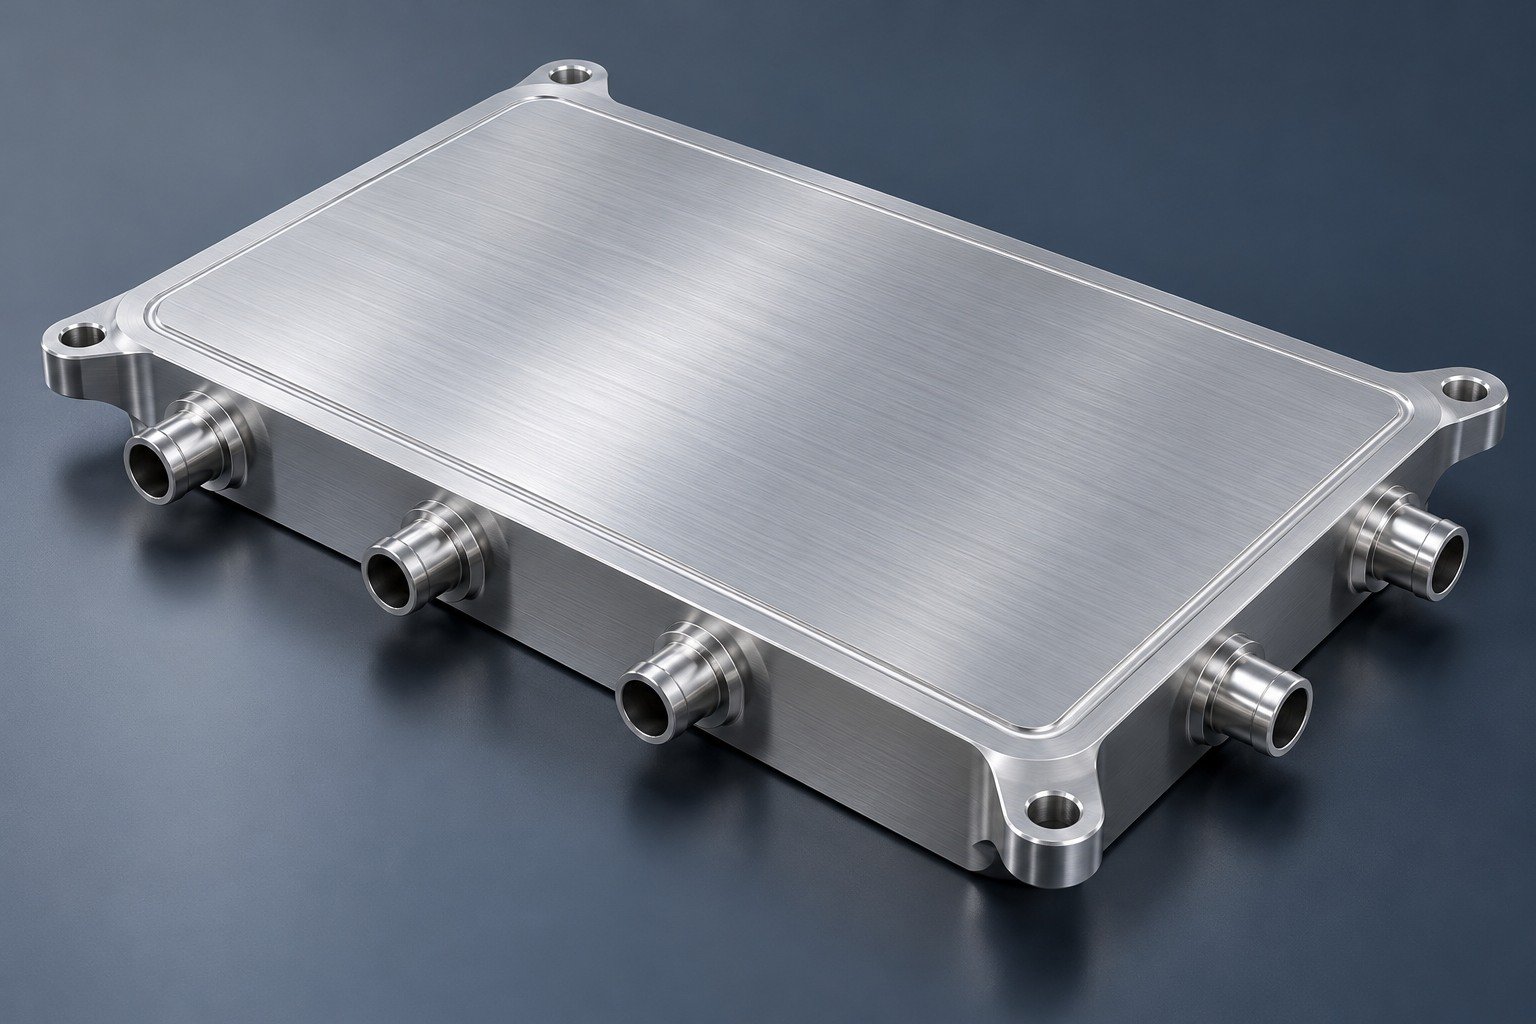
Illustrative component concept
Critical geometry & interfaces
Grades, condition & compatibility
Defined route & final state
Agreed methods & records
Resolve cover geometry, tool access, channel support and final acceptance together before committing to your welded cold plate.
Define FSW cold plate cover thickness, joint location and the material beneath the planned tool path.
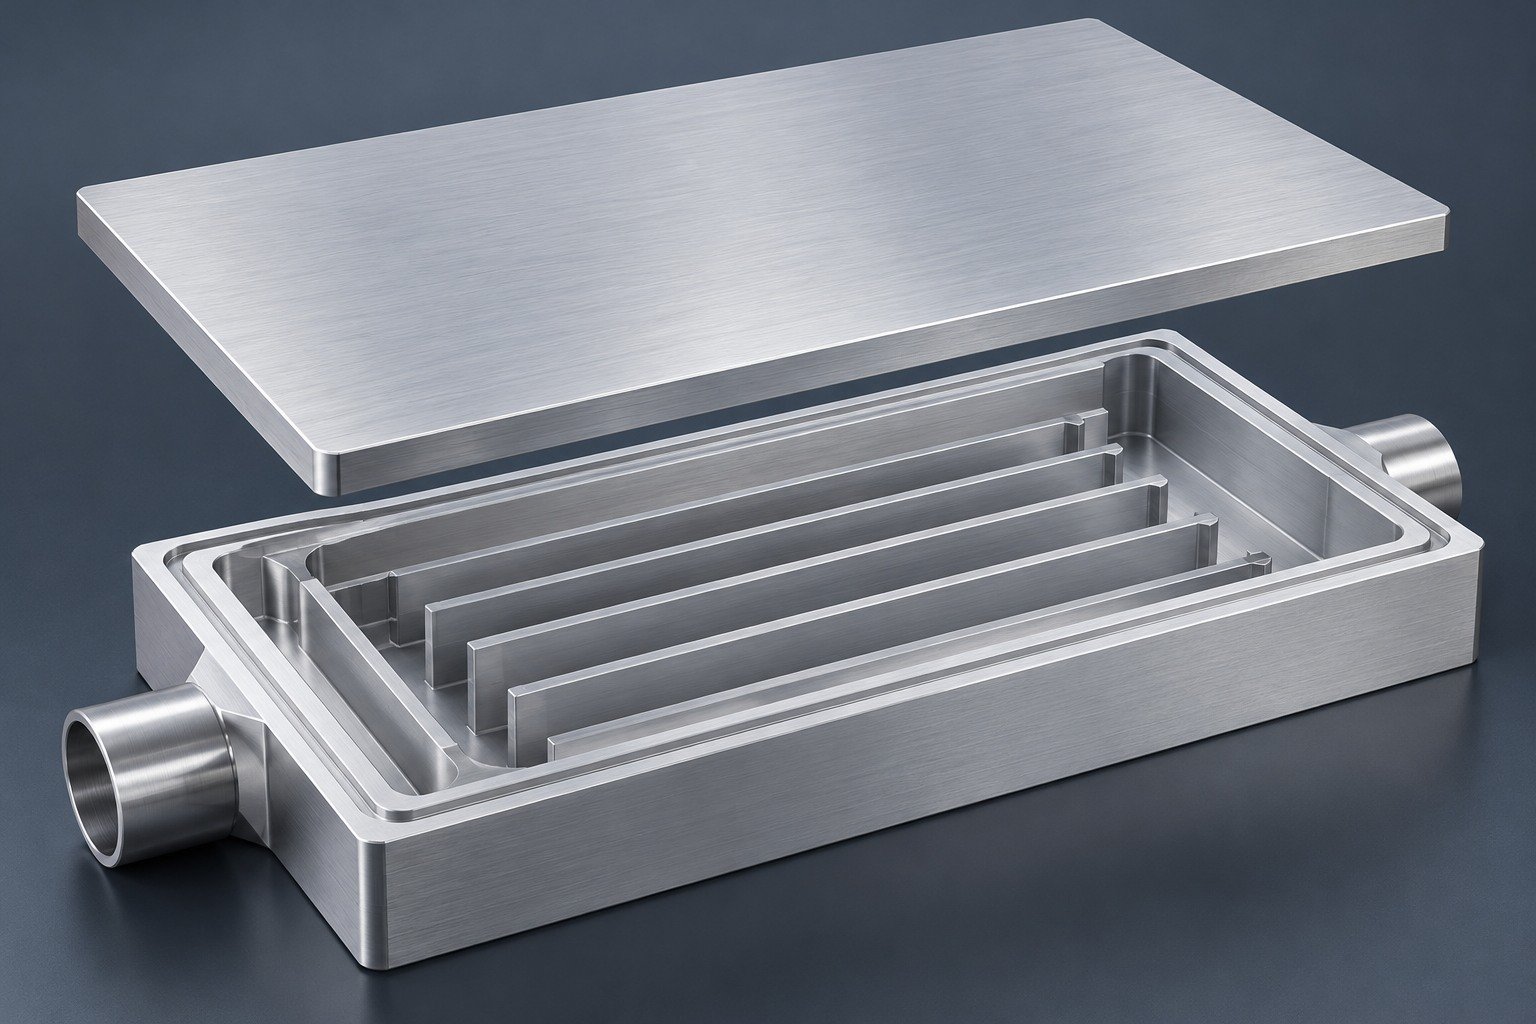
Show channels, ribs and unsupported spans so weld access and fixture support can be reviewed together.
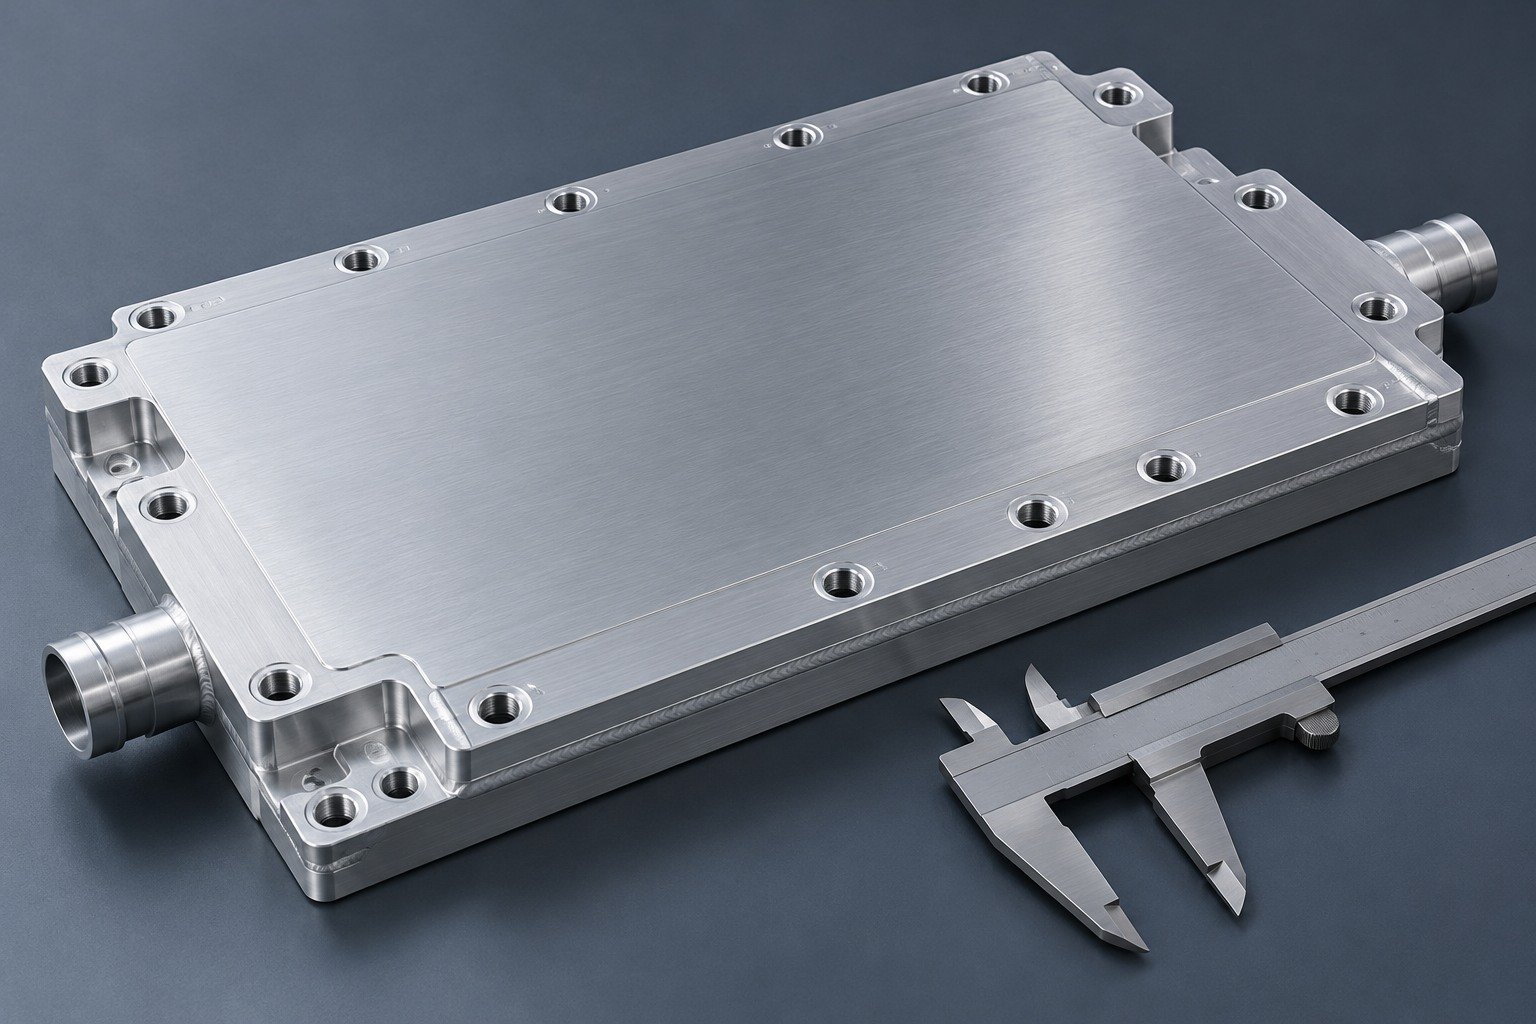
Specify FSW cold plate flatness tolerance on the finished contact face after welding and any agreed machining.
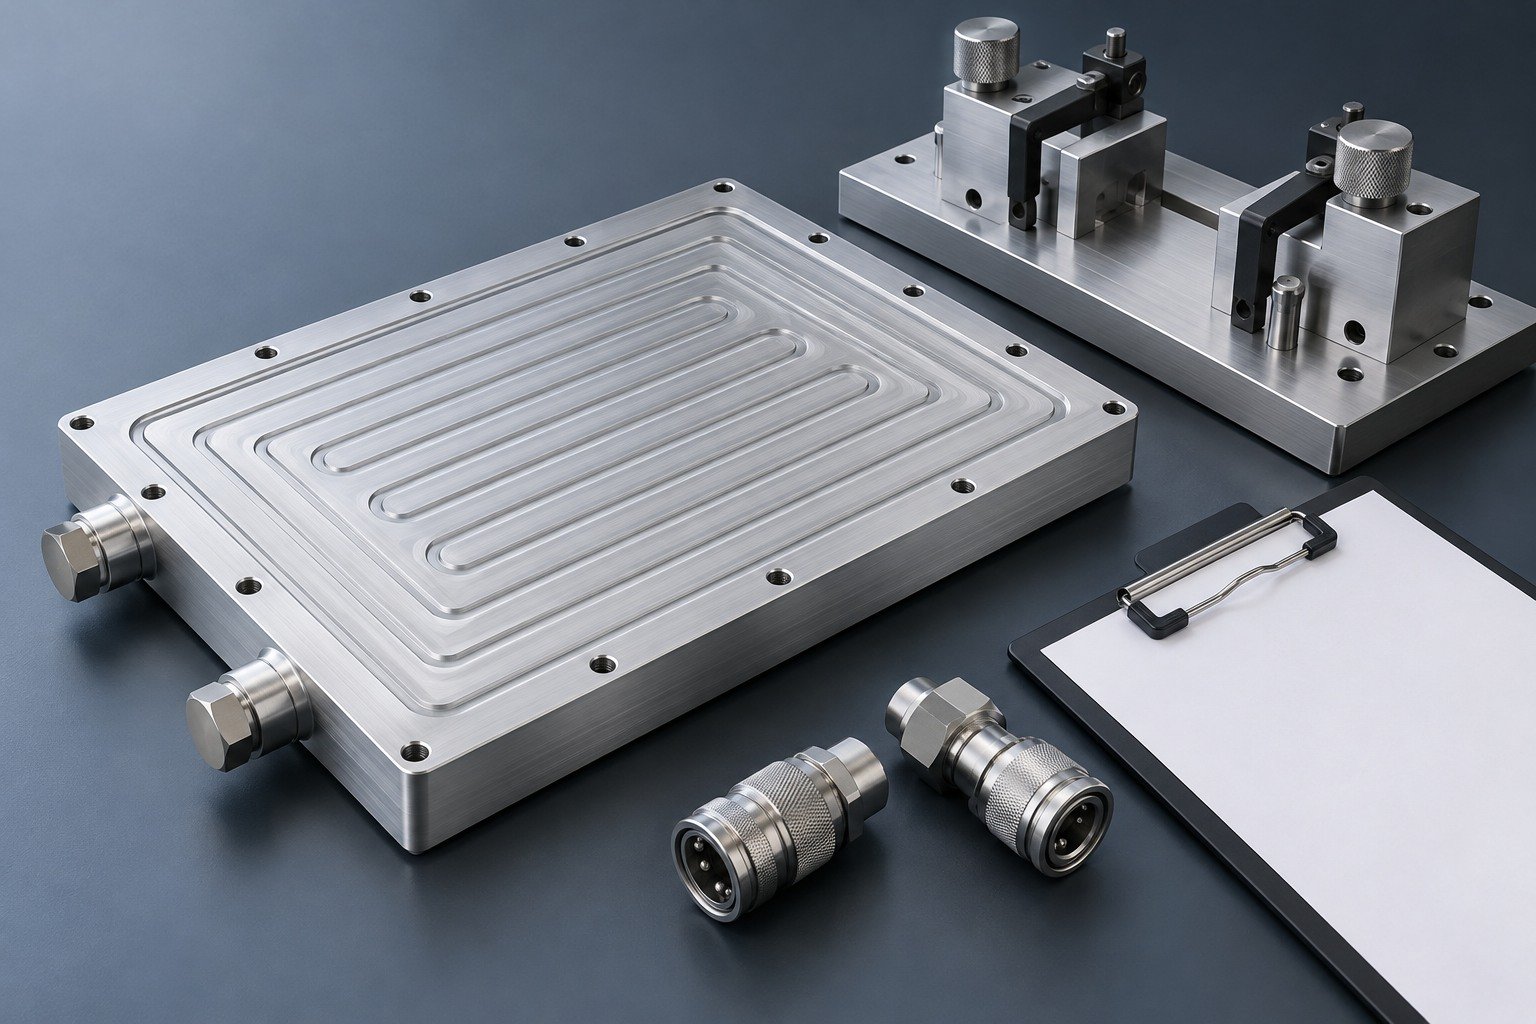
List weld inspection, leak, pressure, flow and thermal checks separately, including ports and installed fittings where required.
Illustrative engineering concepts
Review construction and acceptance together. Your drawing and operating conditions determine the feasible route; the images illustrate structures, not confirmed manufacturing or test capability.
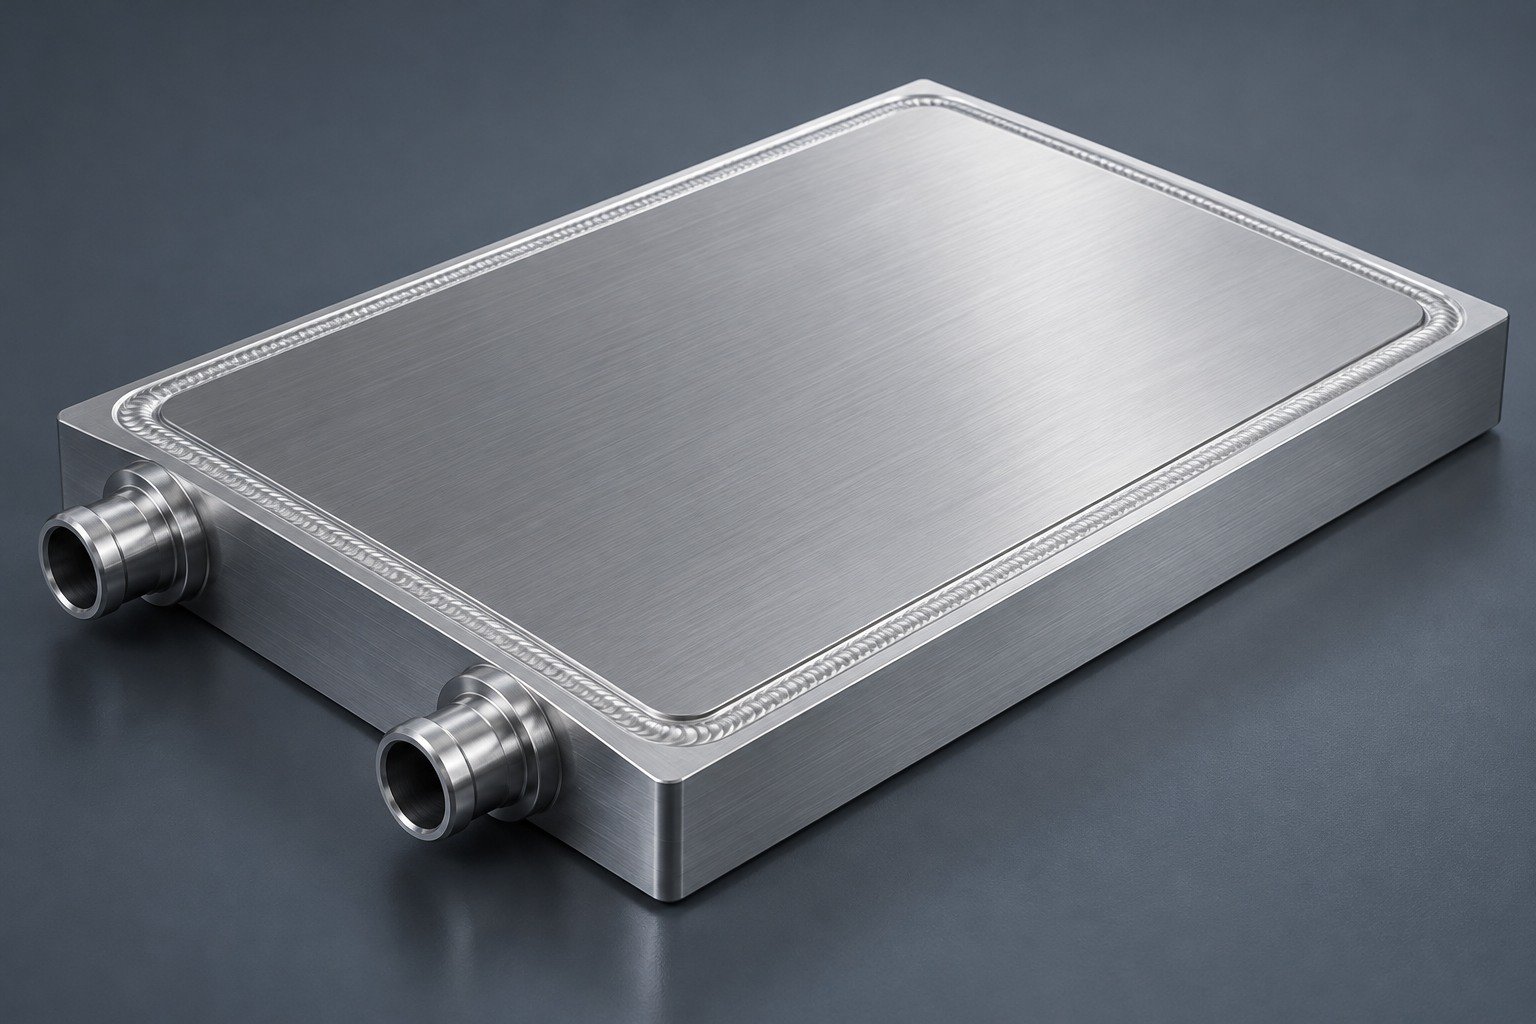
Review externally accessible joint paths, support and final machining.
Review route requirements →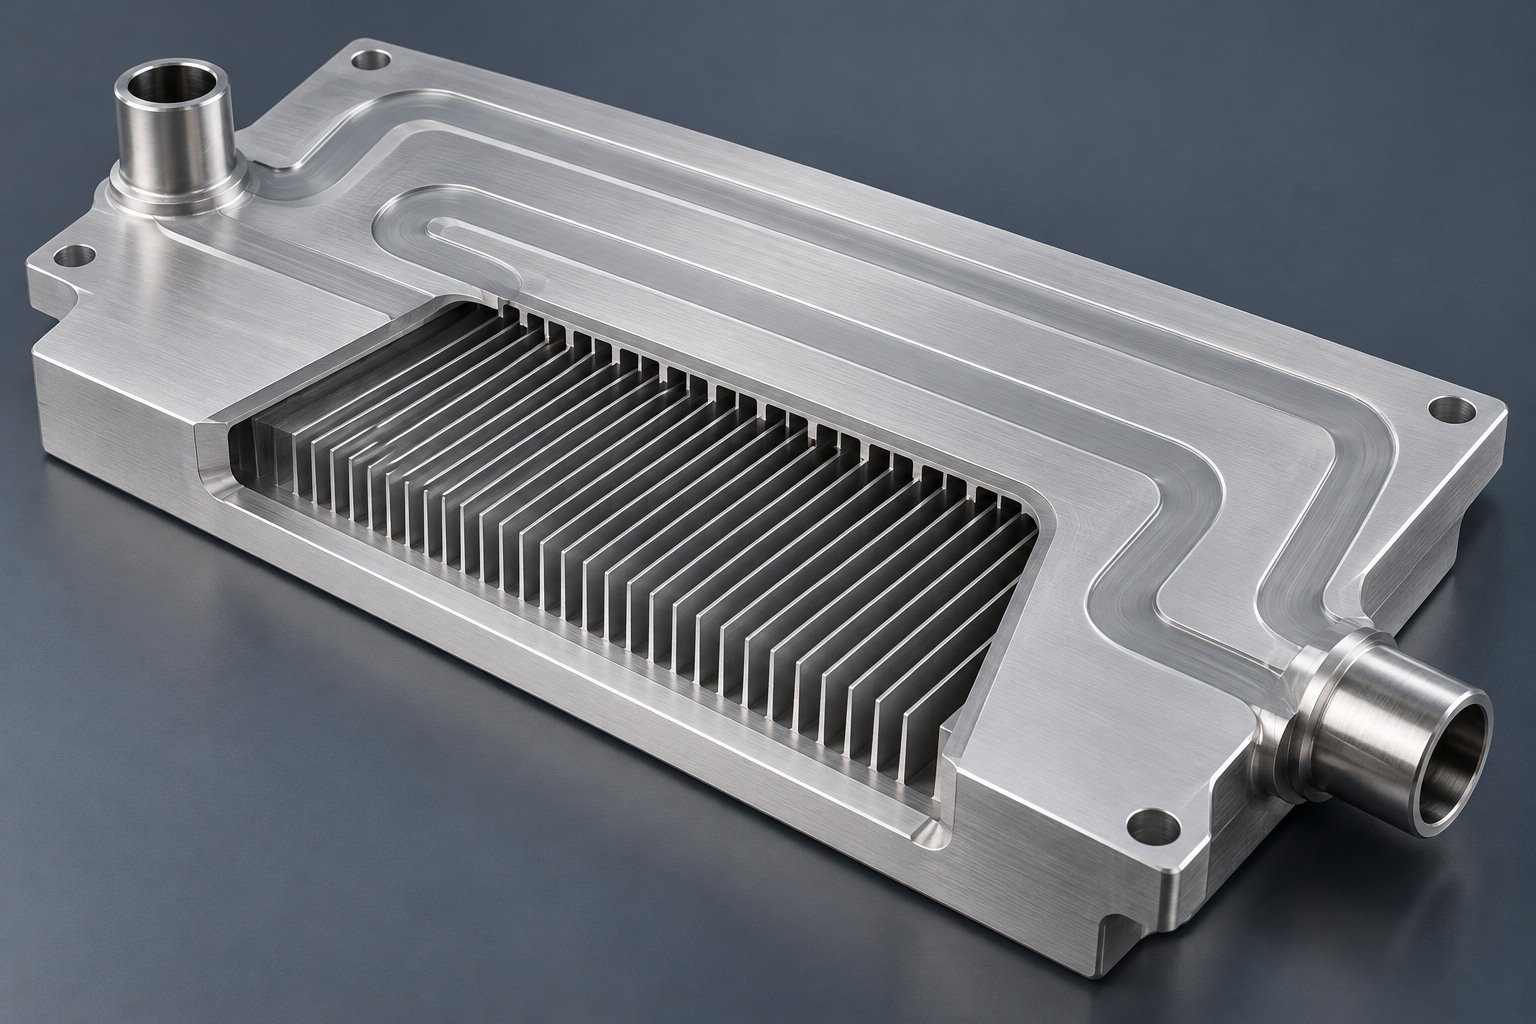
Review enclosed internal joints, filler and final material condition.
Review route requirements →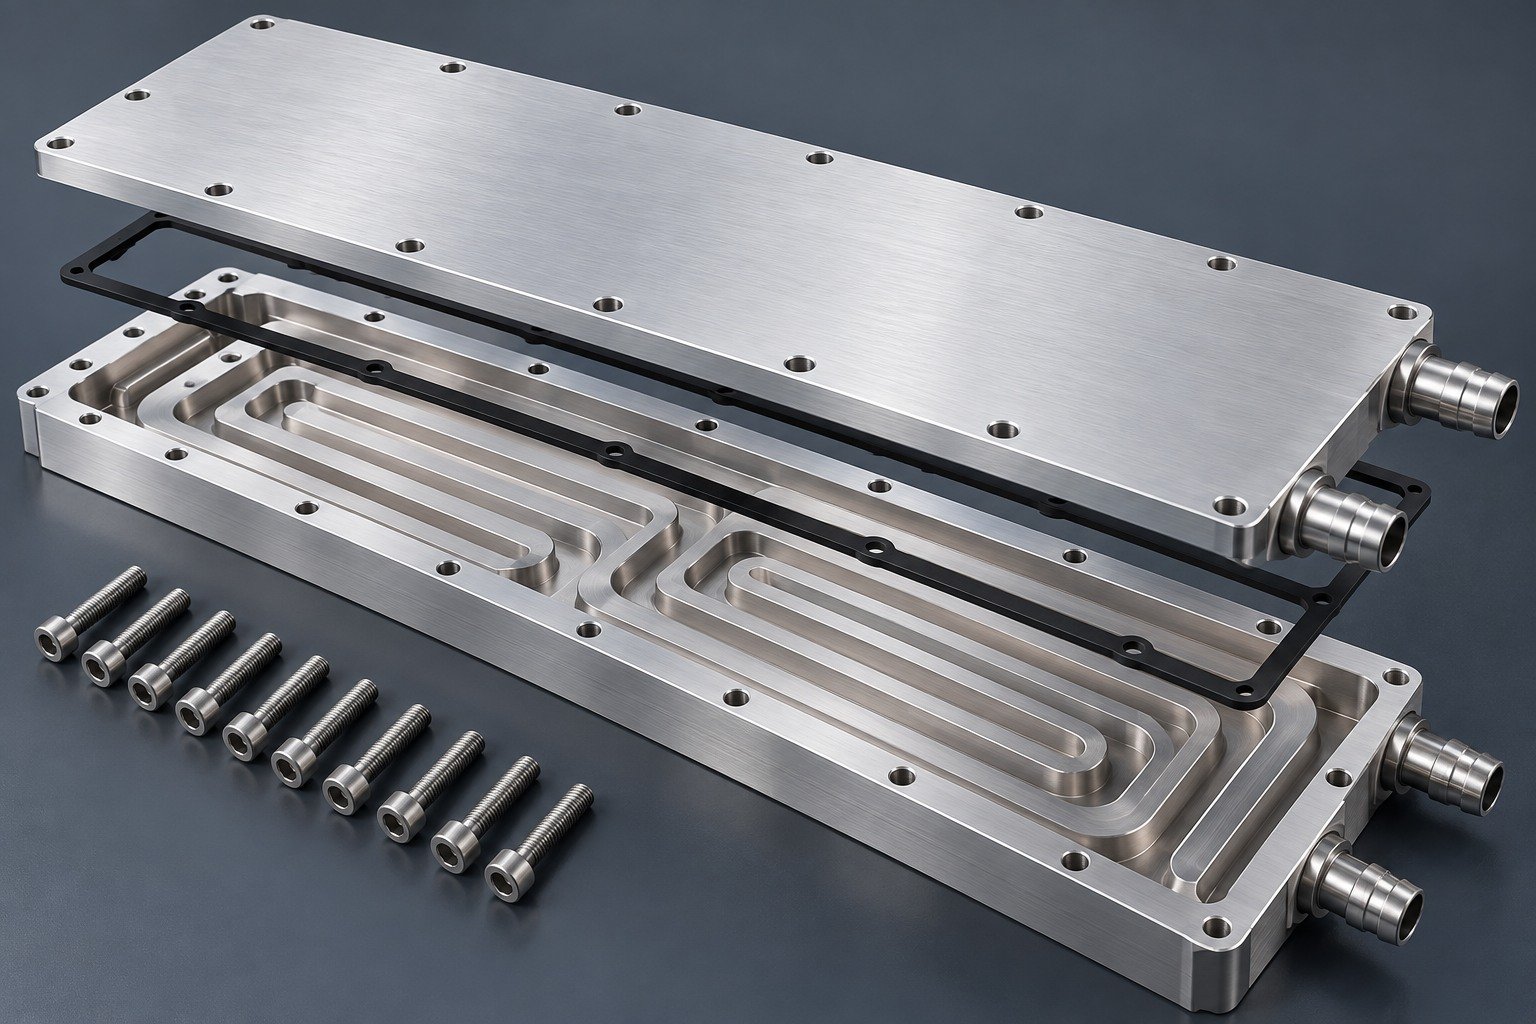
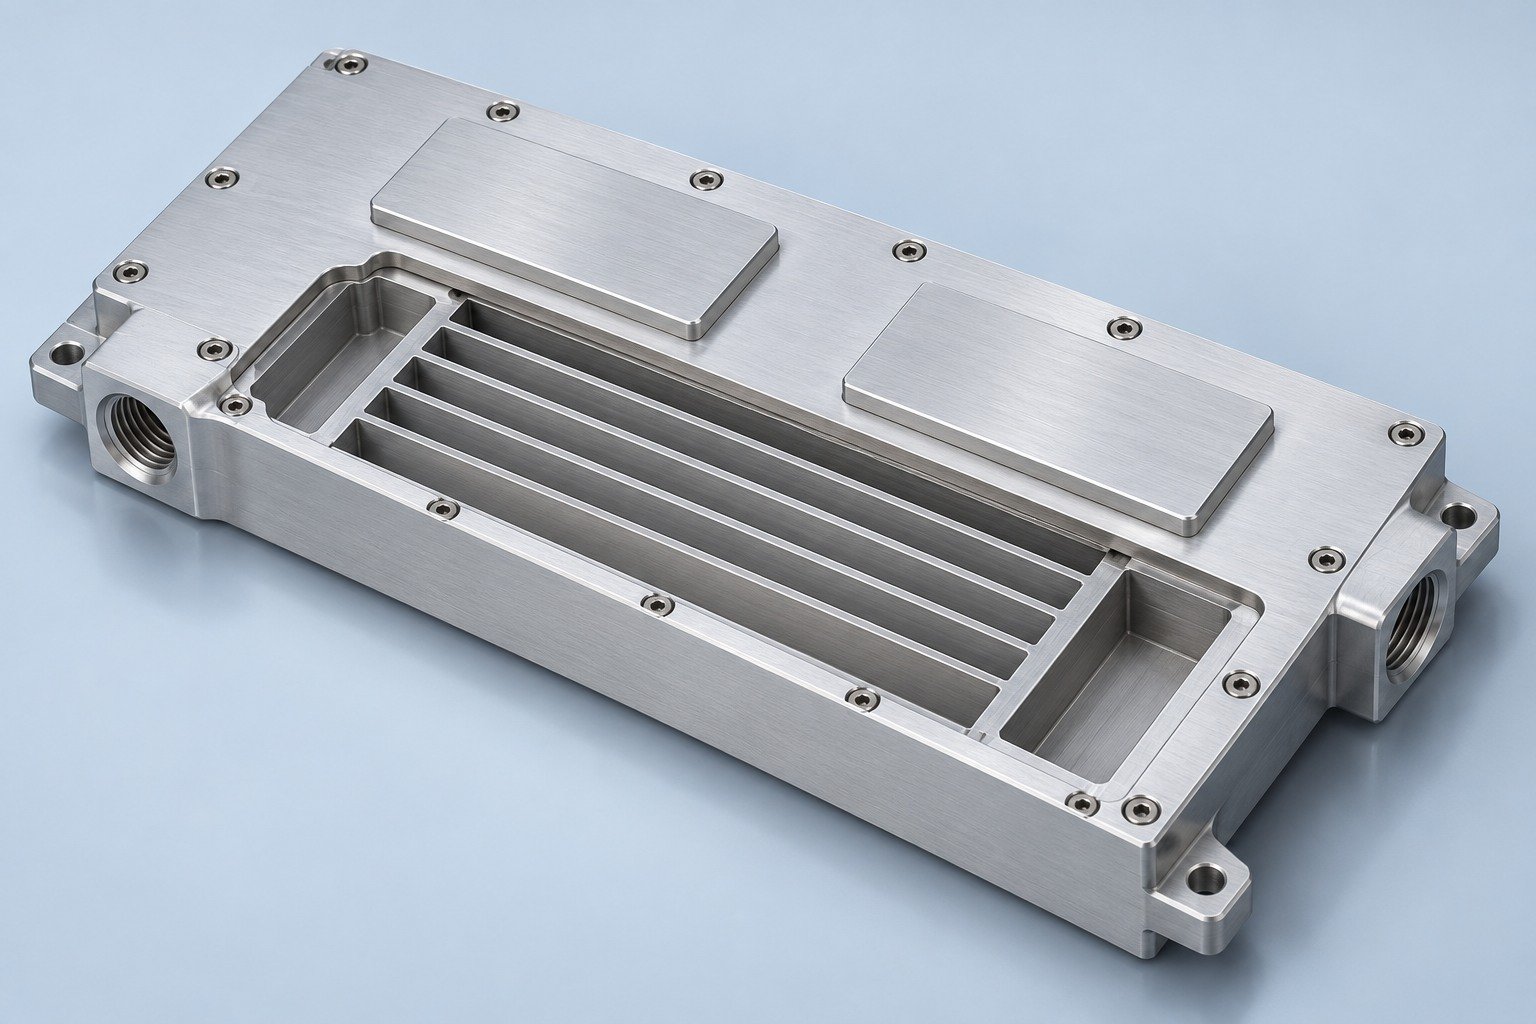
Review removable covers, gasket paths, fasteners and service access.
Review route requirements →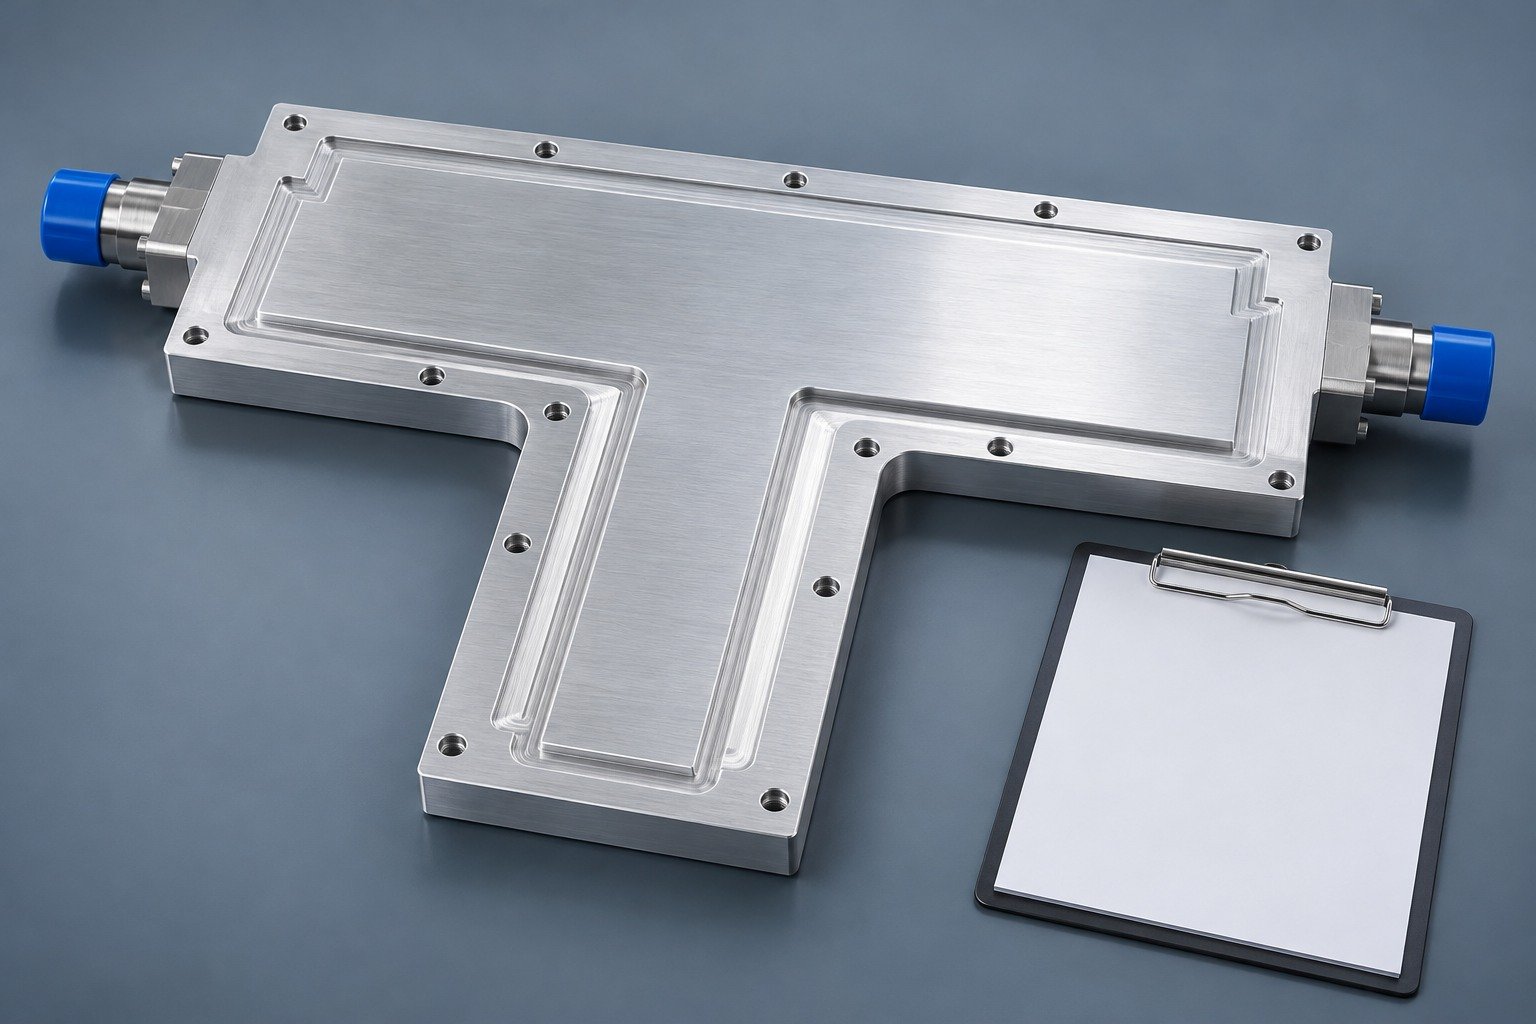
Confirm the joint route and its drawing-specific acceptance evidence.
Review route requirements →Illustrative engineering concepts
Friction stir welding uses a rotating non-consumable tool to form a solid-state joint. For a cold plate, review the accessible cover joint and its support together with the internal flow path. Your FSW cold plate channel design must leave the agreed weld land, cover support and final machining allowance; the drawing review confirms the feasible process scope.
Process background: TWI solid-state joining → · Cold-plate joint review →. General process references do not establish LK MFG equipment, qualification or performance.
Bulk stock properties help you review conduction and mass. These are sourced material references, not LK MFG part tests, approved material substitutions or post-joining performance guarantees.
Hydro 6061-T6 at 25°C; Alumeco 3003 rolled typical; temperature and temper not stated for this physical-property entry.
Calculate finished mass from the actual geometry. A material conductivity difference does not establish a device-temperature reduction.
| Grade | European reference | Si | Fe | Cu | Mn | Mg | Zn | Al |
|---|---|---|---|---|---|---|---|---|
| 6061 | EN AW-6061 · AlMg1SiCu | 0.40–0.80 | ≤0.70 | 0.15–0.40 | ≤0.15 | 0.80–1.20 | ≤0.25 | Balance |
| 3003 rolled | EN AW-3003 · AlMn1Cu | ≤0.60 | ≤0.70 | 0.05–0.20 | 1.0–1.5 | — | ≤0.10 | Balance |
Selected elements only. Dash means not specified in this summary, not zero. 6061: Cr 0.04–0.35%, Ti ≤0.15%; 3003: Ti ≤0.05%; Mg/Cr not listed in the cited selected composition. Aluminum other elements ≤0.05% each / ≤0.15% total. The purchasing standard and certificate govern. Confirm product form, temper, joining compatibility and required final condition.
Sources: Hydro 6061 → · Alumeco 3003 →
Use explicit assumptions to compare a design decision. These examples are calculations and concept diagrams, not measured FSW cold plate results.
Chosen example only: R = t/(kA), using k = 167 W/(m·K), A = 0.01 m² and the labelled wall thickness. This one-dimensional wall term excludes spreading, TIM, fluid convection, channels and the joined condition; it does not predict your device temperature or define an available cover thickness.
Chosen arithmetic example. Identify whether your actual reference is inlet coolant, ambient air or another controlled measurement point before setting a thermal requirement.
Weld inspection, final dimensions, leak and proof checks are separate evidence. A closed joint is not a CFD result or a verified cooling curve.
Separate your thermal contact faces, sealing interfaces and wetted passages. Confirm the specified final condition with the mating assembly.
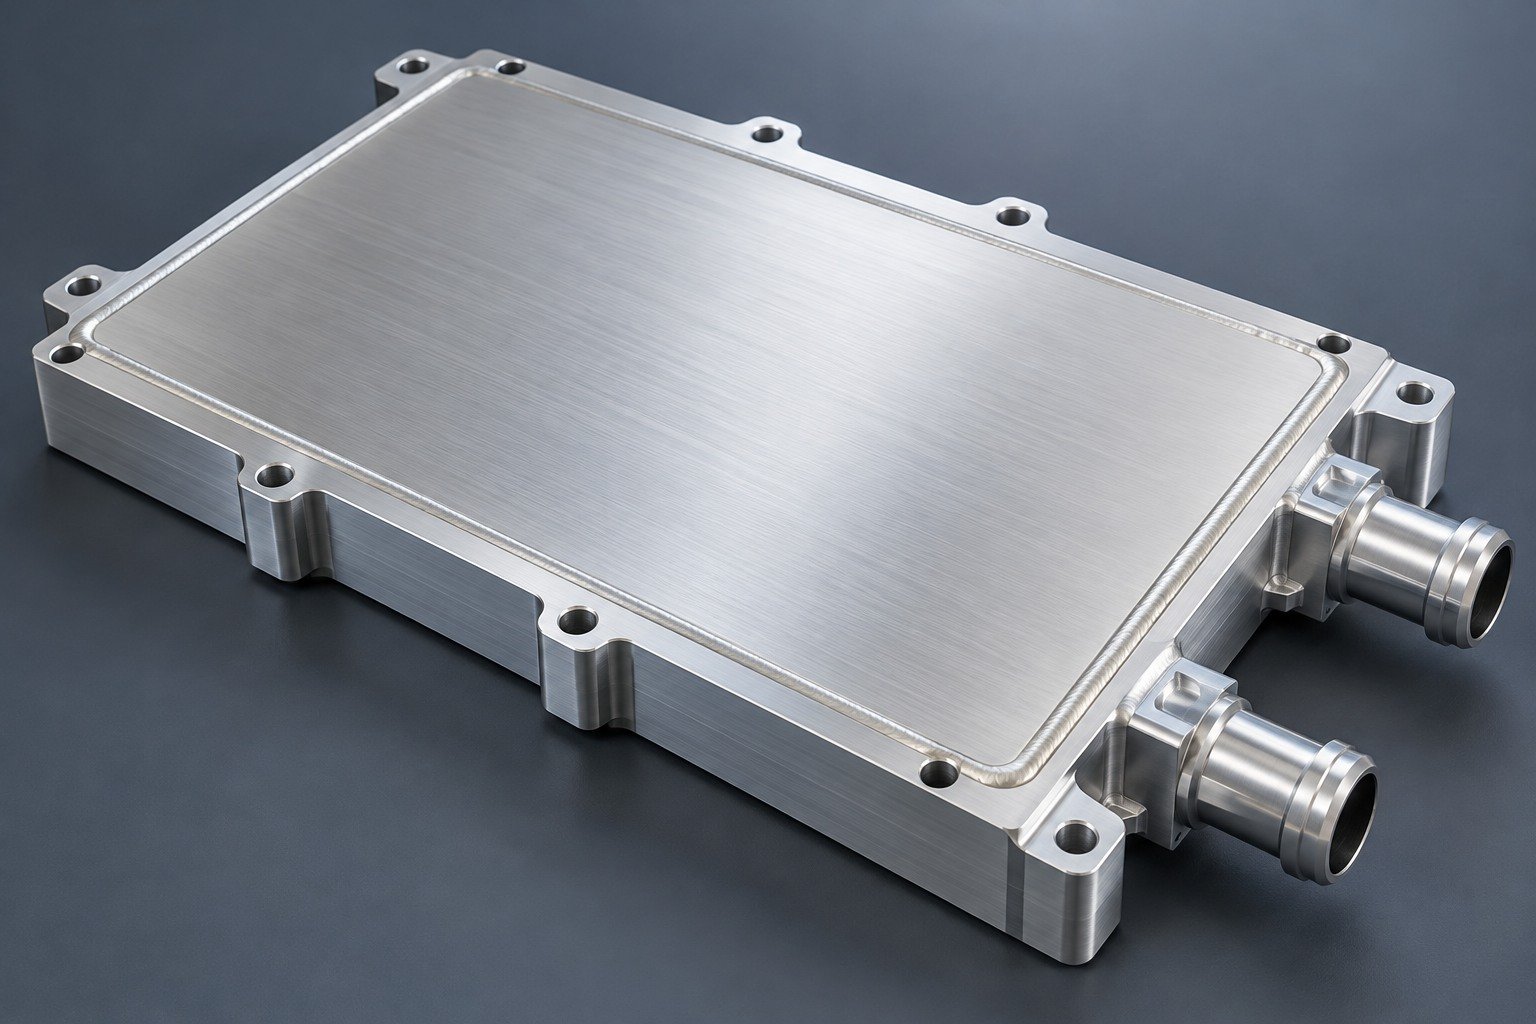
Define the contact area, machining allowance and final inspection state.
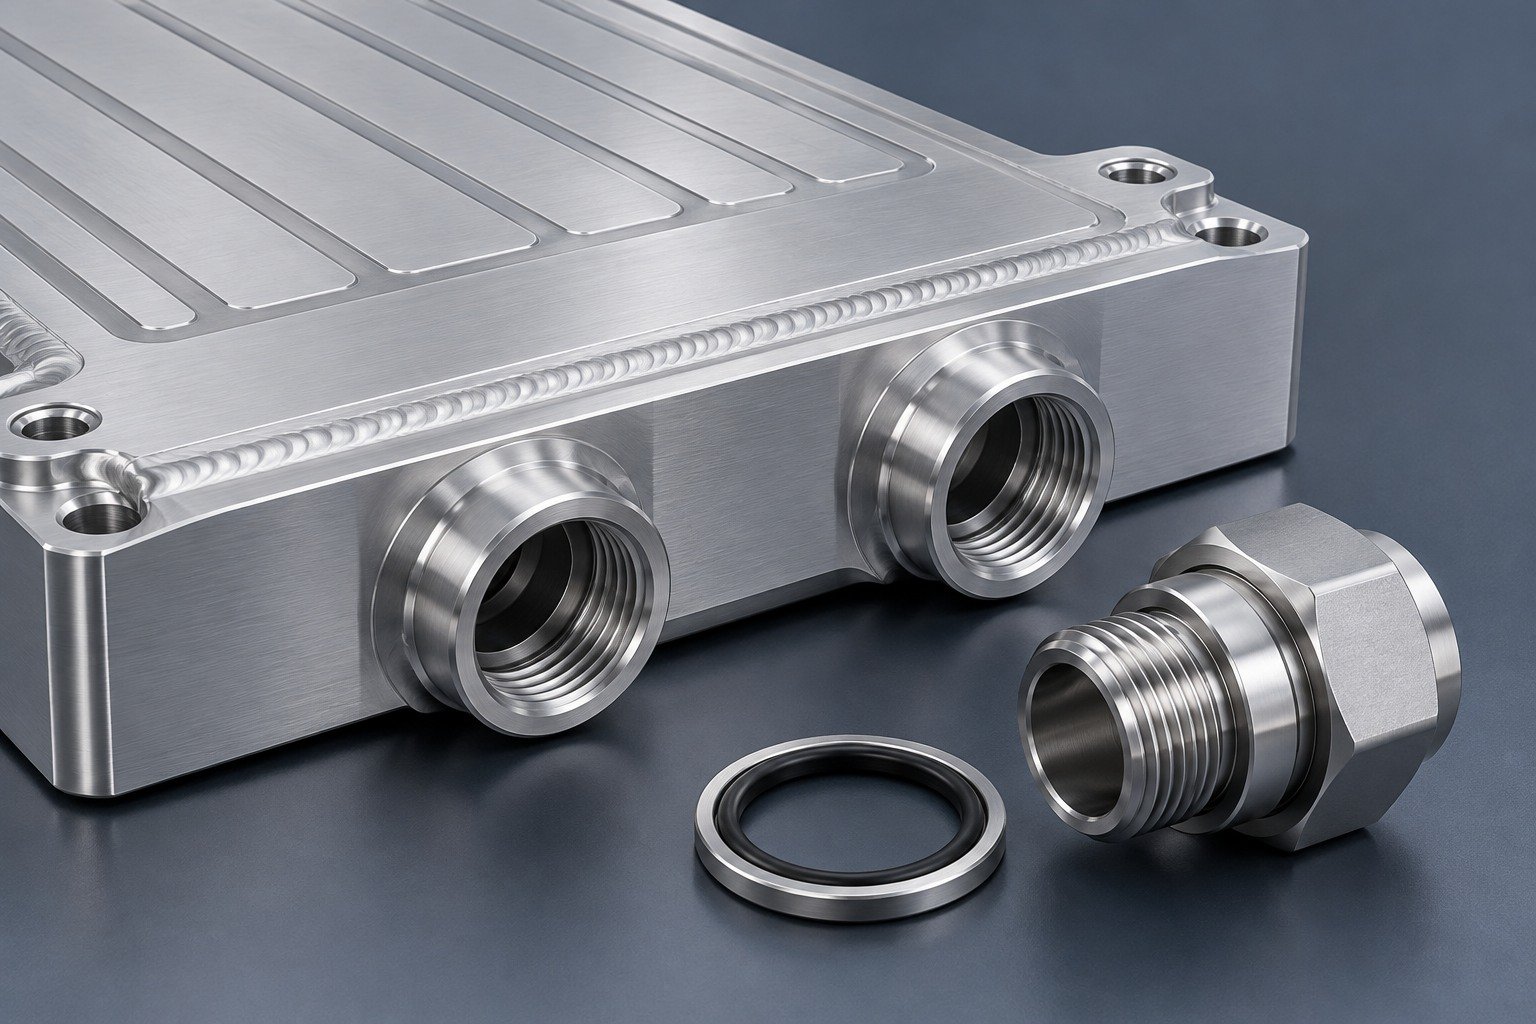
Specify the finished thread, fitting engagement and agreed sealing surfaces.
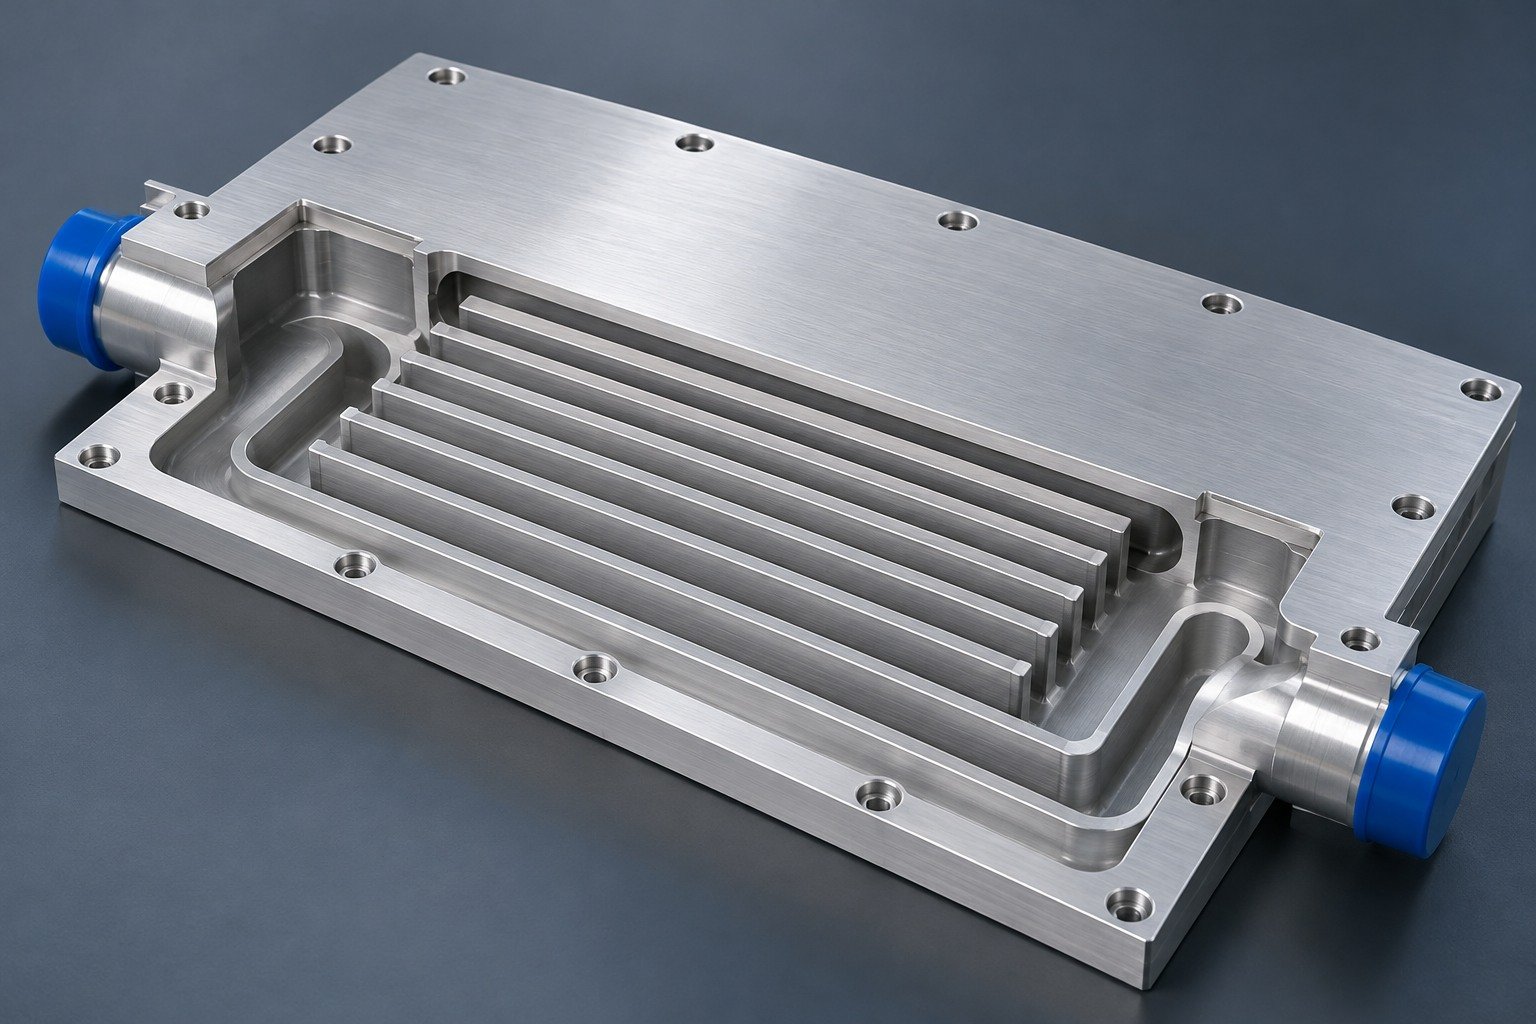
Agree cleaning, residues, port protection and the evidence accessible after joining.
A finish is not a universal cooling improvement. Confirm its purpose, compatibility and inspection state. Review surface finishing options →
Illustrative engineering concepts
Put the dimensions that control sealing, assembly fit and heat transfer on your drawing.
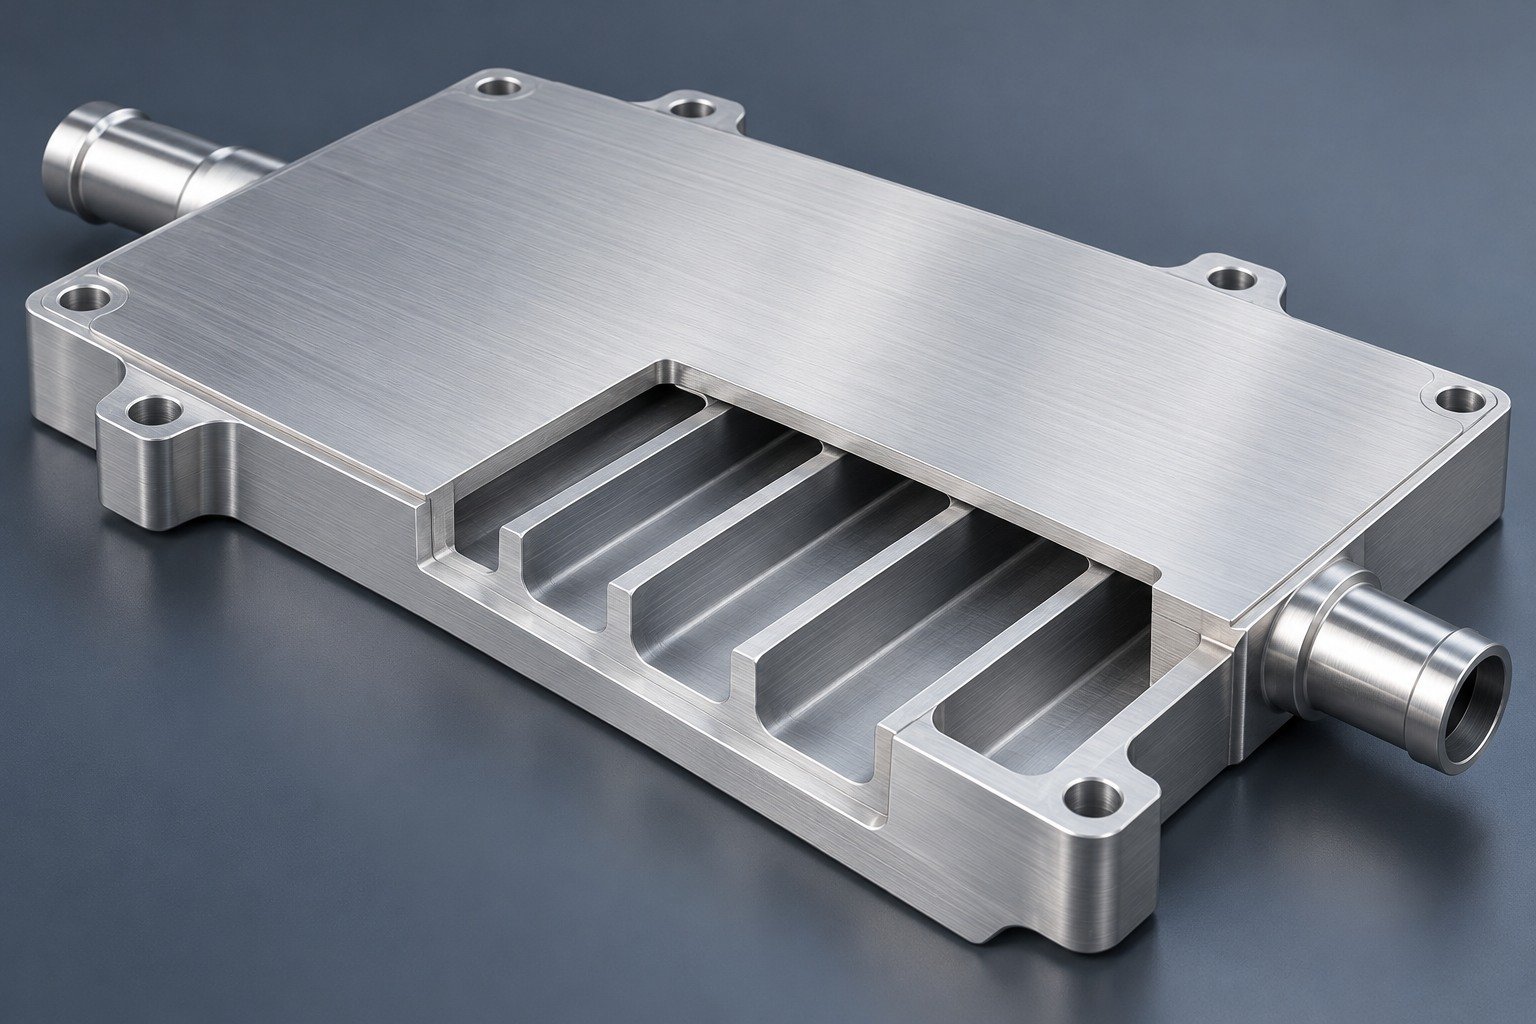
Illustrative cover-joint concept
Heat-source map, TIM and clamping stack
Thread designation, seal land and fitting engagement
Hole pattern, datum scheme and tool access
Joining access, wall thickness and cleaning scope
Flatness, masking, protected interfaces and inspection state
Review your accessible weld path, supported cover, final fit and required records before production.
Your weld path needs external tool access and clearance around ports, bosses and fixtures. Resolve starts, stops and any exit feature before releasing the drawing.
Controlled drawing and the relevant service conditions.
Agreed method, inspection state, limits and required records.
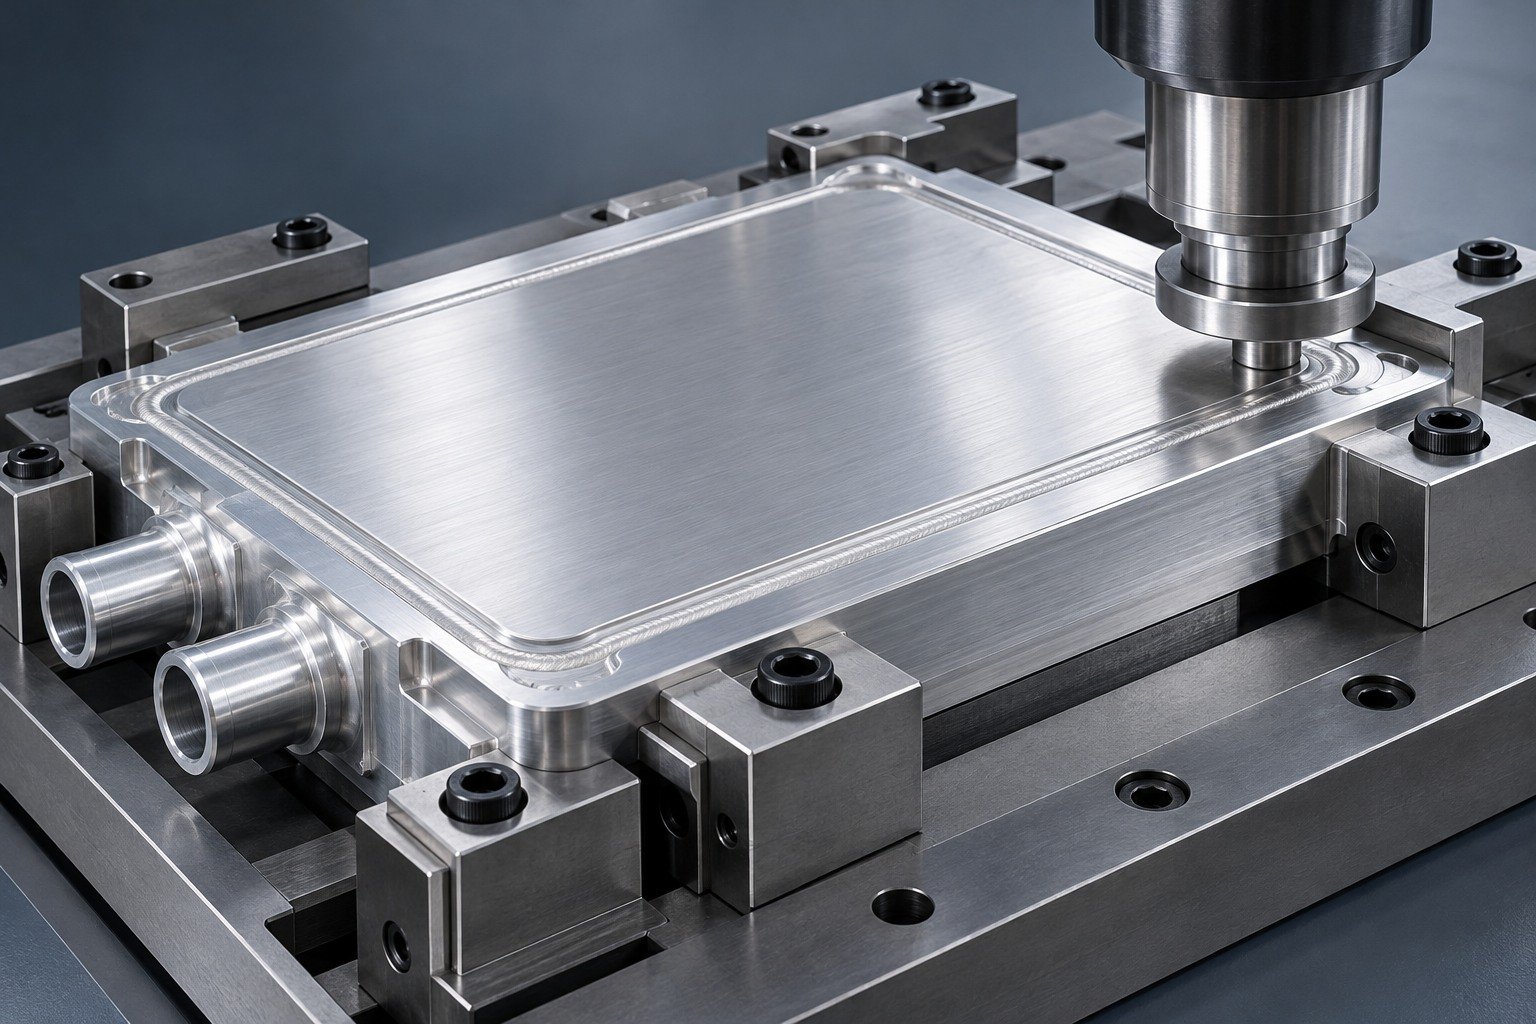
Illustrative engineering concept
Review cover thickness, channel span, backing support and clamping as a combined joining problem. A cover dimension alone does not establish a qualified weld.
Controlled drawing and the relevant service conditions.
Agreed method, inspection state, limits and required records.
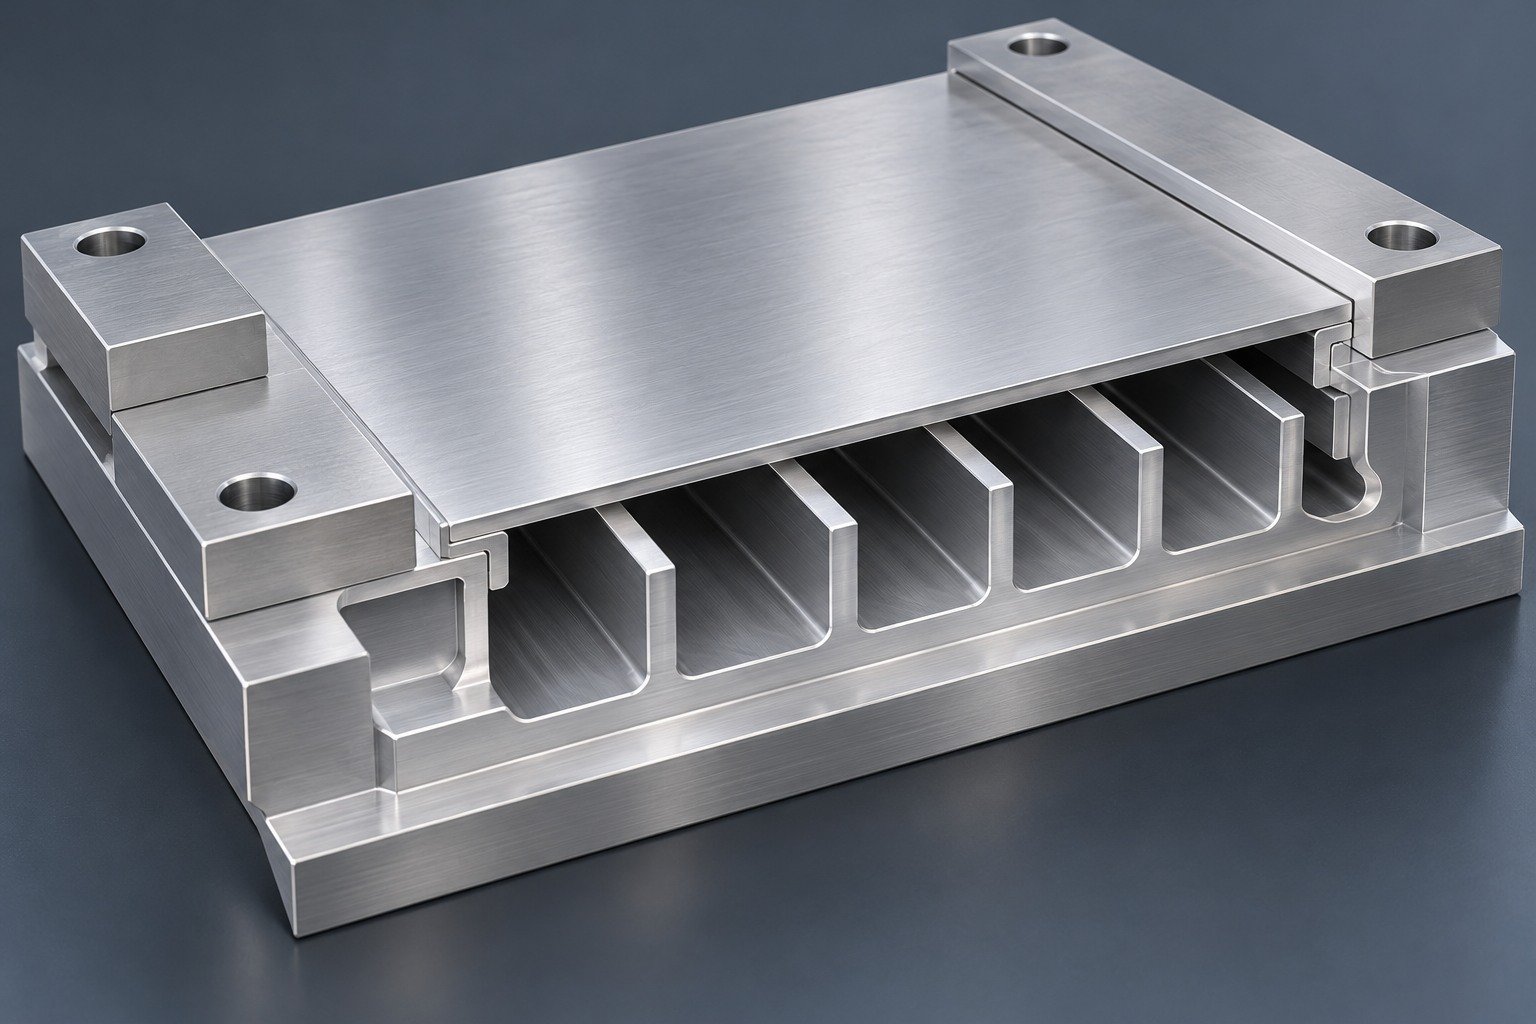
Illustrative engineering concept
Define final datums, contact area, restraint and machining allowance. Measure the finished component; do not assume the stock temper or pre-weld surface remains the accepted final condition.
Controlled drawing and the relevant service conditions.
Agreed method, inspection state, limits and required records.
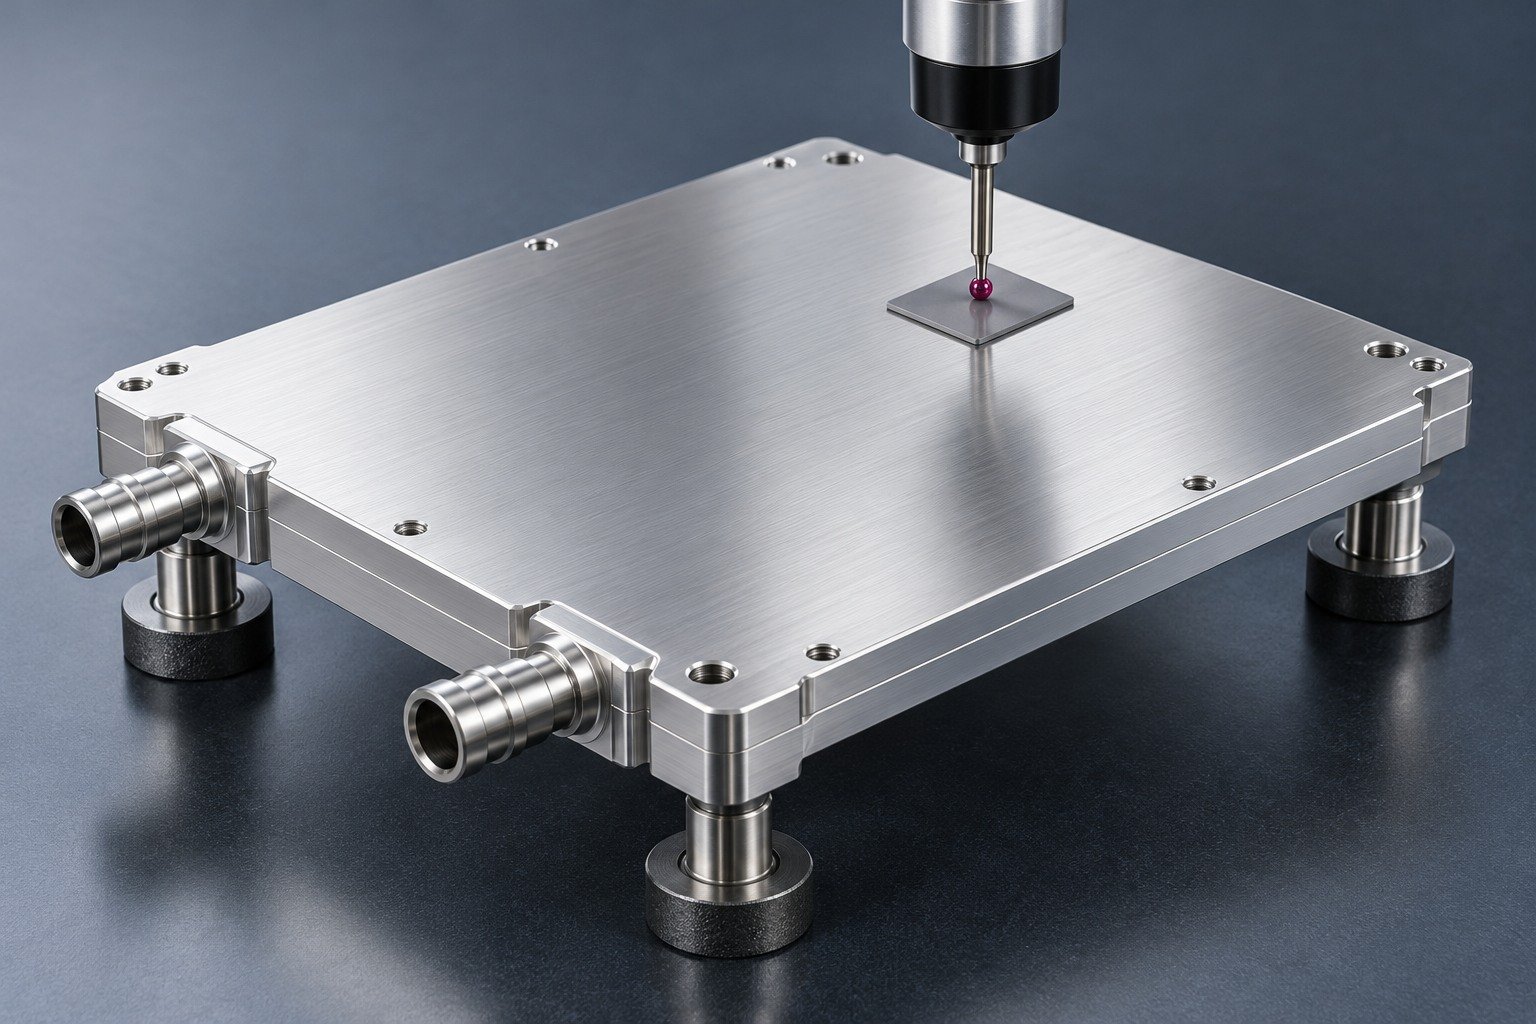
Illustrative engineering concept
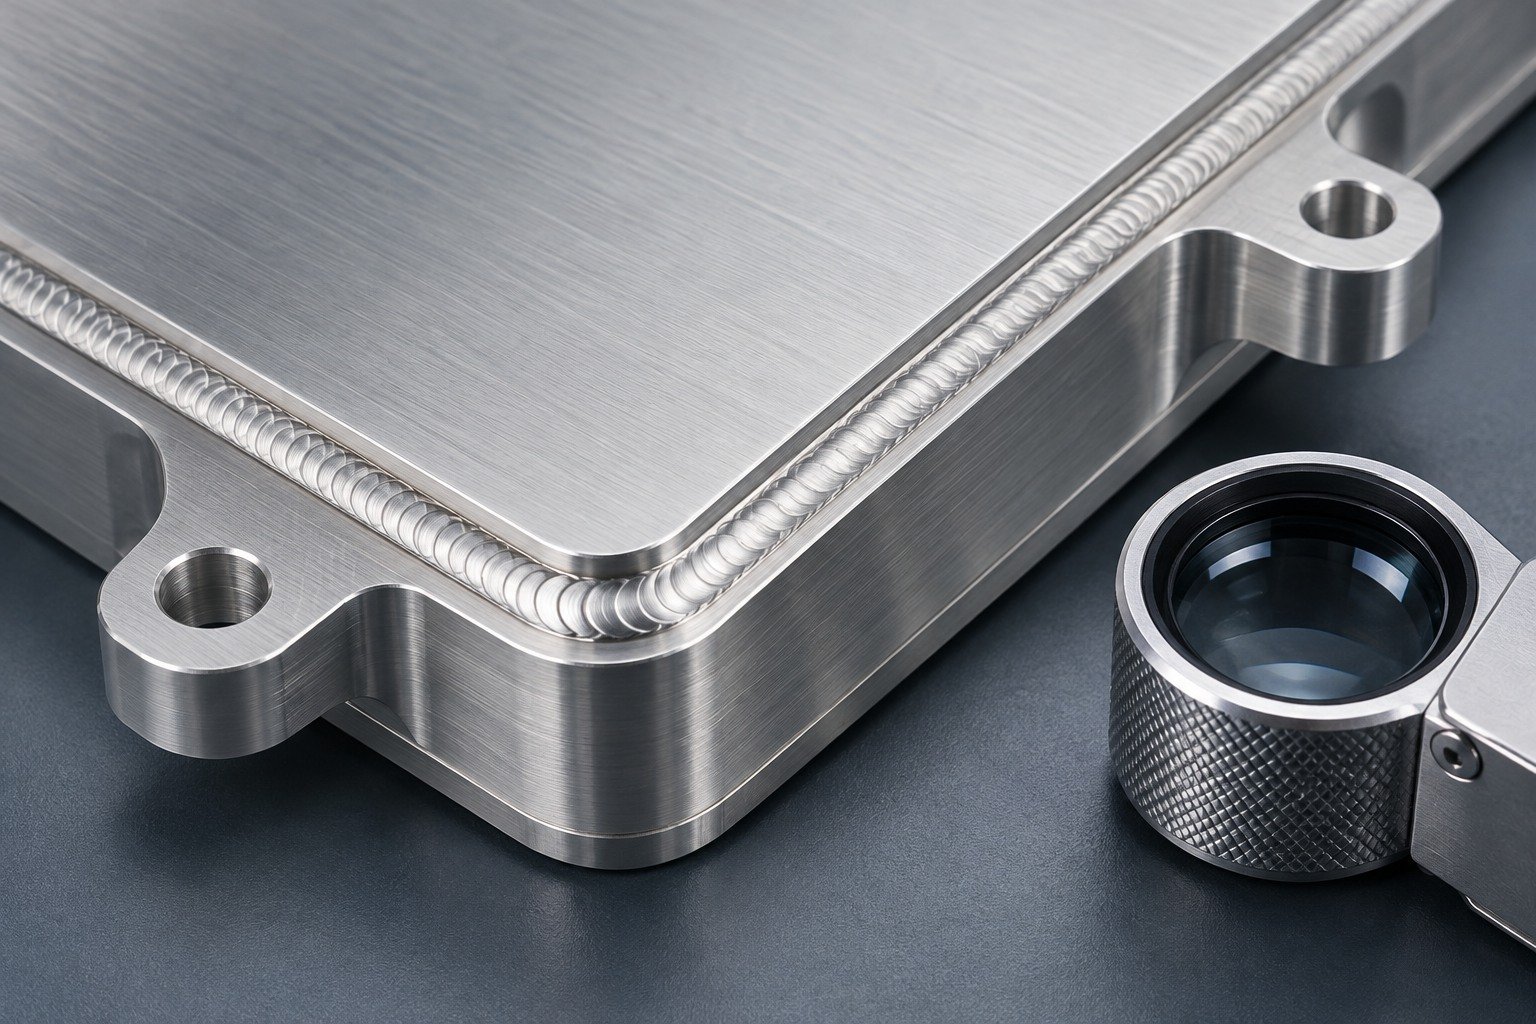
For FSW cold plate weld inspection, agree the method, accessible surfaces, sampling and acceptance criteria. Process records, dimensional checks and specified joint examinations answer different questions.
Controlled drawing and the relevant service conditions.
Agreed method, inspection state, limits and required records.
Illustrative engineering concept
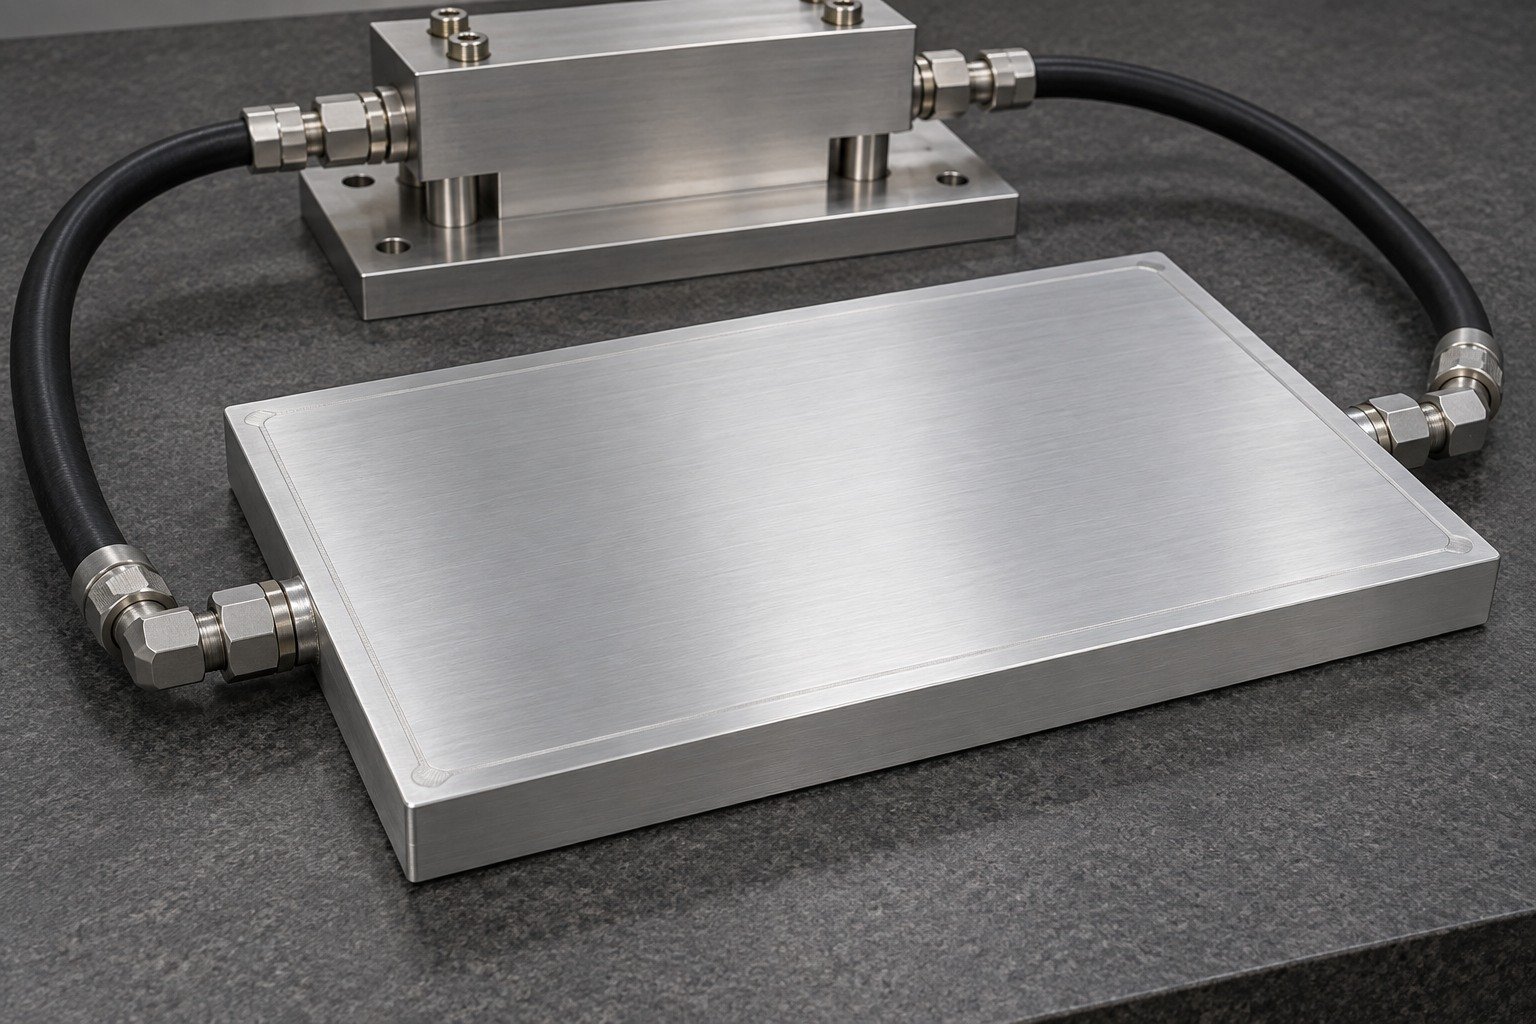
For FSW cold plate leak testing, define method, medium, units, temperature and leakage limit. Specify FSW cold plate pressure testing separately; operating, proof and burst conditions are different requirements.
Controlled drawing and the relevant service conditions.
Agreed method, inspection state, limits and required records.
Illustrative engineering concept
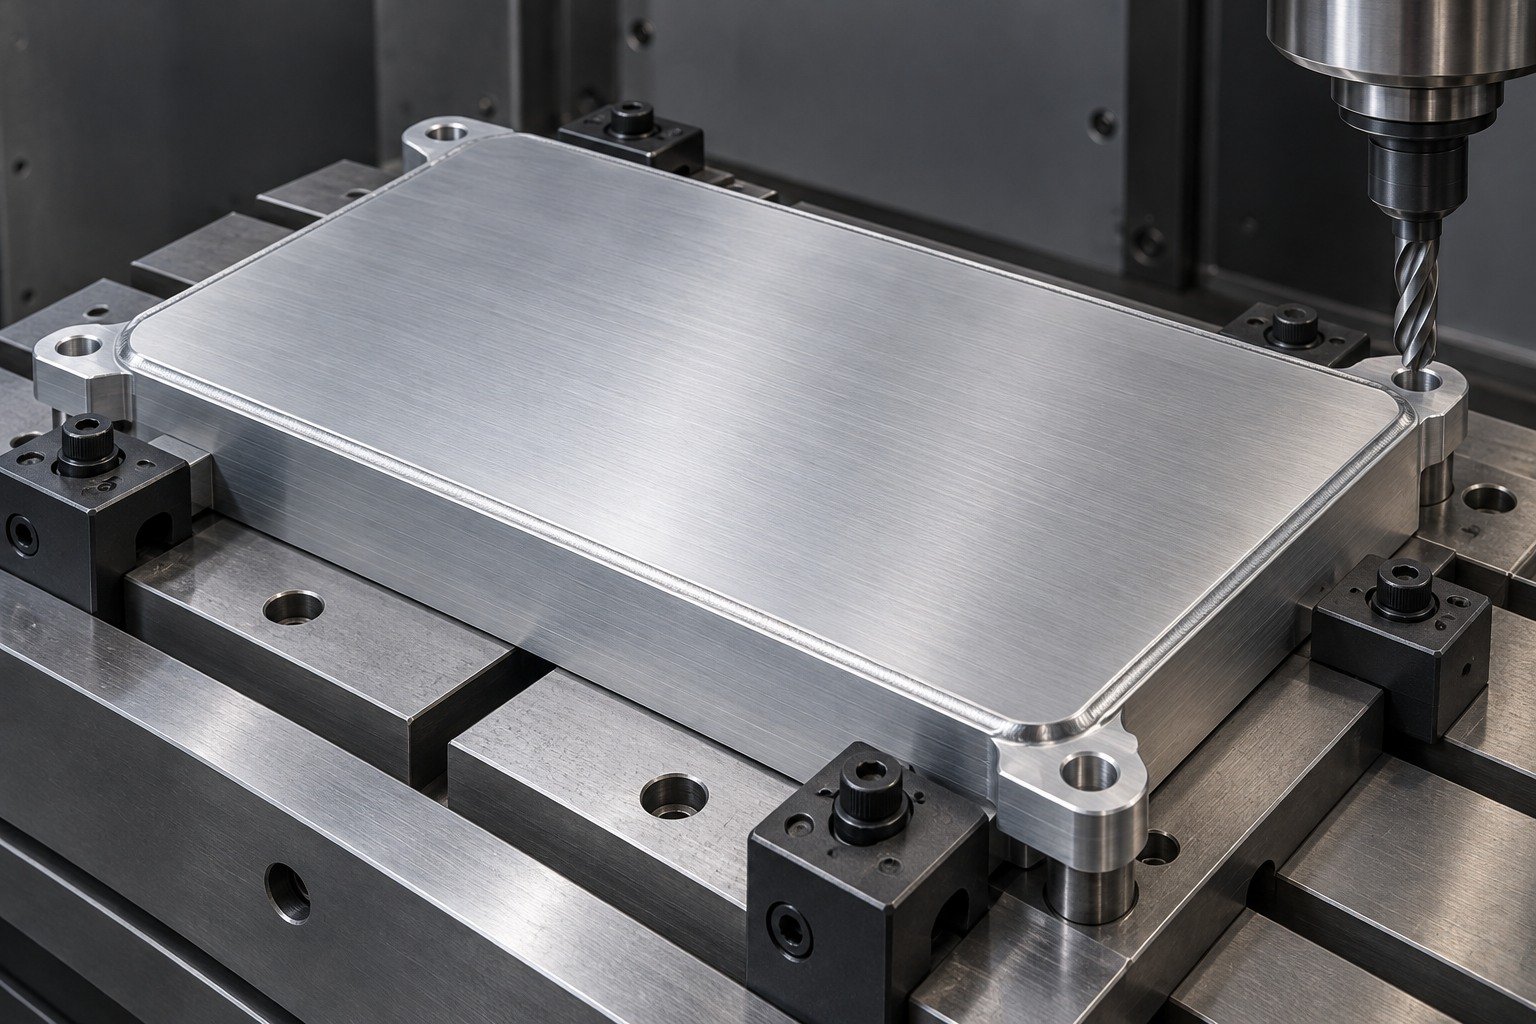
Review FSW cold plate post weld machining with the weld path, remaining cover or wall thickness and final port geometry. Agree which features are finished before and after joining.
Controlled drawing and the relevant service conditions.
Agreed method, inspection state, limits and required records.
Illustrative engineering concept
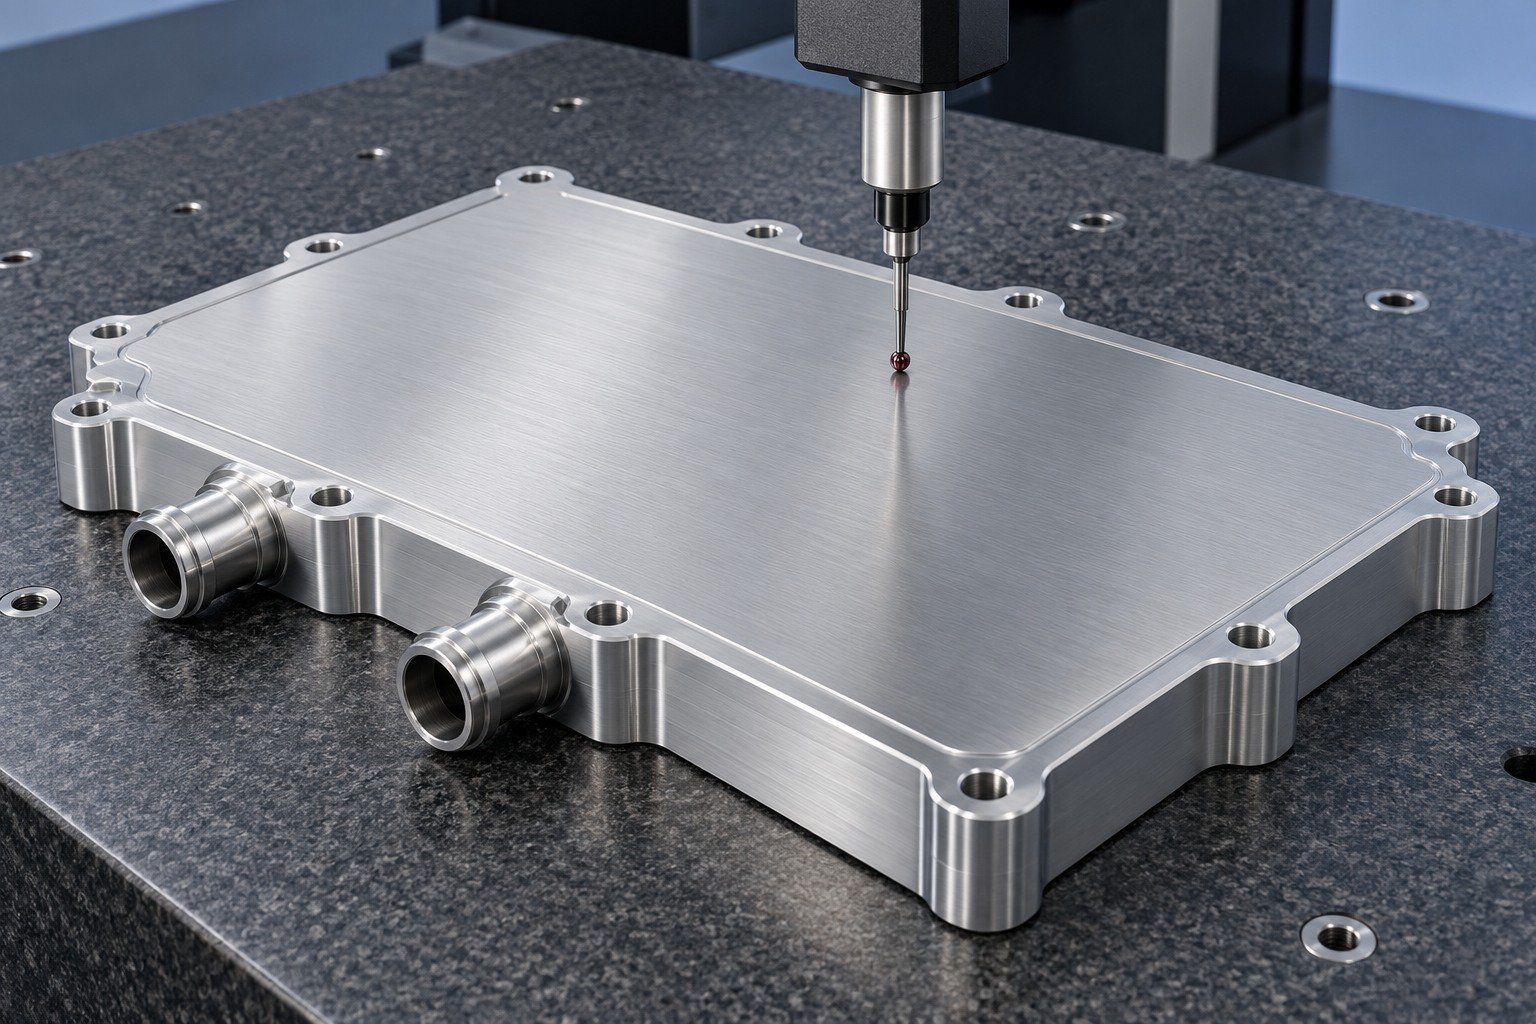
Confirm revision, interfaces and operating inputs.
Agree materials, joining and final machining.
Review the finished component and assembly fit.
Assess specified dimensions, joints and test records.
Release the accepted revision, packaging and repeat-order scope.
Illustrative component concept
When you compare an FSW cold plate manufacturer or an FSW cold plate supplier, request a sample plan tied to your actual drawing. Your FSW cold plate prototype should identify material, released joint geometry, agreed joining records, final dimensional results and the specified leak or pressure evidence. Thermal performance needs its own conditions and approval scope.
Project suitability, manufacturing scope and required records are confirmed from your drawing. These are application review topics, not customer case studies or system certifications.
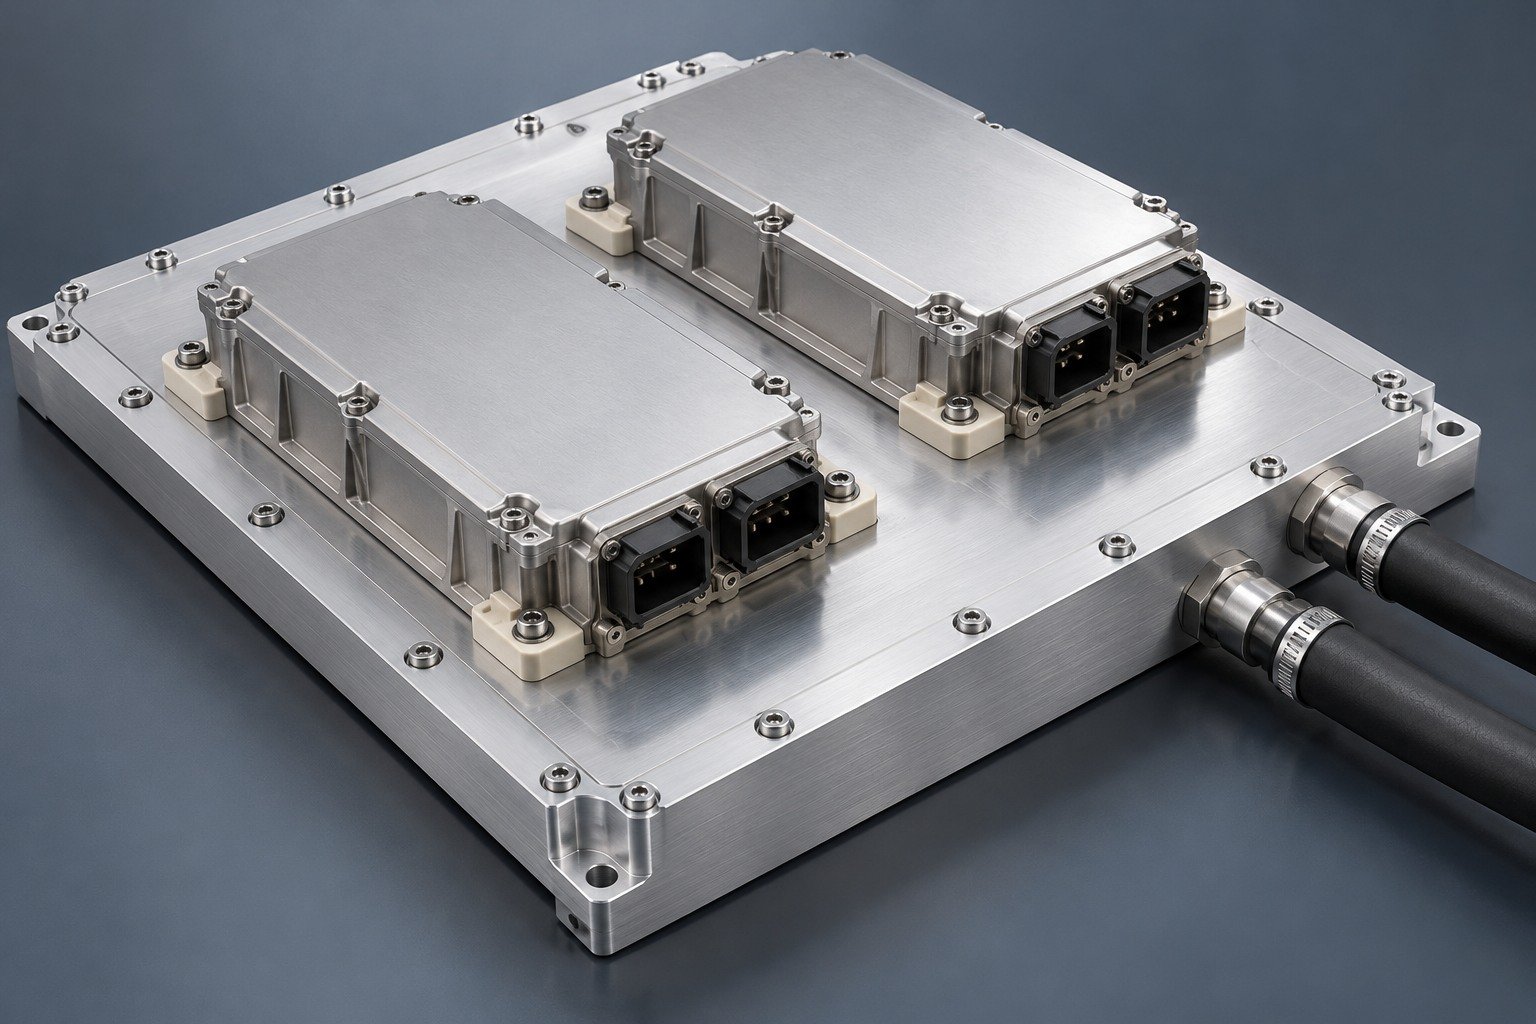
Match module footprint, insulation, clamp load and the heat-source map.
Review switching heat loads, service temperatures and mounting interfaces.
Agree operating conditions and the component acceptance scope.
Review temperature stability requirements, coolant or airflow and service access.
Review the exact device footprint, coolant connections and loop conditions.
Identify instrument clearances, heat loads and service access.
Define contact layout, inlet conditions and the agreed validation scope.
Match the enclosure interfaces, fluid connections and maintenance plan.
Illustrative assembly and application review topics; no customer case study, system certification or universal fit claim. Explore application requirements →
Ask your quote to separate component manufacturing, joining, finishing, inspection and any independently agreed validation. The drawing review confirms availability, quantities and delivery scope.
Provide base and cover geometry, material and condition, cover thickness, channel and rib layout, weld land, access restrictions, final datums and the proposed acceptance checks. Confirm the joint and fixture concept before committing to detailed machining.
Post-weld machining can be reviewed as part of the route. Define which faces, ports and mounting features need final machining, the available allowance and the required remaining wall or cover thickness. The drawing review confirms feasibility.
A leak test evaluates a defined sealing limit using its specified medium and method. A proof-pressure check evaluates an agreed structural pressure condition. Neither alone proves cooling performance, and burst testing is a separate destructive requirement.
Identify the applicable 6061 product specification, starting temper, base and cover thicknesses, joint geometry and required final condition. A 6061-T6 stock data sheet does not certify the properties of the finished welded part.
For an FSW cold plate for battery cooling, review pack interfaces, coolant routing and the defined component test scope. For an FSW cold plate for power electronics, review the module footprint, electrical isolation responsibility, contact stack and heat-source map. Confirm suitability for the actual assembly.
A custom FSW cold plate quote should separate base and cover machining, joining development or agreed process work, finishing, final machining, inspection and the required sample records. Quantities and delivery depend on the released scope; no universal lead time or performance figure is assumed.









