

Injection Molding
Tooling and molding for your repeat plastic parts.
From prototype to production, coordinated manufacturing solutions for your custom parts.
View All Services →
Precision parts for your tight tolerances and complex geometry.
Tooling and molding for your repeat plastic parts.

Metal casting options for your part and production volume.

Cutting, forming and welding for your fabricated parts.

Custom profiles for your section, length and finish requirements.

Finishes for your appearance, corrosion and wear requirements.

Sub-assemblies and final builds for your production program.

Production tooling built around your process and volume.

Prototype parts to check fit, function and design.
DFM, process planning and production support for your project.
Inspection, documentation, inventory and delivery planning for your program.
Choose air- or liquid-cooling components around your thermal and mechanical requirements.

Manufacturing support for your cold plates, manifolds and cooling assemblies.

Find components for your power electronics, energy, laser and telecom application.

Components for your electronic systems.
Start with your functional and quality requirements.
Build around your operating environment.
From prototype to production, review material performance, manufacturability and cost for your part.
Review grade, temper and finish for your metal parts.
 AluminumStrength, weight and machining›
 Stainless SteelCorrosion and finish requirements›
 Carbon & Alloy SteelDiscuss grade and heat treatment›
 Tool SteelDiscuss tooling and wear needs›
 TitaniumReview grade and part geometry›
 Copper & BrassDiscuss conductivity and machining›
Match your polymer to function, process and environment.
 ABSReview enclosure and molding needs›
 Polycarbonate (PC)Discuss clarity and impact needs›
 Nylon (PA)Review moisture and wear conditions›
 POM / AcetalReview fit and sliding features›
 PEEKDiscuss operating conditions›
 PTFEReview friction and chemical exposure›
 ULTEM / PEIDiscuss thermal and electrical needs›
Confirm grade availability and application requirements.
 Silicone / LSRDiscuss flexible component needs›
 TPU / TPEReview flexibility and processing›
 EPDMReview weathering and chemical exposure.›
 NBRReview oil and fuel exposure.›
 FKMReview temperature and chemical exposure.›
 G10 / FR4Review insulation and laminate needs›
 CompositesReview stiffness, weight and laminate.›Customer-Specified MaterialsConfirm your grade and requirements.›Other Specialty MaterialsDiscuss your application and grade.›
Practical guidance for your part geometry and material decisions.
Prepare your process, budget and sourcing questions.
Build your knowledge before production.
Learn who we are and how we operate.
Find our U.S. support team or start a conversation.
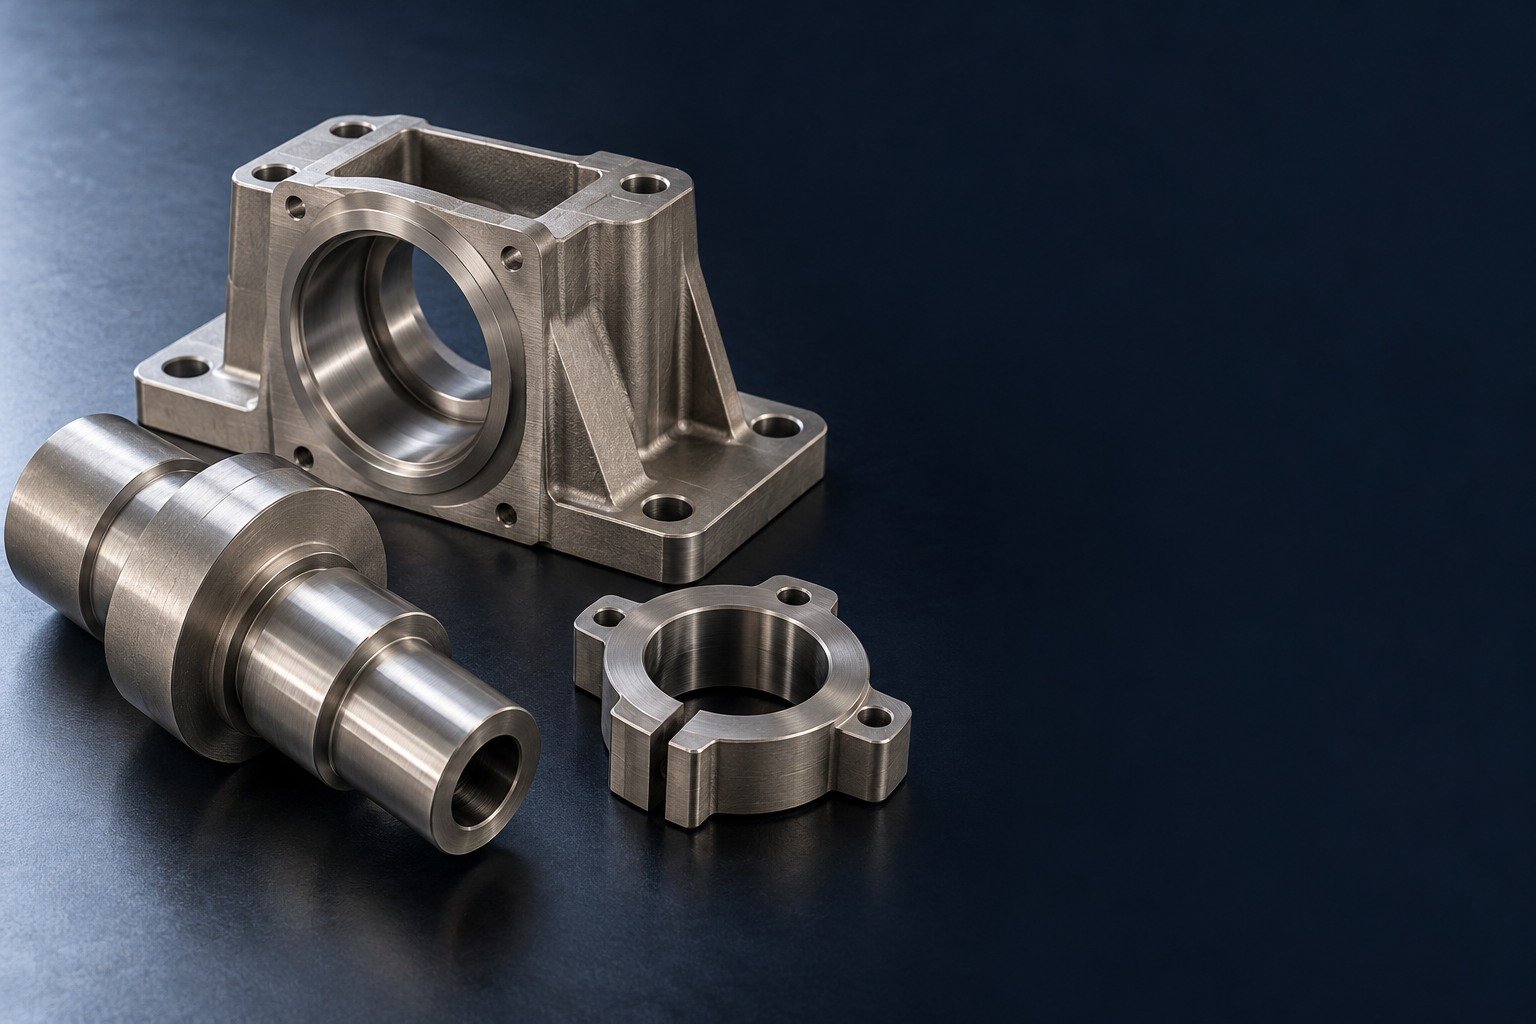
For your Grade 4 titanium machining services inquiry, connect the exact CP grade and stock condition to your locating shoulders, supported bores and final assembly fits. Resolve machining access, surface acceptance and material records before your first sample.
Commercially pure titanium Grade 4 / UNS R50700 is unalloyed titanium with controlled residual and interstitial limits. For your Grade 4 titanium properties review, distinguish the plate reference below from the actual bar, tube or plate specified on your purchase order.
Your U.S. grade identifier; state the applicable product standard and revision.
HSM lists 3.7064 and 3.7065 against Grade 4. These are supply comparison references; confirm the exact form and specification before approving a change.
CP titanium Grade 4 is a material designation, not a complete purchase order. State bar, plate or tube and the applicable standard; a plate table does not accept a tube or finished pressure component.
| Element | ATI CP Grade 4 · max wt.% |
|---|---|
| Fe | 0.50 |
| O | 0.40 |
| C | 0.08 |
| N | 0.05 |
| H | 0.015 |
| Ti | Balance |
ATI published plate reference. Values are maxima except titanium balance; verify the ordered material and lot certificate. No unlisted addition is inferred.
ATI published plate minima · MPa · common axis 0–600 MPa
Producer plate minima, not your lot report or finished-part rating. Grade 4 titanium tensile strength depends on the actual ordered form and condition. These values do not establish fatigue life, corrosion suitability or a substitution approval.
ATI CP Grade 4 ↗ ATI CP Grade 2 ↗ European comparison list ↗
Select your component, then connect machining, supplied condition and final acceptance.
For custom Grade 4 titanium parts with locating shoulders, show the complete short-shaft geometry and mating drawing. Identify the final support state and distinguish working diameters from noncritical reliefs.
| Your decision | What to define |
|---|---|
| Your fit | Shoulder position, controlled diameter, coaxial bore and mating fit. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
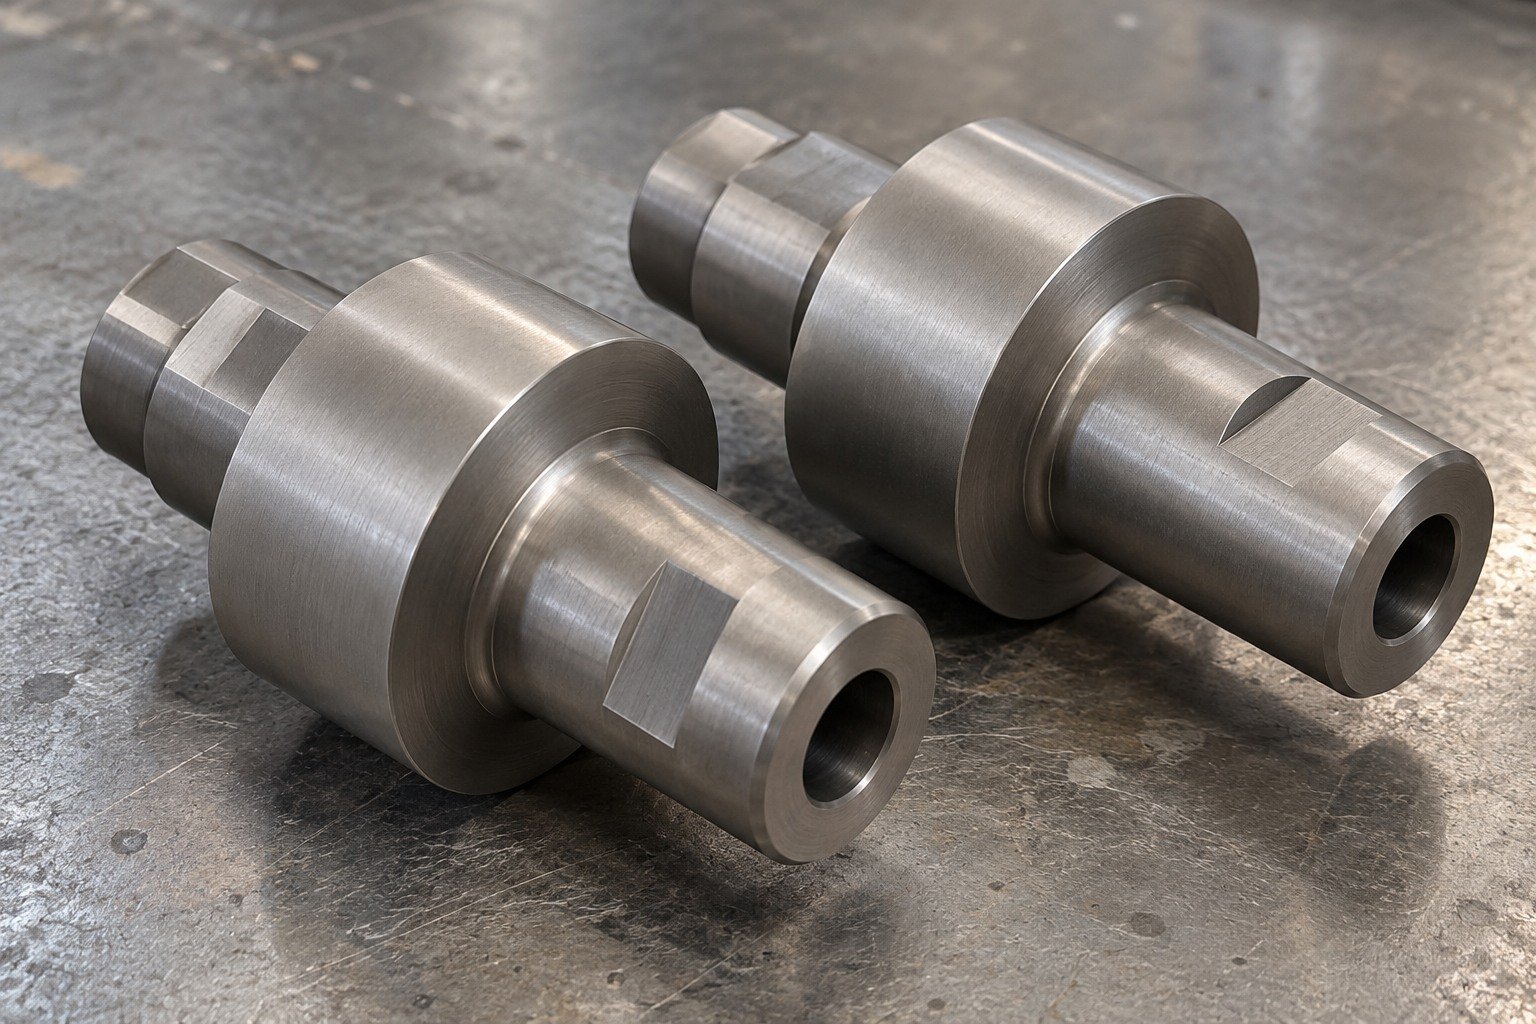
For Grade 4 titanium turning services, connect roughing and finishing to a stable datum. Review support, tool engagement and cutting-fluid delivery around your actual short shaft.
| Your decision | What to define |
|---|---|
| Your fit | Shoulder position, controlled diameter, coaxial bore and mating fit. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
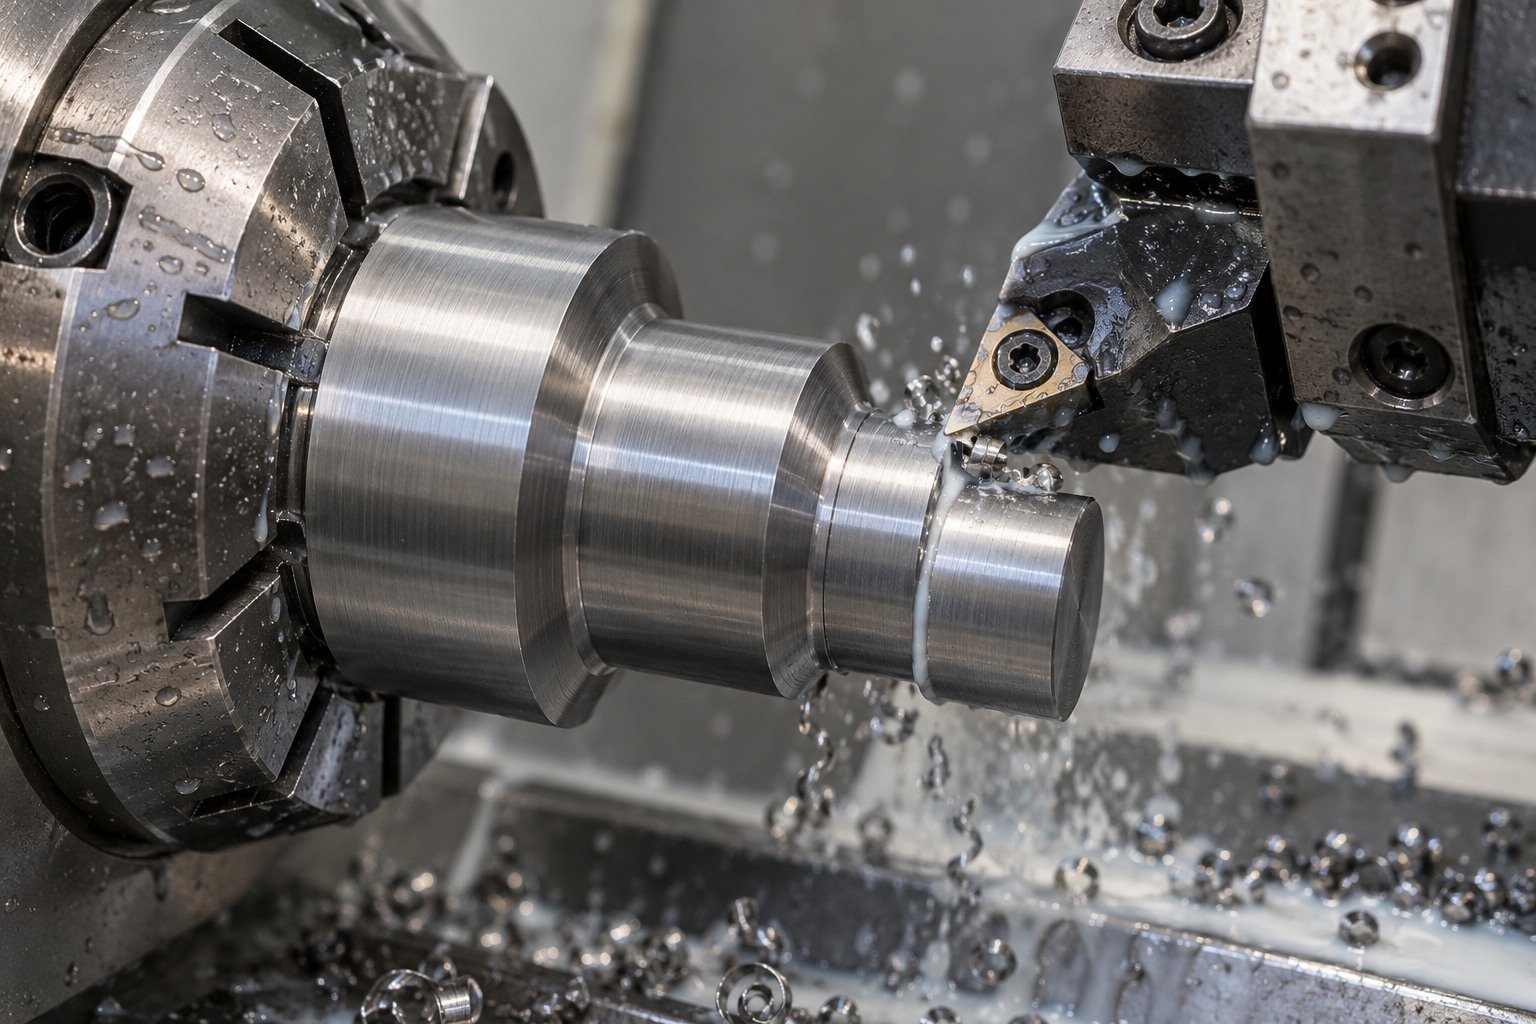
Specify exact stock form, condition and lot identity. Retained finishing stock and setup sequence are reviewed for your geometry, not a generic allowance.
| Your decision | What to define |
|---|---|
| Your fit | Shoulder position, controlled diameter, coaxial bore and mating fit. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
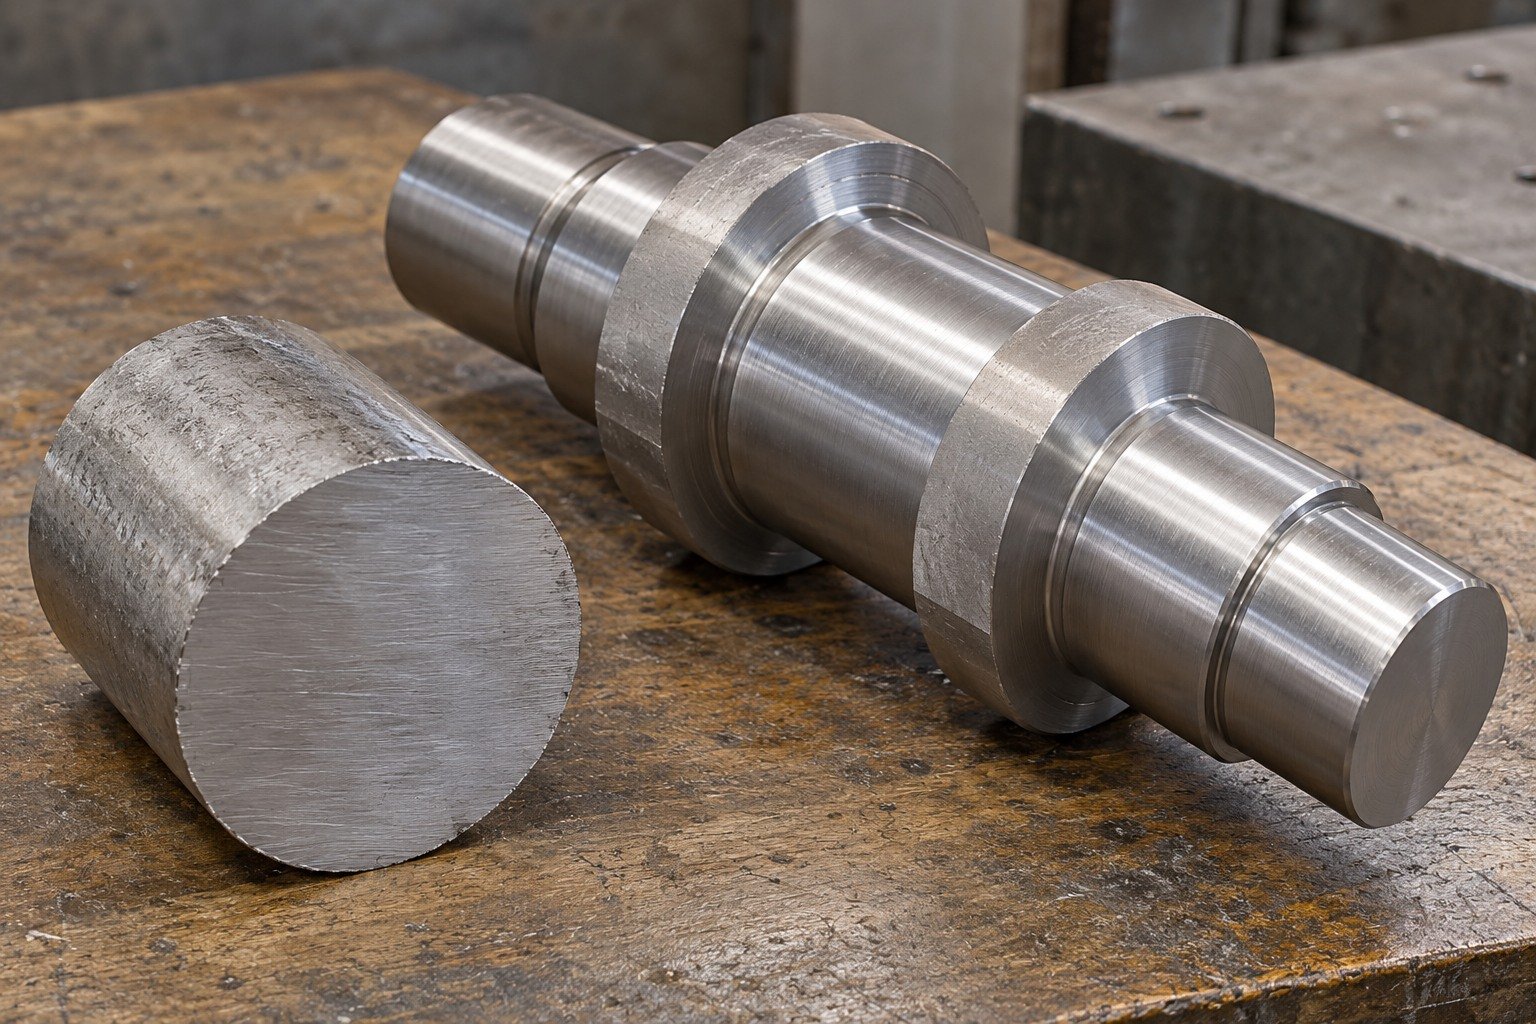
Measure locating shoulders and bore relationships after the agreed route. Keep your controlled fit and measurement support explicit before repeat quantities.
| Your decision | What to define |
|---|---|
| Your fit | Shoulder position, controlled diameter, coaxial bore and mating fit. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
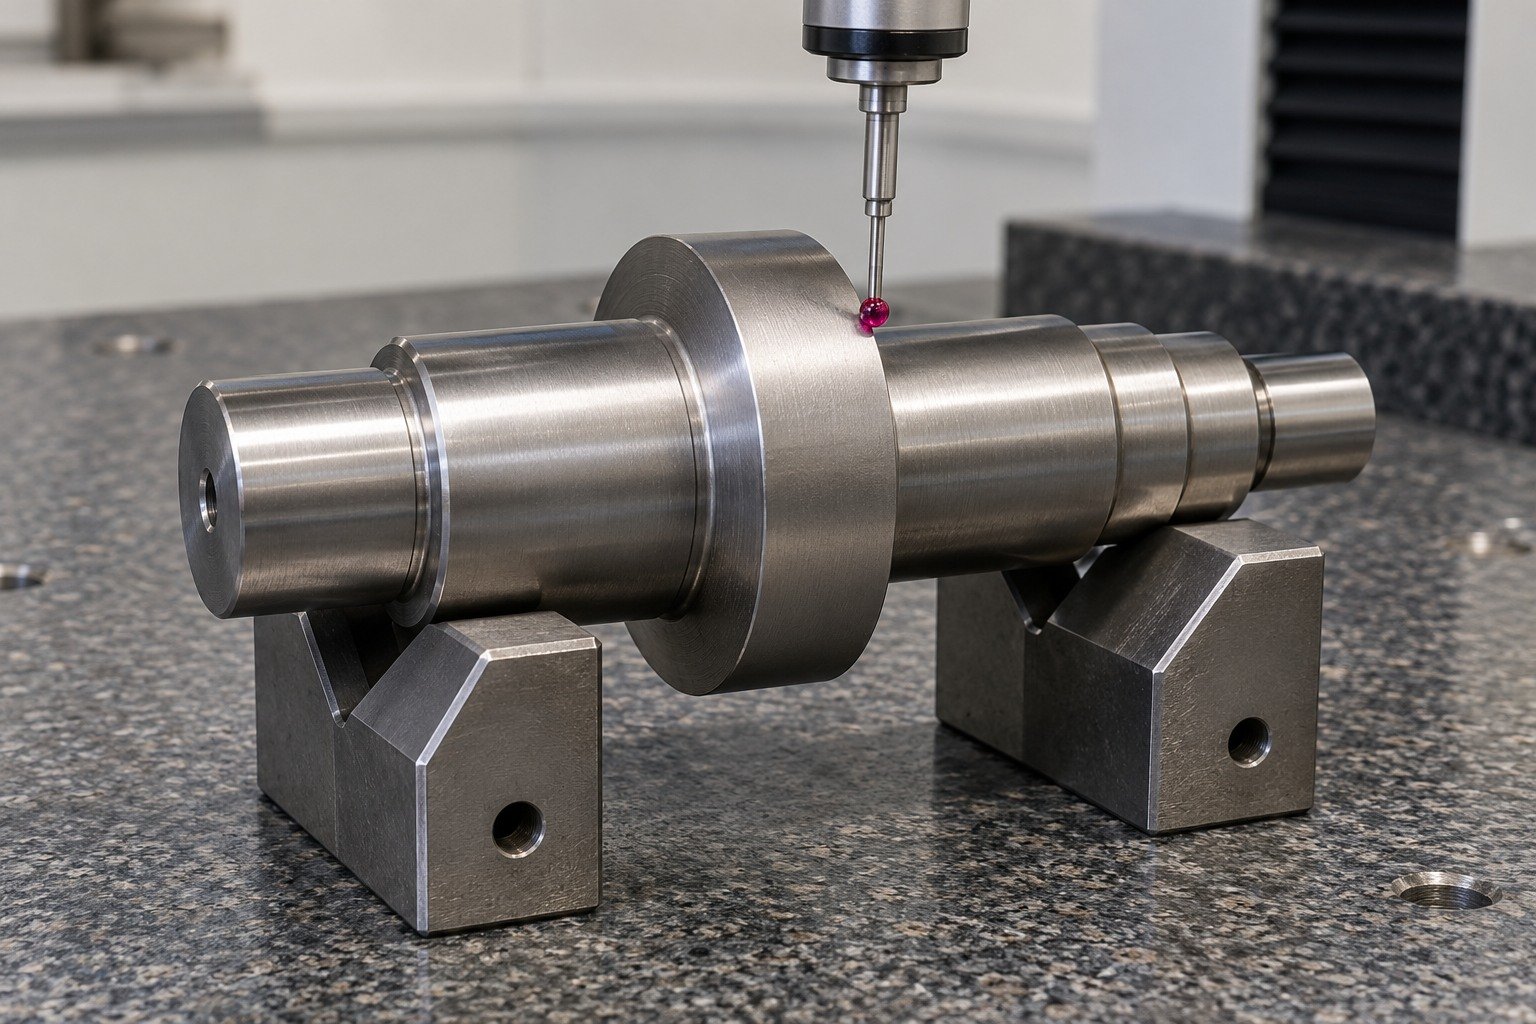
For your Grade 4 titanium CNC machining inquiry, define the housing bore, broad mounting face and supported wall sections together. Provide mating bearing or bushing information where it clarifies the accepted geometry.
| Your decision | What to define |
|---|---|
| Your fit | Bore datum, flange face, support pads and mounting pattern. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
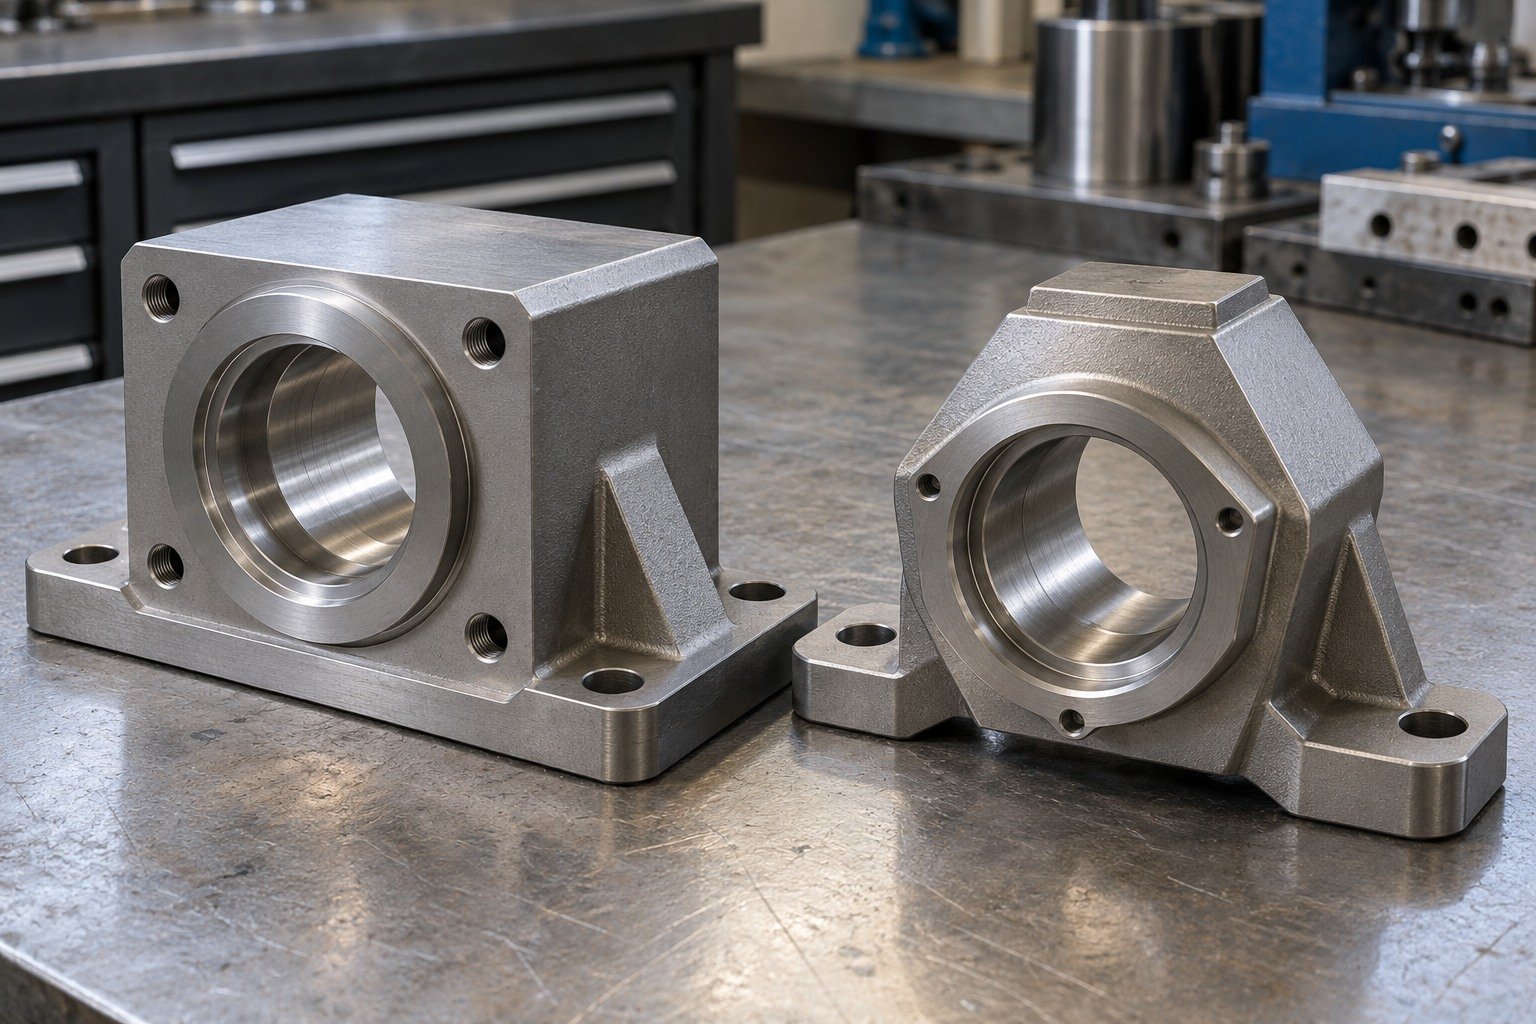
For Grade 4 titanium milling services, review accessible pocket radii, wall support and the final locating plane. Connect Grade 4 titanium drilling to depth, chip escape and gauge access.
| Your decision | What to define |
|---|---|
| Your fit | Bore datum, flange face, support pads and mounting pattern. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |

For Grade 4 titanium chemical processing parts, include medium, temperature, load and mating materials. Neither the grade label nor the housing photograph establishes service acceptance.
| Your decision | What to define |
|---|---|
| Your fit | Bore datum, flange face, support pads and mounting pattern. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
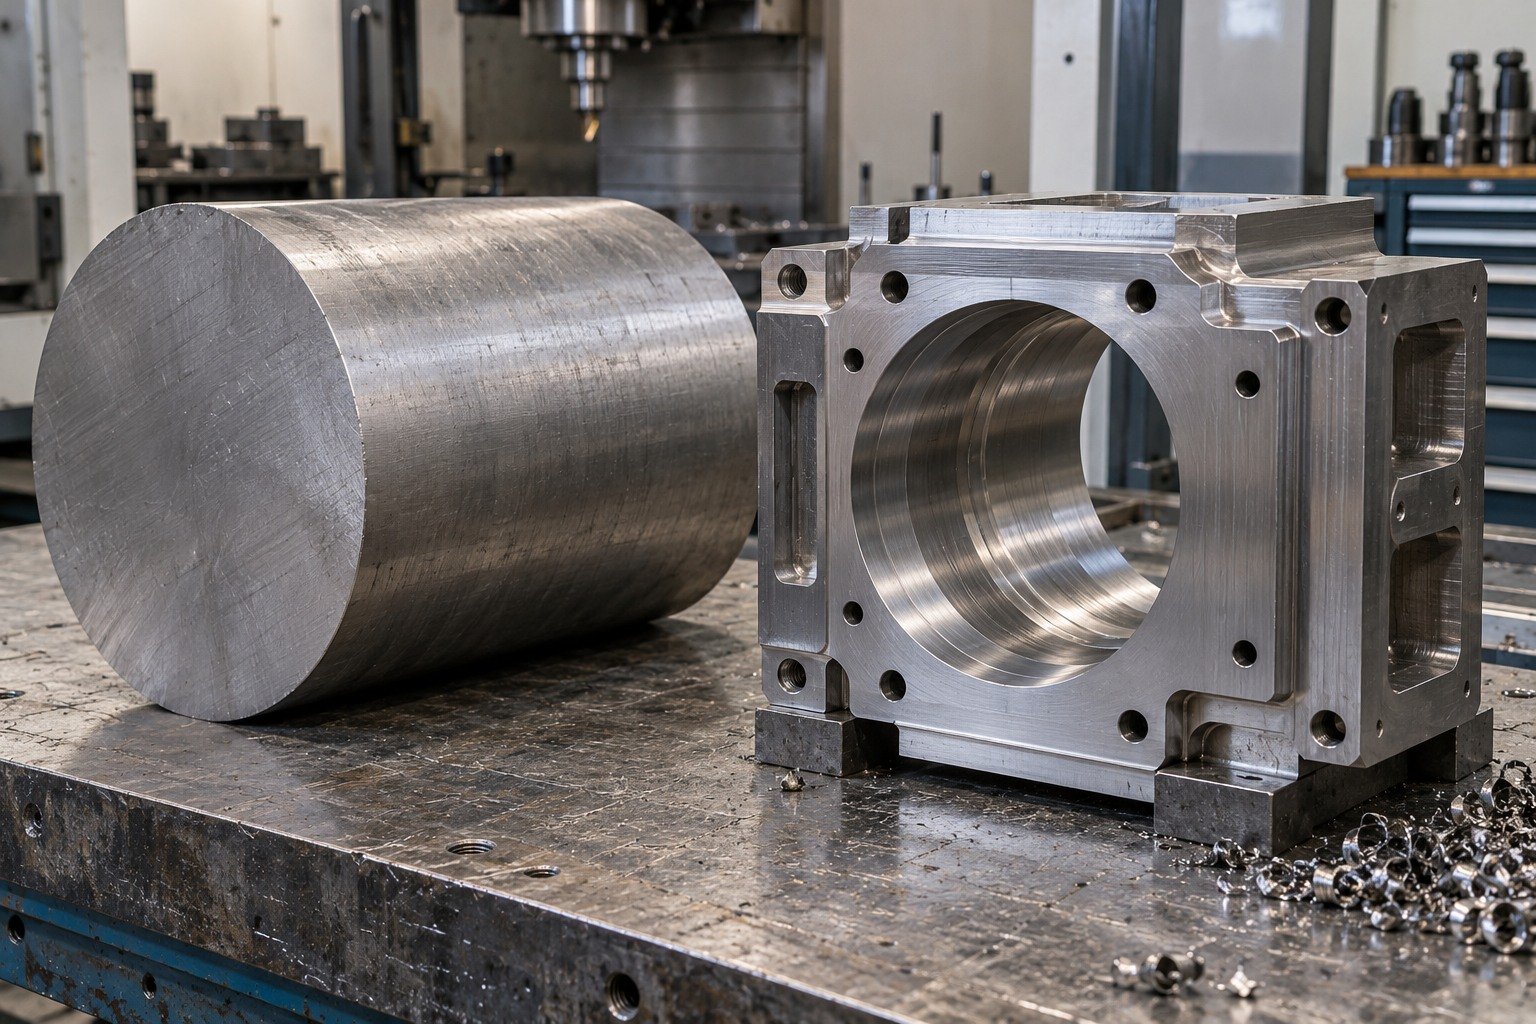
Inspect the accessible datum face and bore in the final support state. State which features need recorded results and what evidence accompanies the material lot.
| Your decision | What to define |
|---|---|
| Your fit | Bore datum, flange face, support pads and mounting pattern. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
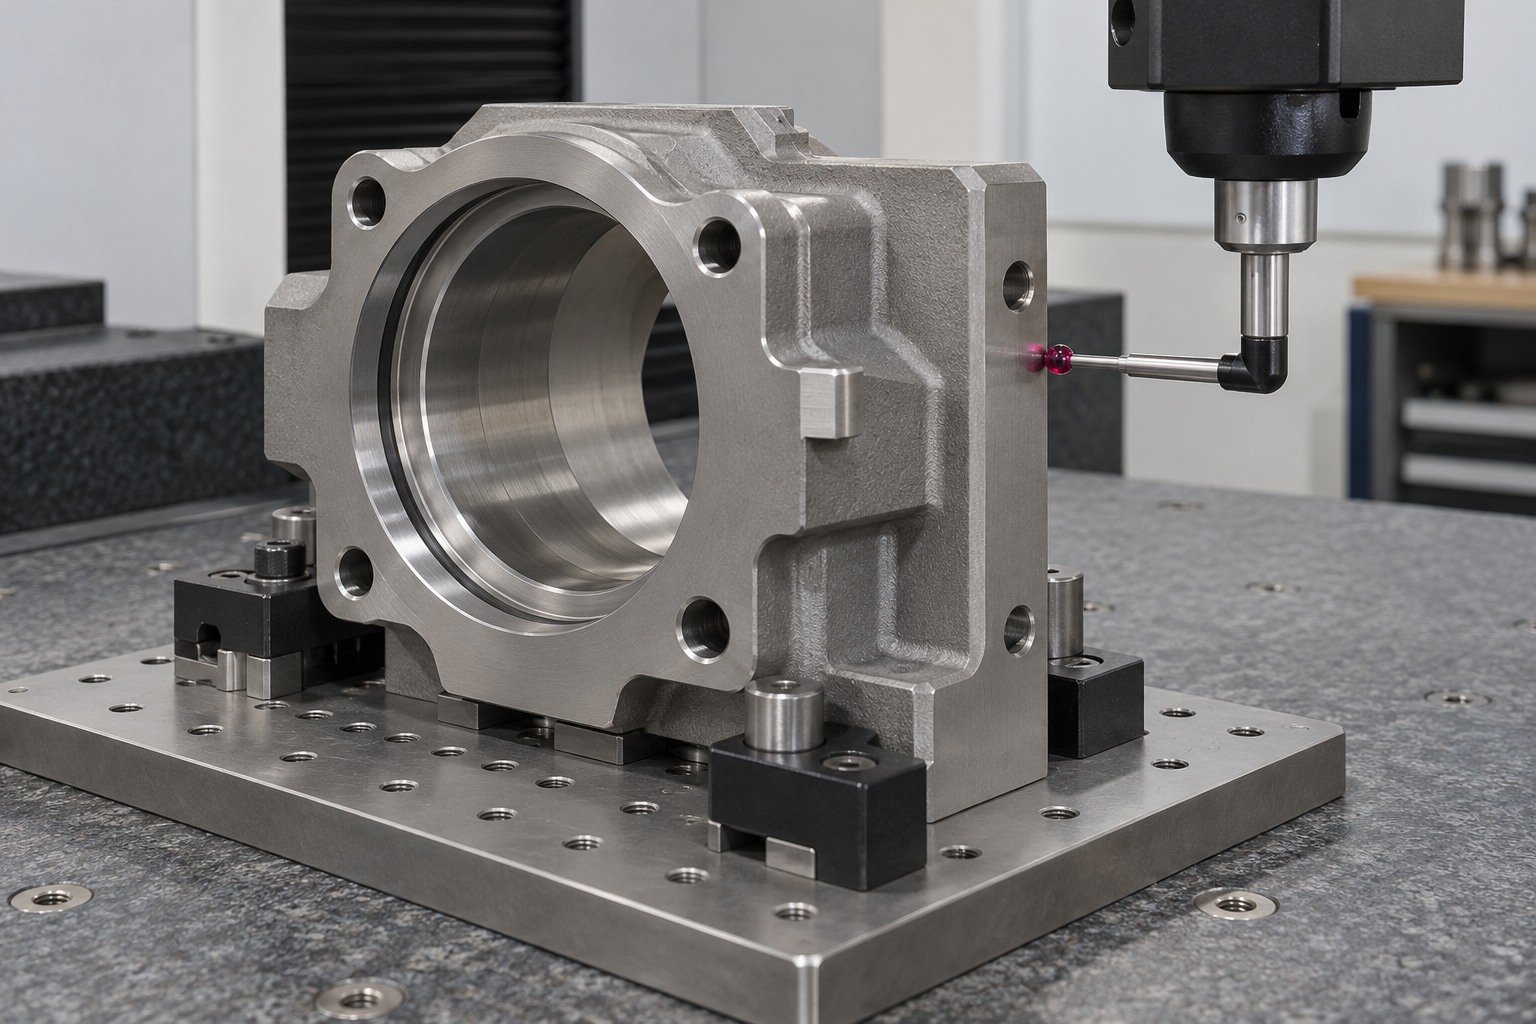
For commercially pure titanium Grade 4 CNC machining, connect mounting plates, supported ribs and offset bores to your actual assembly datums. Specify clamping-sensitive faces and the final unsupported profile.
| Your decision | What to define |
|---|---|
| Your fit | Flat mounting pad, offset bore, slot location and supported rib. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
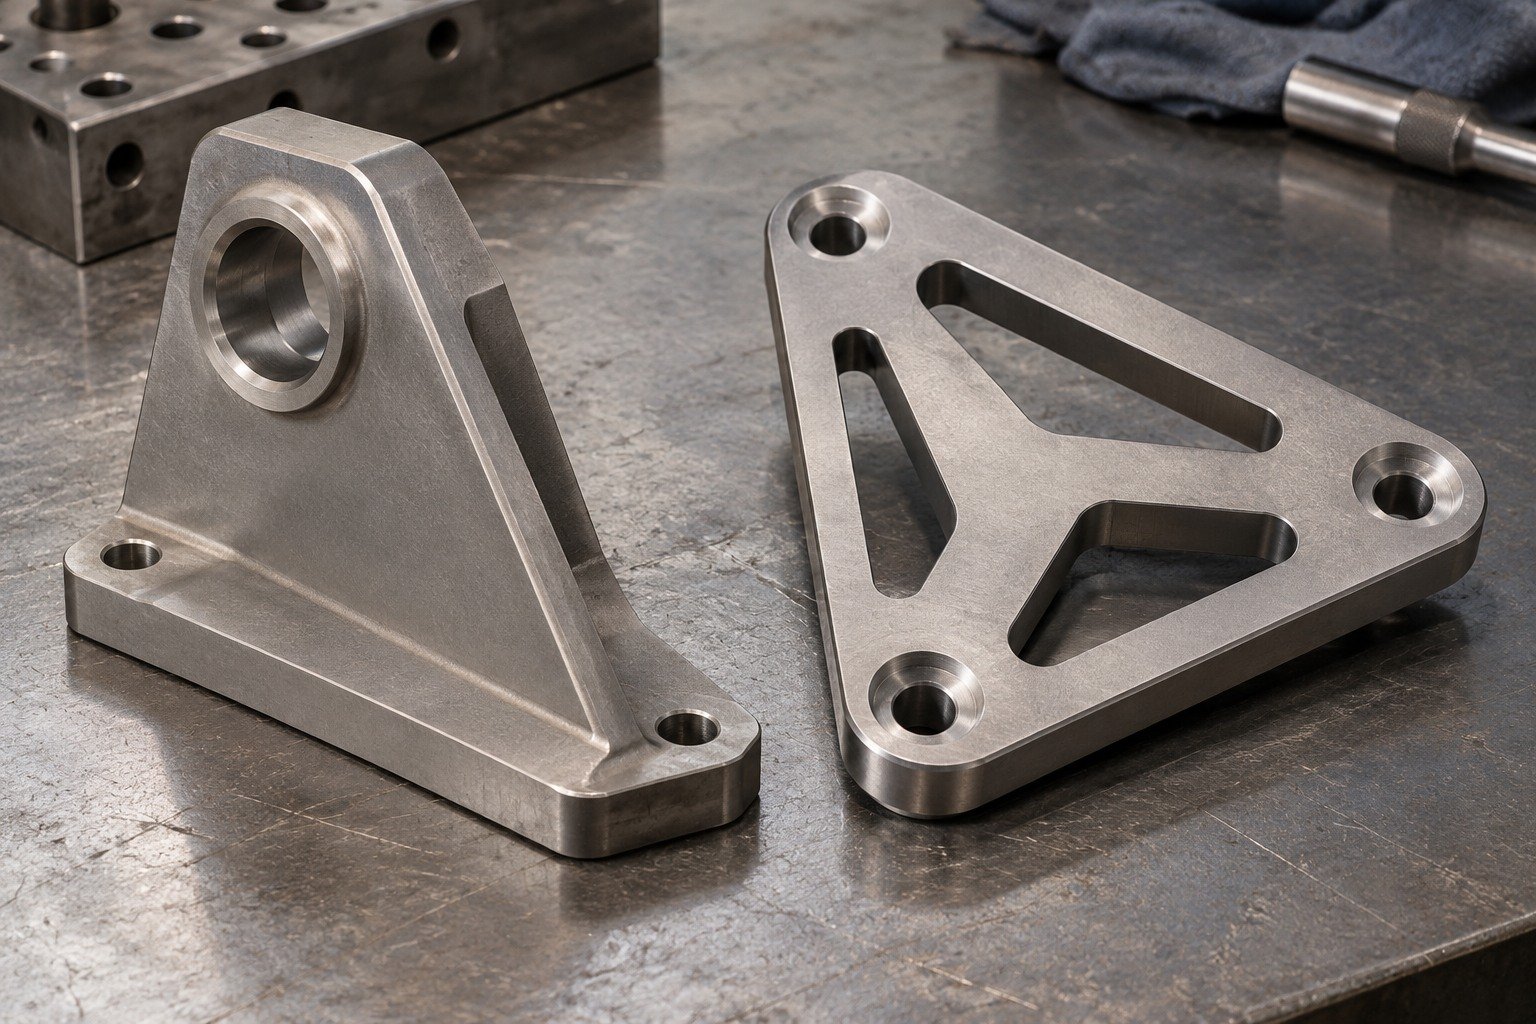
Review tool access and full backing around slots and reliefs. Cutting engagement, coolant delivery and chip removal are selected for the actual supported section.
| Your decision | What to define |
|---|---|
| Your fit | Flat mounting pad, offset bore, slot location and supported rib. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
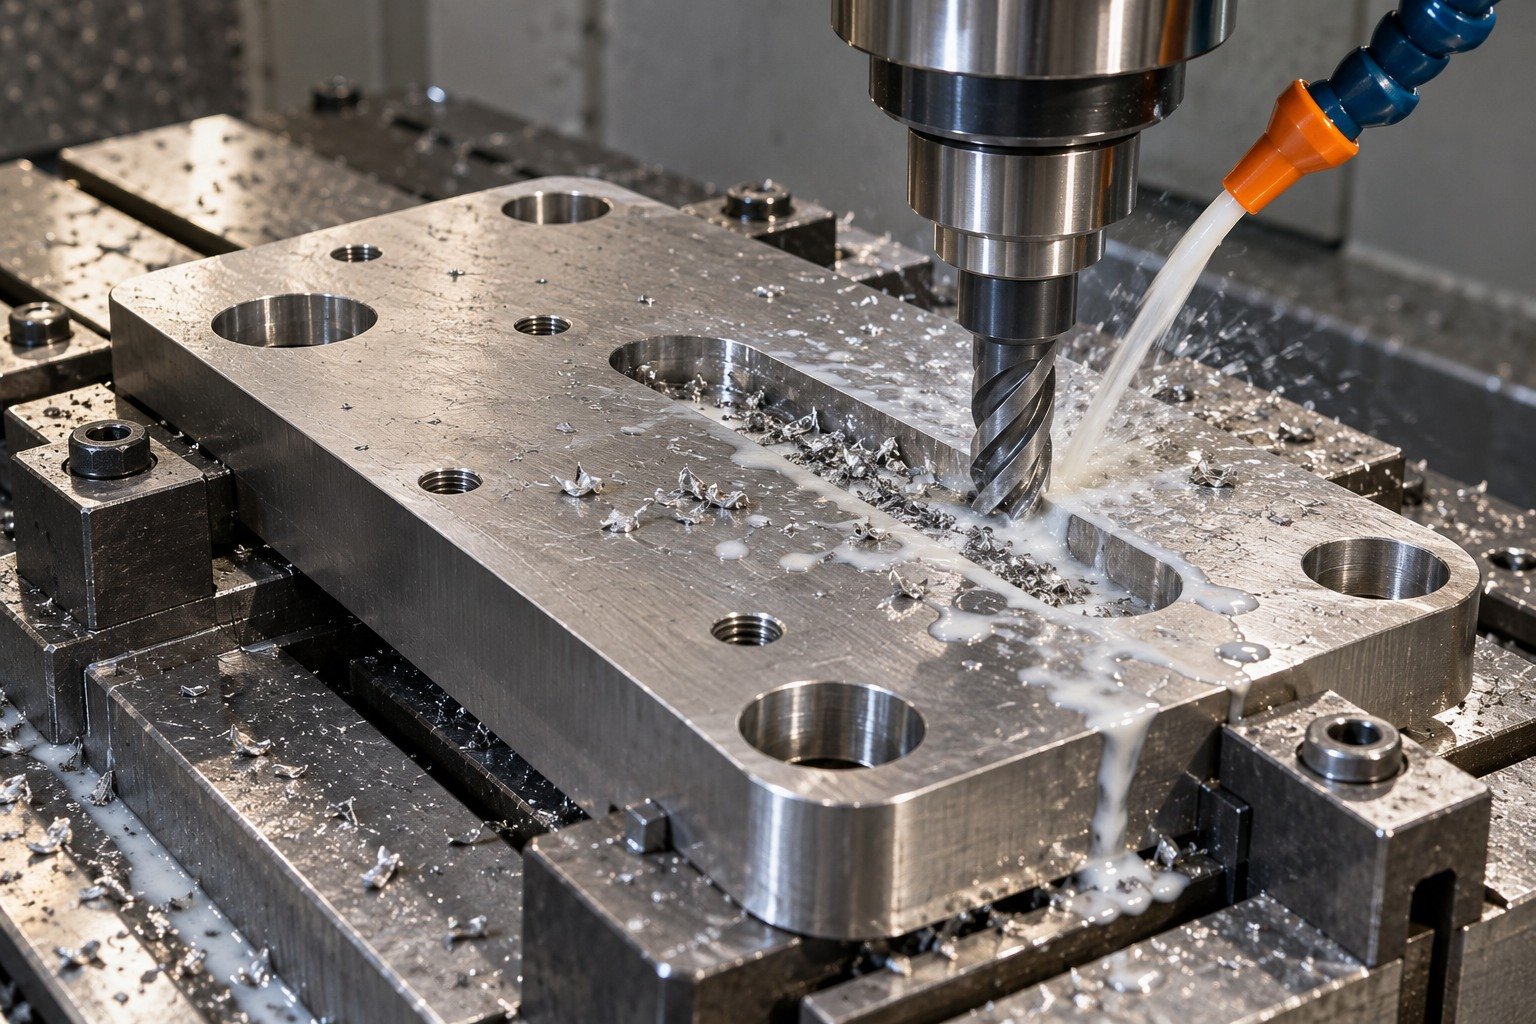
Identify the starting plate and supplied state. Separate purchased material requirements from any later treatment or surface preparation specified by your drawing.
| Your decision | What to define |
|---|---|
| Your fit | Flat mounting pad, offset bore, slot location and supported rib. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
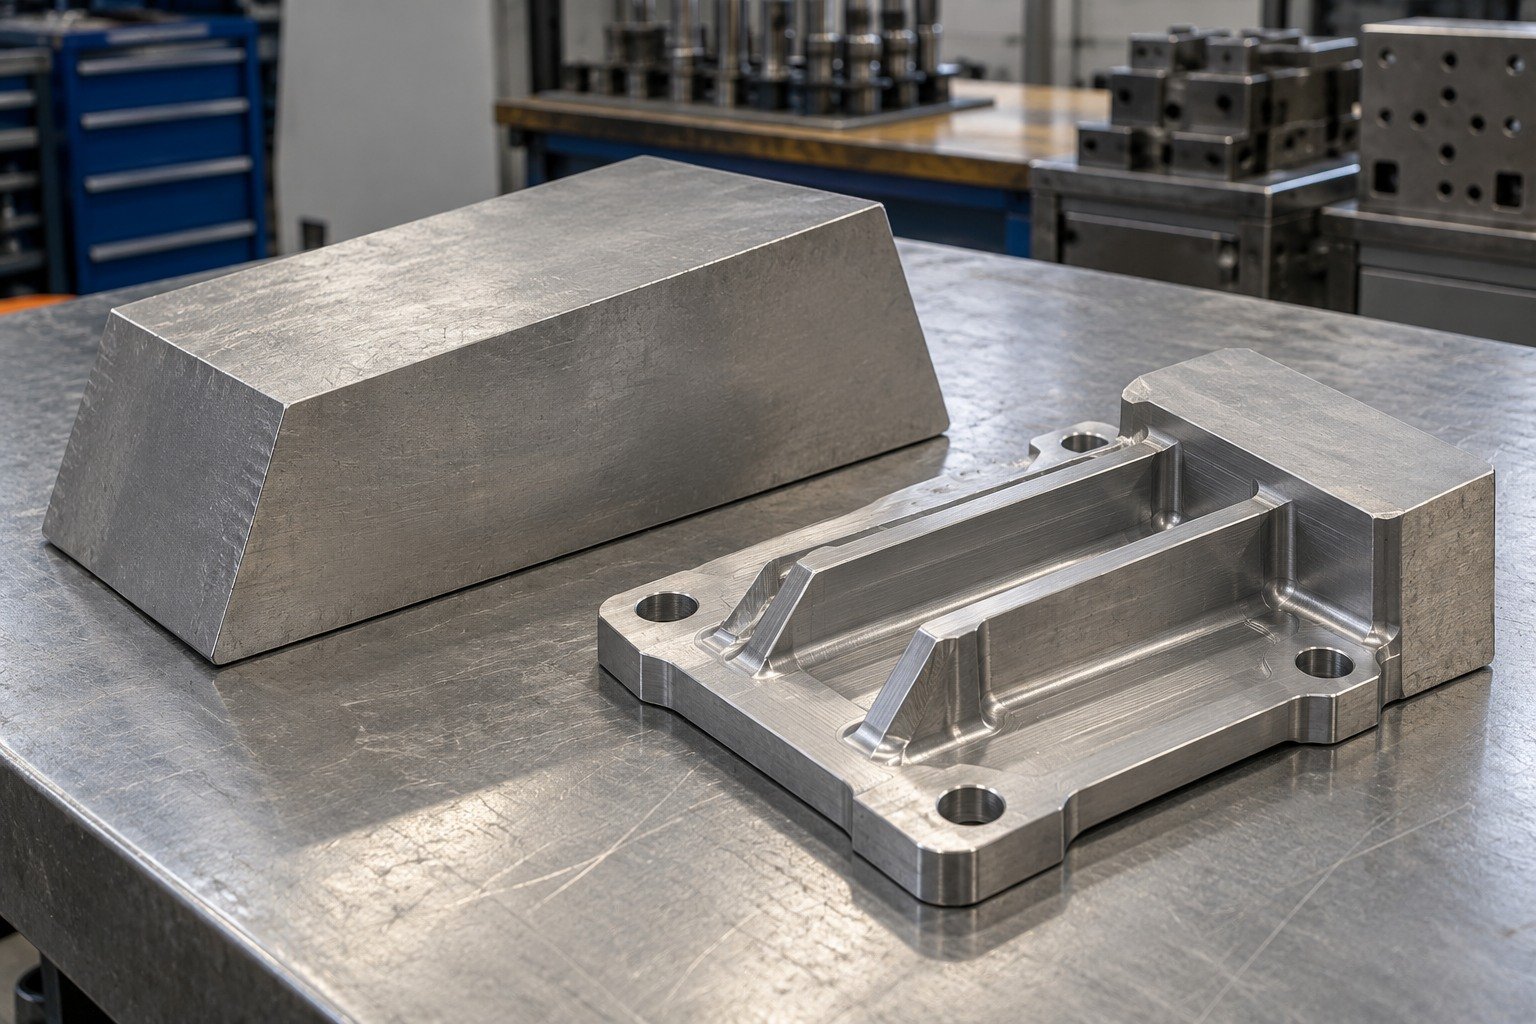
Verify pad flatness and bore position after release from the fixture. Define the accepted support condition rather than using clamped measurements as the final part result.
| Your decision | What to define |
|---|---|
| Your fit | Flat mounting pad, offset bore, slot location and supported rib. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |

For Grade 4 titanium machined components such as broad locating collars, identify the bore, seating shoulder and controlled contact area. Review the split or clamping ear only when it is part of your drawing.
| Your decision | What to define |
|---|---|
| Your fit | Locating bore, seating face, contact area and any split detail. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
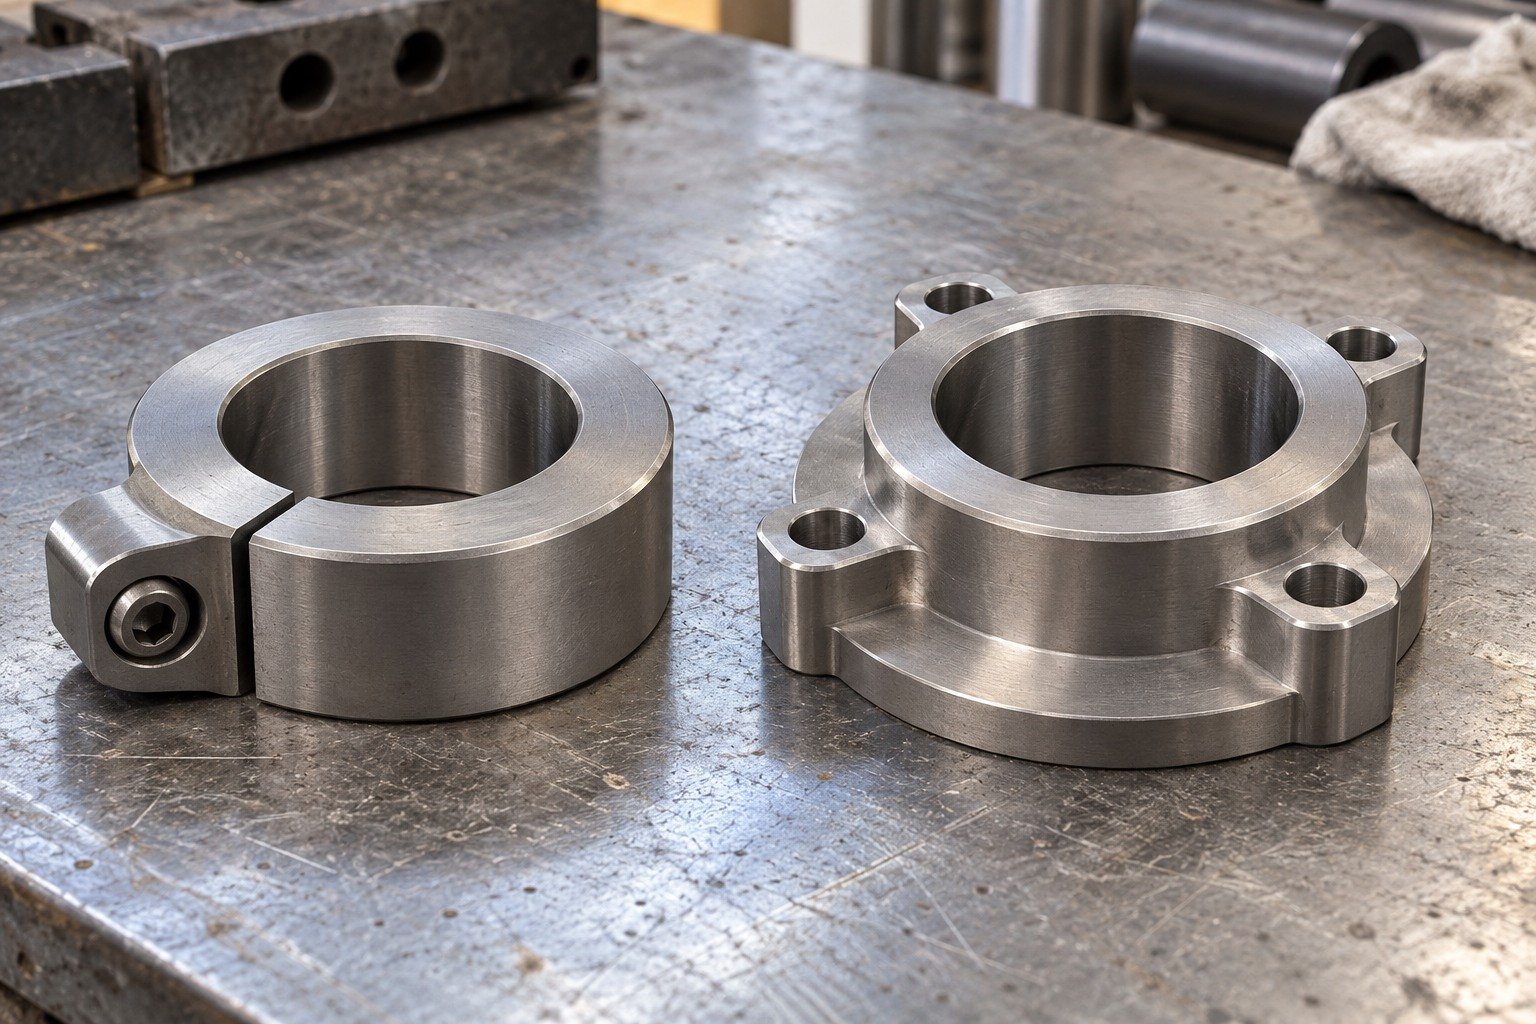
Review Grade 4 titanium threading with the actual engagement, mating material, access and gauge. Separate thread function from adjacent cosmetic surfaces.
| Your decision | What to define |
|---|---|
| Your fit | Locating bore, seating face, contact area and any split detail. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
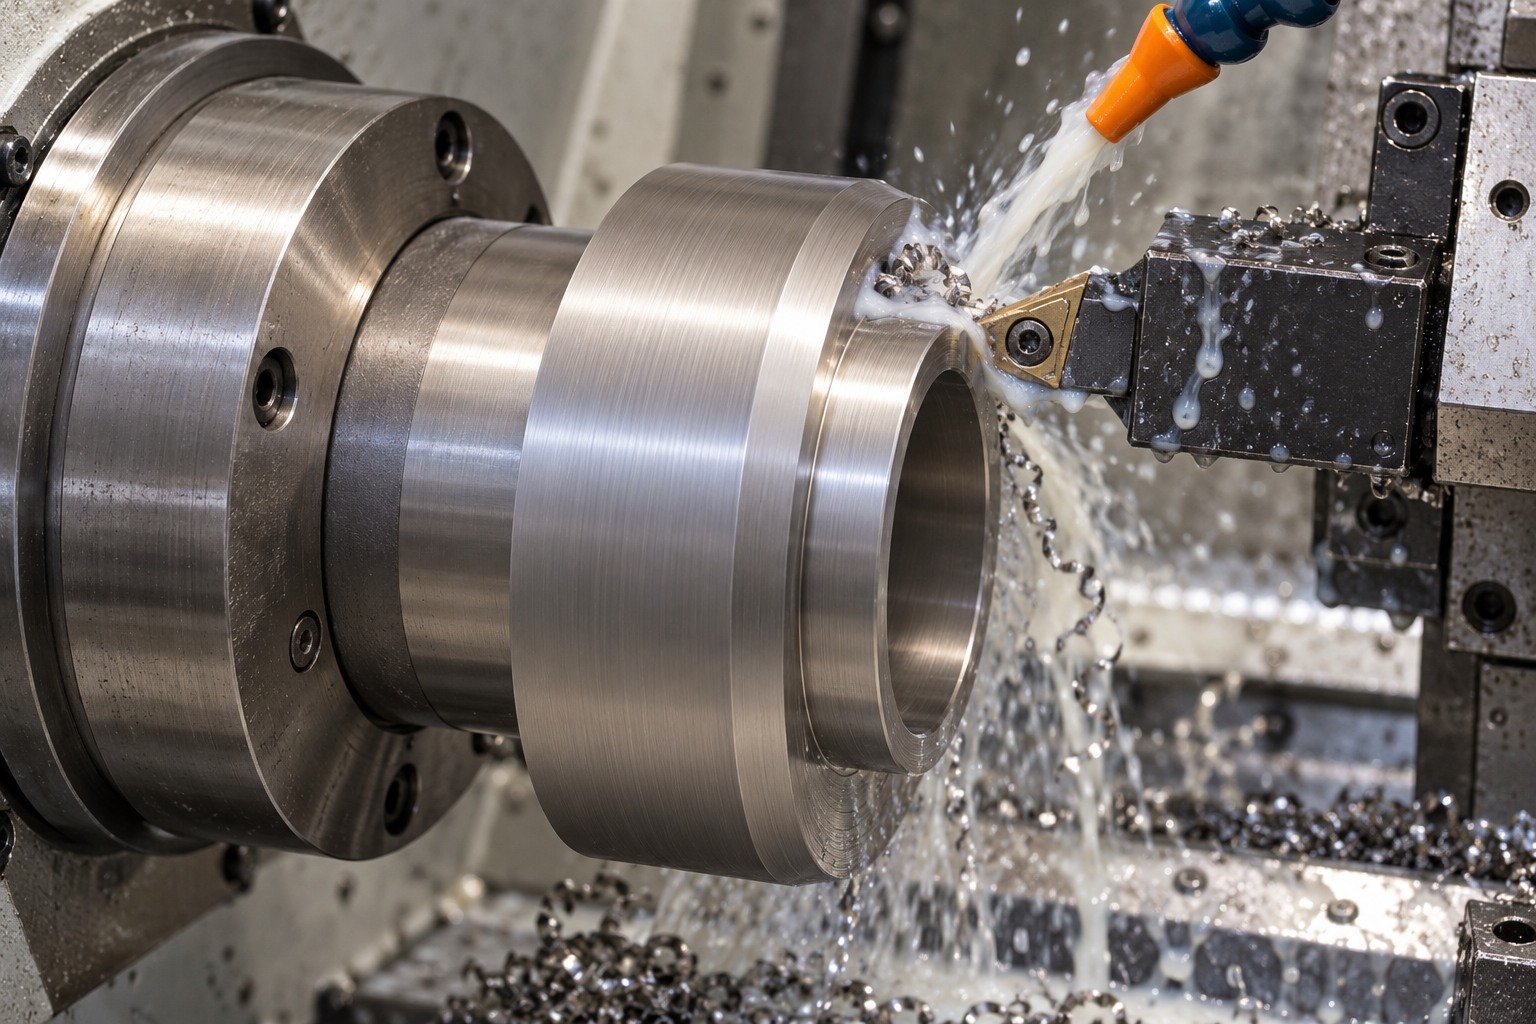
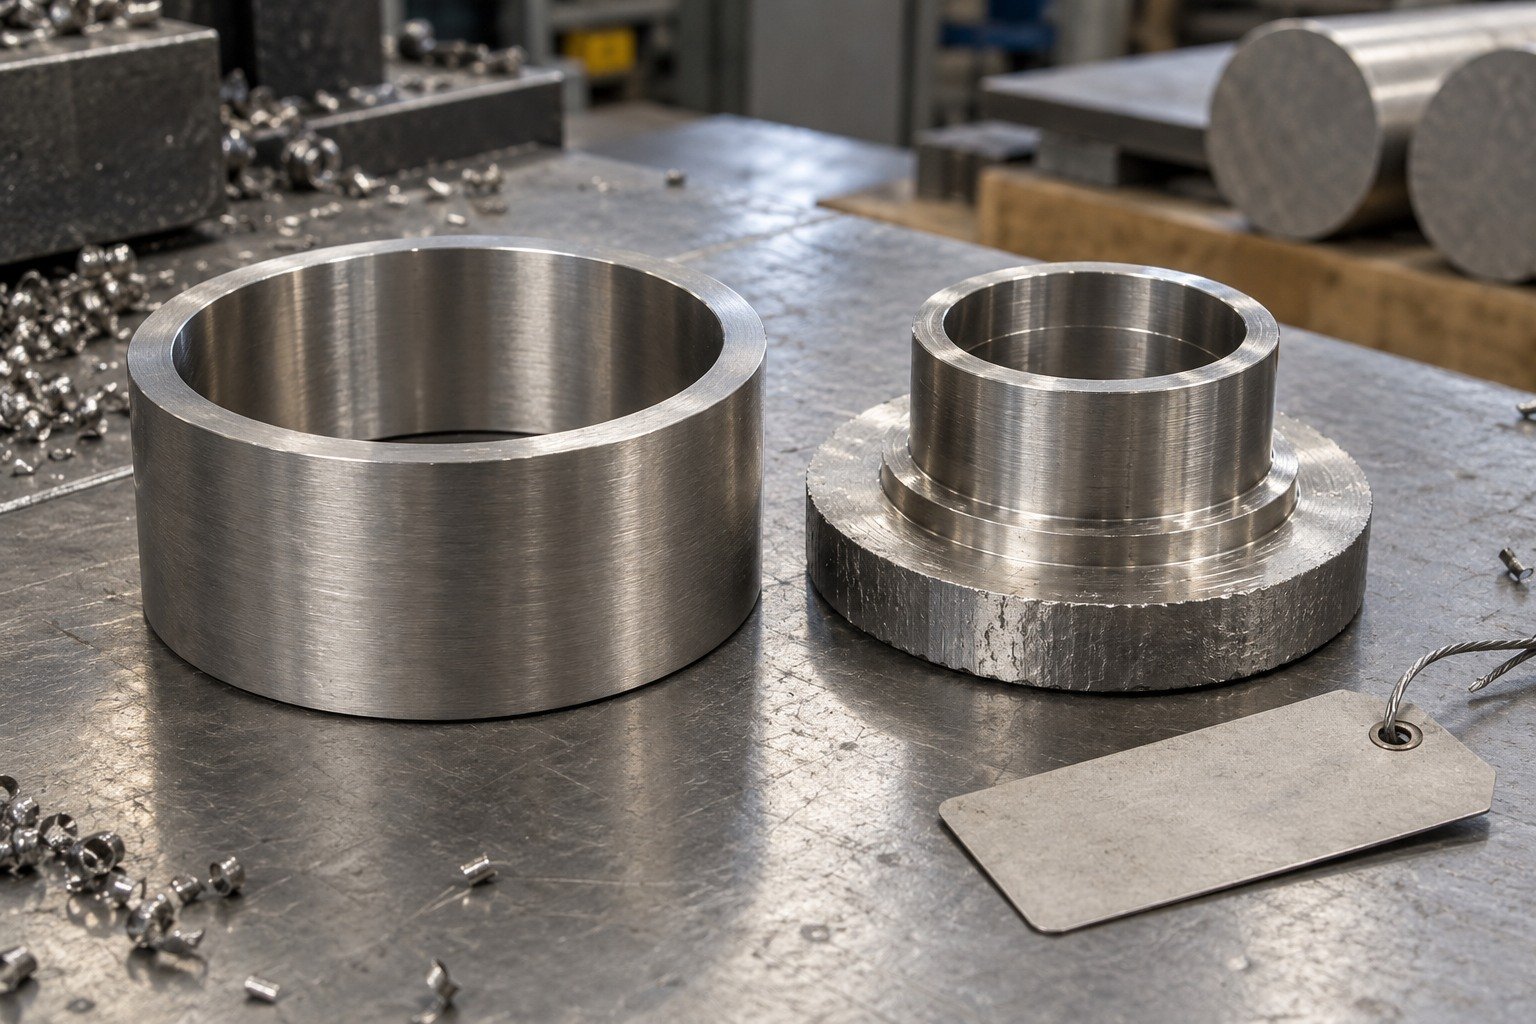
Retain CP Grade 4 identity through blank preparation. Confirm the starting bar or ring form and final operation responsibility before approving stock changes.
| Your decision | What to define |
|---|---|
| Your fit | Locating bore, seating face, contact area and any split detail. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
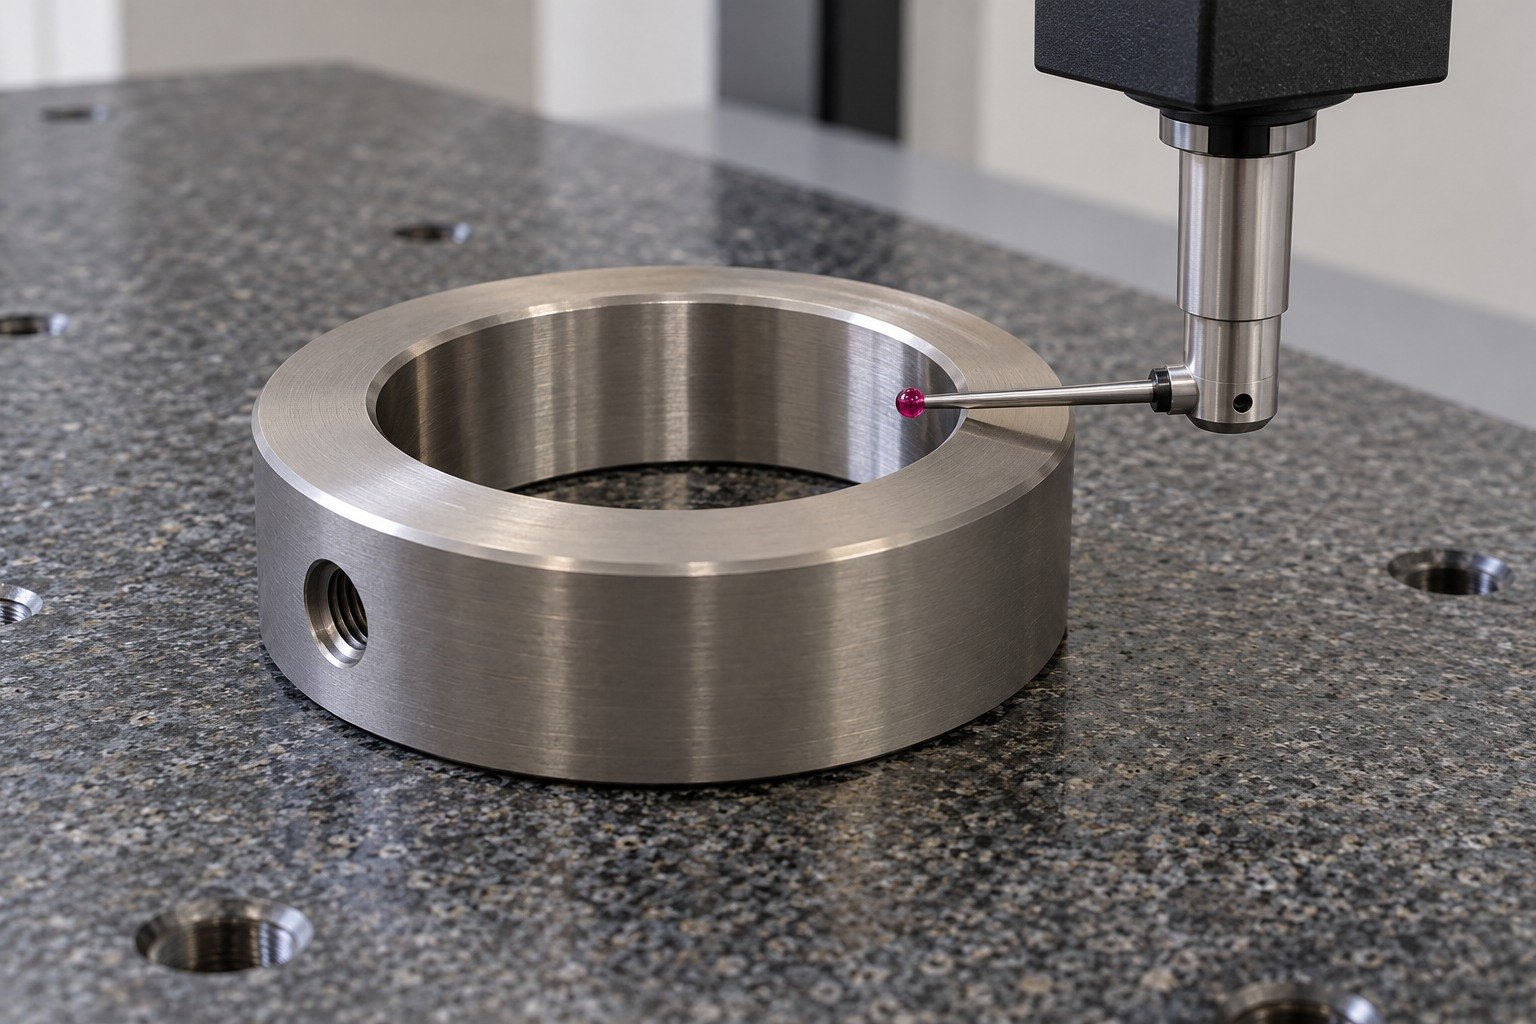
Inspect the bore from the agreed datums and protect locating surfaces during handling. Keep dimensional evidence and material records linked to the same controlled revision.
| Your decision | What to define |
|---|---|
| Your fit | Locating bore, seating face, contact area and any split detail. |
| Your process | Supplied condition, machining sequence and final finishing. |
| Your approval | Controlled geometry, working condition and receiving evidence. |
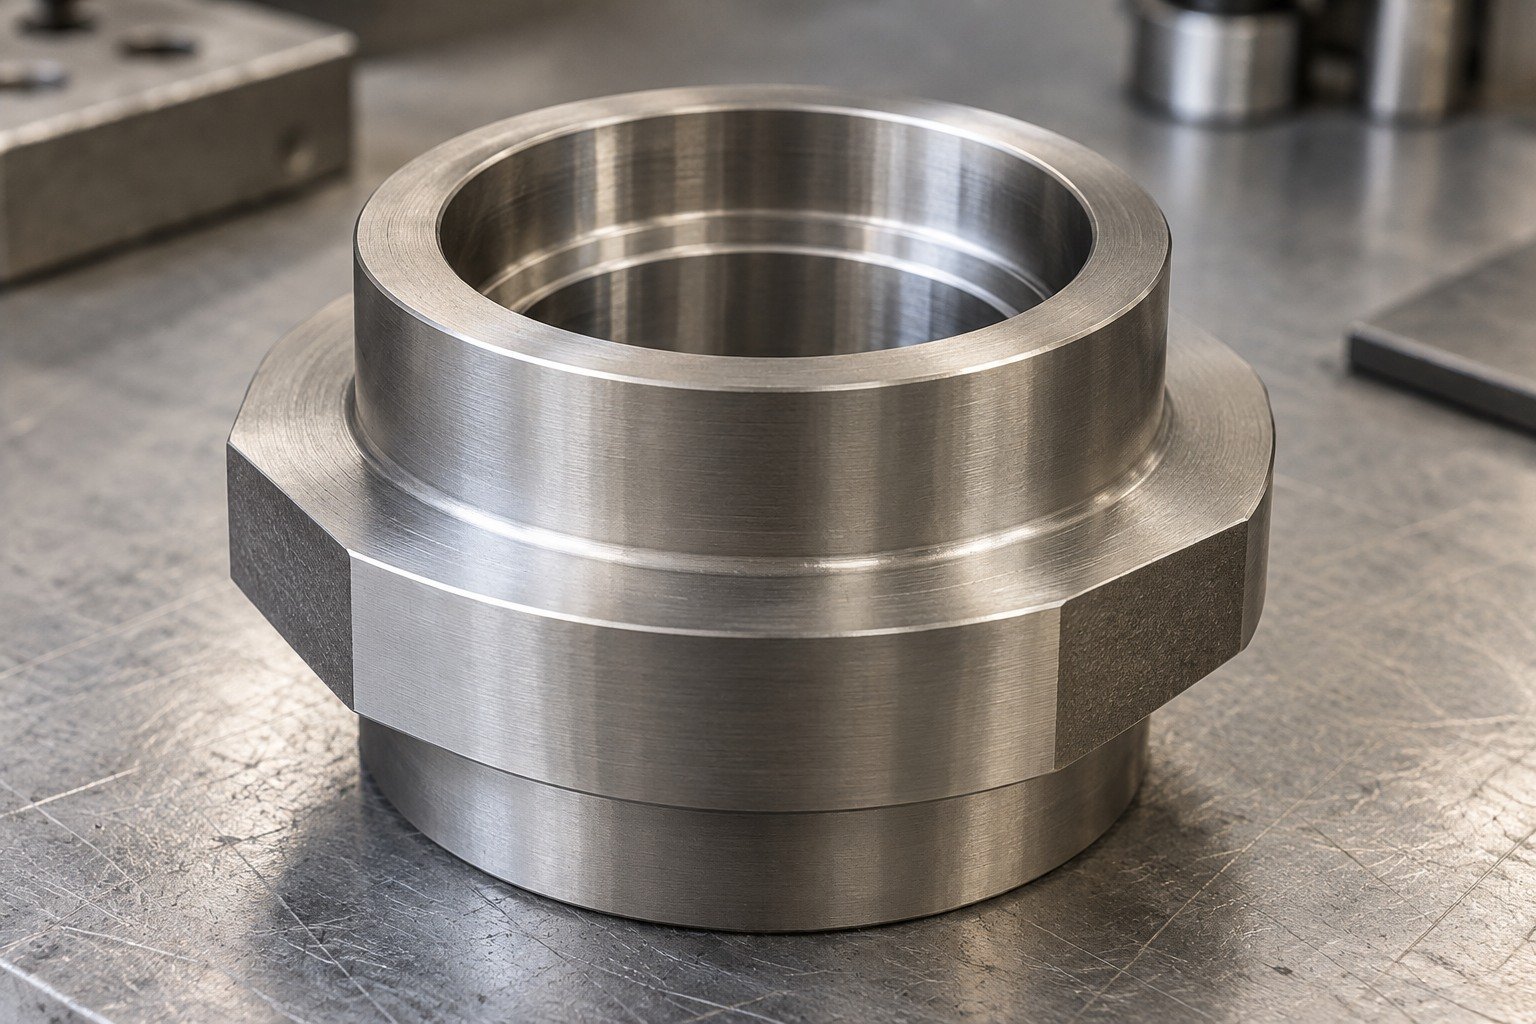
Connect working profile, supplied state and final fit before approving the first route.
Specify UNS R50700, product standard, form, supplied condition and lot identity. State your Grade 4 titanium material certificate requirement at inquiry, including document type and required chemistry or condition evidence.
Identify the mating geometry and supported datum.
Connect stock, clamping access and final surface.
Agree feature results, condition and lot evidence.

For intersecting bores and threads, define tool access, chip escape and burr-sensitive edges. Connect the mating specification and gauge method to the final assembled requirement.
Identify the mating geometry and supported datum.
Connect stock, clamping access and final surface.
Agree feature results, condition and lot evidence.
State the accepted unsupported geometry. Connect broad mounting pads and short locating shoulders to secure support. Agree when finishing stock is removed and how the released part is held for its final measurement.
Identify the mating geometry and supported datum.
Connect stock, clamping access and final surface.
Agree feature results, condition and lot evidence.
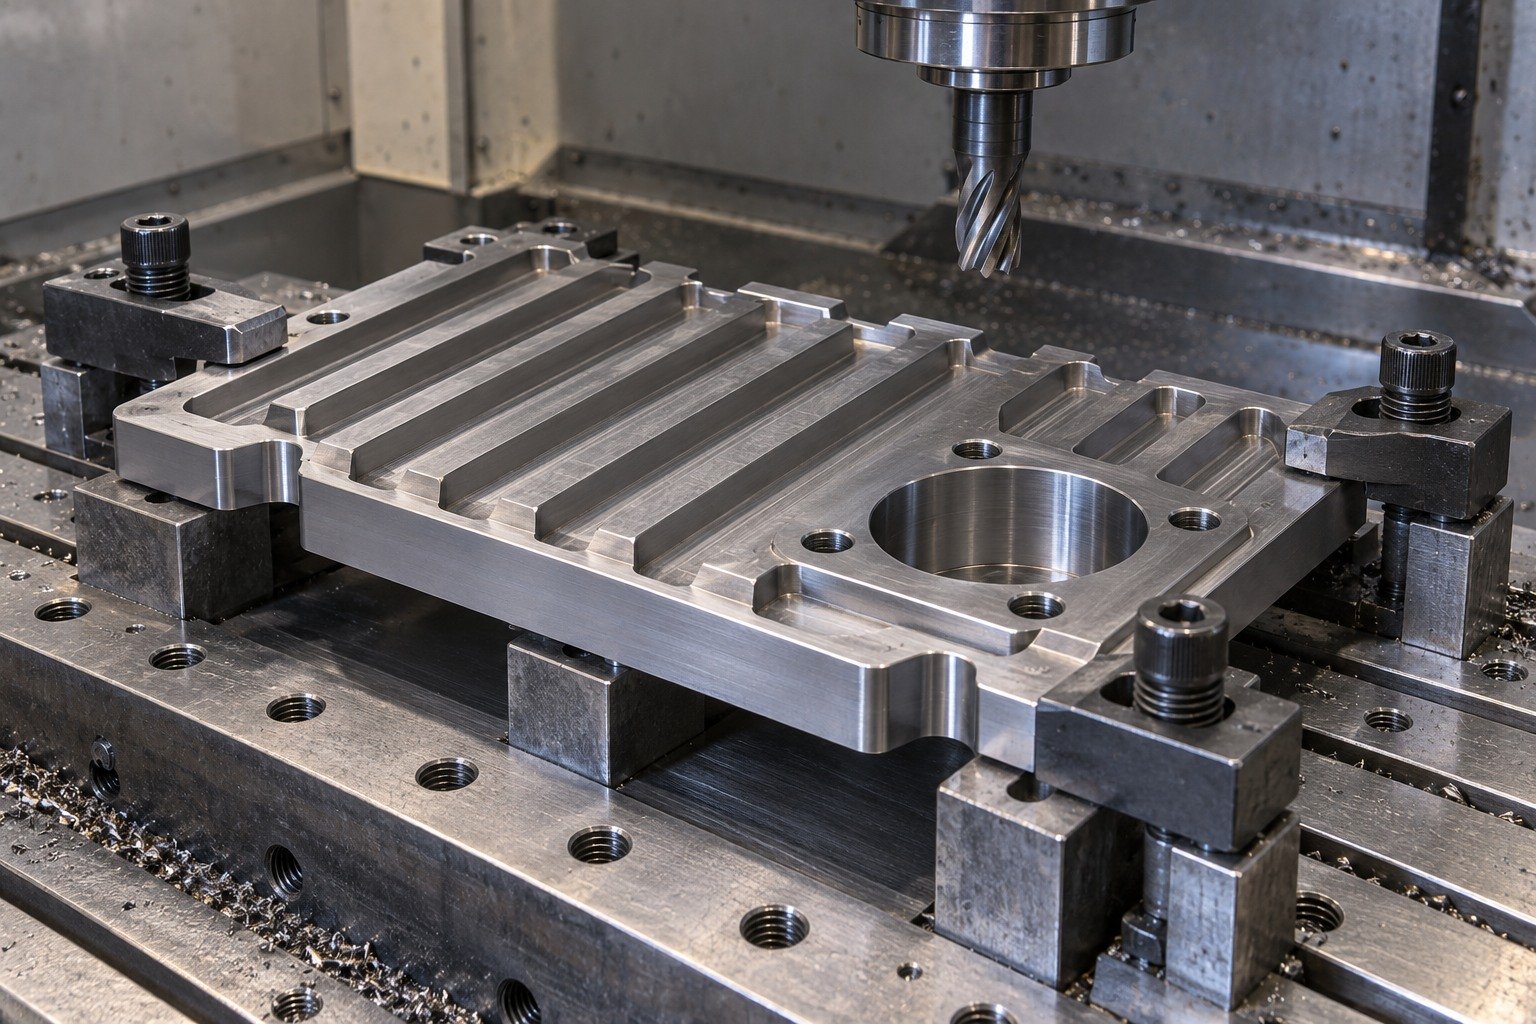
Address Grade 4 titanium machining surface finish problems through defined roughness, visual criteria, tool access and edge acceptance. A roughness number alone does not define the appearance your buyer expects.
Identify the mating geometry and supported datum.
Connect stock, clamping access and final surface.
Agree feature results, condition and lot evidence.
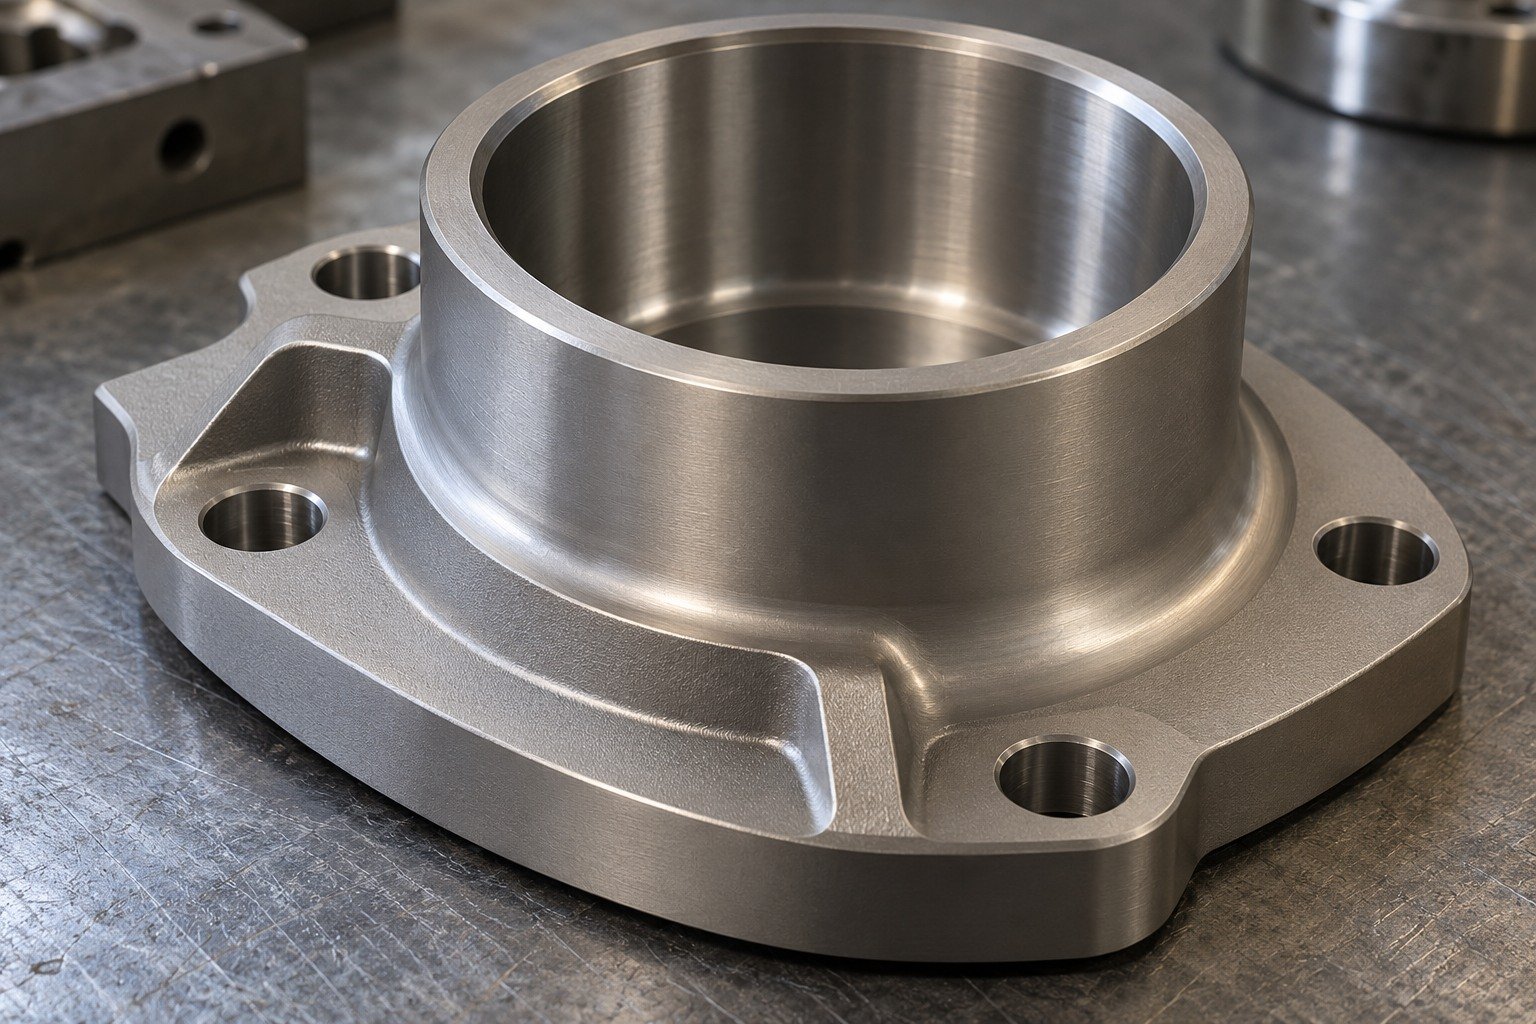
For your Grade 4 titanium galling review, identify the mating material, contact load, relative movement and lubrication or surface requirements. A grade name does not establish wear performance.
Identify the mating geometry and supported datum.
Connect stock, clamping access and final surface.
Agree feature results, condition and lot evidence.
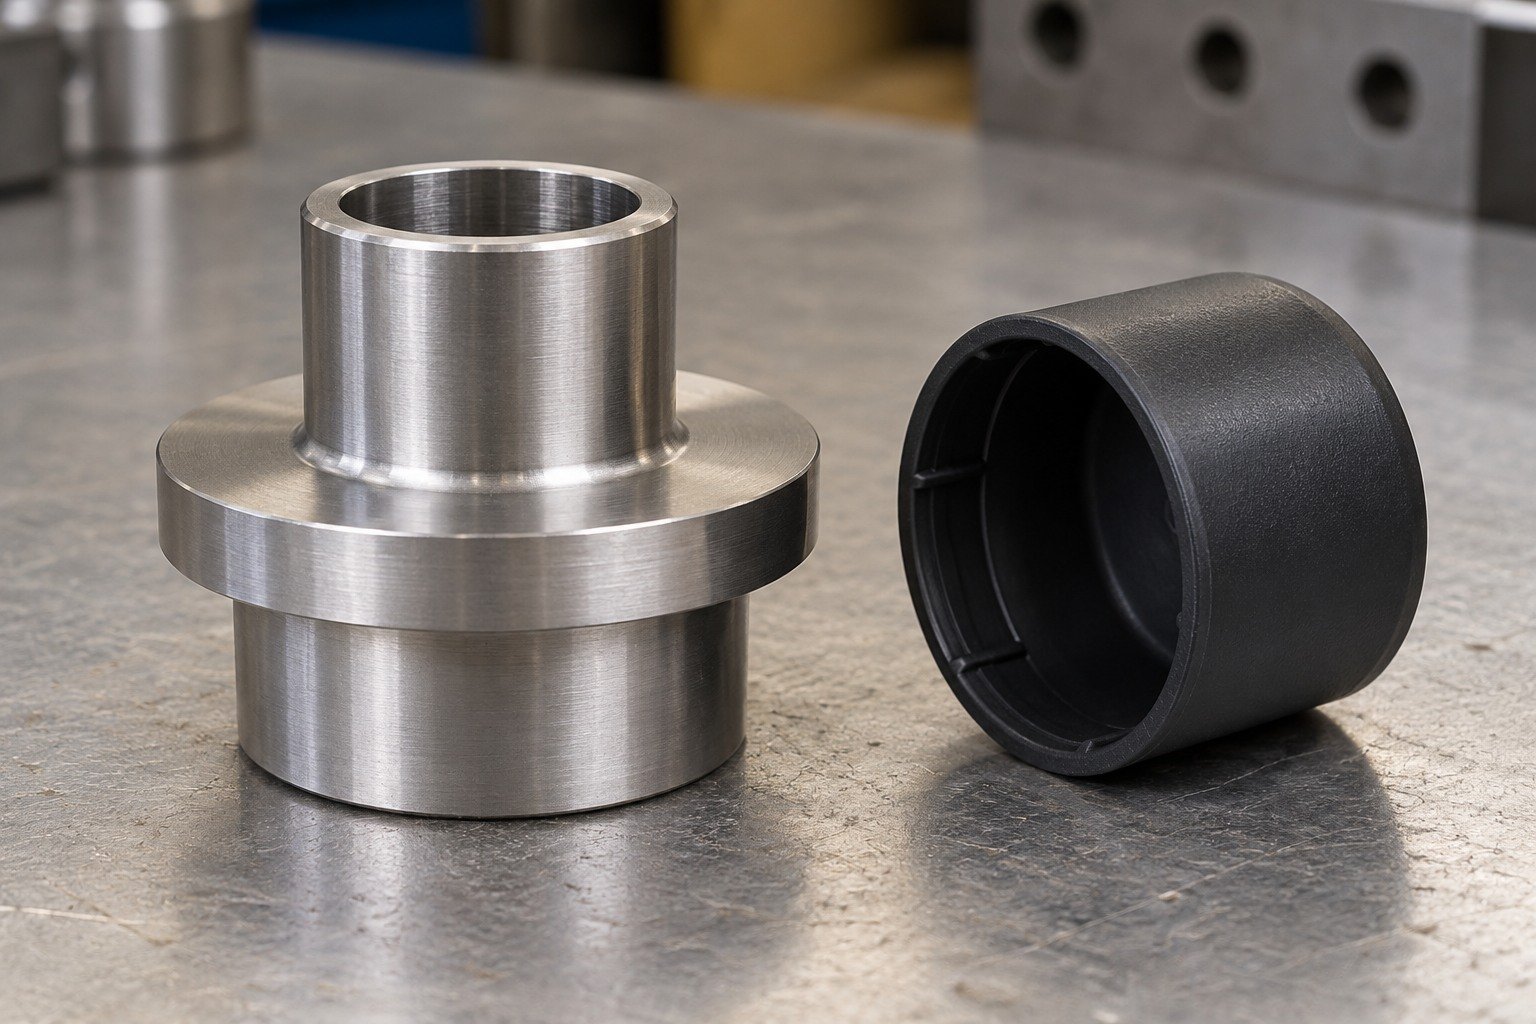
Define controlled dimensions, profile, surfaces and cleaning after the complete agreed route. Grade 4 titanium machining tolerances are reviewed feature by feature; no single tolerance applies to every part.
Identify the mating geometry and supported datum.
Connect stock, clamping access and final surface.
Agree feature results, condition and lot evidence.
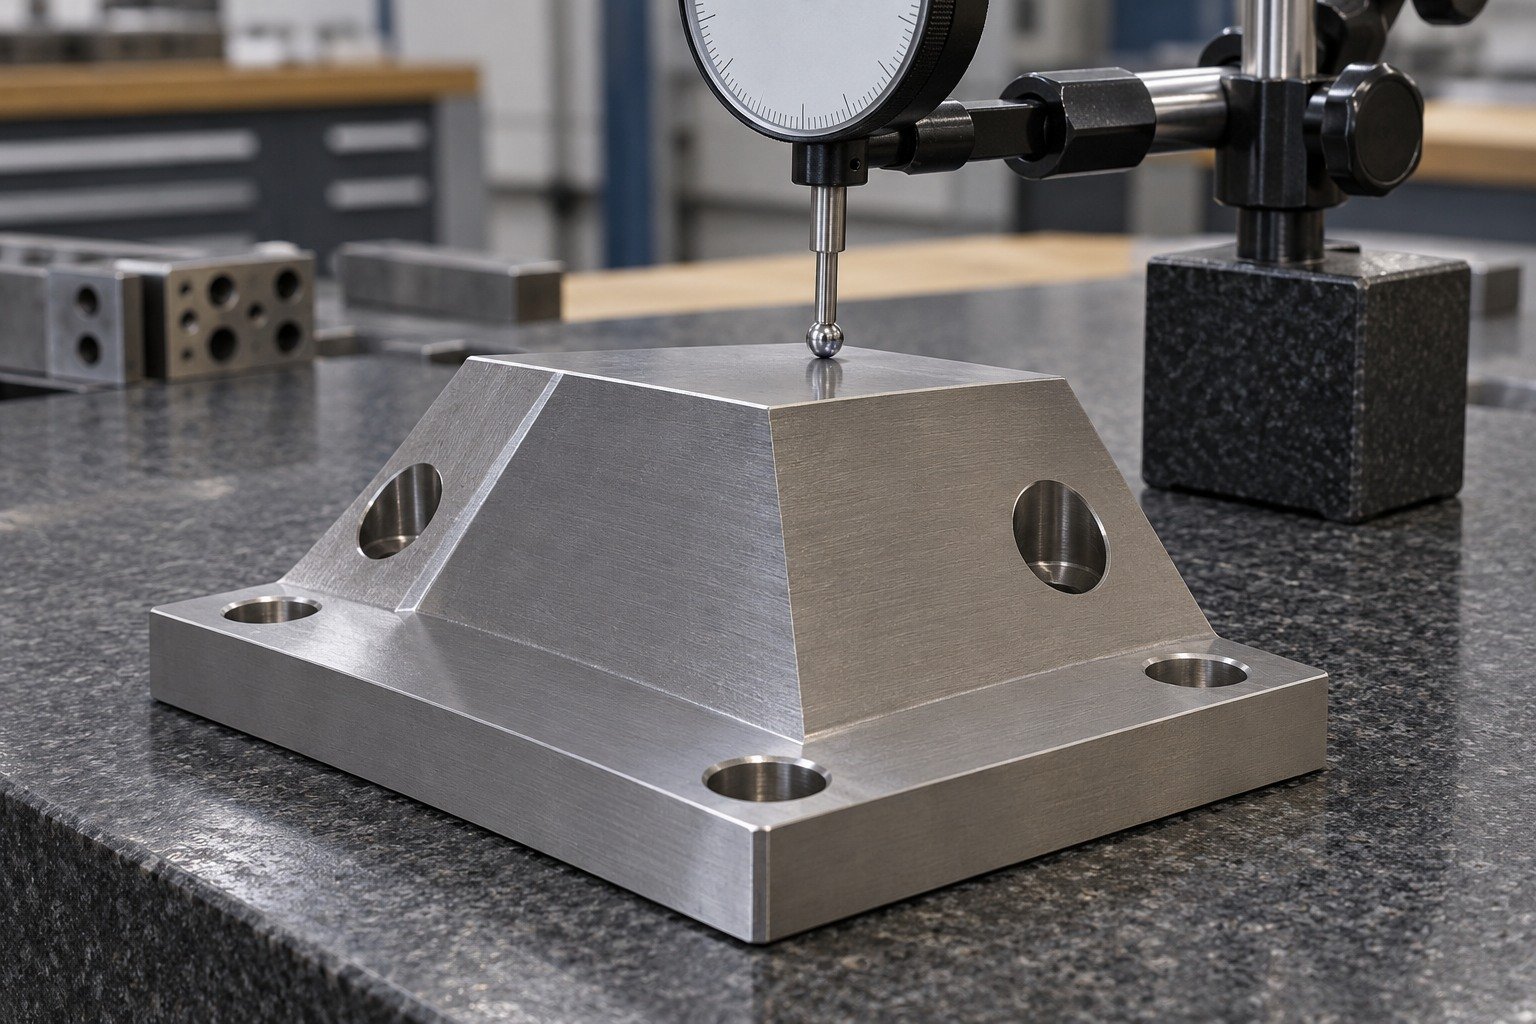
Identity, stock form and supplied state.
Condition, support and final mating features.
Functional geometry, protection and records.
Confirm grade, form, condition and heat or lot identity before cutting. Review the requested certificate against the actual purchase specification.
Sampling and document scope are agreed with your quotation.
Quality Assurance →
Review the first housing or shaft sample against the mating features and drawing datums. Resolve workholding effects, controlled surface criteria and measurement support before repeat quantities.
Sampling and document scope are agreed with your quotation.
Quality Assurance →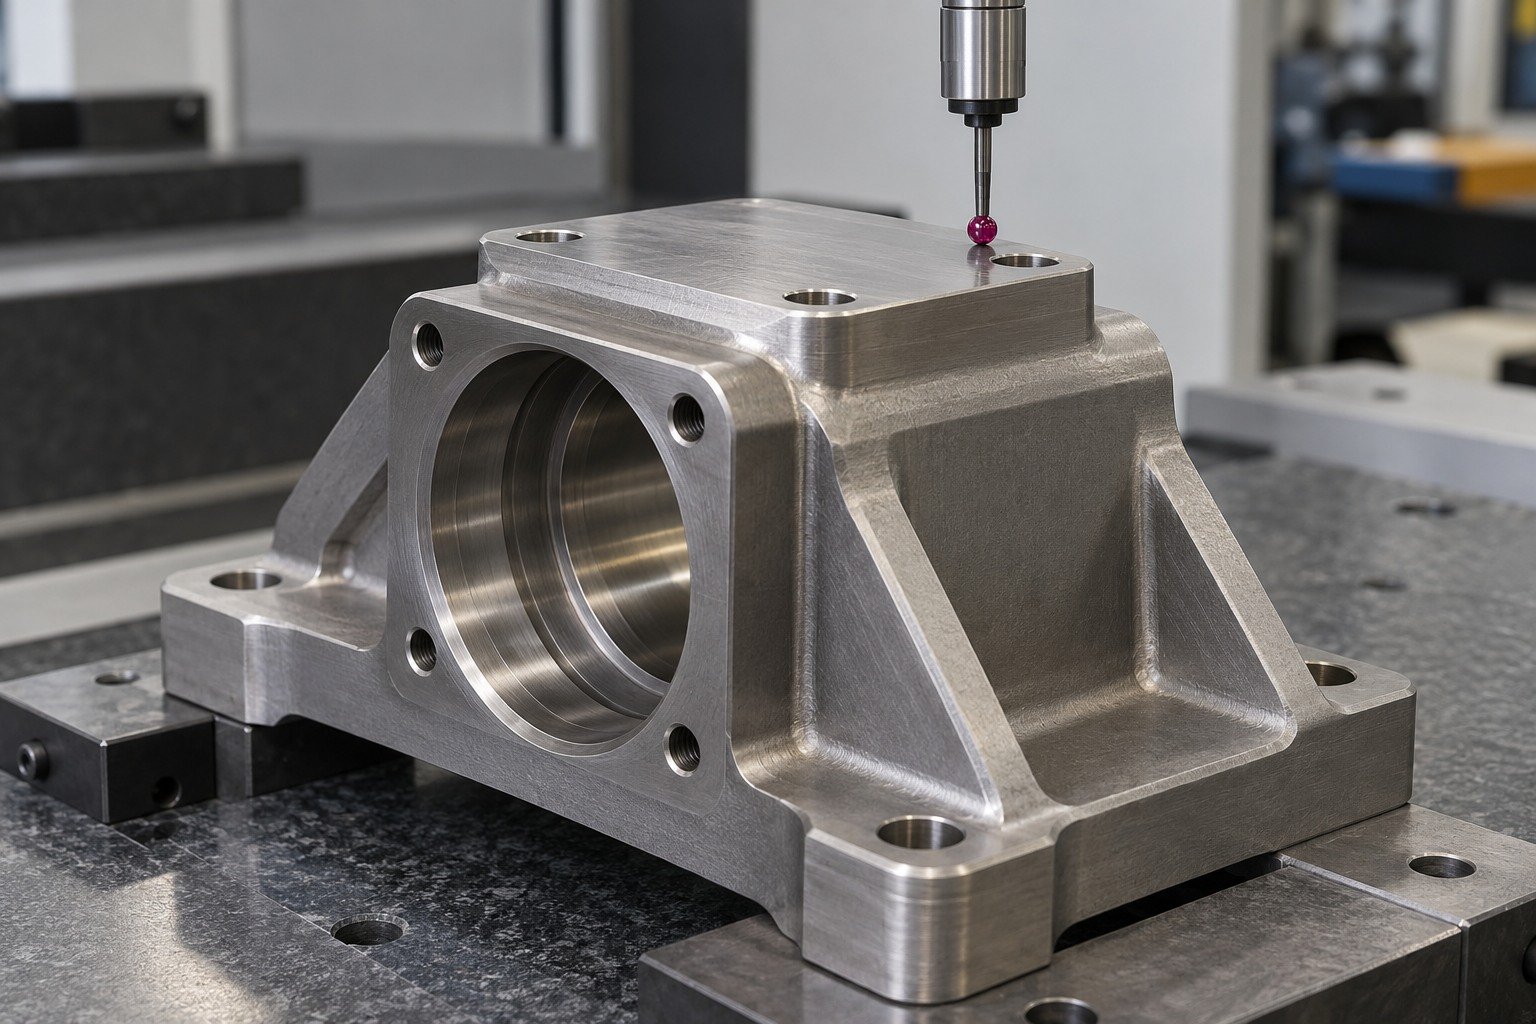
Verify bores, flange position, controlled surfaces and agreed edges. State which dimensions require records and how the finished part is supported during inspection.
Sampling and document scope are agreed with your quotation.
Quality Assurance →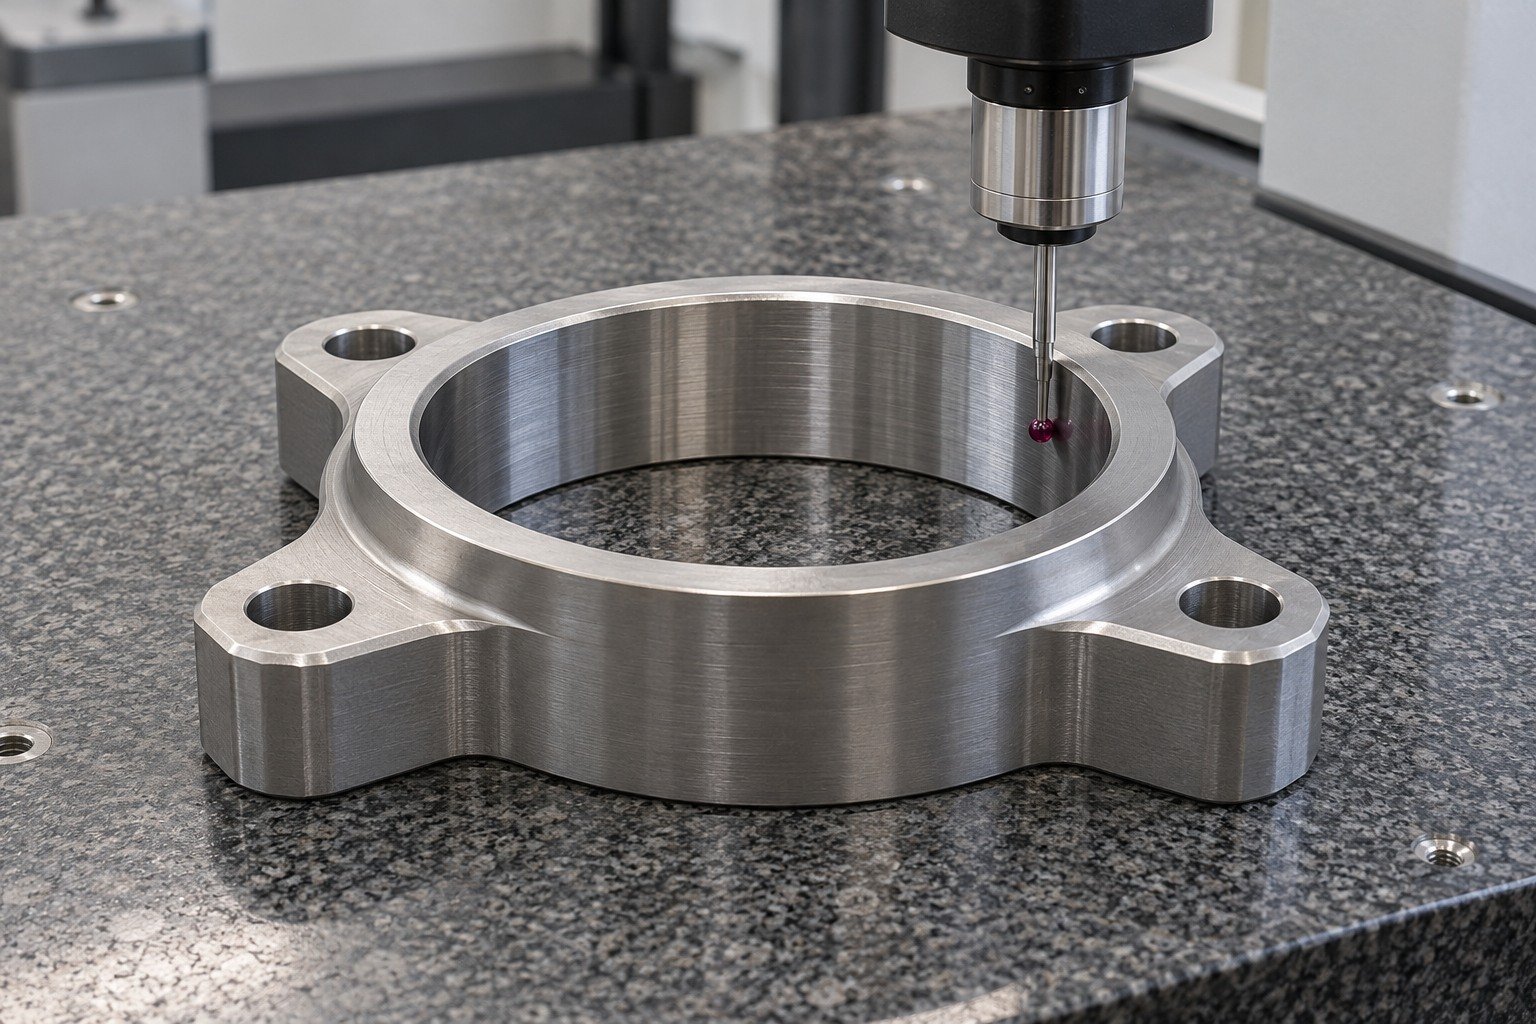
Agree separate pockets and protection for bores, shoulder faces and mounting pads. Link each delivered lot to the requested material and dimensional records.
Sampling and document scope are agreed with your quotation.
Quality Assurance →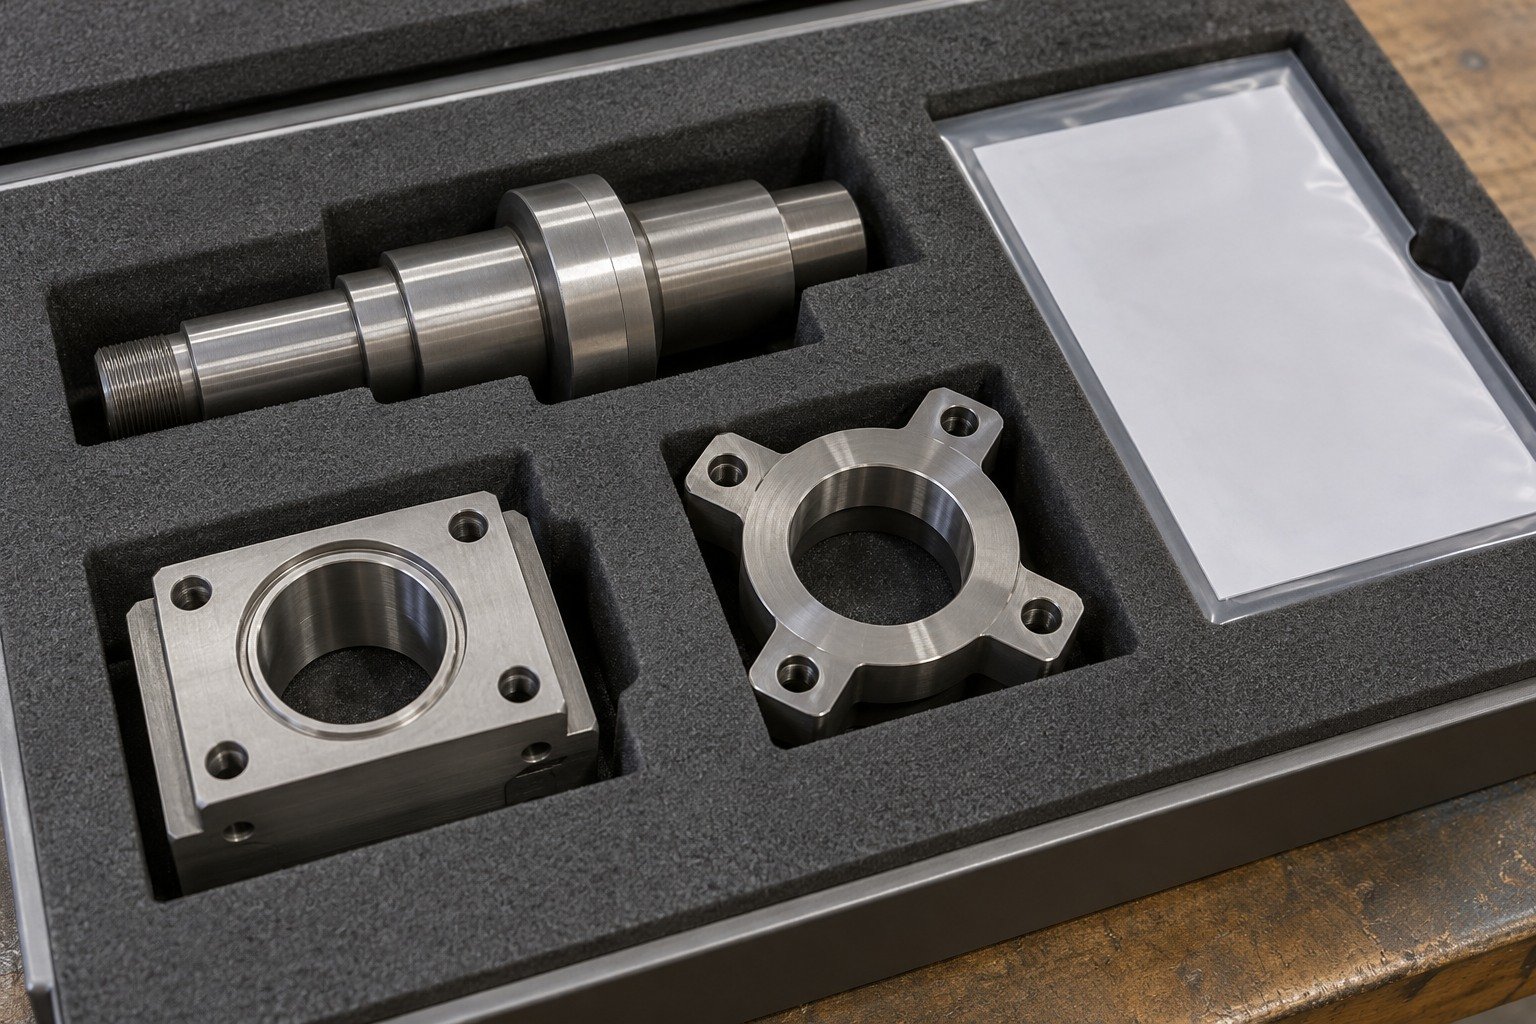
For Grade 4 titanium prototype machining, use the first controlled sample to review datum recovery, supported machining and assembly fits before repeating your drawing. Quantities, timing and scope are confirmed with your quote.

Grade 4 titanium turning: review short stepped shafts, collars and locating shoulders.
Explore CNC Turning →
Grade 4 titanium milling: connect housing pockets, mounting pads and supported plate features.
Explore CNC Milling →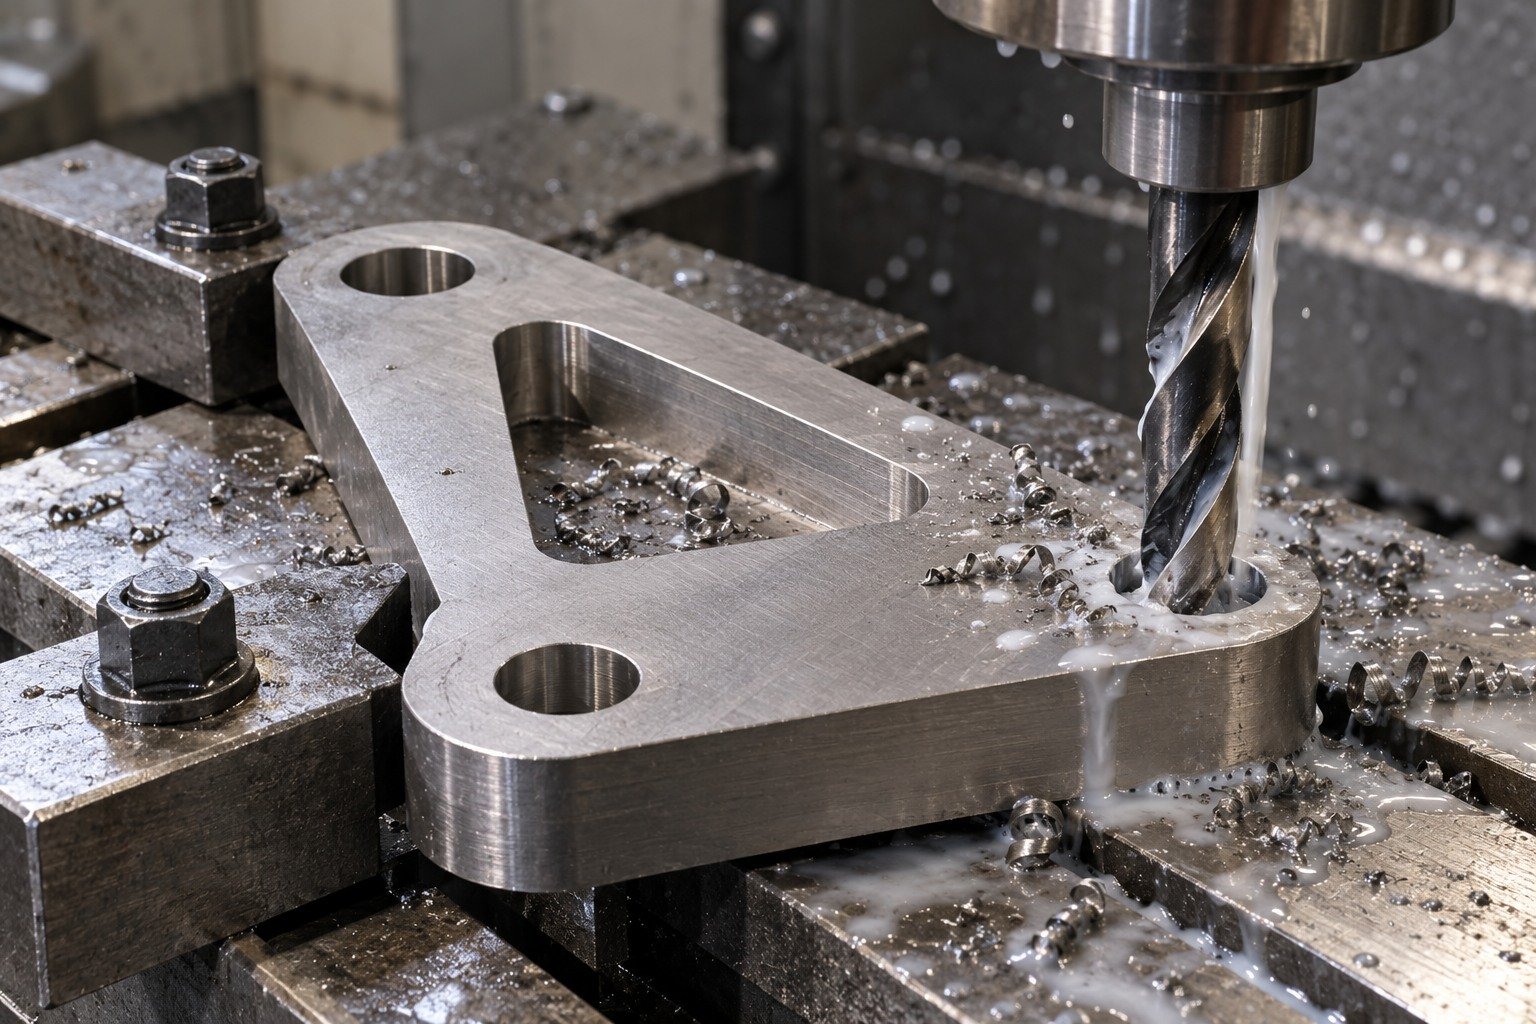
Define hole access, intersections, thread engagement and gauge requirements.
Explore Drilling & Thread Review →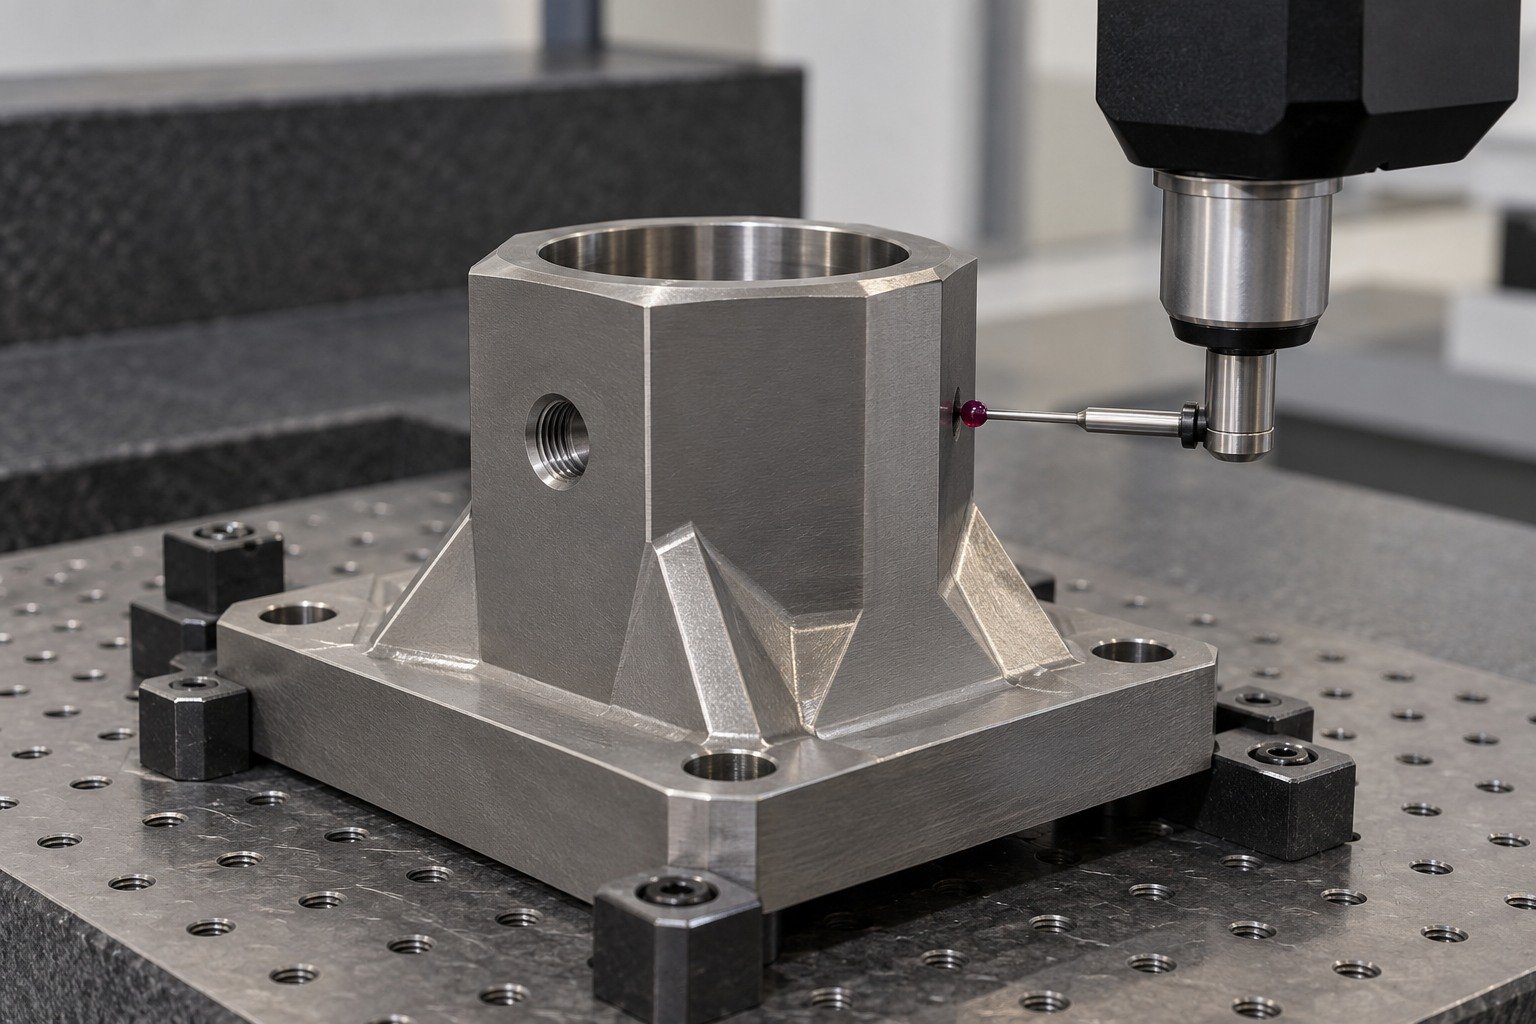
Verify working bores, axial shoulders and mounting datums against the controlled drawing.
Explore Final Interface Inspection →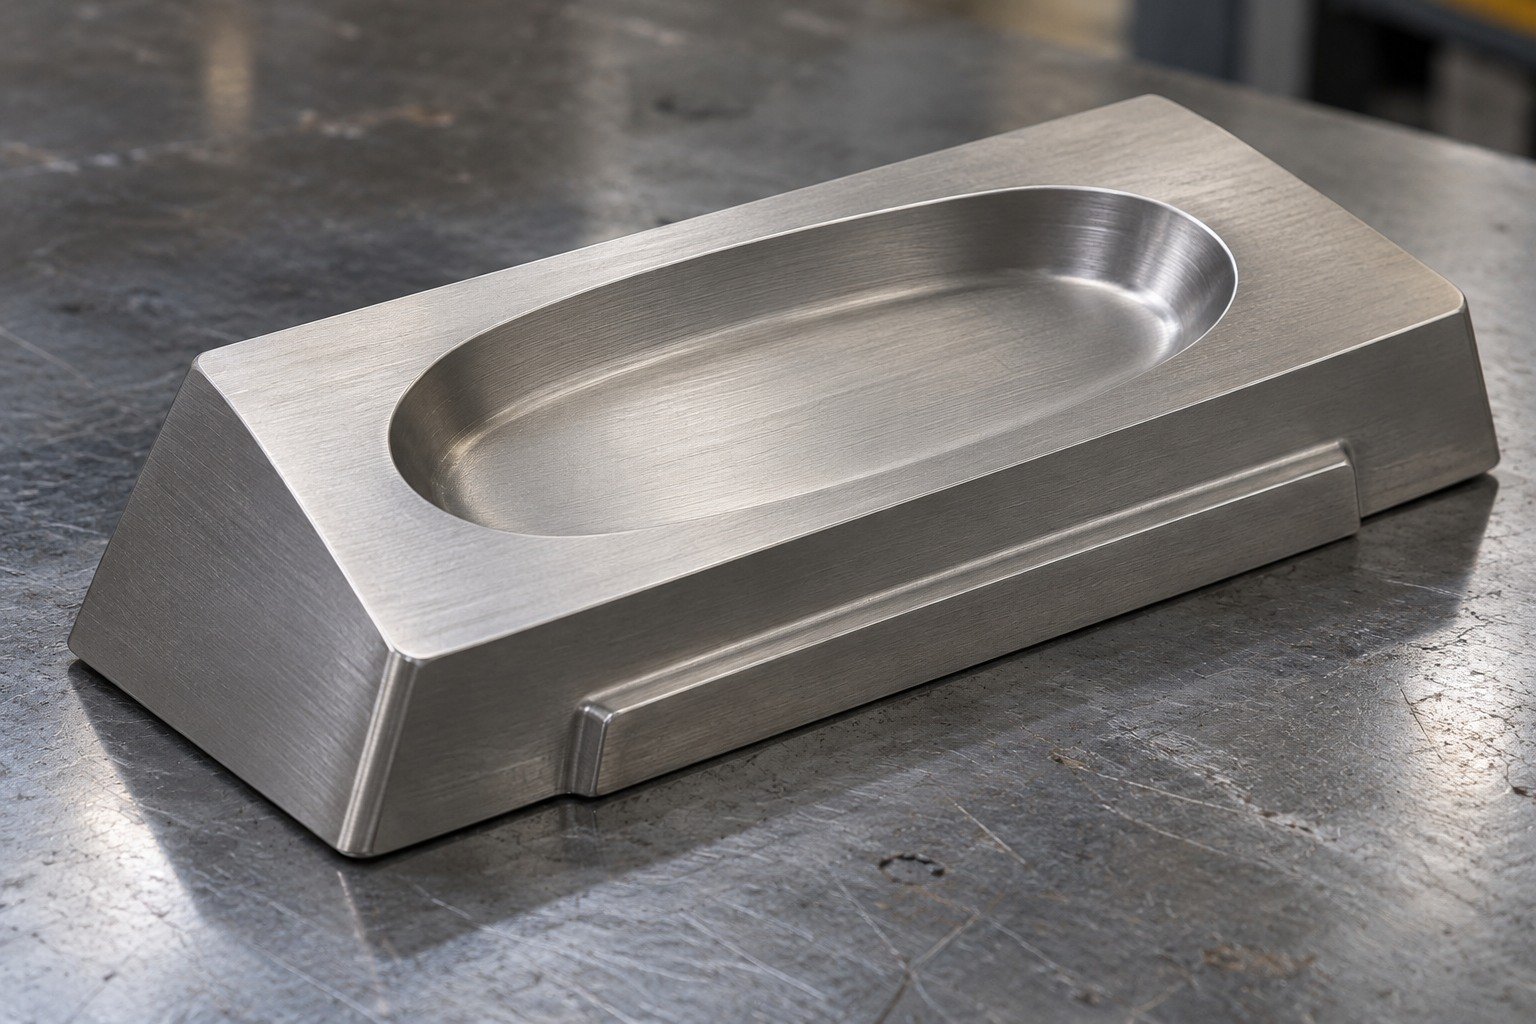
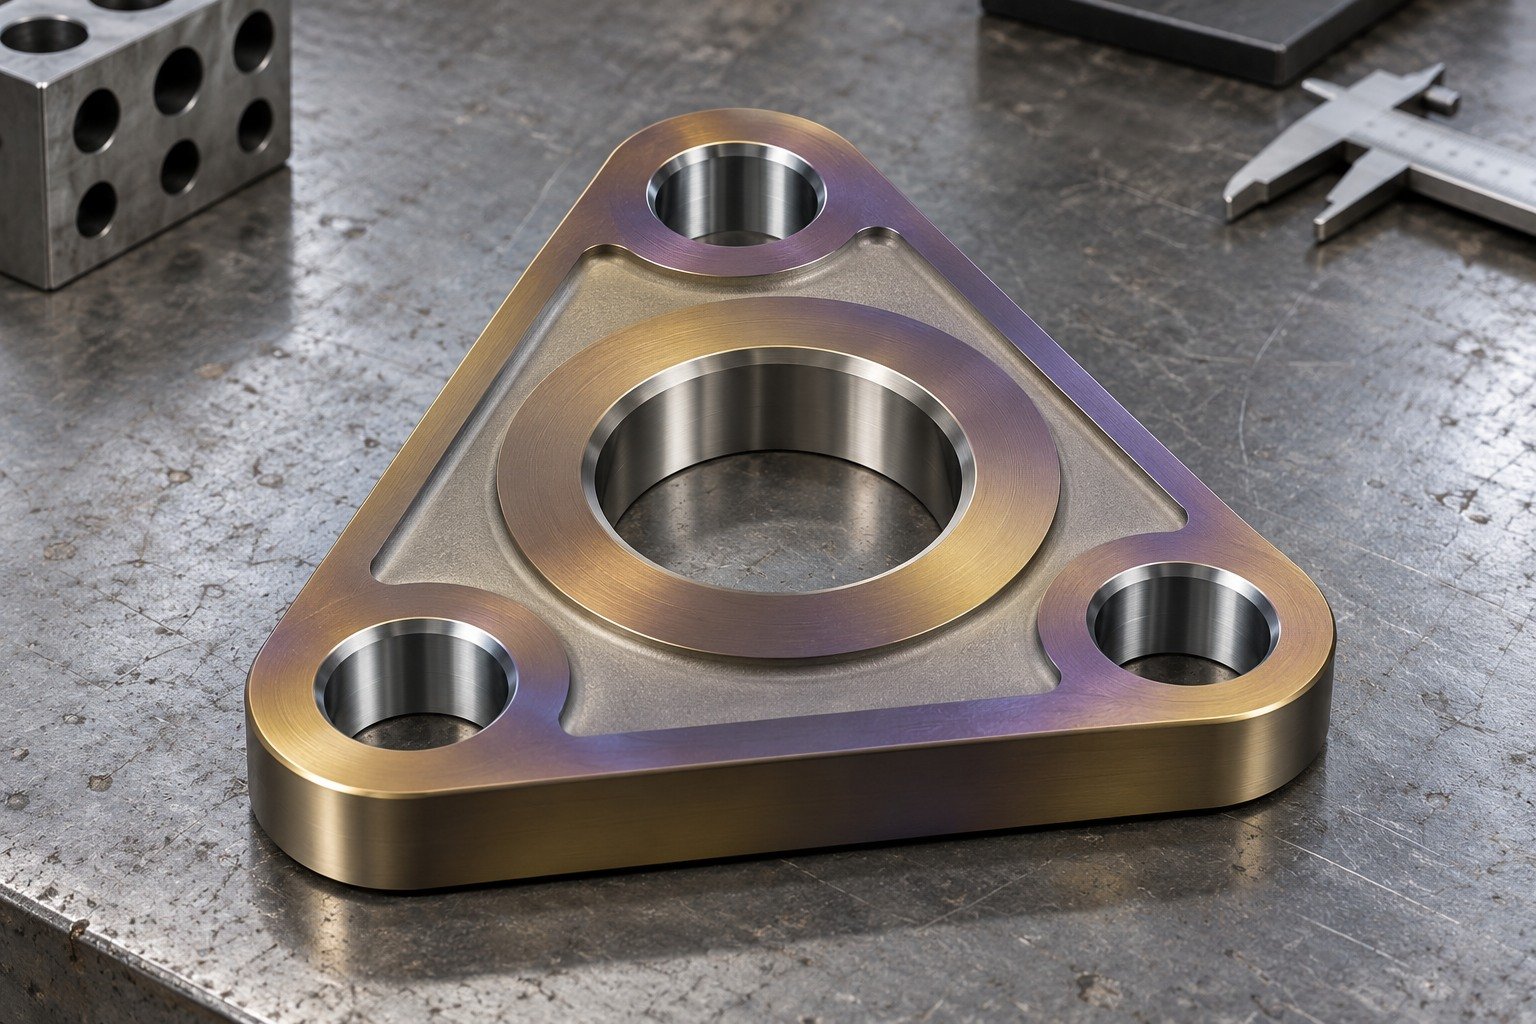
Illustrative appearances only. Agree finish suitability, cleaning, masking and final dimensions for your grade and service conditions. Colour does not prove alloy identity, coating thickness or corrosion life.
Surface Finishing →| Your decision | What to confirm |
|---|---|
| Material identity | Separate grades and the applicable product specification. |
| Forming and geometry | Geometry, available support and actual cutting engagement. |
| Strength and loading | Product-form data and your actual design loads. |
| Service exposure | Medium, concentration, temperature and contact conditions. |
For Grade 4 vs Grade 2 titanium, compare the actual product specification, loading, formability and service exposure. A stronger plate reference does not establish a better material for every part.
Compare the Titanium Family →
Connect China manufacturing with Dallas-area coordination for your drawing review, sample decisions and delivery requirements.
Yes. Commercially pure titanium Grade 4 / UNS R50700 is unalloyed titanium with controlled residual and interstitial limits. CP titanium Grade 4 does not mean unspecified 100% purity. Order the exact product form, condition and applicable specification.
Review short shafts, flanged housings, mounting plates and locating collars against your drawing, load and service exposure. A material designation or illustrative photograph does not certify an application or confirm project acceptance.
Grade 4 titanium corrosion resistance must be reviewed for the actual medium, concentration, temperature, crevices and dissimilar-metal contacts. No general corrosion-life or immunity guarantee follows from the grade name.
For your Grade 4 titanium welding inquiry, define the joint, applicable procedure, cleanliness, shielding and inspection requirements. ATI describes CP titanium welding with appropriate contamination control; responsibility and availability need project review.
Review tool condition, secure support, cutting engagement, cutting-fluid delivery and chip removal for the actual feature. Discuss Grade 4 titanium galling separately for sliding and threaded contacts, including mating material and surface requirements.
Grade 4 titanium machining cost depends on usable stock, quantities, setups, access, surface acceptance and inspection scope. For your Grade 4 titanium machining quote, compare the same revision and final condition rather than a generic per-kilogram machining price.
No. The chart reports selected ATI plate tensile and yield minima. Grade 4 titanium fatigue strength requires relevant design data, loading, geometry, surface condition and agreed evidence. No finished-part fatigue life is promised from the plate bars.
For commercially pure titanium Grade 4 machining services, ask how the supplier connects your material specification, supported datums, first sample and receiving evidence. Agree Grade 4 titanium machining tolerances and surface criteria feature by feature; a generic certificate or tolerance claim does not quote your drawing.





