

Injection Molding
Tooling and molding for your repeat plastic parts.
From prototype to production, coordinated manufacturing solutions for your custom parts.
View All Services →
Precision parts for your tight tolerances and complex geometry.
Tooling and molding for your repeat plastic parts.

Metal casting options for your part and production volume.

Cutting, forming and welding for your fabricated parts.

Custom profiles for your section, length and finish requirements.

Finishes for your appearance, corrosion and wear requirements.

Sub-assemblies and final builds for your production program.

Production tooling built around your process and volume.

Prototype parts to check fit, function and design.
DFM, process planning and production support for your project.
Inspection, documentation, inventory and delivery planning for your program.
Choose air- or liquid-cooling components around your thermal and mechanical requirements.

Manufacturing support for your cold plates, manifolds and cooling assemblies.

Find components for your power electronics, energy, laser and telecom application.

Components for your electronic systems.
Start with your functional and quality requirements.
Build around your operating environment.
From prototype to production, review material performance, manufacturability and cost for your part.
Review grade, temper and finish for your metal parts.
 AluminumStrength, weight and machining›
 Stainless SteelCorrosion and finish requirements›
 Carbon & Alloy SteelDiscuss grade and heat treatment›
 Tool SteelDiscuss tooling and wear needs›
 TitaniumReview grade and part geometry›
 Copper & BrassDiscuss conductivity and machining›
Match your polymer to function, process and environment.
 ABSReview enclosure and molding needs›
 Polycarbonate (PC)Discuss clarity and impact needs›
 Nylon (PA)Review moisture and wear conditions›
 POM / AcetalReview fit and sliding features›
 PEEKDiscuss operating conditions›
 PTFEReview friction and chemical exposure›
 ULTEM / PEIDiscuss thermal and electrical needs›
Confirm grade availability and application requirements.
 Silicone / LSRDiscuss flexible component needs›
 TPU / TPEReview flexibility and processing›
 EPDMReview weathering and chemical exposure.›
 NBRReview oil and fuel exposure.›
 FKMReview temperature and chemical exposure.›
 G10 / FR4Review insulation and laminate needs›
 CompositesReview stiffness, weight and laminate.›Customer-Specified MaterialsConfirm your grade and requirements.›Other Specialty MaterialsDiscuss your application and grade.›
Practical guidance for your part geometry and material decisions.
Prepare your process, budget and sourcing questions.
Build your knowledge before production.
Learn who we are and how we operate.
Find our U.S. support team or start a conversation.
420 · UNS S42000 · confirm your EN variant
Start with the carbon variant, final hardness and mating feature.
For your 420 stainless steel machining project, define the material condition and inspection state that your component needs.

Stainless steel 420 is a hardenable martensitic family. Do not release an order from the abbreviated name alone. European references include EN 1.4021, 1.4028, 1.4031 and 1.4034 with different supplier typical chemistry.
Retain the full grade, product standard and carbon requirement.
Identify supplied condition, required final condition and the processing sequence.
Show the mating surfaces, wear-related requirement and inspection evidence.
UNS S42000 helps you locate the family; it does not approve every European variant as interchangeable.
Outokumpu Dura reference · mass % · axis 0–0.50%
| Dura reference | EN | Typical C % | Typical Cr % |
|---|---|---|---|
| 420/4021 | 1.4021 | 0.20 | 13.0 |
| 420/4028 | 1.4028 | 0.30 | 12.5 |
| 420/4031 | 1.4031 | 0.38 | 13.5 |
| 420/4034 | 1.4034 | 0.45 | 13.7 |
Compare the same supplier reference and product scope. Different carbon values are a reason to check the drawing, not permission to substitute.
| Selected Carpenter type analysis | Mass % |
|---|---|
| Carbon | ≥0.15 |
| Chromium | 12.00–14.00 |
| Manganese / Silicon | ≤1.00 each |
| Phosphorus / Sulfur | ≤0.040 / ≤0.030 |
| Iron | Balance |
This separate 420 supplier analysis is not the same dataset as the Dura typical-chemistry chart. Your controlled specification and actual lot record govern acceptance.
For 420 stainless steel ASTM A276, confirm the applicable bar/shape scope, revision, exact grade and condition.
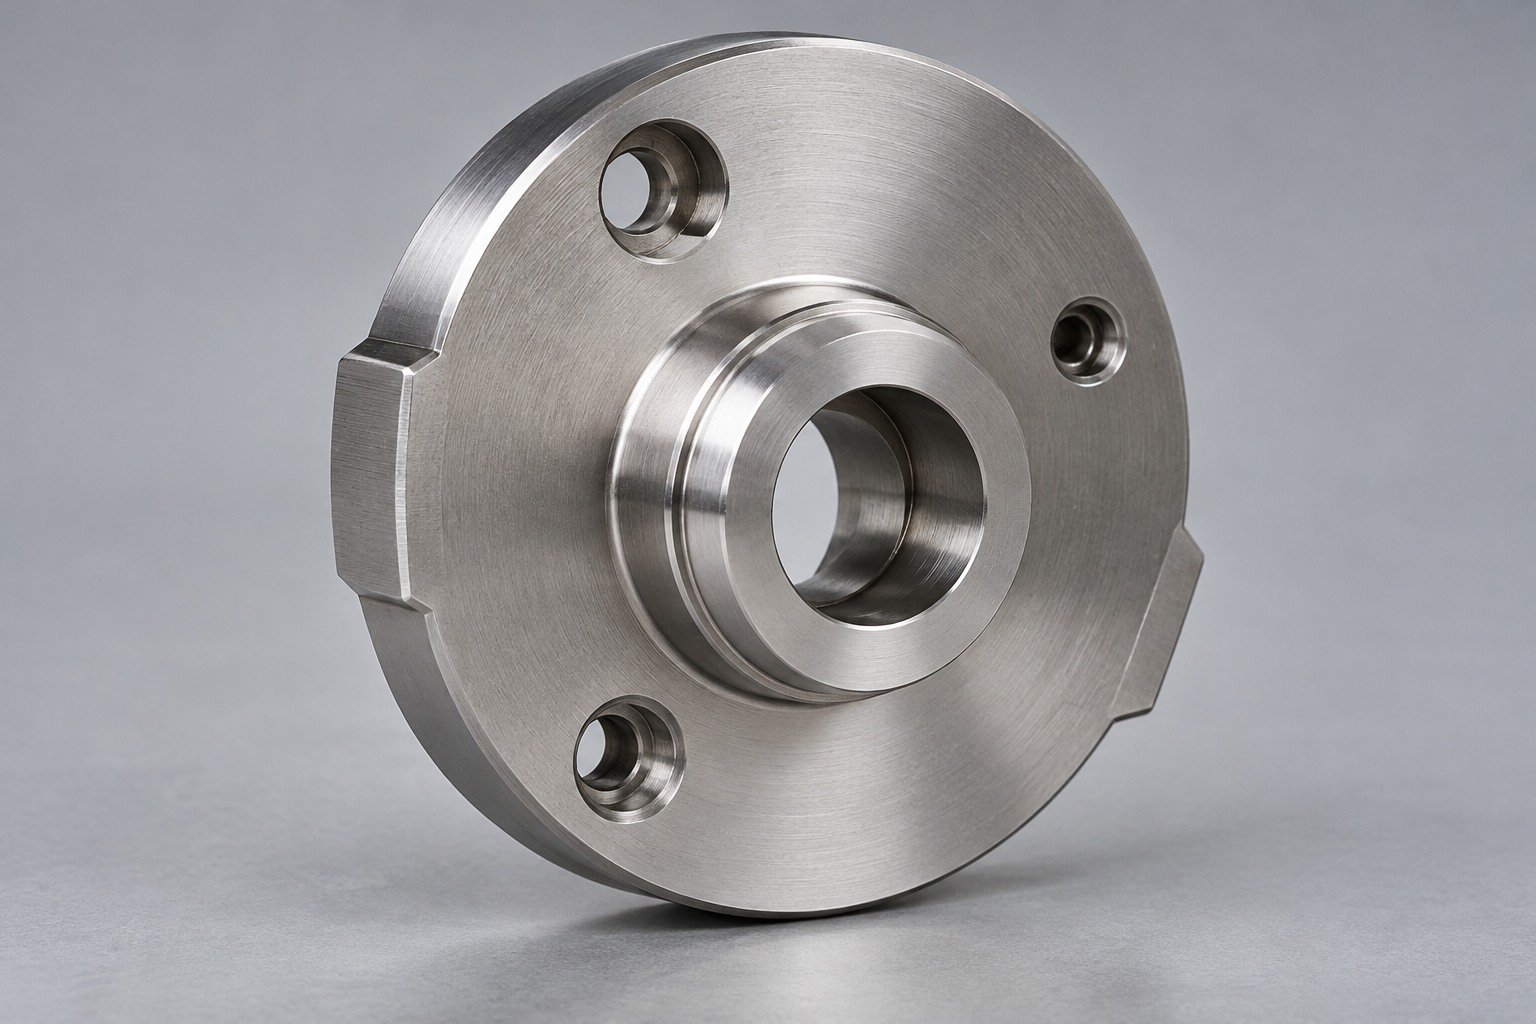
For 420 stainless steel heat treatment, specify the final condition and required evidence. Read 420 stainless steel properties with the variant, stock form and treatment state.
Confirm incoming stock, material identity and any processing allowance.
Agree the governing treatment route and surfaces that must remain recoverable.
Inspect the functional fit, final surface and required material evidence.
Discuss 420 stainless steel grinding when the finished feature requires a reviewed grinding route. A material name alone does not define one final hardness.
For 420 stainless steel turning services, show the datum scheme and the relationships that must hold after all processing.
420 stainless steel turning for 420 stainless steel shafts, 420 stainless steel bushings and 420 stainless steel spacers needs explicit fits, shoulder lengths and surface acceptance.
For 420 stainless steel machined parts, identify any finishing operations after hardening.
CNC Turning →
For 420 stainless steel CNC machining, provide the current condition and intended final state before the route is fixed.
For 420 stainless steel milling, show pocket depth, wall transitions and fixture access. Relate 420 stainless steel drilling and 420 stainless steel tapping to burr control and useful feature depth.
420 stainless steel machinability depends on the variant, condition and actual cut; compare proposed routes against your geometry.
CNC Milling →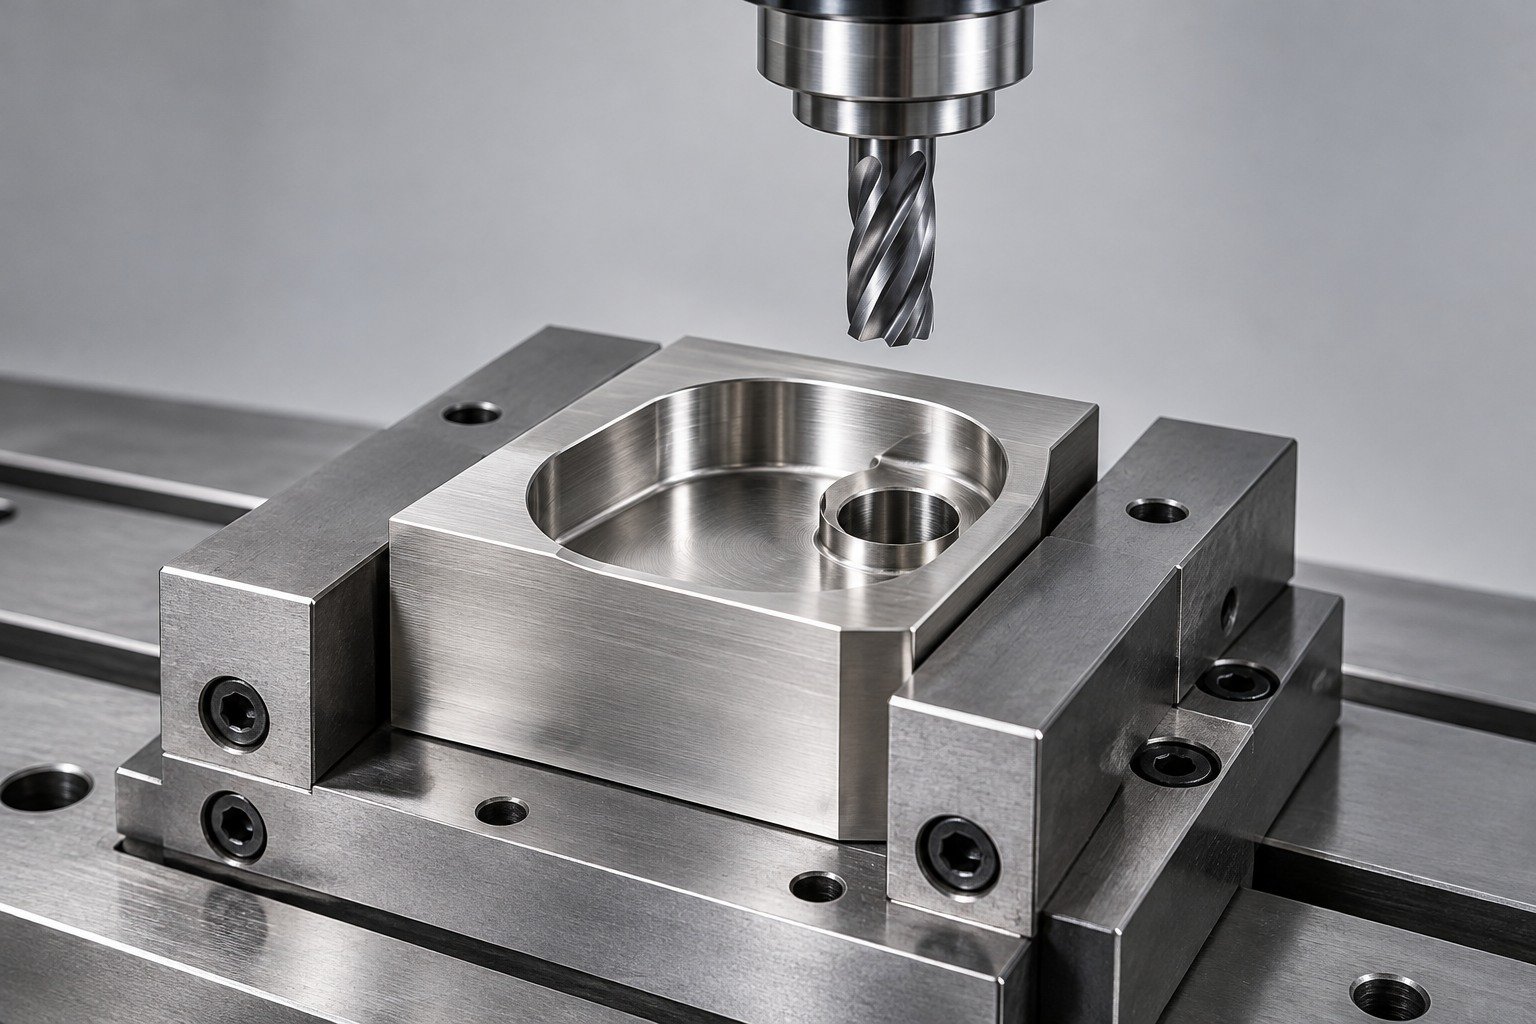
For 420 stainless steel Swiss machining and 420 stainless steel screw machine parts, retain the material variant and condition in the route.
For 420 stainless steel threaded parts, specify the standard, engagement, relief and final functional fit. Identify cross-hole burr access before release.
Swiss Machining →
For 420 stainless steel polishing, define the functional faces, appearance reference and permitted surface changes.
For 420 stainless steel passivation, agree the cleaning, treatment compatibility and verification required for the actual component.
For 420 stainless steel laser marking, identify content, location and restrictions on mating or exposed faces. Surface brightness is not evidence of corrosion suitability.
Surface Finishing Review → · Laser Marking →

01 · Variant & condition
Keep carbon variant, stock condition and final requirement on the same release.
Specify the exact standard and variant before requesting hardness. The three machining stages are illustrative, not a heat-treatment test.
A broad 420 reference minimum; it does not make all European 420-family carbon variants interchangeable.
Read the source and conditions →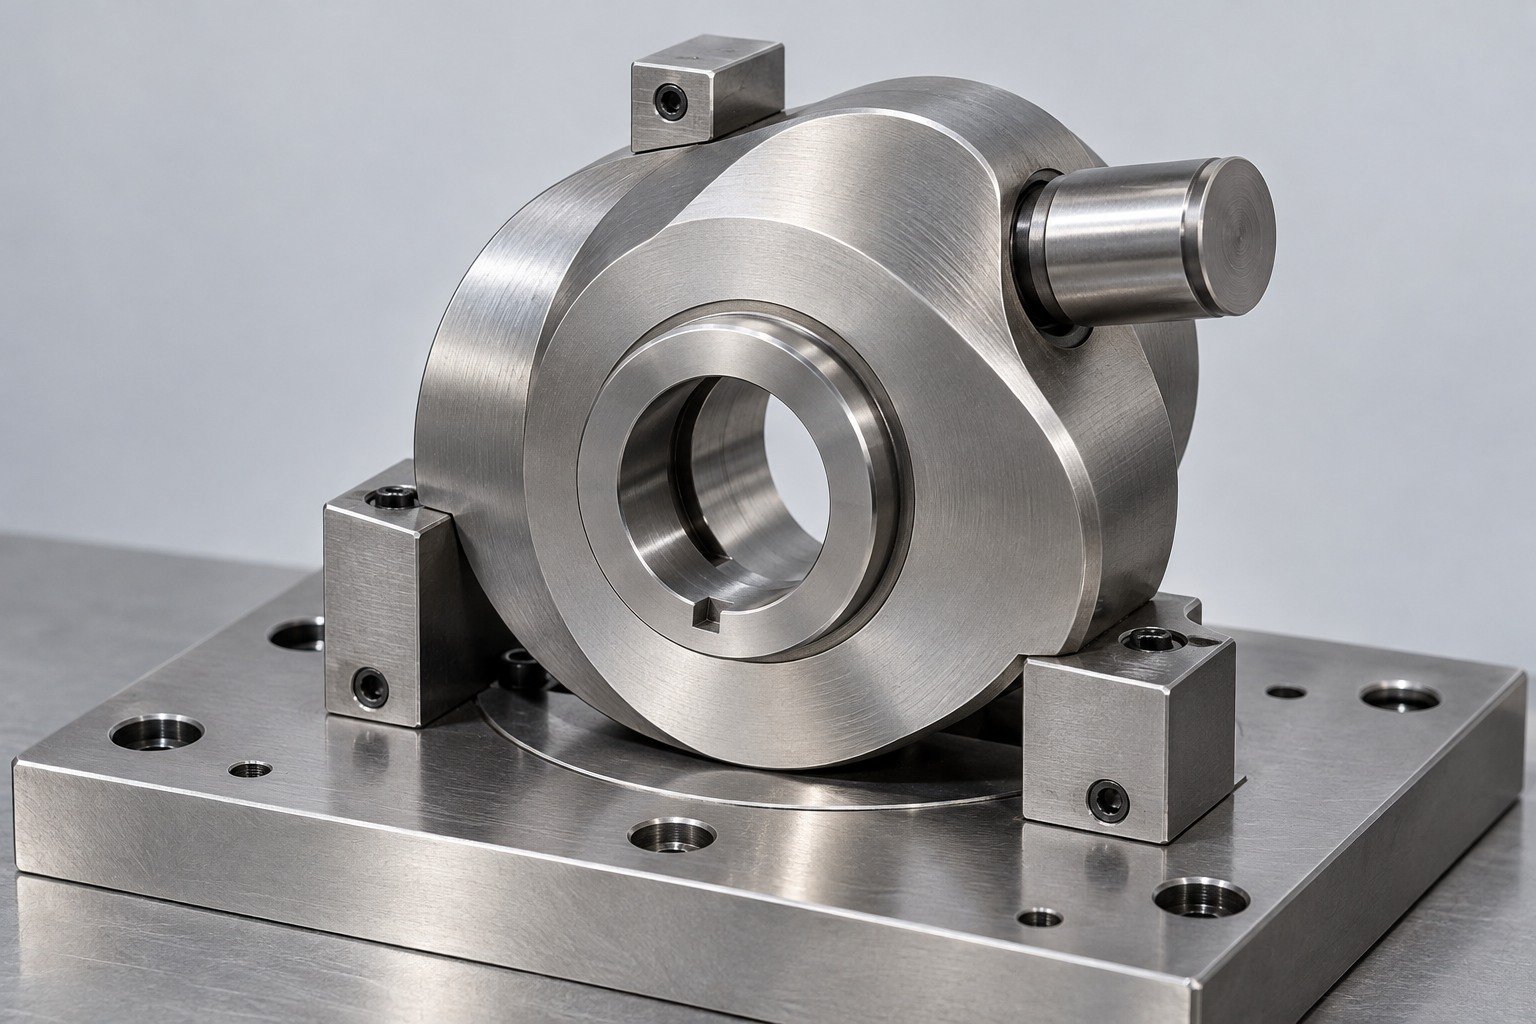
02 · Cam & datum
Connect cam geometry, journal axis and locating face to the functional requirement.
Show the eccentric feature, bore and mounting references together. Define the inspection state after the agreed thermal route.
Grade chemistry provides material context; eccentricity, runout and load acceptance come from your drawing.
Read the source and conditions →
03 · Finish allowance
Agree the sequence and any finishing allowance around heat treatment.
Identify surfaces for grinding, honing or final machining. Match allowance to the heat route and actual part geometry.
A family identifier does not prescribe one finishing allowance or hardness. Keep the complete specification on the order.
Read the source and conditions →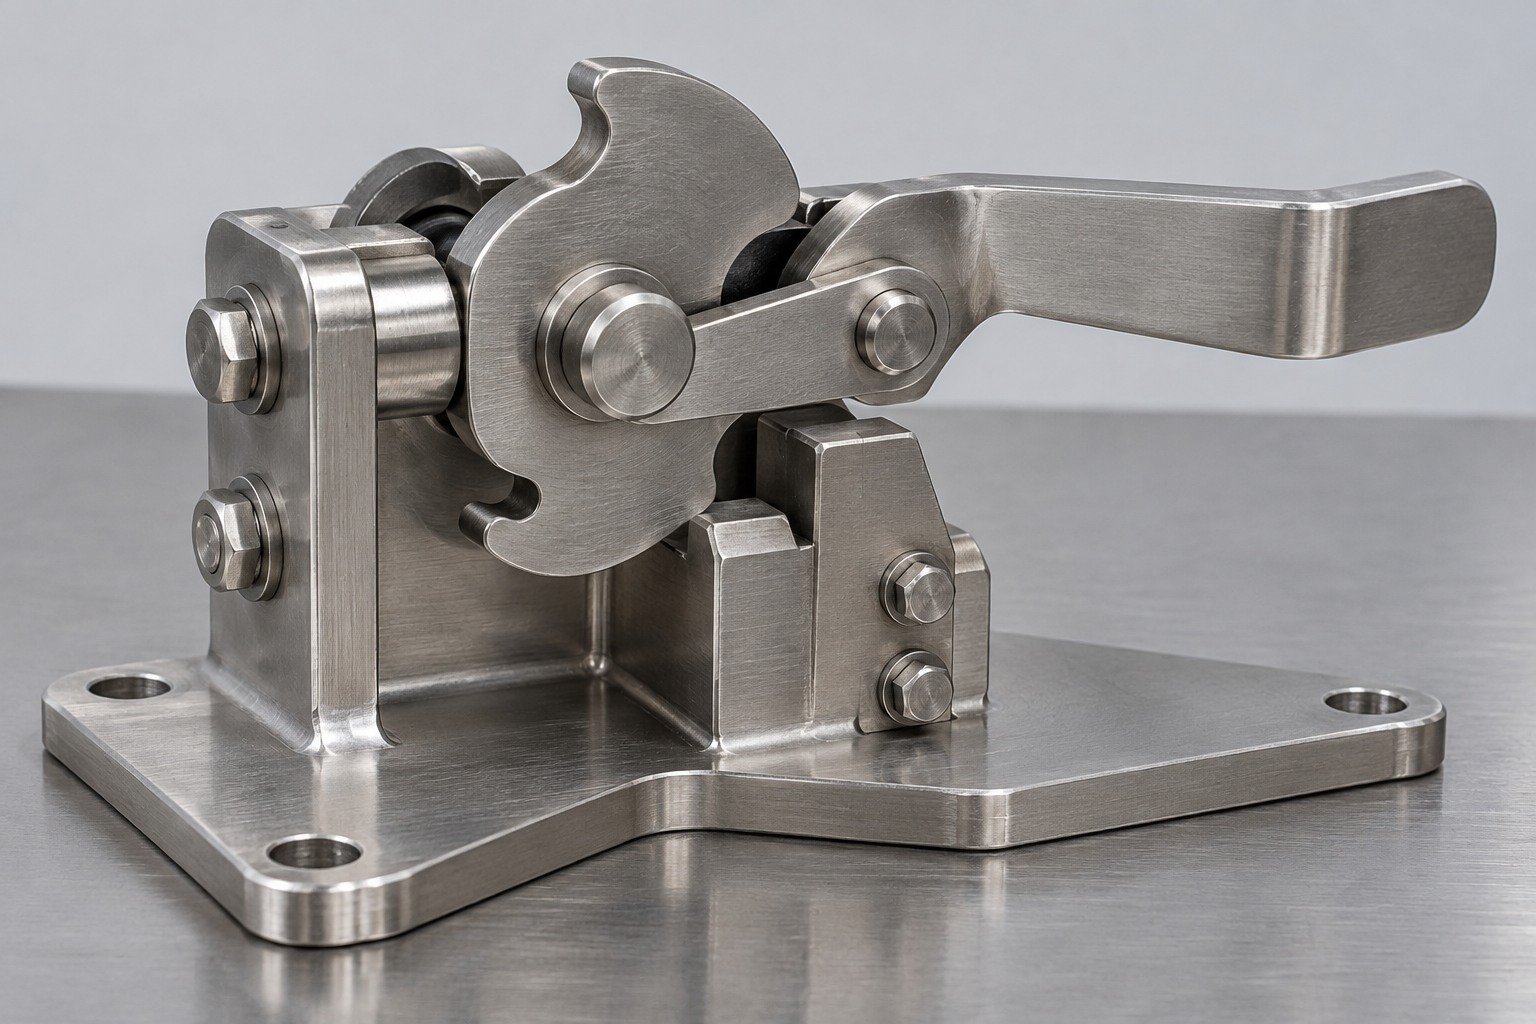
04 · Exposure & joining
Describe environment and any weld requirement before material approval.
Show the actual contact medium, temperature, cleaning and joint. Review welding and any subsequent treatment separately.
These are not blanket equivalents of every 420 requirement; compare the carbon variant and product specification.
Read the source and conditions →Exact variant, product standard and lot identity.
Specified final condition and required verification.
Journals, bores, cam faces and inspection state.
Surface, revision, exceptions and packing.

| Your comparison | Required review |
|---|---|
| 420 vs 410 stainless steel | Compare the exact carbon requirement, final condition and wear-related design need. |
| 420 vs 440C stainless steel | Keep the full grade, heat route and acceptance explicit; the names do not establish equivalence. |
| 420 vs 416 | Review machining, hardness, joining and actual exposure against the same finished drawing. |
| Corrosion-sensitive part | State medium, temperature, cleaning and retained moisture; hardness alone does not decide suitability. |
For your 420 stainless steel machining quote, compare the complete scope. When reviewing a 420 stainless steel CNC parts manufacturer, connect process, final condition and evidence to your drawing.
Material specification and stock form.
Cam faces, bores, threads and access.
Incoming state, final condition and sequence.
Finishing, cleaning and protection.
Quantity, inspection and packing.
For 420 stainless steel prototype machining, define what the sample must prove and how the final production variant and condition will be represented.
Yes, this martensitic family is magnetic. Use agreed material records to verify grade and condition; a magnet alone is insufficient.
It can corrode under unsuitable exposure or surface condition. Review the actual medium, temperature, cleaning and final state.
Welding requires a specific review because this air-hardening grade is seldom welded. Confirm procedure, thermal route and final material and dimensional acceptance.
Yes. The exact variant and treatment determine the result. Specify the required final condition and verification rather than assuming one hardness for all 420 parts.
It may be considered for cams, shafts, guide bushings and other mechanical parts where the specified material suits the design. This is not application certification.
Share the drawing, exact variant, stock form, conditions, quantity, finish and evidence requirements for a finished-part comparison.
No. The Dura examples have different typical carbon and chromium values. Retain the full specification and obtain substitution permission.
Do not assume so. 420F is a modified free-machining variation and needs separate material and application review.
For 420 stainless steel machining services, send the controlled drawing with the exact material and final acceptance.
Revision and CAD.
Variant, form and product standard.
Incoming and final state.
Fits, cam faces, threads and joints.
Prototype and repeat pattern.
Treatment, surface and inspection records.





